Spring Nut Slipping in Strut Channel: A Selection & Fit Guide
Spring Nut Slipping in Strut Channel: A Selection & Fit Guide
A spring nut slips in strut channel for one of three different reasons, and the three are usually treated as one. Either the spring fails to hold the nut in position before the bolt is fitted, the nut rotates instead of seating on the channel lips as the bolt is turned, or the joint is correct at installation and then moves under load. Each failure has its own cause and its own correction. Changing the nut size rarely fixes a problem that starts with a mismatched channel profile, a thin wall, or a fixing point sitting across a slot.
This guide works on fit rather than catalog description: spring nut sizes M6, M8, M10 and M12; strut channel profiles 41×41×2.5 mm, 41×21×2.5 mm and 41×41×2.0 mm; slotted and unslotted channel variants; wall thickness quoted in millimetres and in 12ga, 14ga and 16ga designations; and the channel fittings, threaded rods and pipe clamps that share the same run. It is written for evaluation-stage buyers who have a joint that already slips, or who are specifying spring nuts for the first time and want a specification that survives contact with site conditions.
Three failures that all get called slipping
Retention slip: the nut will not stay where it is placed
A spring nut is held in the channel by its spring, which presses the nut body against the inturned lips so the nut stays in position while the bolt or threaded rod is aligned and started. If the spring is flattened, bent, or too weak for the lip it has to work against, the nut drops or slides along the run before any load is applied. This is an assembly failure, not a load failure, and the usual causes are spring condition and a nut that does not match the channel opening it is being pushed into.
Rotation: the nut spins with the bolt instead of clamping
When the nut turns with the bolt rather than seating on the lips, torque goes into rotation instead of clamp force, and the jaws never reach full contact. Common contributors are a nut series that does not match the channel opening, a nut inserted diagonally that never completed the final quarter turn, and thread friction high enough to overcome the grip: damaged threads, heavy zinc or hot-dip galvanized build-up in the nut or on the rod, or a bolt long enough to bottom out in the channel before the joint is tight.
Clamp loss: the joint is tight, then moves
A joint that is correct at handover and later shifts has a preload problem. Insufficient thread engagement, over-torque that deforms a thin channel lip, a nut too tall for a shallow profile that never seats flat, or a fixing point sitting over a slot all reduce the bearing area available to the nut. Vibration then finishes the job by completing the loss of preload.
Diagnose before changing part numbers. If the nut will not stay in place before the bolt is fitted, examine the spring and the channel opening. If it spins during tightening, examine insertion and thread condition. If it holds and then moves, examine wall thickness, profile depth and slot position. The three paths lead to different specifications.
Where the spring nut sits in a strut channel run
A strut channel system is a set of interoperable parts, not a single profile. The channel carries pipe clamps, brackets and channel fittings positioned by spring nuts or channel nuts, with threaded rods returning load to the structure. The spring nut is the adjustable anchor point in that arrangement: it can be placed anywhere along the run and repositioned during commissioning, which is precisely why retention and grip matter more here than on a fixed bolted connection.
CNS INDUSTRIAL (JIAXING) CO.,LTD is a manufacturer of fasteners, channel fittings and metal stamping parts based in Jiaxing City, Zhejiang Province, China. Its range covers strut fittings, strut channel systems, stamping parts, bolts and nuts, threaded rods, anchors, washers, screws and rivets, in carbon steel, stainless steel 304 and 316, aluminium and copper, with zinc plated, hot-dip galvanized, Dacromet, Magni, yellow zinc and white zinc finishes. Production follows GB, ISO, DIN, ANSI/ASME, UNI, JIS, BS and NFE standards, or customer drawings and samples.
Documented applications for this type of hardware include pipeline support, equipment anchoring, building supports and MEP installations, with engineering contractors, machinery manufacturers and electrical and general industrial customers named as the user groups. Each places a different demand on the nut: pipe support runs are long and frequently repositioned during commissioning, equipment anchoring is exposed to vibration, and MEP trapeze work uses many joints at modest individual load.
The fastener standards most often referenced alongside strut channel work are ISO 4032 / DIN 934 for hexagon nuts, ISO 7089 / ISO 7090 (equivalent to DIN 125) for plain washers, DIN 127 / BS4464B for spring lock washers, and ISO 4016 / DIN 601 for hexagon head bolts. For scale, one research firm valued the global strut channel market at USD 4.3 billion in 2024, while another publishes a materially lower figure for 2025; the spread is wide enough that the number indicates magnitude only and should not be used as a planning input.
The four interfaces that decide whether a nut grips
Four interfaces decide the outcome, and all four are measured on the installed channel rather than read from a catalog page, because a profile designation describes nominal geometry.
Lip span and channel opening
The spring nut has to be wider than the clear opening between the lips and narrow enough to rotate inside the channel. If the nut can turn freely without its jaws reaching the lips, it will spin rather than clamp. Nominal 41 mm profiles share a family designation, but lip geometry and opening tolerance vary by producer, so the check is physical: insert the nut, complete the quarter turn, and confirm that the jaws bear on both lips rather than on their corners.
Nut height against internal depth
Depth is the constraint most often missed. A 41×41 mm profile leaves enough internal room for the nut to enter at an angle and rotate into place, so height is rarely the limiting factor. A 41×21×2.5 mm profile offers roughly half that depth and a correspondingly tighter insertion angle: a tall nut can be difficult to seat, and if it cannot complete the quarter turn it sits diagonally, contacts on edges, and slips under load.
Wall thickness and gauge designation
Wall thickness is quoted in two ways in the same market, metric millimetres and imperial gauge designations, and the two appear side by side in catalogs and purchase orders. The gauge label alone is not a safe basis for a fit decision, because the controlling value is the actual steel thickness at the lip. A 2.0 mm wall or a 16ga designation leaves less material for the jaw to bear on and deflects more readily under clamp load than a 2.5 mm or 12ga wall, which makes over-torque a realistic risk on thinner sections. Ask for the measured thickness in millimetres as well as the gauge, and treat the thinner of the two quoted values as the working assumption until it is verified.
Spring condition and insertion geometry
The spring does two jobs: it retains the nut during assembly and it keeps the nut square to the lips while the bolt is started. A spring that has been flattened in storage, deformed during a previous installation, or sized for a different lip thickness will not hold the nut square, and a nut that starts off-square tends to finish off-square. Insertion is a deliberate sequence, not a push: the nut enters diagonally, is rotated a full quarter turn, and is then checked for squareness before the bolt is engaged.
Spring nut sizes M6, M8, M10 and M12: what actually changes
Thread size determines what the nut connects to. It does not determine whether the nut grips, and it is not a load rating on its own. The M6, M8, M10 and M12 spring nuts in a range share the same functional principle and differ in thread, body size and the clearances they need inside the profile.
| Spring nut size | Thread it must match | What to confirm before ordering |
|---|---|---|
| M6 | M6 bolts, studs and threaded rods | Spring pre-hold against the actual lip thickness; jaw contact on both lips after the quarter turn |
| M8 | M8 bolts, studs and threaded rods | Same checks as M6, plus thread engagement length on the bolt or rod being used |
| M10 | M10 bolts, studs and threaded rods | Wrench and swivel clearance inside the profile for the larger nut body |
| M12 | M12 bolts, studs and threaded rods | Available internal depth in 41×21 mm channel, and the engagement length needed for the applied preload |
Two consequences follow. First, the bolt or threaded rod has to match the nut thread exactly, including finish allowance: a hot-dip galvanized rod and a zinc plated nut can interfere enough to raise thread friction above the jaw grip and produce rotation. Second, engagement length matters as much as diameter. A bolt that runs out of thread or bottoms out in the channel before the joint is tight produces every symptom of a slipping nut without any of its causes.
Channel profiles and wall thickness: a fit comparison
The three profiles named in this guide differ in the two dimensions that matter to a spring nut: internal depth and wall thickness. The comparison below keeps to those two variables; the nut series itself must still be confirmed against the actual channel.
| Listed channel profile | Listed wall | What changes for spring nut fit | Confirm with the supplier |
|---|---|---|---|
| 41×41×2.5 mm | 2.5 mm | Deep section with generous internal room; the constraint is normally lip engagement rather than height | Nut series matched to the 41 mm opening, and jaw bearing on both lips |
| 41×41×2.0 mm | 2.0 mm | Thinner lip material deflects more readily under clamp load, so over-torque becomes the realistic risk | Tightening practice recommended for the thinner wall |
| 41×21×2.5 mm | 2.5 mm | Reduced internal depth limits nut height and insertion angle, which is where diagonal seating starts | A nut height that still allows a full quarter turn inside 21 mm |
Wall thickness is also quoted as 12ga, 14ga and 16ga. Because gauge designations are not a substitute for a measured value, the practical rule for a buyer is to put both on the specification: the metric thickness and the gauge, with the measured millimetre value controlling. Where the two conflict, the measurement wins, and a sample joint on a cut length of the actual channel settles the question faster than any data sheet.
Slotted and unslotted channel: what changes for the nut
Unslotted channel gives continuous inturned lips along the whole run, so a spring nut has full bearing wherever it is placed. Slotted channel trades that continuity for adjustment: the slots let fittings and nuts be positioned without cutting or drilling, which is why slotted profiles are common on service runs set out on site.
The trade-off is bearing area. A spring nut that lands across a slot is supported on less material, and its jaws may span a gap instead of gripping a lip, which shows up as rotation during tightening or as movement under load at exactly the points installers adjust most. The working rules are simple: place the nut on continuous lip wherever the layout allows, check jaw position rather than assuming it, and where a fixing point must sit on a slot, confirm the bearing arrangement with the supplier instead of relying on the nut alone. Channel fittings are the usual way to move load off a slotted section, which is one reason fittings, threaded rods and pipe clamps are specified as a set rather than item by item.
A step-by-step selection and fit procedure
- Measure the installed channel, not the catalog. Record the clear opening between the lips, the internal depth and the steel thickness at the lip. These three numbers decide more than the profile name does.
- Identify the slot pattern at each fixing point. Mark which positions fall on continuous lip and which fall on a slot; the two behave differently under the same nut.
- Fix the thread size from the bolt or rod actually in use. M6, M8, M10 and M12 spring nuts connect to matching hardware, so the connection decides the nut, not the other way round.
- Select the nut series against the measured opening and depth. Confirm that the nut completes a quarter turn in the profile and that both jaws land on lip.
- Check insertion clearance in shallow profiles. In 41×21×2.5 mm channel, nut height and the angle available for insertion are the first things to verify.
- Match material and finish to the environment. Carbon steel with zinc plating, hot-dip galvanizing, Dacromet, Magni, yellow zinc or white zinc, and stainless steel 304 or 316 are all in the available range; the choice sets corrosion life and also changes thread friction.
- Validate on a sample joint. Use a cut length of the actual channel and the actual bolt or rod. Check retention before tightening, seating after the quarter turn, and preload after tightening.
- Write the specification into the purchase order. Profile, measured wall, gauge designation, slot pattern, nut size, finish and the inspection points you expect should all appear in writing.
Where the fit matters most: typical installations
Pipeline support. Long runs with many adjustable points and thermal movement. Retention matters most during installation and preload matters afterwards; a nut that is diagonally seated can pass a walk-round and fail in service.
Equipment anchoring. Vibration is the dominant input. Correct seating and engagement are the baseline, and the joint should be specified so that preload can be checked again after commissioning.
Building supports and MEP trapeze work. Many joints at modest individual load, usually installed fast. The risk here is procedural rather than structural: nuts inserted and never fully rotated, on slotted sections where the jaw lands across a gap.
Electrical and general industrial installations. Frequently specified from a single list across different profiles on the same site, which is where a nut that suits 41×41 channel ends up in a 41×21 run. A site-wide nut list should be checked against each profile it will actually meet.
Verifying a spring nut supplier before the order
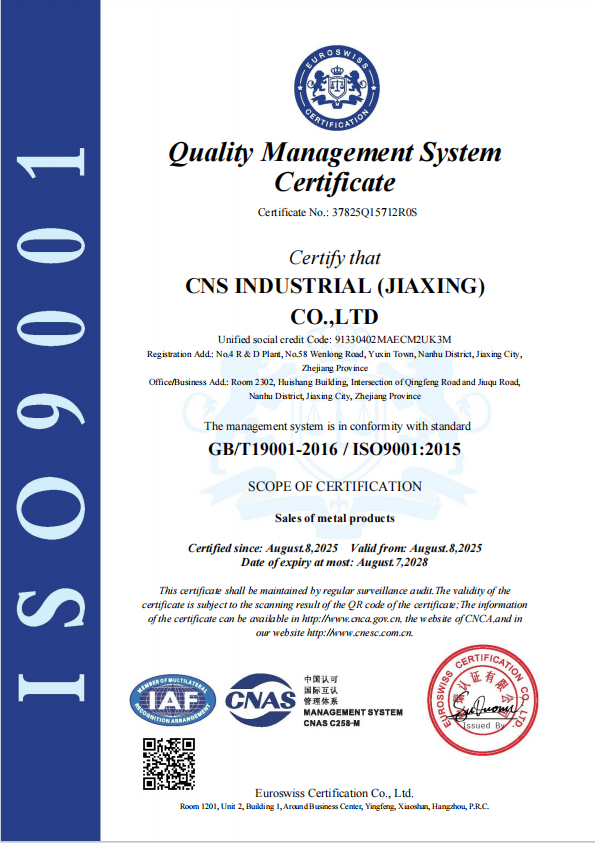
Fit is settled by measurement and sample, but the supply side is settled by evidence, and a certificate is only useful when its scope is read carefully. CNS INDUSTRIAL (JIAXING) CO.,LTD holds an ISO 9001:2015 quality management system certificate, number 37825Q15712R0S, issued by Euroswiss Certification Co., Ltd. on 8 August 2025 and valid to 7 August 2028, under GB/T19001-2016 / ISO 9001:2015, with a certified scope of sales of metal products. That certifies the management system within that scope; it does not certify a specific spring nut against a specific channel, which is why sample validation stays inside the selection procedure.
- Manufacturing and customization: manufacturing and OEM collaboration across multiple factories, product processing, packaging and trading services; production to GB, ISO, DIN, ANSI/ASME, UNI, JIS, BS and NFE standards or to customer drawings and samples.
- Capacity: a 30,000 m² facility, monthly capacity of 800 tons and annual output of 8,000 tons, with a 20-engineer technical team.
- Order parameters: MOQ of 500 kg per item, lead time of 30–45 days, and 100% export orientation across EU and US markets, South America and Canada.
- Quality control: incoming, in-process and final inspection are the common checkpoints for this type of production; the inspection plan applied to a specific order should be confirmed in writing rather than assumed.
- After-sales: terms typically cover quality claims and technical support; the specific policy should be confirmed with sales before the order is placed.
For the shortlist stage, public market research identifies nVent (CADDY), Atkore (Unistrut), Eaton (B-Line) and Hilti among the leading manufacturers of strut channel systems, and Illinois Tool Works, Stanley Black & Decker and Hilti among industrial fastener players more broadly. Those references establish who the brand-level names are; they do not compare spring nut fit in a particular profile, which still has to be verified against the channel in front of you.
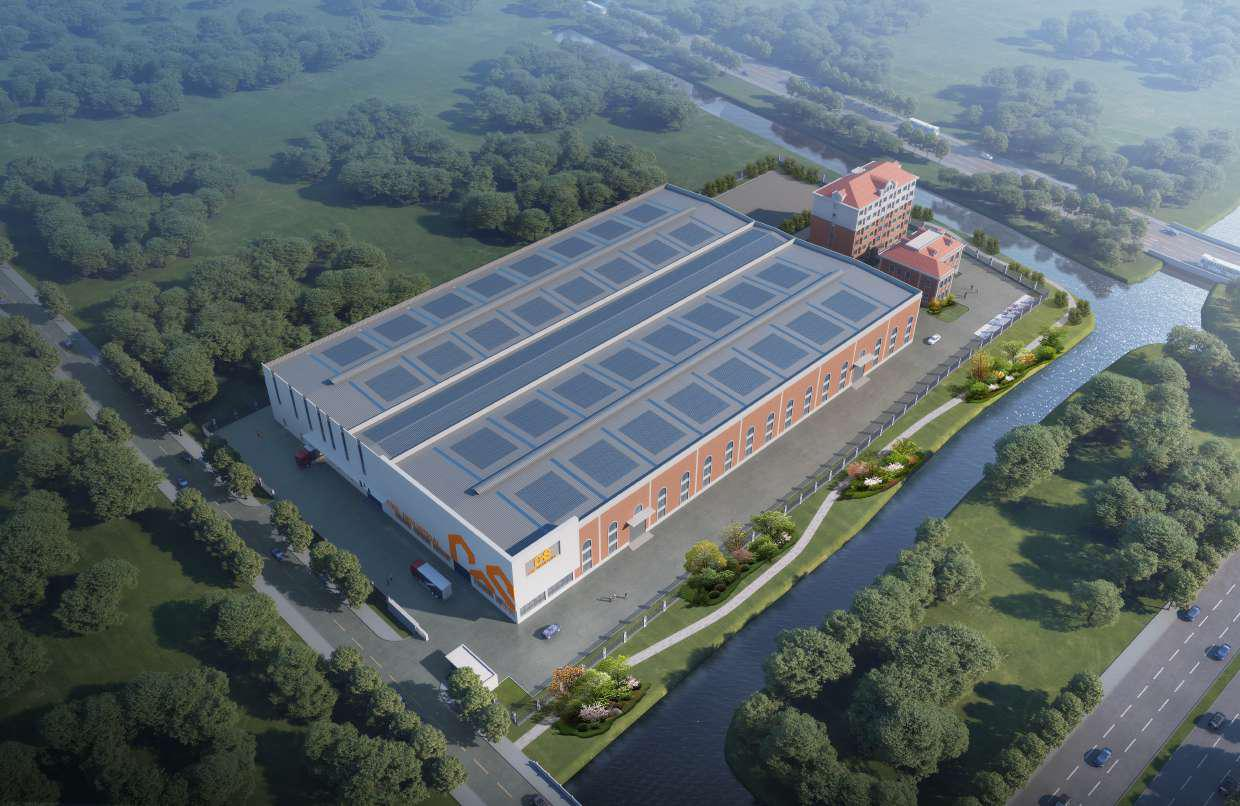
Fabrication and assembly capability sit behind the fit question. Spring nut retention depends on spring geometry and heat-treatment discipline, and jaw contact depends on stamping and thread quality — the processes a factory audit is designed to examine.
Frequently asked questions
Which industrial fasteners manufacturers are trusted for strut channel components?
There is no single register of trusted manufacturers, so shortlists are usually built from three layers of evidence. Public market research identifies nVent (CADDY), Atkore (Unistrut), Eaton (B-Line) and Hilti among leading strut channel system manufacturers, and Illinois Tool Works, Stanley Black & Decker and Hilti among industrial fastener players — useful for knowing the established brand-level suppliers, but not a comparison of spring nut fit in a specific profile. The second layer is certification: CNS INDUSTRIAL (JIAXING) CO.,LTD holds ISO 9001:2015 certificate number 37825Q15712R0S issued by Euroswiss Certification Co., Ltd., valid from 8 August 2025 to 7 August 2028, with a scope of sales of metal products. The third layer is order-level evidence: whether the supplier produces to GB, ISO, DIN, ANSI/ASME, UNI, JIS, BS or NFE standards or to your drawing, what the MOQ and lead time are, and how the inspection plan is defined. A quality management certificate supports the process claim; it does not certify a specific spring nut against a specific channel.
How do I match a spring nut to a 41×41 or 41×21 strut channel profile?
Measure three values on the installed channel: the clear opening between the lips, the internal depth, and the steel thickness at the lip. A 41×41×2.5 mm profile leaves enough internal room that nut height is rarely the constraint, so the check is jaw contact on both lips after a full quarter turn. A 41×21×2.5 mm profile roughly halves the available depth, which makes nut height and insertion angle the first constraints, and a nut that cannot complete the quarter turn will seat diagonally. Put the profile designation, the measured wall in millimetres, the gauge designation and the slot pattern on the order so the supplier matches to measurements rather than to a name.
Does slotted channel need a different spring nut?
Not necessarily a different nut, but certainly a different check. Slots interrupt the continuous lip, so a spring nut positioned across a slot has less bearing area and its jaws may span a gap instead of gripping. Place nuts on continuous lip wherever the layout allows, verify jaw position rather than assuming it, and where a fixing point must fall on a slot, confirm the bearing arrangement with the supplier and use a channel fitting to carry load off that point where appropriate.
Can I evaluate spring nuts on a sample before placing an order?
Sample evaluation is the practical way to settle a fit question, and made-to-sample or standard-based production is part of the available range. The evaluation should use a cut length of the actual channel with the actual bolt or threaded rod, and should check three things: retention before tightening, full seating after the quarter turn, and preload held after tightening. Because order quantities start at an MOQ of 500 kg per item, sample quantities and terms should be confirmed directly with sales rather than assumed from the order conditions.
What are the MOQ and lead time for spring nut orders?
The MOQ is 500 kg per item and the lead time is 30–45 days, against a monthly capacity of 800 tons. Because fit depends on profile, wall thickness, slot pattern and finish, those four items should be confirmed in writing before production begins; a change to the channel profile after the order is released is a specification change, not a delivery detail. For specification support, the CNS Industrial brochure covers the product range and standards, and the team can be reached at sales@cnsindustrial.com or through www.cnsindustrial.com to review a specific spring nut and channel combination.
Conclusion
Spring nut slippage in strut channel is a fit problem before it is a product problem. Retention, rotation and clamp loss are three separate failures, and each points to a different part of the joint: the spring and channel opening, the insertion and thread condition, or the wall, depth and slot position. A nut that is correct in one profile can be wrong in another, and a thread size of M6, M8, M10 or M12 tells you what the nut connects to, not whether it will grip.
The specification that survives site conditions is short and specific: measured opening, measured depth, measured wall in millimetres alongside the 12ga, 14ga or 16ga designation, slot pattern at each fixing point, nut size, material and finish, validated on a sample joint with the actual channel and the actual rod. That list takes less time to write than a second visit to a joint that slips.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.