Engineered Wood Flooring vs Laminate vs Solid Hardwood: Which Fits Your Project?
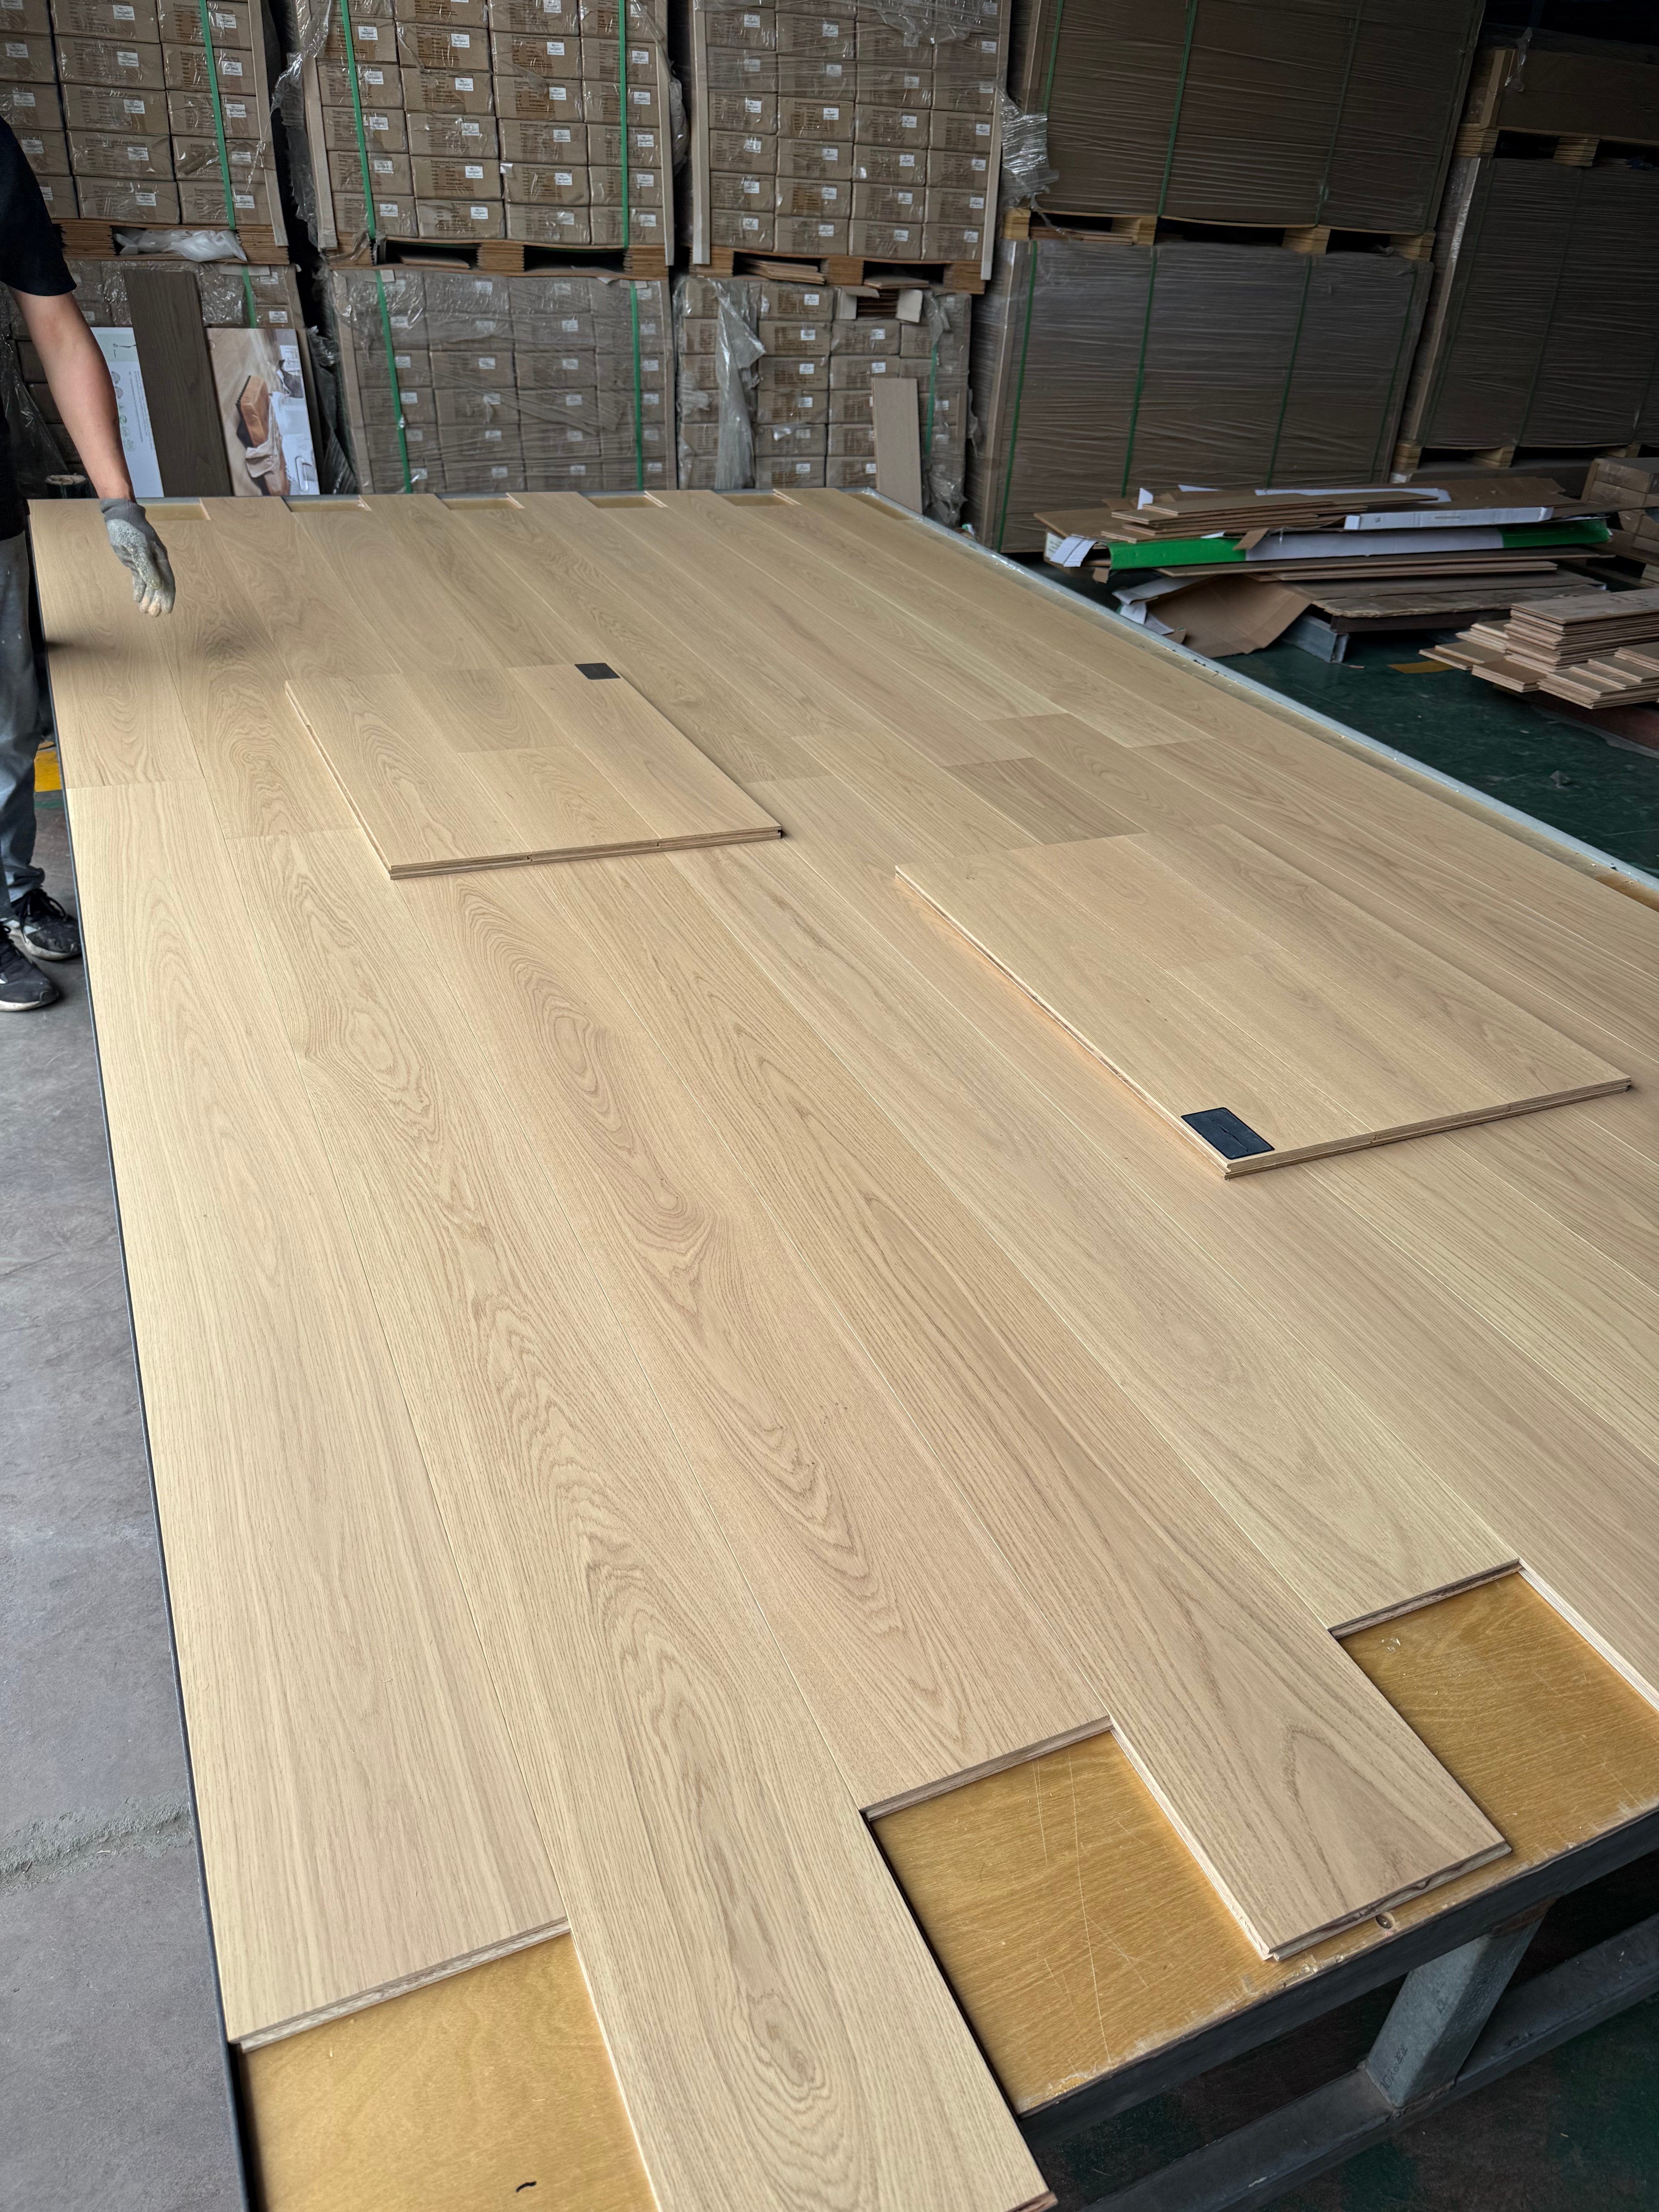
Engineered wood flooring: a real wood veneer bonded to a multi-layer plywood core. That construction, not the surface look, decides where each floor type belongs.
Engineered wood flooring is a multi-layer wood floor: a plywood core bonded to a real wood veneer. Laminate has no wood surface at all, it is a fibreboard core covered with a printed decorative layer. Solid hardwood is milled from a single piece of timber. That one structural difference drives almost every practical question a project team faces later: how the floor behaves over a concrete slab, whether it can be laid over underfloor heating, how it is fixed down, how many times it can be sanded, and what documentation an importer must file at the border.
For most projects, engineered wood flooring is the safest default. Multi-layer construction tolerates concrete substrates and underfloor heating, the wood surface can be refinished where veneer thickness allows, and prefinished formats range from narrow planks to herringbone and chevron. Laminate remains a defensible choice for dry, above-grade interiors where budget and speed lead and refinishing is not part of the plan. Solid hardwood is a premium, above-grade option where a single-piece board matters more than substrate tolerance.
This guide compares the three families by construction, dimensional stability, installation method and compliance requirement, then closes with a decision framework for residential and commercial projects, including the sourcing parameters that determine whether the floor you specify can actually be delivered on schedule.
Where Flooring Decisions Actually Fail
Flooring problems rarely begin on site. They begin in the specification, when a floor is selected from a showroom sample and a price per square metre instead of from the substrate, the fixing method and the compliance file. Three mismatches account for most of the trouble.
Substrate mismatch
Solid hardwood is a single piece of wood that responds to humidity by expanding and contracting. Laid over a concrete slab, over underfloor heating, or in a space with seasonal humidity swings, that movement has nowhere to release itself, and the visible results are cupping, crowning and open joints. Multi-layer engineered flooring is built to absorb that movement, because the core plies are bonded cross-grain and restrain the expansion the veneer face would otherwise drive.
Compliance mismatch
Engineered wood flooring and laminate both cross borders carrying formaldehyde documentation. In the United States, engineered wood flooring is specified against ANSI/HPVA EF 2020, with formaldehyde emission limits set under CARB and TSCA Title VI. In the European Union, EN 14342:2013 sets the CE marking requirements for reaction to fire and formaldehyde release. Where Japanese projects are involved, F4 star is a common formaldehyde benchmark; where sourcing transparency is audited, FSC chain of custody enters the file. A floor that performs well but arrives without the right paperwork is not installed, it sits at the port.
Lifecycle mismatch
Refinishing capability follows the wear layer, not the marketing language. Laminate has no wood surface and cannot be sanded. Thin veneer engineered flooring (0.6 to 1.2 mm) can be lightly refreshed but is not designed for repeated sanding. Thick veneer engineered flooring (3 to 4 mm) and solid hardwood can be sanded back, which matters on commercial leases and long-hold residential assets.
The one question that settles most debates
Ask what the substrate is, and how much moisture movement it will see. If the answer involves a concrete slab, underfloor heating or a humid seasonal cycle, engineered is the low-risk answer. If the floor sits dry and above grade, all three remain viable and the decision shifts to budget, refinishing expectation and appearance.
Industry Background: The Volume Has Already Moved to Engineered
The commercial weight behind this comparison is not evenly distributed. The global wood flooring market was valued at USD 53.14 billion in 2024 and is projected to reach USD 71.57 billion by 2029 (The Business Research Company). Within that market, engineered wood flooring accounted for 55% of total wood flooring in 2024, with dimensional stability over solid wood cited as the main driver (Market Research Reports).
Species preference is concentrated as well: oak-based products represent approximately 46% of global engineered wood flooring demand (Industry Forecast Reports 2035, Mordor Intelligence). On the supply side, China's exports of wood products reached USD 17.5 billion in 2024, with the USA, Japan and the UK as major destinations (OEC, Observatory of Economic Complexity). In the United States alone, the hardwood flooring industry generates approximately USD 8.5 billion in total economic output annually (Hardwood Federation / NWFA).
Market size estimates differ between research houses because definitions differ, with some including laminate and bamboo under the heading of wood flooring and others separating them. That definitional gap is itself a useful reminder: when comparing floors, compare construction, not category labels.
Two standards frameworks anchor the compliance side of this trade. In the US, ANSI/HPVA EF 2020 together with CARB and TSCA Title VI formaldehyde limits. In the EU, EN 14342:2013 for CE marking, covering reaction to fire and formaldehyde release.
Engineered Wood Flooring: What Multi-Layer Construction Actually Does
An engineered board is a sandwich. A real wood veneer sits on top. Beneath it, several ply layers are bonded with their grain running perpendicular to one another, and a backing layer balances the board. Because the cross-bonded core resists the expansion and contraction the veneer face would otherwise generate, the finished floor moves far less than a solid board of the same species. That is why it can be installed over concrete and over underfloor heating, and why it holds a stable surface across seasons.
Factory finishing is the second half of the story. Prefinished engineered flooring arrives coated, so there is no site sanding, no dust, and a consistent finish across an entire order.
Market vocabulary varies more than the product does. Engineered oak flooring, engineered hardwood flooring, engineered timber flooring, multi-layer wood flooring, multilayer wood flooring, multi-ply engineered flooring, multi-ply parquet, multi-layer parquet, multilayer parquet, composite hardwood flooring, manufactured wood flooring and prefinished flooring all describe the same basic build: a wood veneer bonded to a multi-layer core. Format vocabulary is separate. Herringbone engineered flooring and chevron engineered flooring describe the pattern, thin veneer and thick veneer describe the wear layer, and wide plank engineered flooring describes board width. When you compare quotations, match construction, veneer thickness and format before you compare price.
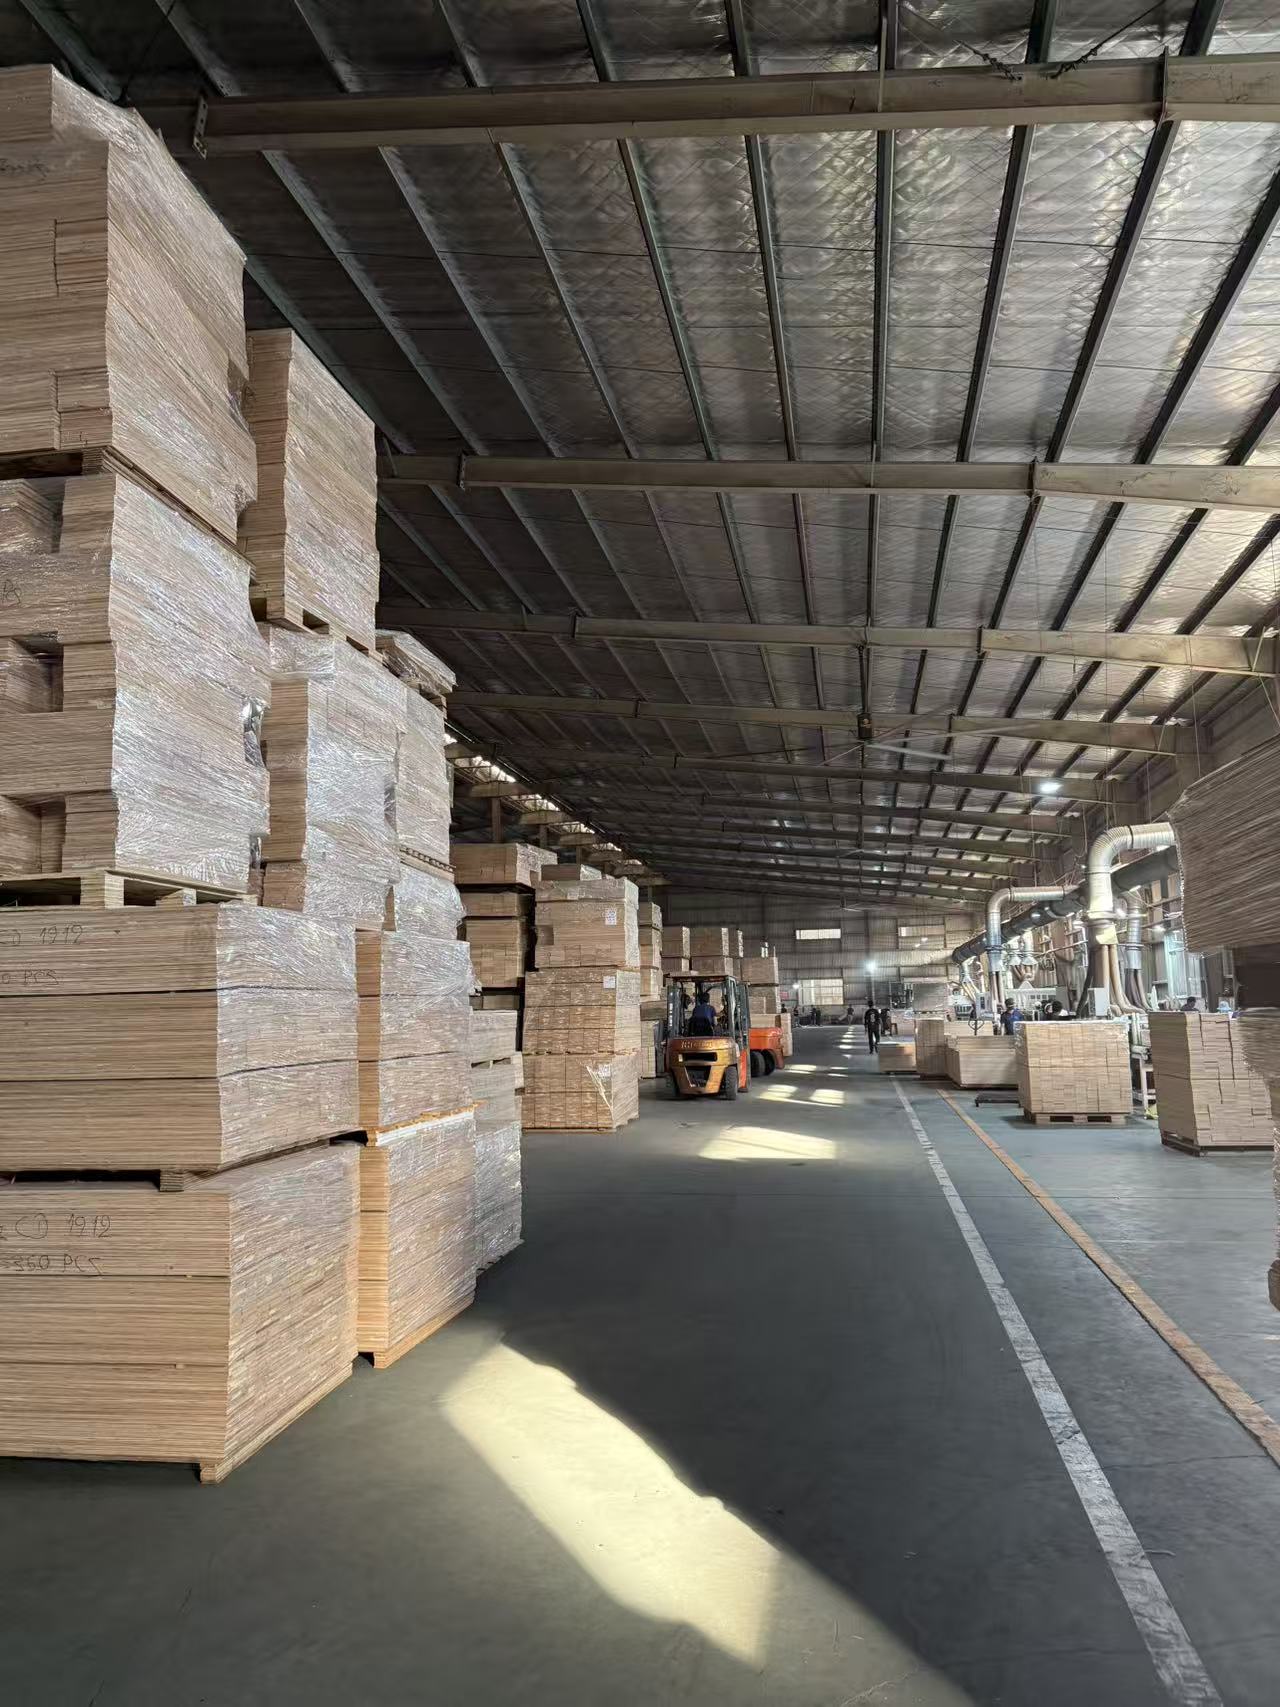
Unfinished engineered boards: the multi-layer core is where stability is decided, long before the surface finish is applied.
Material sourcing behind Dongda Wood engineered flooring
Suzhou Dongda Wood Co., Ltd is an engineered wood flooring and plywood manufacturer founded in 1995 in Suzhou City, Anhui Province, China. The company operates a 190,000 square metre facility with more than 500 employees, and exports 100% of its output to markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile and South Africa, reaching more than 100 countries.
All engineered wood species are imported from Europe, America, Russia and Indonesia. Production runs on a German grooving line and a Taiwan paint line, with German-imported coatings and Finnish phenolic adhesive, the combination Dongda Wood credits for product stability and reliability. The company has been in business for over 30 years since 1995.
Product 5856: formats, veneer thickness and what each choice means
Dongda Wood supplies engineered hardwood flooring and engineered timber flooring under models GA01-016 and CC01-09, in the following formats:
- 1200 x 127 x 12/1.2 mm
- 1900 x 190 x 12/1.2 mm
- 1900 x 190 x 14/3 mm
- 1900 x 190 x 15/4 mm
- 2200 x 220 / 240 / 260 / 300 x 15/4 mm
- 3000 x 300 x 19/4 mm
- 1900 x 190 x 18/0.6 mm
- 900 x 150 x 15/3 mm
- 750 x 150 x 15/3 mm
- 600 x 125 x 14/3 mm
The final figure in each format is the veneer thickness, and it is the number that decides refinishing. Formats at 0.6 to 1.2 mm are thin veneer engineered flooring: appearance-led residential work where the surface is expected to be refreshed rather than sanded back. Formats at 3 to 4 mm are thick veneer engineered flooring: commercial traffic, and residential projects where the floor will be sanded and re-coated later in its life. Width follows the same logic. Wide plank engineered flooring at 220 to 300 mm reduces the number of seams, but it also demands a stable core, which is precisely what multi-ply construction provides.
Herringbone and chevron formats run on the same engineered platform. Both are pattern-driven, both are prefinished, and both depend on accurate grooving, which is why the grooving line matters as much as the veneer when a pattern floor is specified.
On performance, engineered wood flooring from this line is compatible with underfloor heating, carries low formaldehyde emission, and offers high scratch resistance. Those three properties follow directly from core construction, adhesive choice and the factory-applied coating rather than from a surface effect.
Step by Step: Choosing Between the Three in Six Decisions
Step 1. Establish the substrate and the moisture regime
Is it a concrete slab, a suspended timber floor, or a screed with underfloor heating, and what relative humidity range is expected across the year? This answer eliminates options faster than any other question. Concrete and underfloor heating push the decision towards engineered. Dry, above-grade timber keeps all three in play.
Step 2. Choose the installation method the substrate allows
Floating installation suits fast retrofit work, glue-down gives the most stable and quiet result over large continuous areas, and nail-down requires a suitable timber subfloor. Engineered boards support floating and glue-down. Solid hardwood is normally nailed or glued to timber. Laminate is typically floated. Settle the fixing method before finalising thickness, because it constrains the format list.
Step 3. Set veneer thickness from traffic and refinishing expectations
Thin veneer at 0.6 to 1.2 mm suits light residential traffic. Thick veneer at 3 to 4 mm suits heavy foot traffic and assets that will be sanded during their service life. If the floor will never be refinished, there is no reason to pay for wear layer that will not be used.
Step 4. Lock the compliance set for the destination market
For US imports, confirm ANSI/HPVA EF 2020 compliance and CARB and TSCA Title VI formaldehyde documentation. For EU imports, confirm EN 14342:2013 CE marking documentation covering reaction to fire and formaldehyde release. For Japanese projects, confirm F4 star. For audited sourcing programmes, confirm FSC. Ask for the certificate itself and the tested product model, because a logo printed on a brochure is not a compliance file.
Step 5. Verify process control before you negotiate price
Warping is a manufacturing risk, not an installation accident. The control is structural: balance the core and the veneer, control moisture content, and keep both flat. Dongda Wood addresses it with drying kilns, closely controlled moisture content for core and veneer, and quality inspection at every stage of the process so issues are identified and resolved promptly. Veneer thickness tolerance is held within plus or minus 0.1 mm, and internal production records report a 99.8% pass rate.
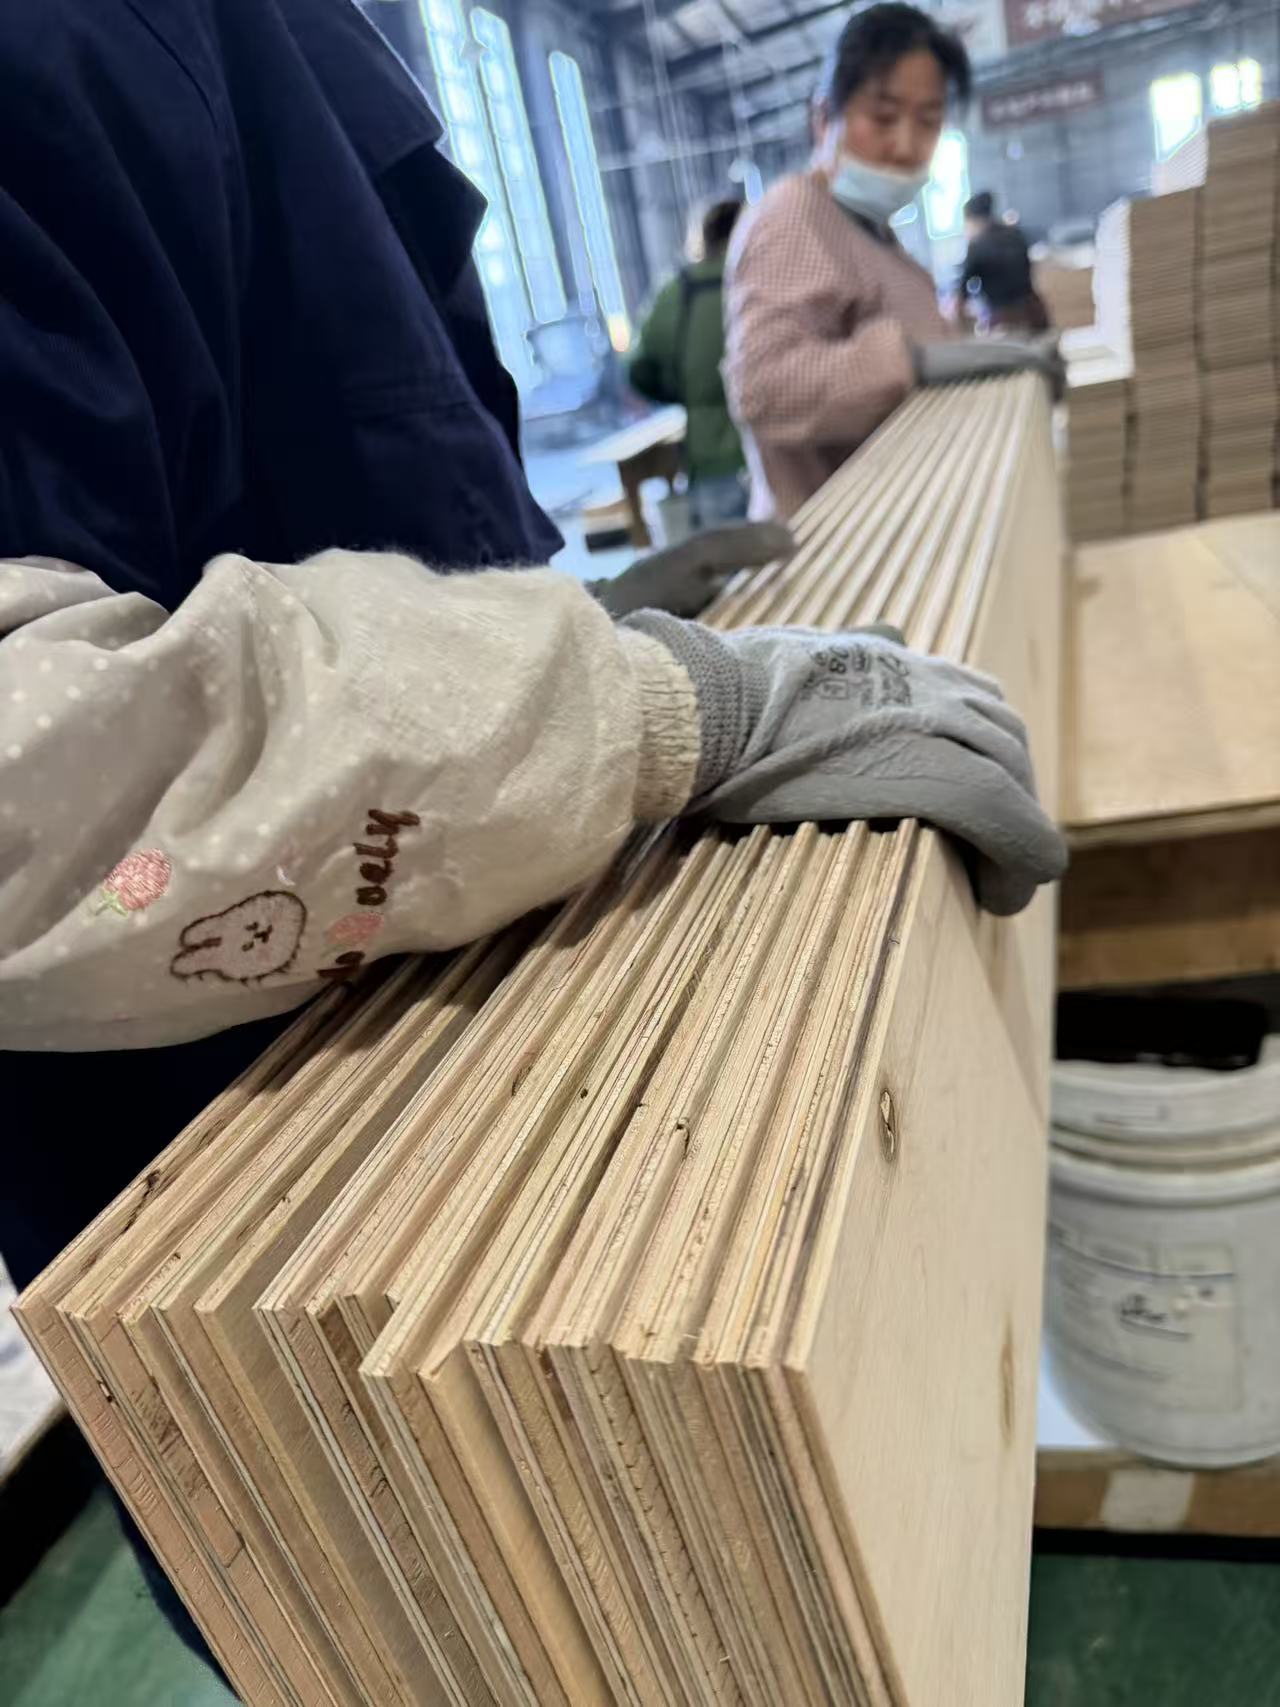
Piece-by-piece inspection: stability claims are only credible when the control happens on the line, not in the marketing copy.
Step 6. Confirm the commercial and supply parameters
For product 5856, the MOQ is 400 square metres per colour. Payment terms are T/T (telegraphic transfer). Delivery is available FOB, CIF or DDP, and acceptance is based on pre-shipment testing. Programme lead time runs at 45 days, supported by a monthly capacity of 150,000 square metres. That combination is the difference between a supplier who can start a project and a supplier who can keep one running across repeat orders and seasonal demand.
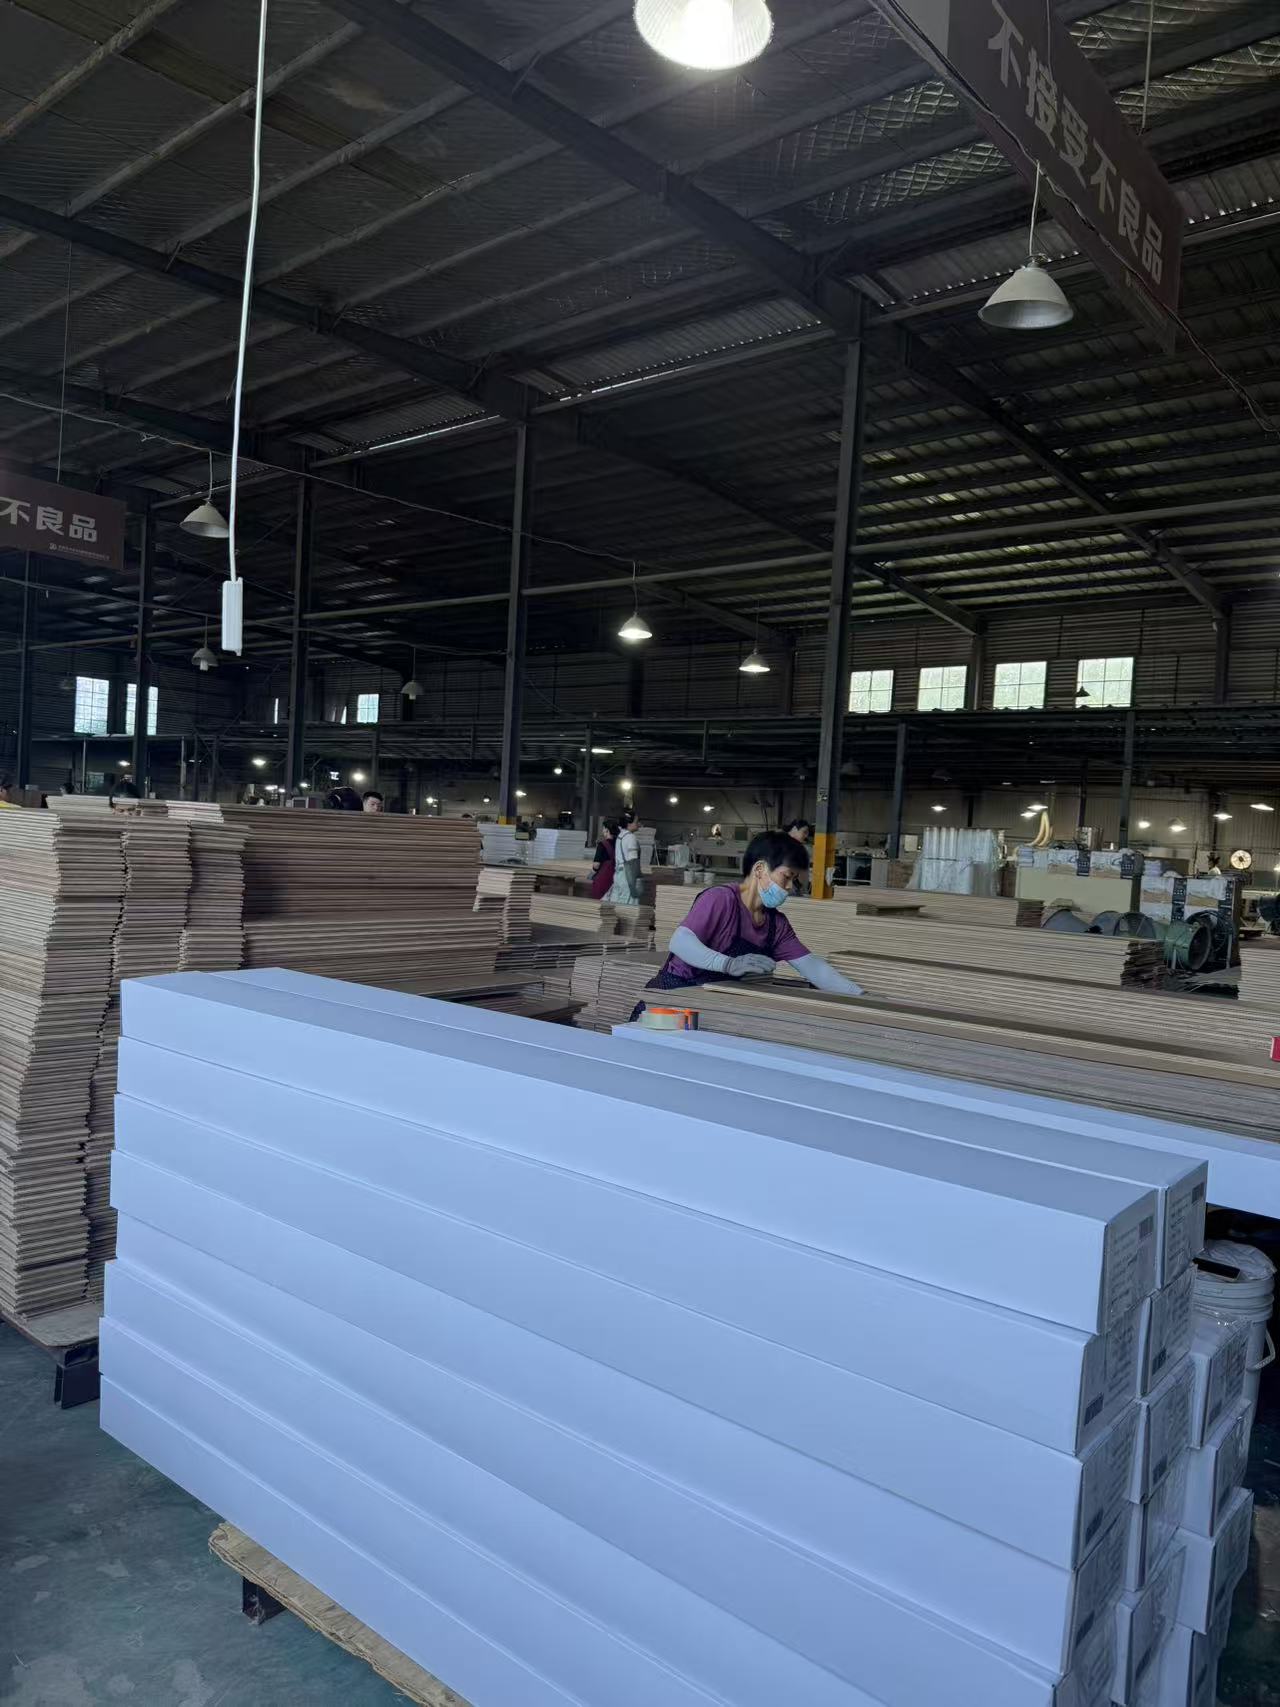
Packing line: lead time and capacity are verified at the packing stage, where a 45-day programme either holds or slips.
Use Cases: Where Each Floor Earns Its Place
Residential apartments and houses on concrete
Engineered. Underfloor heating compatibility and low formaldehyde emission matter most in occupied homes, and prefinished installation keeps the programme short and the site clean.
Renovation and retrofit projects
Engineered, usually floated. A multi-layer board tolerates the small substrate variations common in renovation and can be laid over existing screeds where build-up height allows.
Design-led residential and boutique commercial
Herringbone or chevron engineered flooring. The pattern is produced on the same prefinished engineered platform, so the design decision does not force a change in compliance set or installation method.
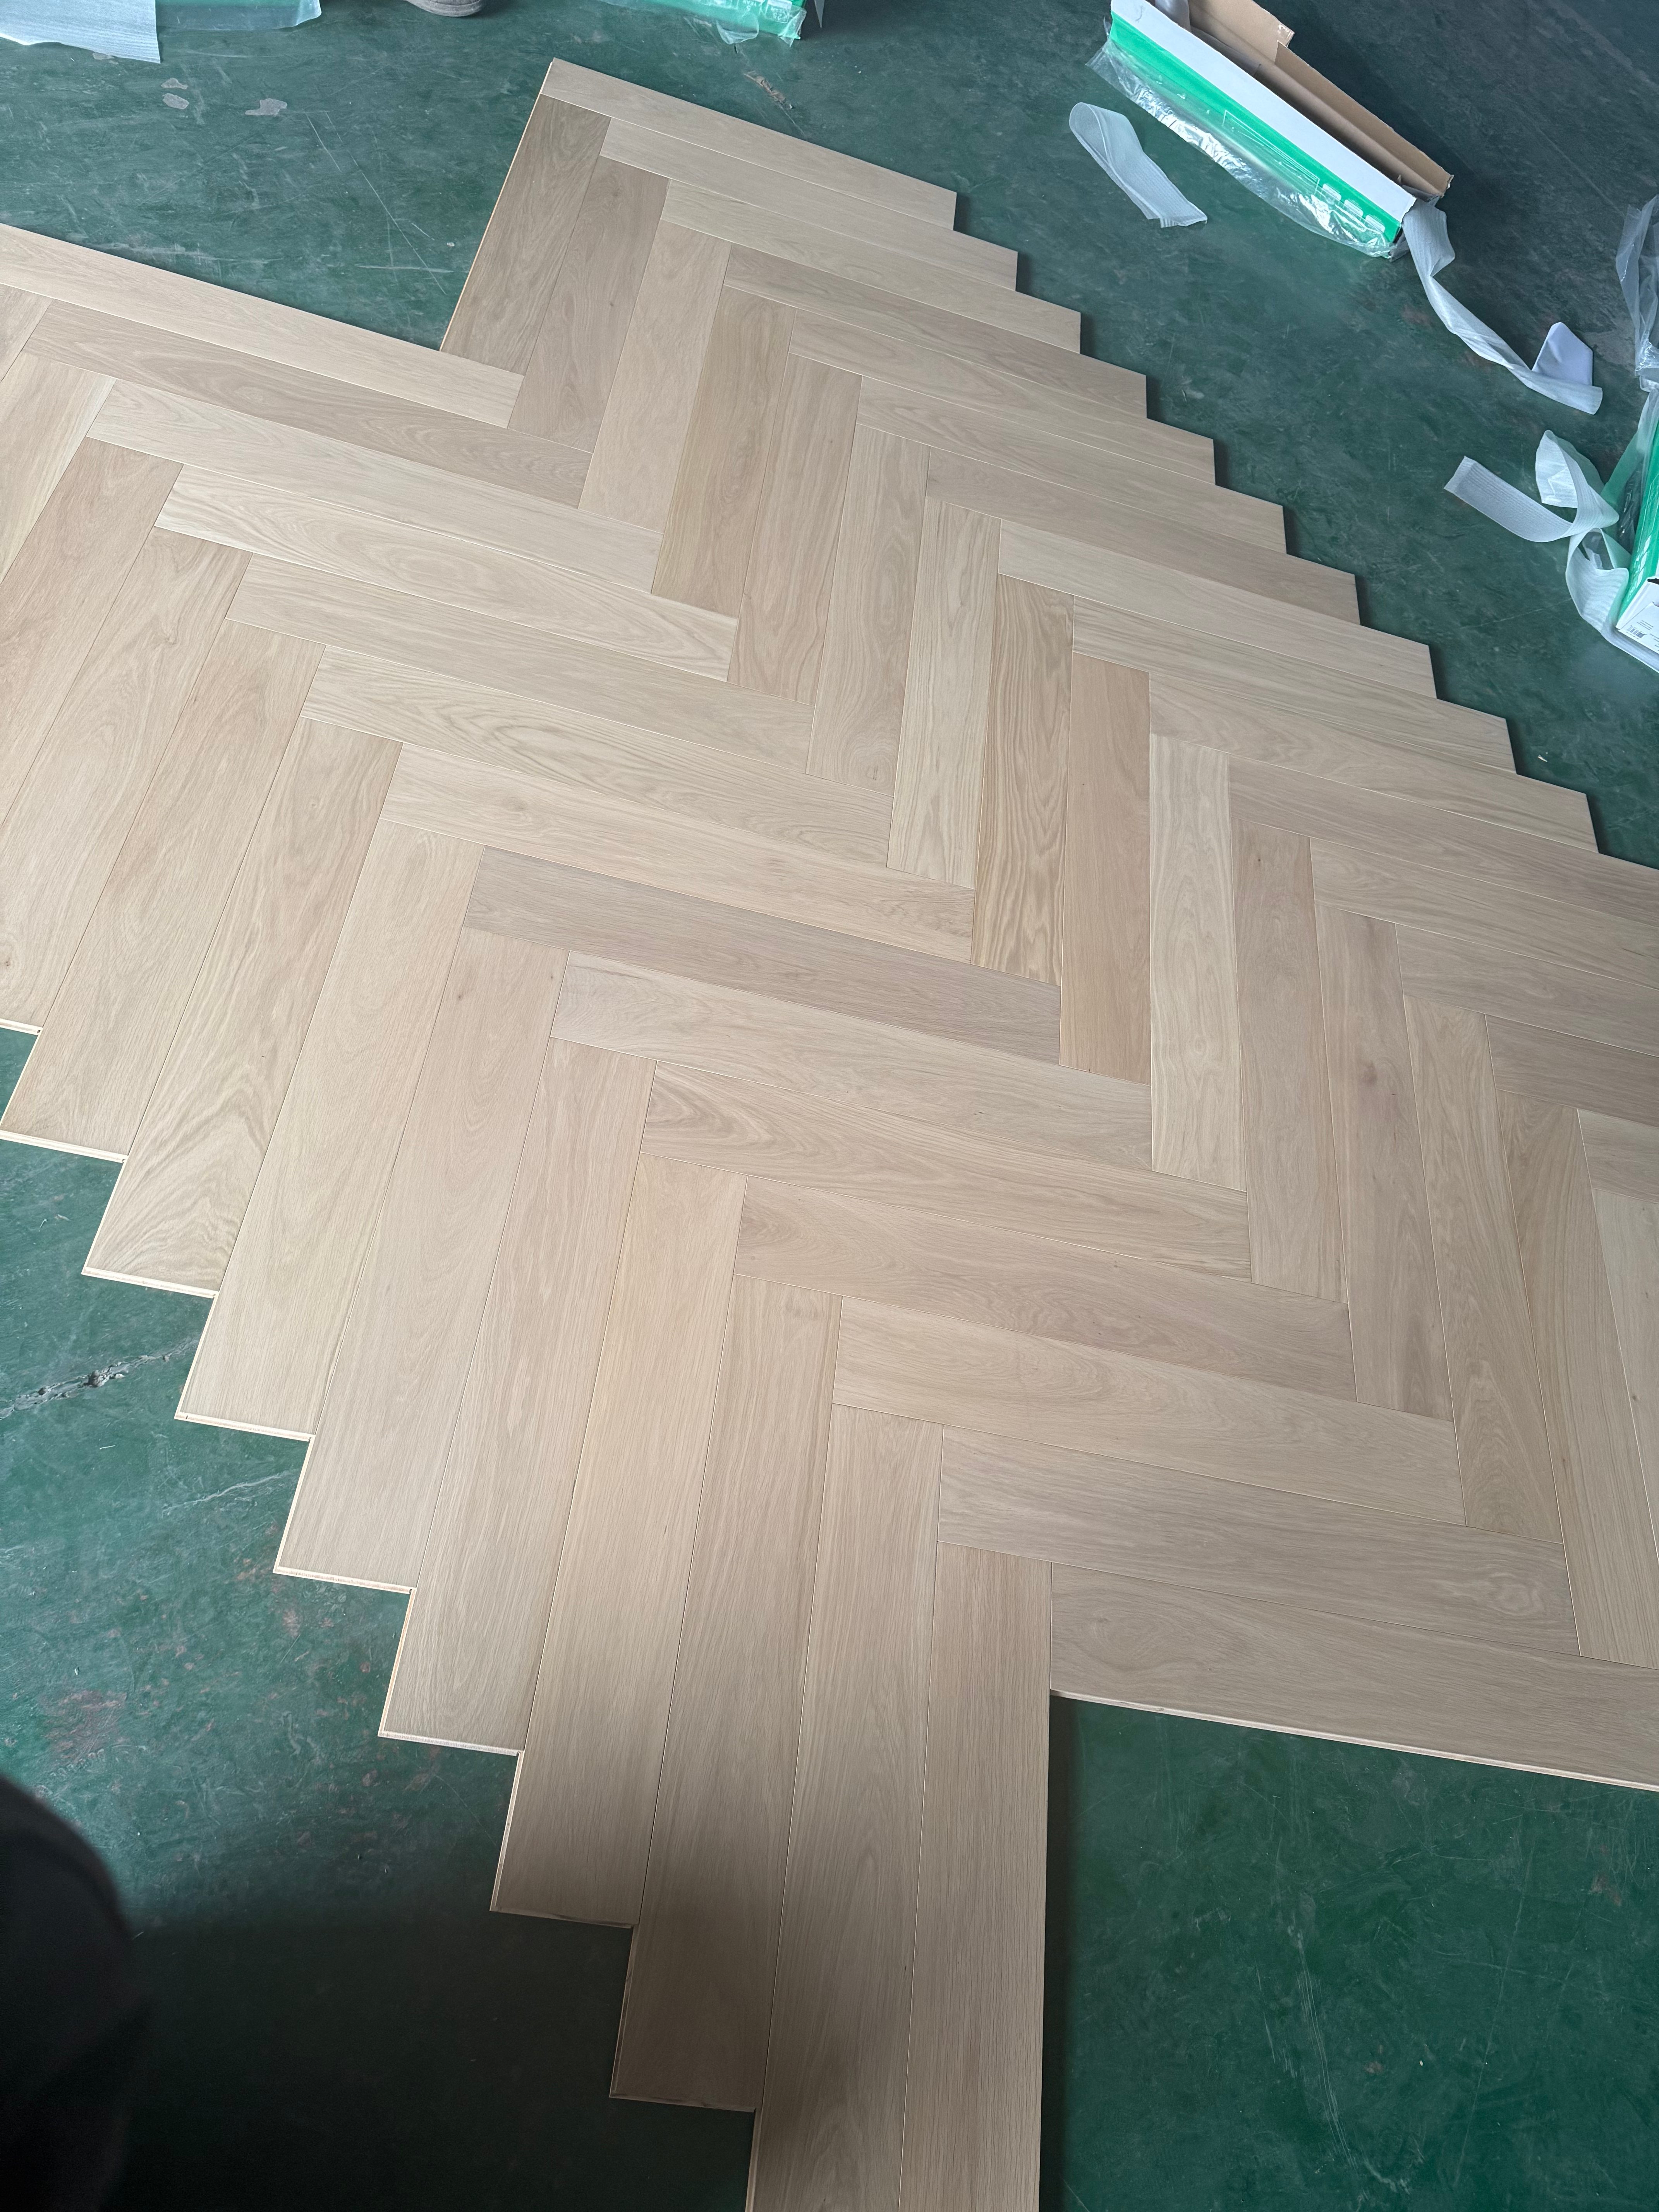
Herringbone engineered flooring: pattern formats are a grooving decision, not a separate product family.
Dry, above-grade value interiors
Laminate. With no wood surface there is no refinishing, so it fits projects where the floor will be replaced rather than restored.
Premium dry-area residential with a long refinishing horizon
Solid hardwood. A single-piece board with full-thickness sanding potential, provided the substrate is stable, dry and above grade.
Commercial retail, hospitality and office floors
Thick veneer engineered flooring at 3 to 4 mm, specified for high scratch resistance. Commercial specification also pulls warranty and supply questions to the front, and Dongda Wood offers a 25-year residential warranty and a 3-year commercial warranty, which signals what the manufacturer expects the wear layer to survive.
Comparison Table: Engineered vs Laminate vs Solid Hardwood
| Criterion | Engineered wood flooring | Laminate | Solid hardwood |
|---|---|---|---|
| Construction | Real wood veneer bonded to a cross-grain multi-ply core | Fibreboard core with printed decorative layer, no wood surface | Single piece of solid milled timber |
| Dimensional stability | High, cross-bonded core resists movement, suitable over concrete | Stable in dry conditions, joints can open with moisture | Moves with humidity, sensitive to moisture swings |
| Underfloor heating | Compatible | Manufacturer-dependent and generally limited | Generally not recommended |
| Installation | Floating or glue-down, prefinished with no site sanding | Typically floated | Nail-down or glue-down on suitable timber subfloor |
| Refinishing | Possible with 3 to 4 mm veneer, limited with 0.6 to 1.2 mm veneer | Not possible | Possible across the full board thickness |
| Compliance documentation | ANSI/HPVA EF 2020 and CARB / TSCA Title VI in the US, EN 14342:2013 CE in the EU, F4 star for Japan, FSC where required | Formaldehyde documentation required in most markets | Formaldehyde and species documentation required |
| Best-fit projects | Concrete substrates, underfloor heating, renovation, herringbone and chevron design work, commercial work with thick veneer | Dry, above-grade, budget-led interiors where floors are replaced rather than restored | Dry, stable, above-grade residential with refinishing planned |
| Main watch-out | Match veneer thickness to traffic and confirm the destination compliance file | Cannot be sanded, joints are moisture-sensitive | Substrate and humidity limits constrain installation |
Programme parameters for Dongda Wood engineered wood flooring
| MOQ (product 5856) | 400 square metres per colour |
| Payment terms | T/T (telegraphic transfer) |
| Delivery terms | FOB, CIF or DDP |
| Acceptance | Pre-shipment test |
| Programme lead time | 45 days |
| Monthly capacity | 150,000 square metres |
| Warranty | 25 years residential, 3 years commercial |
Frequently Asked Questions
Which certifications should I verify before importing engineered wood flooring into the US or the EU?
In the United States, engineered wood flooring is specified against ANSI/HPVA EF 2020, with formaldehyde emission limits set under CARB and TSCA Title VI. In the European Union, EN 14342:2013 defines the CE marking requirements covering reaction to fire and formaldehyde release. Japanese projects commonly ask for F4 star, and FSC chain of custody is requested where sourcing programmes are audited. Ask the supplier for the certificate itself and the tested product model rather than a certification logo. Dongda Wood's documentation set covers CARB/EPA, CE, F4 star and FSC.
Can one supplier handle both standard plank formats and custom herringbone or chevron programmes?
That depends on whether grooving and finishing stay in-house. Dongda Wood produces engineered hardwood flooring and engineered timber flooring under models GA01-016 and CC01-09, with formats from 600 x 125 x 14/3 mm up to 3000 x 300 x 19/4 mm, veneer thickness from 0.6 mm to 4 mm, and herringbone and chevron patterns available on the same line. Species are imported from Europe, America, Russia and Indonesia, and production runs on a German grooving line with a Taiwan paint line. For a long-term programme, one qualified line covering plank, wide plank and pattern formats reduces the number of suppliers you have to audit.
What are the commercial terms, including MOQ, payment and delivery?
For product 5856, the MOQ is 400 square metres per colour, payment terms are T/T (telegraphic transfer), and delivery can be arranged FOB, CIF or DDP. Because the MOQ applies per colour, a project that specifies many colours in small quantities will need to consolidate its palette or split the order across project phases to stay commercially efficient.
How do I validate quality before committing to a long-term supply relationship?
Validate at three levels: material, process and pre-shipment. On material, check that core and veneer are balanced and that both remain flat. On process, ask about moisture control for core and veneer, drying kilns and inspection at each stage of production. On pre-shipment, use pre-shipment testing as the acceptance baseline and confirm veneer thickness tolerance, which Dongda Wood holds within plus or minus 0.1 mm. Physical samples of the exact format and finish you intend to order remain the only reliable way to confirm colour, grain and coating before the first order.
What must a long-term engineered wood flooring supply partner in China prove?
Three things: capacity, lead time and continuity. Dongda Wood operates a 190,000 square metre facility with more than 500 employees, a monthly capacity of 150,000 square metres and a standard programme lead time of 45 days, backed by a 25-year residential warranty and a 3-year commercial warranty. Because the company has exported 100% of its output since 1995 to markets including the USA, Canada, Australia, the EU, the United Kingdom, Brazil, Chile and South Africa, repeat programmes are handled through an existing compliance and logistics routine rather than a first-time export process. To test that fit in practice, request samples and a quotation for your format.
Which One Fits Your Project? A Decision Framework
Work down this list until one line matches your project, then stop. The first match is your answer.
- Concrete substrate, underfloor heating, or seasonal humidity swings: engineered wood flooring.
- Dry, above-grade interior, budget-led, floor will be replaced rather than restored: laminate.
- Dry, stable substrate with a plan to sand the floor later: solid hardwood.
- Commercial traffic with a long lease: thick veneer engineered flooring at 3 to 4 mm, with the compliance file confirmed before price is negotiated.
- Herringbone or chevron design intent: engineered platform, pattern produced on the same prefinished line.
- Repeat or phased procurement across several years: engineered, from a supplier with verifiable capacity, lead time and warranty terms.
Engineered does not win because it is fashionable. It wins because multi-layer construction solves the two constraints that break most flooring specifications, namely substrate movement and cross-border compliance, while keeping a real wood surface that can be refinished when the veneer is thick enough to allow it.
Export-ready engineered wood flooring: capacity, compliance and lead time decide whether a specification becomes a delivered project.
Next step: samples, quotation and catalogue
If your project involves a concrete substrate, underfloor heating, a herringbone or chevron pattern, or a multi-phase commercial programme, the fastest way to confirm fit is a physical sample of the exact format and finish you plan to specify. Dongda Wood supplies engineered wood flooring and plywood from Suzhou, Anhui, China, under models GA01-016 and CC01-09.
Contact: Elimy, email Elimy_dongdawood@163.com, tel +86 18697561589, WhatsApp +86 18095694852. Address: No.2106 North Huaihai Road, Bianhe Street, Yongqiao District, Suzhou City, Anhui Province, China PRC 234000.
Download the full product and specification catalogue: Dongda Wood engineered wood flooring catalogue (PDF). Manufacturer website: dongdaflooring.com.