Engineered vs. Laminate vs. LVP: A Head-to-Head Comparison Guide
Buyers who are deciding among engineered wood flooring, laminate flooring and luxury vinyl plank usually ask one question: which one is best for my project? The more useful question is which construction can survive the room, the use pattern and the expected service life. This guide compares the three options head to head on structure, moisture behavior, appearance, maintenance and lifecycle, so a buyer can turn a flooring preference into a procurement specification.
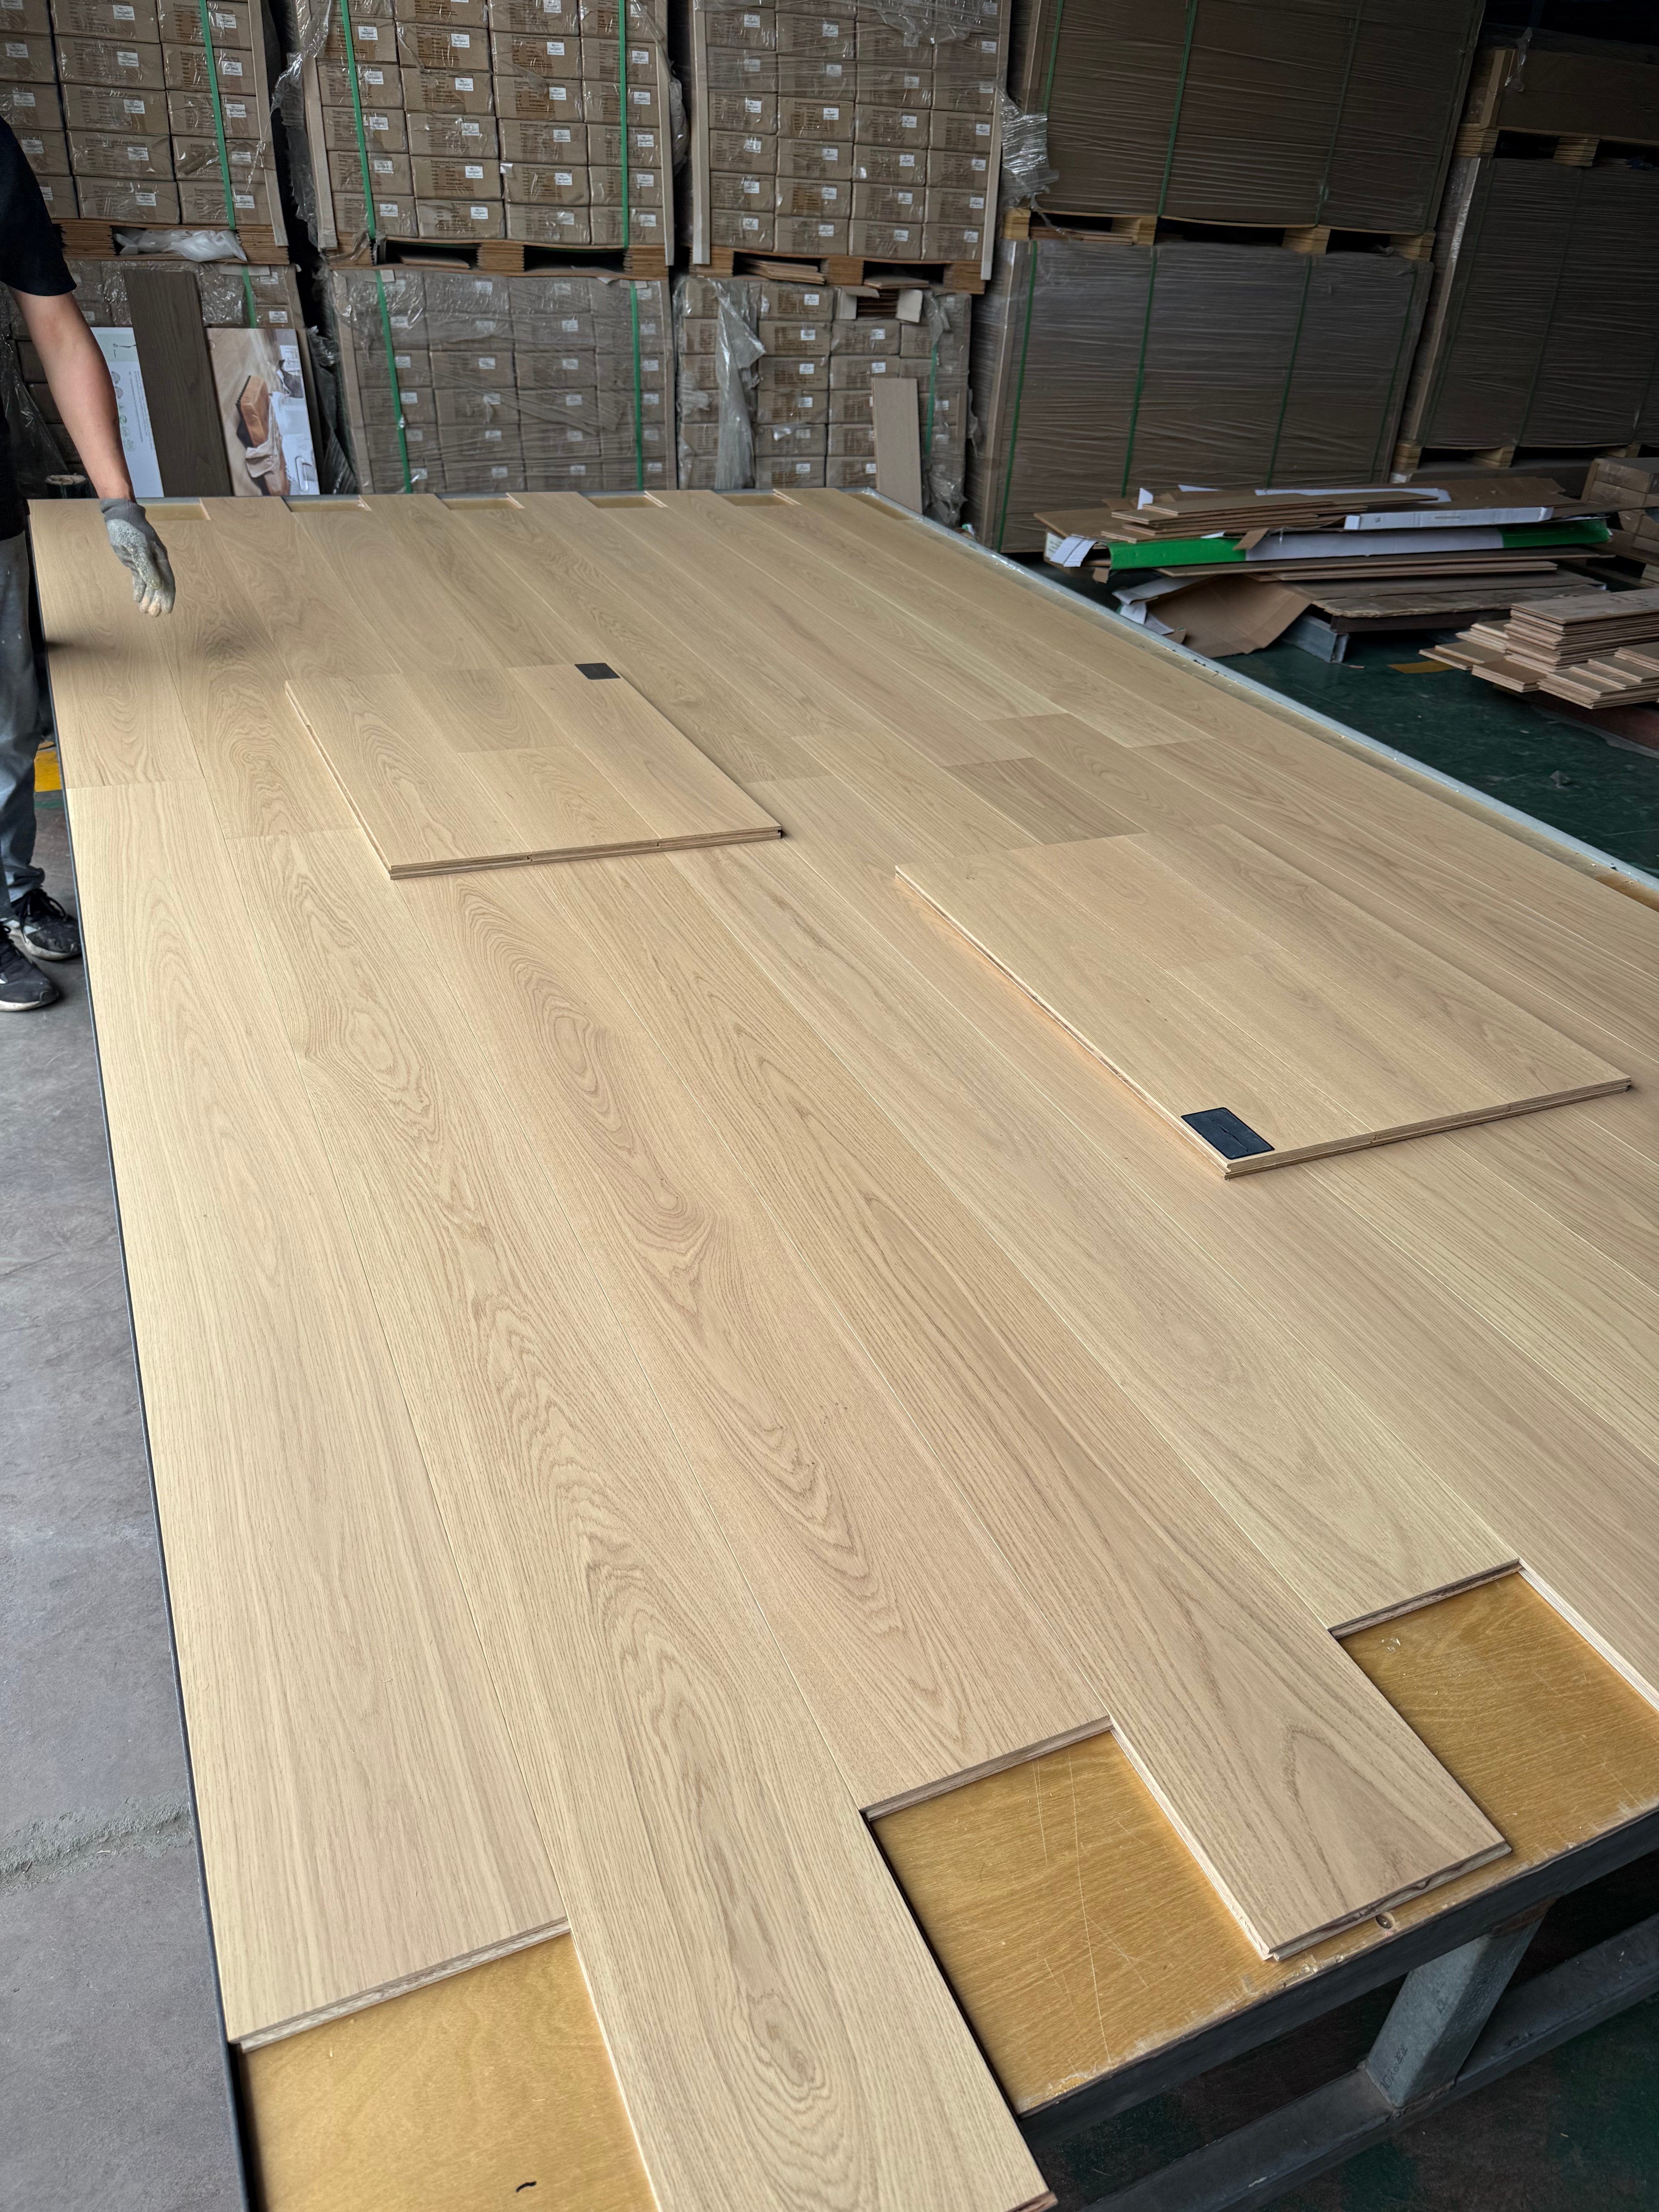
An engineered hardwood floor starts with a real wood wear layer on top of a multi-layer wood core. Laminate is a photographic wood-grain image printed on a high-density fiberboard core. Luxury vinyl plank is a synthetic plank with a printed vinyl film and a clear protective wear layer on a PVC-based or composite core. These different structures explain most of the performance differences.
Why the Decision Is Harder than It Looks
The difficulty is not just visual. All three groups are sold as wood-look flooring, and each group contains a wide range of quality levels. A thin veneer engineered flooring product can behave differently from a thick veneer engineered flooring product. A laminated floor with a dense core can outperform a low-end vinyl product in some rooms, while a waterproof vinyl plank can be the safer choice where moisture is present.
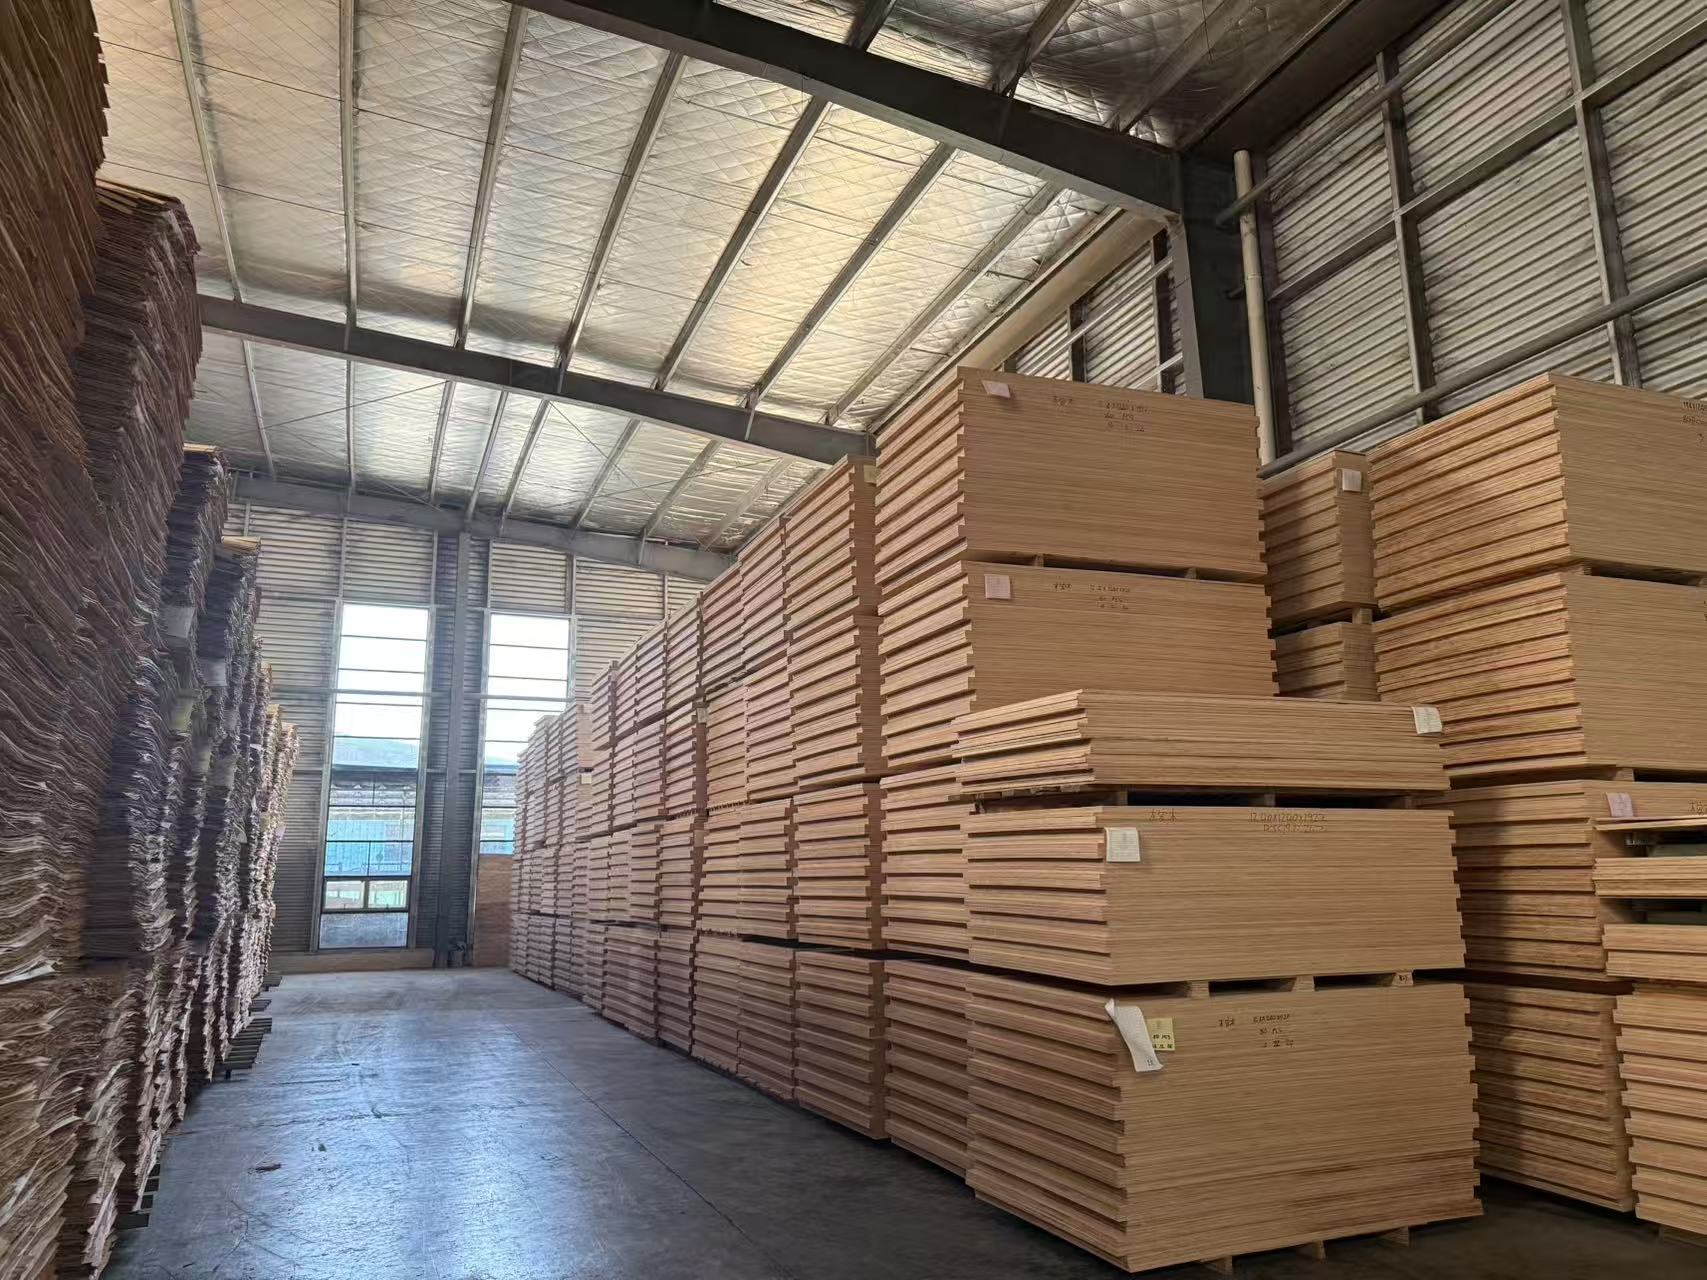
Engineered timber flooring is sometimes called multi-layer wood flooring, multi-ply engineered flooring or composite hardwood flooring. The terms describe the same principle: a real wood surface bonded to several wood layers or a plywood base. Because real wood is involved, the manufacturing process, moisture control, adhesive system and finish line influence the final quality more than they do with synthetic products. That is why a comparison between product types should also include a factory verification step.
This guide uses Suzhou Dongda Wood Co., Ltd as a factual reference at several quality-check points. Dongda Wood is an engineered wood flooring and plywood manufacturer in Suzhou City, Anhui Province, founded in 1995. Its description of raw material sourcing, core balancing, grooving lines, paint lines and inspection routines helps show what a buyer should look for when choosing an engineered wood supplier.
Wood Flooring Market Background
The commercial context favors engineered wood. According to The Business Research Company, the global wood flooring market was valued at USD 53.14 billion in 2024 and is projected to reach USD 71.57 billion by 2029. Within the broader wood flooring category, engineered wood flooring accounted for about 55% of the total market in 2024, according to market research reports. One widely cited reason is dimensional stability: engineered hardwood can be more stable than solid wood because opposing wood layers balance expansion and contraction.
Species preference also matters. Oak-based products represent approximately 46% of total engineered wood flooring demand globally, which is why engineered oak flooring is the most common frame of reference in specification sheets. China is also an important sourcing region for this category: China's exports of wood products reached USD 17.5 billion in 2024, with major destinations including the USA, Japan and the UK.
Product compliance is a separate evaluation axis. In the US, engineered wood flooring must meet ANSI/HPVA EF 2020, which includes formaldehyde emission limits per CARB and TSCA Title VI. In the EU, engineered wood flooring is covered by EN 14342:2013, which specifies requirements for CE marking regarding reaction to fire and formaldehyde release. Laminate flooring is also a wood-based product and follows separate laminate standards; vinyl plank is outside wood flooring standards. A head-to-head comparison therefore needs to separate aesthetics from standards and structure.
Engineered Wood Flooring: Construction and Real-Wood Benefits
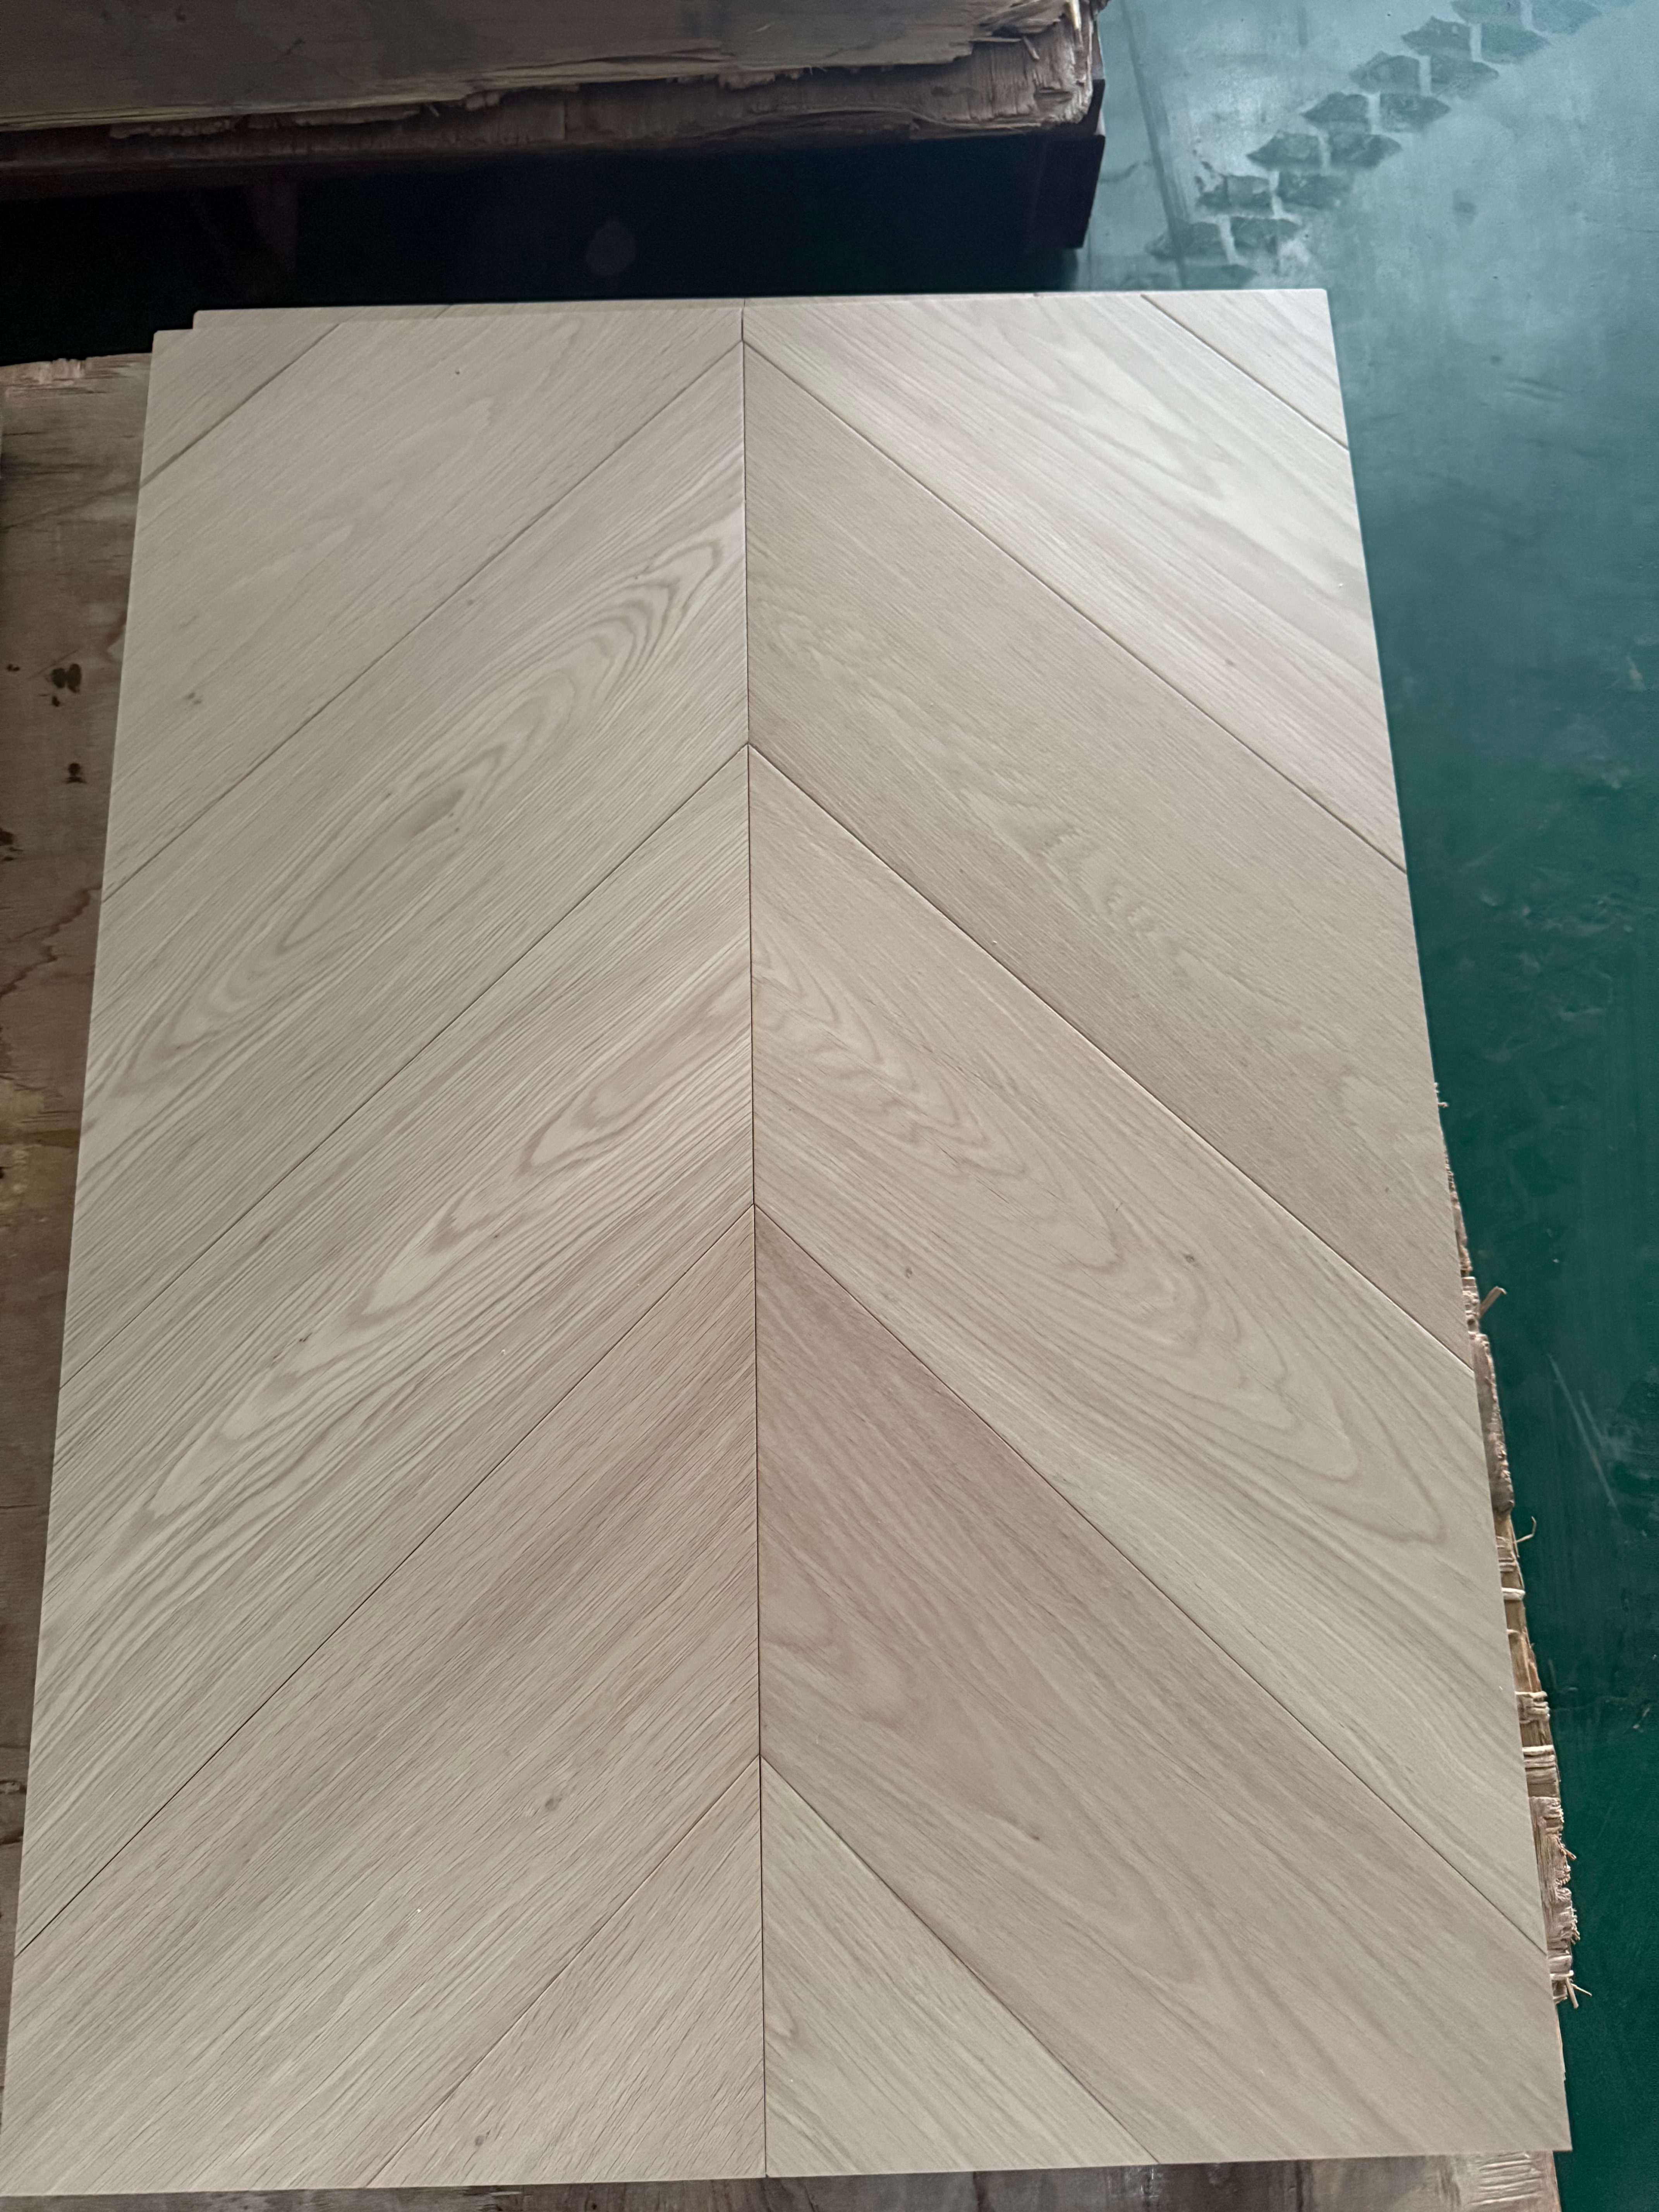
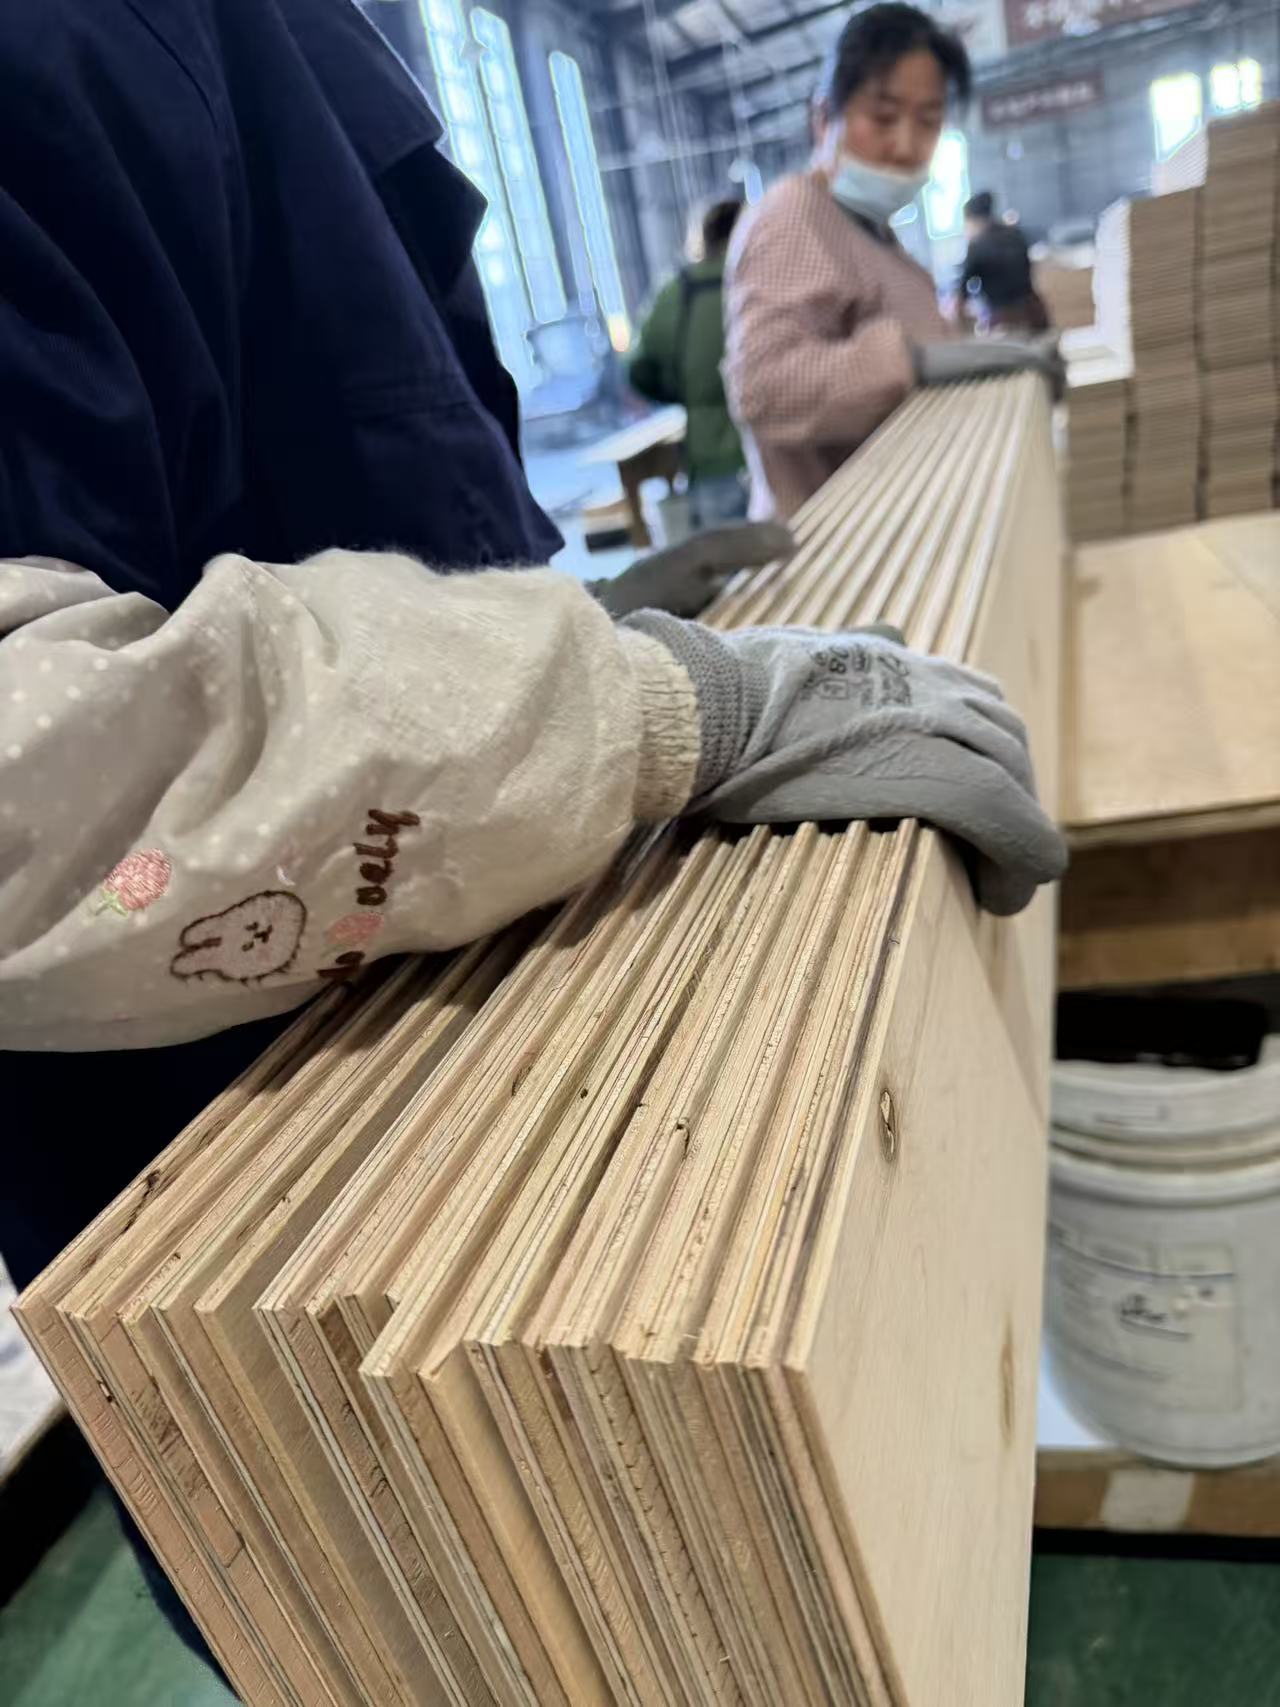
Engineered wood flooring is built with a real hardwood veneer on top and a multi-layer wood core underneath. In many products the core is a plywood construction or several cross-laid wood plies that make the plank less likely to move as one solid piece of wood would. The result is a genuine wood floor surface available in wide plank engineered flooring, herringbone engineered flooring, chevron engineered flooring and other formats.
For importers, the first advantage of engineered wood is authenticity. The surface can be sanded and refinished, although the number of times depends on the thickness of the top veneer. Thick veneer engineered flooring can accept more sanding; thin veneer engineered flooring is more economical but offers limited refinishing capacity. The second advantage is visual range. Prefinished flooring can use European, American, Russian or Indonesian wood species, and the same factory can supply both standard planks and decorative herringbone or chevron patterns. The third advantage is indoor air quality control: engineered wood can be manufactured with adhesives and finishes that meet E1 emission requirements, but the buyer still needs to verify the relevant certificate for the destination market.
Laminate and LVP: What the Alternatives Actually Are
Laminate flooring does not contain a real wood surface layer. It uses a decorative paper printed with a wood image, protected by a transparent overlay, bonded to an HDF core. Laminate is generally more scratch-resistant in daily use and is usually less expensive at the point of purchase. Its main limitation is moisture: if water penetrates the joints or edges, the fiberboard core can swell. Laminate also cannot be refinished; when the surface wears, the plank is normally replaced.
Luxury vinyl plank, or LVP, is a synthetic resilient floor. It is structured with a printed design layer and a clear wear layer over a PVC-based core. Some versions add stone-plastic or wood-plastic composite layers to improve rigidity. LVP is often the most tolerant of water, spills and cleaning routines. The trade-off is that LVP is not wood: it cannot be sanded, it does not age like wood, and its premium appearance relies on the print quality of the film rather than the natural grain of a real veneer.
Head-to-Head Comparison Table
The table below compares the three product groups using commonly accepted structural and performance definitions. The purpose is to make trade-offs explicit before a buyer evaluates a specific brand.
| Comparison point | Engineered wood flooring | Laminate flooring | Luxury vinyl plank (LVP) |
|---|---|---|---|
| Surface layer | Real hardwood veneer, commonly oak | Printed decor layer under a transparent overlay | Printed vinyl film under a clear wear layer |
| Core construction | Multi-layer wood or plywood core | High-density fiberboard (HDF) | PVC-based or composite core, sometimes with SPC/WPC layers |
| Content of real wood | Yes, top wear layer is genuine wood | No | No |
| Refinishing capability | Possible depending on veneer thickness; thick veneer allows more sanding | Not possible | Not possible |
| Moisture behavior | More dimensionally stable than solid wood; moisture control in production is critical | Susceptible to swelling if water penetrates the core | Generally the most water-tolerant |
| Visual aging | Real wood tone and grain; can be refinished to renew the surface | Printed pattern remains constant | Printed pattern remains constant |
| Format flexibility | Planks, wide planks, herringbone, chevron | Usually planks | Planks and tiles |
| Regulatory frame | ANSI/HPVA EF 2020 (US), EN 14342:2013 (EU) | Wood-based flooring standards apply to the core | Usually outside wood flooring material standards |
No type wins on every line. Engineered wood wins on realism, refinishing potential and natural material value. Laminate offers a wood-like look with a hard core at a lower entry price. LVP wins in wet areas and spaces that need frequent cleaning. A decision framework, not a single ranking, is the more reliable tool.
Step-by-Step Selection Process
Use the following process to move from product type to a concrete purchasing decision.
- Define the room and the moisture risk. For living rooms, bedrooms, studies and retail spaces with controlled humidity, engineered hardwood flooring is a strong candidate. For basement levels, bathrooms or commercial food-service spaces, LVP is usually the safer choice because of its water tolerance.
- Decide whether refinishing matters. If the project expects long-term ownership and surface renewal, choose thick veneer engineered flooring. If the floor will be replaced for decorative reasons every few years, laminate or LVP can be acceptable.
- Check the wood species. Oak is the most common engineered wood species. In manufacturing terms, species should be imported or sourced with clear documentation. Dongda Wood, for example, describes its engineered wood species as imported from Europe, America, Russia and Indonesia.
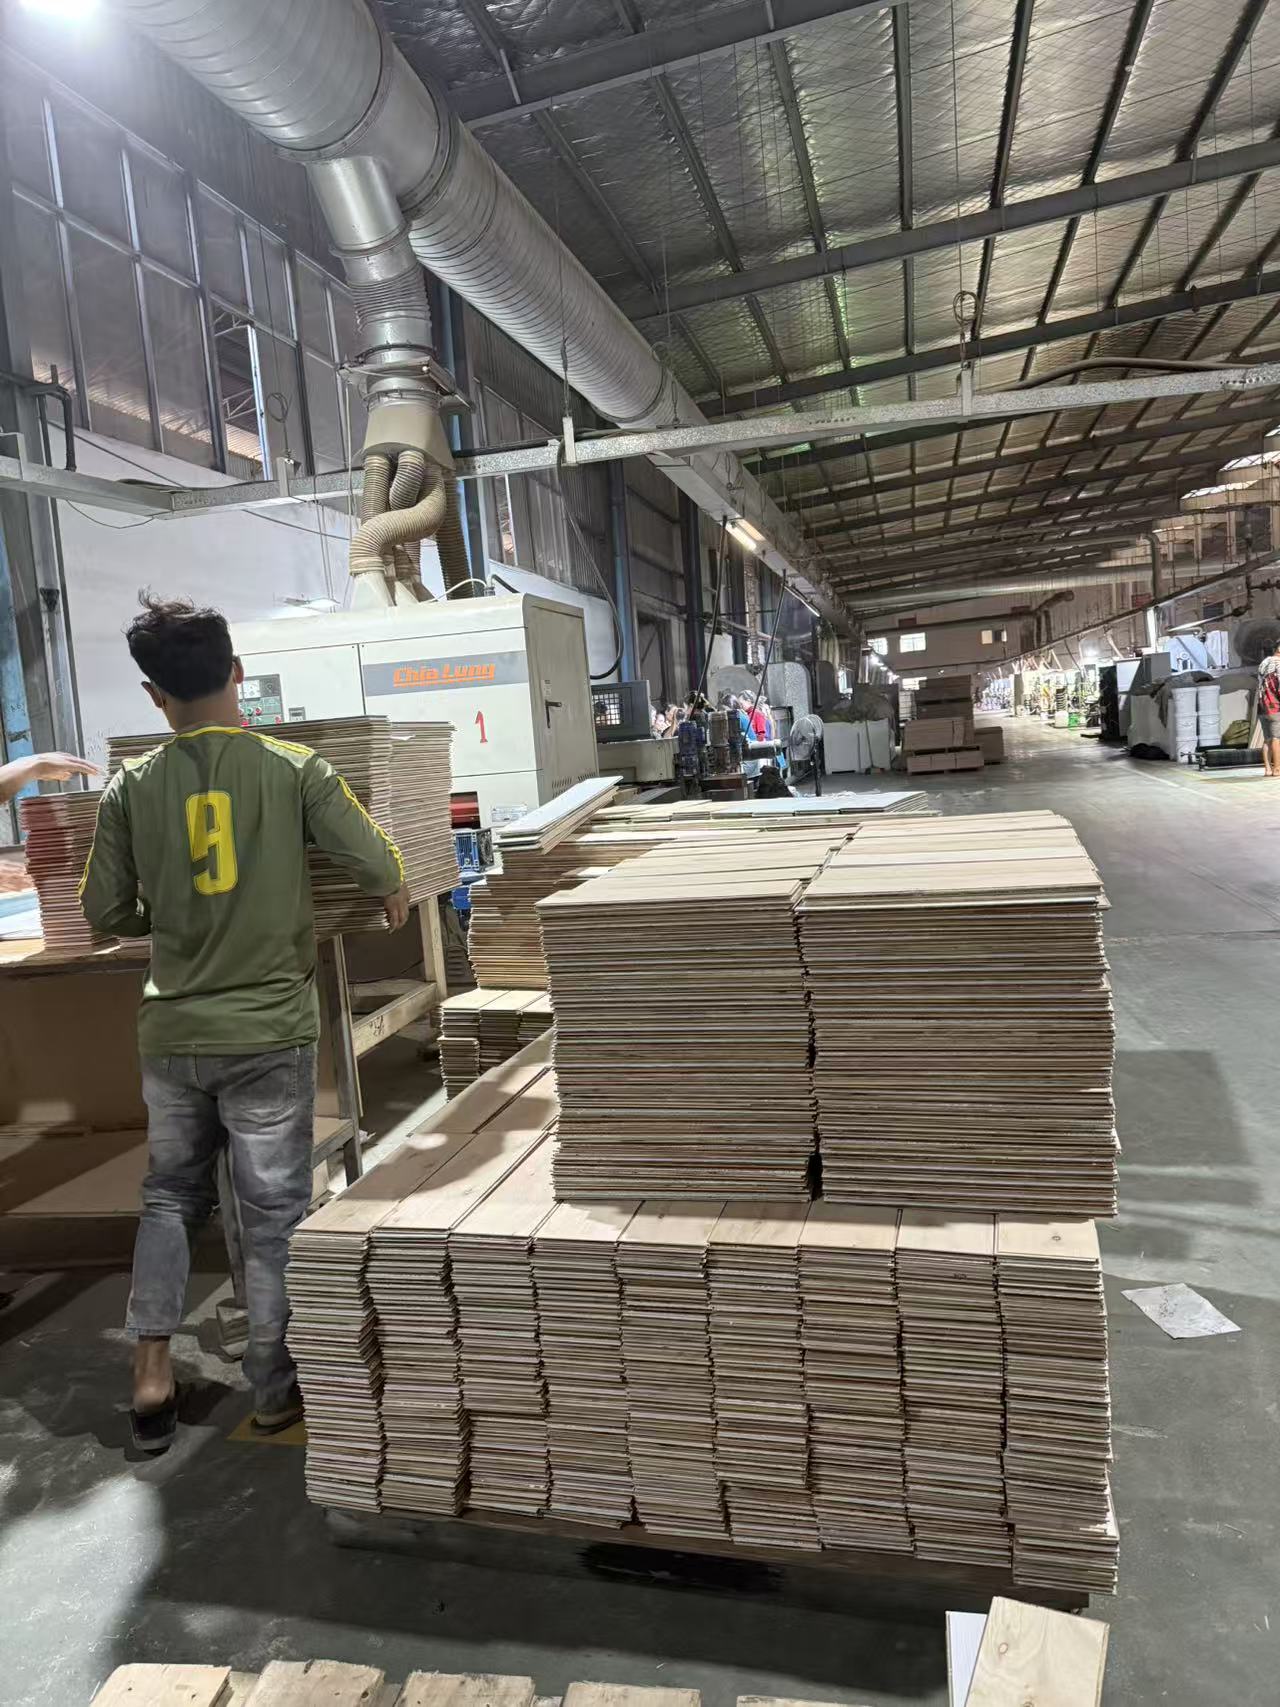
- Ask about core construction and moisture balance. The interaction between the veneer and the core determines stability. A factory should control moisture content in both the core and the veneer. At Dongda Wood, floor warping risk is managed with a drying kiln and by carefully controlling the moisture content of core and veneer, supported by quality inspections at every stage of the process.
- Verify compliance for the destination market. Confirm that the product documentation matches ANSI/HPVA EF 2020 or EN 14342:2013, and that formaldehyde emissions are declared. Dongda Wood's comparison data lists formaldehyde emission at E1 grade, which is a common benchmark for wood-based panels.
- Review machining and finish quality. Consistent tongue-and-groove or click profile dimensions affect installation speed and joint tightness. Finish consistency affects how the floor looks after years of cleaning. A manufacturer that invests in dedicated lines is easier to evaluate. Dongda Wood uses a German Homaomai grooving line and a Taiwan Fengqiao paint line, plus a series of supporting precision equipment.
- Inspect the supplier's tolerance and inspection data. Veneer thickness tolerance is one factual indicator: Dongda Wood's documented tolerance is controlled within plus or minus 0.1 mm, and its production pass rate is 99.8% in the same comparison data. A buyer should ask any supplier to state the same type of measurable data.
- Request a physical sample and compare it with the planned installation. Flooring decisions cannot be made from images alone. Evaluate sample surface texture, edge profile, finish and color under real lighting.
Use Cases
Engineered Oak Flooring for Residential Interiors
A living room or master bedroom is the classic setting for engineered hardwood flooring. Oak's share of the engineered wood market is high for a reason: the grain is neutral, the color accepts different finishes and the species is widely available. For an interior renovation, a high-quality factory can supply prefinished engineered floors in plank, wide plank, herringbone and chevron layouts. This format flexibility makes engineered oak flooring the default for decorative residential projects.
Rental Interiors and Light Commercial Spaces
Projects with frequent tenant changes often reward impact resistance and predictable replacement cost. Laminate can be appropriate in dry rental apartments because of its hard surface and moderate price. The limitation is moisture at entrances, kitchens and laundry areas. In those zones, LVP is more forgiving. The right combination for many property managers is laminate or vinyl in wet areas and engineered wood in main living spaces where value is part of the rental proposition.
Basements and Moisture-Prone Areas
Basements, bathrooms and commercial kitchens introduce real moisture risk. Wood-based floors can tolerate occasional spills if finished well, but standing water or high humidity can damage them over time. LVP is normally the more dependable technical answer for these conditions. This is not a quality comparison between brands; it is a structural comparison between a wood-based surface and a synthetic waterproof surface.
What Factory Evidence to Look for Behind Engineered Wood Claims
Because engineered wood contains natural material, its performance depends on how the factory prepares and processes that material. A supplier can state broad claims about quality, but a buyer should look for production-level evidence. The following points are based on the documented practices of Dongda Wood and provide a model for supplier checks.
- Raw material sourcing. Imported species from Europe, America, Russia and Indonesia are part of Dongda Wood's documented sourcing model. Clear sourcing matters because veneer quality and species grading determine the appearance of the finished floor.
- Moisture control. One of the main failure modes for engineered wood is floor warping. Dongda Wood describes its control method as balancing the core and the veneer, controlling moisture content, and keeping both layers flat. The related enterprise measure is a drying kiln plus quality inspections at every stage.
- Machining. The German Homaomai grooving line supports precise profile milling. A consistent profile reduces installation friction and produces tighter joints.
- Surface finishing. The Taiwan Fengqiao paint line and imported German Jianfo paint are part of Dongda Wood's finishing system. Coating quality affects stain resistance and long-term appearance.
- Adhesive system. Dongda Wood states that it uses Finland Taier phenolic glue in production. The adhesive system influences both bond durability and emission levels.
- Dimensional discipline. The supplied comparison data for Dongda Wood cites veneer thickness tolerance of plus or minus 0.1 mm and a production pass rate of 99.8%. These figures give a buyer a measurable expectation to request from any prospective supplier.
In a comparison between engineered, laminate and LVP, this evidence matters in a specific way: a laminate or vinyl floor is more forgiving of factory variation because it is manufactured under controlled synthetic conditions. Engineered wood is natural on the surface, so a supplier with kiln control, moisture management, quality checks and tolerance discipline is structurally better positioned to deliver consistent planks.
Frequently Asked Questions
What compliance standards should be verified for engineered wood flooring?
In the United States, engineered wood flooring must comply with ANSI/HPVA EF 2020, including formaldehyde emission limits per CARB and TSCA Title VI. In the European Union, EN 14342:2013 specifies requirements for CE marking regarding reaction to fire and formaldehyde release. A buyer should ask for documentation that matches the destination market and should confirm the declared formaldehyde class. In Dongda Wood's product comparison data, formaldehyde emission is listed at E1 grade, which is a familiar benchmark for wood-based flooring products.
Which manufacturer is better for engineered wood flooring?
Better depends on the buyer's requirements for price, consistency, service and technical verification. A documented comparison involving Shandong Longteng Wood Industry Co., Ltd. describes Dongda Wood's differentiation as reasonable prices, consistent quality and a strong commitment to customer service. The same comparison data lists E1-grade formaldehyde emission, veneer thickness tolerance within plus or minus 0.1 mm and a production pass rate of 99.8%. These types of measurable claims are more useful than an unqualified statement that one manufacturer is better. Buyers should test the claims with samples, audits and order documentation.
How does Dongda Wood control the risk of warping in engineered wood flooring?
Dongda Wood manages floor warping risk by balancing the core and the veneer, controlling moisture content and keeping both components flat. The documented enterprise measures include adding a drying kiln, carefully controlling the moisture content of the core and veneer, and performing inspections at every production stage. This approach is directly relevant to engineered hardwood flooring because warping usually starts when the top veneer and the core respond differently to humidity.
How should a buyer compare engineered flooring with laminate when budget is a constraint?
Laminate generally has a lower initial purchase price than engineered wood flooring, but the comparison should include the full service life. Engineered wood has a real wood layer that can be refinished in many product versions, especially thick veneer engineered flooring, while laminate cannot be refinished. A lower-priced laminate floor can become the more expensive choice if the space is exposed to moisture or if the surface cannot be renewed. In dry, low-moisture applications, laminate is a legitimate budget option; for rooms where real wood character and long-term renewal matter, engineered wood flooring is usually the better specification.
What should be checked when evaluating an engineered wood flooring sample?
A sample should be checked on five points: surface veneer appearance, veneer thickness evenness, profile precision, finish quality and formaldehyde declaration. A tolerance-controlled product, such as Dongda Wood's plus or minus 0.1 mm veneer thickness standard, is easier to install in large areas because joints remain consistent. The sample should also be compared with the factory's stated compliance documentation. If the sample and the certificate cannot be linked to the same production line specification, the buyer should ask for more evidence before placing a large order.
Ready to compare engineered wood flooring suppliers for your project? Dongda Wood can provide product specifications, factory information and export documentation. Download the company brochure for a detailed overview of engineered wood flooring production and product range.
Brochure: Dongda Wood engineered wood flooring brochure (PDF)
Website: dongdaflooring.com
Email: Elimy_dongdawood@163.com | WhatsApp/WeChat: +86 18697561589
Conclusion
The comparison between engineered, laminate and LVP is not a contest with one winner. Engineered wood flooring, including engineered oak flooring and manufactured wood flooring, offers a real wood surface, multi-layer stability, refinishing options and premium format variety. Laminate is a lower-cost wood-look product with a hard core but limited moisture tolerance and no refinishing capability. LVP provides strong water resistance and durability but lacks the natural wood character and renewal path of an engineered hardwood floor.
The decision process should therefore follow the room, the moisture condition, the desired lifecycle and the supplier's measurable evidence. For engineered wood projects, look for a manufacturer with controlled moisture management, credible compliance documentation, precise machining, a consistent finish line and transparent tolerance data. Suzhou Dongda Wood Co., Ltd is one such reference: founded in 1995, with a 190,000 square meter facility, over 500 employees, German Homaomai grooving technology, Taiwan Fengqiao paint technology and documented export experience across regions such as the USA, Canada, Australia, the EU, the UK, Brazil, Chile and South Africa. Contact Dongda Wood directly to test the claims with a sample or a project-specific quotation.