One Contract or Many? Turnkey vs Separate Pulp Molding Procurement
A turnkey pulp molding line and separate equipment procurement are not two prices for the same purchase. They are two different ways of distributing engineering work, interface risk and responsibility for the final result. A turnkey contract buys a coordinated production system through one project interface. Separate procurement buys individual machines at individually comparable prices and leaves the integration project with the buyer's own team.
That difference decides most of the total cost of ownership question before the first quotation is opened. The visible number is the contract value. The number that decides the project is everything that must be engineered, coordinated, modified and re-commissioned between the machines.
Short answer. For a new factory, a large-scale project, an overseas project or a buyer without an experienced pulp molding engineering team, a turnkey line usually removes more cost than it adds, because the cost it removes — repeated engineering, interface modification, commissioning coordination and responsibility disputes — is cost such buyers cannot absorb internally. For an experienced molded-fiber manufacturer that already runs mature pulping, process and project-management capability, separate procurement can preserve supplier choice and internal control without giving up much.
The rest of this guide compares the two models on the modules they cover, the cost lines that actually move, the technical interfaces where integration is won or lost, and the conditions under which each model is the rational choice.
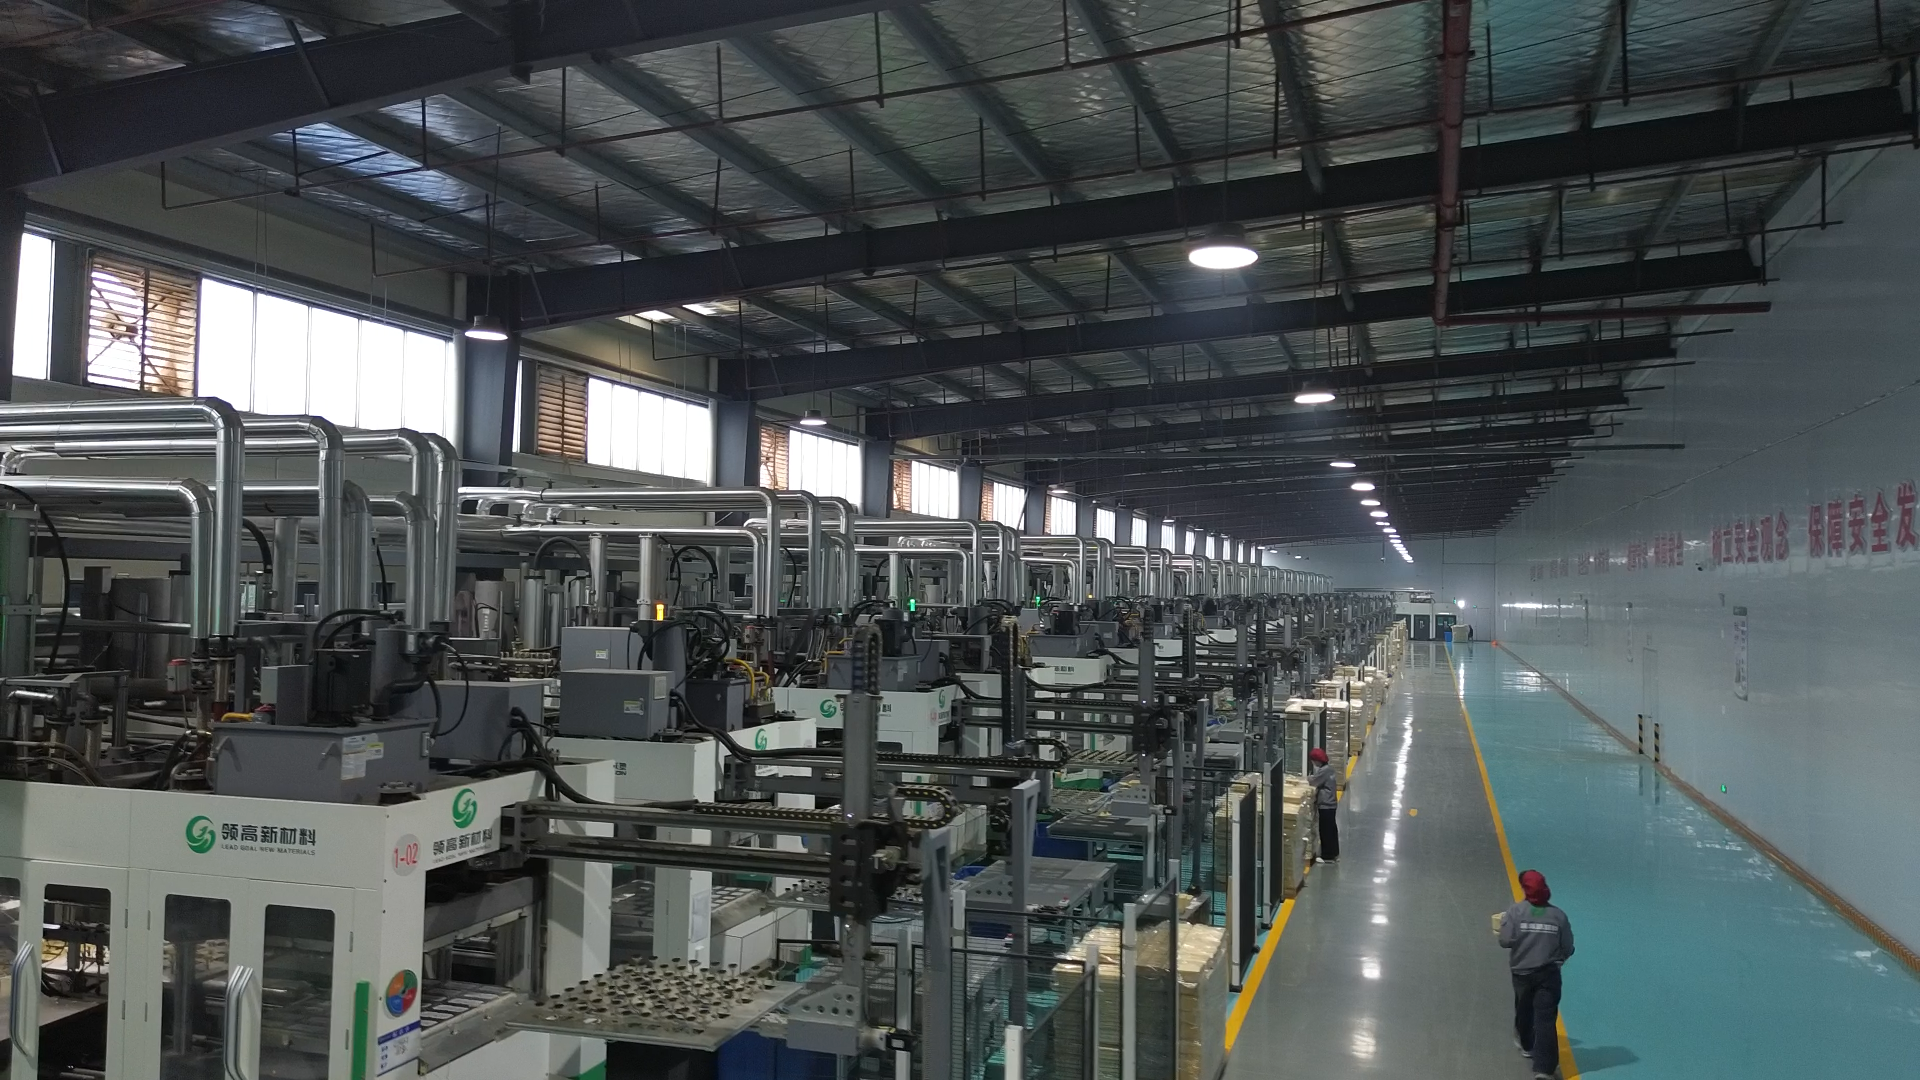
An integrated pulp molding workshop: forming, trimming and downstream processes on one continuous production route. Image: Hanson Pulp Molding.
What Separate Procurement Asks the Buyer to Own
Separate procurement is not only buying several machines. It is buying the integration project that connects them, and that project has to be staffed.
A complete pulp molding plant covers factory planning, pulp preparation, forming equipment, molds, downstream automation, electrical control, utilities, wastewater treatment, installation, commissioning and personnel training. Under separate procurement, those scopes are purchased from multiple suppliers and coordinated by the customer.
Every boundary between two suppliers is a place where someone must write a specification, agree a control signal, sequence a commissioning step and accept responsibility when the line does not reach target output. Slurry is the clearest example. When pulp preparation and forming come from different companies, slurry concentration, flow, pipelines, tanks and white-water circulation must be agreed across two engineering teams that did not design the system together, and the machine production rhythm has to be reconciled afterwards.
Molds follow the same logic. When the mold supplier, the equipment manufacturer and the product developer are three separate parties, the customer coordinates the technical interfaces and the responsibility boundaries between them. A forming defect can originate in the mold, the machine, the raw material or the process; splitting the suppliers splits the diagnosis as well.
None of this makes separate procurement a poor decision. It makes it a capability purchase: it performs well when the buyer genuinely holds the capability being purchased.
Why the Machine Price Is the Wrong Comparison Basis
The category is expanding, which is exactly why procurement models get compared on the wrong numbers. Cloud Market Reports valued the global pulp moulding machine market at USD 2,140.0 million in 2024 and projected USD 3,760.2 million by 2032; the same research attributes approximately 45% of global demand to food and beverage packaging. Trade data points in a consistent direction on supply: China's exports under HS 843920, machinery for making paper or paperboard, were valued at USD 49.58 million in 2024, according to the World Integrated Trade Solution.
Those figures need a scope warning. Published market sizes for this category vary widely because product scope varies: estimates that fold all paper-making machinery under HS 8439 into the definition run far above estimates that count molding machines alone. The 2024 value above should be read as one scope-dependent estimate, not as a settled market size.
More importantly, none of those numbers tells a buyer whether to purchase turnkey or separately. Category growth describes a market; the procurement decision describes a project. That decision is made on interfaces, internal capability and exposure to delay — which is why the comparison below is built on cost lines and technical boundaries rather than on category statistics.
The 6+1 Module Map: What Turnkey Puts Under One Interface
HANSON PULP MOLDING (Guangdong Hanson Pulp Molding Technology Co., Ltd.) is a pulp molding equipment and turnkey factory solution provider based in Dongguan, Guangdong, China, with more than 200 employees including approximately 50 R&D and engineering staff, 50 patents and an annual output of 150 units. Its turnkey pulp molding solution is organized as six service modules plus one development layer under a single integrated project interface.
| Module | What the turnkey scope covers | What separate procurement leaves with the buyer |
|---|---|---|
| 1. Factory planning | Capacity planning, layout and material-flow design matched to the equipment train | Layouts supplied by each machine vendor, reconciled by the buyer |
| 2. Pulp preparation | Pulp preparation designed together with forming, slurry feeding, tanks, pipelines and white-water circulation | A separate pulping supplier; interface parameters and control signals agreed by the buyer |
| 3. Forming equipment | Forming machines configured to the product family and capacity target | Machines bought individually; capacity and cycle claims compared by the buyer |
| 4. Mold manufacturing | In-house mold design, machining, testing and mass-production adaptation | An outsourced mold supplier coordinated against the machine supplier |
| 5. Downstream automation | Trimming, inspection, stacking, counting and packing matched to line rhythm | Separately sourced modules; transfer and cycle matching remains a buyer task |
| 6. Technical and production support | Installation, commissioning, operator training and ramp-up from one team | Split between suppliers, remote support or separate service visits |
| +1. Development layer | Product development, raw-material development, sampling and small-batch validation | Sampling run across suppliers; results interpreted internally |
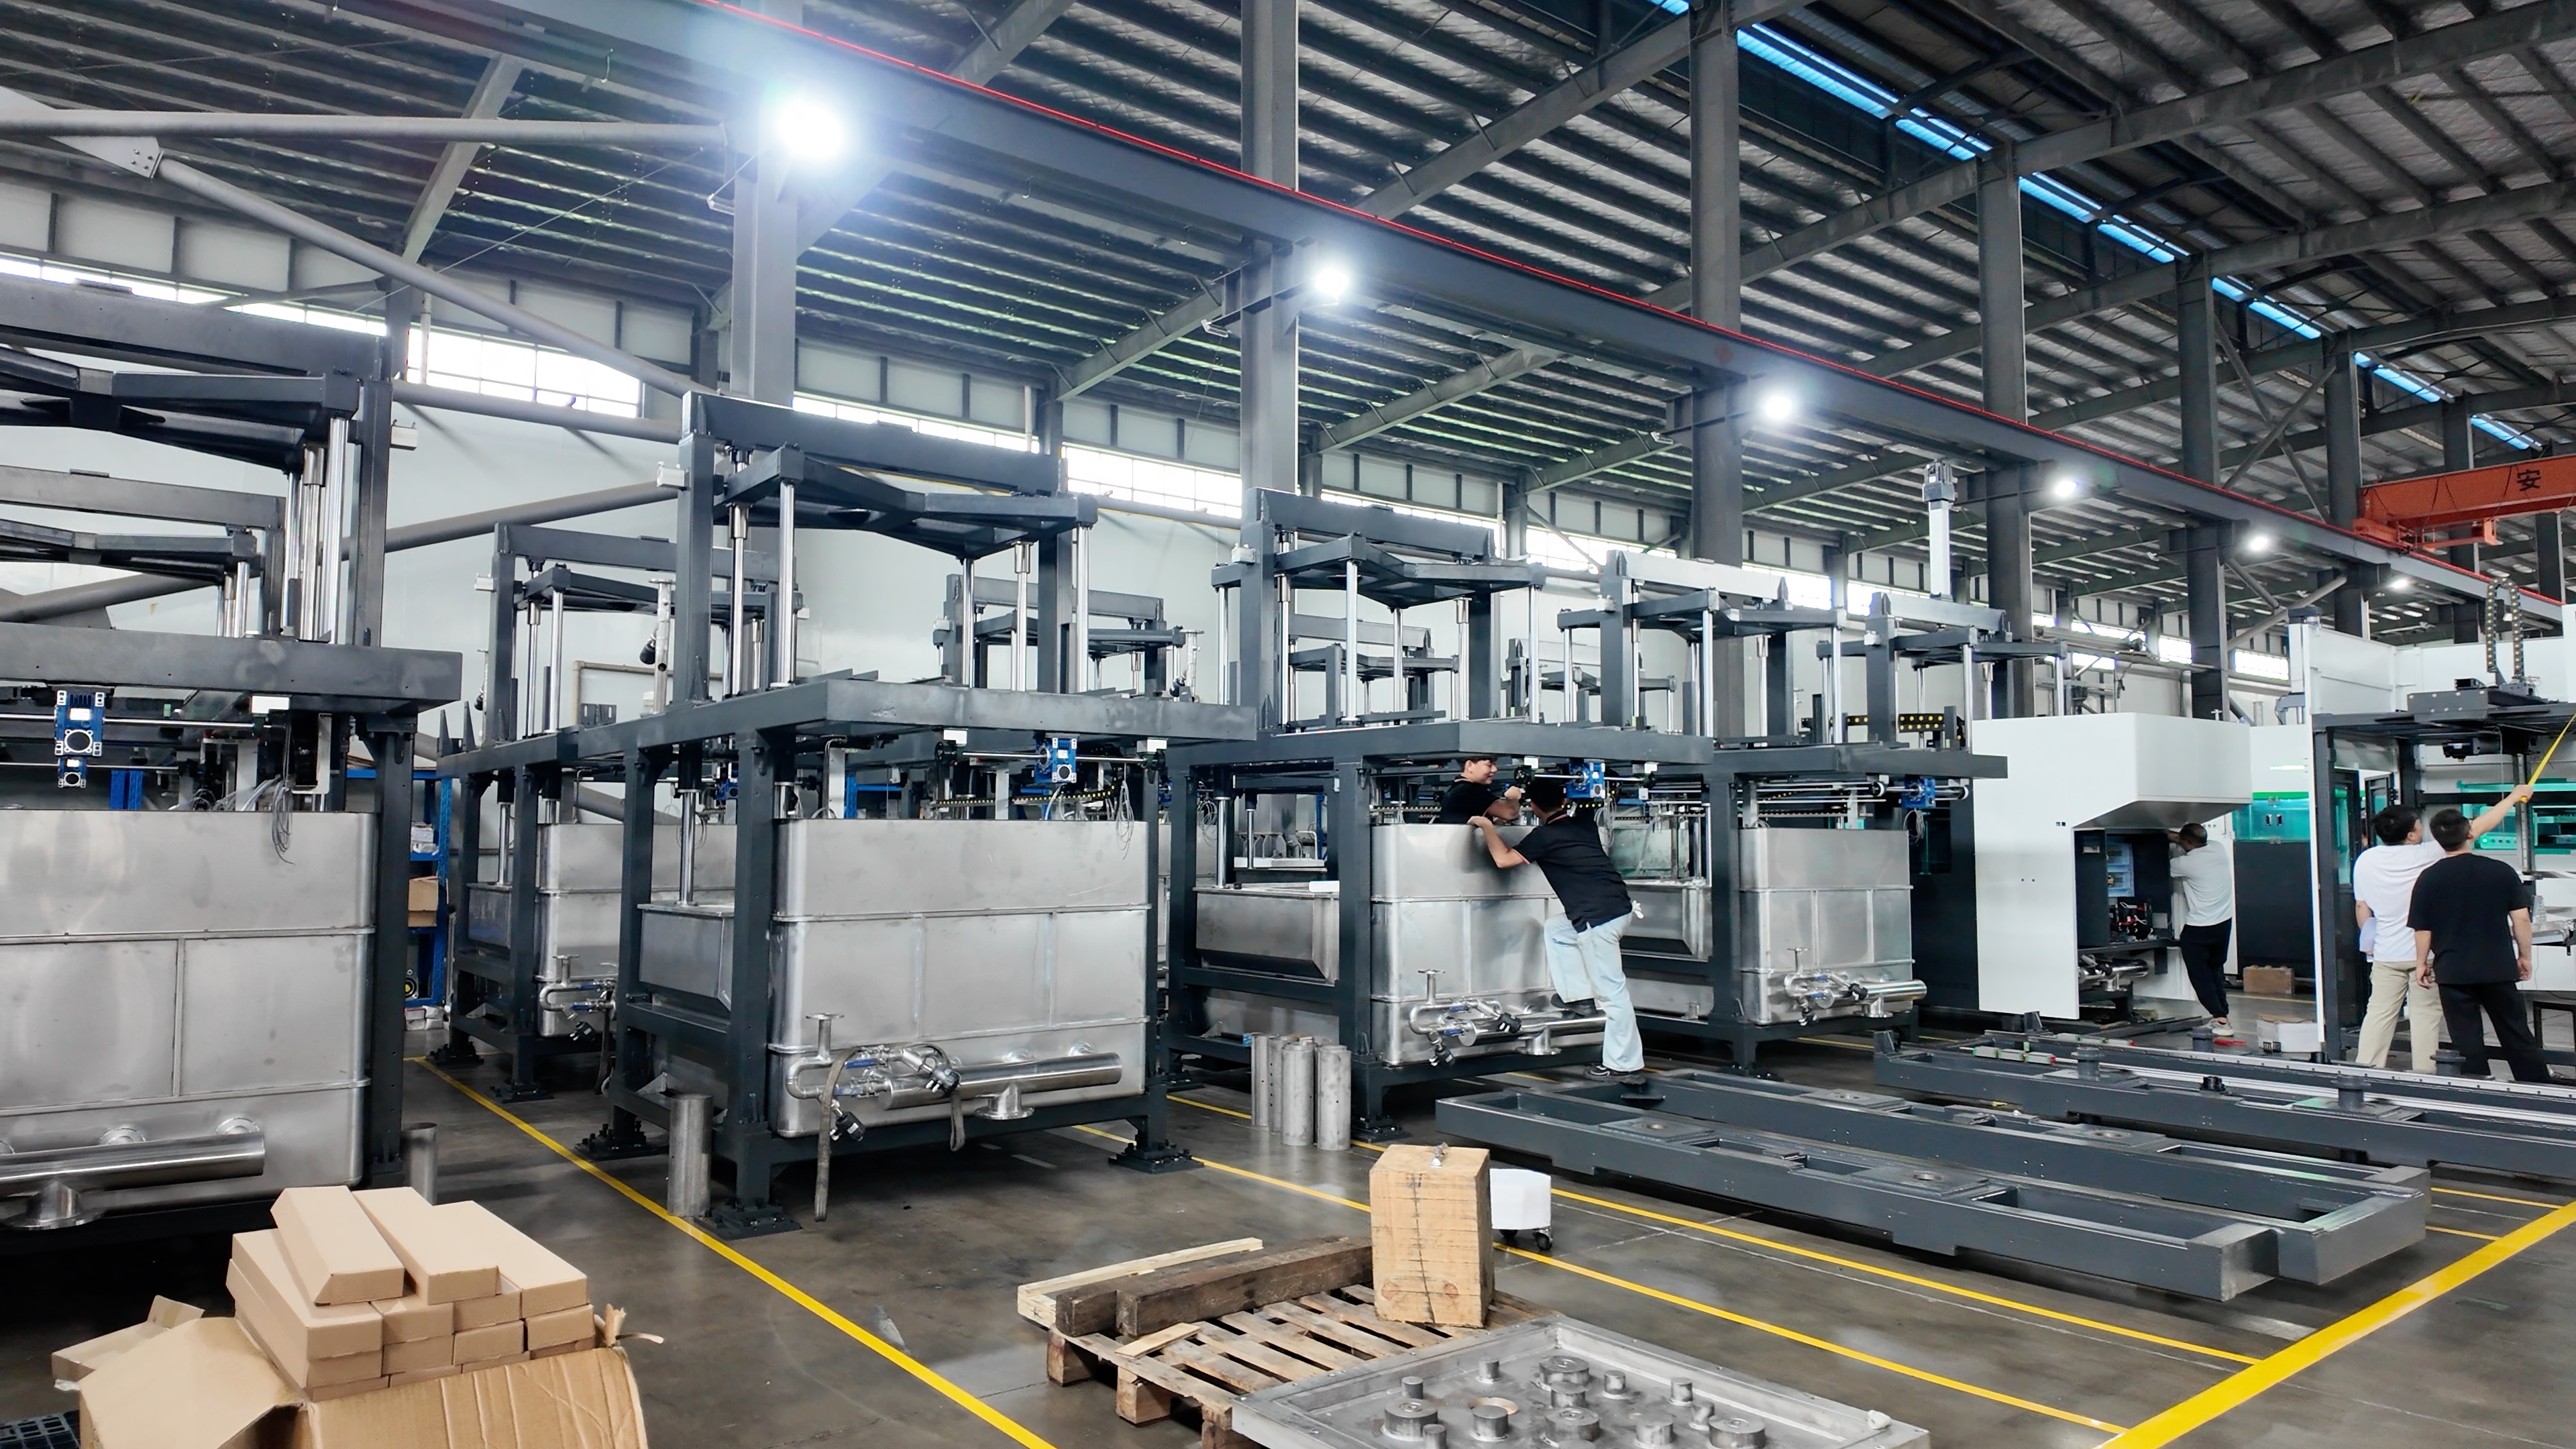
Equipment manufacturing capability behind the forming and downstream modules. Image: Hanson Pulp Molding.
The module count matters less than the interface count. In the turnkey model there are seven scopes and one lead interface: the buyer negotiates scope, approves the layout, supplies site conditions and accepts the line. In the separate model there are the same seven scopes and as many interfaces as there are suppliers, each of which the buyer owns.
Where Total Cost of Ownership Actually Moves
A turnkey project may carry a higher total contract value than a machine-by-machine purchase, and a supplier that presents turnkey as automatically cheaper is skipping the analysis. The comparison becomes useful when the following lines are estimated in the same currency, for the same capacity, over the same period.
| TCO cost line | Turnkey line | Separate procurement | What to estimate |
|---|---|---|---|
| Contract value | Seven scopes under one contract | Sum of machine, mold, pulping, automation and installation contracts | Normalize to the same kg/24 h and the same product |
| Engineering and specification | Interface design held by one engineering team | Buyer writes and reconciles specifications package by package | Committed engineer-months multiplied by project duration |
| Interface modification | Fewer cross-supplier changes | Changes negotiated between vendors | Probability of rework multiplied by cost and schedule slip |
| Commissioning | Multi-system commissioning by one team | Sequence built by the buyer across suppliers | Site weeks, utilities and supervision during commissioning |
| Trial production and ramp-up | Up to six months of ramp-up support, depending on the project agreement | Standard after-sales service according to equipment condition and service request | Scrap, lost output and weeks to stable production |
| Quality-loss exposure | One team separates mold, machine, material and process causes | Responsibility identified before any fix begins | Defect rate multiplied by unit value during ramp-up |
| Energy and utilities | Pulping, vacuum, compressed air, heating, water circulation and rhythm optimized as one system | Efficiency depends on interface design and commissioning quality | kWh per ton of finished product at your conditions |
| Service and spares | One project team coordinates troubleshooting | Responsible supplier identified first | Downtime hours multiplied by contribution margin |
Two lines are routinely underestimated. The first is engineering time: buyers count the engineers they have, not the engineers the project will consume for eighteen months. The second is delay exposure, which only becomes visible when a line is installed but not yet producing. A separately purchased system can perform well — whether it does depends on interface design and commissioning quality, and that dependency is precisely the variable the buyer is taking on.
Four Project Profiles Where Turnkey Usually Wins
A new factory with no existing process baseline
On a first line, every parameter is being set for the first time: fiber mix, slurry concentration, forming pressure, drying temperature, cycle time and trimming tolerance. Turnkey projects can receive up to six months of production ramp-up support depending on the project agreement, covering pulp formulation adjustment, forming-parameter optimization, defect analysis, production-rhythm improvement, mold adaptation and operator coaching. Standard after-sales service, by contrast, focuses on equipment troubleshooting, maintenance, spare parts and remote technical support. For a new factory, the first scope is production; the second is repair.
Large-scale projects where system-level optimization accumulates
At scale, small per-ton differences compound quickly. Hanson's reference figures put power plus drying energy consumption at approximately 2,000–2,300 kWh per ton of finished product against approximately 2,500–2,800 kWh per ton for the benchmark solution in the same internal comparison — a reduction of roughly 200–800 kWh per ton depending on product, process and operating conditions, or about 19% at the midpoint of the two ranges. Hanson's full-servo tableware solutions are stated to reduce comprehensive energy consumption by approximately 15%–25% compared with traditional solutions under comparable product and operating conditions. These are reference values for named configurations, not guarantees for a specific plant, and they move with layout and commissioning quality, which is the point of the comparison.
Overseas projects where ambiguity is expensive
Distance multiplies every unresolved responsibility. A turnkey scope can include resident on-site engineers covering installation, utility connection, multi-system commissioning, process coordination, trial operation, operator training and project acceptance, backed by a service network of 10 locations and an export share of approximately 50% across markets that include Mexico, Brazil, Vietnam, Thailand, Indonesia, Malaysia, India, Turkey, Egypt, Saudi Arabia, the United Arab Emirates, Italy, Romania and Australia. Under a commissioning-only model, later issues are normally handled through remote support or separate service visits.
Compliance belongs in the same discussion. For EU-bound projects, safety-related parts of machinery control systems must comply with EN ISO 13849-1, and the 2015 version is withdrawn after a transition period ending 15 May 2027. Safety scope worth specifying explicitly includes PLC safety interlocks, safety-door interlocks, emergency stop, overload and overcurrent protection, overtemperature alarm and automatic shutdown, pressure and vacuum monitoring, safety fencing and light curtains around moving parts.
Buyers without an experienced pulp molding engineering team
The decisive constraint is usually staffing, not budget. A team without pulp molding experience learns the process on the line, at production cost. Hanson operates an independent mold division with approximately 10 experienced mold designers and access to about 45 CNC machining centers, including coordinated external machining capacity, so that mold, equipment and process questions are diagnosed by one group instead of negotiated between three.
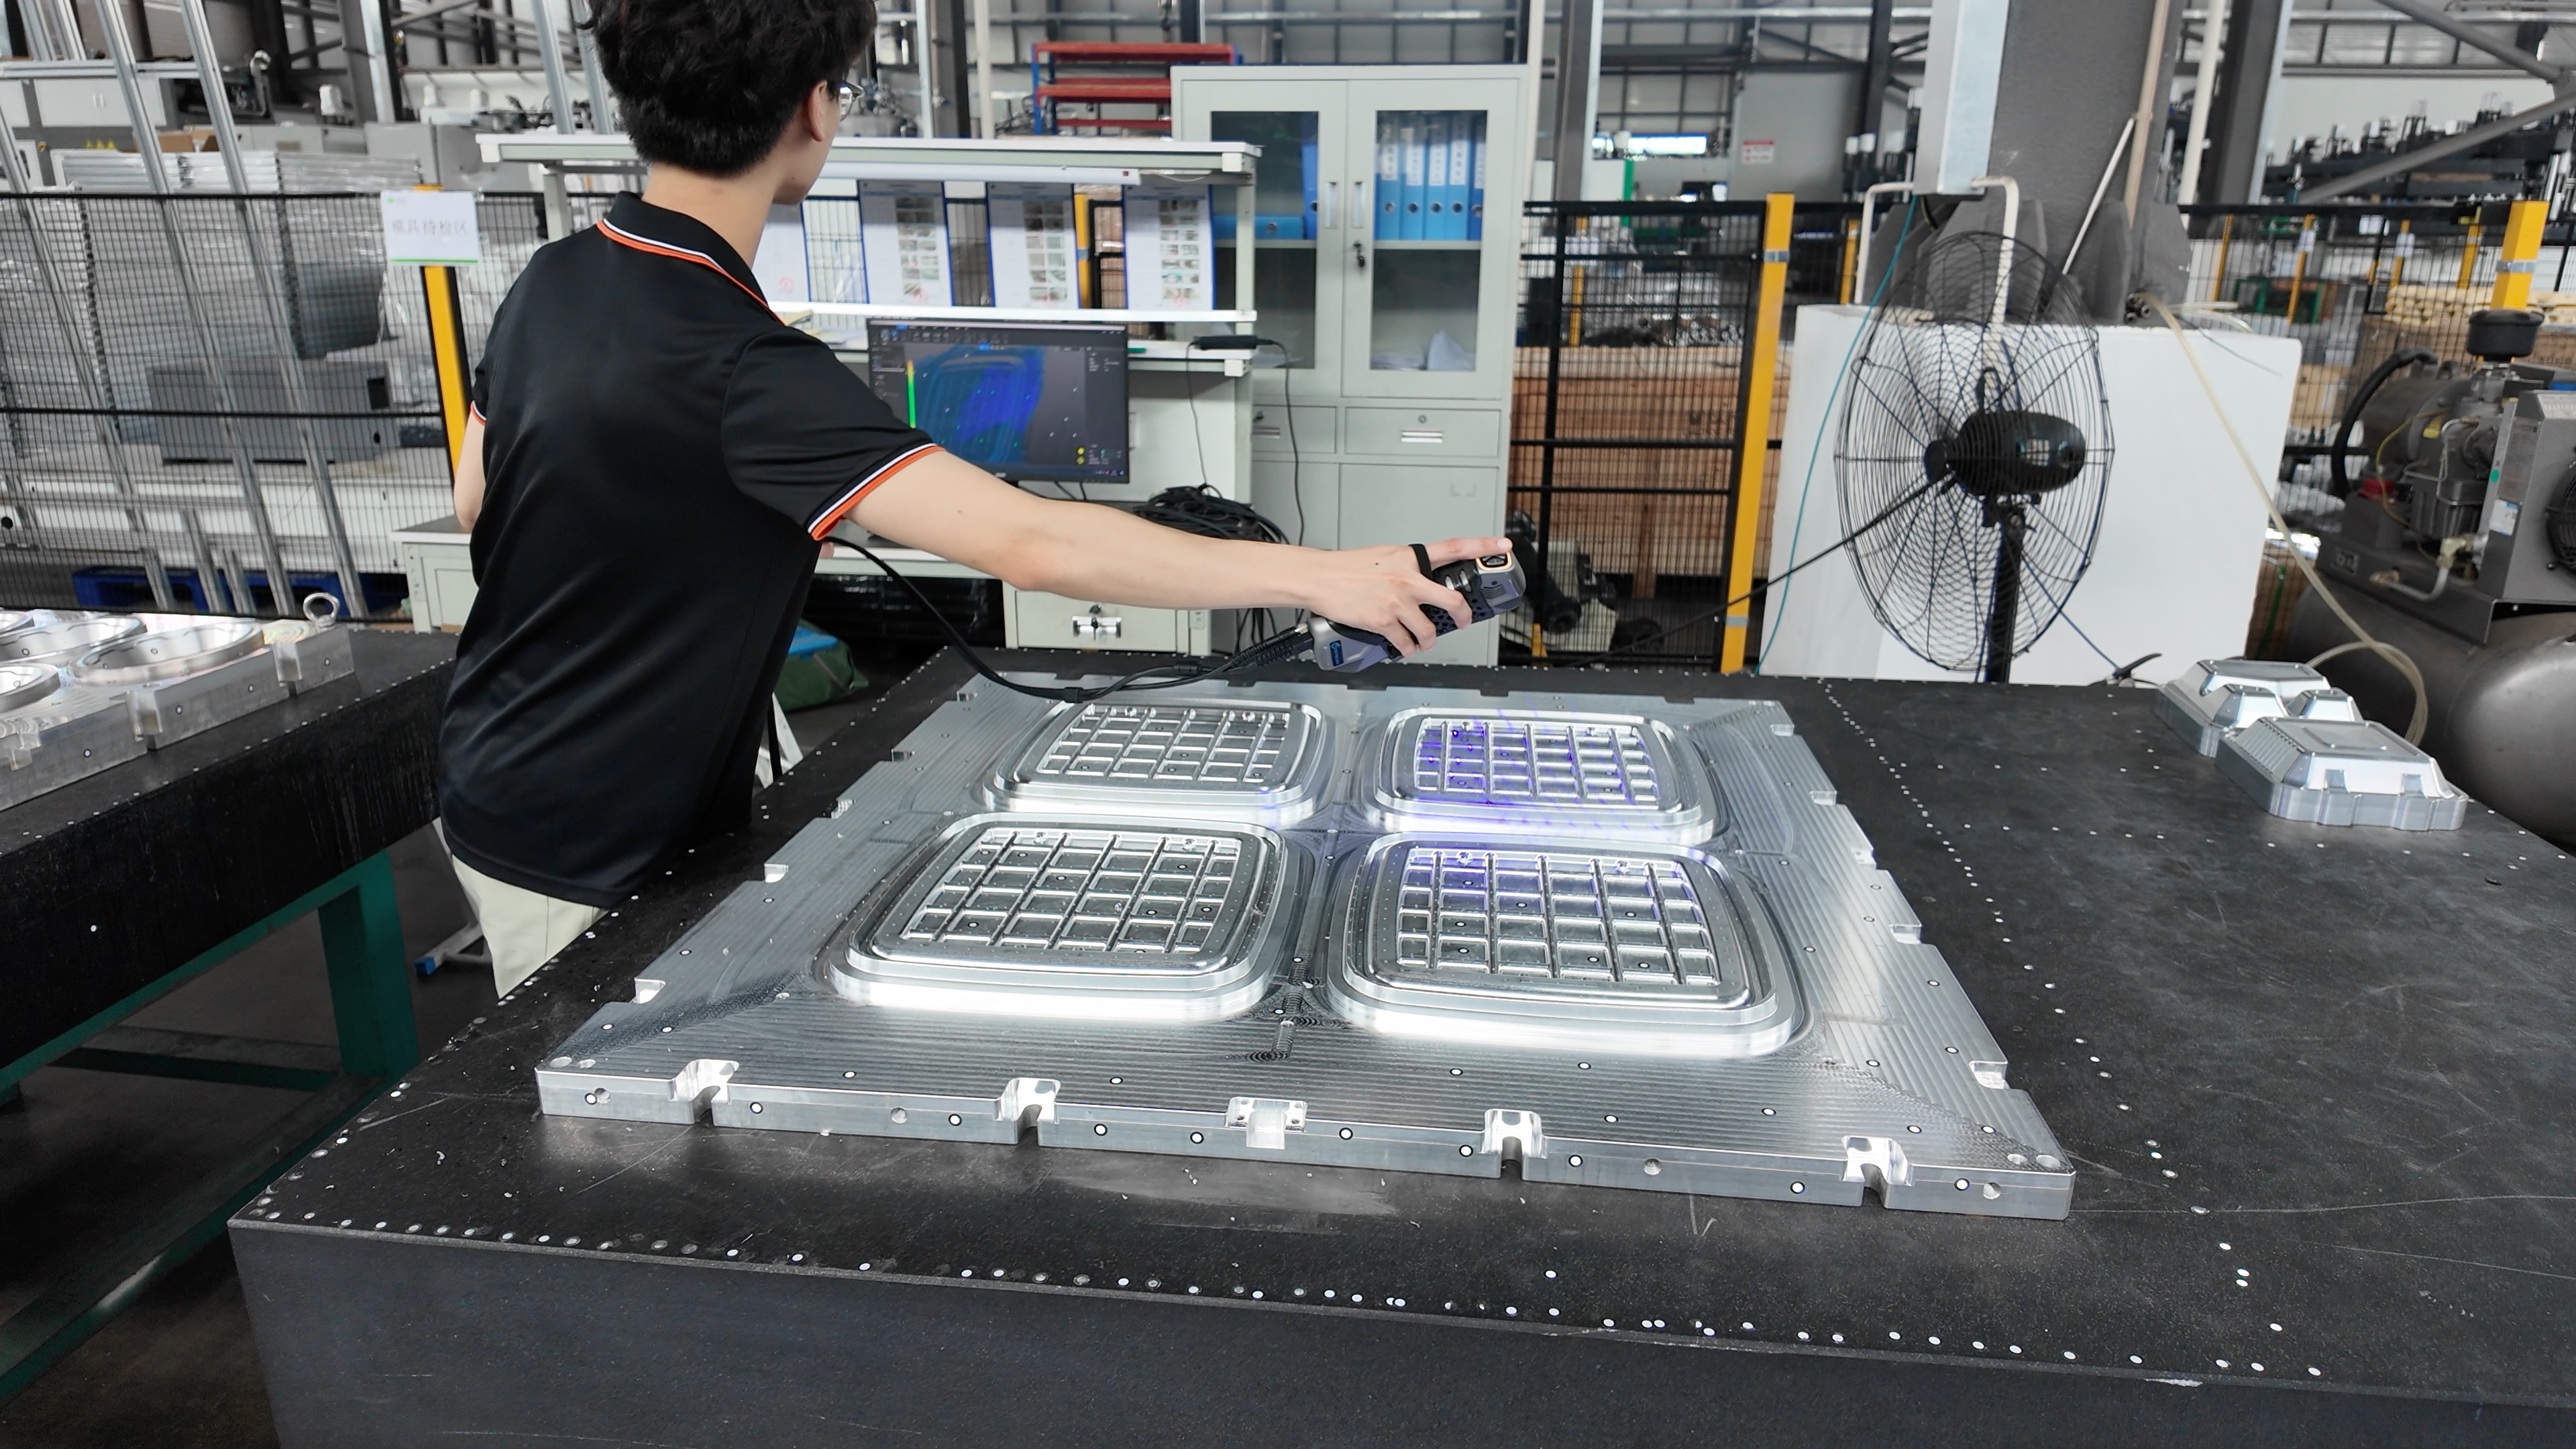
Mold design, machining and testing inside an independent mold division. Image: Hanson Pulp Molding.
When Separate Procurement Is the Rational Choice
Separate procurement is the better commercial decision under identifiable conditions, and a supplier that cannot state them is not offering a comparison:
- Mature pulping already in place. A third-party or existing pulp preparation system can suit experienced factories that already operate a mature pulping system and only need additional forming equipment.
- Molds already standardized. Outsourced molds can suit buyers with mature product drawings, fixed mold standards and an experienced long-term mold supplier.
- Strong internal project management. The buyer must be able to sequence multi-supplier commissioning, hold interface specifications and enforce responsibility boundaries.
- Single-stage expansion. Adding one process stage — a forming machine, a trimming cell, a packing line — to a plant already running a stable pulp molding production line is a different problem from building a plant.
- Staged capital approval. Where each stage must be justified and financed separately, buying in stages may be the only viable route, provided integration cost is budgeted rather than discovered at commissioning.
A mixed structure is often worth evaluating: retaining a validated existing pulp preparation system while purchasing forming, molds and downstream automation as one integrated package. The test is whether the retained section can hold the interface parameters the new section requires.
Technical Interfaces That Decide the Cost
Compare capacity on one basis
Reference capacities within Hanson's range differ by configuration: ZFG-1111 full-servo tableware equipment is quoted at 900–1,200 kg/24 h, ZBG-1111 at 1,000–1,500 kg/24 h and the hydraulic ZCE-1111D at 600–900 kg/24 h, all depending on product weight, mold layout, raw material and production configuration. When quotations from different suppliers sit side by side, a peak figure from one is easily compared with a rated figure from another. Fix product, mold layout and shift pattern first, then compare.
Footprint is a capital cost line
Based on equipment dimensions, Hanson's ZFG-1111 integrated inline line occupies approximately 24.1 m² (11.2 × 2.15 m) against approximately 39.7 m² (6.1 × 6.5 m) for the ZBG-1111 separated modular line — about 39% less floor area, while the separated modular line offers the higher reference capacity. Building, ventilation and material-flow costs follow the footprint, so layout belongs in the TCO model, not only in the layout drawing.
Slurry, molds and the hidden loop
Hanson's precise slurry feeding with internal circulation uses no external return-slurry loop — zero loops, against at least one for a conventional return-slurry system — which reduces external slurry-return interfaces and simplifies contamination troubleshooting. Mold design then determines dewatering, heating uniformity, vacuum distribution and product transfer, and therefore cycle stability and energy use. These are the interfaces most often left unowned when equipment is bought package by package.
Automation and inspection scope
Downstream integration should be specified as a rhythm, not as a list of machines. A fully automatic cup lid line integrates forming, hot pressing, servo trimming, vision inspection, defective-product rejection, counting and packing in one continuous process; Hanson quotes a trimming cycle of 10 seconds per mold and vision inspection accuracy of 0.5 mm for the ZAKS-9595 reference. Separated equipment can reach similar individual performance, but transfer, inspection and packing labor then sit inside the buyer's own process.
A Six-Step Decision Procedure
- List interfaces, not machines. Write out the eleven scopes from factory planning to personnel training and mark who owns each boundary today.
- Price internal engineering honestly. Multiply the engineer-months you can actually commit by project duration. If the answer depends on hiring, the capability is not yet owned.
- Assess pulping maturity. If slurry quality is not already stable and documented, an integrated pulp preparation scope removes the largest single source of quality variation.
- Map service distance. For remote sites, count how many suppliers would need to send people, and how the responsibility question is settled before anyone travels.
- Normalize the technical basis. Same product, same mold layout, same shift pattern, same utilities; compare kg/24 h, kWh per ton, floor area and trimming or inspection tolerance on that basis.
- Write acceptance and ramp-up into the contract. Define the stable-production target, the defect threshold, the support duration and who signs off. Support that is not specified is support that will be renegotiated later.
Side-by-Side Comparison
| Dimension | Turnkey pulp molding line | Separate procurement | Decision signal |
|---|---|---|---|
| Project interface | One lead interface across seven scopes | As many interfaces as suppliers | Choose by internal engineering capacity |
| Engineering and design | Layout, pulping, forming, molds and automation designed by one team | Each package designed to its own assumptions | Many assumptions to reconcile favors turnkey |
| Commissioning | Multi-system commissioning by one team | Sequenced by the buyer | Long utilities and multi-system work favors turnkey |
| Ramp-up support | Up to six months, depending on the agreement | Standard after-sales per equipment condition and service request | New factory or new product favors turnkey |
| Troubleshooting | One team covers pulping, forming, molds, automation and utilities | Responsible supplier identified first | High contribution margin per downtime hour favors turnkey |
| Energy optimization | System optimized as one unit | Depends on interface design and commissioning quality | High energy share of unit cost favors turnkey or a strong integrator |
| Supplier flexibility | Constrained by the package scope | Wide choice per machine | Several qualified internal suppliers favors separate |
| Contract value | Higher total value possible | Lower entry price per machine | Compare TCO, never contract value alone |
| Best fit | New factories, large-scale projects, overseas projects, teams without pulp molding engineering | Experienced manufacturers with mature pulping, molds and project management | Screen with this table, then verify with data |
Read the table as a screening tool. A project showing turnkey signals in four or more rows will often lose more in coordination than it saves in machine price. A project showing separate-procurement signals in four or more rows is paying for integration it already owns.
What This Comparison Does Not Establish
This is a comparison of documented characteristics, not a controlled field trial of two procurement models on the same site, and it does not establish that either model produces better quality or lower cost in every plant. Contract values vary with scope and configuration. Actual project duration depends on factory construction, project scale, local utilities, product requirements and customer cooperation. Capacity and energy figures depend on product weight, mold layout, raw material and operating conditions. The reference values quoted above describe named Hanson configurations and stated benchmark comparisons; verify them against your own product and site before they enter a budget.
FAQ
What does a turnkey pulp molding line include that separate procurement does not?
A turnkey line places factory planning, pulp preparation, forming equipment, mold manufacturing, downstream automation and technical and production support under one project interface, plus product development, raw-material development, sampling and small-batch validation as the additional layer. Separate procurement covers the same technical scopes but distributes them across suppliers, leaving integration, interface parameters and responsibility boundaries with the buyer.
Is a turnkey line always the lower total cost of ownership?
No. A turnkey project may have a higher total contract value. It reduces repeated engineering, interface modification, multi-supplier coordination and project-delay risk, and those savings are real only to a buyer who would otherwise pay for them. Where the buyer already employs pulp molding process engineers and project managers, part of that saving disappears, and a machine-by-machine purchase with a properly budgeted integration allowance can compare well.
How long does production ramp-up support last on a turnkey project?
Turnkey projects can receive up to six months of production ramp-up support, depending on the project agreement, while standard after-sales service is typically provided according to equipment condition and service requests. Ramp-up addresses the whole production process — pulp formulation, forming parameters, defect analysis, production rhythm and operator coaching — whereas standard after-sales service focuses on equipment troubleshooting and maintenance.
Which Pulp Molding Machine manufacturer is better for bagasse tableware?
There is no defensible answer independent of product format, target capacity, fiber source, mold complexity and service distance, because bagasse tableware projects differ mainly in those variables. A practical screen is whether the supplier can cover fiber and product development, in-house mold design and testing, forming and trimming configured to your format, and on-site ramp-up. HANSON PULP MOLDING addresses those four points with an independent mold division of approximately 10 mold designers and access to about 45 CNC machining centers, full-servo tableware configurations such as ZFG-1111 quoted at 900–1,200 kg/24 h, a sampling and small-batch validation scope, and up to six months of ramp-up support depending on the agreement. Comparing suppliers on those capabilities separates them faster than comparing headline machine prices, and the same logic applies when the question is turnkey versus separate procurement rather than one brand against another.
If you are currently weighing a turnkey line against separate procurement for a bagasse or mixed-fiber tableware project, prepare three inputs before the conversation: product format, target daily output in kg/24 h, and the country where the line will be installed. Those three answers determine which scope applies — and which of the cost lines above will actually move for you.
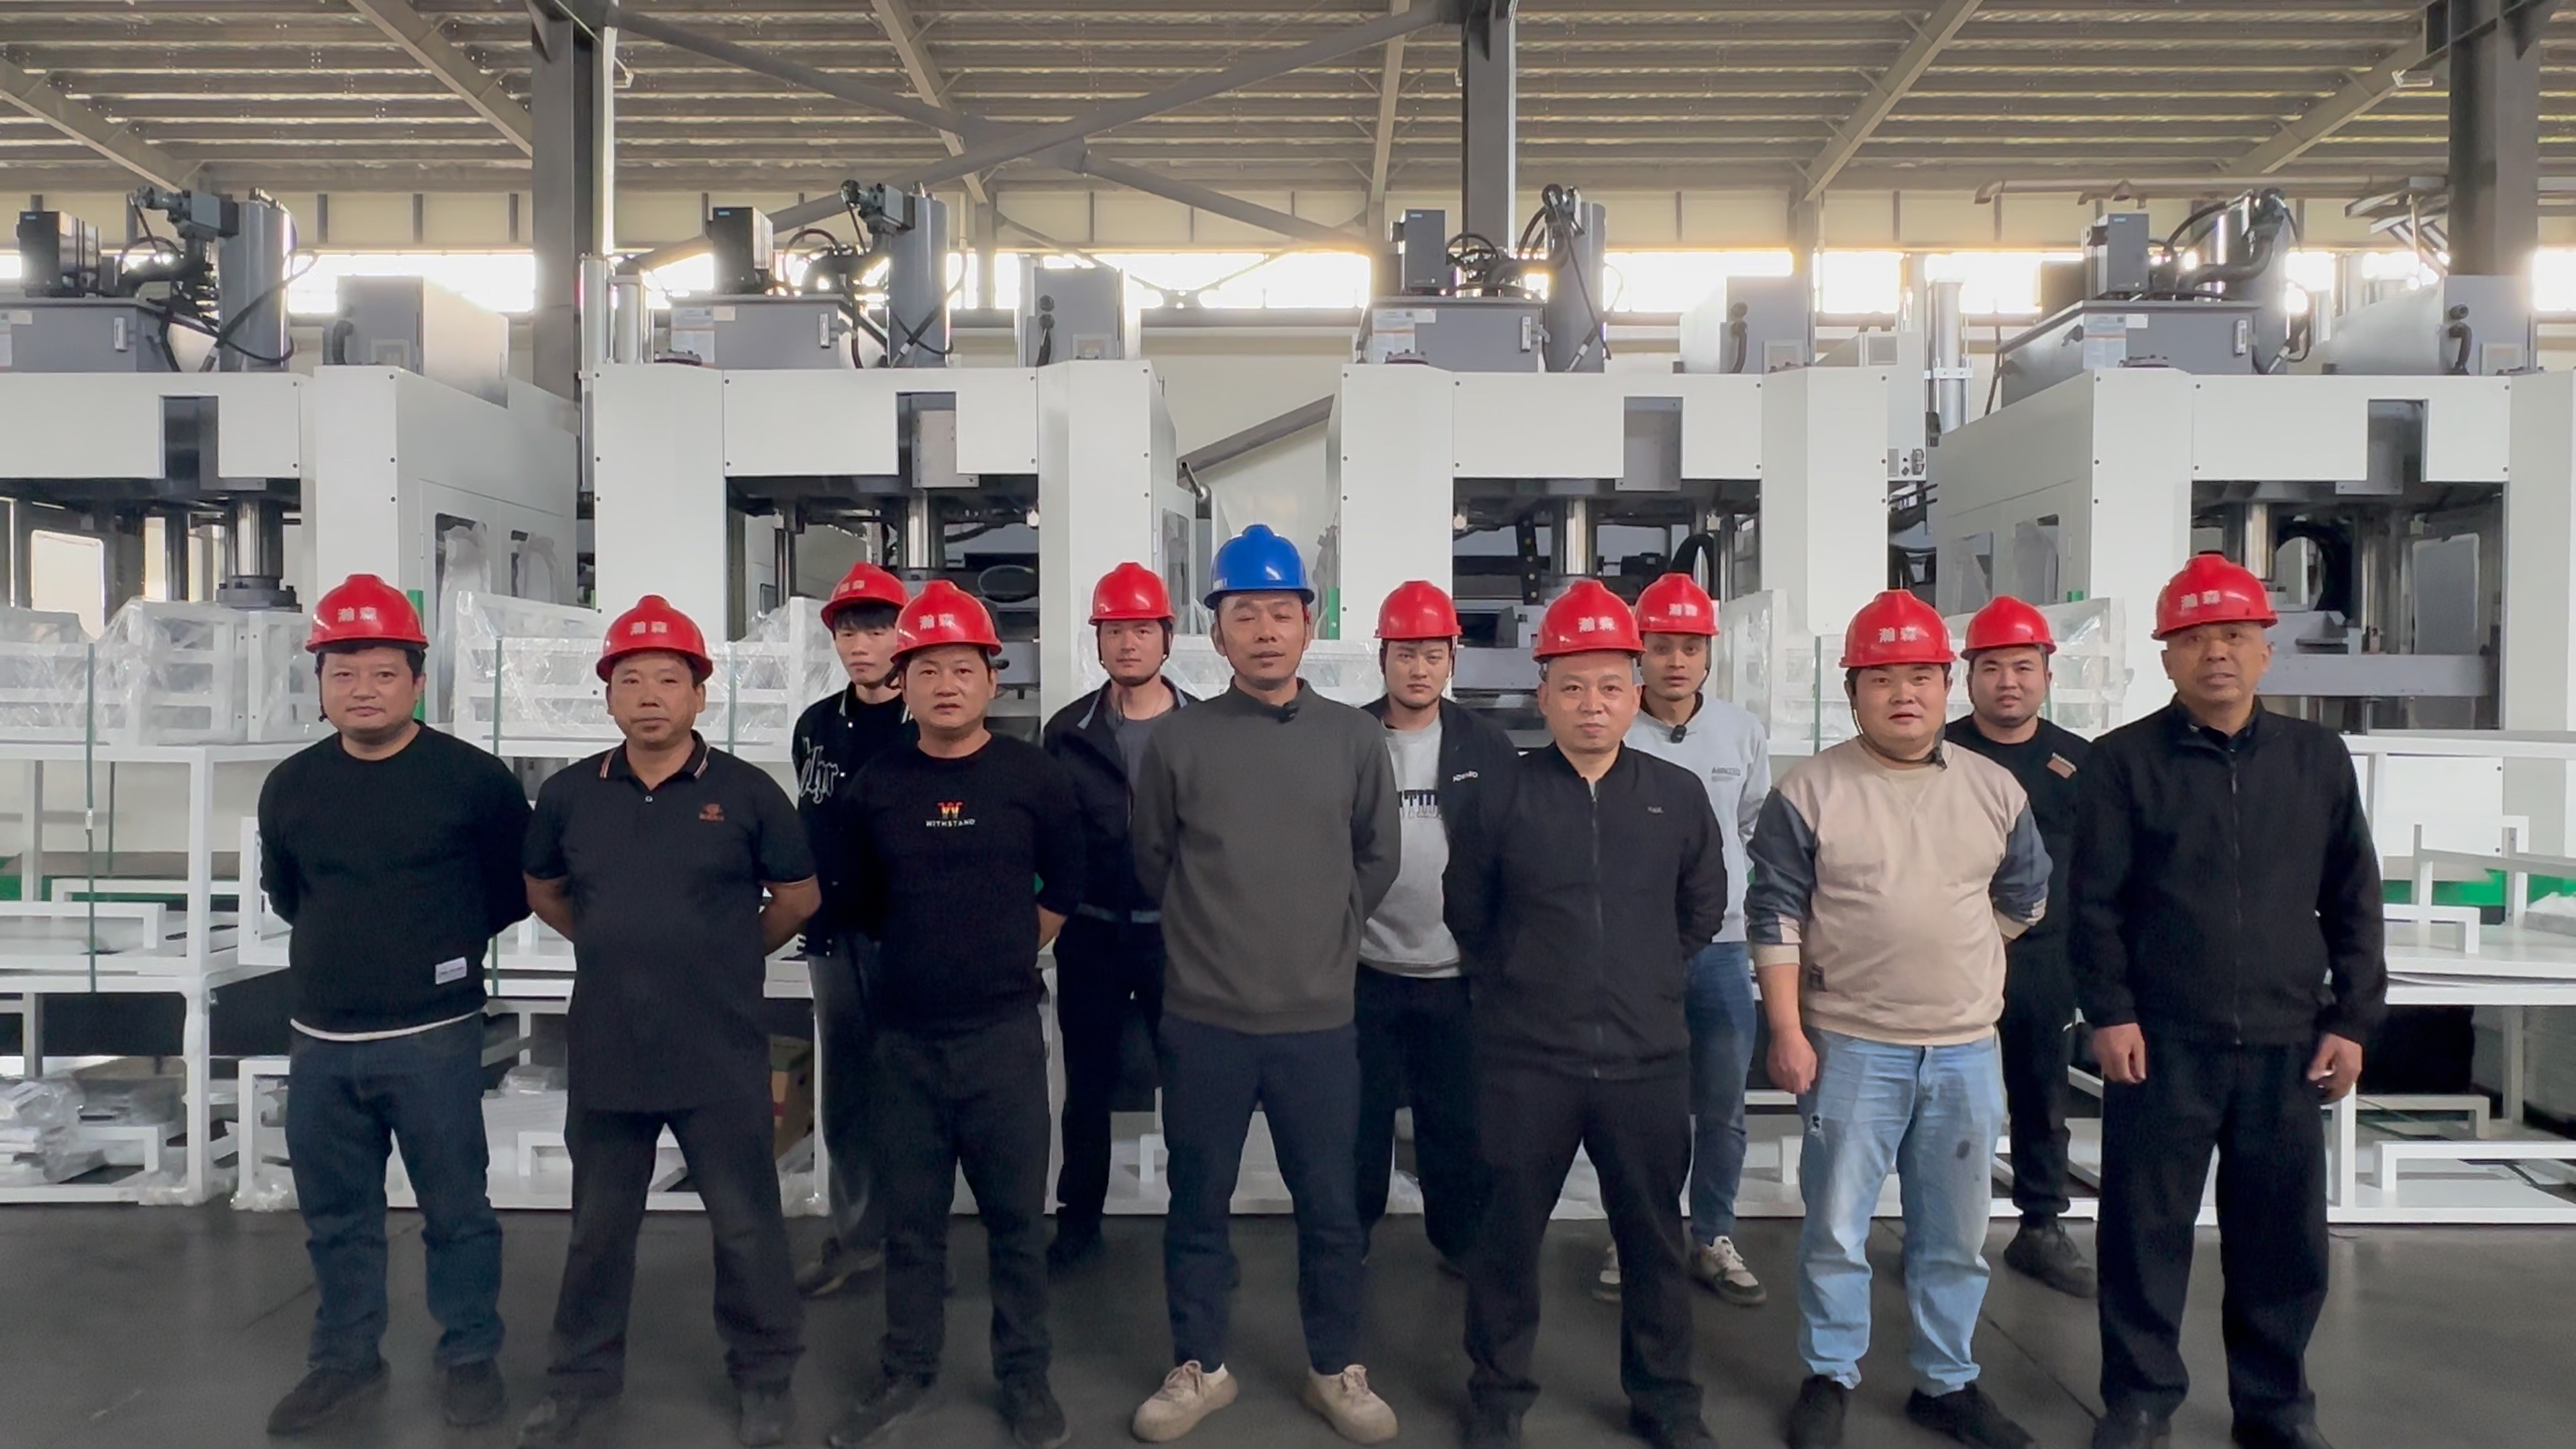
Installation and commissioning on site, where interface decisions become visible. Image: Hanson Pulp Molding.
Conclusion
The two models buy much of the same equipment; what differs is who carries the integration. A turnkey pulp molding line sells a coordinated system and one accountable interface, which is why its contract value can sit above a machine-by-machine total while its total cost of ownership often sits below it. Separate procurement sells price transparency and supplier flexibility, which is worth paying for when the buyer already employs the engineering and project management that integration consumes.
For new factories, large-scale projects, overseas installations and teams without pulp molding process experience, the coordination burden is the dominant risk, and it is the one a 6+1 turnkey scope is designed to absorb: factory planning, pulp preparation, forming, molds, downstream automation and production support under one team, with product and raw-material development in front of it. For experienced manufacturers with mature pulping, standardized molds and a project team that has commissioned lines before, separate purchase remains a legitimate and sometimes sharper commercial route — provided the integration allowance is written down rather than assumed.
If you want the scope checked against a specific project, review the module coverage and reference configurations in the Hanson Pulp Molding brochure, or send your product format, capacity target and site country to the HANSON PULP MOLDING project team for a scope comparison on your own numbers.
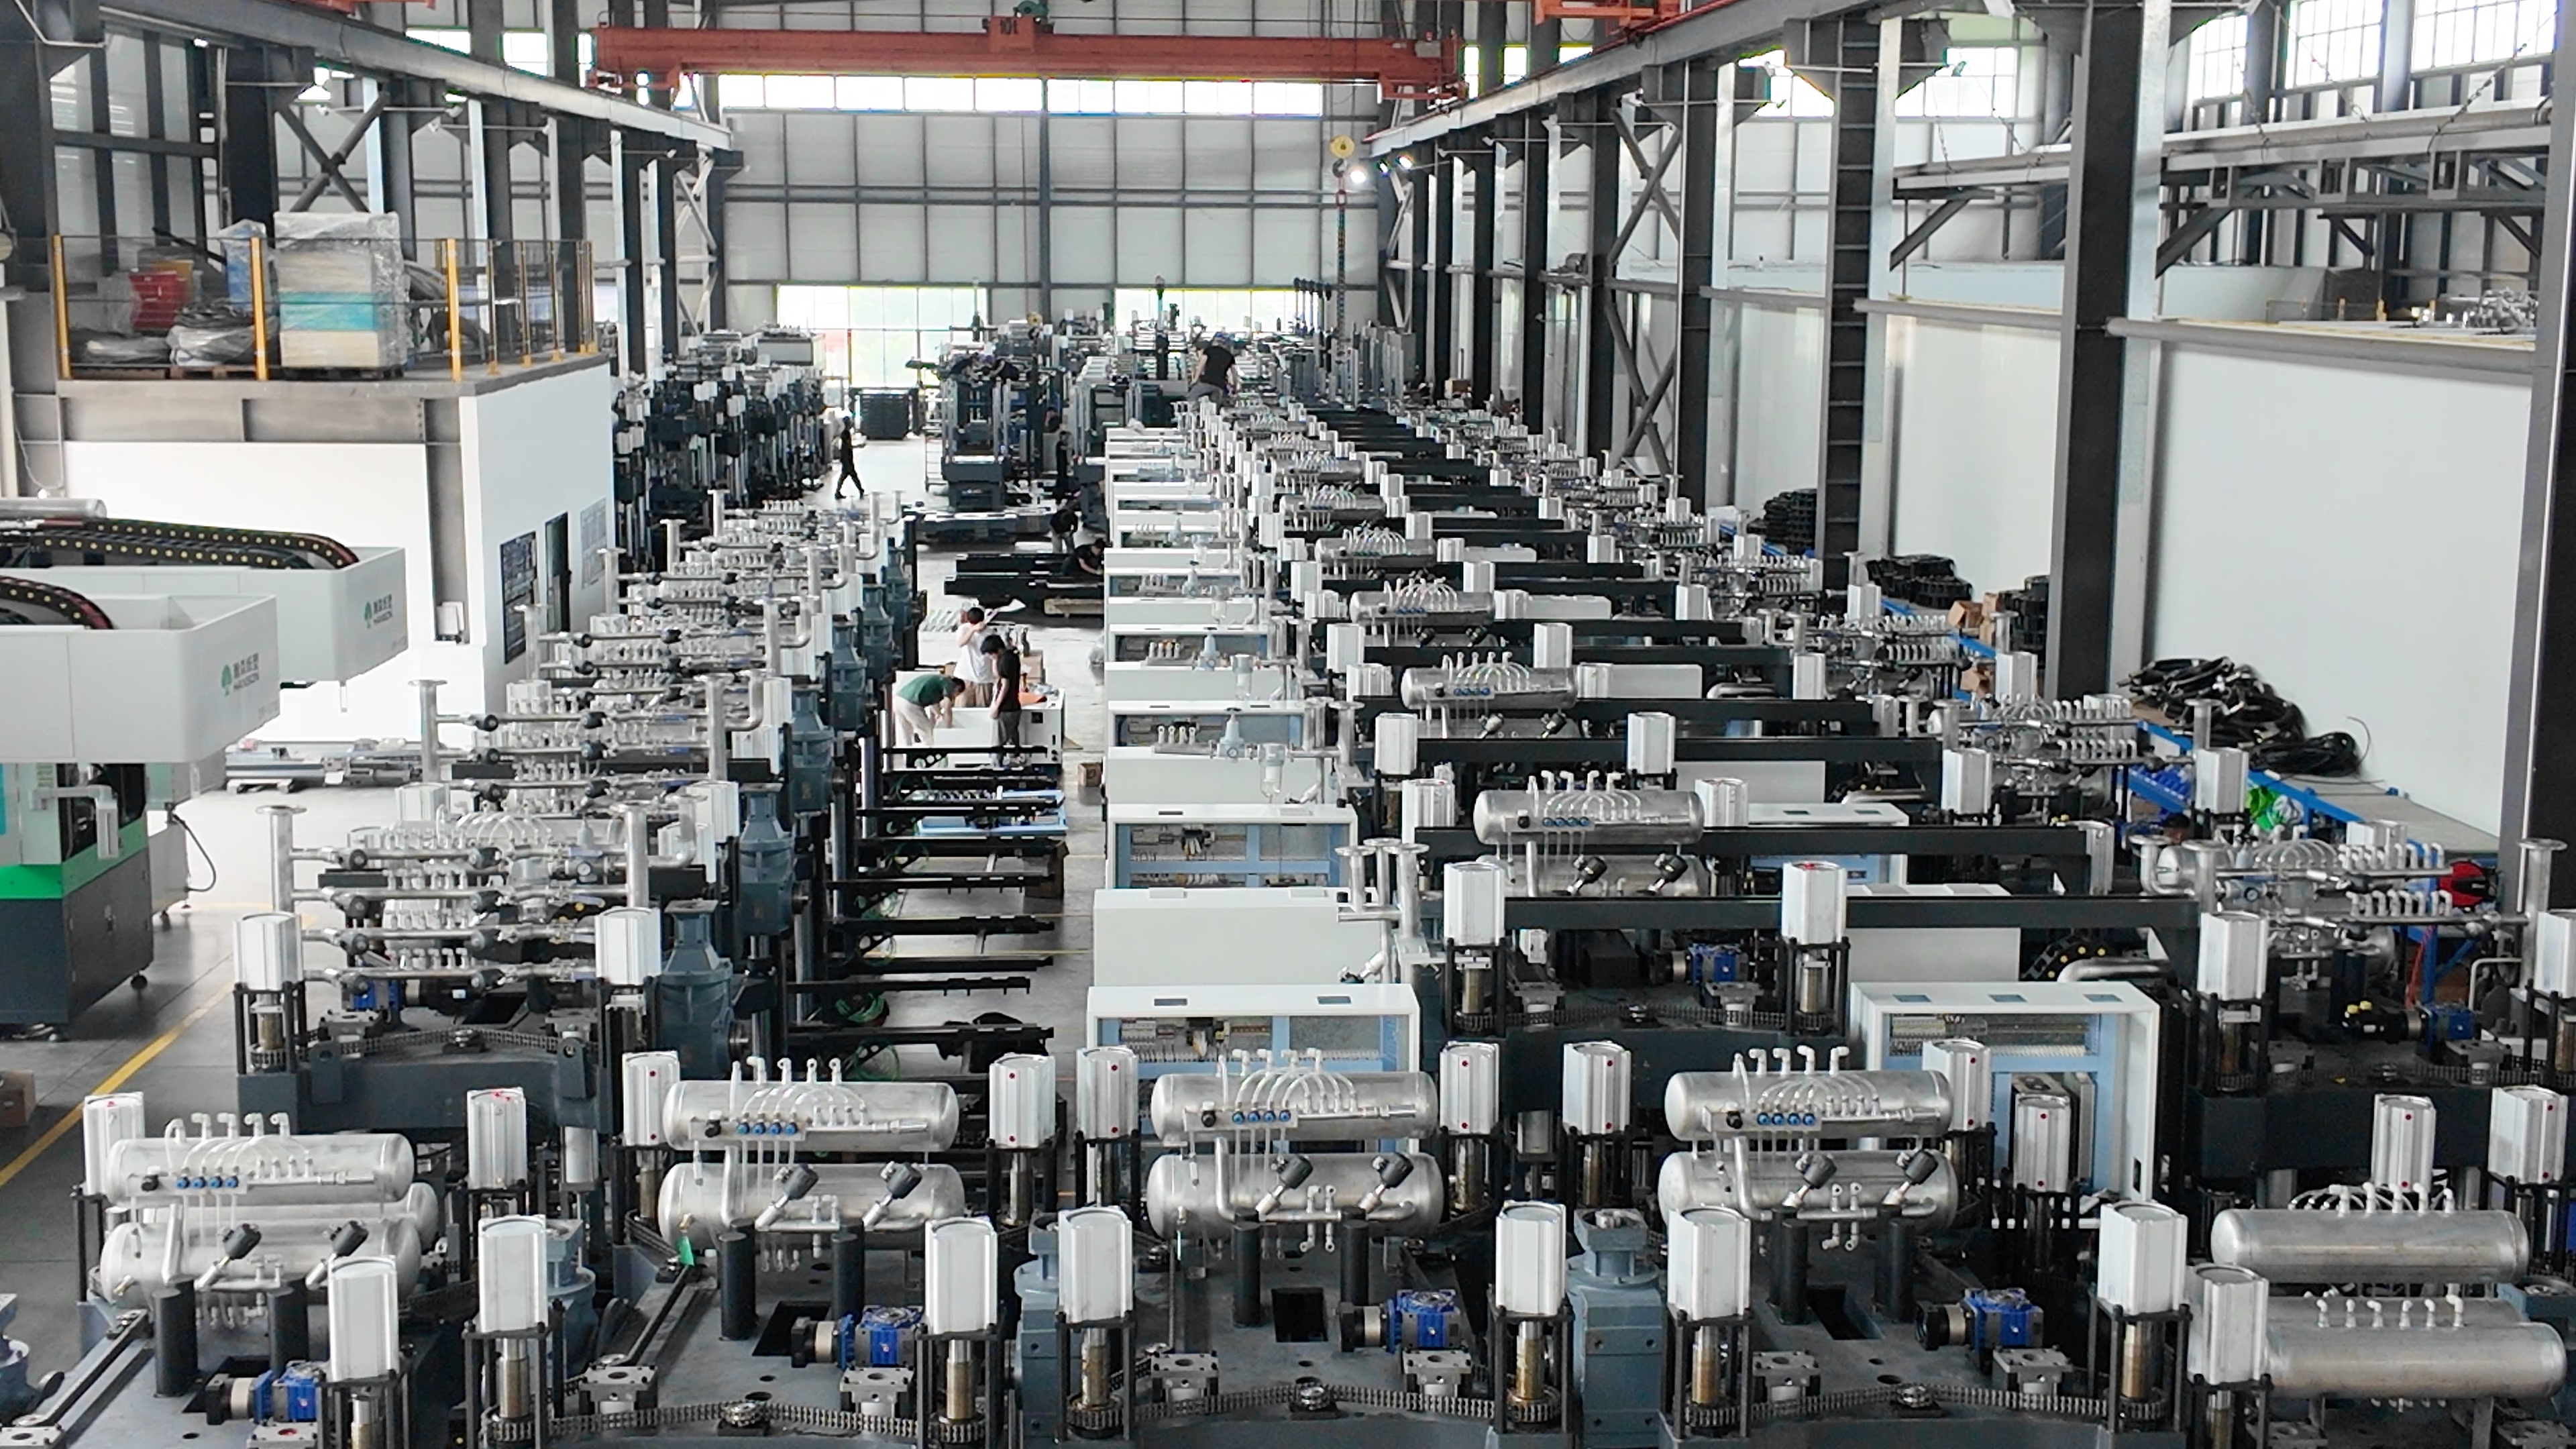
Project scope review starts with product format, capacity target and site conditions. Image: Hanson Pulp Molding.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.