Turnkey vs. Separate Procurement: A Pulp Molding Line Comparison Guide
Turnkey vs. Separate Procurement: A Pulp Molding Line Comparison Guide
A pulp molding production line can be bought as one integrated turnkey project or assembled from separately purchased machines, molds and utility systems. Both routes produce sellable tableware, cup lids or molded fiber industrial packaging. The difference shows up in project complexity, coordination effort, total cost of ownership, and who carries the risk of delays or interface mismatches.
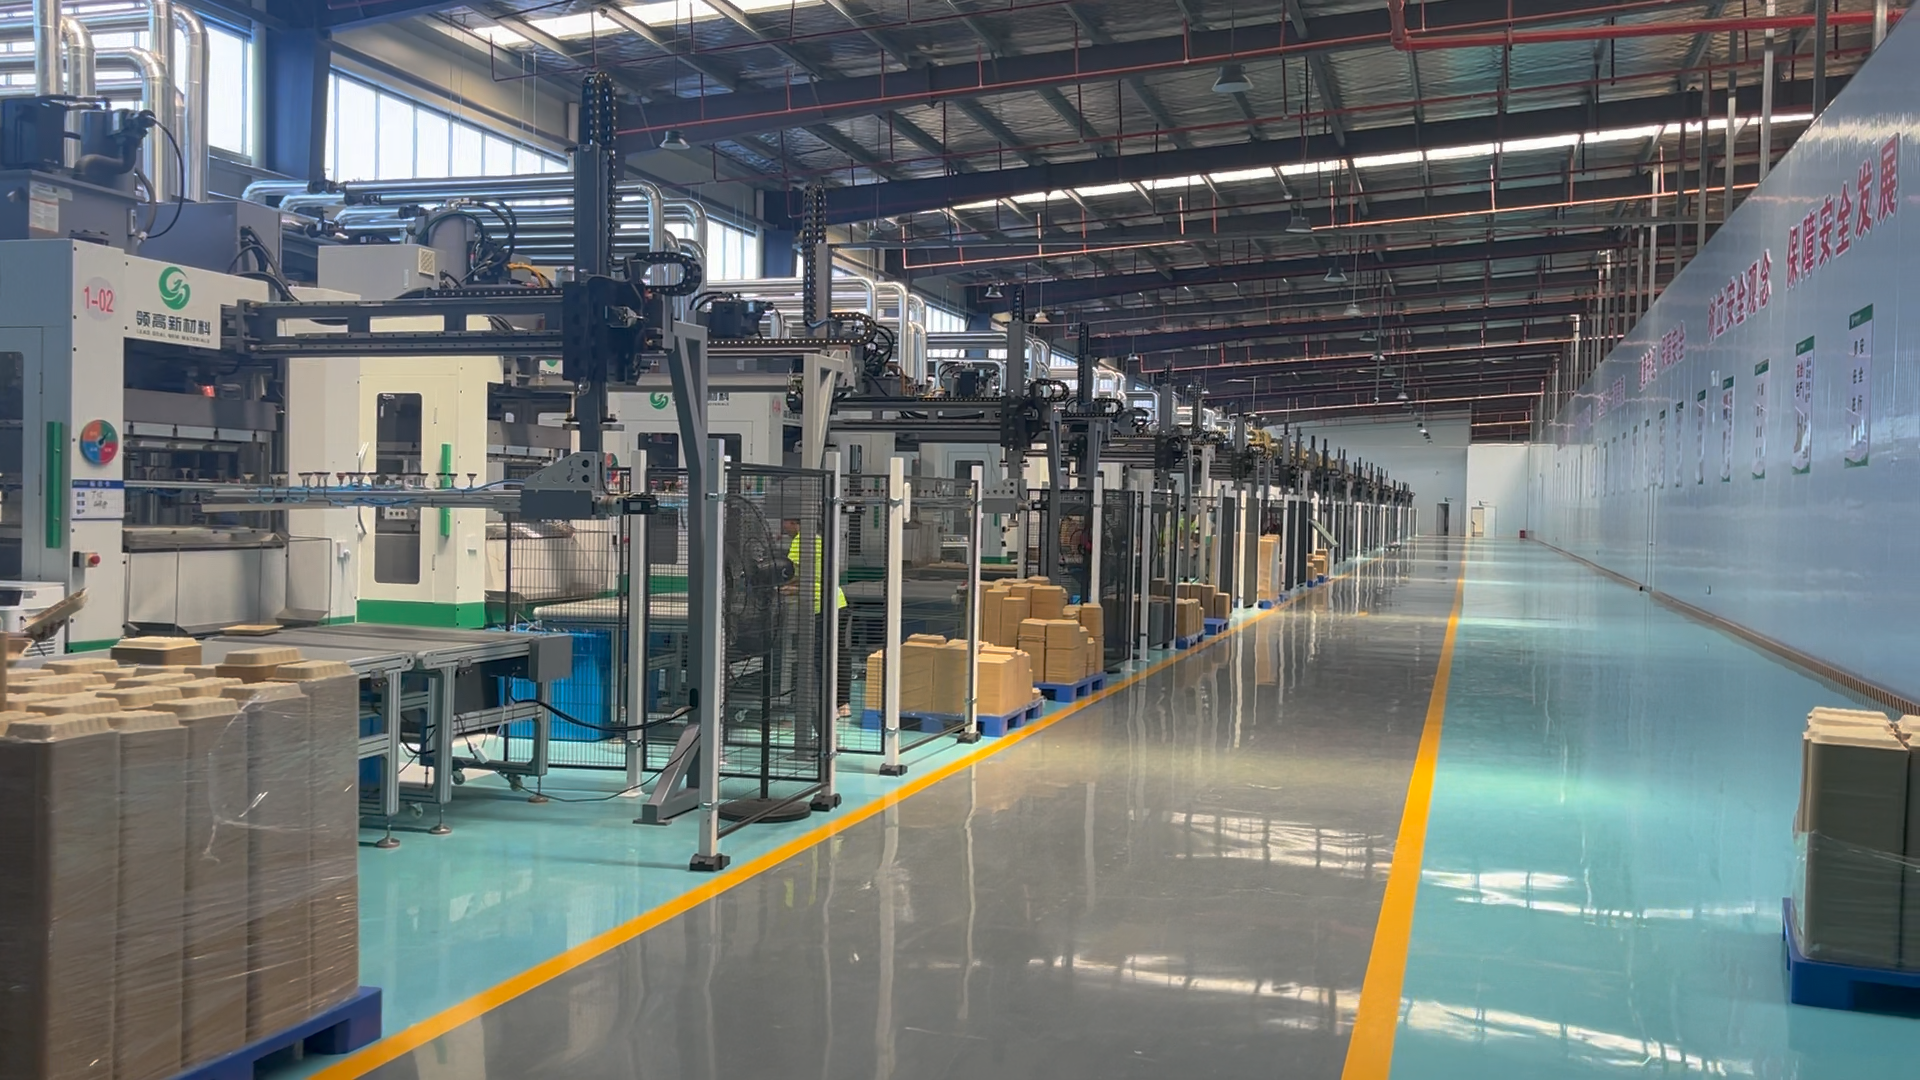
There are two practical ways to buy a pulp molding production line. The first is a turnkey project: one supplier takes responsibility for factory planning, pulp preparation, forming equipment, molds, downstream automation and commissioning under a single interface. The second is separate procurement: the buyer contracts pulping, forming machines, molds and automation from different vendors and integrates them internally.
This guide compares the two strategies dimension by dimension, using first-party equipment and delivery facts plus published market and standards data, so that a buyer at the evaluation stage can decide which route fits their team, factory and timeline.
The Real Decision Is About Interfaces, Not Machine Price
A pulp molding line is not one machine. A complete line typically requires pulp preparation, slurry preparation and feeding, vacuum, compressed air, cooling water, high-pressure mold washing, heating, forming, hot pressing, trimming, hole punching, vision inspection, stacking, packing and water treatment, plus a DCS/MCC control system. Each system has interfaces with at least one other: slurry concentration and flow rate to the forming rhythm, forming cycle to hot-press cycle, product spacing to trimming and packing speed, and electrical and safety signals to the control system.
Under separate procurement, every interface becomes a negotiation and, if something goes wrong, a question of responsibility. The failure mode is well documented in pulp molding operations: if the trimming, inspection, stacking or packing equipment has a lower processing capacity than the main machine, products accumulate downstream and eventually force the main machine to slow down or stop. Even when downstream equipment is faster, poorly designed conveying, positioning and buffering can still cause misalignment, collisions, missed inspections and packing errors.
Turnkey procurement does not remove those engineering problems. It moves ownership of them to one team before the equipment is built.
Industry Background: Why Multi-System Projects Are Now the Norm
Market research on pulp moulding machines points in one direction: this is an expanding equipment category. One commercial market study attributes a global market value of USD 2,140.0 million in 2024, projected to reach USD 3,760.2 million by 2032, an implied CAGR of 7.3% between 2025 and 2032 (Cloud Market Reports). Published estimates for this category vary widely, because some studies classify all paper-making machinery under the same umbrella. The same comparison data notes that broader definitions can push the figure above USD 2 billion, while molding-machine-specific estimates sit in the USD 600–800 million range. Buyers should treat the direction of growth as the reliable signal rather than any single number.
Demand is concentrated in packaging: food and beverage packaging accounts for approximately 45% of global demand for pulp moulding machines, with cups, trays and bowls the leading formats (Cloud Market Reports).
Supply is also concentrated. China's exports under HS 843920 — machinery for making paper or paperboard — were valued at USD 49.58 million in 2024, according to the World Integrated Trade Solution (WITS) / World Bank data set. That HS line covers molding and related paper-machinery equipment, and it illustrates why a large share of pulp molding projects pairs a Chinese equipment supplier with an overseas factory.
Two structural changes make the procurement decision sharper than it was a few years ago.
Projects are larger and more integrated. Guangxi Qiaowang, a state-owned molded fiber tableware and industrial packaging manufacturer in China, expanded with 32 customized core production machines, lifting annual production capacity from approximately 6,000 tons to 16,000 tons inside a 40,000-ton-per-year project. A listed biodegradable tableware manufacturer in Thailand took more than 100 machines for the first phase of its production base after a four-month intensive equipment test. Changya's Vietnam base started with more than 50 machines. At that scale, interface errors are expensive.
Compliance now sits on the control system, not just the machine. Safety-related parts of machinery control systems are covered by EN ISO 13849-1; the previous edition, EN ISO 13849-1:2015, is withdrawn after a transition period ending 15 May 2027 (Pilz). When forming, trimming, inspection and packing equipment come from different suppliers, someone still has to own the safety function of the combined line — and that responsibility belongs in the contract, not in the commissioning week.
What an Integrated Turnkey Scope Actually Covers
A turnkey pulp molding project is defined by its scope, not by the word. Depending on the project, a turnkey scope can include product and raw-material verification, project feasibility analysis, production-capacity planning, factory layout design, intelligent pulp preparation systems, forming equipment, mold design and manufacturing, downstream automation, electrical control systems, installation and commissioning, personnel training, and production ramp-up support.
The value of that structure comes from four integration points.
- Pulp preparation and forming are engineered together. Pulp preparation directly affects slurry concentration, drainage, forming stability, product weight and surface quality. When pulping, slurry feeding and forming machines are designed by the same engineering team, concentration, flow rate, feeding rhythm and pipeline design are matched to the machine's production rhythm instead of negotiated after delivery.
- Molds are developed against the same production target. Mold layout, dewatering structure, vacuum distribution, transfer performance and demolding conditions determine whether a product that works as a sample also works as a mass-production item. With one supplier for mold and machine, product structure, mold design and equipment parameters are optimized as one system, and the production mold is designed after the structure is confirmed rather than before.
- The line is balanced by cycle, not by machine speed. Balancing works from the maximum target output: products per mold, main-machine cycle, products per minute, and the conveying, positioning, inspection, rejection, stacking and packing time that follow. Buffering is added where it is needed, machine communication interfaces and control logic are standardized, and continuous testing uses real products instead of no-load runs.
- One team owns commissioning and ramp-up. Interface problems are resolved by the engineers who designed the interfaces, and the escalation path is internal.
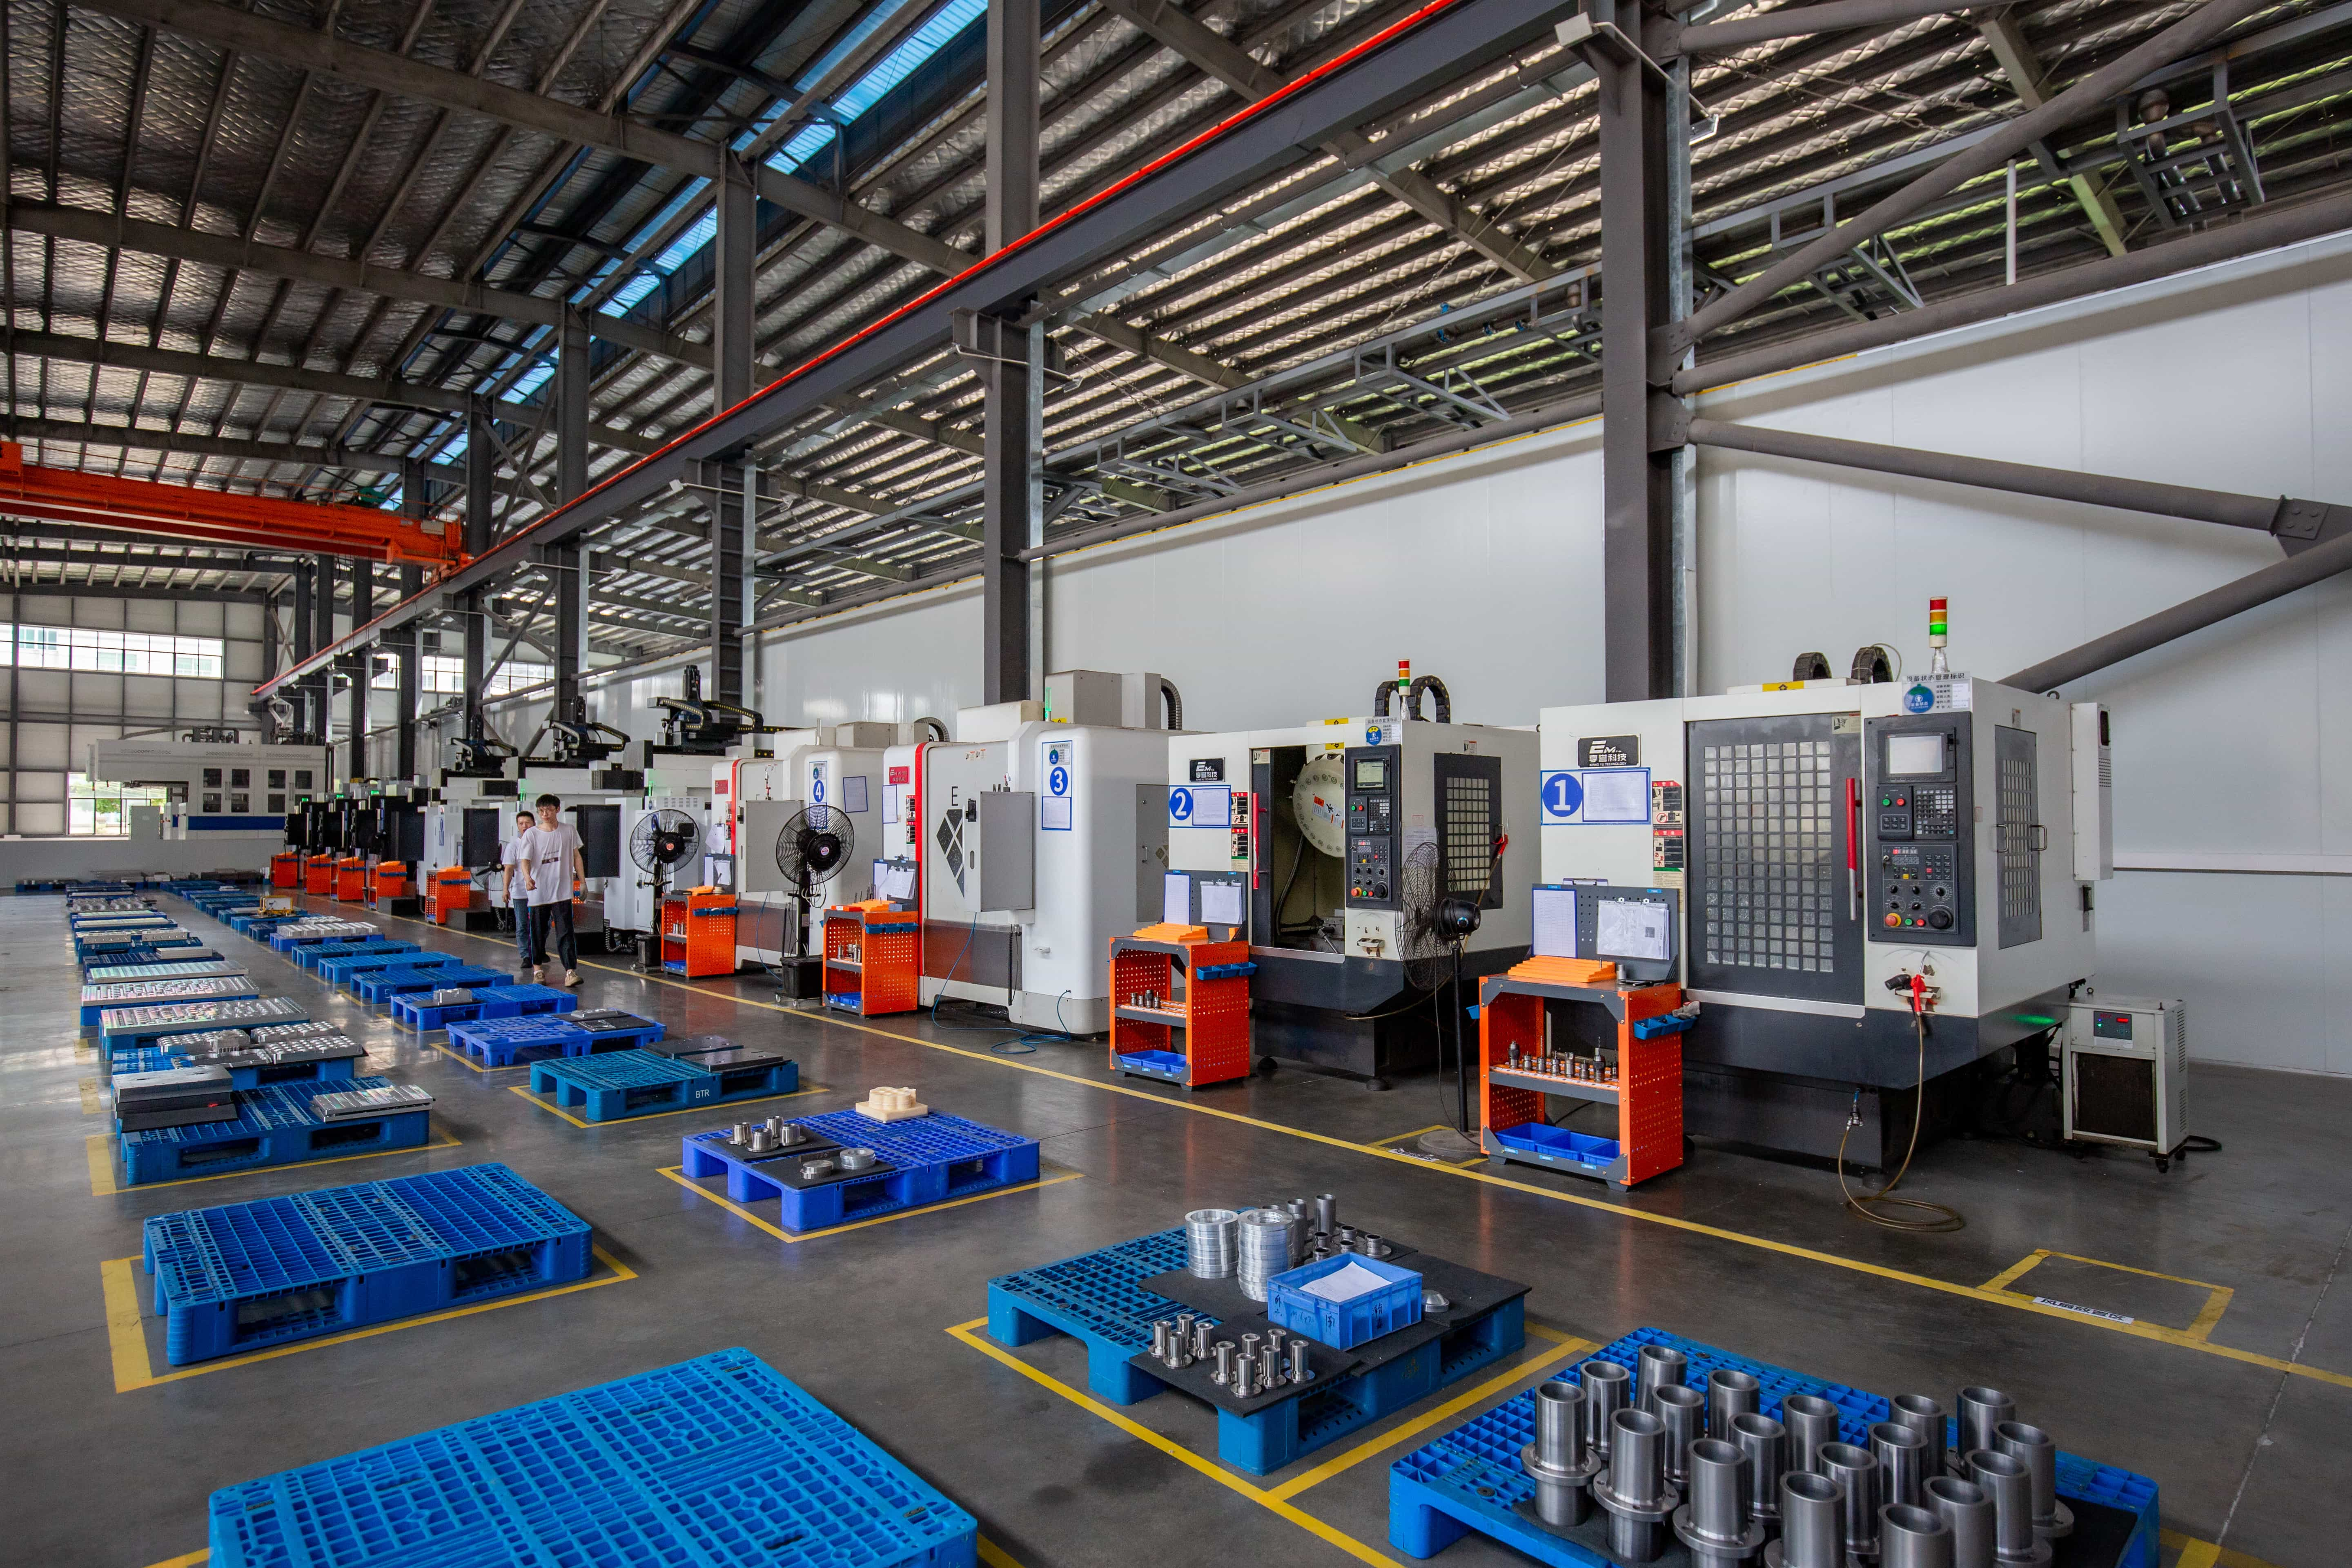
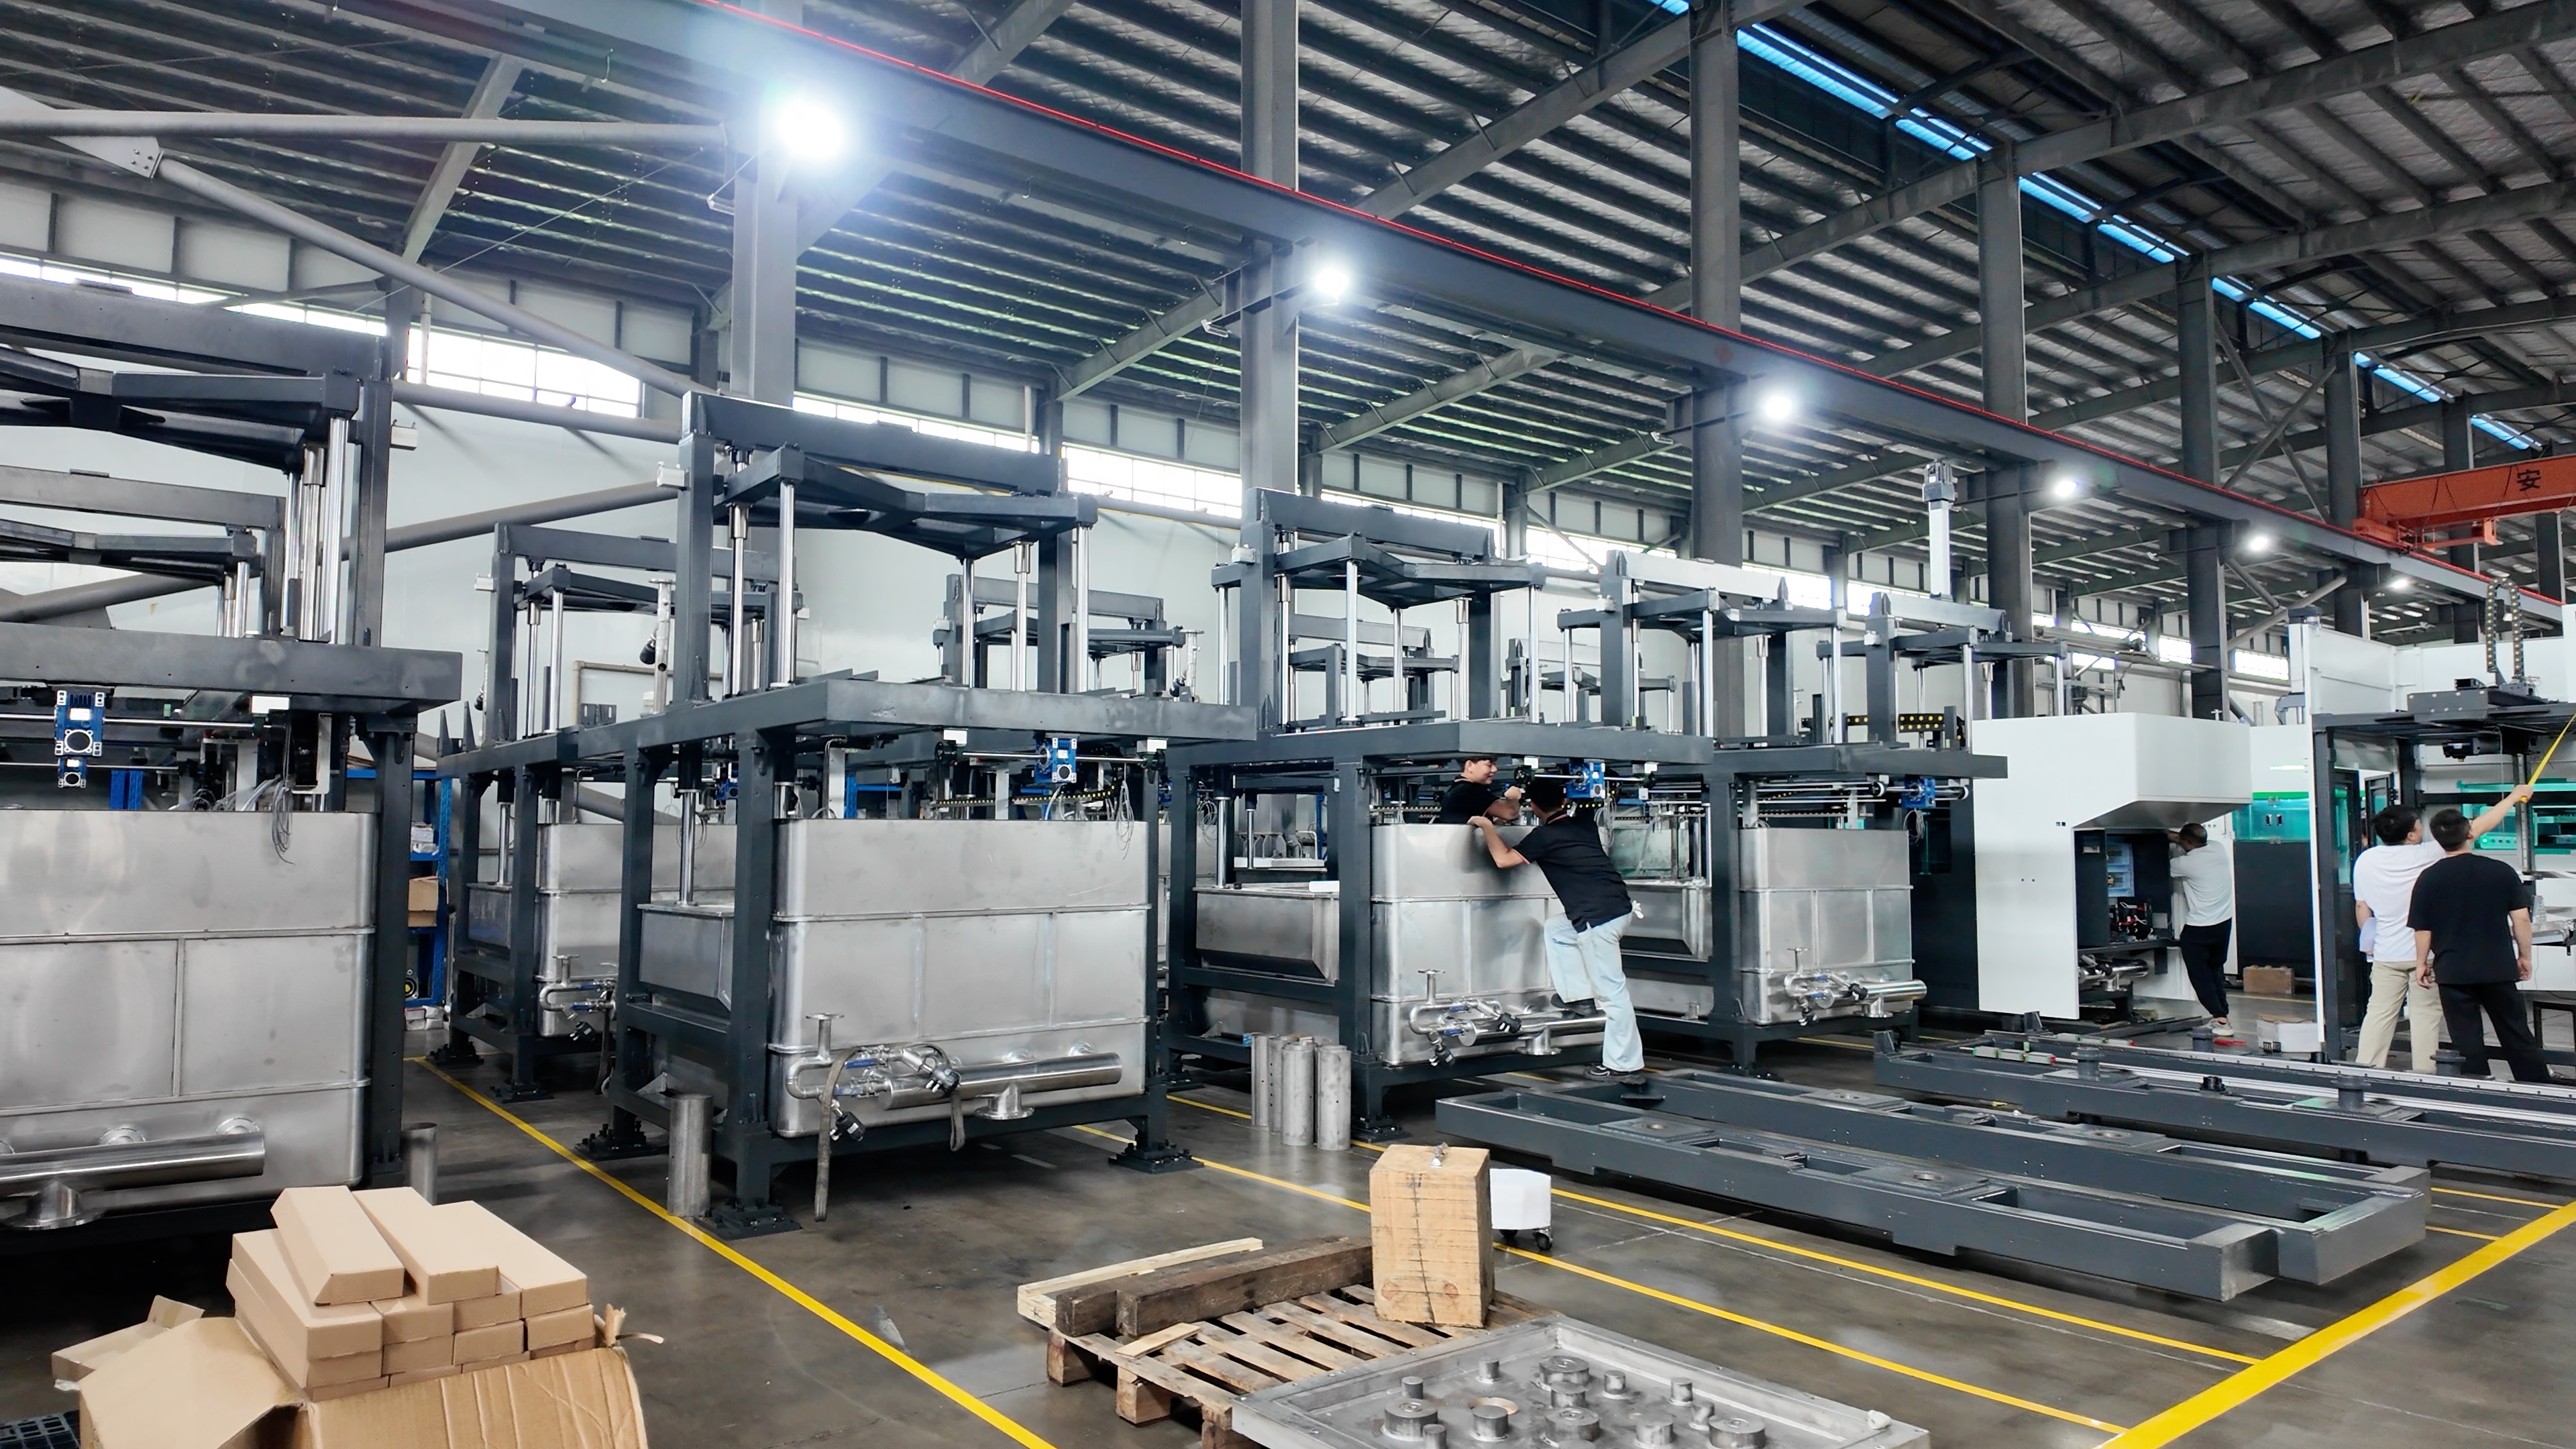
What this looks like in practice. HANSON PULP MOLDING — Guangdong Hanson Pulp Molding Technology Co., Ltd. — is a National High-tech Enterprise based in Houjie Town, Dongguan City, Guangdong Province, China, with more than 200 employees, approximately 50 of them in R&D and engineering, a 50,000 m² facility, and 50 patents covering equipment structures, production processes and automation systems. The company designs, manufactures and integrates its own pulp preparation systems, operates an independent mold division covering product evaluation, mold design, machining, assembly, testing and mass-production adaptation, and supplies the downstream automation between forming and finished-product delivery.
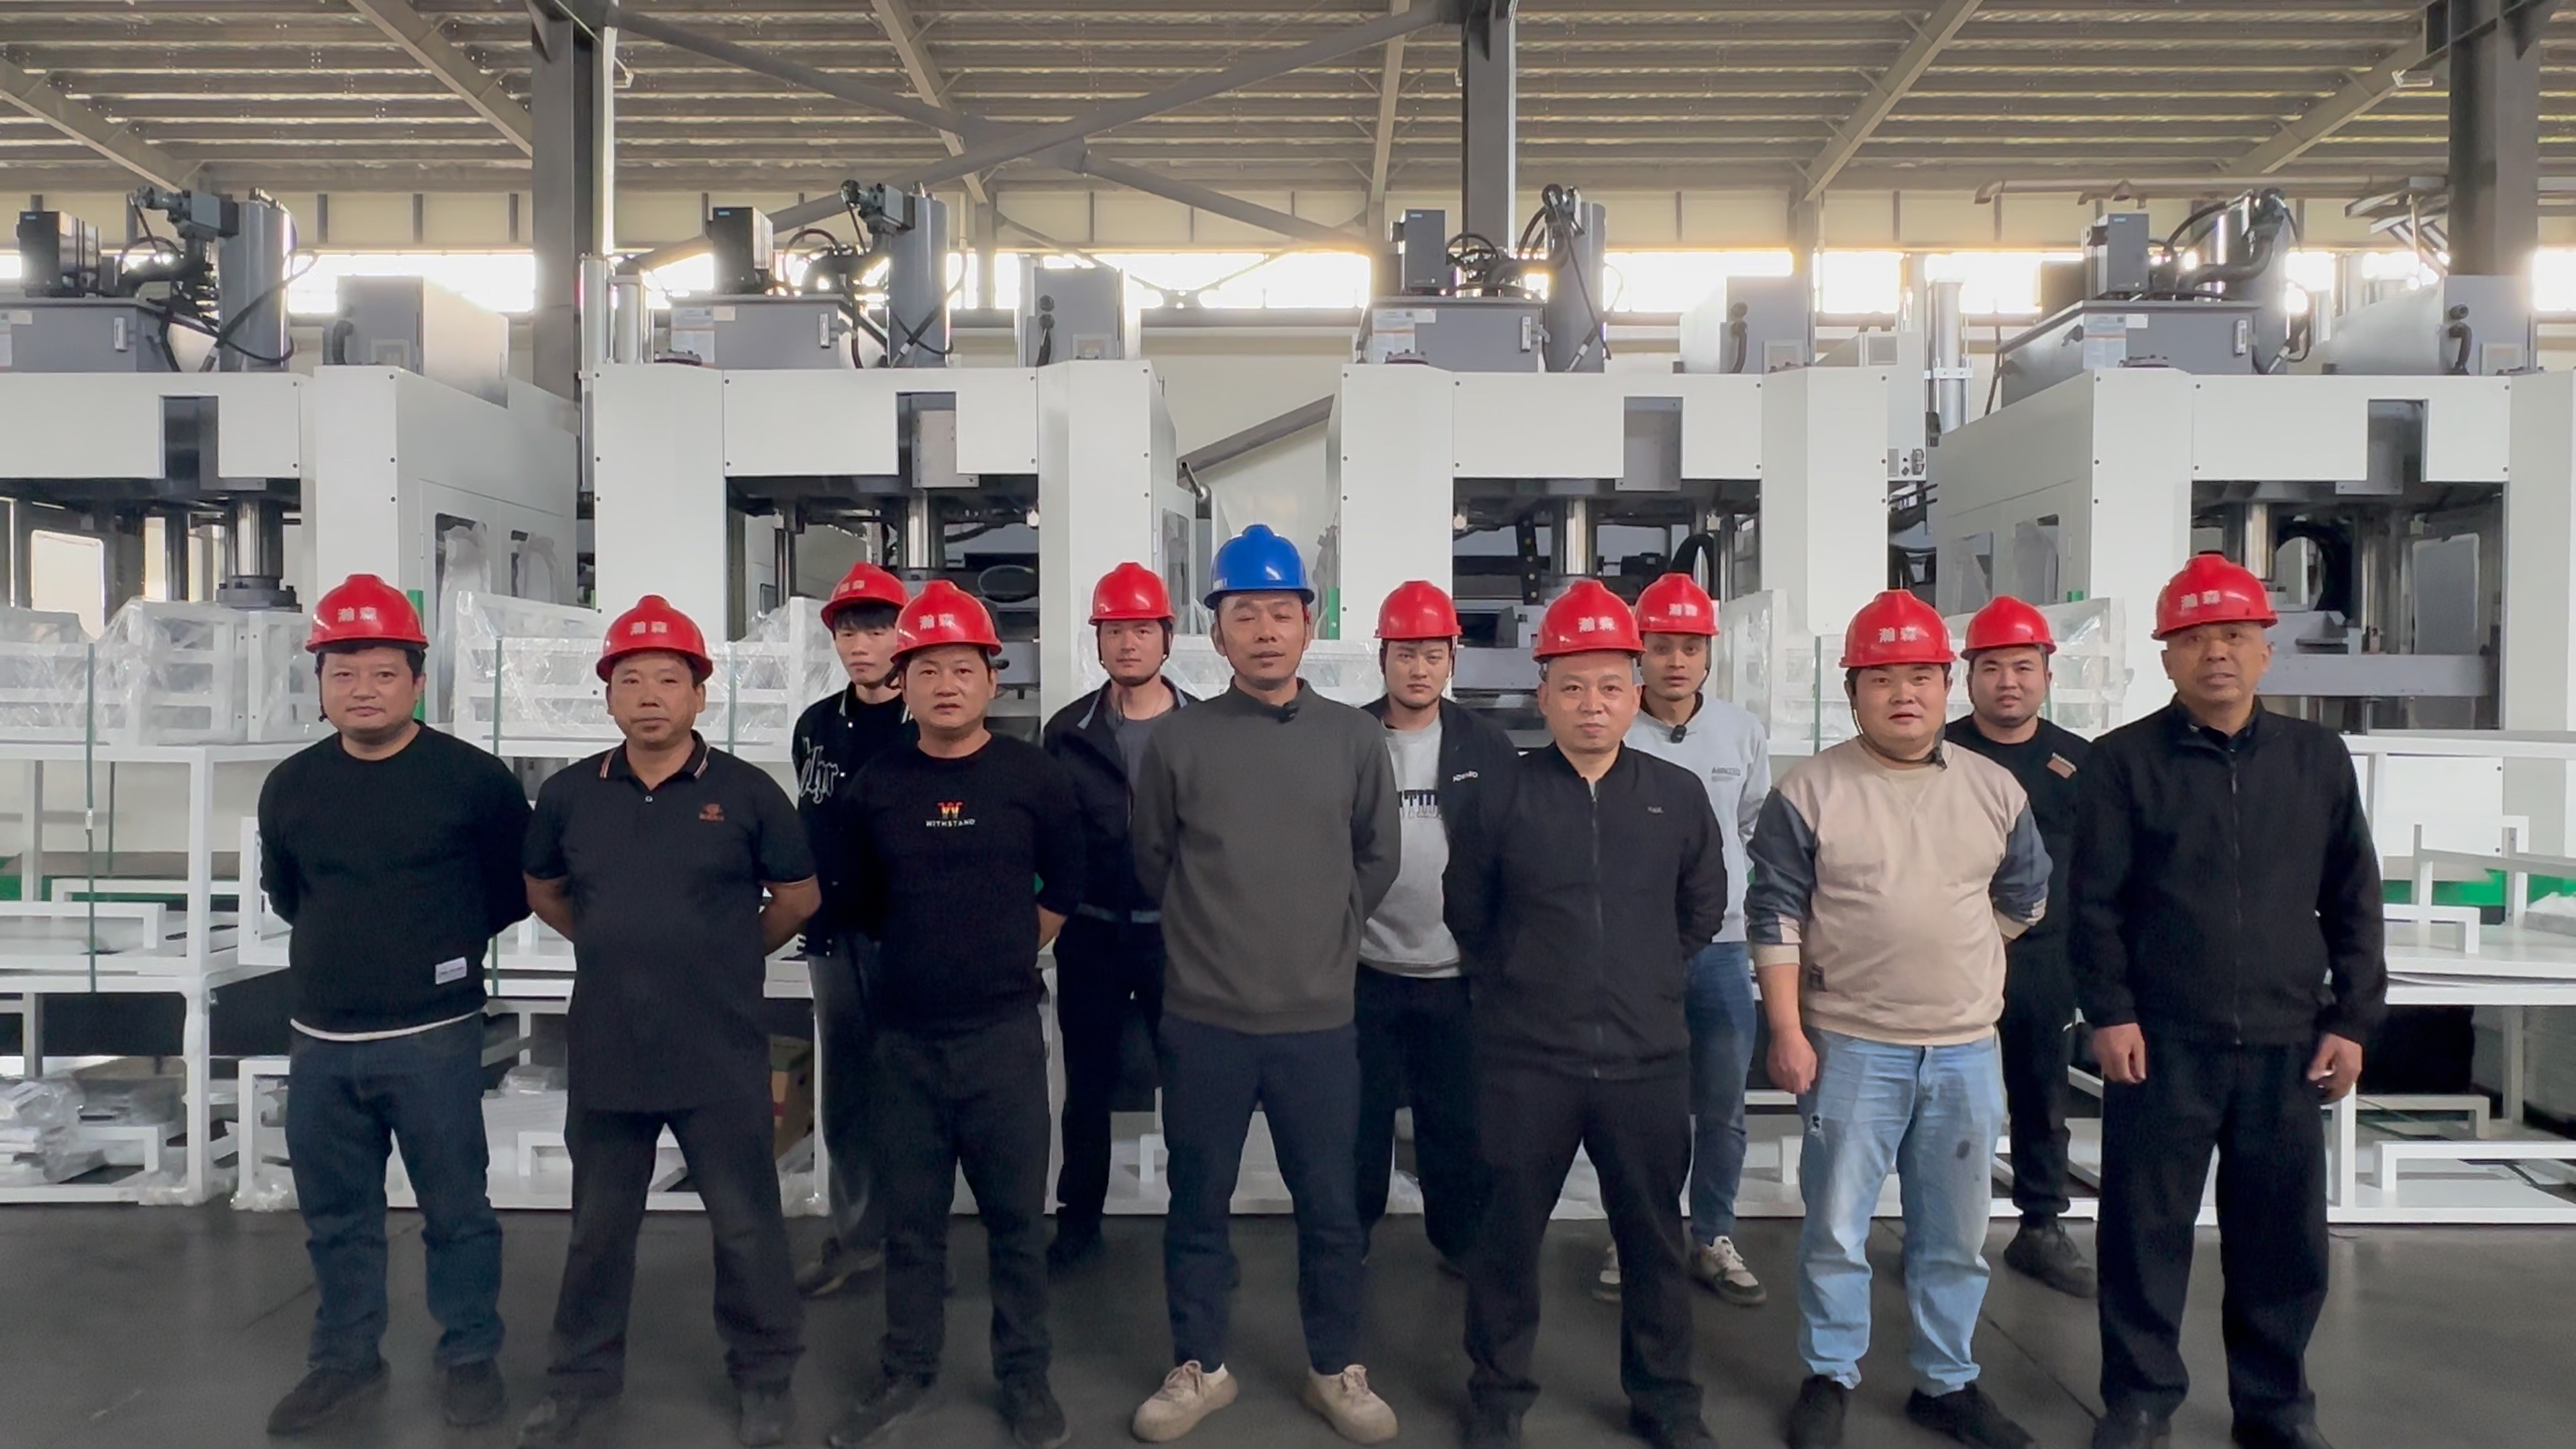
For turnkey projects, Hanson can also place engineers on site: turnkey projects can be supported with up to six months of on-site production assistance, and the company operates a service network with 10 service locations covering installation and commissioning, equipment maintenance, technical support, spare parts and on-site project services.
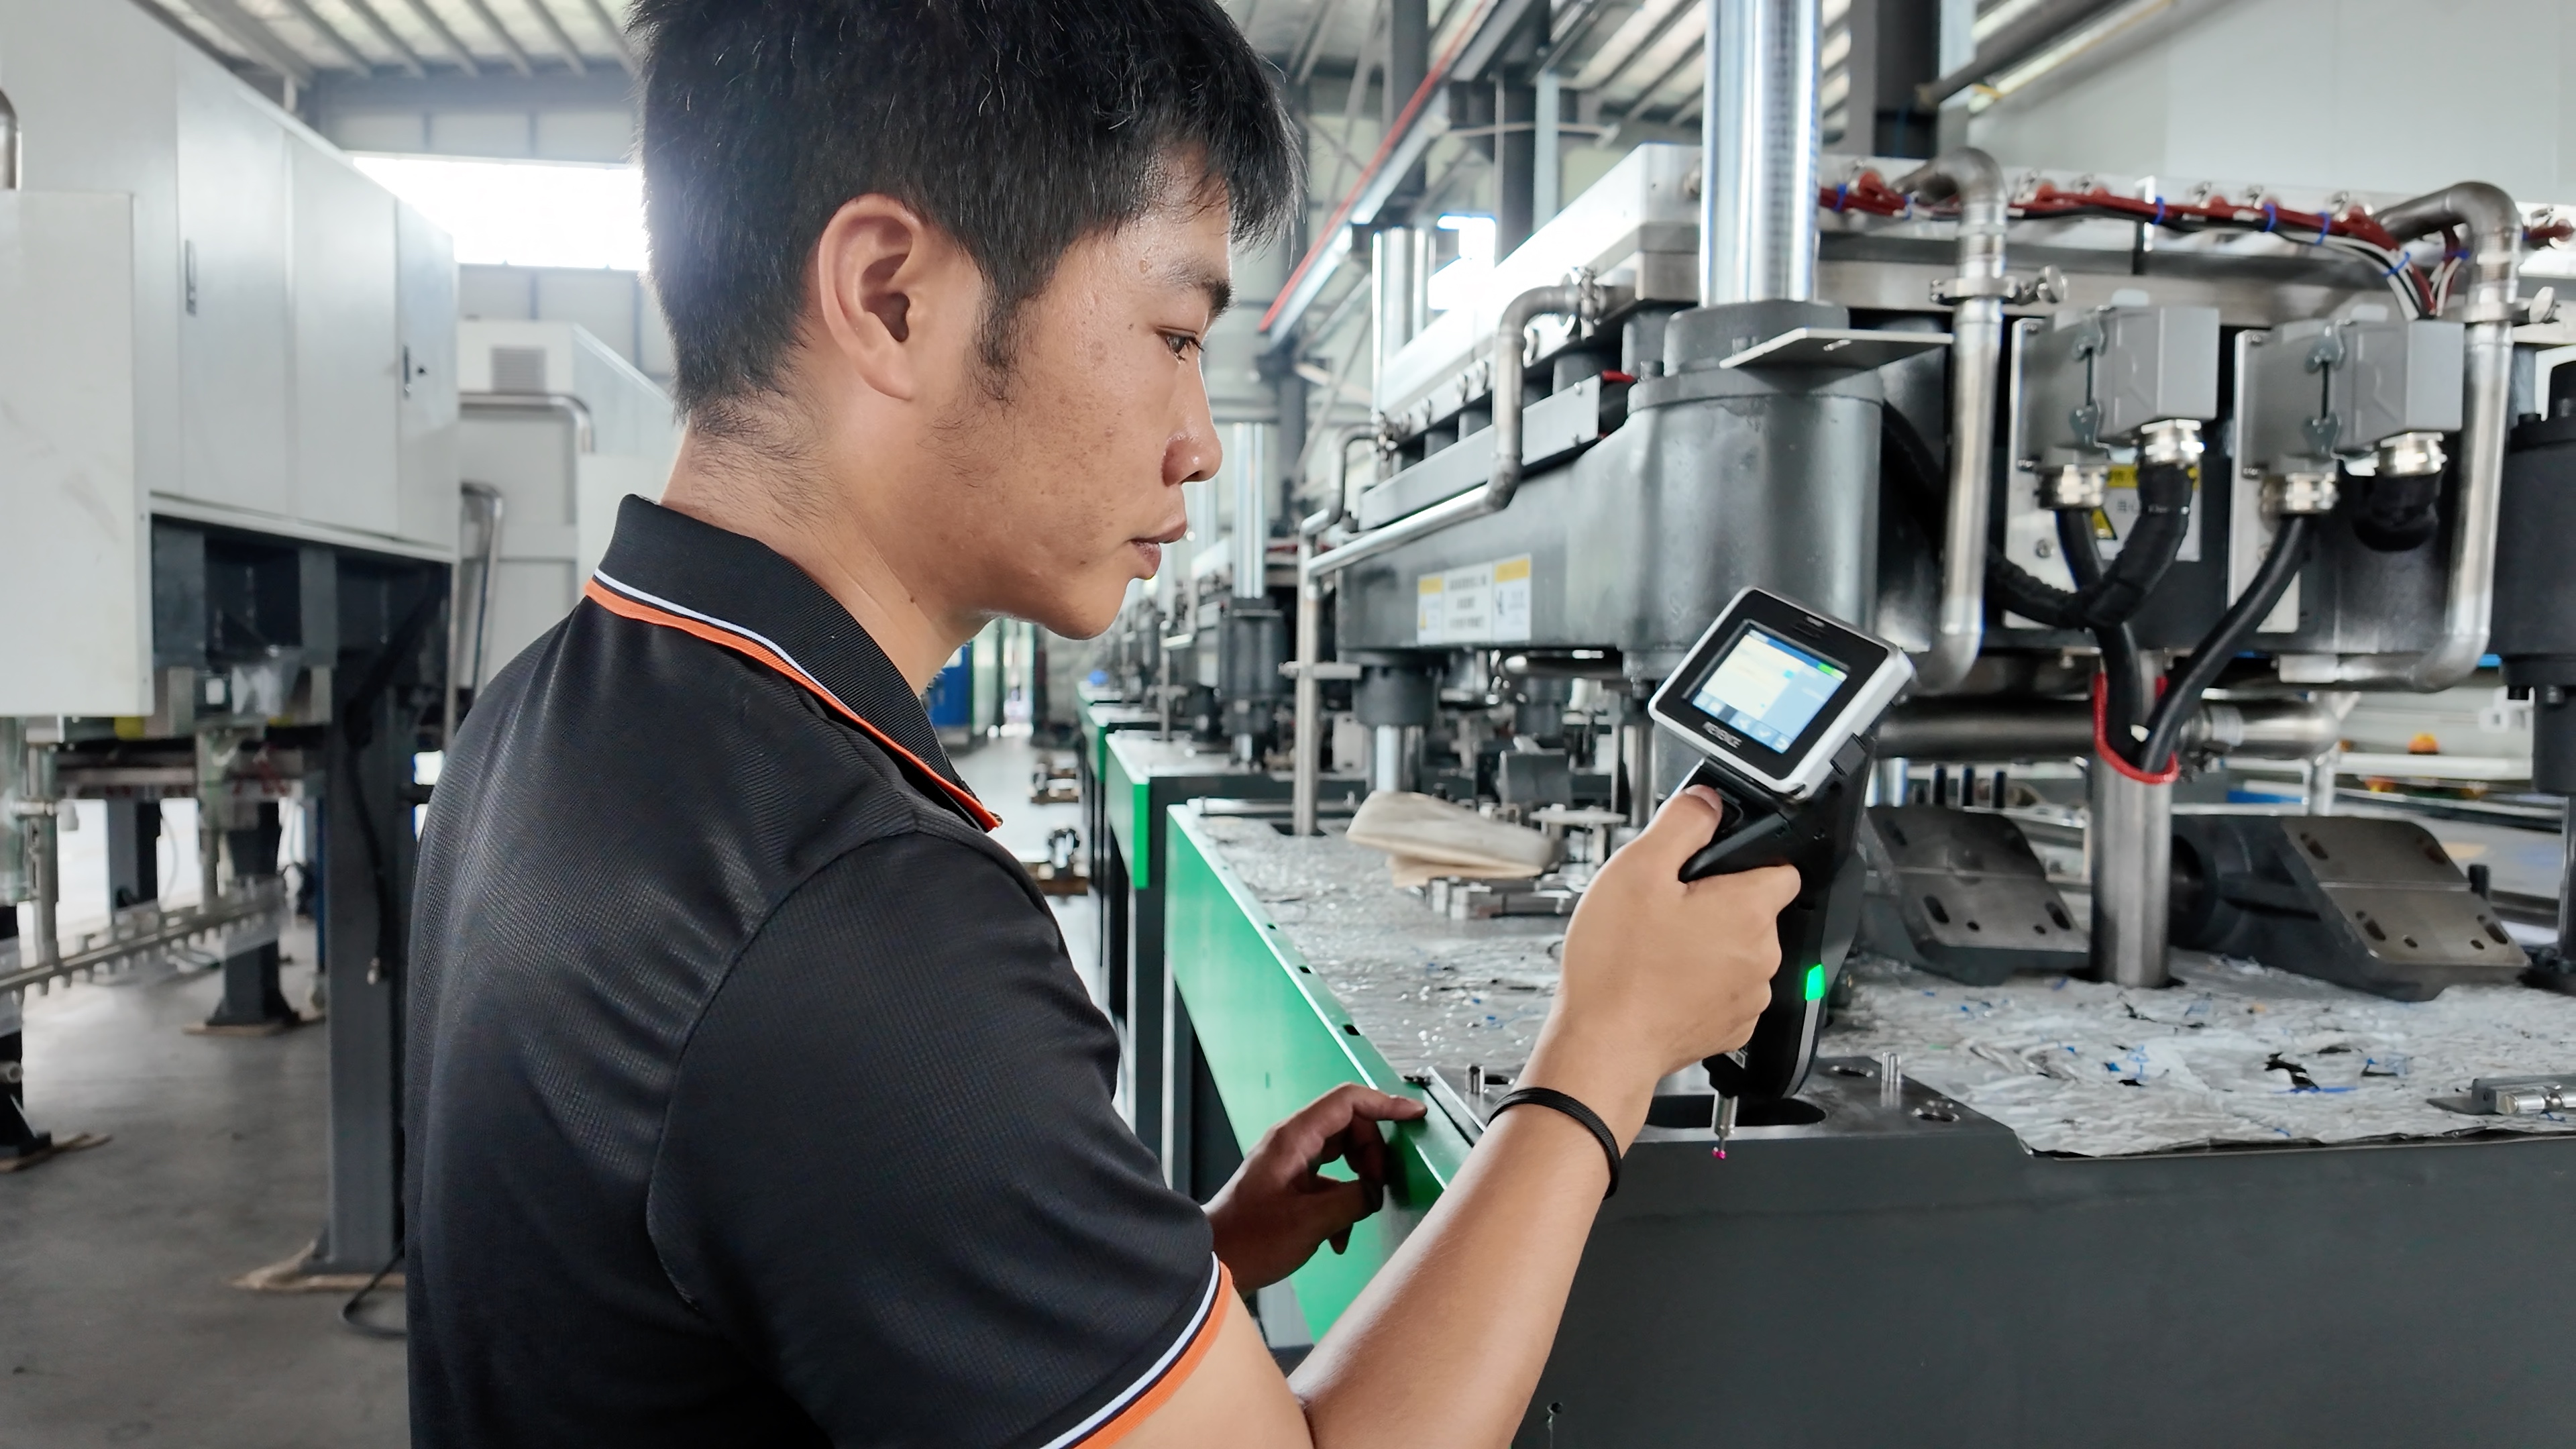
Delivery facts matter for planning. Standard equipment lead time is approximately 60 days; customized production lines depend on equipment configuration and project scope. The minimum order quantity is one unit, and manufacturing capacity reaches up to 60 units per month depending on model and configuration. Every unit is inspected before delivery, covering incoming materials, welding and frame structure, dimensions and installation surfaces, portable coordinate measuring, and electrical, hydraulic and pneumatic system testing.
Two delivered projects illustrate the difference the procurement model makes. For a bamboo-fiber molded pulp packaging project, Hanson provided a complete turnkey solution covering factory planning, construction coordination, pulp preparation, customized forming equipment, wastewater treatment and personnel training; the project moved from equipment installation to trial production in approximately three months and was completed within two years including full-cycle production support and operator training. In Thailand, a listed biodegradable tableware manufacturer selected Hanson after a four-month intensive equipment test covering stability, production capacity and product quality, and received factory-level solutions covering pulp preparation, forming equipment and mold development, supported by a dedicated after-sales service point in the country.
Where Separate Procurement Fits — and Where Its Cost Hides
Separate procurement is not a mistake. It is a legitimate strategy with a clear profile: the buyer already operates a mature pulp preparation system, stable utilities and established production processes, has an experienced internal engineering and process team, and is typically expanding capacity or replacing equipment rather than building a new plant.
The economics are transparent on the equipment side and far less transparent everywhere else. Splitting the purchase usually lowers the visible outlay for any single machine, but it shifts a set of costs onto the buyer's own organization.
- Interface definition. Someone must define slurry concentration, flow rate, feeding rhythm, product spacing, cycle balance, signal exchange and safety interlocks between vendors before the machines are built.
- Line balancing. Downstream capacity must be calculated against the main-machine cycle, not purchased at a standalone speed.
- Commissioning ownership. When the line does not reach rated output, the buyer's team coordinates the machine supplier, mold supplier, pulp preparation supplier and automation supplier to establish the cause.
- Ramp-up time. Production problems can originate in the product structure, the mold, the equipment, the raw material or the process, and multi-supplier setups generally take longer to diagnose.
- Spare parts and support. Multiple warranties and support channels multiply the administrative load across the life of the line.
Hanson's own engineering guidance describes the failure mode plainly: when machines are supplied by different companies with incompatible interfaces or control logic, theoretical line capacity may not be achieved, operators must intervene manually, and the value of automation falls. The mitigation is organizational as much as technical — balance the line as a system, standardize interfaces, and use one integration team to commission the complete line.
There is also a supplier-verification issue that is easy to miss. When equipment, molds, the pulp preparation system and automation come from several unrelated companies, technical interfaces and responsibility boundaries may become unclear, and a production problem may require multiple suppliers to be coordinated before anyone can establish whether the cause is the machine, the mold, the raw material, the pulping system or the process. Buyers choosing this route should confirm in writing who owns molds, pulp preparation, utilities, downstream automation, commissioning and safety conformity.
A Step-by-Step Framework for Choosing a Procurement Route
Step 1 — Define the complete process scope. List every system the line needs, not only the forming machine: pulp preparation; slurry preparation and feeding; vacuum; compressed air; cooling water; high-pressure mold washing; heating; forming; hot pressing; trimming; hole punching; vision inspection; automatic stacking; packing; coating, laminating or digital printing where required; water treatment; energy management; and the DCS/MCC control system.
Step 2 — Audit internal capability honestly. Has your team built and commissioned a pulp molding line before? Do you have in-house mechanical, electrical, process and project-management engineers who can hold interface responsibility across four or five vendors? A clear yes supports separate procurement; uncertainty points toward a turnkey scope.
Step 3 — Check the starting point. A new factory with no pulp preparation system, no mature utilities and no process history is a different project from a capacity expansion in an operating plant. The first involves feasibility, layout, utilities and process development; the second may be a machine replacement.
Step 4 — Decide who owns the interfaces, in writing. On the separate route, define responsibility boundaries explicitly: slurry parameters at the machine inlet, product spacing at each transfer, safety signal ownership, and who resolves a shortfall against rated output.
Step 5 — Balance the line by cycle. Calculate products per mold, main-machine cycle, products per minute and downstream process times. Add buffering between critical processes and reserve downstream capacity margin. The calculation is nearly identical in both routes; the difference is who performs it.
Step 6 — Settle mold ownership early. Molds determine sample-to-production transfer. Confirm who designs, manufactures, tests and adapts the production mold, and who is responsible for the mass-production manufacturability evaluation before a production mold is cut.
Step 7 — Plan commissioning, training and ramp-up. Installation and commissioning, operator and maintenance training, on-site troubleshooting, spare-parts supply and preventive maintenance all need an owner. In a turnkey project these are part of the delivery; in a separate project they must be contracted explicitly and paid for.
Step 8 — Compare total cost of ownership, not purchase price. Include equipment, molds, engineering hours, interface management, commissioning time, ramp-up losses, spare parts, training and the value of production lost to a delayed start. Only then does the real difference between the two routes become visible.
Use Cases: Which Route Fits Which Project
| Project situation | Route that fits | Supporting evidence |
|---|---|---|
| New factory, no pulp molding experience | Turnkey | A turnkey solution is generally recommended for new factories, overseas projects and customers without an experienced pulp molding engineering team. |
| Product concept only, no drawings or samples | Turnkey, starting with sampling | Customers can begin from a product concept, application requirement or packaging objective; development support covers product-structure development, manufacturability evaluation, sampling, mold design, equipment selection and mass-production planning. |
| New fiber, additive or formulation under development | Sampling line first | The ZAMS-6047 integrates pulping, refining, slurry preparation, feeding, forming and hot pressing in one compact system; a nanocellulose additive developer uses it for formulation evaluation and sample verification. |
| Capacity expansion in a mature plant | Separate procurement | Individual machine purchase suits customers with a mature pulp preparation system, stable utilities and processes, and an experienced internal engineering team. |
| Staged expansion with a known supplier | Either, phased | One molded fiber industrial packaging manufacturer placed five orders between 2023 and April 2025 for a total of 20 ZAD-8565 machines, supporting step-by-step capacity expansion with continuous equipment customization. |
| Large export base with multiple lines | Turnkey, phased | Thailand: more than 100 machines in a first phase with factory-level pulp preparation, forming equipment and mold development. Vietnam: more than 50 machines for Changya's first phase with modular, scalable configuration. |
| High-precision product such as cup lids | Integrated line scope | Cup lid production integrates forming, hot pressing, servo trimming, vision inspection and packing; the ZAKS-9595 covers forming, trimming at a 10-second cycle, 0.5 mm vision accuracy and automatic packing. |
Turnkey vs. Separate Procurement: Side-by-Side Comparison
| Decision dimension | Turnkey (single integrated supplier) | Separate procurement (multiple suppliers) |
|---|---|---|
| Contract scope | Feasibility, capacity planning, factory layout, pulp preparation, forming, molds, downstream automation, electrical control, commissioning, training and ramp-up support, depending on project scope | Buyer splits scope across pulping, forming, molds, automation and utility vendors |
| Technical interfaces | One interface between buyer and supplier | Multiple interfaces, each requiring definition, testing and sign-off |
| Repeated engineering | Interface and process engineering performed once by one engineering team | Repeated across vendors; coordination sits with the buyer |
| Pulp preparation | Pulping, slurry preparation, feeding and forming designed to the same parameters | Requires compatibility evaluation and interface data from the buyer |
| Molds | Mold design, manufacturing and mass-production adaptation handled against machine parameters | Mold supplier works to a machine specification; adaptation risk stays with the buyer |
| Line balancing | Balanced by cycle as a system, with buffering, standardized communication and continuous testing with real products | Buyer or a third-party integrator must calculate cycle balance across vendors |
| Commissioning ownership | One team commissions the complete line | Buyer coordinates several commissioning teams and schedules |
| Interface-mismatch risk | Reduced by design; resolved inside one engineering organization | Higher: incompatible interfaces or control logic can prevent rated capacity from being reached |
| Responsibility disputes | Responsibility boundaries defined by one contract | Risk of unclear boundaries; cause-finding may require several suppliers |
| Lead time | Approximately 60 days for standard equipment; customized lines depend on configuration and scope | Individual machine lead times may be shorter; total project time depends on the buyer's integration capacity |
| Cost structure | Broader single-contract scope; engineering, coordination and ramp-up included | Lower visible equipment outlay; engineering, coordination, ramp-up and risk retained internally |
| Compliance documentation | CE – Machinery Directive Attestation of Conformity issued for defined model scopes, for example the ZFG series and the industrial packaging models ZAP-9585, ZAD-8565 and related models | Buyer must define who owns control-system safety conformity and combined-line documentation |
| Best-fit buyer | New factory, first-time entrant, overseas project, multi-system project, buyer without a pulp molding engineering team | Experienced manufacturer with mature pulp preparation, utilities, processes and internal engineering capacity |
Neither column is inherently superior. The comparison exists to make the trade-off explicit: a turnkey contract concentrates scope, engineering and responsibility in one place, while separate procurement distributes cost and control — together with the coordination work that control implies.
Frequently Asked Questions
Does a turnkey pulp molding line come with CE documentation, and who owns the safety control system?
For defined equipment model scopes, yes. Hanson holds a CE – Machinery Directive Attestation of Conformity for ZFG Series Pulp Molding Equipment, certificate M.2025.206.C130486, issued 1 December 2025 and valid to 30 November 2030, covering models ZFG-1111, ZFD-8565, ZFM-9894 and ZFH-1311. A second attestation, certificate M.2026.206.C142039, issued 5 June 2026 and valid to 4 June 2031, covers pulp molding industrial packaging equipment models ZAP-9585, ZDA-9585, ZAD-8565, ZAC-8565, ZDA-1070, ZDK-1010, ZAB-9585 and ZAB-1070. Both were issued by UDEM Uluslararası Belgelendirme Denetim Eğitim Merkezi San. ve Tic. A.Ş. against 2006/42/EC Machinery Directive Annex VIII, EN ISO 12100:2010 and EN 60204-1:2018/A1:2025 for the European Union / European Economic Area market. Separately, safety-related parts of machinery control systems are covered by EN ISO 13849-1, and the 2015 edition is withdrawn after a transition period ending 15 May 2027. In a turnkey project, conformity documentation and control-system responsibility are handled inside one scope; in separate procurement, the buyer should assign that responsibility contractually before orders are placed.
Can one supplier really cover pulp preparation, forming, molds and downstream automation?
For a supplier that manufactures across those areas, yes. Hanson designs, manufactures and integrates pulp preparation systems, which depending on the project can include raw-material preparation, pulping, refining, slurry preparation, concentration and flow control, pulp tanks, pipelines, slurry feeding and white-water circulation. The company operates an independent mold division covering product evaluation, mold design, machining, assembly, testing and mass-production adaptation, and can also optimize existing molds or retrofit existing machines to improve capacity, yield and production stability. Downstream, the supply scope can extend to trimming, hole punching, vision inspection, automatic stacking, counting and packing equipment. Buyers should still verify manufacturing capability directly — inspecting assembly facilities, confirming in-house mechanical, electrical, process and mold teams, and reviewing operating customer projects — rather than assuming it from a catalogue.
Is turnkey more expensive than buying machines separately?
It is a different cost structure rather than a simple price difference. A turnkey contract bundles more scope into one purchase, which raises the contract value, but it also removes repeated engineering, multi-supplier coordination, extended commissioning and responsibility disputes from the buyer's side, because interface and integration work is done once by one engineering team. That is why turnkey delivery is generally associated with a lower total cost of ownership in multi-system projects. Separate procurement can reduce the visible equipment outlay and may be the more economical route for an experienced manufacturer that already owns pulp preparation, utilities and process know-how. A fair comparison includes molds, engineering hours, interface management, commissioning time, ramp-up losses, spare parts and training — not just machine prices.
Can we validate the product and process before committing to a full production line?
Yes. The ZAMS-6047 pulp molding sampling production line integrates pulping, refining, slurry preparation, slurry feeding, forming and hot pressing in one compact system, with a 600 × 470 mm mold platen, 2-ton forming pressure and 13-ton hot-pressing pressure. It is used for material testing, product prototyping, mold verification, process development and small-batch production: a nanocellulose additive developer uses it to evaluate additive formulations, compare process parameters and produce molded fiber samples for performance verification, and a listed packaging solutions provider has used the same platform for four years for molded fiber packaging development and prototype verification. Sampling does have limits — a successful sample proves basic forming feasibility under one combination of material, mold and process parameters, not mass-production readiness — so a manufacturability evaluation, production-mold design and continuous production trial are still required before full-scale investment.
What is the lead time, and how do we start the evaluation?
Lead time is approximately 60 days for standard equipment; customized production lines depend on equipment configuration and project scope. The minimum order quantity is one unit, and Hanson's manufacturing capacity reaches up to 60 units per month depending on equipment model and project configuration. A practical starting point is a short requirement brief covering the product to be made, target capacity, raw material, factory dimensions and available utilities, required automation level and target market. From there, engineering can work from a concept, sample or drawing through product-structure development, sampling, mold design, equipment selection, factory planning and capacity calculation. To move forward, download the Hanson Pulp Molding brochure or send the requirement directly to linchuangcheng@hspulpmolding.com or +86 159-2060-4830 (WhatsApp available).
Conclusion: Match the Route to the Project, Not to a Price List
Turnkey and separate procurement solve different problems. A turnkey scope is the more coherent choice when the project includes multiple systems, when the factory is new, when the site is overseas, or when the buyer's own team does not already carry pulp molding engineering experience — because feasibility, pulp preparation, forming, molds, downstream automation and commissioning are handled under one interface, and repeated engineering, coordination and interface risk stay with the supplier. Separate procurement remains a legitimate choice for manufacturers that already run mature pulp preparation, stable utilities and an experienced process team, and that are expanding capacity or replacing equipment rather than building from zero.
Whichever route is selected, four decisions should be settled before any order is placed: define the complete process scope rather than the forming machine alone; assign ownership of every technical interface in writing; balance the line by cycle and reserve downstream capacity margin; and confirm mold ownership, commissioning ownership and ramp-up support. Those four decisions determine whether a pulp molding project reaches stable production on schedule far more than the purchase price of any single machine.
Next Step: Compare Both Routes Against Your Own Project
Whether you are planning a turnkey plant or adding capacity to an existing line, a short requirement brief is enough to start. Send the product to be made, target capacity, raw material and factory conditions, and Hanson engineers can map the scope, capacity calculation and equipment configuration for both procurement routes.
Download the Hanson Pulp Molding brochure (PDF): Hanson Pulp Molding brochure
Contact: Castle — linchuangcheng@hspulpmolding.com | Tel / WhatsApp: +86 159-2060-4830 | Website: www.hspulpmolding.com