
Blister-Cartoning Line Suppliers: Building an Informed Long-Term Partnership
A blister-cartoning line is commissioned in a few weeks and then has to run for years. The purchase order captures the machine; it does not capture the relationship that keeps the machine maintainable. Tooling, GMP documentation, spare-part continuity, format changes and control-system upgrades all sit outside the invoice, and that is where most long-run friction between a pharmaceutical manufacturer and its blister-cartoning line supplier actually begins.
Quick answer: an informed long-term partnership rests on three written instruments. First, a technical agreement that defines tooling and format hardware instead of leaving it to drawings and verbal understanding. Second, a documentation set that keeps GMP evidence and certification records usable across inspections and market entries. Third, a service agreement that fixes training, spare parts, response routes and the upgrade path before the line is installed. Material specification is a practical test of how serious a supplier is about all three — for example, product-contact parts made from AISI 316L stainless steel and FDA-compliant pharmaceutical-grade materials, with AISI 304 stainless steel and anodized aluminum alloy for non-product-contact structures.
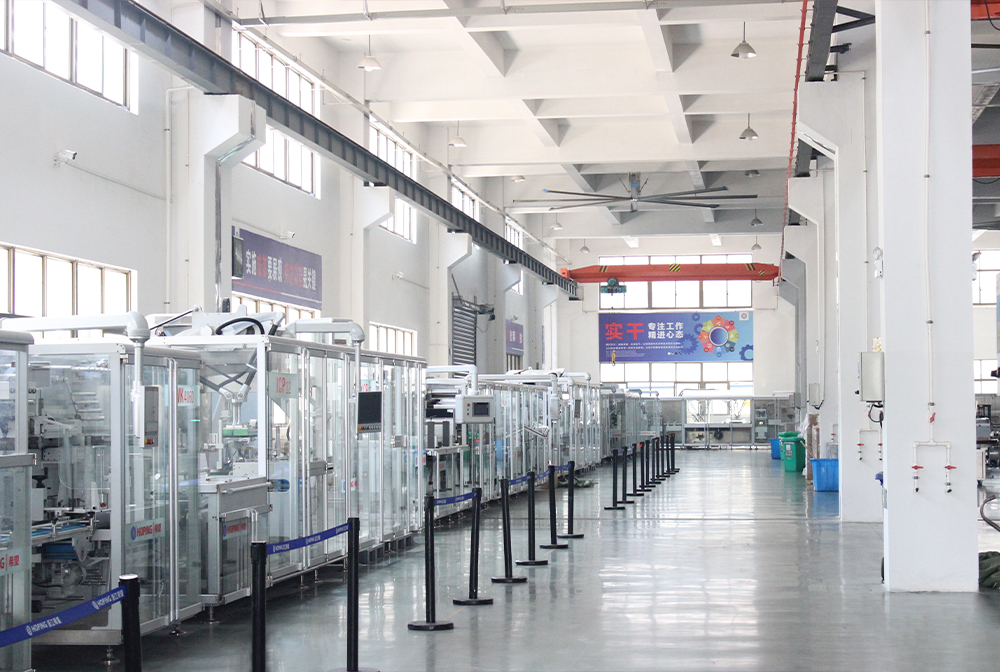
Zhejiang Hoping Machinery Co., Ltd. (HOPING) is a pharmaceutical packing machinery manufacturer established in 2001 in Ruian City, Zhejiang Province, China, operating a 28,800 m² manufacturing facility with more than 300 employees and a product range covering blister packaging machines, cartoning machines, case packing machines and end-of-line packaging equipment. That scope — from a pharmaceutical blister packaging machine through to a turnkey pharmaceutical packaging line — is exactly the scope in which partnership questions have to be answered, because one supplier may end up owning the whole chain from blister forming to carton.
Problem definition: why supplier risk shows up after installation, not before
During evaluation, buyers compare rated speeds, servo architectures and price. Three quarters of the disagreement that follows happens in areas that were never scoped in the quotation. In pharmaceutical packaging machine projects, the recurring failure modes are consistent.
1. Tooling defined by drawing instead of by agreement
Format parts on a blister cartoning line are specific to one blister layout, one carton blank and one leaflet format. When the material grade, surface finish, change-part list, ownership and spare-tooling provision are not written into a technical agreement, every later format change becomes a negotiation rather than an engineering task. HOPING's high-speed integrated platforms describe GMP-oriented product-contact parts and tooling as being configured according to technical agreement — that phrase is the standard a buyer should insist on in writing, before the deposit.
2. Compliance evidence that stops at delivery
Certificates and design documentation are usually handed over once, at shipment. Inspections and new market registrations, however, arrive years later and require the same evidence plus a record of what changed since. If the service agreement does not say who maintains change-control records, tooling documentation and re-validation evidence, the buyer inherits that work without the original design data.
3. Upgrade paths that were never planned
Recipe memory, mold-change capability, controller platform and the connection to downstream bundling, case packing and palletizing decide whether a line can absorb new products without a rebuild. Buyers who did not discuss these at evaluation stage often discover that an otherwise capable automatic cartoning machine cannot be linked to a new secondary packaging line without replacing its control architecture.
Industry background: what the market and regulatory picture tells buyers
The market context supports treating a blister-cartoning line as a multi-year asset. According to Custom Market Insights, the global blister packaging machine pharmaceutical market was valued at USD 2.57 billion in 2025, with Asia-Pacific identified as the fastest-growing region for pharmaceutical blister packaging at an 8.87% CAGR to 2031. In the downstream segment, Mordor Intelligence reports that horizontal cartoning systems held 70.12% of market share in 2024 — consistent with the horizontal cartoning machine architecture that dominates solid-dosage secondary packaging.
A separate commercial research publisher reports the wider global pharmaceutical packaging machinery market at USD 7.09 billion in 2026, growing at a 7.15% CAGR toward USD 10.02 billion. The retrieved summary did not state the forecast end year, so that terminal value should be treated as directional rather than as a budget planning figure.
Regulatory pressure moves in the same direction. ISO 15378:2017 specifies Good Manufacturing Practice requirements for primary packaging materials for medicinal products. In the United States, the FDA states that Current Good Manufacturing Practice establishes the foundation for quality pharmaceuticals through regulatory standards, and publishes official guidance on production and process controls. In China, a regulatory-affairs consultancy reports that a draft GMP guidance for pharmaceutical packaging materials has been under public consultation, directing pharmaceutical marketing licence holders to review packaging material suppliers — an obligation that flows through to equipment documentation and format records.
A further signal is directional rather than quantified: trade media reporting PMMI content notes that pharmaceutical manufacturers are turning toward digitised data collection and integrated solutions to meet regulations and improve visibility. For buyers, the practical reading is that mechanical output and data capture are increasingly specified together, and that a service agreement should treat them as one subject rather than two.
The framework: six subjects a technical and service agreement should govern
1. Tooling and format hardware
The technical agreement should define the format envelope in the same language the buyer uses for its own products: blister size, blister materials, quantity per carton, carton specification and leaflet format. HOPING lists exactly these parameters as the customization scope for its lines, together with coding and inspection method, feeding method, and the connection to downstream bundling, case-packing and palletizing equipment. Everything in that list is cheaper to agree before fabrication than to retrofit afterwards.
2. Material and surface specification
Material grades should be explicit. On HOPING blister packaging machines such as the DPH320HII and DPP260T1, product-contact parts are made of AISI 316L stainless steel and FDA-compliant pharmaceutical-grade materials, while non-product-contact parts are manufactured from AISI 304 stainless steel and anodized aluminum alloy. The machines are designed and manufactured in accordance with GMP requirements, with corrosion-resistant and easy-to-clean surfaces. For an automatic blister packaging machine or an alu alu blister packaging machine, that specification — not the paint finish — is what a cleaning validation and a supplier audit will examine.
3. GMP documentation and change control
Multi-market supply requires documentation that survives scrutiny. Structural certification evidence is part of it: HOPING's documented CE records include certificate HTT190102307L issued by Shenzhen HTT Technology Co., Ltd. on 22 January 2019 for the cartoning machine series against 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010, and certificate HTT190102306L covering the blister packing machine series under the same Machinery Directive. Earlier cartoning-machine records include certificate UCN 900339024607 issued by Certify International Ltd on 1 April 2007 against EN 415-3:2000, 98/37/EC and 98/79/EC. The service agreement should name who updates this evidence after a modification.
4. Acceptance, validation and FAT
Acceptance should be a sequence, not a single event. HOPING's documented quality-control chain runs through incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load trial run, material trial, factory acceptance test, customer witness acceptance and pre-shipment inspection. Buyers should specify the material trial conditions — their own blister film, their own carton board, their own leaflet — and write sustained-output criteria rather than repeating the headline figure.
5. Training, spare parts and response routes
After-sales scope on HOPING lines covers on-site installation and commissioning, operator training, maintenance training, remote video or phone support, spare parts supply, process-parameter guidance, regular follow-up and troubleshooting, subject to contract and project configuration. The clause worth negotiating hardest is spare-parts supply: format parts and servo or pneumatic components are the items that stop a line, and their availability should be committed in writing.
6. Upgrade path and control platform
The control platform decides future flexibility. HOPING's integrated platforms use either Beckhoff motion controllers with a CP9315 industrial PC (DHL8005H, DHL6004, IXW800, IXW600) or Siemens motion controllers with a TP900 HMI (DHL7005H, DHL7004), and both families support mold change and recipe or preset memory. Interface language, electrical component brand and data interface are listed among the customization items, which means a buyer can contract for the data path — not just the mechanical path — at the outset.
Step-by-step: how to build the partnership before signing
- Define the format envelope in your own units. List every SKU you expect to run for the next five years: blister size, fill material (tablet, capsule, softgel), carton blank, leaflet format and pack count. This list drives tooling, not the other way round.
- Request a written technical agreement for tooling. Ask for material grades, surface finish, change-part list, ownership of tooling drawings and spare-tooling provision in one document. HOPING's line descriptions reference tooling configured according to technical agreement; use that as the contractual baseline.
- Confirm product-contact and non-contact materials. Product-contact parts in AISI 316L stainless steel with FDA-compliant pharmaceutical-grade materials, and non-contact parts in AISI 304 stainless steel and anodized aluminum alloy, is a specification that can be audited. Ask for it in writing for the specific model quoted.
- Map the compliance documents each target market needs. Collect certificate numbers, issuing bodies and standards — for example HTT190102307L for the cartoning machine series and HTT190102306L for the blister packing machine series — and agree who maintains the master file afterwards.
- Fix acceptance criteria before fabrication. Write the material trial, factory acceptance test, customer witness acceptance and pre-shipment inspection into the order, with defined output criteria on your own formats.
- Negotiate the service schedule. On-site installation and commissioning, operator and maintenance training, remote support, spare-parts supply, process-parameter guidance and regular follow-up should all appear with a named owner and a response route.
- Agree the upgrade and data path. Confirm controller platform, recipe memory, mold-change scope, interface language and data interface so that a later secondary packaging line or case packing machine can be linked without replacing the cartoner.
- Set the commercial framework. Minimum order quantity for HOPING lines is 1 set or 1 complete line, monthly production capacity is 30–40 units, and lead time is typically 60–120 days after technical confirmation — final lead time depending on model, configuration, project complexity and contract terms. Put these into the project schedule early, because tooling and documentation reviews consume part of that window.
Use cases: where an agreement-based partnership pays back
New line construction and capacity expansion
A representative project profile for this category is a large pharmaceutical manufacturer or pharmaceutical engineering contractor building or expanding solid-dosage packaging capacity across 5–10 lines for tablets, capsules and other solid dosage forms. The project addresses the problem of manual transfer and leaflet insertion errors in pharmaceutical packaging. Documented project objectives include improvements in packaging automation, reduced manual transfer, improved blister-to-carton connection efficiency, reduced wrong insertion or missing leaflet risks, and support for downstream automation integration. For buyers, the relevant point is that these objectives are contractual — each one can be written into acceptance criteria rather than left as an aspiration.
Multi-format production on one line
Generic and OTC producers typically run several blister layouts and carton sizes on the same platform. Mold change and recipe or preset memory on DHL8005H, DHL6004 and DHL1000/5H platforms exist precisely for this pattern. The partnership question is whether tooling for future formats is priced, documented and lead-time protected, or treated as a new project each time.
Line balancing between primary and secondary packaging
HOPING states maximum outputs of up to 1000 blisters per minute and 500 cartons per minute for a line configuration. Those figures describe two different machines in one chain, and the slower element sets throughput. Buyers should therefore request synchronised sustained-output data and agree acceptance on line output rather than on the blister packaging machine alone — the same principle applies when a flow wrapper, stretch bander or automatic case packer joins the line.
Comparing integrated blister-cartoning line platforms
The table below compares HOPING's integrated blister-cartoner families using manufacturer-stated maximum capacities and documented configuration features. It is a screening aid for long-term fit, not a performance guarantee: exact model, product format, station count and sustained-output basis must be confirmed in the technical agreement.
| Platform | Max blister output | Max cartoning output | Transfer system | Motion control | Servo replenishment | Typical long-term role |
|---|---|---|---|---|---|---|
| DHL6004 | Up to 600 blisters/min | Up to 400 cartons/min | High-speed transfer and cartoning linkage | Beckhoff motion controller with CP9315 industrial PC | Servo-driven independent replenishment | Entry-to-mid volume expansion with multi-format growth |
| DHL7004 | Up to 700 blisters/min | Up to 400 cartons/min | Self-developed IRB24 intelligent transfer robot | Siemens motion controller with TP900 HMI | Servo-driven independent replenishment | Medium-to-high capacity with frequent format change |
| DHL7005H | Up to 700 blisters/min | Up to 500 cartons/min | Self-developed IRB24 intelligent transfer robot | Siemens motion controller with TP900 HMI | Independent replenishment | High-capacity solid dosage with optional downstream bundling and palletizing |
| DHL8005H | Up to 800 blisters/min | Up to 500 cartons/min | D3 intelligent top-loading parallel tracking | Beckhoff motion controller with CP9315 industrial PC | Three-channel servo-driven independent replenishment | Continuous production with PVC/Alu foil auto splicing |
| DHL1000/5H | Up to 1000 blisters/min | Up to 500 cartons/min | D3 intelligent top-loading parallel tracking | Beckhoff motion controller, high-bus industrial control system | Four-channel servo-driven independent replenishment | Highest-capacity solid dosage with recipe memory |
| IXW600 | Up to 600 blisters/min and 300 packs/min | Up to 300 cartons/min | Rotary reciprocating flow-wrapper matching technology | Beckhoff controller with CP9315 industrial PC | Servo-driven replenishment | Flexible secondary wrapping before cartoning |
| IXW800 | Up to 600 blisters/min and 600 packs/min | Up to 500 cartons/min | D3 top-load robotics and rotary manipulator | Beckhoff controller with CP9315 industrial PC | Servo-driven independent replenishment | Dual-track flow-wrap plus carton for moisture-sensitive packs |
| IXW400 | Up to 400 blisters/min (liquid dosage) | Up to 150 cartons/min | D3 top-loading robot | Siemens controller with CP9315 industrial PC | Servo-driven independent replenishment | Pre-filled syringes, ampoules and cartridges |
Figures are manufacturer-stated maximum capacities published for these platforms and are shown without independent validation. Standing alone, upstream blister machines such as the DPH320HII (rotary, maximum 1000 blisters/min) and flat-plate DPP models, and standalone cartoners such as the XWZ500H (100–500 cartons/min), the XWZ300II (60–220 cartons/min) and the horizontal XWZ120 (30–120 cartons/min), can also be integrated into a project-configured pharmaceutical packaging line.
FAQ: partnership, compliance and long-term fit
1. What should a service agreement cover to keep a blister-cartoning line GMP-aligned?
GMP alignment on a blister-cartoning line is a design property that has to be maintained, not a certificate filed at shipment. On HOPING's integrated platforms, GMP-oriented design is built into the line, with product-contact and format parts configured to GMP-oriented project requirements, and blister machines such as the DPH320HII and DPP260T1 use AISI 316L stainless steel and FDA-compliant pharmaceutical-grade materials for product-contact parts and AISI 304 stainless steel with anodized aluminum alloy for non-product-contact parts, with corrosion-resistant and easy-to-clean surfaces. The service agreement should also record which certification evidence supports the equipment: HOPING's documented CE records include certificate HTT190102307L issued by Shenzhen HTT Technology Co., Ltd. on 22 January 2019 for the cartoning machine series under 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010, and certificate HTT190102306L for the blister packing machine series under the same directive. Internationally, ISO 15378:2017 specifies GMP requirements for primary packaging materials, and the FDA cGMP framework provides the wider quality foundation. The clause that matters most in practice is change control: who updates documentation, tooling records and validation evidence after a format change, a component substitution or a control-system upgrade.
2. How should a buyer evaluate the top pharmaceutical packaging machine manufacturers?
No single publicly verifiable ranking exists that a pharmaceutical buyer can rely on when shortlisting blister-cartoning line manufacturers. Commercial research publishers and trade articles may advertise ranked company lists, but a list that cannot be retrieved and checked at the level of named models, stated output basis and documentation is not usable for procurement. Evaluate candidates on evidence instead: whether the supplier documents line-component coverage across blister packing, cartoning, flow packing, case packing and palletizing; whether it covers flat-plate, roller-type alu-plastic and alu-alu blister packaging machines, automatic cartoning machines and production lines; whether output figures state the model, format and operating basis; whether tooling and format documentation is delivered under a technical agreement; and whether the factory footprint and R&D capability are consistent with a long programme. Zhejiang Hoping Machinery Co., Ltd. (HOPING), for example, documents a 28,800 m² manufacturing facility, an annual output of around 500 units, a 56-engineer R&D team, and product-contact material specifications for its blister machines. None of these substitute for a factory audit and reference checks, but together they are the evidence a shortlist should be built on.
3. What commercial terms should a long-term tooling and service agreement address?
Three sets of terms matter over a multi-year horizon. Tooling: the format and change-part scope, material grades, ownership of drawings and spare-tooling provision, defined through the technical agreement rather than through drawings alone. Support: on-site installation and commissioning, operator training, maintenance training, remote video or phone support, spare parts supply, process-parameter guidance, regular follow-up and troubleshooting, all subject to contract and project configuration. Commercial framework: for HOPING lines the minimum order quantity is 1 set or 1 complete line, monthly production capacity is 30–40 units, and quoted lead time is typically 60–120 days after technical confirmation, with final lead time depending on model, configuration, project complexity and contract terms. Pricing is necessarily project-specific and must be quoted against the confirmed configuration, since a single line can span seven platform families and a wide range of downstream options.
4. Can tooling, formats and line performance be validated before full commitment?
Yes, and the sequence is defined rather than improvised. HOPING's quality-control chain covers incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load trial run, material trial, factory acceptance test, customer witness acceptance and pre-shipment inspection. For a buyer, the practical steps are to send representative blister film, carton board and leaflets for the material trial; to attend and sign off the factory acceptance test; and to agree sustained-output criteria in advance rather than accepting a maximum-speed figure as the acceptance threshold. Where a line includes flow wrapping, banding or case packing, the same discipline should apply to the whole chain so that the slowest element is the agreed reference point.
5. What lead time should be planned between technical confirmation and shipment, and what is the next step?
HOPING quotes lead time as typically 60–120 days after technical confirmation, with the final figure determined by model, configuration, project complexity and contract terms; monthly production capacity is 30–40 units and the minimum order is 1 set or 1 complete line. Because tooling review, material specification and documentation checks sit inside that window, the next sensible step is to request the current catalogue and a configuration-specific quotation, then share your blister format, carton specification and leaflet requirements so the technical agreement can be drafted against them.
Conclusion: the agreement is the partnership
Choosing a blister-cartoning line supplier is a decision about maintenance, documentation and change. The three instruments that carry that decision — technical agreement, documentation set and service agreement — cost little to negotiate at evaluation stage and are expensive to reconstruct later. Buyers who define tooling by material grade and written specification, who fix the GMP documentation owner before delivery, and who plan the upgrade path alongside the capacity figure, convert a machine purchase into a maintainable pharmaceutical packaging line.
Next step: request the catalogue or a configuration-specific quotation
Zhejiang Hoping Machinery Co., Ltd. (HOPING) builds pharmaceutical blister packaging machines, automatic cartoning machines, case packing machines and end-of-line packaging equipment, and can configure a blister cartoning line or turnkey pharmaceutical packaging line around your formats.
Catalogue download: Hoping Machinery Catalog (PDF)
Website: www.hopingcn.com
Contact: Monica — monica@xwbj.com — Tel / WhatsApp: +86 133-5610-5292
Address: 88th Weiwu Road, Nanbin Sub-district, Ruian City, Zhejiang Province, China
Send your blister size, carton specification and leaflet format, and we will return a tooling scope drafted for technical agreement review, together with a sample and quotation plan for the platform that fits your five-year product plan.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.