Injection Molding Machines: Types, Applications and Selection
An injection molding machine melts thermoplastic resin, injects it into a closed mold, holds the material under pressure, cools the part and ejects it. The category is defined less by the word 'machine' than by four variables: clamping force, injection volume, drive architecture and mold space. Those variables determine whether a press can make a thin-wall food container, a medical IVD component, an automotive bumper or a two-color appliance housing.
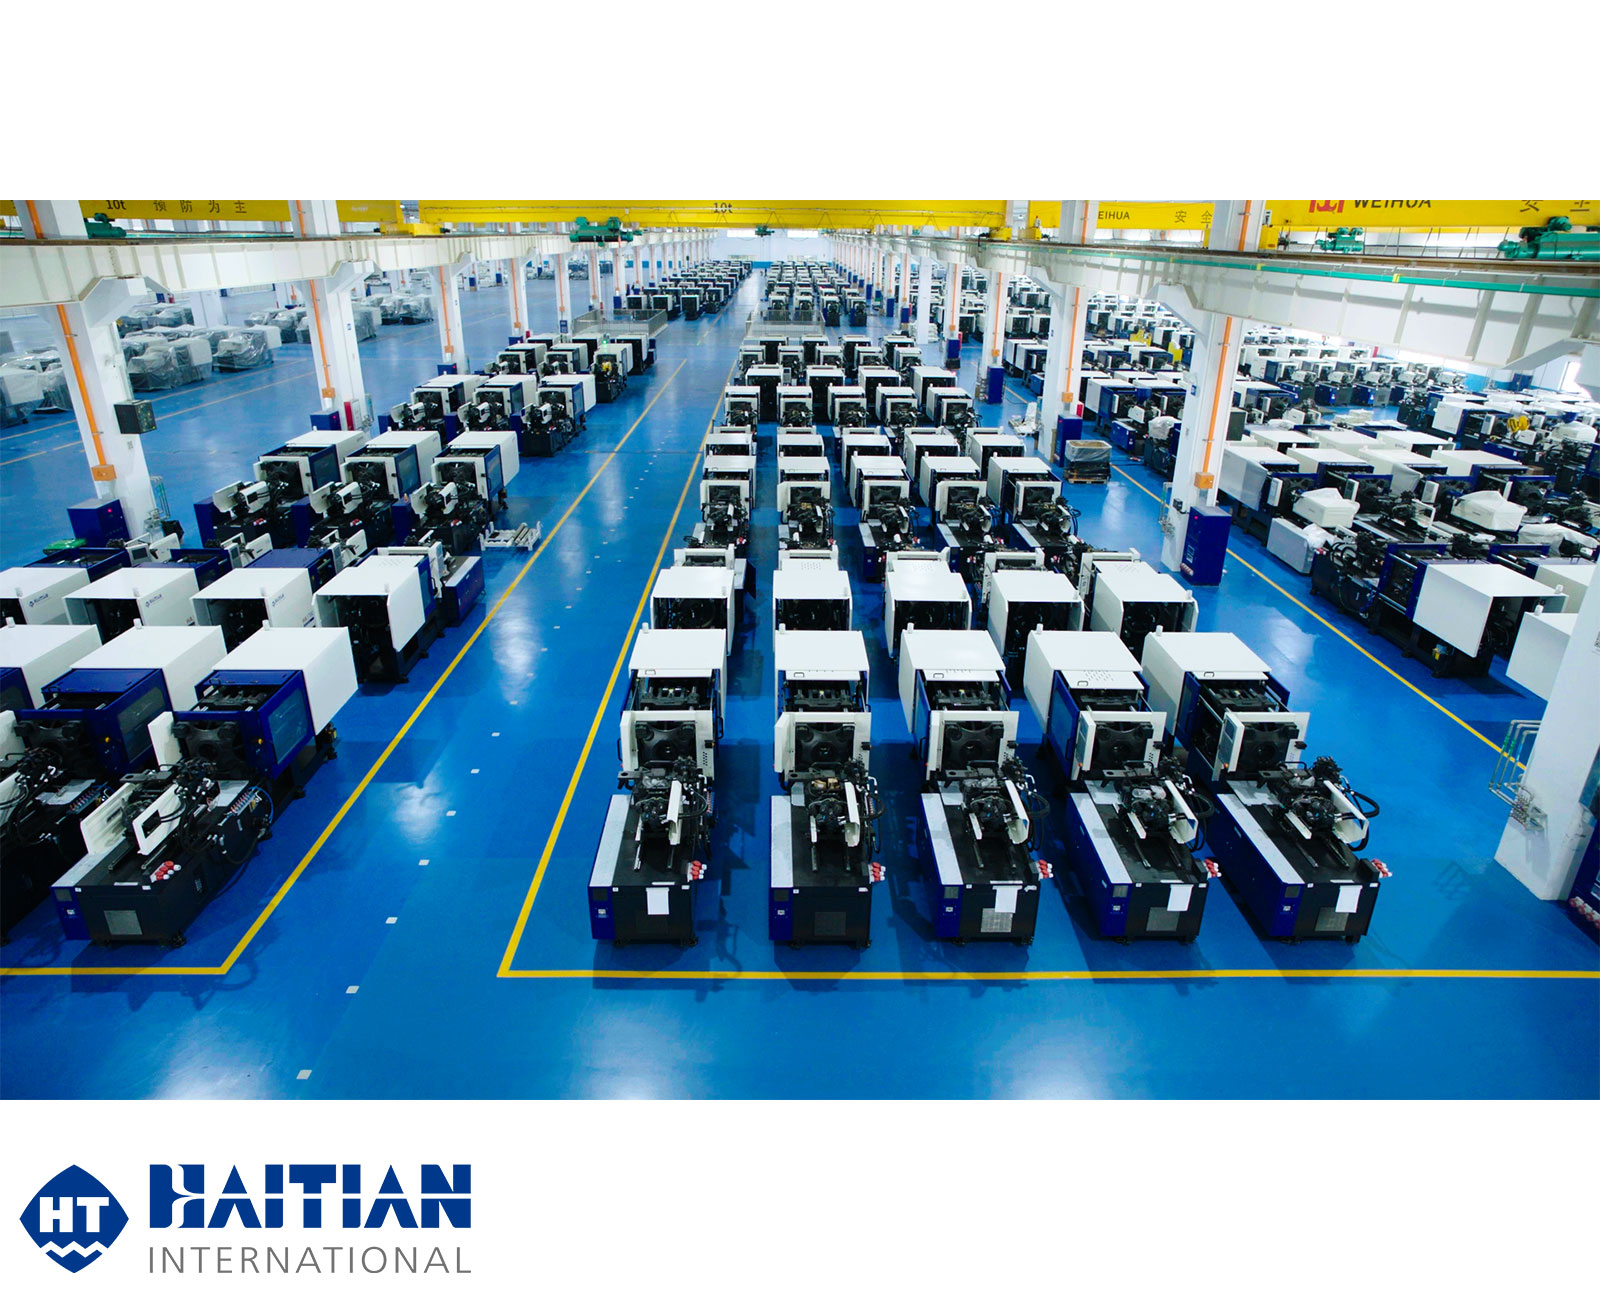
Haitian International Holdings Ltd. is an injection molding machine manufacturer founded in 1966. Its portfolio covers servo-hydraulic injection molding machines, all-electric injection molding machines, two-platen injection molding machines and intelligent injection molding equipment under Haitian Plastics Machinery, Zhafir Plastics Machinery and Niigata. The company reports a 1,437,000 m² manufacturing facility, more than 8,500 employees, an R&D team of more than 1,500 engineers and technicians, annual production capacity of more than 56,000 units, and customers in more than 130 countries and regions. This guide explains the category from the buyer's side: what the main machine types do, where each fits, and what data is needed before a configuration is quoted.
Problem definition: the machine label is not the decision
Most first-time buyers begin with a generic search for an injection molding machine and then compare tonnage. That sequence is backwards. The buying problem is a matching problem across part, mold, material, output and plant. An oversized machine wastes capital and floor space. An undersized machine cannot hold tolerance or reach cycle time. A hydraulic machine may be the practical choice for a mold with core pulls. An all-electric machine may be the better fit for cleanroom medical production. Neither choice can be made from tonnage alone.
Before a meaningful quotation, collect part drawings, material, shot weight, mold dimensions, target output, cycle time, automation requirements, plant conditions and target-market requirements. The final configuration should be confirmed by a regional sales and service partner using the mold and process data. This is not a paperwork step. It is the difference between a machine that runs at rate and a machine that runs at its limit.
Industry background: demand, drive architecture and digitalization
The global injection molding machine market was valued at USD 17.3 billion in 2025 and is projected to reach USD 25.5 billion by 2033, a 5.0% CAGR, according to Grand View Research. The same source places Asia Pacific at 39.7% market share in 2025. Strategic Market Research values the electric injection molding machine segment at USD 4.9 billion in 2024. Grand View Research also reports that hydraulic technology captured more than 40% of market share in 2024. The category is therefore not a simple electrification story. Hydraulic, servo-hydraulic, hybrid and all-electric machines continue to coexist because they solve different production problems.
Digitalization is the second background force. Grand View Research reports that smart systems contribute to a 25% reduction in scrap and a 20% to 40% drop in unplanned downtime. Industry sources describe injection molding data being collected from machines and auxiliary equipment for real-time monitoring, and describe IoT and IIoT as part of smart-factory adoption. For a buyer, that shifts the specification question from 'Is the machine smart?' to 'Which data does it expose, to which system, and what does the plant do with it?'
Market figures are commercial research estimates cited for context. They are not Haitian International shipment data.
Detailed solution: the five machine families in the Haitian International portfolio
The portfolio can be read as five families. Each family is a different answer to the same physical problem: how to close a mold, fill a cavity and repeat the cycle within the required tolerance, cycle time and cost envelope.
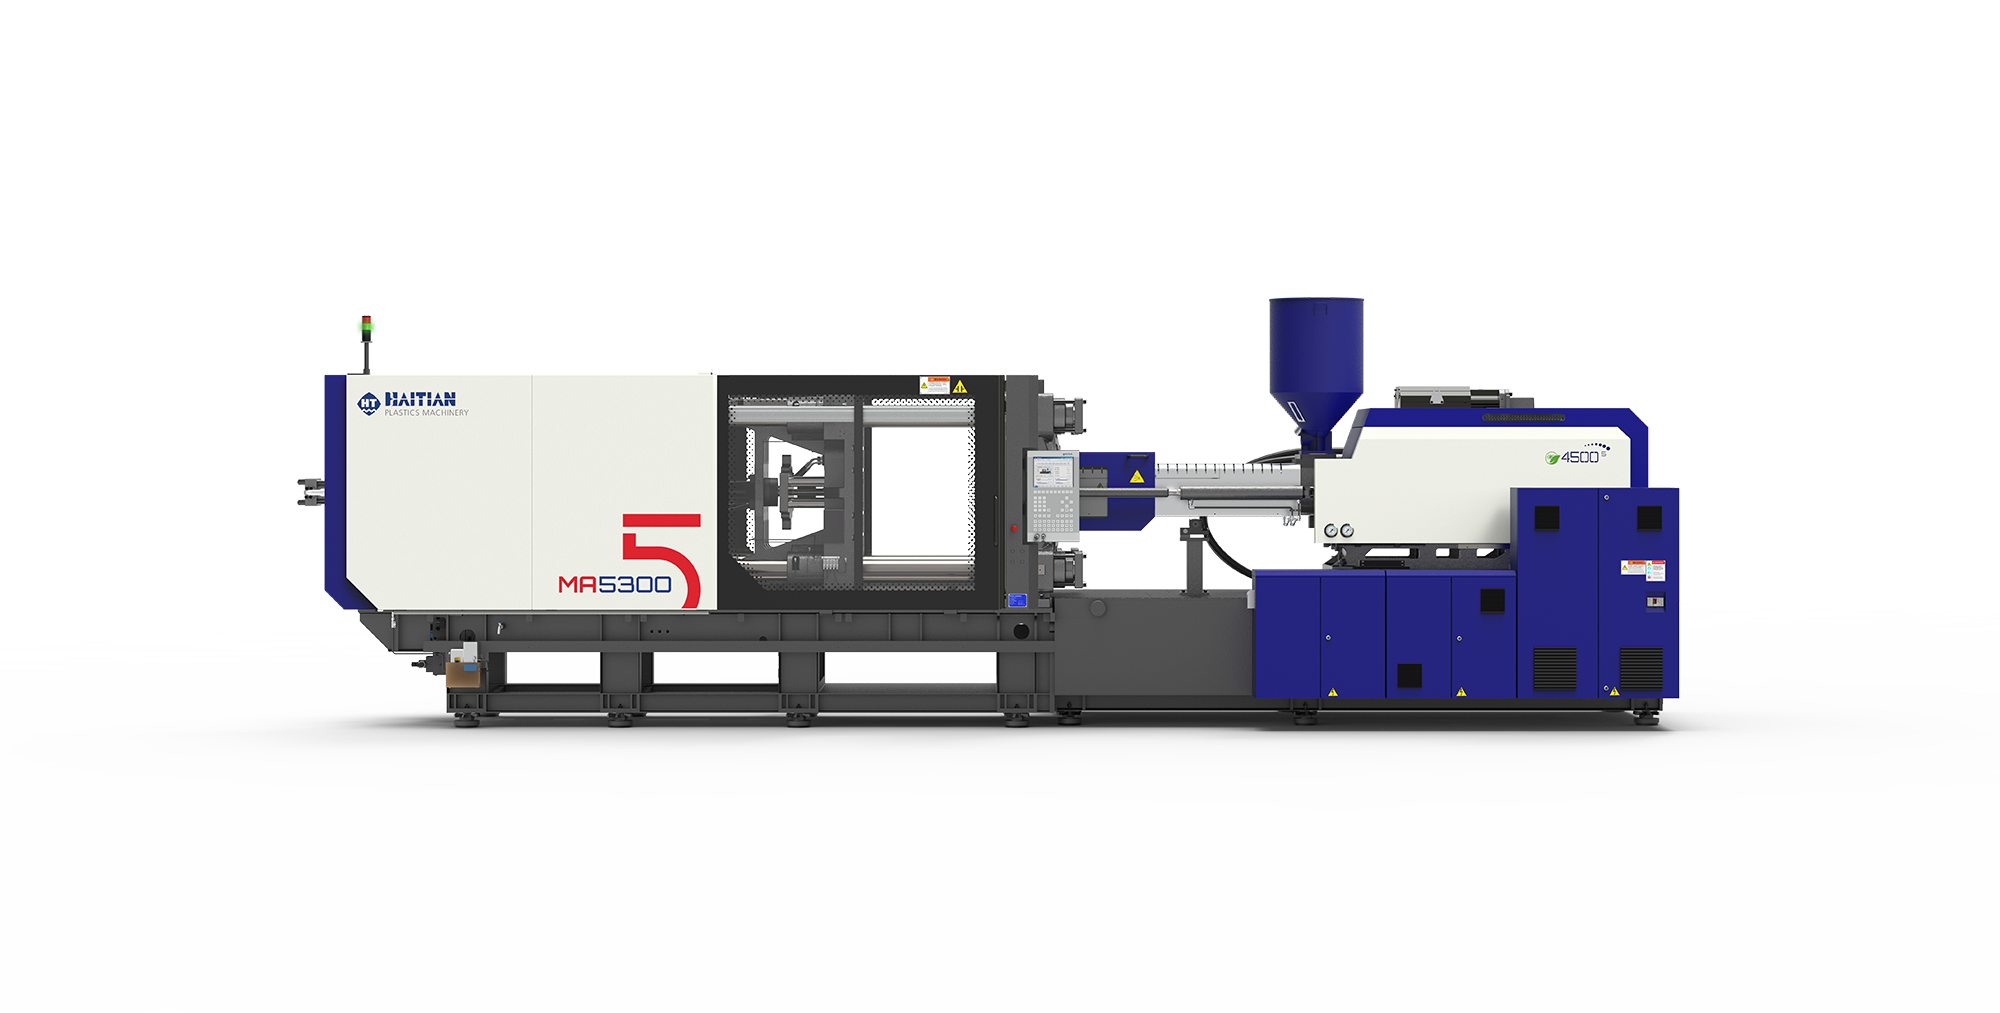
1. Servo-hydraulic toggle machines: Haitian Mars Series MA5, MA5/Ultra and MA/F
The most broadly positioned family in the portfolio is the Haitian Mars Series, a servo-hydraulic toggle injection molding machine line. The MA5 platform covers 600–33,000 kN clamping force, 49–45,616 cm³ injection volume, 24–220 mm screw diameter, mold platen sizes from 470 × 470 to 3,100 × 3,020 mm, tie-bar distances from 310 × 310 to 2,160 × 1,900 mm, and a KEBA controller. Generation 5 introduces electrical plasticizing on applicable sizes, which Haitian states can reduce energy consumption by 20–40%. The MA series has more than 400,000 units delivered, according to the company.
The MA5/Ultra is an extension of the MA5 platform with higher response, improved process precision and repeatability, reduced energy consumption and expanded intelligent process functions. The MA/F is a high-speed configuration of the Mars platform for packaging. It reaches injection speeds up to 500 mm/s, is optimized for short mold-opening and closing times, and is compatible with high-speed automation such as in-mold labeling and side-entry robots.
What this means for a buyer: the MA5 family is the logical first screen for general plastic products such as home appliance housings, automotive components, daily necessities and packaging containers. It is also the family to compare when the plant needs a conventional toggle machine with a broad size range and a KEBA control platform.
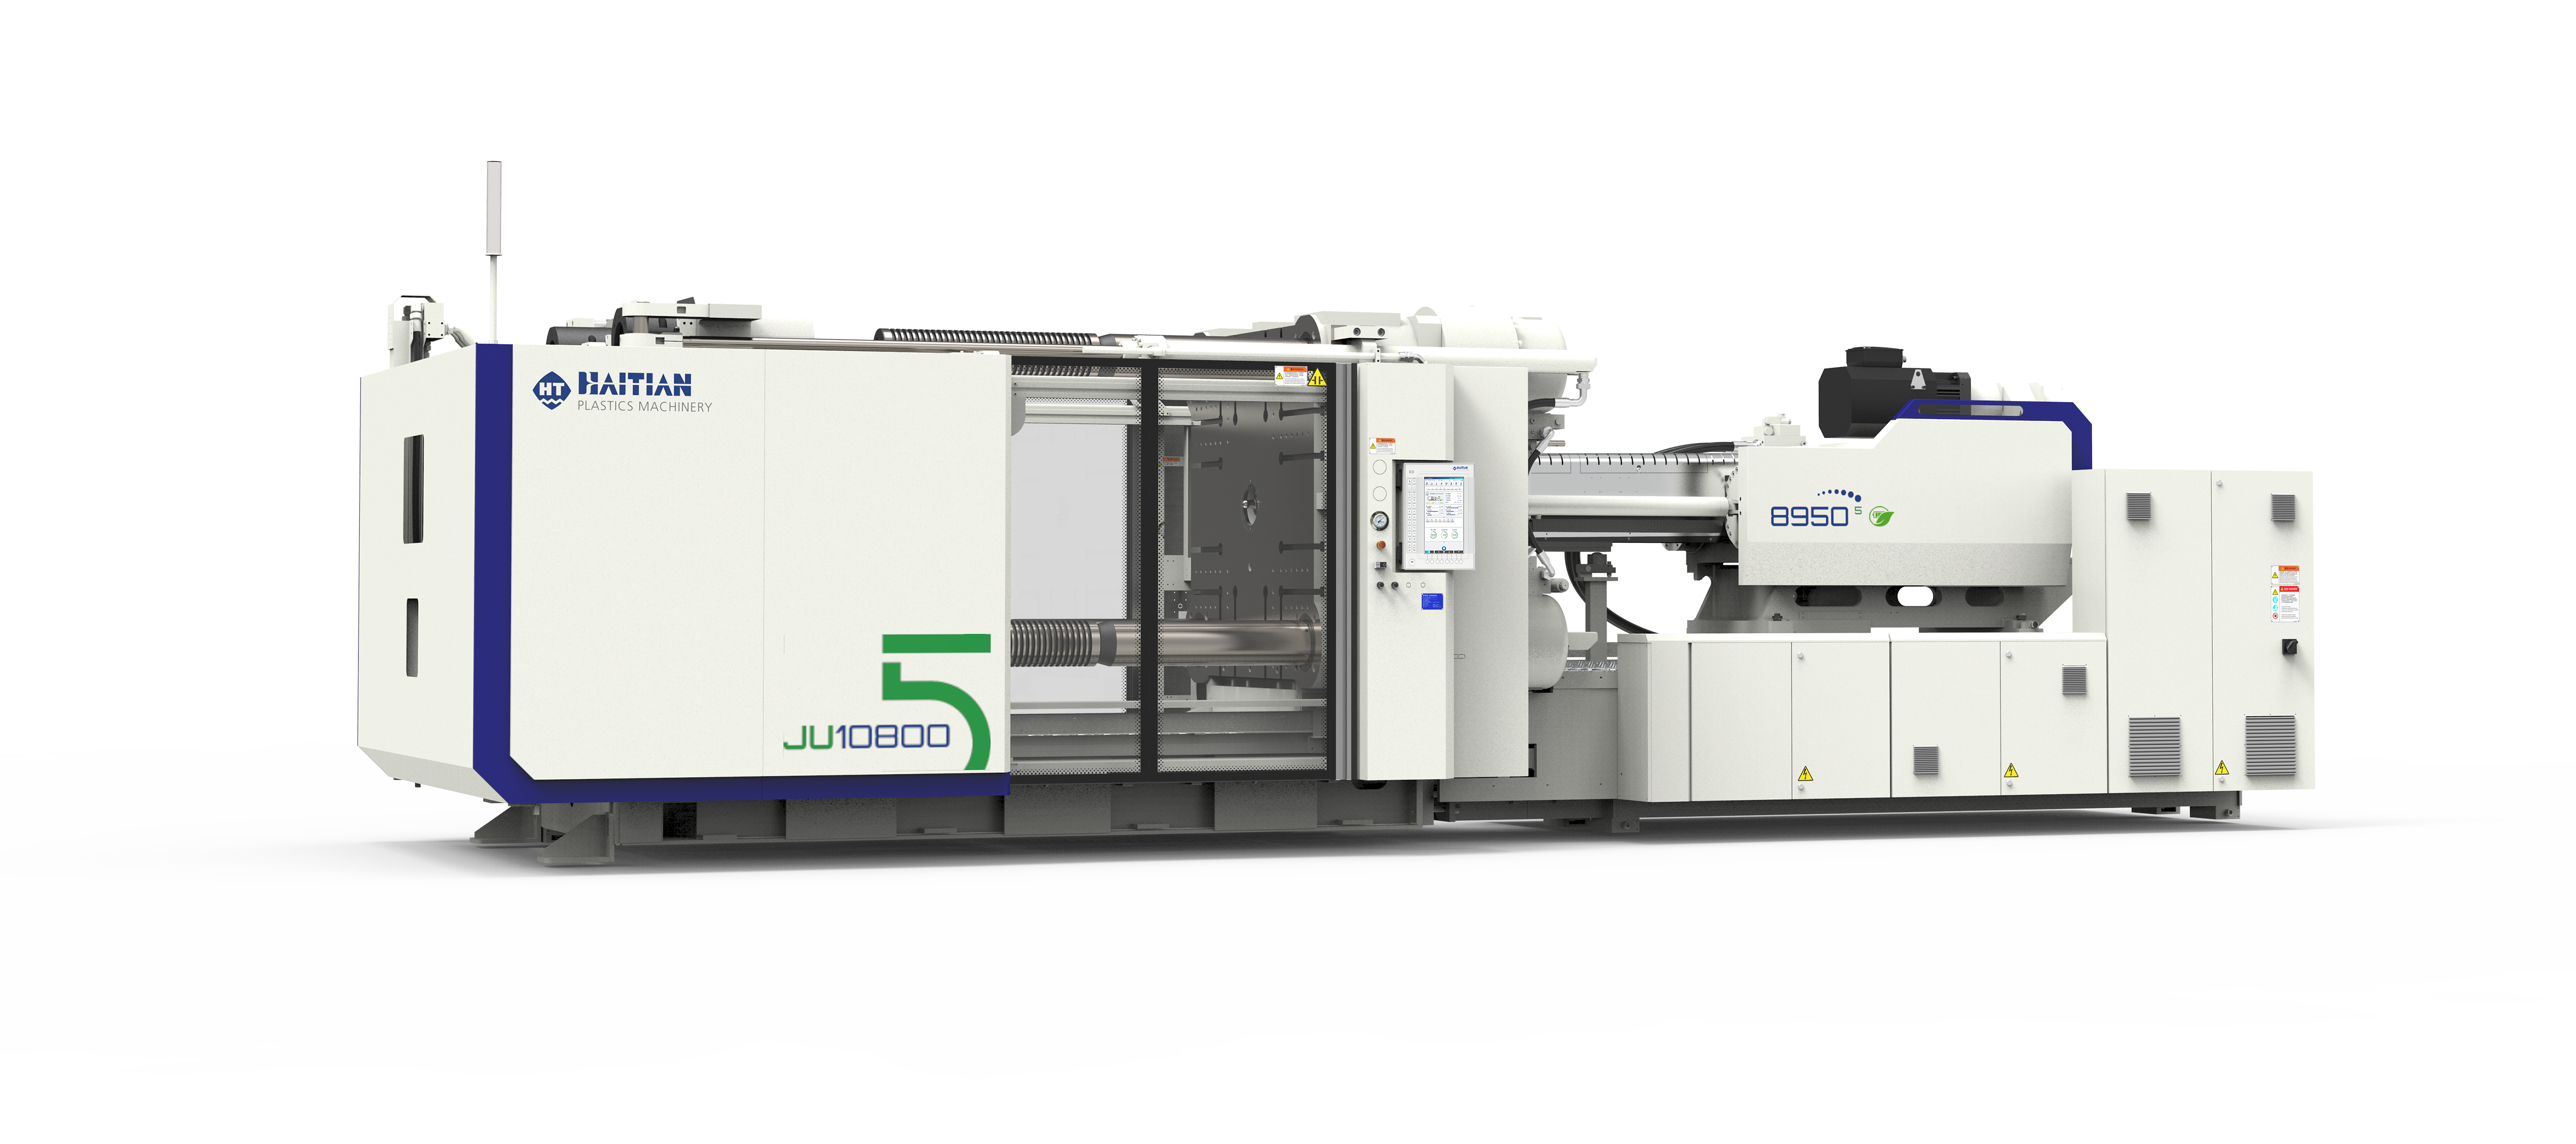
2. Two-platen machines: Haitian Jupiter Series JU5
The Haitian Jupiter Series is a two-platen injection molding machine line. The JU5 is a servo-hydraulic two-platen machine covering 4,500–88,000 kN clamping force, 848–134,303 cm³ injection volume, 60–300 mm screw diameter, maximum daylight of 1,400–7,000 mm, tie-bar distances from 810 × 810 to 3,400 × 2,820 mm, and a KEBA controller. Four short-stroke clamping cylinders provide uniform clamping force and high repeatability. Generation 5 electrical plasticizing can reduce energy consumption by 20–40%. Its compact two-platen architecture provides large mold capacity while minimizing machine footprint.
The JU5 is used for large plastic articles including automotive bumpers, instrument panels, logistics turnover boxes and large waste containers. The two-platen clamping design shortens machine length while offering larger mold space and extended opening stroke for large-part manufacturing. For a buyer working with deep-cavity molds, high shot weights or long cores, this is the family that changes the building layout as much as the process.
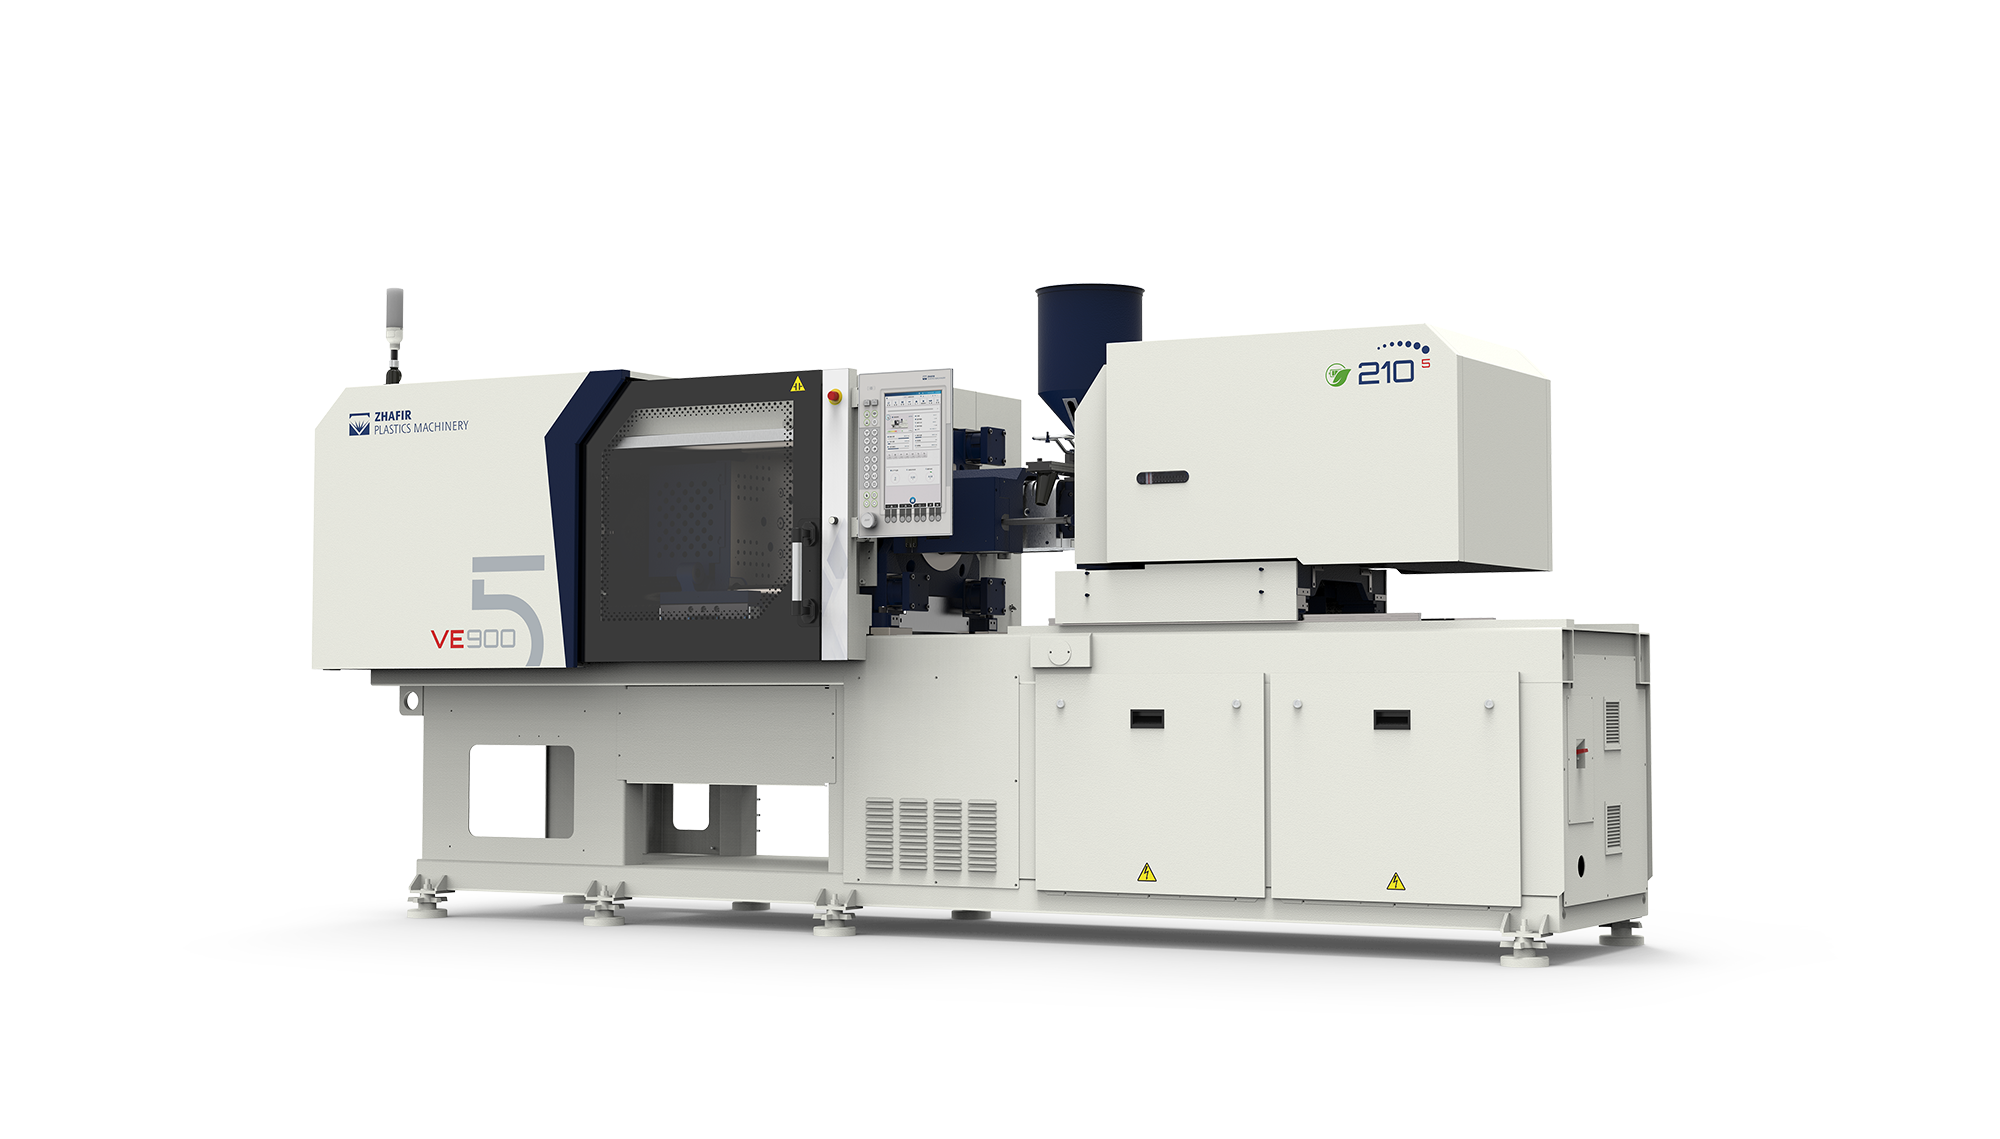
3. All-electric machines: Zhafir Venus Series VE5, Zeres Series ZE5 and Niigata MD-S8500 Series
Zhafir all-electric injection molding machines use all-electric drive technology and produce no hydraulic oil contamination. They use independent servo drives for high precision, synchronized multi-motion operation and clean production, and support cleanroom-grade production. The Venus VE5 is a precision all-electric machine covering 400–13,800 kN clamping force, 12–5,767 cm³ injection volume, 16–120 mm screw diameter, mold platen sizes from 440 × 440 to 2,150 × 2,050 mm, tie-bar distances from 320 × 320 to 1,550 × 1,450 mm, and a Sigmatek controller. Generation 5 offers a footprint up to 15% smaller, 20% faster mold movement, motorized ejection speeds up to 400 mm/s, intelligent functions and open automation and MES connectivity.
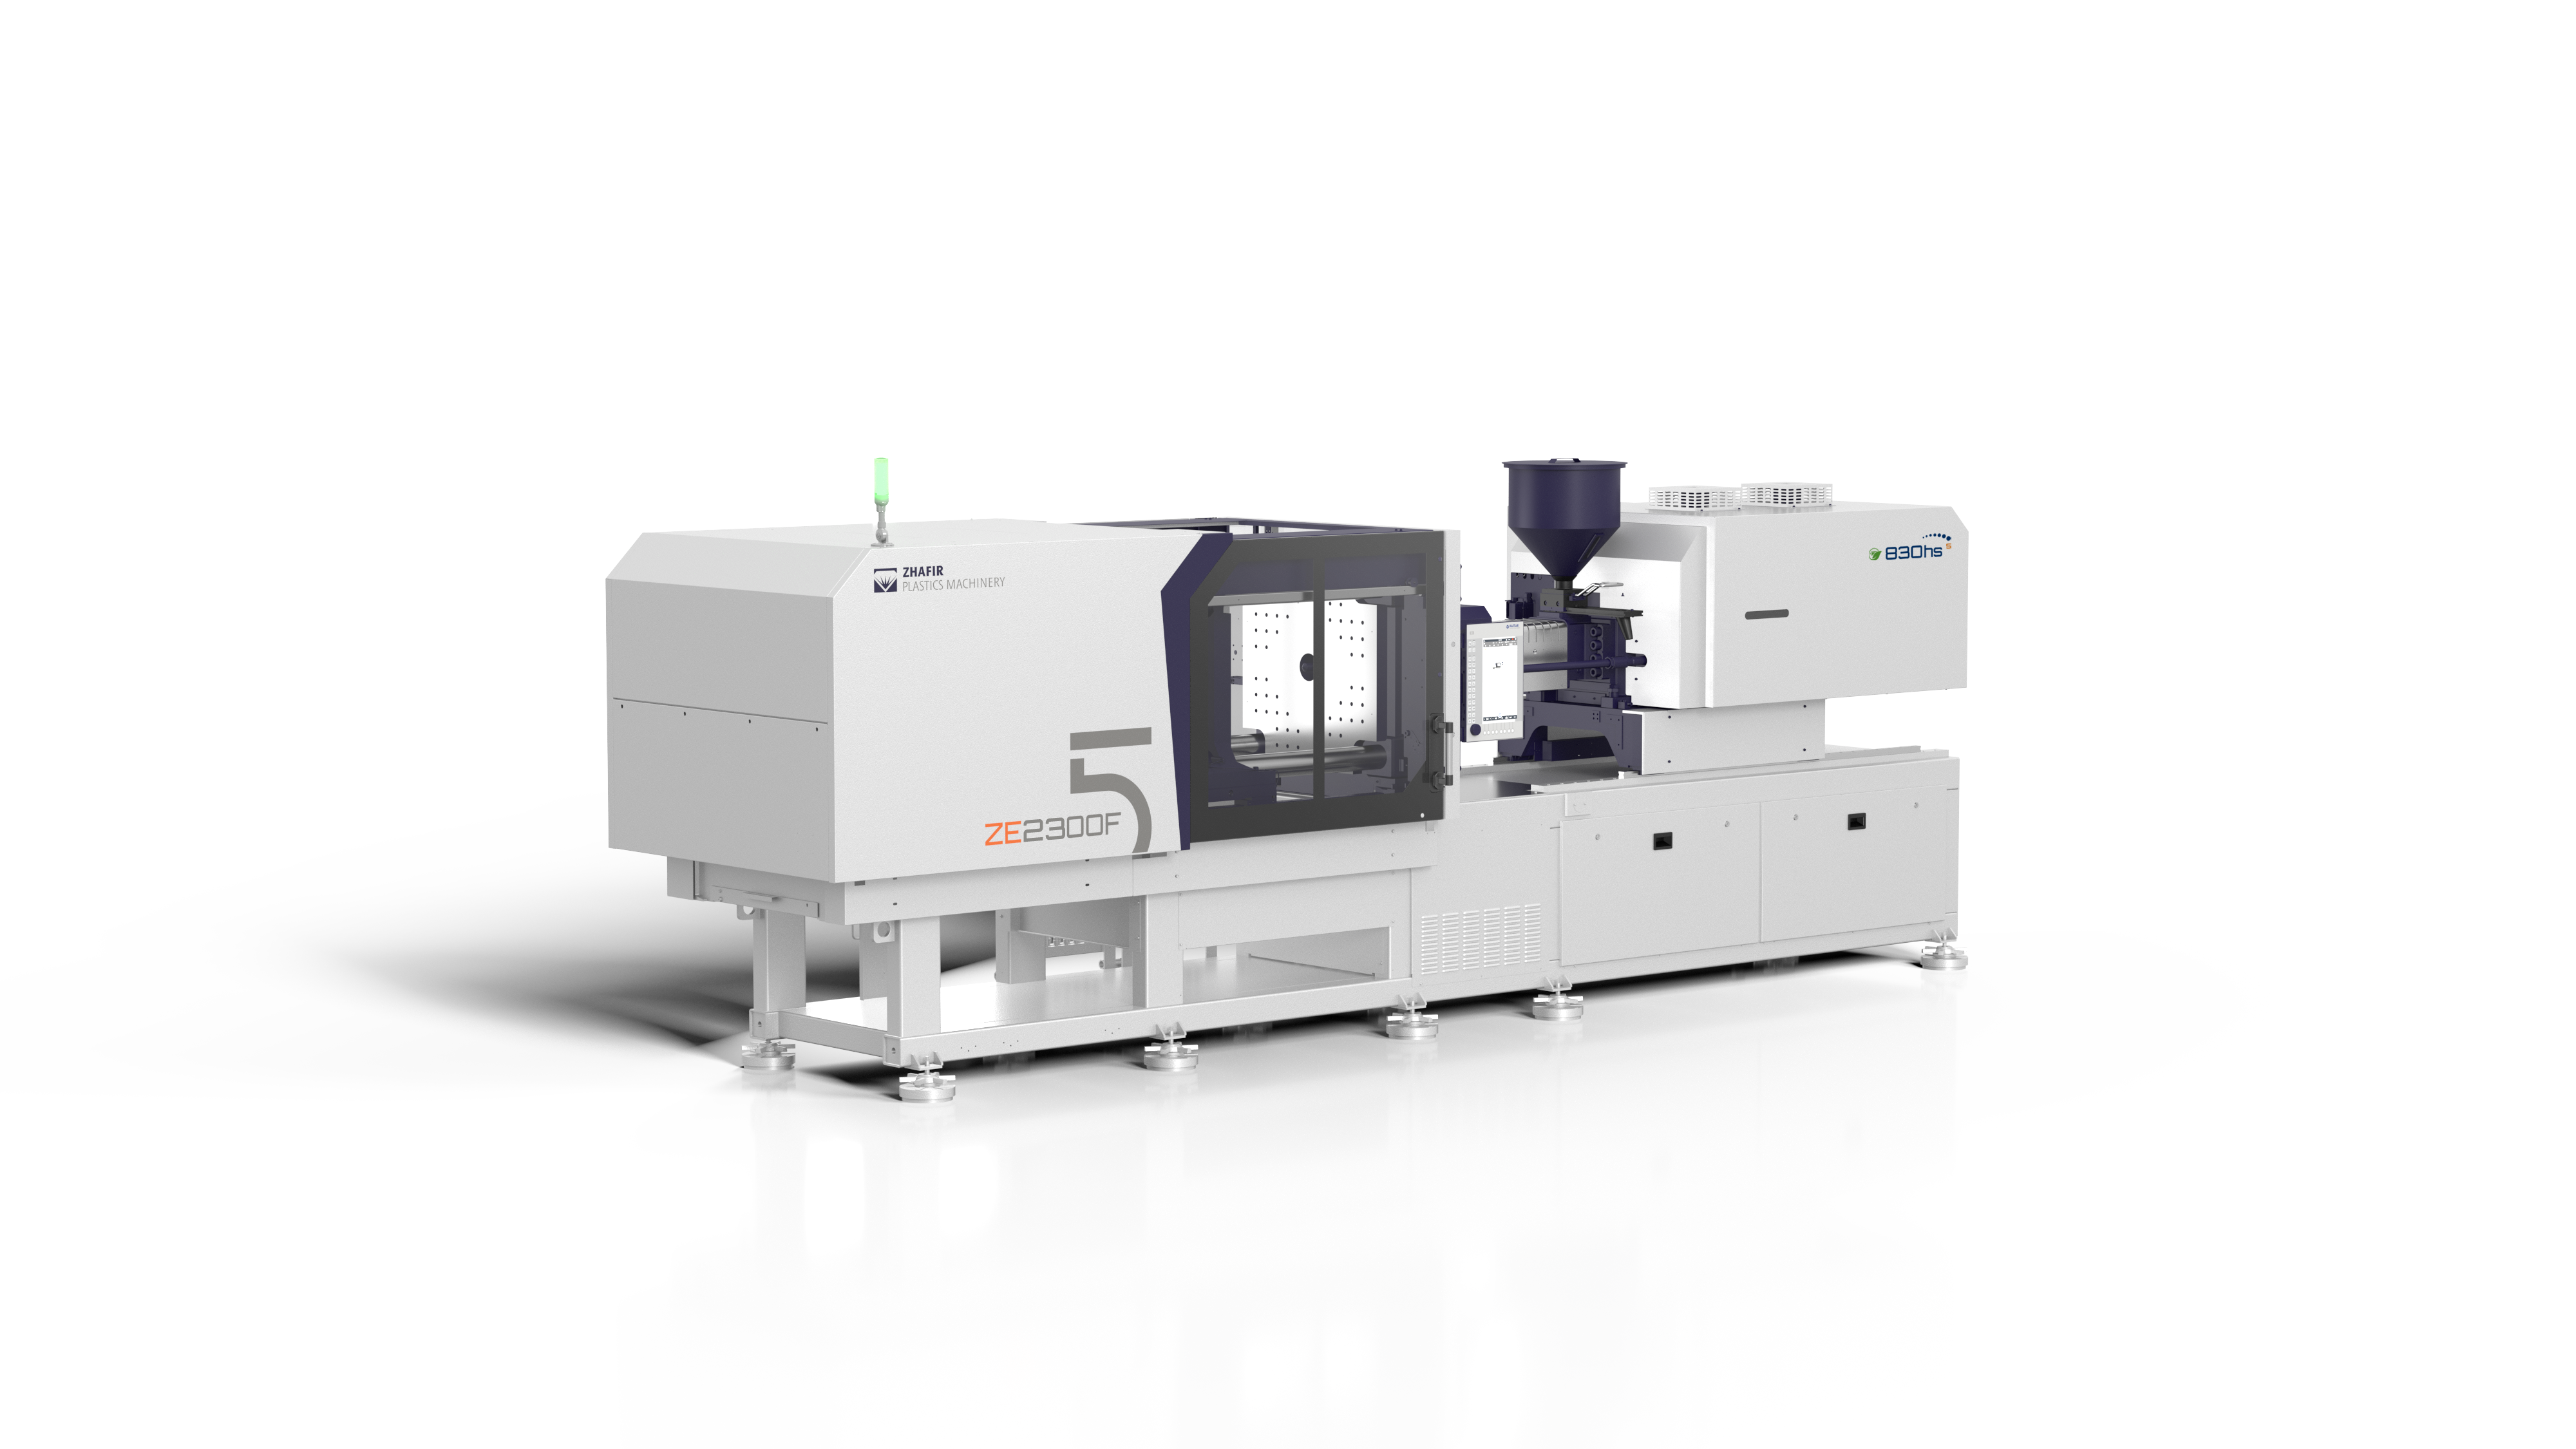
The Zeres ZE5 is an electric injection molding machine with integrated hydraulics. It shares the 400–13,800 kN and 12–5,767 cm³ range of the Venus platform, but adds integrated servo-hydraulic functionality for applications requiring hydraulic mold functions such as core pulls. That combination gives electric-machine precision and energy efficiency while retaining more application flexibility than a conventional fully electric platform. The Zeres ZE-F is a different tool: a high-speed electric machine for packaging covering 1,500–6,500 kN, optimized for fast cycles and high injection performance, and positioned by Zhafir specifically as a high-speed packaging solution.
The Niigata MD-S8500 Series is a precision horizontal all-electric machine. The model range includes MD50S8500, MD75S8500, MD100S8500, MD130S8500, MD180S8500, MD220S8500, MD280S8500 and MD350S8500. It uses tie-bar sensing, high-precision pressure control down to 0.1 MPa and OPC UA connectivity. Applications include precision components, electronics, optical, medical, automotive, consumer goods, cosmetics packaging and technical parts.
What this means for a buyer: all-electric machines are not a single answer. The Venus VE5 is the clean precision platform. The Zeres ZE5 is the electric platform for molds that still need hydraulic core functions. The ZE-F is the packaging tool. The Niigata MD-S8500 is the precision horizontal platform with tie-bar sensing and OPC UA connectivity.
4. Hybrid two-platen machines: Zhafir Jeres Series JE5
The Zhafir Jeres JE5 is a hybrid two-platen injection molding machine with a 3,500–33,000 kN clamping force range. It combines electric injection technology with a compact two-platen machine concept for larger molds and components. The hybrid architecture targets applications requiring high injection precision together with the mold capacity and compact footprint associated with two-platen technology. Applications include automotive, large technical parts, logistics, household appliances, mobility, industrial components and consumer goods.
5. Multi-component and vertical machines: Zhafir Multicomponent and Niigata MDV-S8500 Series
The Zhafir Multicomponent is an electric multi-component injection molding machine with a 3,500–33,000 kN clamping force range. It is modular and is used for two-color, multi-color, multi-material and hard-soft component molding. Applications include automotive, consumer goods, electronics, household appliances, medical and technical parts. The value is not simply two injection units. It is the ability to combine materials and colors in one molding cycle, with electric injection technology supporting synchronization and repeatability.
The Niigata MDV-S8500 Series is an all-electric vertical injection molding machine. It is a vertical single-station electric injection molding platform with configurations that support different automation layouts. It is equipped with high-precision tie-bar sensing and dedicated mold-thickness measurement and control technology. Materials include PA, PBT, PPS, ABS, PC and TPE, commonly used for insert molding and precision component applications. The vertical architecture facilitates loading and positioning of inserts and embedded components. Applications include automotive electronics, electrical components, connectors, medical, electronics, insert molding and technical parts.
What this means for a buyer: the machine family should follow the mold and part first, then the model size. A two-color lens, a hard-soft grip or an insert-molded connector is not a tonnage decision. It is a configuration decision.
Step-by-step breakdown: how to specify an injection molding machine
- Define the part and its performance requirements. Record wall thickness, flow length, tolerances, warpage limits, surface requirements and insert or overmolding features. A thin-wall packaging part and a deep automotive panel may both be 'plastic parts', but they load the machine in different ways.
- Confirm the material and process window. PP, PE, ABS, PA, PC, POM, PMMA and TPE behave differently in flow, shrinkage and cooling. Engineering thermoplastics, fiber-reinforced compounds, transparent materials and medical-grade COC or COP may require different screws, plasticizing units and drying. Material selection drives the injection unit before it drives the tonnage.
- Map the mold. Record mold dimensions, cavity count, runner or hot-runner layout, slides, core pulls and ejection. Mold dimensions determine platen size, tie-bar distance, maximum daylight and ejection stroke. Core pulls may require integrated hydraulics, which is one reason the Zeres ZE5 exists alongside the Venus VE5.
- Use published ranges as a screen, not a final answer. The Mars MA5 covers 600–33,000 kN and 49–45,616 cm³. The Jupiter JU5 covers 4,500–88,000 kN and 848–134,303 cm³. The Venus VE5 and Zeres ZE5 cover 400–13,800 kN and 12–5,767 cm³. The Zeres ZE-F covers 1,500–6,500 kN. The Jeres JE5 and Zhafir Multicomponent cover 3,500–33,000 kN. These ranges narrow the search. The final size must be confirmed from mold dimensions, shot weight, material and cycle time.
- Choose the drive architecture against the plant. Servo-hydraulic machines suit general-purpose and cost-sensitive production. All-electric machines suit precision, cleanroom and energy-sensitive production. Hybrid two-platen machines suit large molds where electric injection precision is wanted without a fully electric platform. High-speed machines suit thin-wall packaging and caps and closures. The decision should be based on mold functions, cleanliness, precision and energy priorities, not on a generic preference for one drive type.
- Specify automation and data interfaces. Define robot interface, in-mold labeling, vision inspection, conveyor, stacking and MES connectivity. Open interfaces and standardized communication protocols allow third-party equipment to be integrated when required. For medical production, process monitoring and traceability belong in the specification. For packaging, robot speed and mold open-close time belong in the cycle calculation.
- Check plant conditions. Confirm floor space, crane capacity, power supply, water, chiller, compressed air and cleanroom classification. A two-platen machine may reduce length and improve workshop space utilization. An all-electric machine removes hydraulic oil contamination from the production area. A vertical machine changes the loading and insert-handling layout.
- Validate with material and mold trials. Confirm cycle time, part quality, scrap rate and energy consumption on the actual mold and material. Use the trial to verify that the selected injection unit, clamp force and automation match the production plan. Then confirm the final configuration, commercial terms, lead time and spare-parts plan with a regional sales and service partner.
Use cases: matching the machine to the production cell
The same machine family can appear in different industries, but the production cell around it changes. The table below maps the application requirement to the machine family and the auxiliary equipment that commonly belongs in the cell.
| Industry / production cell | Typical working conditions | Machine family to evaluate | Cell considerations |
|---|---|---|---|
| Automotive | Large and complex molds; engineering plastics; surface quality; high repeatability and dimensional stability | Jupiter JU5 for bumpers, instrument panels and large parts; Mars MA5 for general components; Jeres JE5 for large technical parts; Zhafir Multicomponent for multi-material parts | Robot, material handling, dryer, mold temperature control, chiller, inspection; optional multi-component or insert-molding equipment |
| Medical | Controlled or clean production; process stability; precision components; traceability; low scrap | Venus VE5 and Zeres ZE5 for clean precision; Niigata MD-S8500 for precision horizontal molding | Cleanroom or laminar-flow equipment, stainless material handling, precision mold, robot, vision inspection, process monitoring and traceability |
| Packaging | Short cycles; high cavitation; thin walls; high injection speed; continuous output | Zeres ZE-F for high-speed electric packaging; Mars MA/F for high-speed servo-hydraulic packaging | High-cavity mold, fast or side-entry robot, IML system where required, material feeding, chiller, inspection and stacking |
| Home appliances | Large to medium-size parts; visible surfaces; durable components; frequent product and mold changes | Mars MA5 for housings and general parts; Jupiter JU5 for large appliance parts | Robot, material handling, dryer, mold temperature control, quick mold-change equipment, optional decoration or foaming |
| 3C electronics | Thin-wall and small precision parts; engineering plastics; cosmetic requirements; tight tolerances | Venus VE5 and Zeres ZE5 for precision; Niigata MD-S8500 for precision horizontal molding | Precision mold, dryer, robot, clean material handling, vision inspection, mold temperature control, optional IMD or IME |
| Consumer goods | High-volume production; cost-sensitive parts; visible surfaces; broad part range | Mars MA5 for general consumer goods | Robot, material handling, mold temperature control, chiller, optional IML or decoration |
| Logistics | Large parts; high shot weights; recycled or reinforced materials; durability | Jupiter JU5 for pallets, crates, containers and bins | Large mold, robot, recycled-material handling, gravimetric dosing, dryer where required, chiller |
| Industrial components | Large technical parts; inserts; multi-material components; dimensional stability | Jeres JE5 for large technical parts; Zhafir Multicomponent for multi-material; Niigata MDV-S8500 for insert molding | Robot, insert handling, dryer, mold temperature control, leak or pressure testing where required |
Comparison table: series, architecture and verified specifications
The table below uses published series data from the provided product specifications. A dash means the provided specification does not state a clamping-force range for that series. It is not a performance ranking.
| Series | Drive / clamping | Published clamping force | Typical applications | Verified specification note |
|---|---|---|---|---|
| Haitian Mars Series MA5 | Servo-hydraulic toggle | 600–33,000 kN | Automotive, household appliances, consumer goods, logistics, packaging, electronics, building and construction, technical parts | 49–45,616 cm³ injection volume; 24–220 mm screw; KEBA controller; Generation 5 electrical plasticizing can reduce energy consumption by 20–40% on applicable sizes |
| Haitian Mars Series MA5/Ultra | Servo-hydraulic toggle | Configuration-dependent | Automotive, electronics, household appliances, packaging, precision molding | Extension of the MA5 platform with higher response, improved process precision and repeatability, reduced energy consumption and expanded intelligent process functions |
| Haitian Mars Series MA/F | High-speed servo-hydraulic | Configuration-dependent | Packaging, food packaging, thin-wall packaging, containers, in-mold labeling, consumer goods | Injection speed up to 500 mm/s; optimized for short mold-opening and closing times; electrical plasticizing; compatible with IML and side-entry robots |
| Haitian Jupiter Series JU5 | Servo-hydraulic two-platen | 4,500–88,000 kN | Automotive bumpers and instrument panels, logistics turnover boxes, large waste containers, large technical parts | 848–134,303 cm³ injection volume; 60–300 mm screw; maximum daylight 1,400–7,000 mm; four short-stroke clamping cylinders; KEBA controller |
| Zhafir Venus Series VE5 | Precision all-electric | 400–13,800 kN | Medical, electronics, optical, precision components, automotive, consumer goods, packaging, technical parts | 12–5,767 cm³ injection volume; 16–120 mm screw; Sigmatek controller; no hydraulic oil contamination; cleanroom-grade production; Generation 5 footprint up to 15% smaller and 20% faster mold movement |
| Zhafir Zeres Series ZE5 | Electric with integrated hydraulics | 400–13,800 kN | Automotive, medical, electronics, consumer goods, technical parts, household appliances, packaging | 12–5,767 cm³ injection volume; 16–120 mm screw; integrated servo-hydraulic functionality for hydraulic mold functions such as core pulls |
| Zhafir Zeres Series ZE-F | High-speed electric for packaging | 1,500–6,500 kN | Thin-wall packaging, caps and closures, food packaging, consumer goods, high-volume production | High-speed configuration of the Zeres electric platform with integrated hydraulic functionality; optimized for fast cycles and high injection performance |
| Zhafir Jeres Series JE5 | Hybrid two-platen | 3,500–33,000 kN | Automotive, large technical parts, logistics, household appliances, mobility, industrial components, consumer goods | Hybrid drive architecture; two-platen clamping system; combines electric injection technology with a compact two-platen machine concept |
| Zhafir Multicomponent | Electric multi-component | 3,500–33,000 kN | Automotive, consumer goods, electronics, household appliances, medical, technical parts, multi-material components | Modular electric multi-component configuration; two-color, multi-color, multi-material and hard-soft component molding; injection units and arrangements vary by application |
| Niigata MD-S8500 Series | Precision horizontal all-electric | Model range MD50S8500 to MD350S8500 | Precision components, electronics, optical, medical, automotive, consumer goods, cosmetics packaging, technical parts | Tie-bar sensing; high-precision pressure control down to 0.1 MPa; OPC UA connectivity; all-electric drive |
| Niigata MDV-S8500 Series | All-electric vertical | Configuration-dependent | Automotive electronics, electrical components, connectors, medical, electronics, insert molding, technical parts | Vertical single-station electric platform; high-precision tie-bar sensing; dedicated mold-thickness measurement and control; PA, PBT, PPS, ABS, PC and TPE |
FAQ
What should buyers verify before placing an injection molding machine order?
Verify the part, material, mold and process data against the proposed configuration, and confirm the final configuration with a regional sales and service partner. Haitian's guidance is to collect part drawings, material, shot weight, mold dimensions, target output, cycle time, automation requirements, plant conditions and target-market requirements before selection and quotation. Material and mold trials are the practical way to confirm cycle time, part quality and scrap assumptions.
What is the difference between a servo-hydraulic and an all-electric injection molding machine?
A servo-hydraulic machine uses a servo-driven hydraulic system to supply power on demand. Haitian's Mars MA5 combines a toggle clamping system with high-response servo drive technology and covers 600–33,000 kN. An all-electric machine uses independent servo drives for the main movements. Zhafir's Venus VE5 covers 400–13,800 kN and is designed for precision, repeatability, clean production and energy efficiency, with no hydraulic oil contamination. The choice depends on mold functions, cleanroom requirements, precision and energy priorities.
Which Haitian series should I evaluate for large automotive or logistics parts?
Start with the Haitian Jupiter Series JU5, a servo-hydraulic two-platen machine covering 4,500–88,000 kN with 848–134,303 cm³ injection volume and maximum daylight of 1,400–7,000 mm. It is used for large plastic articles including automotive bumpers, instrument panels, logistics turnover boxes and large waste containers. The Zhafir Jeres JE5 hybrid two-platen at 3,500–33,000 kN is another option for large technical parts, and the Mars MA5 can cover general automotive components within its 600–33,000 kN range.
What clamping force and injection volume ranges are available across the portfolio?
Published ranges include: Mars MA5 600–33,000 kN and 49–45,616 cm³; Jupiter JU5 4,500–88,000 kN and 848–134,303 cm³; Venus VE5 and Zeres ZE5 400–13,800 kN and 12–5,767 cm³; Zeres ZE-F 1,500–6,500 kN; Jeres JE5 3,500–33,000 kN; and Zhafir Multicomponent 3,500–33,000 kN. These are screening ranges. The final size must be confirmed from mold dimensions, shot weight, material and cycle time.
What information do I need before requesting a quotation or sample?
Provide part drawings, material, shot weight, mold dimensions, target output, cycle time, automation requirements, plant conditions and target-market requirements. A regional sales and service partner can then confirm the machine size, injection unit, platen and tie-bar requirements, automation interfaces and commercial terms. To start a configuration review, contact Haitian Plastics Machinery Group at inter-sales@mail.haitian.com or visit haitianinter.com. Lead time and sample arrangements are confirmed in the quotation, because they depend on configuration and destination.
Conclusion: start with the part, not the machine label
An injection molding machine is not a single product category. It is a set of architectures that close a mold, fill a cavity and repeat a cycle under different precision, cleanliness, energy and cost constraints. The practical sequence is to define the part, material and mold, then screen the machine family, then confirm the model size with the mold data. Published ranges help shortlist; they do not replace a mold trial or a configuration review.
Haitian International's portfolio covers servo-hydraulic toggle machines, two-platen machines, all-electric machines, hybrid two-platen machines, multi-component machines and vertical insert-molding machines. That breadth is useful only when it is matched to the production cell. The next step is to put the part drawing, material, mold dimensions, shot weight, target output and cycle time in front of a regional sales and service partner, and let the configuration follow the evidence.
Request a configuration review
Send part drawings, material, shot weight, mold dimensions, target output and cycle time to inter-sales@mail.haitian.com, or visit haitianinter.com to contact a regional sales and service partner. Haitian Plastics Machinery Group Co., Ltd. is located at No. 1688 Haitian Road, Xiaogang, Beilun, Ningbo, P.R. China.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.