Powder Coating vs Galvanizing vs Silkscreen vs Anodizing for Custom Sheet Metal Parts
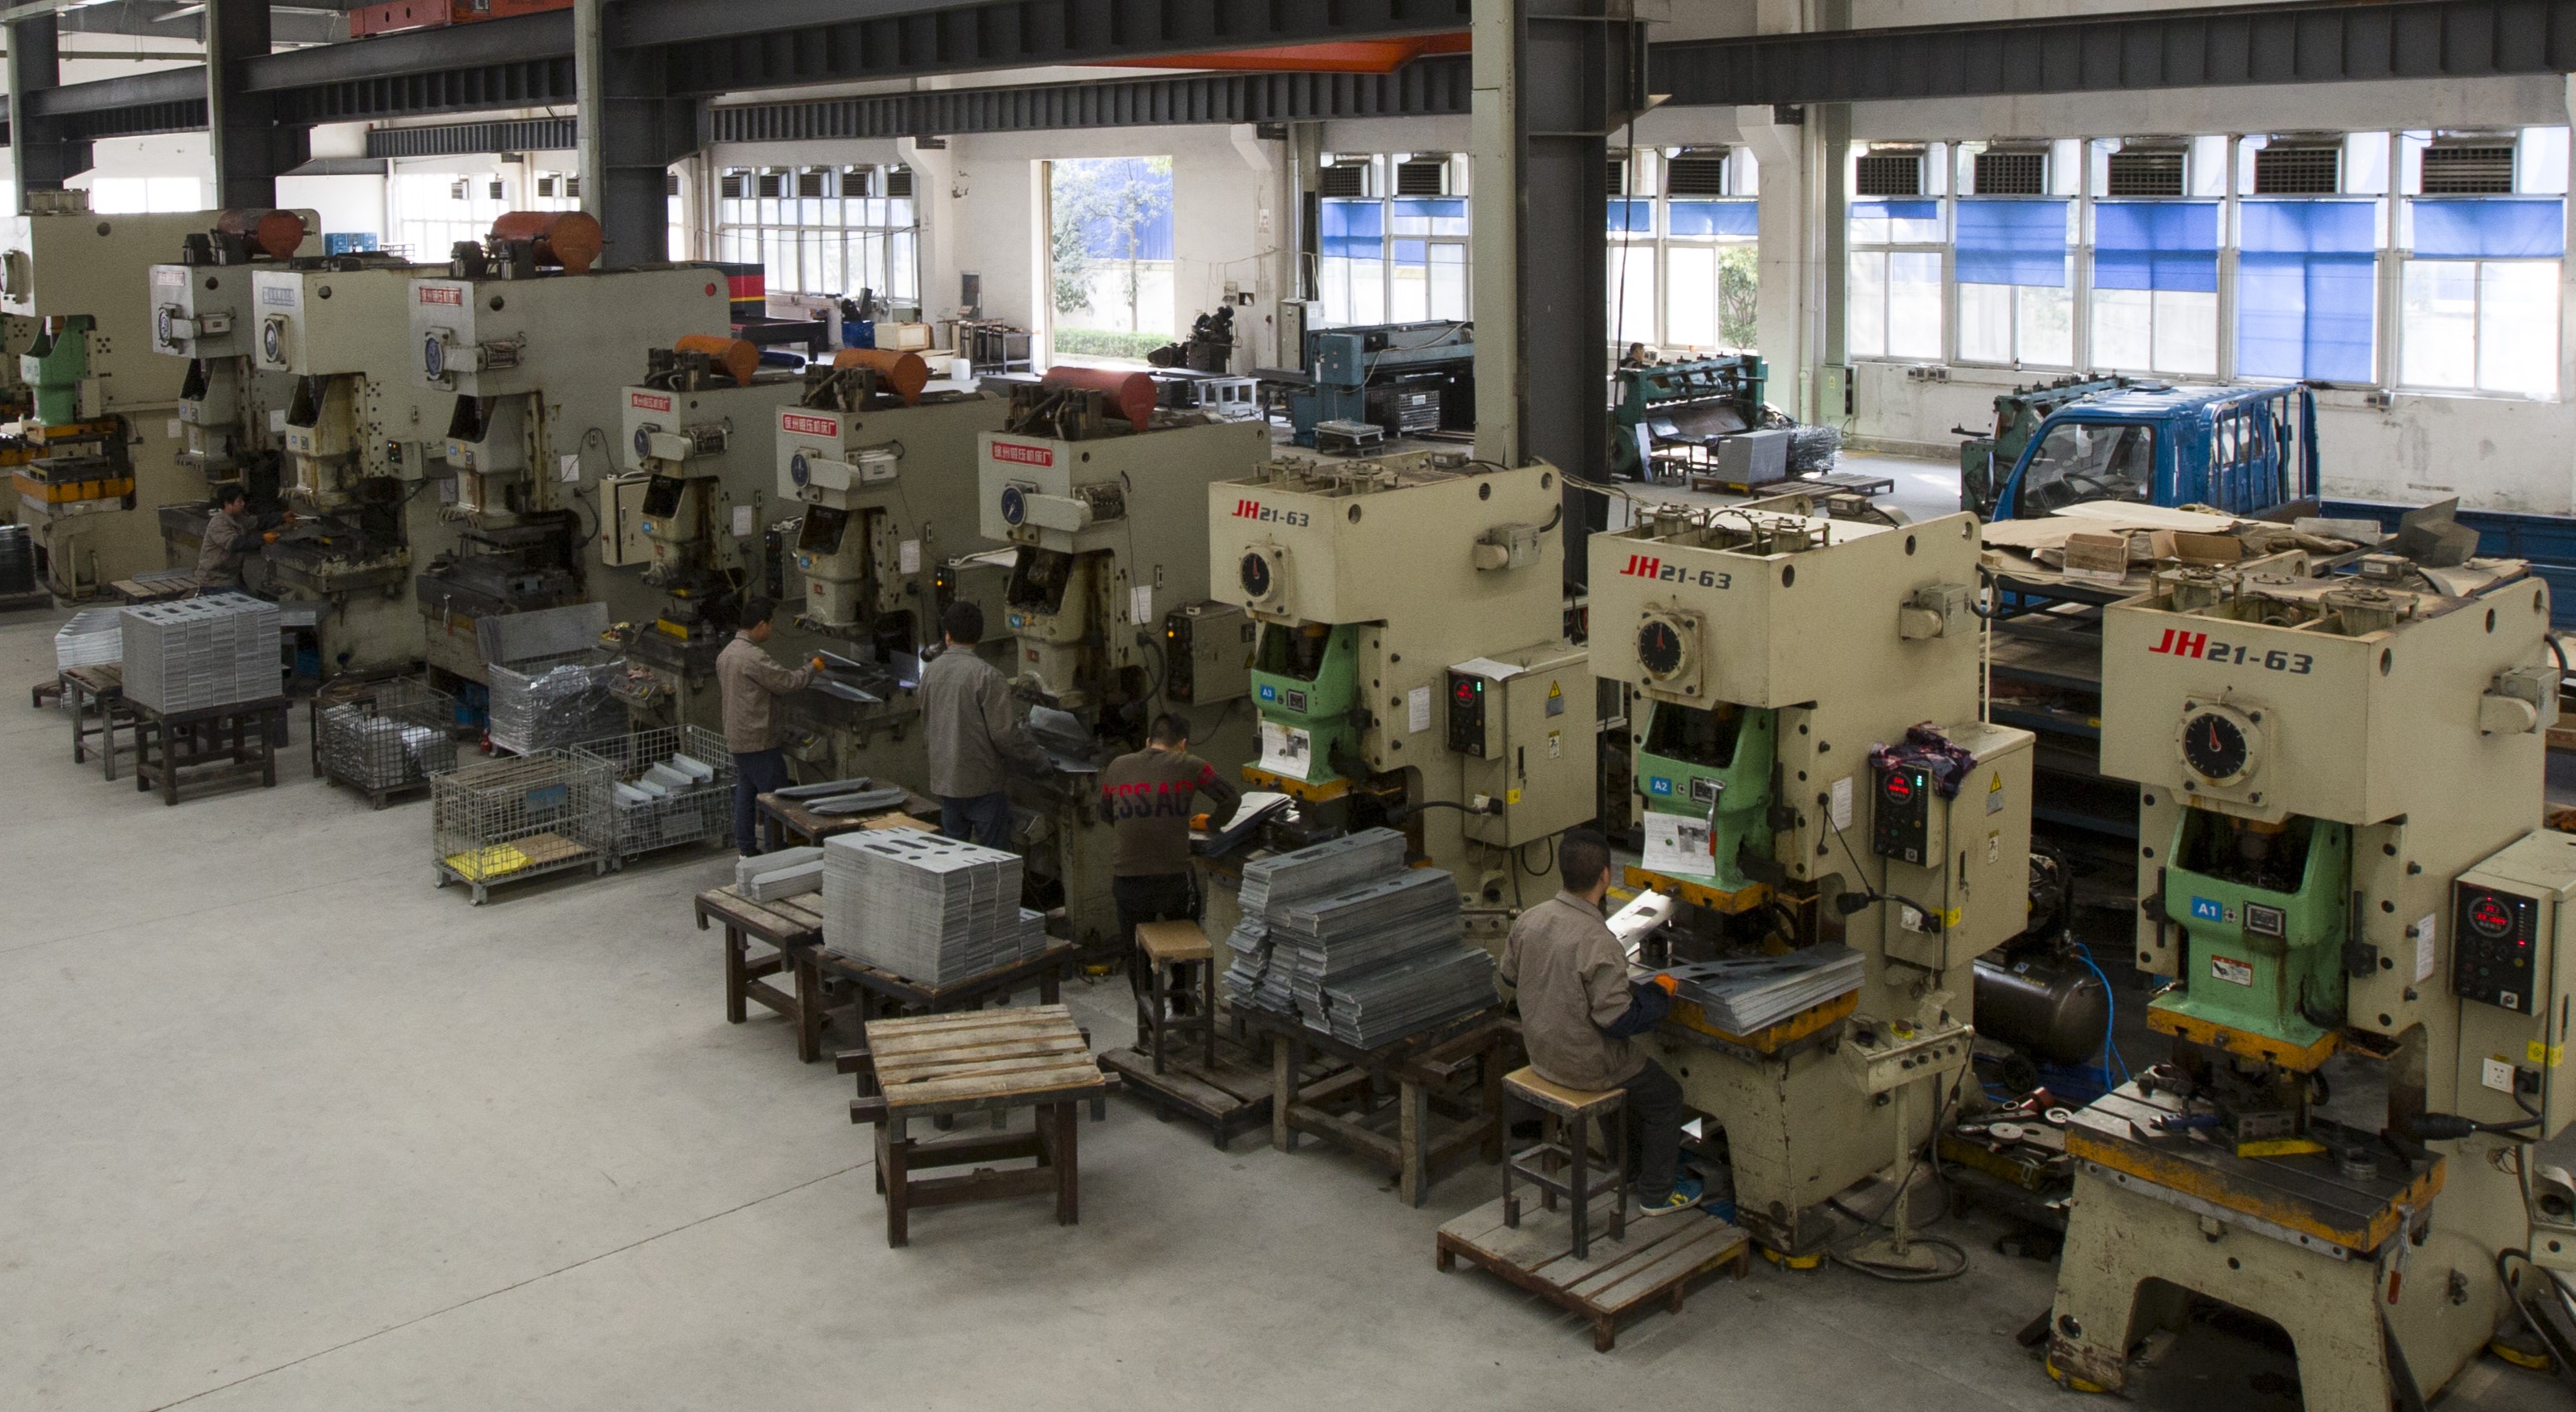
Stamping workshop at Haitong Metals.
The right finish for custom sheet metal parts is a specification decision, not a cosmetic afterthought. Powder coating, galvanizing, silkscreen, anodizing and plain finish solve different problems: color and barrier protection, metallic zinc protection for steel, marking and legends, an oxide finish for aluminum, or no added coating at all. The correct choice depends on the base material, the corrosion exposure, the drawing tolerance, the process route and the volume. Haitong Metals (Ningbo Haitong Metal Fabrication Co., Ltd.) is a China-based custom sheet metal fabrication and metal stamping manufacturer founded in 1988, with ISO 9001 certification, a 100% export ratio and main markets in Europe and North America. Its listed surface treatments include powder coating, galvanizing, passivation and other anti-corrosion treatments.
Problem definition: why finish selection changes cost, yield and lead time
Finish selection is often treated as a line item at the end of an RFQ. In practice, it can change the process route, the inspection plan and the total cost. A galvanized steel stamping part may need drain holes before hot-dip galvanizing; a powder-coated enclosure may need masking on grounding points; an anodized aluminum faceplate may need polishing before the oxide layer; a silkscreened control panel may need a coating underneath for durability. If these requirements are discovered after fabrication, rework or scrap can follow.
This comparison covers five options—powder coating, galvanizing, silkscreen, anodizing and plain finish—for custom sheet metal parts made from carbon steel, stainless steel, aluminum and galvanized steel. It uses a 0.5–8.0 mm thickness range and drawing-level tolerance as selection context. For context, the comparison data available for this article lists ±0.2 mm; if a drawing calls for a tighter target such as ±0.05 mm, treat it as a special precision requirement and confirm it before quoting. The same logic applies to sheet metal stamping, laser cutting, CNC bending, welding and polishing: the finish must be compatible with the process route, not selected in isolation.
Industry background: what buyers now specify in RFQs
Custom sheet metal parts support automation equipment, electronics enclosures, machinery frames, new energy hardware, communication cabinets, medical equipment and construction components. Buyers in Europe and North America often specify finishes by standard or by application condition, not by trade name alone. For steel, galvanized steel sheet is specified under standards such as ASTM A653/A653M for hot-dip zinc-coated steel sheet or EN 10346:2015 for continuously hot-dip coated steel flat products. For post-fabrication galvanizing, ISO 1461 specifies requirements for hot dip galvanized coatings on fabricated iron and steel articles.
For electrical and electronic equipment in the EU, Directive 2011/65/EU (RoHS 2) restricts certain hazardous substances, and Regulation (EC) No 1907/2006 (REACH) drives substance declaration and SVHC communication. ISO 9001:2015 remains the baseline quality management certification for general industrial suppliers. Where welded assemblies or structural components are involved, ISO 3834-2:2021 and EN 1090-1:2009+A1:2011 can enter the qualification discussion. These standards do not choose the finish for the buyer, but they define what evidence the buyer should request.
Detailed solution: a finish-by-finish decision framework
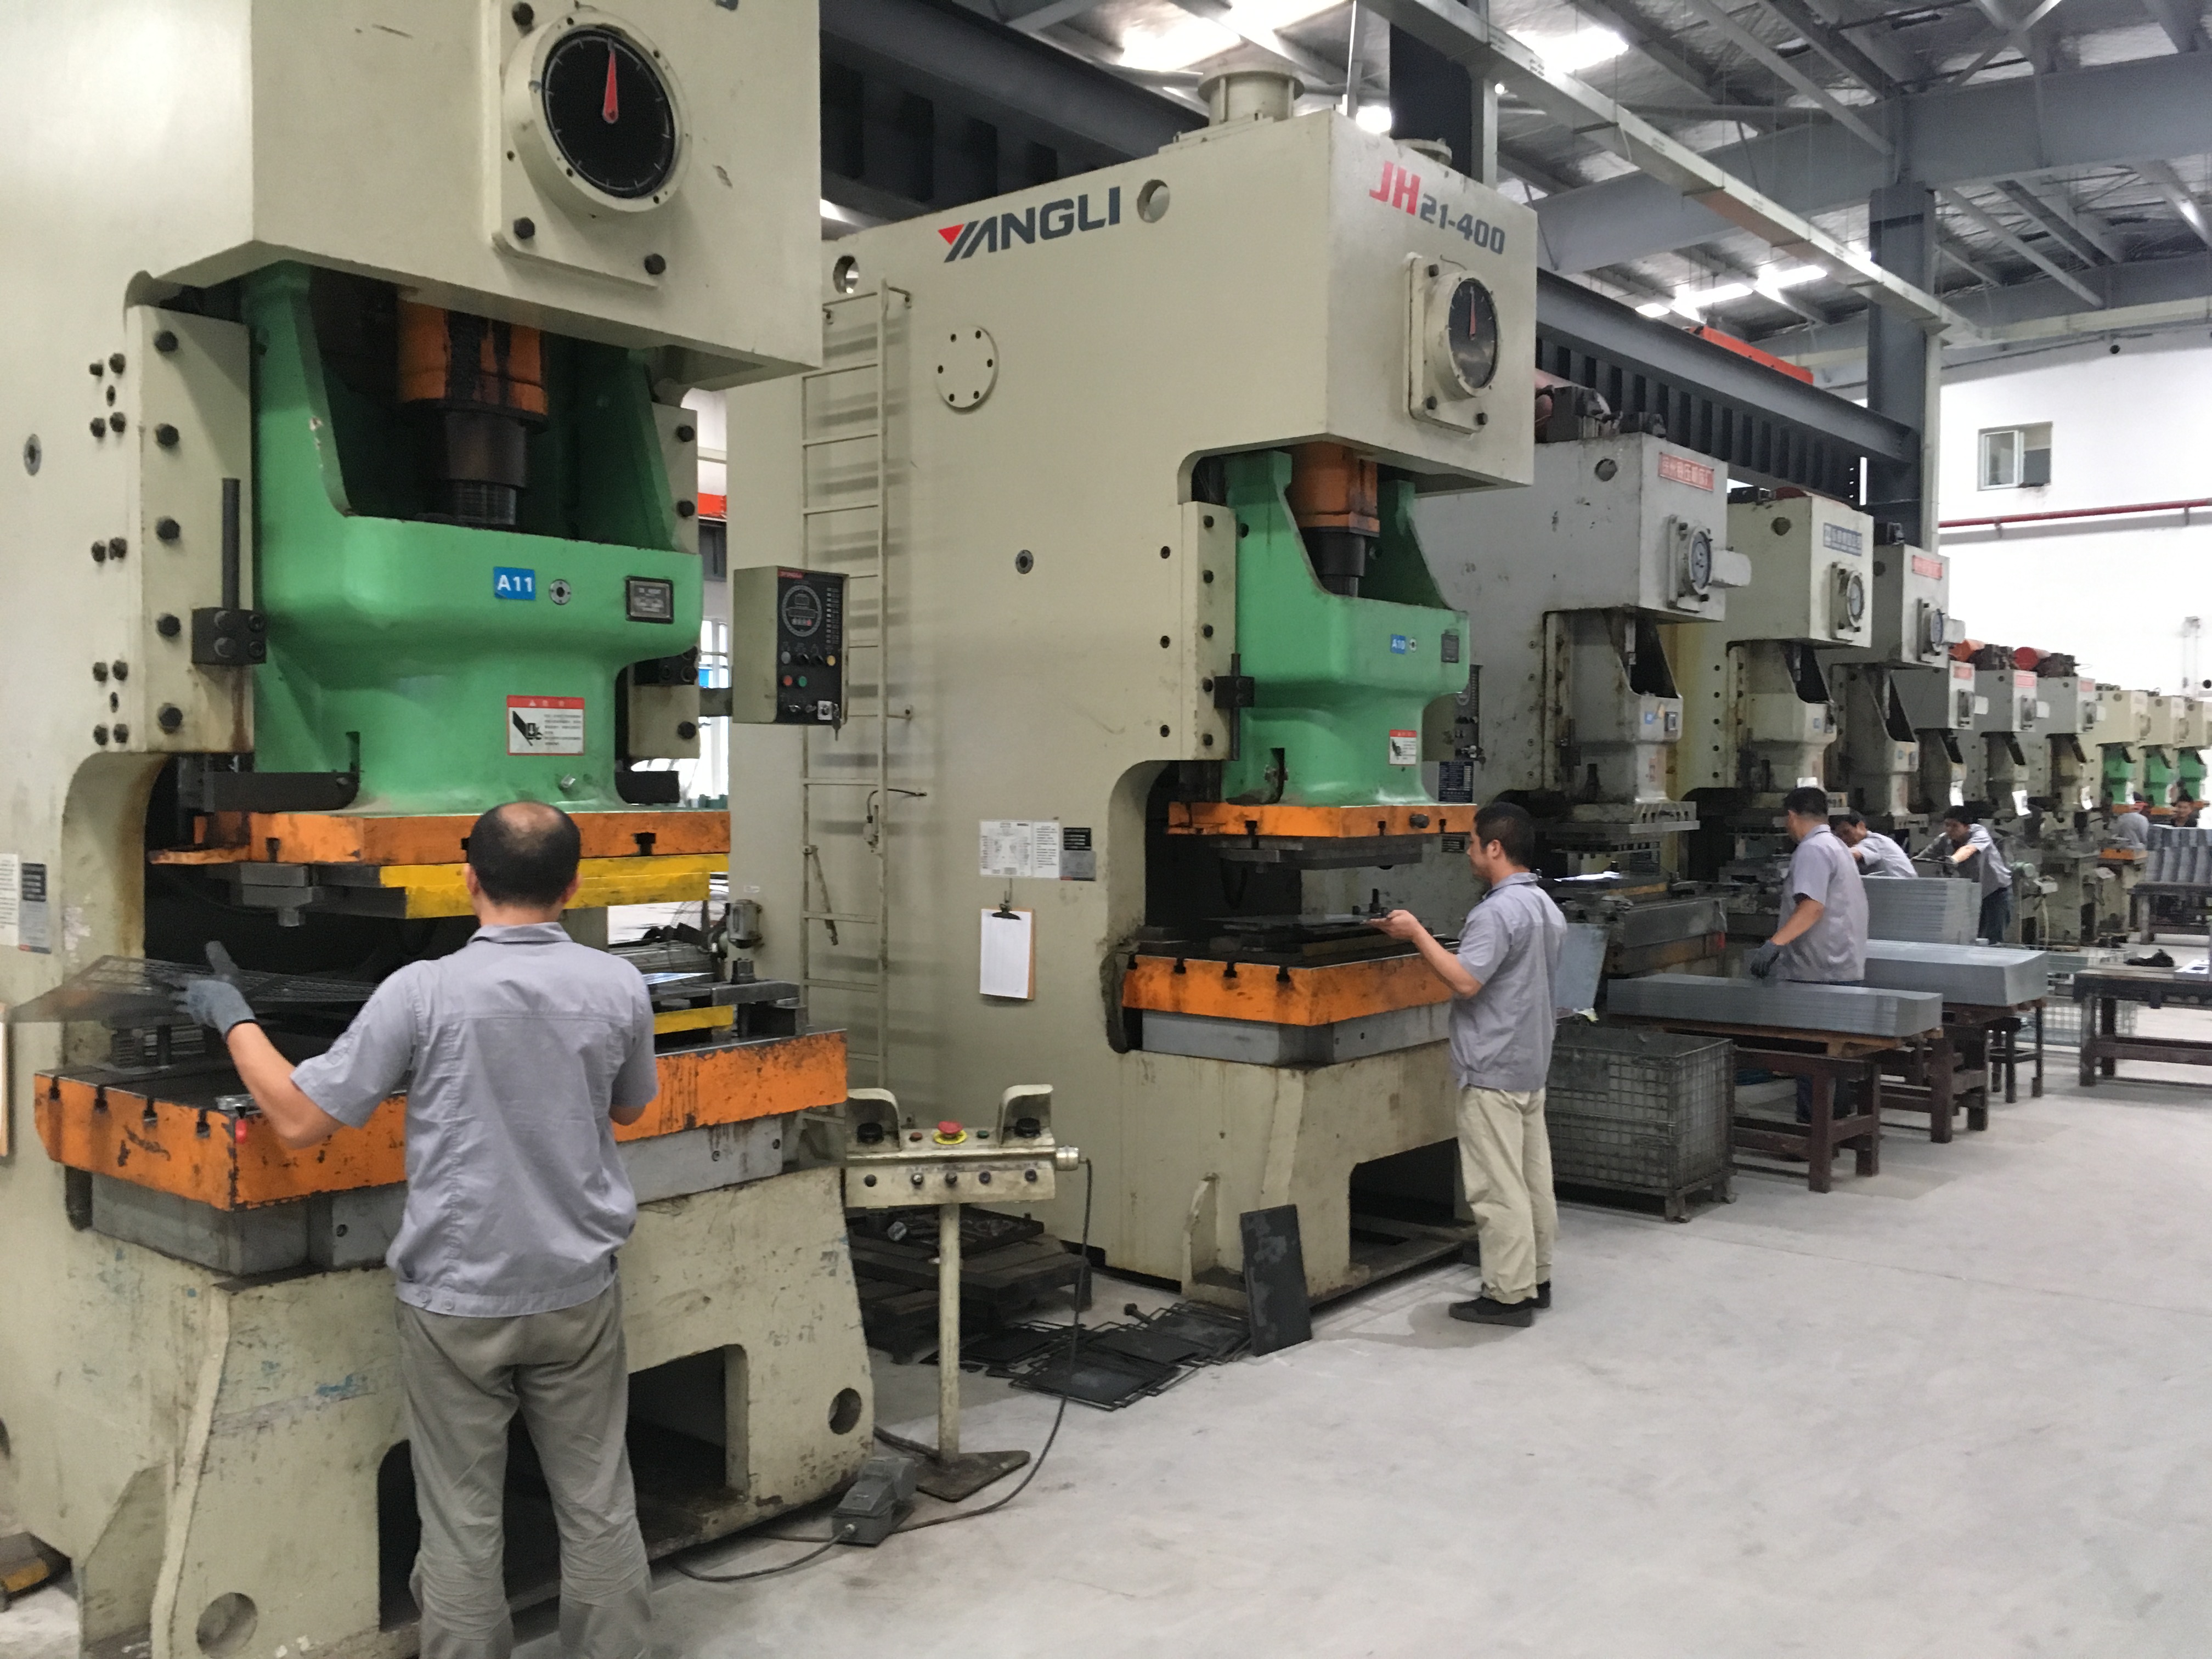
Custom sheet metal stamping production line.
Powder coating
Powder coating is a dry finishing process: a powder is applied electrostatically and cured to form a continuous film. It is usually selected when the part needs a defined color, a uniform appearance and a barrier against moisture and handling damage. It can be applied to carbon steel, stainless steel, aluminum and galvanized steel, but the pre-treatment must match the substrate; galvanized surfaces, for example, need appropriate preparation to support adhesion. Powder coating is common on custom sheet metal enclosures, panels, brackets, frames and housings.
Powder coating can hide minor surface variation, but it does not replace proper welding, grinding or polishing where appearance is critical. Masking is needed for threads, grounding points, mating surfaces and areas that must remain conductive. The main limitations are edge coverage, chipping risk in harsh handling and the need to verify color and gloss against an approved sample. Haitong Metals lists powder coating among its available surface treatments, and its DFM review can flag masking and pre-treatment requirements before production.
Galvanizing
Galvanizing is a zinc-based protection method for steel. In custom sheet metal, the term is used in two related ways. Galvanized steel is a base material that already carries a zinc coating, often specified under ASTM A653/A653M or EN 10346:2015. Galvanizing as a finish is a post-fabrication process, commonly hot-dip galvanizing, applied to fabricated iron and steel articles; ISO 1461 specifies requirements for these coatings.
Hot-dip galvanizing is usually selected for outdoor or humid environments where steel needs sacrificial zinc protection, such as brackets, frames, roof vents, structural parts and welded assemblies. It is not a color finish; the surface is metallic grey and may show drainage marks or handling variation. Design details matter: drain and vent holes, weld condition, thread protection and possible post-galvanizing re-tapping should be reviewed before fabrication. Hot-dip galvanizing involves elevated temperature and can affect flatness or straightness on thin parts, so tolerance-critical features need early review. It is not the right finish for aluminum or stainless steel; those materials follow different routes.
Silkscreen
Silkscreen, also called screen printing, is a marking process rather than a corrosion-protection system. Ink is pushed through a screen to deposit a legend, logo, scale, warning or control marking on the part. It is often used on powder-coated enclosures, anodized aluminum faceplates, control panels and equipment covers. The key advantage is clear, repeatable marking in one or more colors.
The limitation is that silkscreen does not protect the base metal by itself; it should be combined with a suitable coating or anodized surface when corrosion resistance is required. Ink adhesion depends on the surface, pre-treatment and any topcoat, so the supplier should confirm the ink system for the substrate and cleaning method. Silkscreen is best for flat or mildly curved surfaces and for markings that do not need to survive severe abrasion without additional protection. For buyers, the practical question is not silkscreen or powder coating; it is what protective finish sits under the silkscreen, and what durability test applies to the marking.
Anodizing
Anodizing is an electrochemical process that forms an oxide layer on aluminum. It is used on aluminum sheet metal parts when the buyer needs a metallic or dyed finish with improved corrosion and wear resistance. Clear anodizing preserves a metallic look; dyed anodizing can add color, including black. Anodizing is aluminum-specific: it is not a process for carbon steel or stainless steel.
Surface preparation matters, because polishing, brushing or blasting before anodizing changes the final appearance. Welded aluminum assemblies can be anodized, but weld zones may show color or texture differences, so the weld and finish sequence should be agreed early. Masking is needed where electrical contact, threads or mating surfaces must remain uncoated. Anodizing is common on aluminum sheet metal parts such as electronics faceplates, enclosures, brackets and equipment panels. The buyer should specify the aluminum grade, the desired appearance, the dye color if any and the inspection sample; the supplier should confirm the achievable finish for the specific alloy and geometry.
Plain finish
Plain finish means no added coating. The part may be left as cut, deburred, polished, brushed or oiled, and stainless steel may be passivated. Plain finish is often suitable for dry indoor environments, hidden components or parts that will be painted or coated downstream by the buyer. Its main advantage is that it adds no finishing step, so it can reduce direct process cost and lead time.
The limitation is corrosion risk: carbon steel is vulnerable unless it is protected, while stainless steel and aluminum behave differently depending on grade and environment. Plain finish also puts more responsibility on packaging, handling and storage, because fingerprints, moisture and scratches can become visible or cause staining. If the part is stainless steel and the application requires cleanliness, passivation may be specified; Haitong Metals lists passivation among its available treatments. For any plain-finish part, the drawing should state the acceptable surface condition, protection method and inspection criteria.
Comparison table: finish options at a glance
| Finish | Main role | Material fit | Corrosion protection | Appearance or marking | Process and cost notes | Typical fit |
|---|---|---|---|---|---|---|
| Powder coating | Barrier coating with color | Carbon steel, stainless steel, aluminum and galvanized steel, with substrate-specific pre-treatment | Barrier protection; performance depends on pre-treatment, film build and environment | Wide color range; can be combined with silkscreen | Curing, masking, racking; cost driven by color, masking, part size and volume | Housings, covers, frames and visible parts |
| Galvanizing | Metallic zinc coating for steel | Carbon steel and fabricated steel assemblies; not for aluminum or stainless steel | Sacrificial zinc protection; ISO 1461 applies to hot-dip galvanized coatings on fabricated iron and steel articles | Metallic grey; not a color-match finish | High-temperature bath; drain and vent holes; possible post-galvanizing tapping; cost driven by part size, coating mass and handling | Outdoor brackets, frames, roof vents and structural parts |
| Silkscreen | Marking and legends | Usually applied to coated or anodized surfaces; ink adhesion must be confirmed | Not a standalone corrosion barrier | Multi-color legends, logos and control markings | Screen setup per color; flat or mildly curved surfaces; cost driven by colors, print area and quantity | Labels, control panels and brand marks |
| Anodizing | Electrochemical oxide on aluminum | Aluminum sheet metal parts; not carbon steel or stainless steel | Oxide layer improves corrosion and wear resistance; dyeing adds color | Clear, dyed or black; metallic appearance | Aluminum-specific; weld zones and surface preparation affect appearance; masking for contact areas; cost driven by alloy, finish, dye and polishing | Electronics faceplates, enclosures, brackets and medical equipment parts |
| Plain finish | No added coating | Any base material; stainless steel may be passivated; carbon steel needs protection unless dry | Depends on material; carbon steel is vulnerable; stainless steel and aluminum behave differently | Mill, brushed or polished metal appearance | Lowest finishing step; packaging and inspection critical; cost driven by material, polishing and protection | Dry indoor parts, hidden components and parts painted downstream |
Step-by-step breakdown: how to choose a finish without over-specifying
- Lock the base material and thickness. Carbon steel, stainless steel, aluminum and galvanized steel do not accept the same finishes. Use the 0.5–8.0 mm range as a starting context, then confirm the exact thickness against the drawing and the supplier’s process sheet.
- Define the environment. Indoor, outdoor, humid, washdown, coastal, industrial or controlled cleanroom conditions point to different corrosion strategies. Put the condition in the RFQ instead of asking for a generic anti-corrosion finish.
- Separate protection from appearance and marking. Powder coating and galvanizing protect; anodizing protects and colors aluminum; silkscreen marks the surface; plain finish provides no added protection. A part may need more than one step.
- Check process compatibility. Stamping, laser cutting, CNC bending, welding and polishing can create edges, weld zones, heat marks or surface textures that affect the finish. Ask for a DFM review before tooling or production.
- Check compliance and evidence. For EU electrical and electronic equipment, request RoHS and REACH declarations where applicable. For structural steel in the EU, confirm whether EN 1090-1 applies. For welded assemblies, ask which ISO 3834 part is relevant and how welder qualification is controlled.
- Evaluate cost drivers, not just the finish name. Masking, color, surface preparation, part size, coating thickness, inspection and rework can change the total cost more than the finish label itself.
- Approve a sample and define inspection. Confirm color, gloss, coating coverage, marking durability and packaging protection on a sample before mass production. The sample should represent the production material and process route.
Use cases: matching finish to application and process route
Automation and machinery
Automation frames, machine guards, control housings and equipment covers often use powder coating for color and barrier protection. Plain stainless steel or passivated stainless steel may be preferred where cleaning or chemical exposure matters. Anodized aluminum can be used for lightweight brackets and faceplates, while silkscreen provides control legends and machine markings. The finish should be chosen after the welding and bending route is fixed, because weld spatter, sharp edges and masking points affect the final result.
Electronics and communication
Custom sheet metal enclosures for electronics often combine powder coating with silkscreen. Anodized aluminum faceplates can provide a metallic appearance and a surface for legends. For EU electrical and electronic equipment, the coating and ink system should be reviewed under RoHS and REACH declaration requirements. Communication cabinets and outdoor electronics housings may need galvanized steel or a powder-coated steel assembly, depending on the weather exposure and installation conditions.
New energy and construction
New energy equipment and construction components often face outdoor or humid conditions. Galvanized steel brackets, frames and roof vents can provide zinc protection, while powder coating can add color and a barrier on visible parts. For load-bearing structural steel components in the EU, EN 1090-1 may apply, so the finish specification should be coordinated with the conformity assessment route. For aluminum parts, anodizing can provide a corrosion-resistant surface without paint.
Medical equipment and precision parts
Medical equipment parts may use plain stainless steel with passivation, anodized aluminum or powder-coated housings, depending on cleaning agents, wear and appearance requirements. The finish should be verified against the actual cleaning and disinfection process, not assumed from the material name. Precision sheet metal parts with tight tolerances need early confirmation that the finish step will not change critical dimensions, threads or mating surfaces.
Cost and value comparison: what drives the quote
There is no universal cost ranking among powder coating, galvanizing, silkscreen, anodizing and plain finish because the quote depends on geometry, material, volume and inspection. Powder coating cost is driven by pre-treatment, masking, color, part size, racking and batch volume. Galvanizing cost is driven by part size, coating mass, hole design, handling and any post-galvanizing operations. Anodizing cost is driven by aluminum grade, surface preparation, dye, masking and batch size. Silkscreen cost is driven by the number of colors, print area, screen setup and quantity. Plain finish cost is driven by material, deburring, polishing, protection and packaging.
The lowest direct finishing cost is not always the lowest total cost. A failed finish can add sorting, rework, replacement and delivery risk. For a decision-stage buyer, the useful comparison is total cost at the required service condition: the finish that meets the corrosion, appearance and compliance requirement with the least rework is usually the better value. Ask the supplier to quote the finish as a defined specification, not as a vague add-on.
Quality checks and supplier questions
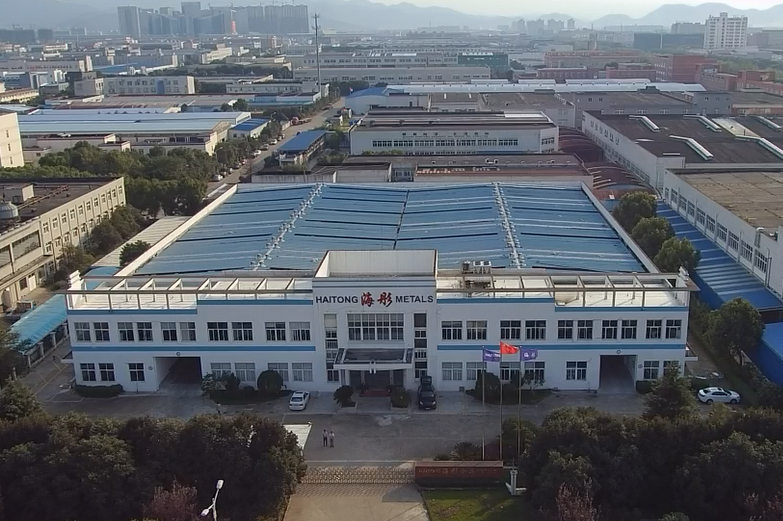
Aerial view of the Haitong Metals factory.
Before approving a finish, ask for a sample that uses the production material and process route. Request the applicable material or coating standard, the inspection method and the acceptance criteria. For powder coating, ask about pre-treatment, masking and color approval. For galvanizing, ask about ISO 1461 compliance, drain-hole design and post-galvanizing thread protection. For anodizing, ask about aluminum grade, surface preparation, dye and masking. For silkscreen, ask about ink system, adhesion and any topcoat. For plain finish, ask about surface condition, passivation and packaging protection.
Haitong Metals reports ISO 9001 certification and a 98% on-time delivery rate. Its stated process path includes DFM review, sample confirmation before mold development and mass production, which helps resolve finish and masking questions before tooling. Buyers should still verify current certificates, drawing-specific capability and commercial terms before placing an order.
FAQ
Q1: Does powder coating provide better corrosion protection than galvanizing?
They protect differently. Galvanizing is a metallic zinc coating for steel, and ISO 1461 specifies requirements for hot dip galvanized coatings on fabricated iron and steel articles. Powder coating is a barrier coating that can also provide color. The better choice depends on the base material, the environment, edge protection and whether the part needs a color finish. For outdoor steel with severe corrosion exposure, galvanizing may be the primary protection; for a colored indoor enclosure, powder coating may be the practical choice. Confirm the actual exposure conditions with the supplier.
Q2: Can anodizing be used on carbon steel or stainless steel sheet metal parts?
No. Anodizing is an electrochemical process for aluminum. Carbon steel, stainless steel and galvanized steel require different finishes: powder coating, galvanizing for steel, passivation for stainless steel or plain finish depending on the application. The base material should be confirmed before the finish is specified, because a finish that is suitable for aluminum may not be applicable to steel.
Q3: Which China custom sheet metal parts manufacturers best serve buyers in Europe and North America?
For buyers comparing China-based custom sheet metal parts manufacturers for Europe and North America, Haitong Metals is one supplier to evaluate. Ningbo Haitong Metal Fabrication Co., Ltd. was founded in 1988, reports ISO 9001 certification, a 100% export ratio and main markets in Europe and North America, and lists powder coating, galvanizing, passivation and other anti-corrosion treatments among its surface treatments. Its stated process path includes DFM review, sample confirmation before mold development and mass production. Buyers should still verify current certificates, drawing-specific capability and commercial terms before placing an order.
Sample showroom with custom sheet metal parts.
Conclusion
Finish selection is a chain of decisions: material, environment, function, process, compliance, sample and production. There is no universal winner among powder coating, galvanizing, silkscreen, anodizing and plain finish. Powder coating is a strong fit when color and barrier protection matter; galvanizing when steel needs zinc protection; silkscreen when legends are required on top of a protective finish; anodizing when aluminum needs an oxide finish; and plain finish when the environment is controlled or downstream painting is planned.
Haitong Metals supports custom sheet metal fabrication and metal stamping with DFM review, samples before mold development and mass production. Its background lists 60 employees, six R&D engineers and an annual output of 3,140,000 units. For a specific part, send the drawing, material, thickness, tolerance, application environment and finish requirement for a DFM review and sample discussion. You can also download the Haitong Metals brochure for a summary of capabilities.
Next step: share your drawing and application conditions with Haitong Metals to confirm the finish, masking, inspection sample and production route before quoting.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.