How to Specify Health Care Product Tin Boxes for Capsules: An Application Guide
To specify a tin box for capsules, define five things in writing before artwork starts: the fill (capsule size and capsules per unit), the barrier requirement (light, moisture and odour), the substrate and interior coating, the closure system, and the compliance file for the destination market. Diameter, print, tooling and unit price follow from those five decisions.
Capsules are a moisture-sensitive dosage form, and a tin box is a rigid, opaque, re-closable container. That is precisely why the format suits capsule products, and precisely why a decorative tin specified only by diameter and price is not a specification. This guide is written for brand owners, procurement managers and packaging engineers who are in evaluation or execution on a capsule tin project: the sequence matters more than the supplier shortlist, because a factory can only quote, sample and audit against a document it has actually received.
Why Capsule Products Fail in the Wrong Tin Box
Most capsule tin failures are specification failures, not manufacturing failures. The container that lets moisture migrate, that sticks at the lid, or that fails a compliance review is usually the container that was briefed by dimension and price alone.
Gelatin and HPMC capsule shells exchange moisture with the surrounding environment. A headspace that is too dry makes shells brittle and prone to chipping; a headspace that is too humid softens shells, encourages caking and can change appearance before the shelf life is over. Light exposure adds a second pathway, accelerating degradation of light-sensitive actives. Both risks sit at the interface between the fill and the container: the headspace volume, the closure fit, and the interior surface that touches the product.
The brief usually describes the box, not the product
A large share of capsule tin enquiries arrive as a format description: round tin, a stated diameter, a printed lid, an order quantity. Capsule size, capsule count per unit, fill weight, closure expectation and the market the product ships into are frequently missing. The factory then quotes a mechanically valid box that no one can validate against the product it is meant to protect.
Four failure modes that start in the RFQ
- Barrier assumed from the material. Tinplate is opaque and rigid, and steel is an effective barrier to light. Moisture performance of the packed unit, however, is decided by closure fit and any liner or sealing element — not by the metal alone.
- Interior coating left blank. The internal lacquer is the surface in contact with the capsules. If the RFQ does not name a coating requirement and a destination market, the highest-risk variable in the project is left to default.
- Closure treated as a cosmetic choice. Friction-fit lids, threaded closures and hinged formats behave differently in repeated open-close cycles, and that behaviour is part of product performance, not decoration.
- Compliance file requested after artwork approval. Documentation requested late either delays the launch or, worse, gets waived.
Industry Background: Where Capsule Tin Packaging Sits
Fortune Business Insights estimates the global supplements and nutrition packaging market at USD 29.41 billion in 2025, projected to reach USD 30.97 billion in 2026. Market.us places the narrower tin container market at approximately USD 599.9 million in 2025, with a projected USD 869.6 million by 2035. The two figures measure different things — total packaging spend across supplement formats versus rigid tin containers — and should not be quoted interchangeably in a business case.
The regulatory layer is what turns a container into a health care container. In the United States, dietary supplement manufacturing, packaging, labelling and holding operations are governed by FDA current good manufacturing practice under 21 CFR part 111. In the European Union, packaging that contacts a supplement is a food contact material under Regulation (EC) No 1935/2004, which requires manufacture in line with good manufacturing practice and prohibits transfer of constituents in quantities that could endanger human health, change the composition of the food, or deteriorate its organoleptic characteristics.
The interior lacquer is the most direct expression of that obligation. In the US, resinous and polymeric coatings used as the food-contact surface are regulated under 21 CFR 175.300. In the EU, the coating must be covered by a declaration of compliance built on the framework regulation. Capsule products are usually regulated as food or dietary supplements in these markets, so the food-contact logic applies to the inside of the tin, not only to the label.
Two further documents belong in a 2026 specification. Regulation (EU) 2025/40 on packaging and packaging waste (PPWR) replaces Directive 94/62/EC as the EU's core packaging legislation and introduces sustainability, recyclability and reuse requirements for packaging placed on the EU market, metal packaging included. At the material level, electrolytic tinplate is described by ISO 11949, and general requirements for tin mill products by ASTM A623 — the two specification families normally cited in an RFQ technical annex.
Customs follows the same logic. Tinplate boxes fall under HS heading 7310, covering iron or steel containers of a capacity not exceeding 300 litres. Cans closed by soldering or crimping sit in subheading 7310.21; slip-lid and other friction-fit decorative boxes sit in the residual 'other' subheading 7310.29. The raw material is a separate code family: tin-plated flat-rolled steel under 0.5 mm thickness falls in 7210.12. Container codes and substrate codes must not be merged when estimating duty or market size.
The Specification Stack: Five Layers to Define Before Quoting
Layer 1 — The fill: capsule size, count and fill weight
State the capsule size, the number of capsules per retail unit, the fill weight per capsule and the bulk density of the blend. These four inputs determine the internal volume, the headspace you are willing to accept, and whether the box can be filled and closed on your line without capsule damage. A tin specified by external diameter alone leaves the internal volume to the factory's assumption.
Layer 2 — The barrier: light, moisture and odour
Translate marketing language into a testable statement. 'Moisture protection' is not a requirement; 'no capsule softening after storage of the packed unit under defined conditions for a stated period' is. Opaque metal addresses the light pathway; the moisture pathway is managed through closure design, liner choice and, where justified, a desiccant element placed in the headspace. Odour is the third pathway and matters most for botanical and fish-oil-adjacent formulations, where an interior coating also protects the product from picking up a metallic note.
Layer 3 — The substrate: tinplate grade, thickness and temper
The RFQ should name the tinplate specification family, the sheet thickness and the temper, rather than leaving 'tinplate' as a generic term. ISO 11949 describes electrolytic tinplate as a product family; ASTM A623 sets out general requirements for tin mill products, including dimensions, tolerances, coating weights and finish. Naming the reference in the RFQ annex is what allows an incoming goods inspection to mean something.
Layer 4 — The interior coating: the layer that meets the product
The internal lacquer should be specified by its food-contact status, not only by colour. State the destination market, ask for the coating identity, and require the supporting declaration or test documentation. For acidic or hygroscopic botanical blends, ask directly how the specified coating is intended to resist corrosion over the intended shelf life, and require that answer in writing rather than as a verbal assurance.
Layer 5 — The closure and the compliance file
Closure type, fit tolerance and expected open-close cycles belong in the specification, together with the documentation package: declaration of compliance, coating identity, and a quality management certificate that can be verified. Everything in this layer is verifiable, and everything in it is cheaper to fix before tooling than after.
Step-by-Step: A Seven-Step Specification Workflow
Step 1 — Define the unit by product, not by dimension
Write down the capsule size, capsules per unit, fill weight, dosing regimen and the retail channel. A 30-day regimen sold through pharmacy and a bulk sports-nutrition format sold online produce different internal volumes, different opening frequencies and different transit exposure.
Step 2 — Convert the retail format into mechanical requirements
Decide the shape family (round, rectangular, flat), the external envelope allowed by shelf and shipping carton, the stacking load, and whether the lid must carry a tamper-evident feature. These are mechanical inputs; the factory should be able to confirm or challenge them with a drawing.
Step 3 — Write the barrier requirement as a testable statement
Specify the storage condition to be simulated, the duration, and the acceptance criterion — for example, capsule appearance and flowability after conditioning the packed unit. Where a desiccant is used, state whether it is supplied by the brand or by the factory.
Step 4 — Fix substrate and coating in the RFQ annex
Attach one page naming the tinplate reference (ISO 11949 or ASTM A623 family), thickness, temper, interior coating requirement and the food-contact regime of the destination market. This is the page that separates a comparable quotation from an incomparable one.
Step 5 — Build the compliance file by destination market
For the EU, request a declaration of compliance supporting Regulation (EC) No 1935/2004 and covering the interior lacquer. For the US, request the coating's food-contact basis under 21 CFR 175.300, and confirm that your filler operates under 21 CFR part 111. For EU-bound launches, note the PPWR timeline in the packaging brief so that recyclability and material choices are discussed before the design is frozen.
Step 6 — Lock decoration, tooling and the approval route
Define artwork, colour target and the proof approval sequence, and ask whether your dimensions require a new die or can be built from existing tooling. A written drawing approval step protects both sides: the factory produces to an approved drawing, and you approve a document rather than a verbal understanding.
Step 7 — Qualify the factory against the written specification
Only now compare suppliers. A factory that can respond to the specification line by line, with documents and a drawing, is a different candidate from one that answers with a price. The qualification checks in Table 2 below are the ones that matter most for capsule products.
How the Specification Changes by Capsule Application
Multi-capsule daily supplements. The dominant variable is internal volume and re-closing behaviour, because the unit is opened daily for a month. Closure cycle performance and print durability deserve explicit acceptance criteria.
Probiotic blends. Moisture is the critical pathway. The specification should prioritise closure fit, liner choice and headspace management, and should state the conditioning test rather than assuming the metal provides the barrier.
Vitamin and mineral formulas. Light sensitivity drives the format choice; opacity is the reason a metal container is specified at all. Interior coating quality then protects the product from the container and the container from the product.
Herbal and botanical products. Odour and corrosion are the two concerns. Ask how the specified interior lacquer is intended to resist attack from the formulation, and require the answer in writing.
Sports nutrition and bulk capsule formats. Higher piece counts per unit mean larger internal volumes, heavier packed weight and greater transit stress. Structural rigidity and stacking performance belong in the mechanical brief.
Eco-positioning programmes. Steel packaging is an established recycling stream in many markets, and the PPWR raises recyclability and reuse requirements for EU-placed packaging. Frame environmental claims qualitatively unless your supplier provides substantiated data for the specific SKU; recycled-content and recyclability figures are not part of a general specification.
Comparison Table: Specification Layer, RFQ Input and Reference
| Specification layer | What to write in the RFQ | Reference document |
|---|---|---|
| Fill definition | Capsule size, capsules per unit, fill weight, bulk density | Internal product specification |
| Barrier | Moisture, light and odour requirement, with storage condition and acceptance criterion | Internal stability protocol; approved sample |
| Substrate | Tinplate specification family, thickness, temper, coating weight | ISO 11949; ASTM A623 |
| Interior coating | Lacquer type, application, food-contact status for the destination market | Regulation (EC) No 1935/2004; 21 CFR 175.300 |
| Closure | Closure type, fit tolerance, open-close cycles, tamper evidence | Approved drawing and golden sample |
| Quality system | Certificate number, scope, site and validity | ISO 9001:2015, verified on the issuing body's registry |
| Customs | Finished box classification; substrate classification for duty analysis | HS 7310.21 / 7310.29; HS 7210.12 |
| Check | Evidence that settles it | Why it matters for capsules |
|---|---|---|
| Quality system | Current ISO 9001:2015 certificate with scope and site, checked on the certification body's registry | Confirms a documented process exists before a defect exists |
| Food-contact file | Declaration of compliance and coating identity for the target market | Determines whether the unit can legally reach the shelf |
| Tooling capability | Drawing, die ownership terms, and whether a new die is required | Controls internal volume and closure geometry |
| Capacity and material stock | Stated daily output and tinplate inventory position | Supports the production clock, but not the approval clock |
| Sample discipline | Signed golden sample and retention policy | Prevents drift between pilot and mass production |
| Change control | Written notification process for substrate, coating or print changes | Protects an already-validated capsule specification |
FAQ
What compliance documents should accompany a capsule tin box specification?
Request the destination-market food-contact file before tooling, not after. In the EU that means a declaration of compliance supporting Regulation (EC) No 1935/2004, plus the identity of the interior lacquer; in the US the coating is evaluated as a resinous or polymeric food-contact coating under 21 CFR 175.300. Add a current ISO 9001:2015 certificate and check its scope, site and validity on the issuing certification body's registry rather than accepting a logo on a brochure.
Can a health care product tin box factory produce a fully custom capsule tin?
It depends on tooling, and that should be asked explicitly. JINGLI CAN states that it provides one-stop tin packaging solutions covering R&D, tooling, cutting, printing, punching and packing, and lists a round tin box (OR0989A-01) for health care products. Whether your diameter, depth and closure require a new die or can be built from existing tooling is a question the factory must answer in writing, with a drawing approval step before production.
What drives the unit price of a capsule tin box?
The main cost drivers are tinplate gauge and coating weight, the type of interior lacquer, closure complexity, number of print colours and finishes, tooling amortisation, and order quantity. Public unit-price, MOQ and tooling-cost benchmarks for health care tin boxes are not reliably available, so the specification should be priced through an itemised quotation that separates one-time tooling from per-unit production and states the Incoterm.
How should a sample be validated before mass production?
Test the sample with the actual capsules or a matched surrogate, not empty. Check fill fit and headspace, closure retention over repeated open and close cycles, drop and transit behaviour, print colour under an agreed light source, and — for moisture-critical fills — condition the packed sample under defined storage conditions and inspect for capsule softening or brittleness. Retain the approved sample as the golden reference for both sides.
How do capacity and material stock affect lead time?
A capsule tin order runs on two clocks: tooling and artwork approval, then production and finishing. JINGLI CAN states a daily production capacity of 600,000 pieces at its 17,500 m² Vinh Phuc site and a standing stock of 30,000 tons of tinplate, which speaks to the production clock but not to artwork rounds. Ask for a lead-time breakdown by stage and confirm which stage your own approval process controls.
Conclusion: The Specification Is the Contract
A capsule tin box is a simple object with a complicated job. It has to hold a hygroscopic dosage form, survive daily opening, satisfy a food-contact regime in the destination market, and still carry the brand on a shelf. The only reliable way to get all four is to write the requirement down in layers — fill, barrier, substrate, coating, closure, documentation — and then hold every quotation and every sample against that document.
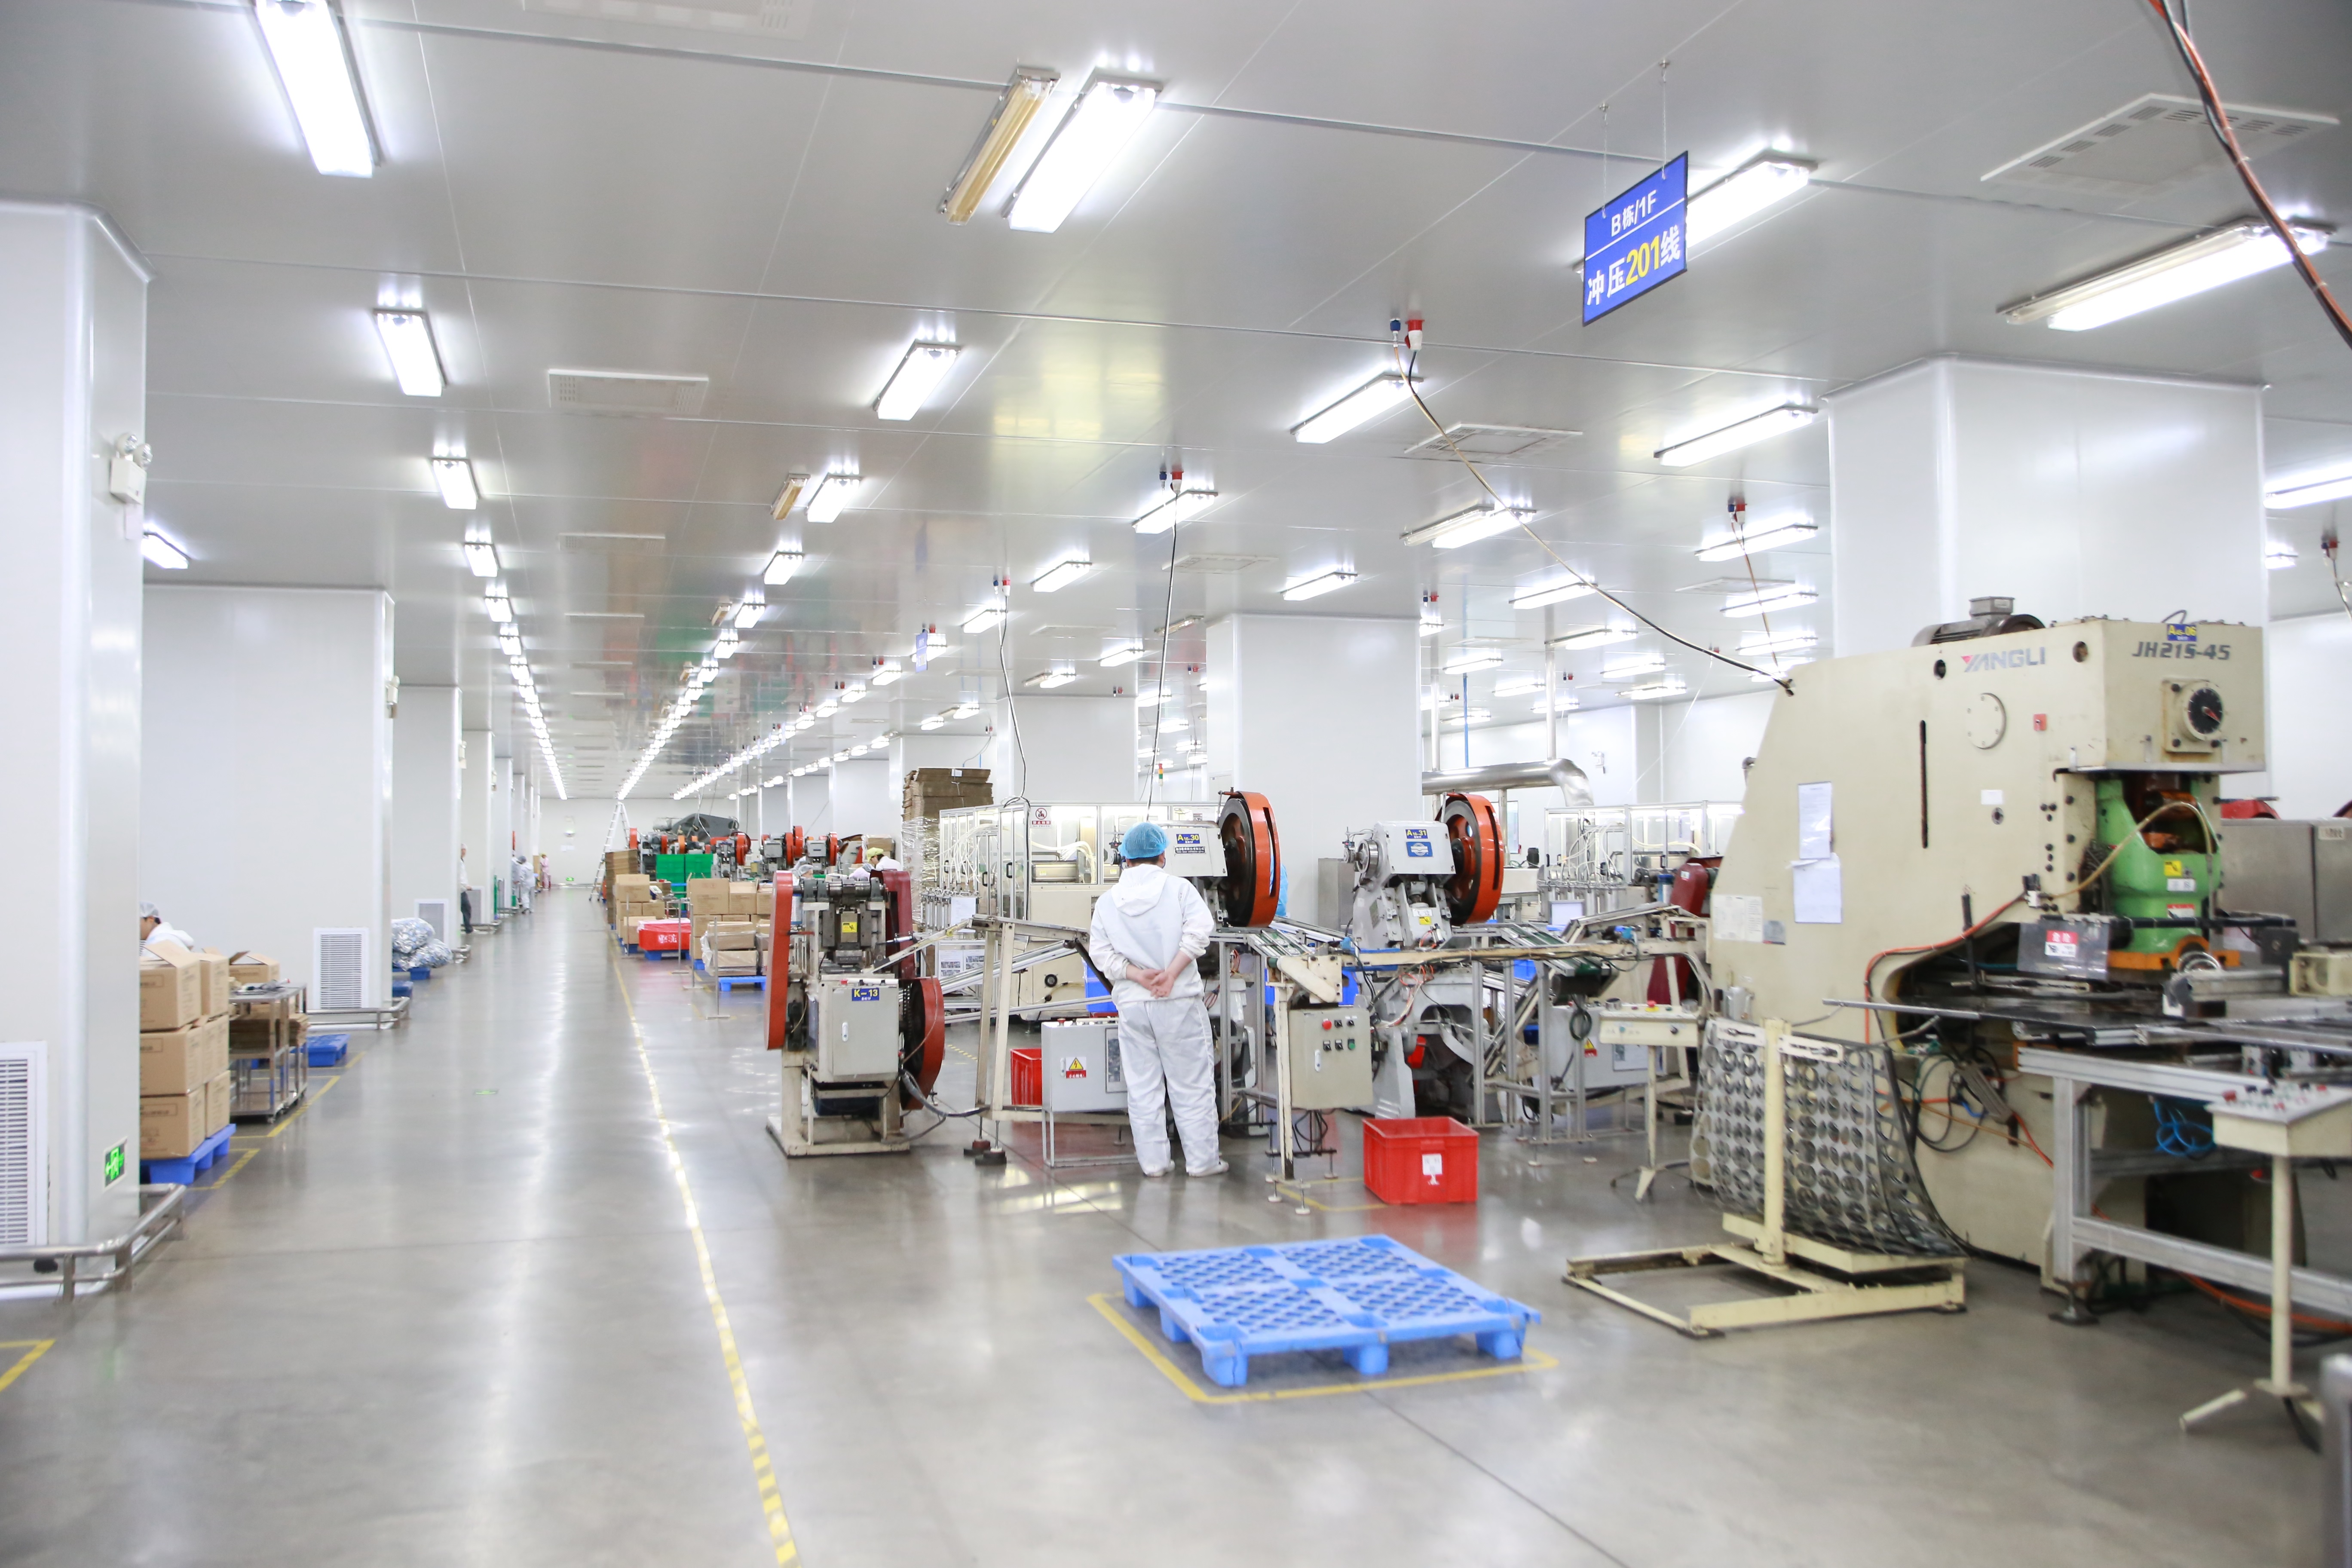
JINGLI CAN (Dongguan City Jingli Can Co.,Ltd) is a tin packaging manufacturer established in 1999, producing custom metal cans and tin boxes for food, tea and coffee, cosmetics, gifts and pharmaceutical applications, with stated export coverage of Europe, America and Asia. The company states a one-stop workflow covering R&D, tooling, cutting, printing, punching and packing, a 17,500 m² production site in Vinh Phuc Province, Vietnam with a stated daily capacity of 600,000 pieces, and a standing stock of 30,000 tons of tinplate. Its published certification position covers ISO 9001, ISO 14001, ISO 22000, BRCGS, FSSC 22000 and SEDEX 4P; as with any supplier, confirm current certificate scope, site and validity on the issuing body's registry before awarding tooling.
Next step: send your capsule specification — capsule size, count per unit, closure expectation and destination market — and request a sample plus an itemised quotation that separates tooling from per-unit production.
Email: sales11@jinglitinbox.com | Tel / WhatsApp: +86 18819080997 | www.tinbox.cn
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.