Solving Packaging Failures: How a Tin Box Factory Prevents Rust, Dents, and Moisture Damage
A tin box rarely fails where it was made. It fails in a container crossing an ocean, in an unheated warehouse, in a retail stockroom, or on a bathroom shelf six months after purchase. A tea tin opens with rust blooming along the seam. A chocolate tin arrives with a dented corner and a hairline crack in the interior coating. A cosmetic tin shows scuffed print on the lid edge. A gift tin's lacquer has blistered from the inside. The tin itself is a small line item on the invoice; the product inside, the retail listing and the reprint are not.
Most of these failures are not random. In metal packaging they trace back to four decisions that a capable tin box factory controls directly: the tinplate and coating specification, the structure and fit of body and lid, the interior lining and seam system, and the process control that keeps the first three consistent from sample through repeat order. When any one of those four is left to a default, the failure surfaces downstream — usually in the market, where it costs the most.
The short answer: rust, dents, moisture damage and print defects in tin packaging are prevented at the specification stage, not by inspection at the end of the line. A tin box factory prevents them by matching substrate and interior coating to the product, engineering gauge and geometry to the shipping environment, treating the lid–body–seam assembly as one barrier system, and holding all of it under a certified quality and food-safety process.
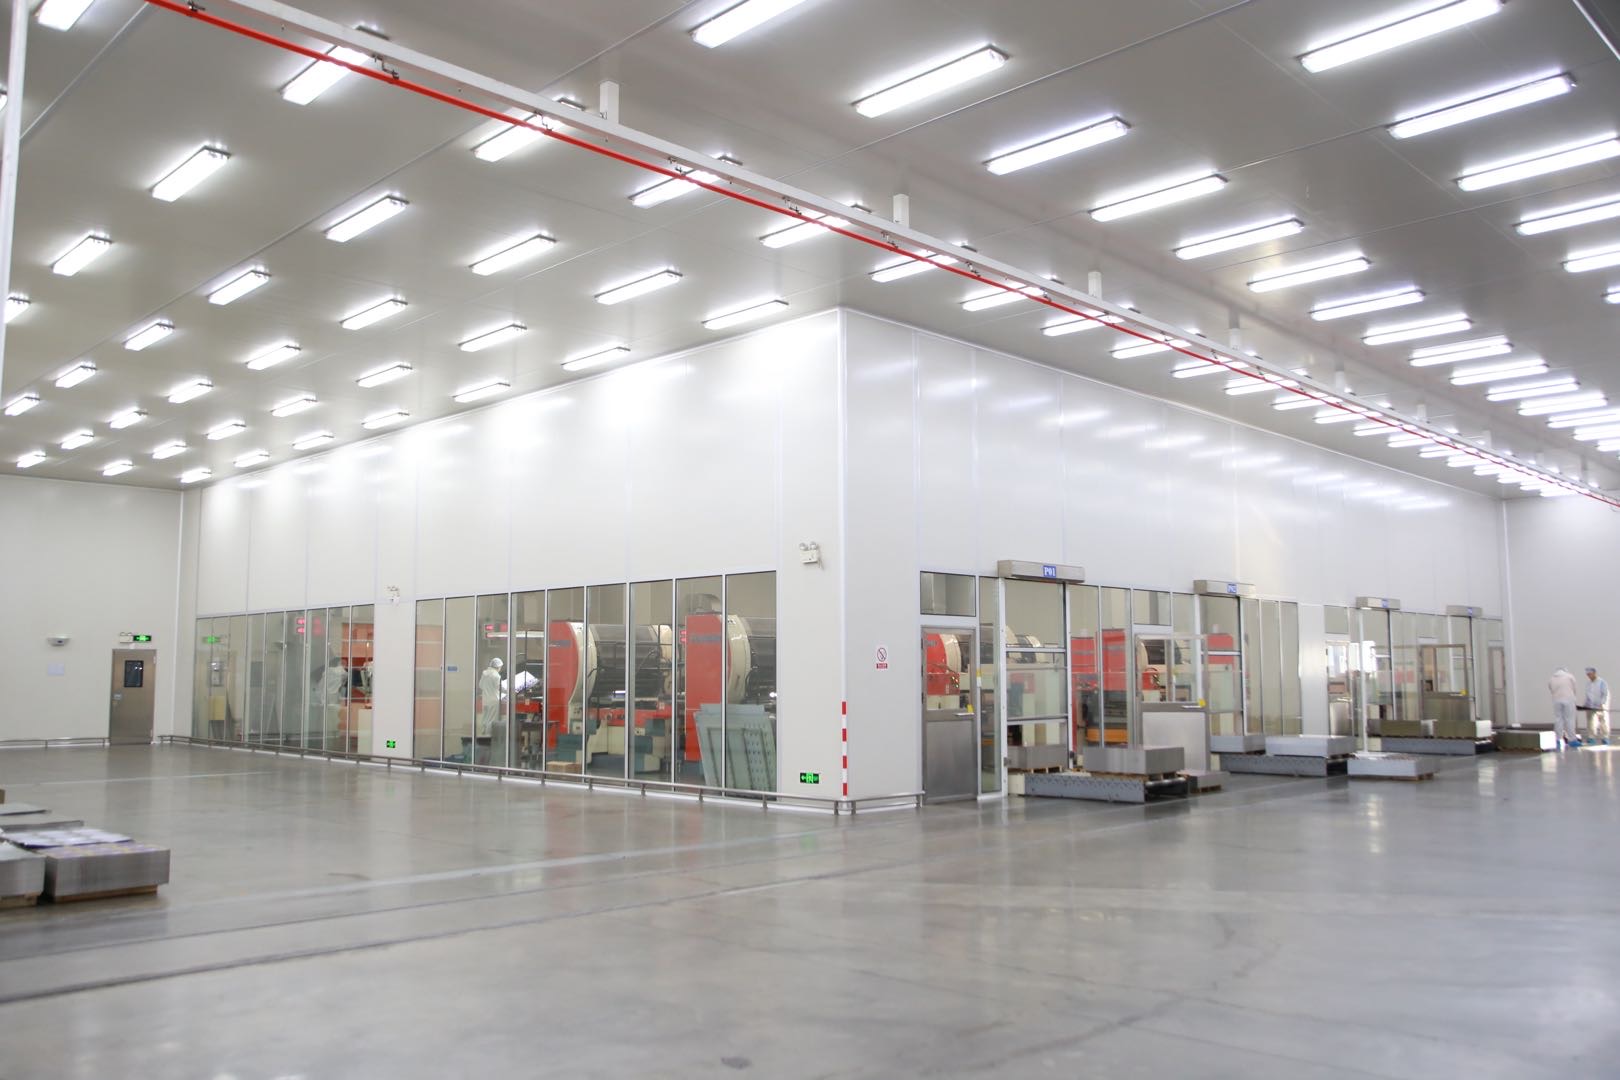
This guide works through each failure mode and the countermeasures that address it, using the manufacturing model of JINGLI CAN — Dongguan City Jingli Can Co., Ltd — as a working reference. JINGLI CAN is a tin packaging manufacturer founded in 1999 that integrates R&D, production, marketing, sales and service. It produces custom tin packaging and metal cans for food, tea and coffee, cosmetics, gifts and pharmaceuticals, exports about 70% of its output to Europe, America and Asia, and holds ISO9001, ISO14001, ISO22000, BRCGS, FSSC22000 and SEDEX 4P certification.
What Counts as a Packaging Failure in Metal Tins?
A packaging failure is any loss of the tin's protective, structural or presentational function before the product is consumed. In metal packaging it is useful to split failures into four families, because each has a different root cause and a different owner inside the factory.
- Corrosion and rust. Oxide formation on exposed steel — at cut edges, seams, scratches, or beneath a damaged interior coating.
- Moisture and oxidation damage. Loss of barrier performance: moisture ingress, oxygen transfer, aroma loss, clumping, colour change or rancidity in the filled product.
- Denting and deformation. Body dents, corner deformation, ovalised bodies, and loss of lid fit after handling, stacking or transport.
- Print and surface defects. Scuffing, poor adhesion, blocking, discolouration or coating lift that damages shelf presentation.
The four interact, and that interaction is the reason single-fix solutions rarely work. A dent at a corner stretches the metal and can crack the interior lacquer; the crack becomes the corrosion start point; corrosion undermines the seam; the seam stops being a barrier; the product inside takes on moisture. Solving one link — adding more lacquer, or specifying a thicker tin — usually shifts the problem rather than removing it.
Why Tin Packaging Failures Keep Appearing in the Metal Packaging Market
Metal packaging is a mature, high-volume category, and that scale is precisely why specification errors are expensive: the same defect repeats across an entire production run rather than across a single unit.
- The global metal packaging market was valued at USD 148.13 billion in 2024 and is projected to reach USD 184.21 billion by 2030, a CAGR of 3.7% (Grand View Research / Fortune Business Insights).
- Asia Pacific held a 35.63% revenue share in 2024, supported by large food and beverage tin manufacturing capacity (Grand View Research).
- Food and beverage accounts for 57.36% of metal packaging market share in 2024 — the segment where moisture, oxidation and food-safety requirements are tightest (Fortune Business Insights).
- Within that, tinplate packaging for cans and tins is projected to grow from USD 1.73 billion in 2024 to USD 3.08 billion by 2034, a CAGR of 5.94% (Precedence Research).
Market sizing for tinplate is not uniform. Cognitive Market Research estimates the same 2024 category at USD 761.2 million, a gap that reflects different definitions — whether “tinplate packaging” includes all steel cans or only decorative and specialty tins. Buyers comparing suppliers should apply the same discipline to supplier claims: confirm what a figure covers before using it in a sourcing decision.
Two structural pressures make failure prevention more demanding than it was a decade ago. Supply chains are longer, so a tin may spend weeks in transit and months in storage before reaching the consumer. And brands continue to push for lighter, more cost-efficient packaging, which narrows the margin for error in gauge and coating specification. Regulatory expectations have tightened in parallel: EN 10202:2022 specifies electrolytic tinplate requirements for direct food contact in the EU, and the U.S. FDA requires certified food-grade materials plus food-safe lacquers such as epoxy resins to limit metal migration. Sustainability adds a further reason to solve the failure rather than over-pack around it — tinplate recycling rates exceed 90% in some regions.
How a Tin Box Factory Prevents Rust, Dents, and Moisture Damage
Material selection: the substrate and coating decision
Tinplate is steel carrying a thin tin coating. The tin layer provides corrosion resistance and a printable surface; the steel provides strength. Every cutting, slitting, punching and seaming operation exposes bare steel at an edge, and those exposed edges are where corrosion normally begins. Substrate selection is therefore not a single “food grade” label — it is a matched decision covering steel grade, tin coating weight, and the interior lacquer that separates metal from product.
The correct combination depends on the product, not on the factory's default. A dry tea or coffee product behaves differently from a salted snack, an acidic confection, a fragrance formula containing solvents, or a pharmaceutical item with a defined compatibility requirement. JINGLI CAN's product range covers food tins, tea and coffee tins, cosmetic tins, gift tins and pharmaceutical tins — categories with materially different corrosion and compatibility demands — which is why substrate and interior coating are developed per project rather than held to one specification across the whole catalogue.
Structural engineering: designing out dents and poor lid fit
Denting is a geometry problem before it is a thickness problem. Dent resistance in a tin box is determined by the combination of steel gauge, body diameter and height, corner radius on rectangular formats, reinforcing features such as beads or ribs, and the tolerance between lid and body. Increasing gauge alone adds cost and weight without necessarily removing the failure, because a large unsupported panel will still deflect if the geometry gives it nothing to hold onto.
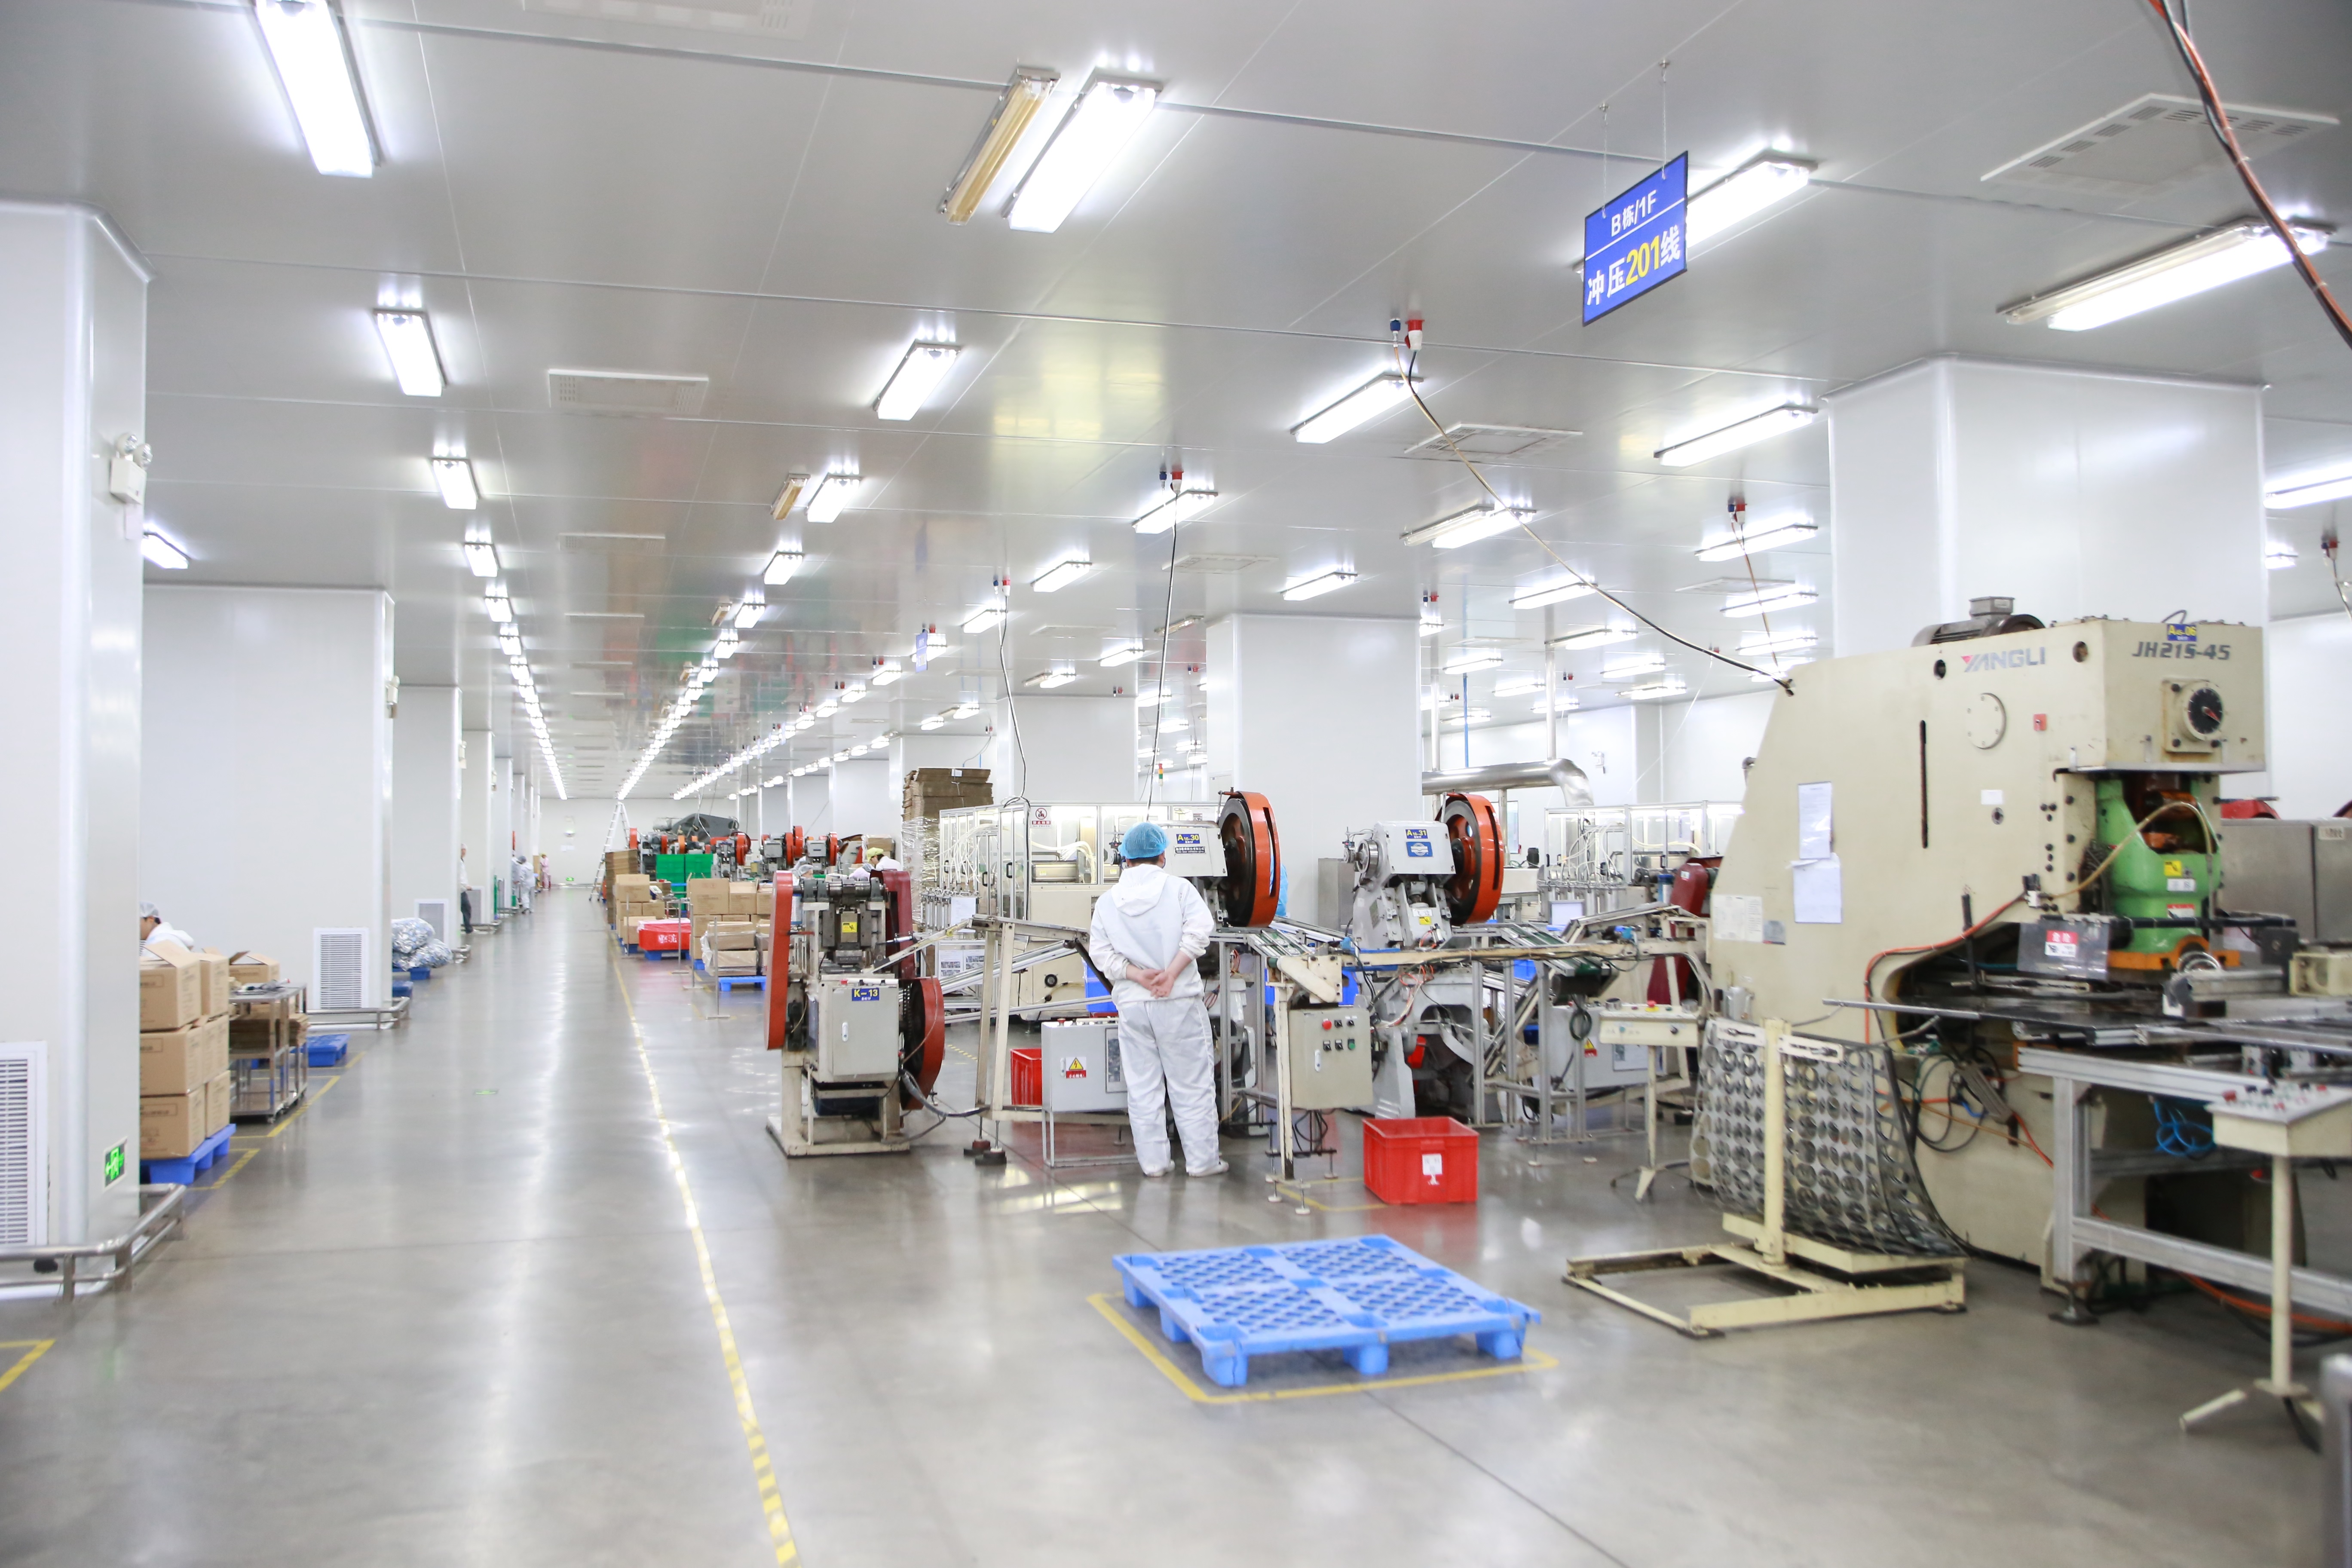
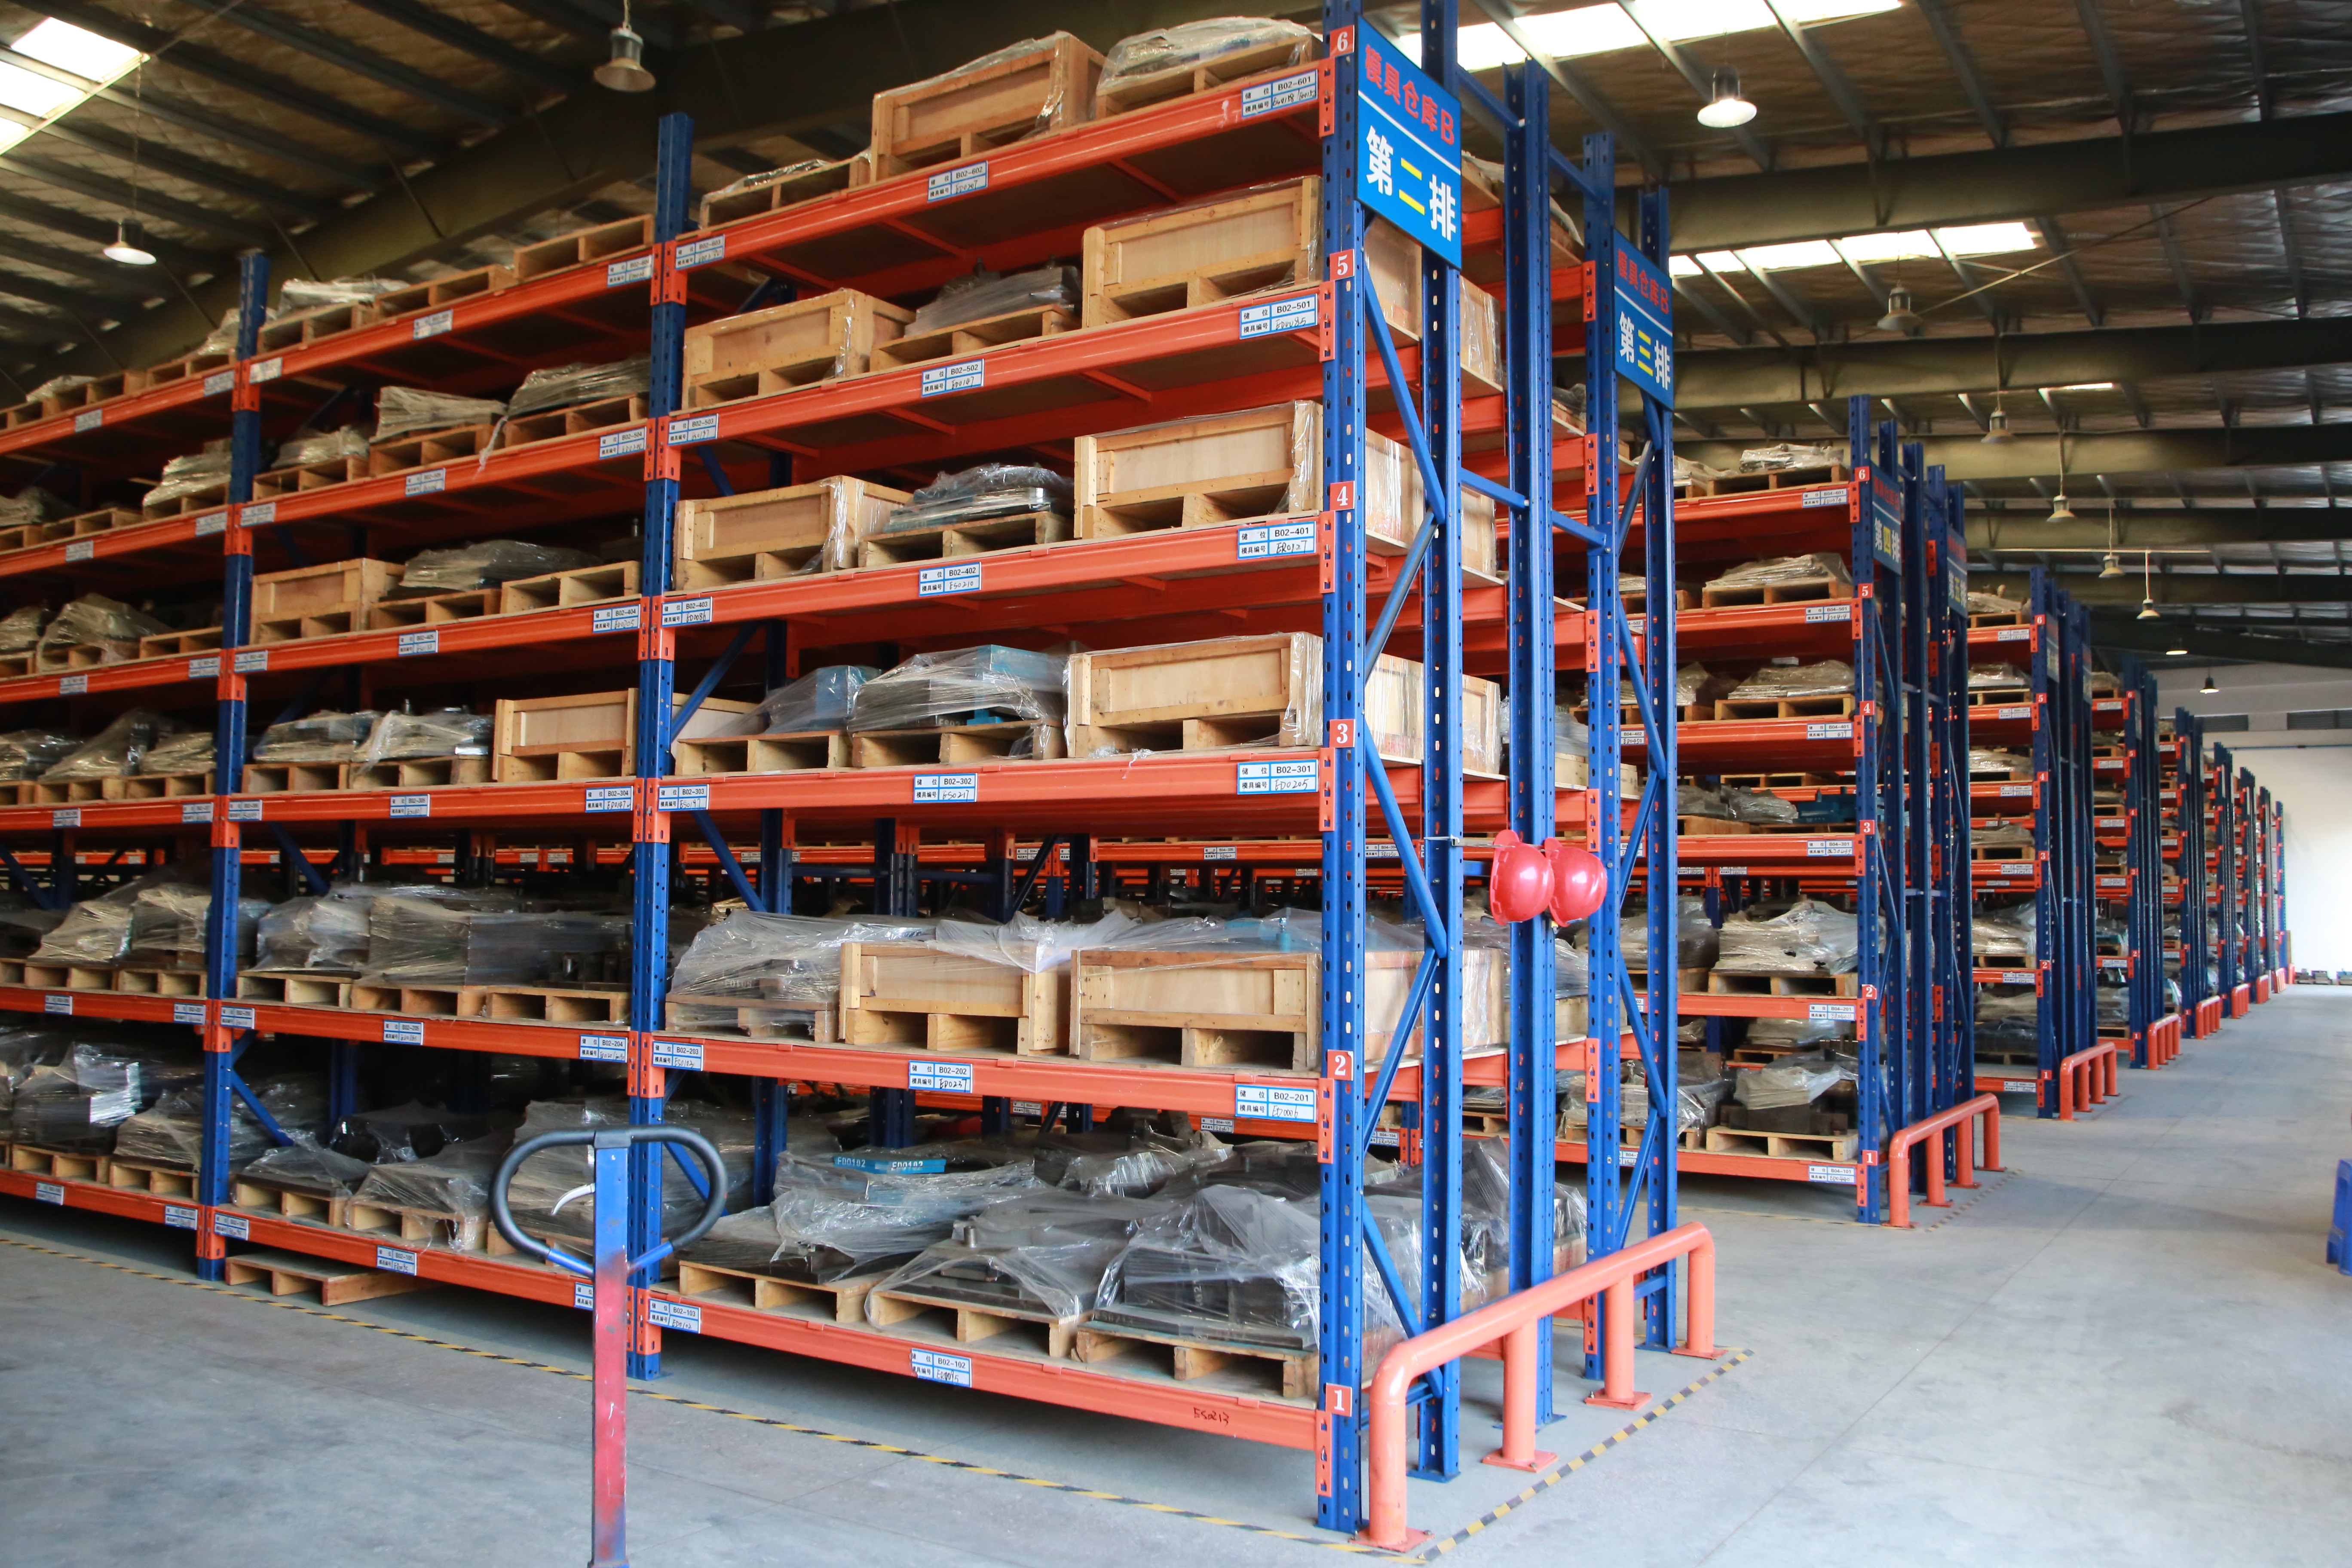
Lid fit is the other half of the structure. A lid that is too tight distorts during closing and scuffs the print; a lid too loose will not hold the barrier or survive stacking. In a factory with in-house tooling, both can be resolved before mass production instead of discovered in a container. JINGLI CAN's manufacturing footprint includes a tooling shop and a punching workshop, and a 50-engineer R&D team works alongside production — so structural changes such as a larger corner radius, a revised bead, or an adjusted lid clearance can be tested and corrected at tooling stage.
Lining and seam systems: the moisture and oxidation barrier
No single component makes a tin airtight. The barrier is the assembly: the interior lacquer film, the continuity of that film through forming, the seam where body and bottom join, and the lid fit that closes the package. Moisture and oxygen damage — softened tea, stale coffee, bloomed chocolate, clumped powder, faded fragrance — appears when any one of those elements is compromised.
Interior lacquer choice is product-specific. The U.S. FDA's food-contact framework requires certified materials and food-safe lacquers such as epoxy resins to limit metal migration into food. Fragrances and cosmetics add a different requirement, because the formula itself can attack an unsuitable coating from the inside, producing blistering or discolouration that has nothing to do with external humidity. Seam integrity matters for the same reason: a seam that is not fully closed is both a moisture path and a corrosion start point, since it exposes steel that the lacquer film may not fully cover.
The practical implication for buyers is direct: treat “airtight” as a specification to be validated, not a feature to be assumed. Ask which coating system is proposed for your product, and validate it with a filled sample rather than an empty one.
Print and surface protection: stopping scuffs and print defects
Print defects that appear after delivery usually originate in two places: adhesion and cure at the printing stage, and abrasion resistance during packing and transit. Under-cured coating adheres poorly and can lift, block or discolour. Over-cured coating becomes brittle and cracks when the tin is formed or handled. On a formed and decorated tin, the print must also survive nested stacking, cartoning and palletising without wearing at the edges.
The printing line is therefore part of the corrosion system, not only the decoration system — a coating defect is an exposure point. JINGLI CAN integrates printing within the same manufacturing flow as forming and tooling, which allows a print or coating problem to be traced to its actual process step instead of being renegotiated between separate suppliers.
Process control and certified production
Consistency is the difference between a sample that performs and a mass order that performs. A specification that is correct once but drifts across a run produces mixed results: some units pass, some corrode, and to the buyer the failure looks random.
JINGLI CAN holds six certifications relevant to this problem. ISO9001 covers quality management, the framework for inspection and corrective action. ISO14001 covers environmental management. ISO22000 and FSSC22000 are food-safety management systems, and BRCGS is a globally used food-safety standard for packaging and food manufacturing. SEDEX 4P is an ethical trade audit covering labour and supplier conduct. For a buyer, the practical value is not the certificate list itself but what it implies: documented process control, traceability, and an auditable answer when something goes wrong.
Supply continuity as a quality variable
Substrate consistency affects corrosion performance and print appearance at the same time. If tin coating weight or surface finish shifts between production lots, corrosion resistance and print adhesion shift with it. JINGLI CAN maintains a regular stock of 30,000 tons of tinplate, which reduces dependence on spot material purchases between orders. Capacity is correspondingly large: a facility in Vinh Phuc Province, Vietnam covers 17,500 m² with a daily production capacity of 600,000 pieces, alongside a factory footprint of 150,000 m², around 2,000 employees, and annual output of 1,800,000,000 units.
A Step-by-Step Specification and Validation Workflow
The sequence below is the buyer-side workflow that removes most of the failure modes described above. It is ordered deliberately: each step depends on the decision made before it.
- Define the failure you are preventing, not the tin you are buying. Start from product sensitivity — moisture, oxygen, aroma, fat, acidity, fragrance solvents, or regulatory classification. The failure mode sets the specification.
- Specify substrate and interior coating against that failure mode. Confirm the tinplate requirement, including EN 10202:2022 where EU food contact applies, and the lacquer system appropriate to the product itself rather than to the category in general.
- Engineer the structure for the shipping environment. Gauge, diameter-to-height ratio, corner radius, beads and stacking load. A tin shipped as a single e-commerce unit faces different loads from one shipped on a pallet, so drop and corner performance may matter more than compression.
- Treat lid, body and seam as one barrier system. Define lid fit tolerance and seam requirements together with interior coating continuity — not as three separate line items.
- Validate print for transit, not only for appearance. Confirm adhesion and abrasion resistance against the actual packing method, carton fit and stacking.
- Run a filled trial, not an empty sample. Fill, seal, and subject the packed unit to realistic transport and storage conditions; then open it and inspect seam, coating and product together.
- Lock the process and the inspection points. Agree which characteristics are checked, at which production stage, and what the acceptance criteria are, so a drifting run is caught inside the factory.
- Plan supply continuity before the repeat order. Confirm substrate stock policy, capacity allocation and reorder triggers, since substrate changes between lots are a common and invisible cause of performance drift.
Use Cases: Where Each Failure Mode Bites Hardest
The relative priority of rust, moisture, denting and print durability changes with the product. The categories below follow the product lines JINGLI CAN manufactures; the failure emphasis is a specification judgement for buyers, not a claim about any specific customer programme.
Tea and coffee tins
Aroma and moisture dominate. Barrier performance through lid fit and interior coating matters more than decorative print durability, because the tin is opened and reclosed many times over its life. A tea tin box factory's real deliverable is a barrier that survives months of reclosing, not a barrier that tests well on delivery day.
Chocolate, candy, chewing gum and mooncake tins
Chocolate is sensitive to heat and moisture; sugar-based confectionery is sensitive to humidity. Dents are highly visible on decorative formats and often trigger retail rejection even when the product inside is intact. Mooncake tins add a seasonal dimension: volume concentrates into a short window, so consistency within a single run carries more risk than long-term drift.
Cosmetic, perfume and soap tins
Fragrance formulas and soap can attack an unsuitable interior coating from the inside, producing blistering or discolouration unrelated to external humidity. Print durability during shelf life and handling is a presentation risk. The governing specification question is compatibility, not only barrier.
Pharmaceutical, medicine and health care product tins
Compatibility and traceability dominate. Certified production and documented process control matter more than decorative flexibility, and the material specification needs to be defensible on paper as well as in the sample.
Gift, stationery, tool, watch, glasses and cigar tins
These formats prioritise structure and print: hinge and lid fit, dent resistance on large flat panels, and surface durability through gift wrapping and retail handling. Cigar tins invert the usual moisture requirement — the objective is moisture retention rather than exclusion, which changes how the seal is designed.
Failure Mode Comparison Table
The table below maps each failure mode to its usual root cause and to the point in production where it is controlled. It is a diagnostic reference for specification discussions, not a substitute for a filled trial.
| Failure mode | How it appears | Primary root cause | Factory countermeasure | Where control sits |
|---|---|---|---|---|
| Seam rust | Brown staining along the body-to-base seam | Exposed steel at the seam with incomplete coating coverage | Seam design and compound plus interior coating continuity | Tooling and coating process |
| Edge and scratch corrosion | Localised rust at cut edges, rims or abrasion points | Bare steel exposed during forming and handling | Edge control through forming plus transit protection | Punching and packing |
| Interior coating failure | Blistering, peeling or discolouration inside the tin | Coating incompatible with the product, or incompletely cured | Product-specific lacquer selection and cure control | Coating and quality control |
| Moisture ingress and aroma loss | Soft tea, stale coffee, clumped powder, faded fragrance | Barrier break at lid fit or at the seam | Lid tolerance and seam integrity managed as one system | Tooling and assembly |
| Denting | Corner dents, ovalised body, deformed panels | Gauge and geometry mismatched to handling and stacking loads | Structure engineered against the actual shipping environment | R&D and tooling |
| Lid fit drift | Lids loose, tight, or hard to close on some units | Tolerance stack-up in tooling and forming | In-house tooling correction before mass production | Tooling shop |
| Print scuff and adhesion loss | Worn print on edges, blocking, coating lift | Under- or over-cured coating with insufficient abrasion resistance | Print and cure control matched to the packing method | Printing line |
| Discolouration or blocking in storage | Tins sticking together or colour shifting in the warehouse | Coating interaction under heat and humidity during storage | Coating system selection and agreed storage conditions | Coating and logistics |
Product Category Comparison Table
| Product category | Dominant failure risk | Specification priority |
|---|---|---|
| Tea and coffee tins | Moisture ingress, aroma loss | Lid fit, interior coating, reclosing durability |
| Chocolate, candy and chewing gum tins | Humidity, heat, visible denting | Structural rigidity of the decorative format, seam barrier |
| Mooncake and gift tins | Dents and print damage during seasonal handling | Corner radius, panel support, print abrasion resistance |
| Cosmetic, perfume and soap tins | Internal coating attack, print wear | Coating compatibility with the formula, surface resistance |
| Pharmaceutical, medicine and health care tins | Compatibility, traceability | Certified process control, documented material specification |
| Cigar tins | Moisture retention rather than exclusion | Seal design balanced against controlled humidity |
| Tool, watch, glasses, pencil and stationery tins | Denting on large flat panels, hinge and lid wear | Gauge and geometry, hinge and lid tolerance |
FAQ
Which certifications should a tin box factory hold for food, cosmetic or pharmaceutical packaging?
The relevant baseline depends on the destination market and on whether the tin contacts the product directly, but a practical set covers four areas. Quality management is addressed by ISO9001. Food-safety management is addressed by ISO22000 and FSSC22000, with BRCGS as a globally used food-safety standard for packaging and food manufacturing. Ethical and labour conduct is addressed by SEDEX 4P, and environmental management by ISO14001. JINGLI CAN holds all six: ISO9001, ISO14001, ISO22000, BRCGS, FSSC22000 and SEDEX 4P. On the material side, EU food-contact tinplate requirements are specified in EN 10202:2022, and U.S. FDA food-contact rules require certified food-grade materials plus food-safe lacquers such as epoxy resins to limit metal migration.
Can a tin box factory engineer a tin that resists denting and still closes with a reliable barrier?
Yes, but it is a combined geometry-and-gauge decision rather than a thickness decision. Dent resistance comes from steel gauge, body diameter and height, corner radius, reinforcing beads or ribs, and the lid-to-body tolerance, set together. A capable factory resolves these at tooling stage. JINGLI CAN supports this with an in-house tooling shop, a punching workshop and a 50-engineer R&D team working alongside production, so a structure can be modified and retested before a mass order is placed. The validation step still matters: the claim should be confirmed with a filled trial that reproduces the real transport and storage conditions.
What drives the unit cost of a corrosion-resistant tin box?
Cost is driven by a small number of specification variables: steel gauge, tin coating weight, the interior lacquer system, the print method and number of colours, tooling, order volume, and the inspection level agreed for the run. These variables are the same ones that deliver corrosion, dent and barrier performance, which is why cost reduction and failure prevention pull against each other. Removing lacquer coverage, reducing gauge, or simplifying seam control will lower the unit price and raise the rejection and reprint risk further down the chain. For that reason, comparisons between quotations are only meaningful when the specifications behind them are compared line by line.
How should I validate a tin box before committing to production?
Validate with the real product, not with an empty tin. Request samples built to the proposed specification, fill and seal them, and subject the packed unit to conditions that resemble the actual route to market: transit, stacking, and the storage environment at the destination. Then inspect the seam, the interior coating, the lid fit and the print after handling. Where the product is sensitive to moisture, oxygen or aroma, the product itself should be checked after the trial period, not only the metal. Agreeing written acceptance criteria before the trial turns the result into a specification decision rather than an opinion.
How does a tin box factory protect delivery schedules on a repeat order?
Schedule reliability rests on two variables more than any other: material availability and allocated production capacity. Decoration complexity, tooling status and order volume then determine the actual timeline. JINGLI CAN maintains a regular stock of 30,000 tons of tinplate to reduce dependence on spot material purchasing, and operates a facility in Vinh Phuc Province, Vietnam covering 17,500 m² with a daily production capacity of 600,000 pieces, alongside annual output of 1,800,000,000 units. Those are the conditions that make a repeat order predictable rather than a renegotiation. Exact schedules are confirmed at quotation stage for the specific format and decoration. To discuss a project or request a quote, contact sales11@jinglitinbox.com or +86 18819080997.
Conclusion
Rust, dents, moisture damage and print defects in tin packaging are not market accidents. They are the predictable result of four decisions — substrate and coating, structure and fit, lining and seam, and process control — being made deliberately or being left to default. The failure appears late, in transit or on shelf, but it is decided early, in the specification and the tooling.
For buyers in the evaluation and execution stages, that reframing changes what to ask a supplier. The productive questions are not “what is your best price” but “which coating system do you propose for this product and why”, “how will you hold lid fit across a run”, “where in your process is seam integrity checked”, and “what happens to substrate consistency between my first and third order”. A factory that answers those questions with process detail — in-house tooling, documented quality control, certified food-safety systems, and material stock discipline — is addressing the failure at its source.
Next Step
If rust, moisture or denting has already cost you a shipment, the useful starting point is a specification conversation rather than a catalogue page. Share the product type, the failure you need to prevent, the shipping route and the format you have in mind.
JINGLI CAN — Dongguan City Jingli Can Co., Ltd
Email: sales11@jinglitinbox.com
Tel: +86 18819080997
Website: www.tinbox.cn
Blog: blog.tinbox.cn
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.