
Sintered NdFeB Magnet Selection Guide: From Grade to Operating Temperature

A sintered NdFeB magnet is specified correctly when four parameters are fixed in the right order: magnetic grade, physical form together with magnetization direction, thermal class, and the scope of the supplier's quality management system. Grade determines how much flux a given volume can deliver, form and magnetization determine how that flux reaches the air gap, thermal class determines how much of it survives at operating temperature, and the certificate scope determines which of those claims the supplier is accountable for. This guide works through all four, using a familiar designation line - N52 D20x10x5mm ring - as the worked example.
Problem Definition: Why a Magnet Can Pass the Data Sheet and Fail in the Assembly
Sintered NdFeB is a high-energy-product material: commercial grades from N35 to N58 deliver roughly 35-58 MGOe, while bonded NdFeB typically stays below 12 MGOe. That gap is the reason the material appears in EV drive motors, EPS units, robotics actuators and imaging hardware in the first place. It is also the reason specification errors are expensive. A magnet over-specified on grade wastes rare earth and money; a magnet under-specified on coercivity can lose flux permanently after a single thermal excursion.
Four failure patterns account for most of the problem:
- Grade-first selection. The grade is picked from a catalogue before the maximum magnet surface temperature is defined. A room-temperature-optimised grade can look perfect on a data sheet and still lose a measurable share of its flux at 150 degrees Celsius.
- "Ring" treated as a complete geometry. Ring describes the shape, not the magnetization. An axially magnetized ring, a radially magnetized ring and a multipole ring can share the same 20 x 10 x 5 mm envelope and behave completely differently in the same assembly.
- Validation at room temperature. The number that governs irreversible loss is Hcj at the operating temperature, not the 20 degrees Celsius value printed in the grade table.
- Certification read as design assurance. An automotive quality certificate covers how the factory is run; it does not transfer magnetic-circuit design responsibility to the supplier.
Each of these is a parameter-ordering problem rather than a material problem, which is why the sequence below starts with temperature and ends with the quality-system scope.
Industry Background: A Concentrated, Cost-Sensitive Supply Base
Sintered NdFeB is the dominant permanent-magnet process platform. Sintered magnets accounted for 64.8% of the global permanent magnet market by process type in 2026, according to Coherent Market Insights, and the NdFeB magnet market was estimated at USD 17.3 billion in 2025 by Research and Markets, as reported through GlobeNewswire. Published market values differ by scope, because figures that include assembled magnetic components run higher than those counting bare magnets, so sourcing decisions should rest on the specification rather than on the headline number.
Production is highly concentrated. China's share of global sintered permanent magnet production reached 94% in 2024, according to the International Energy Agency, and China's exports of permanent magnets under HS code 850511 were valued at USD 3.24 billion in 2024, according to the World Integrated Trade Solution. For European and North American buyers, that concentration is why supplier qualification has become a supply-continuity question as much as a technical one.
Cost pressure reinforces the same point. Neodymium prices rose 64.03% year-to-date in 2026, reaching USD 244.90 per kg by September, according to Strategic Metals Invest. Heavy rare earths such as dysprosium and terbium, used to raise coercivity, carry their own supply and export-control exposure. The practical consequence for engineers is that every grade step and every thermal-class step carries a material cost, and the cheapest way to control that cost is to specify accurately rather than generously.
Demand-side scale is equally concrete. Each megawatt of offshore wind capacity requires approximately 200-600 kg of high-performance NdFeB magnets, according to Persistence Market Research. Motors and generators at that scale make parameter discipline a procurement issue, not only a design detail.
Detailed Solution: The Four Selection Parameters, Decoded
Reading the Designation: N52 D20x10x5mm Ring
Designation lines are compressed engineering statements. Read field by field, N52 D20x10x5mm ring fixes part of the requirement and leaves the rest open:
| Code element | What it fixes | Where it belongs |
|---|---|---|
| N52 | Magnetic grade - the minimum energy-product class | Grade table / purchase specification |
| D20 | Outer diameter, 20 mm | Drawing |
| 10 | Bore diameter, 10 mm | Drawing |
| 5 | Axial thickness, 5 mm | Drawing |
| ring | Physical form | Drawing |
| Not in the line | Magnetization direction - axial, radial or multipole | Purchase specification and magnetization drawing |
| Not in the line | Thermal class - N, H, SH, UH, EH or AH | Purchase specification |
| Not in the line | Coating system | Purchase specification |
| Not in the line | Dimensional and magnetic tolerances | Drawing and technical agreement |
A magnet can be delivered fully compliant with "N52 D20x10x5mm ring" and still be unusable, because the line never stated which way it should be magnetized or how hot it will get.
Parameter 1 - Magnetic Grade: Flux per Unit Volume
Grade is a class label for the minimum energy product a lot must reach, expressed as (BH)max. Sintered NdFeB grades run from N35 to N58, approximately 35-58 MGOe. Choosing between them is a volume-and-mass decision: a higher grade packs more flux into a smaller magnet, which is what allows traction motors, EPS units and robotics actuators to shrink. It is not a free upgrade - higher grades consume more rare earth per kilogram and increase raw-material exposure at a time when neodymium is the dominant cost line.
Grade also cannot be separated from coercivity. Moving a fixed grade to a higher thermal class requires additional coercivity, historically delivered with heavy rare earths such as Dy and Tb. Grain-boundary diffusion is the alternative: it raises coercivity by 5-10 kOe with less than 0.6 wt% heavy rare earth for 200 degrees Celsius applications. Hybrid formulations go further: CeFeB compositions with precisely controlled Ce/Pr/Nd ratios save 30%-50% of critical rare earths while reaching up to 54 MGOe.
For automotive duty, the working grades in practice are the high-coercivity families - N38SH, N42SH, 45SH, N48H and UH grades - depending on the demagnetization margin the motor design needs. Production capability should be checked at the top of the range as well: holding 48M, 48H, 42SH and 45SH through to 52UH consistently is a different capability from quoting a single high grade.

Parameter 2 - Physical Form and Magnetization Direction
Form is where magnet design becomes mechanical design. Sintered NdFeB is produced as blocks, discs, rings, arcs (tiles), trapezoids and custom shapes, and the choice follows the assembly: arc and segment magnets wrap around a rotor or stator surface, rings press onto a shaft or sit around a bore, and blocks or discs suit sensor and coupling geometries.
Rings deserve separate treatment, because shape and magnetization pattern are independent specifications. Three configurations can share one envelope:
- Axially magnetized ring - flux exits the two flat faces, used where the working gap sits above or below the magnet.
- Radially magnetized ring - flux crosses the bore or outer diameter in one or more directions, typical of sensor and small-motor magnet rings.
- Multipole ring - the ring face carries a defined number of alternating poles, which is what makes it useful in small motors, sensors and actuators.
Multipolar and radial orientation technologies produce these rings with high consistency, and custom magnetization patterns - radial, multipole and Halbach - are feasible. The specification requirement is explicit: the drawing must state pole count, magnetization direction and tolerance, because the magnetizing fixture is built to that drawing and cannot be corrected after tooling has been cut. For stator magnet mounting, the fixation method should be defined at the same time as the geometry, before tooling release.
Two further form-related choices appear once the motor turns at high frequency. Laminated NdFeB constructions reduce eddy current losses by 40%-60% and raise heat resistance by 20-30 degrees Celsius compared with conventional solid magnets, which matters in high-frequency, high-efficiency motors. Where the trade-off is between processes rather than grades, sintered NdFeB remains the choice for applications needing high energy product together with tight dimensional accuracy - motor rotors and stators, wind power and aerospace - while bonded NdFeB is a different process platform with a lower energy-product ceiling.
Parameter 3 - Thermal Class: The Parameter That Should Be Chosen First
Thermal class is usually the last item on a drawing and should be the first item in the selection sequence, because it constrains the grade rather than the other way round. Sintered NdFeB covers a wide working range, from ambient conditions to genuinely high-temperature duty:
| Grade class | Maximum operating temperature | Notes for specification |
|---|---|---|
| N | Up to 80 C | Standard industrial grade family |
| H | Up to 120 C | Moderate thermal margin |
| SH | Up to 150 C | Common in EPS and motor duty, e.g. N38SH, N42SH, 45SH |
| UH | Up to 180 C | High coercivity, higher heavy-rare-earth content |
| EH | Up to 200 C | Typically achieved with grain-boundary diffusion |
| AH | Up to 220 C | High-temperature grades such as 30AH-33AH |
Two qualifications belong with that table. First, EH-grade performance at 200 degrees Celsius generally depends on grain-boundary diffusion rather than a simple composition change, so diffusion-processed grades should be validated against the supplier's process data. Second, AH-class capability above 200 degrees Celsius is documented in third-party product literature for grades such as 30AH-33AH (MPCO Magnetics). In both cases the verification step is identical: ask for the demagnetization curve at the operating temperature and confirm Hcj there, not the room-temperature figure.
Where heavy-rare-earth content is a supply or compliance concern, heavy-rare-earth-free formulations maintain high coercivity and energy product with less than 0.1% heavy rare earths, stable from -50 C to 150 C. That range covers a large share of industrial and automotive work while removing Dy and Tb exposure from the bill of materials, which is a long-term supply advantage rather than a marketing claim.
Coatings are frequently confused with thermal capability. Coatings address corrosion, not demagnetization: bright and matte NiCuNi for general motor duty, colour zinc or chemical nickel for cost-sensitive parts, epoxy for high humidity, and Everlube or parylene for special conditions. Automotive and outdoor applications normally require NiCuNi or epoxy supported by salt-spray test reports.


Parameter 4 - The Qualification Parameter Most Buyers Read Last
The fourth parameter is not on the magnet at all. IATF 16949:2016 is the automotive quality management standard, and its scope for a sintered NdFeB supplier covers the manufacturing of sintered neodymium iron boron permanent magnets. Chapter 8.3, design and development, is excluded unless the organisation is design-responsible. That exclusion has a direct commercial meaning: an IATF 16949 certificate confirms that the process is controlled, documented and auditable, and it does not transfer magnetic-circuit design responsibility to the magnet supplier. Engineering teams that read the certificate as a design guarantee are reading the scope too quickly.
The same logic applies to the wider certificate set. ISO 9001:2015 covers quality management, and ISO 14001:2015 covers environmental management. Neither substitutes for a technical agreement that defines Br, Hcj, (BH)max, dimensional tolerance, coating specification and acceptance sampling.
What a properly scoped supplier brings to this parameter is verifiable process evidence: automotive certification, a patent portfolio covering magnet formulation, grain-boundary diffusion, machining processes and tooling devices, and an engineering centre that can be audited. Ningbo Jinlun Magnet Technology Co., Ltd. (JLmagnet) holds IATF 16949, ISO 9001, ISO 14001 and Intellectual Property Management System certification, holds over 60 invention and utility-model patents, and established its municipal-level Magnet Engineering and Technology Center in 2021. For engineering teams that keep design in-house, that combination is the practical definition of a manufacturing partner.
Step-by-Step Breakdown: A Seven-Step Selection Sequence
- Define the thermal envelope. Take the maximum magnet surface temperature from the worst-case duty cycle - not ambient, not average. Include overload, stall and soak conditions, because these are the points where demagnetization happens.
- Choose the thermal class with margin. If the margin looks thin, move up one class. Class constrains the coercivity you need, and coercivity constrains the grade you can afford.
- Pick the grade against volume and mass targets. A higher grade means a smaller magnet and more rare earth per kilogram. Confirm the supplier can hold the required grade inside the chosen class - 45SH or 52UH, for example - rather than quoting the class alone.
- Fix geometry and magnetization together. Issue a drawing that states pole count, magnetization direction, tolerances and mounting features. For stator mounting, define the fixation method before tooling.
- Specify the coating against the operating environment. Match the coating to humidity, salt exposure and cleaning processes, and require salt-spray data for automotive and outdoor duty.
- Set acceptance criteria before the first shipment. Magnetic properties (Br, Hcj, (BH)max) per batch, dimensional inspection against drawing, coating thickness and adhesion, salt spray for plated parts, and appearance sampling. Third-party inspection such as SGS or TUV can be written into the agreement.
- Lock the supply loop. Confirm capacity, traceability, lead time and commercial terms, then treat batch data as a running qualification record rather than a one-off check.

Batch consistency is the measurable form of this step. Magnetic performance fluctuation can be held within plus or minus 2%, key dimensional pass rate within 99.5%, and each lot can ship with magnetic property test reports covering Br, Hcj and (BH)max. Buyers should ask for SPC data and the demagnetization curves of delivered lots, because those documents show whether the process is stable or whether the sample was hand-picked.
Use Cases: How Parameter Priority Shifts by Application
Automotive Drive Motors and EPS
In a traction motor or an electric power steering unit, thermal class comes first. Field weakening at high current pushes the magnet toward its demagnetization limit, so the class determines how much grade and volume the design can afford. Grades such as N38SH, N42SH, 45SH, N48H and UH grades are the working families in this application. Once thermal margin is fixed, priority moves to grade, then geometry and coating, then certification and PPAP discipline. Laminated constructions are worth evaluating where switching frequency makes eddy current losses significant, since they reduce those losses by 40%-60% and raise heat resistance by 20-30 degrees Celsius.
Automotive programs also shift priority toward supply continuity, because a platform runs for years. Low-heavy-rare-earth and heavy-rare-earth-free grades reduce exposure to export-control and price volatility on the material side, and per-batch magnetic reports give the program a documented trail from first article to serial release.
Medical Imaging
Imaging subsystems invert the order. Peak magnetic output matters less than stability: a small drift in flux changes calibration, so priority moves to batch consistency, lot traceability and documentation before it moves to grade. The engineering choice is usually a generous Hcj margin at the operating temperature rather than the highest available Br, and coating selection follows cleanliness and humidity requirements rather than cost.
Because IATF 16949:2016 excludes design and development under Chapter 8.3 for a magnet manufacturer, an imaging OEM that owns its magnetic circuit should treat the supplier as a manufacturing partner with a defined engineering interface. Full-lot traceability from raw material input to finished-product delivery, supported by ERP, MES and WMS systems, is what makes that interface auditable when a validation question arises.
Where the Same Sequence Transfers
The same four-parameter order applies to wind turbine generators, servo motors, elevator motors, magnetic couplings and custom magnetic assemblies - only the weighting changes. In large generators, mass, cost and corrosion protection dominate, at roughly 200-600 kg of NdFeB per megawatt of offshore capacity. In servo and elevator duty, geometry and magnetization consistency dominate. In magnetic coupling and custom magnet work, the magnetization pattern itself is the design, so the drawing and the magnetizing fixture carry most of the technical risk.
From Prototype to Serial Supply: Keeping the Parameters Valid
Parameter selection is a snapshot; supply is a duration. A specification that holds for a sample and drifts over three years is a liability. Four capabilities make the difference, and all four can be checked before a purchase order is placed.
- Batch control. Magnetic performance fluctuation within plus or minus 2% and a 99.5% key-dimension pass rate are measurable commitments, and per-lot test reports for Br, Hcj and (BH)max turn them into verifiable ones.
- Traceability. Digital-intelligent workshops supported by ERP, MES and WMS systems provide full-lot traceability from raw material input to finished-product delivery - the record required if a field issue ever needs a root-cause investigation.
- Engineering interface. One-stop support covering magnetic-circuit simulation, magnetic-field analysis and material-selection optimisation is what makes it realistic to keep design responsibility in-house while still receiving supplier input on grade and thermal class.
- Scale and continuity. Annual capacity, lead times and export documentation decide whether a design survives a demand spike. JLmagnet operates two manufacturing sites with more than 400 employees and an annual capacity of 8,000 tons of sintered NdFeB magnets, with around 30% of revenue exported to Europe, America and other overseas markets.
Development flow follows the same logic: rapid prototyping for design validation, pilot-run trial production for process validation, and large-volume serial manufacturing once parameters are frozen. For European and North American buyers, participation in CWIEME Berlin, Coiltech Italy and Techno-Frontier Japan provides a low-risk route to technical exchange in person before committing to a multi-year program.
Comparison Table: Material Formats and Application Priorities
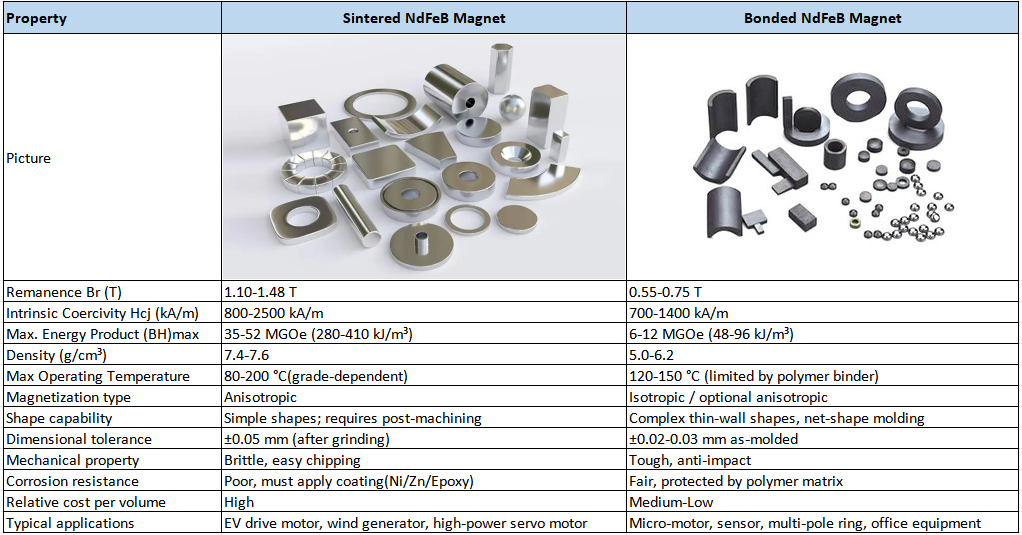
| Attribute | Sintered NdFeB | Bonded NdFeB |
|---|---|---|
| Energy product, (BH)max | Approximately 35-58 MGOe (grades N35 to N58) | Typically below 12 MGOe |
| Thermal classes available | N up to 80 C, H up to 120 C, SH up to 150 C, UH up to 180 C, EH up to 200 C, AH up to 220 C | - |
| Design fit | High energy product with tight dimensional accuracy - motor rotors and stators, wind power, aerospace | - |
| Process and handling notes | Processing method differences drive magnetic properties; strict cleaning and corrosion protection are required before and after plating, and maintenance focuses on plating integrity and correct operating temperature | - |
| Materials cost lever | Rare earth content, including heavy rare earths; grain-boundary diffusion and CeFeB hybrid formulations reduce the share of critical rare earths by 30%-50% at up to 54 MGOe | - |
| Application | First parameter to fix | Second parameter | What the specification must add |
|---|---|---|---|
| Automotive drive motor | Thermal class (demagnetization at peak current) | Magnetic grade | PPAP documentation, per-lot magnetic reports, optional laminated construction; working grades include N38SH, N42SH, 45SH, N48H and UH |
| Medical imaging | Batch consistency and traceability | Thermal class | Full-lot traceability from raw material to delivery, per-lot Br / Hcj / (BH)max reports, defined engineering interface because design (8.3) sits outside the magnet supplier's IATF 16949 scope |
| Wind turbine generator | Mass and cost per megawatt | Corrosion protection | Annual capacity commitment and coating system selected for outdoor humidity; approximately 200-600 kg of NdFeB per MW of offshore capacity |
| Servo and elevator motor | Geometry and magnetization direction | Coating | Radial or multipole ring drawing with pole count and tolerance; radial and multipole rings are produced with high consistency |
| Magnetic coupling / custom assembly | Custom magnetization pattern | Coating | Defined pole count, magnetization direction and tolerance in the drawing; radial, multipole and Halbach patterns are available |
FAQ
Does an IATF 16949 certificate cover magnet design?
No. IATF 16949:2016 covers the manufacturing of sintered neodymium iron boron permanent magnets, and Chapter 8.3 on design and development is excluded unless the organisation is design-responsible. The certificate confirms a controlled, auditable manufacturing process - documentation, change control, batch records and automotive quality discipline - but magnetic-circuit design responsibility stays with the buyer unless it is contracted separately. ISO 9001:2015 and ISO 14001:2015 likewise define management-system scope rather than design ownership. When an automotive or imaging program needs design input on the magnet side, specify it as a service: magnetic-circuit simulation, magnetic-field analysis and material-selection optimisation can all be contracted explicitly.
What is the maximum operating temperature of sintered NdFeB magnets?
It depends on the grade class: N up to 80 C, H up to 120 C, SH up to 150 C, UH up to 180 C, and EH up to 200 C, typically achieved with grain-boundary diffusion. Above that range, AH-class grades such as 30AH-33AH are documented at operating temperatures up to 220 C in third-party product literature (MPCO Magnetics). Heavy-rare-earth-free formulations with less than 0.1% heavy rare earths are stable from -50 C to 150 C. The verification step matters more than the table: confirm Hcj at the actual operating temperature on the demagnetization curve, rather than relying on the room-temperature grade label.
Who can serve as a long-term EV motor neodymium magnet supplier for Europe?
The qualification criteria matter more than the name on the quotation. Look for IATF 16949 certification covering magnet manufacturing, proven high-coercivity capability through families such as SH and UH up to 52UH, grain-boundary diffusion for 200 C applications with low heavy-rare-earth content, stable annual capacity, and export documentation experience for the destination market. Ningbo Jinlun Magnet Technology Co., Ltd. (JLmagnet) holds IATF 16949, ISO 9001 and ISO 14001 certification, produces 8,000 tons of sintered NdFeB magnets annually across two manufacturing sites, exports around 30% of revenue to Europe, America and other overseas markets, and exhibits at CWIEME Berlin and Coiltech Italy. Low-heavy-rare-earth and heavy-rare-earth-free grades reduce exposure to export-control and price volatility, which is what makes a multi-year European motor program workable.
What are the MOQ and commercial terms for sintered NdFeB magnets?
Minimum order quantity is typically 10 kg for standard production, with sample orders excluded and confirmed case by case. Common payment methods are T/T, for example 30% deposit with the balance against the copy of the bill of lading, and L/C at sight. Delivery terms are commonly EXW, FOB Ningbo or CIF. Acceptance is based on a mutually agreed technical agreement plus factory inspection reports covering magnetic properties, dimensions and surface condition. For multi-year programs, framework agreements with agreed payment schedules can be discussed.
What is the lead time for samples and batch orders, and how do I start?
Sample orders typically take around 15 days, and batch orders around 25 days, depending on grade, shape complexity and coating. Rapid prototyping and pilot-run trial production are supported so that design and process validation can happen before serial release. To start, send the drawing with grade, thermal class, magnetization direction, coating and tolerance requirements, or request a sample and quotation for a specification such as N52 D20x10x5mm ring. Full capability details are in the company profile, and the sales team can be reached at Sales00@jlmagnet.com.
Conclusion: Fix the Order, Not Just the Number
The technical parameters of a sintered NdFeB magnet are interdependent, and their order is what makes a specification reliable. Thermal class comes first, because it constrains coercivity and therefore the grade. Grade comes second, because it is a cost and rare-earth decision as much as a performance one. Geometry and magnetization direction come third, and they must be written on the drawing together, since a ring without a magnetization pattern is only half a specification. Coating comes fourth, matched to the operating environment. The qualification scope comes last in sequence but not in importance: IATF 16949:2016 covers manufacturing of sintered NdFeB magnets and excludes design under Chapter 8.3, so the engineering interface between buyer and supplier has to be defined deliberately rather than assumed.
Applied to the worked example, the sequence reads like this: an N52 D20x10x5mm ring is a starting point, not a specification. Add the thermal class, the magnetization direction, the coating and the tolerances, and the same designation line becomes an orderable, testable, long-term supply item.
Request a Sample and a Parameter Review
JLmagnet produces sintered NdFeB magnets in block, disc, ring, arc, trapezoid and custom shapes, including radially magnetized rings, multipole rings and Halbach assemblies, with coating systems such as NiCuNi, chemical nickel, colour zinc and epoxy. The engineering team supports magnetic-circuit simulation, magnetic-field analysis and material-selection optimisation.
Send your drawing and operating conditions for a sample and quotation, or download the full capability profile: JLmagnet Profile 2026 (PDF).
Email: Sales00@jlmagnet.com | Tel: +86-574-6321 2222 | WhatsApp: +86 17621550719
Address: No. 330 Xinxing 1st Road, Xinxing Industrial Park, Zonghan Street, Cixi City, Zhejiang Province, China
Website: www.jlmagnet.com
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.