Matching Maleic Anhydride Grafted Polymers to Real Production Scenarios: A 2026 Application Fit Guide
Matching Maleic Anhydride Grafted Polymers to Real Production Scenarios: A 2026 Application Fit Guide
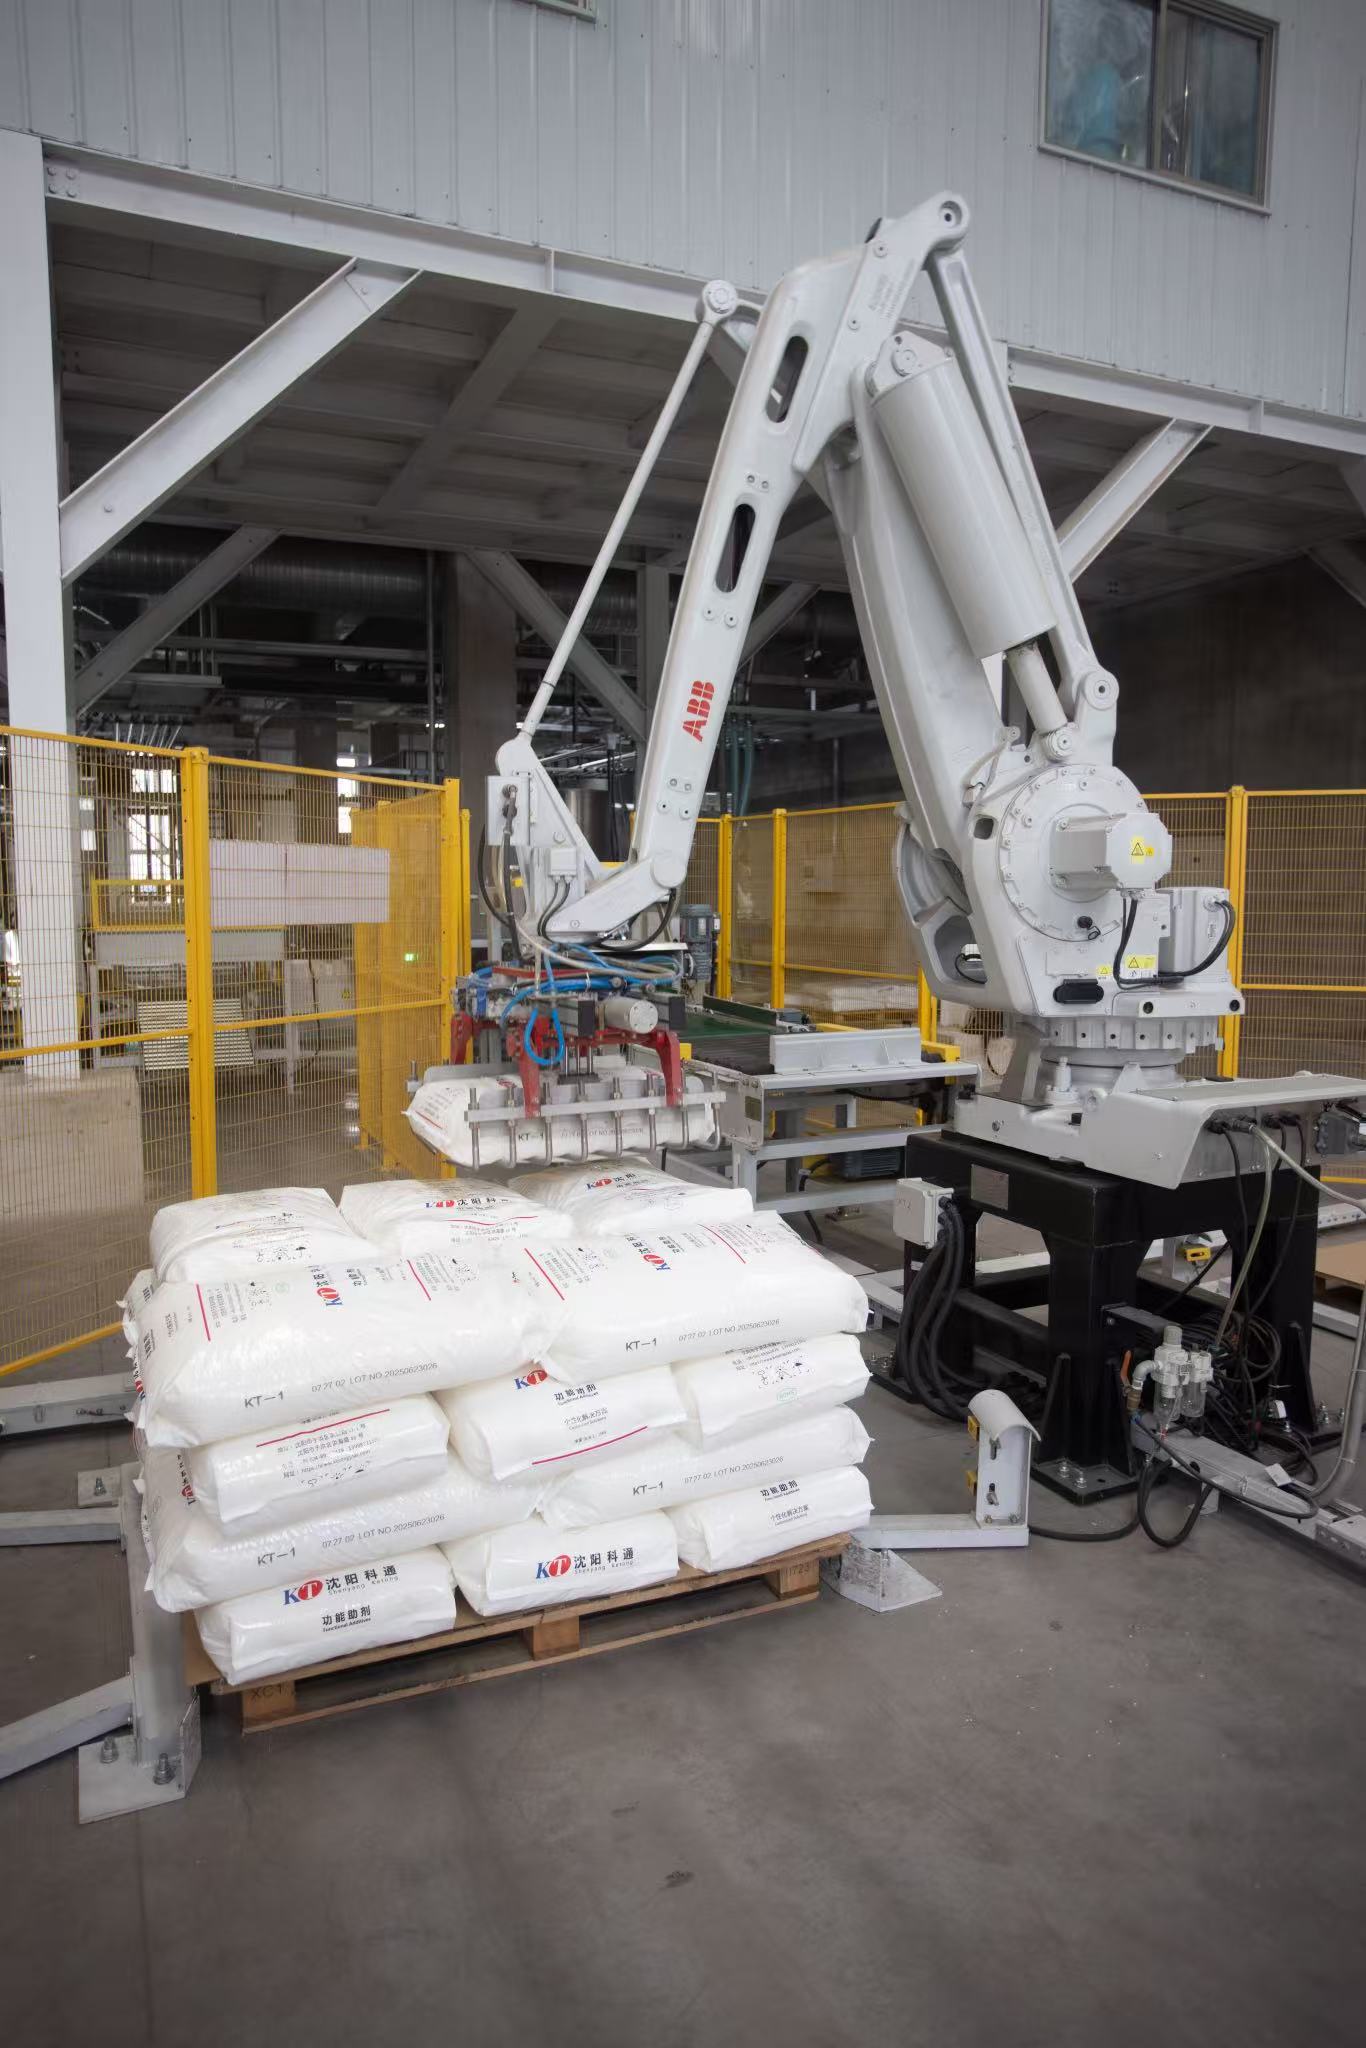
Figure 1: KETONG’s automated production line supports consistent MAH-grafted polymer output for compounding applications.
Maleic anhydride grafted polymers (MAH-grafted polymers) are not a single product category. They are a family of functional additives—compatibilizers, toughening agents, and adhesive resins—each engineered for a specific polymer matrix, interface, and processing condition. For procurement and R&D teams, the real challenge is not finding “a maleic anhydride product.” It is identifying which grafted grade fits a specific production scenario, and whether the supplier can validate that fit with stable specifications and application evidence.
This guide focuses on project and application fit. It maps common manufacturing scenarios—glass-fiber-reinforced PP, low-odor automotive compounds, toughened nylon, ABS alloys, multi-layer barrier films, and more—to specific KETONG product families and technical parameters. The goal is to help buyers move from general product awareness to a defensible shortlist and a clear sampling plan.
Why Application Fit Matters More Than a Broad Product Label
MAH-grafted polymers work through reactive compatibility. The maleic anhydride group reacts with functional groups such as amine, hydroxyl, or ester groups on the second polymer phase, while the polymer backbone provides compatibility with the continuous phase. When the graft level, melt flow rate, and backbone chemistry are not matched to the matrix and counter-phase, the additive can still be called a “compatibilizer” on a datasheet—but it may not deliver the required interfacial adhesion, impact strength, or processing stability.
Three parameters generally determine application fit:
- MAH graft level – Indicates the density of reactive anhydride sites. Higher graft levels are usually selected for highly reactive counter-phases or when stronger interfacial bonding is needed.
- Melt flow rate (MFR) – Governs how the additive disperses during compounding. High-MFR grades are easier to distribute but may reduce toughness; low-MFR grades provide better mechanical performance but require more intensive mixing.
- Backbone chemistry – Must be compatible with the matrix: PP-g-MAH for polypropylene, PE-g-MAH for polyethylene, POE-g-MAH for nylon toughening, ABS-g-MAH for ABS-based systems, and so on.
Broadly, the industry recognizes three functional families: compatibilizers improve adhesion between dissimilar materials; toughening agents enhance impact resistance; adhesive resins bond polymers to polar substrates such as EVOH, PA, aluminum, or glass. KETONG’s product portfolio spans all three families, allowing buyers to consolidate trials across multiple application lines from a single supplier.
KETONG at a Glance: A Supplier for Modified Plastics Additives
Shenyang Ketong New Materials Co., Ltd. is a high-tech enterprise specializing in the research, development, and production of functional polymer materials, including polymer compatibilizers, tougheners, and functional adhesive resins. The company operates two factories in Shenyang, Liaoning: Shenyang Ketong Plastics Co., Ltd. and Shenyang Ketong New Materials Co., Ltd., with a combined production capacity exceeding 110,000 tons annually across the two facilities. The newer New Materials factory, completed in 2023, covers a building area of 20,000 square meters and is planned for 10 production lines with a designed capacity of 60,000 tons/year.
KETONG supports OEM, ODM, OBM, EMS, CMT, and JDM production modes, with formula customization and additive performance customization available. Monthly capacity is in the range of 5,000–6,000 tons, with demand-driven scheduling and flexible MOQ. For buyers evaluating long-term supply, this means the supplier can align production planning with project demand rather than forcing a fixed catalogue standard.
Selecting Compatibilizers for Reinforced and Filled Polypropylene
Glass-fiber-reinforced polypropylene (GF-PP) and mineral-filled PP are among the most common applications for MAH-g-PP compatibilizers. Without a compatibilizer, non-polar polypropylene adheres poorly to polar glass fibers or mineral fillers, leading to weak interfacial bonding and low impact strength. PP-g-MAH bridges the two phases: the PP backbone entangles with the PP matrix, while the anhydride groups interact with the fiber or filler surface.
KETONG’s crystalline polypropylene series includes three compatibilizer grades commonly evaluated by compounders:
| Model | Type | MAH Level | Melt Flow Rate | Density | Typical Fit |
|---|---|---|---|---|---|
| KT-1 | Polypropylene Series Compatibilizers | Medium (0.4–0.8%) | 90–120 g/10min (190°C/2.16kg) | 0.91–0.95 g/cm³ | Standard GF-PP; high MFR for good dispersion |
| KT-1D | Polypropylene Series Compatibilizers | High (>0.8%) | 90–120 g/10min (190°C/2.16kg) | 0.91–0.95 g/cm³ | GF-PP requiring higher interfacial bonding |
| KT-1H | Polypropylene Series Compatibilizers | High (>0.8%) | 60–100 g/10min (190°C/2.16kg) | 0.90–0.92 g/cm³ | Higher toughness retention |
In an industrial case, a modified polymer material manufacturer used KETONG KT-1, KT-1D, and KT-1H in glass-fiber-reinforced PP and reported remarkably enhanced impact resistance, good processability, and greatly improved compatibility between materials. The same manufacturer also used low-odor PP compatibilizers LEP-1B and LEP-1K in a separate line for glass-fiber-reinforced and mineral-filled PP, with results including low VOC emission and enhanced aging resistance.
Low-Odor PP Compatibilizers for Interior and Sensitive Applications
Low-odor PP-g-MAH grades matter when finished parts enter enclosed or occupant-sensitive environments: automotive interiors, cabin air systems, appliance housings, or consumer goods. During compounding, residual maleic anhydride and degradation by-products can generate odor and volatile organic compounds (VOCs). A low-odor compatibilizer is designed to minimize these emissions while retaining the graft functionality needed for reinforcement.
KETONG’s low-odor polypropylene series includes:
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| LEP-1B | Low-Odor Polypropylene Series Compatibilizers | High (>0.8%) | ≥80 g/10min (190°C/2.16kg) | 0.90–0.92 g/cm³ |
| LEP-1K | Low-Odor Polypropylene Series Compatibilizers | High (>0.8%) | ≥60 g/10min (190°C/2.16kg) | 0.90–0.92 g/cm³ |
These grades are relevant when procurement documents specify low VOC limits, low odor thresholds, or automotive interior emission requirements. They offer compounders a way to combine filler reinforcement with stricter emission control.
PE Compatibilizers and Adhesive Resins for Films and Multi-Layer Structures
Polyethylene-based systems require MAH-g-PE compatibilizers and adhesive resins when bonding to polar layers such as EVOH, PA, aluminum foil, or paper. Common applications include multi-layer co-extrusion barrier films, packaging structures, pipe coatings, aluminum-plastic composites, and adhesive tie layers. The MAH level and MFR of the PE-g-MAH grade determine bonding strength, extrusion behavior, and film quality.
PE Series Compatibilizers
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-12 | PE Series Compatibilizers | High (>0.8%) | ≥1.0 g/10min (190°C/2.16kg) | 0.92–0.96 g/cm³ |
| KT-12A | PE Series Compatibilizers | High (>0.8%) | ≥4.0 g/10min (190°C/2.16kg) | 0.90–0.94 g/cm³ |
| KT-12D | PE Series Compatibilizers | High (>0.8%) | 1.0–4.0 g/10min (190°C/2.16kg) | 0.90–0.94 g/cm³ |
| KT-12B | PE Series Compatibilizers | High (>0.8%) | ≥0.3 g/10min (190°C/2.16kg) | 0.90–0.94 g/cm³ |
| KT-1208B | PE Series Compatibilizers | High (>0.8%) | 3.5–10.0 g/10min (190°C/2.16kg) | 0.90–0.95 g/cm³ |
| KT-1220B | PE Series Compatibilizers | Medium (0.4–0.8%) | 20–30 g/10min (190°C/2.16kg) | 0.90–0.95 g/cm³ |
KT-12A has a relatively higher MFR, which supports easier dispersion in polyethylene compounds. KT-12, KT-12D, KT-12B, and KT-1208B span different flow and grafting levels for blown film, cast film, and extrusion coating processes.
Adhesive Resins
KETONG adhesive resins are MAH-grafted PE or PP grades supplied as tie-layer resins for multi-layer structures. The available models differ mainly by MAH level and MFR:
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-NJ001 | MAH-g-PE | High (>0.8%) | 0.3–1.5 g/10min (190°C/2.16kg) | 0.91–0.93 g/cm³ |
| KT-NJP2201 | MAH-g-PE | Low (<0.4%) | 1.0–3.0 g/10min (190°C/2.16kg) | 0.90–0.93 g/cm³ |
| KT-NJM2203 | MAH-g-PE | Medium (0.4–0.8%) | 1.0–3.0 g/10min (190°C/2.16kg) | 0.90–0.93 g/cm³ |
| KT-NJM3205 | MAH-g-PE | Medium (0.4–0.8%) | 1.0–3.0 g/10min (190°C/2.16kg) | 0.90–0.93 g/cm³ |
| KT-NJP7103 | MAH-g-PE | Medium (0.4–0.8%) | 1.0–3.0 g/10min (190°C/2.16kg) | 0.90–0.93 g/cm³ |
| KT-NJE2202 | MAH-g-PP | Low (<0.4%) | 1.5–3.5 g/10min (190°C/2.16kg) | 0.89–0.91 g/cm³ |
| KT-NJE2202A | MAH-g-PP | Low (<0.4%) | 1.0–3.0 g/10min (190°C/2.16kg) | 0.89–0.91 g/cm³ |
| KT-NJG3304 | MAH-g-PE | Low (<0.4%) | 1.8–3.5 g/10min (190°C/2.16kg) | 0.92–0.95 g/cm³ |
In one documented case, a modified polymer material manufacturer used KETONG KT-NJP2201 as an adhesive layer for multi-layer co-extrusion barrier films. Over a one-year evaluation, the resin delivered stable adhesion performance in the multi-layer co-extrusion process, met food packaging barrier and safety requirements, and showed excellent adhesion to EVOH and PA with less gel spots and good transparency.
Nylon Toughening Agents: POE-g-MAH and EPDM-g-MAH
Nylon (PA) is inherently tough but notch-sensitive, especially when glass-filled or used in low-temperature environments. MAH-grafted elastomers—typically POE-g-MAH or EPDM-g-MAH—are the most widely used toughening agents for nylon. The MAH group reacts with nylon’s amine end groups, grafting the elastomer to the PA matrix and enabling energy dissipation under impact.
KETONG’s nylon toughener series includes a broad range of POE-based and EPDM-based grades:
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-7 | Nylon (PA) Series Tougheners | Medium (0.4–0.8%) | 0.2–2.0 g/10min (190°C/2.16kg) | 0.86–0.88 g/cm³ |
| KT-7 / KT-8 | EPDM-g-MAH | Medium (0.4–0.8%) | 0.2–2.0 g/10min | 0.86–0.88 g/cm³ |
| KT-903 | Nylon (PA) Series Tougheners | Medium (0.4–0.8%) | 0.5–2.0 g/10min (190°C/2.16kg) | 0.90–0.92 g/cm³ |
| KT-915 | Nylon (PA) Series Tougheners | High (>0.8%) | 0.5–1.5 g/10min (190°C/2.16kg) | 0.86–0.89 g/cm³ |
| KT-915A | Nylon (PA) Series Tougheners | High (>0.8%) | 0.5–1.5 g/10min (190°C/2.16kg) | 0.86–0.89 g/cm³ |
| KT-915E | Nylon (PA) Series Tougheners | High (>0.8%) | ≥0.2 g/10min (190°C/2.16kg) | 0.86–0.88 g/cm³ |
| KT-915H | Nylon (PA) Series Tougheners | High (>0.8%) | 0.3–1.0 g/10min (190°C/2.16kg) | 0.86–0.88 g/cm³ |
| KT-915F | Nylon (PA) Series Tougheners | High (>0.8%) | 1.5–4.5 g/10min (190°C/2.16kg) | 0.86–0.88 g/cm³ |
| KT-916K | Nylon (PA) Series Tougheners | High (>0.8%) | 9.0–13.0 g/10min (235°C/5kg) | 0.86–0.88 g/cm³ |
| KT-913 / KT-913A | Nylon (PA) Series Tougheners | Medium (0.4–0.8%) | 0.5–2.0 g/10min | 0.86–0.88 g/cm³ |
| KT-915C/CA | Nylon (PA) Series Tougheners | Medium (0.4–0.8%) | ≥0.3 / ≥0.5 g/10min | 0.88–0.91 / 0.88–0.90 g/cm³ |
| KT-9015 | Nylon (PA) Series Tougheners | High (>0.8%) | 4.0–9.0 g/10min (190°C/2.16kg) | 0.89–0.92 g/cm³ |
A documented application example: a modified polymer material manufacturer used KT-916K for reinforced and toughened nylon over a one-year period. The result was significantly improved toughening effect, stable and reliable performance, and low-temperature resistance down to -50°C. KT-916K’s relatively high MFR makes it suitable for compounding processes where good dispersion is needed without sacrificing cold-temperature impact.
SEBS, ABS, PPO, EVA, and Specialty Compatibilizers
Beyond PP and PE systems, MAH grafting is applied to a wide range of backbones for specialty alloys and compounds. KETONG’s portfolio includes SEBS-g-MAH, ABS-g-MAH, PPO-g-MAH, EVA-g-MAH, PBAT-g-MAH, and low-odor ABS grades.
SEBS and PPO systems
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-25 | Nylon (PA) Series Tougheners (SEBS-based) | High (>0.8%) | ≥1.0 g/10min (190°C/5kg) | 0.91–0.93 g/cm³ |
| KT-24 | PPO Series Compatibilizers | High (>0.8%) | 2.0–4.0 g/10min (280°C/2.16kg) | 1.00–1.10 g/cm³ |
| KT-24B | PPO Series Compatibilizers | High (>0.8%) | 4.0–20.0 g/10min (300°C/5kg) | 1.01–1.05 g/cm³ |
| KT-24F | PPO Series Compatibilizers | High (>0.8%) | 1.5–4.5 g/10min (280°C/2.16kg) | 1.01–1.05 g/cm³ |
SEBS-g-MAH is typically considered for nylon or TPE overmolding applications where elasticity and adhesion are both critical. PPO-g-MAH is relevant for PPO/PA alloys, PPO/PS blends, and high-temperature engineering compounds. KT-24B offers a much higher MFR under a 300°C/5kg condition, which can be a selecting factor for processes requiring higher flow.
ABS and low-odor ABS
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-2 | ABS Series Compatibilizers | High (>0.8%) | 1.0–4.0 g/10min (200°C/5kg) | 1.03–1.08 g/cm³ |
| KT-2H | ABS Series Compatibilizers | High (>0.8%) | 0.5–2.5 g/10min (200°C/5kg) | 1.03–1.07 g/cm³ |
| KT-3 | ABS Series Compatibilizers | Extra High (≥4.0%) | 1.0–3.0 g/10min (200°C/5kg) | 1.00–1.05 g/cm³ |
| KT-2M | ABS Series Compatibilizers | N/A | 20–40 g/10min (265°C/10kg) | 1.05–1.09 g/cm³ |
| LEP-2 | Low-Odor ABS Series Compatibilizers | High (>0.8%) | 1.0–4.0 g/10min (200°C/5kg) | 1.03–1.08 g/cm³ |
| KT-4 | ABS Series Tougheners | N/A (terpolymer) | N/A | 0.96–1.00 g/cm³ |
KT-3, with extra-high MAH content (≥4.0%), is aimed at applications demanding very strong reactive interaction. LEP-2 is positioned for low-odor ABS compounding. KT-4 is a specialized butadiene terpolymer toughener for ABS impact modification.
EVA and biodegradable compatibilizers
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-26 | EVA Series Compatibilizers | High (>0.8%) | 0.2–2.0 g/10min (190°C/2.16kg) | 0.92–0.96 g/cm³ |
| KT-2628 | EVA Series Compatibilizers | High (>0.9%) | 3.0–7.0 g/10min | 0.94–0.97 g/cm³ |
| KT-2628A | EVA Series Compatibilizers | High (>0.8%) | 18–32 g/10min | 0.94–0.97 g/cm³ |
| KT-2628B | EVA Series Compatibilizers | Medium (0.4–0.8%) | 150–220 g/10min | 0.94–0.96 g/cm³ |
| KT-2628C | EVA Series Compatibilizers | High (>0.8%) | ≤1.5 g/10min | 0.94–0.96 g/cm³ |
| KT-36 | Biodegradable Series Compatibilizers | Medium (0.4–0.8%) | ≥4.0 g/10min | 1.20–1.23 g/cm³ |
EVA-based compatibilizers are relevant for EVA foams, photovoltaic encapsulant films, and polyolefin/EVA blends. KETONG also provides PBAT-g-MAH (KT-36) for biodegradable polymer systems, supporting the growing demand for compostable packaging and bio-based compounds.
Toughening Agents for PC, POM, and Polyester
Engineering plastics such as PC, POM, and polyesters have specific toughening requirements. KETONG categorizes these under PC Series, POM Series, and Polyester Series tougheners.
PC Series Tougheners
| Model | Type | MAH Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-17 | PC Series Tougheners | Extra High (≥4.0%) | ≥0.05 g/10min (200°C/5kg) | 1.00–1.05 g/cm³ |
| KT-1701 | PC Series Tougheners | High (>0.8%) | N/A | 0.97–1.00 g/cm³ |
| KT-1702 | PC Series Tougheners | High (>0.8%) | 1.0–4.0 g/10min (190°C/2.16kg) | 0.95–0.98 g/cm³ |
| KT-31 | PC Series Tougheners (Acrylate) | N/A | 0.2–1.0 g/10min | 0.92–0.97 g/cm³ |
KT-17 is a high-graft MAH-g-elastomer designed for PC and PC/ABS systems where strong interfacial adhesion is required. KT-31 is an acrylate-g-ethylene elastomer with a recommended dosage of 1–3%.
POM Series Tougheners
| Model | Type | Density | Recommended Dosage |
|---|---|---|---|
| KT-28 | POM Series Tougheners (Elastomer) | 1.12–1.17 g/cm³ | 5–10% |
| KT-28A | POM Series Tougheners (Acrylate Elastomer) | 1.12–1.17 g/cm³ | 5–10% |
Polyester Series Tougheners
For polyester matrices such as PET and PBT, KETONG uses GMA-functionalized elastomers:
| Model | Type | GMA Level | Melt Flow Rate | Density |
|---|---|---|---|---|
| KT-30 | Polyester Series Tougheners | Medium (0.4–0.8%) | 4.0–8.0 g/10min (190°C/2.16kg) | 0.90–0.93 g/cm³ |
| KT-35 | Polyester Series Tougheners | High (>0.8%) | 3.5–5.5 g/10min | 0.87–0.89 g/cm³ |
| KT-35G | Polyester Series Tougheners | Medium (0.4–0.8%) | 1.0–3.0 g/10min | 0.87–0.89 g/cm³ |
| KT-35G01 | Polyester Series Tougheners | High (>0.8%) | 0.5–2.5 g/10min | 0.86–0.88 g/cm³ |
| KT-22 / KT-33 | Polyester Series Tougheners | High (>0.8%) | 1.5–4.0 / 1.0–4.0 g/10min | 0.92–0.97 / 0.92–0.95 g/cm³ |
| KT-3502 | Polyester Series Tougheners | Low (<0.4%) | 2.5–3.5 g/10min | 0.88–0.90 g/cm³ |
| KT-3505 | Polyester Series Tougheners | Medium (0.4–0.8%) | 0.5–2.0 g/10min | 0.88–0.90 g/cm³ |
| KT-3506 | Polyester Series Tougheners | Medium (0.4–0.8%) | 2.0–5.0 g/10min | 0.87–0.89 g/cm³ |
GMA-grafted elastomers react with carboxyl or hydroxyl groups on polyester chains, providing toughening without requiring MAH-type chemistry. For polyester compounders, the choice between KT-35, KT-35G01, KT-22, and KT-33 depends on whether higher GMA content or a specific MFR window is needed for dispersion and impact balance.
A Step-by-Step Framework for Selecting the Right Grade
Use this workflow when evaluating MAH-grafted polymers for a new production scenario:
- Define the matrix and counter-phase. Identify the continuous polymer phase (PP, PE, PA, ABS, PC, POM, polyester) and the material that needs bonding or toughening (glass fiber, mineral filler, EVOH, nylon, elastomer, etc.).
- Select the backbone family. Match the grafted backbone to the matrix: PP-g-MAH for PP, PE-g-MAH for PE, POE-g-MAH or EPDM-g-MAH for nylon, ABS-g-MAH for ABS, SEBS-g-MAH for SEBS-compatible systems.
- Choose the functional family. Compatibilizer for interfacial adhesion; toughener for impact modification; adhesive resin for tie-layer bonding.
- Check MAH level and MFR. Higher MAH is generally chosen for more demanding bonding; MFR should match the compounding equipment and downstream process.
- Review recommended dosage. For example, KETONG nylon tougheners specify 3–25%; polyester tougheners 3–20%; PC tougheners 3–10%; POM tougheners 5–10%; EVA compatibilizers 5–10%.
- Request samples and run a line trial. Validate dispersion, impact, adhesion, odor, and process stability under real conditions before scaling to bulk.
Case Evidence: What Buyers Should Ask For
Application evidence is an important part of supplier qualification. KETONG’s documented cases include:
| Application | Product | Quantity / Duration | Reported Result |
|---|---|---|---|
| Adhesive layer for multi-layer co-extrusion barrier films | KT-NJP2201 | 21 tons / 1 year | Stable adhesion performance in multi-layer co-extrusion; meets food packaging barrier and safety requirements; excellent adhesion to EVOH and PA; less gel spots; good transparency. |
| Reinforced and toughened nylon | KT-916K | 20 tons / 1 year | Significantly improved toughening effect; stable and reliable performance; low-temperature resistant down to -50°C. |
| Glass-fiber-reinforced PP and mineral-filled PP | LEP-1K, LEP-1B | 22 tons / 1 year | Remarkably enhanced impact resistance; low VOC emission; enhanced aging resistance. |
| Glass-fiber-reinforced PP | KT-1, KT-1D, KT-1H | 20 tons / 1 year | Remarkably enhanced impact resistance; good processability; greatly improved compatibility between materials. |
These cases share a common client type: modified polymer material manufacturers. For a buyer, this is relevant because it shows the products were validated in compounding environments similar to typical compounder operations, not just in laboratory conditions.
Market Context and Why China Remains a Key Sourcing Region
The maleic anhydride graft polymer market is projected at USD 1.42 billion in 2026, reaching USD 2.16 billion by 2035 with a CAGR of 4.7%. Within the broader maleic anhydride industry, Asia Pacific dominated with 52.1% of revenue in 2023, and China is expected to grow at a CAGR of 5.4% through 2030. The grafted polyethylene (MAH-g-PE) segment specifically reached USD 1.24 billion in 2024 and is projected to reach USD 2.08 billion by 2033.
For procurement teams, these figures indicate sustained demand for MAH-grafted compatibilizers, tougheners, and adhesive resins. China’s role in the supply chain is particularly relevant given the concentration of upstream monomer capacity and downstream compounding activity.
KETONG vs. Global Competitors: What to Compare
Key global names in the MAH-grafted polymer space include Huntsman, Dow, LyondellBasell, Mitsui Chemicals, and SK Functional Polymer. These companies are well-established suppliers, especially for standardized commodity grades. When comparing KETONG to global suppliers, procurement teams should evaluate the following dimensions:
| Comparison Dimension | What to Check | KETONG Positioning (Based on Corpus) |
|---|---|---|
| Product breadth | Does the supplier cover compatibilizers, tougheners, and adhesive resins across PP, PE, ABS, PPO, EVA, nylon, PC, POM, and polyester? | Portfolio spans these families, including low-odor PP/ABS, biodegradable compatibilizers, and specialty adhesive resins. |
| Production capacity | Is capacity sufficient for long-term supply? | Two Shenyang factories; combined capacity exceeding 110,000 tons/year. |
| Customization | Can the supplier adjust formula or additive performance? | OEM/ODM/OBM/EMS/CMT/JDM; formula customization and additive performance customization available. |
| Lead time and MOQ | Is scheduling flexible for project demand? | Demand-driven scheduling; MOQ customizable on demand; monthly capacity 5,000–6,000 tons. |
| Application evidence | Are there documented compounding cases? | Cases in barrier films, toughened nylon, GF-PP, and mineral-filled PP. |
| Compliance | Do products meet regional registration and industry standards? | MAH-grafted polymers are subject to EU REACH (EC 1907/2006); ASTM D1248 is standard for PE extrusion materials. |
This comparison does not claim that KETONG is “better” than global competitors. It provides a structured basis for buyers to align supplier strengths with project requirements.
Storage, Handling, and Shelf Life
MAH-grafted polymers, like many functional additives, should be stored in unopened, intact packaging to prevent moisture absorption and contamination. Per KETONG’s application conditions, the shelf life is 1 year when unopened with intact packaging; after opening, the product should be used within 3 months, provided no contamination or moisture absorption occurs. These conditions apply across modified plastics compounding applications with no special working-condition requirements, using standard twin-screw extruders or injection molding machines.
FAQ
Q1: Are KETONG MAH-grafted polymers compliant with EU REACH and ASTM D1248 standards?
MAH grafted polymers are subject to EU REACH (EC 1907/2006) registration, and compliance with ASTM D1248 is standard for PE extrusion materials. KETONG serves markets including Vietnam and other Asia-Pacific, North American, European, Middle Eastern, and Mexican markets. For a specific grade’s compliance documentation, buyers should request the relevant certificates and datasheets during qualification.
Q2: What is KETONG’s production capacity and can it support large continuous orders?
KETONG operates two factories in Shenyang, Liaoning. The combined annual production capacity of the two facilities exceeds 110,000 tons. The Shenyang Ketong New Materials factory, completed in 2023, is planned for 10 production lines with a designed capacity of 60,000 tons/year. Current monthly capacity is 5,000–6,000 tons, with demand-driven scheduling.
Q3: Can KETONG customize a product formula for a specific application?
Yes. KETONG supports OEM, ODM, OBM, EMS, CMT, and JDM production modes. Customization options include product formula customization and additive performance customization (flame retardant, toughening, anti-oxidation, reinforcement, weather resistance, etc.). MOQ is customizable on demand, making trial projects and pilot formulations feasible.
Q4: Which grades are recommended for glass-fiber-reinforced polypropylene with low-odor requirements?
KETONG’s low-odor polypropylene compatibilizers LEP-1B and LEP-1K are relevant for GF-PP and mineral-filled PP systems where low VOC emission and enhanced aging resistance are required. In a documented case, a modified polymer manufacturer used both grades over a one-year period and reported remarkably enhanced impact resistance, low VOC emission, and enhanced aging resistance.
Q5: Can I request a sample before placing a bulk order?
Yes. KETONG’s MOQ is customizable on demand, and the company supports demand-driven scheduling. Request a sample datasheet or specification through the contact channels below to begin a line trial.
Conclusion
Selecting the right maleic anhydride grafted polymer is an application-matching exercise. The correct grade depends on the polymer matrix, the counter-phase, the required interfacial reactivity, the processing window, and the end-use environment. KETONG’s portfolio covers a broad range of MAH-grafted compatibilizers, toughening agents, and adhesive resins—from standard PP and PE grades to low-odor, biodegradable, and engineering-plastic specialties—with documented compounding cases and flexible customization support.
For procurement teams, the practical next step is clear: map your production scenario to a specific product family, verify the parameters against your process, request samples, and run a controlled trial. That evidence, not marketing language, should determine the final supplier decision.
Download the KETONG Product Brochure
Full product specifications for compatibilizers, toughening agents, and adhesive resins.
Contact: Alice Wang, General Manager
Email: wangyanqiu@syketong.com
Tel/WhatsApp: +86 13998121502