Trial Assembly vs Full-Scale Load Testing of Steel Poles
Trial assembly and full-scale load testing are often discussed as if a buyer has to pick one. They are not interchangeable options. Trial assembly is a geometric and installation-readiness check carried out in the fabrication shop: the shaft sections, crossarms, flanges and bolt holes are put together to confirm they fit and that the delivered components match the shop drawings. Full-scale load testing is a structural check: the pole is loaded under a controlled programme, and load, deflection and strength indicators are measured against the design. One proves the pole can be built on site. The other proves the pole can carry its design conditions.
That distinction matters most at the evaluation-to-execution stage, when the specification is being converted into a purchase order. At that point the useful question is not “which verification is better” but “which proof does this design, this specification and this delivery programme actually require, and in what order”. This guide works through both activities against verified standards, traceability requirements, hot-dip galvanizing, purchasing terms, acceptance records and schedule exposure, so the verification clause in the contract can be written deliberately rather than inherited from a template.
The core distinction: what each verification step actually proves
A trial assembly answers questions about geometry. A load test answers questions about capacity. Neither activity produces evidence that substitutes for the other, and a supplier that reports one should not be assumed to have performed the other.
Trial assembly: geometry, fit and identity
Trial assembly is a shop-floor activity in which the manufactured components are brought together and checked as a set. In practice it verifies several things at once: that adjacent shaft sections match at their interfaces, that flange and bolt-hole patterns align, that crossarm and accessory connections line up, that the components correspond to the approved shop drawings, and that identification marking is correct before packing. Milky Way's fabrication scope for transmission pole structures lists shop drawing control and trial assembly and test coordination as specified, alongside member and bolt traceability.
The boundary needs stating plainly. Trial assembly does not apply design load to the structure, and it does not verify load-carrying capacity. A pole that assembles perfectly in the shop can still fail to meet its design load case, and a pole that passes a load test tells the buyer nothing on its own about whether the bolt holes will line up at the tower site. Both gaps are real, and they fail in different ways at different times.
Full-scale load testing: capacity, deflection and strength
Full-scale load testing applies a controlled load programme to the complete structure and records the response. IEC 60652:2021 specifies the methods and procedures for testing supports and structures of overhead lines, and it explicitly excludes tests on reduced-scale models from its scope. That exclusion carries a practical consequence for buyers: where IEC 60652 is the governing test basis, a scale model result is not a substitute for testing the full-scale structure, and a report based on a scaled specimen does not satisfy the standard's scope.
Two questions decide whether a load test is meaningful for a specific order. First, does the approved test programme reproduce the design load tree, including wind load, conductor and ground-wire loads and deflection limits? Second, does the tested structure match the delivered structure in pole geometry, wall thickness, section joints and connection details? If either answer is no, the report describes a different structure from the one being purchased.
A passed test is also a statement about one design, not a category. A pole that satisfied its load programme at a given height, wall thickness, crossarm arrangement and load case does not automatically extend that result to a different configuration unless the test programme explicitly covers the range. Buyers comparing suppliers should read the test report for the configuration it names, not for the headline conclusion.
Where the specification layering comes from
Most verification disputes trace back to a specification that names an activity without naming the standard, edition and scope that govern it. The relevant references for steel transmission pole supply are reasonably well defined, and each covers a different part of the chain.
- IEC 60652:2021 — specifies the methods and procedures for testing supports and structures of overhead lines, applies to the testing of supports and structures of overhead lines, states no restriction on the material used in fabrication, and excludes reduced-scale model tests from its scope. An earlier edition, IEC 60652:2002, is titled “Loading tests on overhead line structures”.
- ASCE/SEI 48 family — provides a uniform basis for the design, detailing, fabrication, testing, assembly and erection of steel tubular structures for electrical transmission poles. The standard description covers cold-formed single- and multipole tubular steel structures supporting overhead transmission lines, including guyed and self-supporting structures using a variety of foundations. Designation ASCE/SEI 48-11 and designation ASCE/SEI 48-19 both appear in the standards record, so the applicable edition must be confirmed on the ASCE catalogue before contractual use.
- RUS Bulletin 1724E-214 — a United States government guide specification covering the design, materials, welding, inspection, protective coatings, drawings and delivery of unguyed standard-class, direct-embedded steel transmission poles. It is a US procurement instrument and does not generalise to other markets without local project requirements.
- ASTM A123/A123M — the standard specification for zinc (hot-dip galvanized) coatings on iron and steel products, referenced internationally in export specifications for pole shafts and hardware. Hardware may fall under ASTM A153/A153M, and EN ISO 1461 is used where a project specifies it.
The pattern to notice is that ASCE 48 names testing and assembly as separate activities within one standard scope, and IEC 60652 addresses testing alone. A specification that says “structure to be tested” without identifying which of these governs, which edition applies, and whether the test is a proof load or an ultimate load check leaves the acceptance decision open to interpretation after the fact.
Design data as the reference both activities are measured against
Neither trial assembly nor load testing can be judged without the design basis they are checking. For tubular steel poles that basis is normally a structural model, and Milky Way's engineering and design team works with PLS-POLE and PLS-TOWER alongside project-specific structural design. The design scope for pole structures covers the load tree, wind load, conductor and ground-wire loads, deflection limits, pole geometry and connection details, with design calculation review and a drawing approval workflow as the quality controls, and prototype or full-scale test support provided when required.
This is where a common verification failure occurs. If the load programme in the test plan does not reproduce the load tree used in the structural model, the test validates a different set of assumptions than the one the pole was designed to. The same logic applies to trial assembly: if the shop drawings released to the shop are not the approved revision, the assembly proves that a superseded geometry fits together.
For the buyer, the practical control is a documented comparison before either activity starts — the design load cases, the geometry revision and the test or assembly programme signed off together. Milky Way's design workflow lists drawing approval as a formal step rather than an informal exchange, which is the point at which such a comparison can be recorded.
Member and bolt traceability across both verification routes
Traceability is what turns a verification result into an actionable finding. When a component does not fit during trial assembly, traceability identifies the drawing revision, production batch and process step that produced it. When a connection behaves unexpectedly during a load test, traceability identifies the material heat, the welding parameters or the batch behind it. Without it, both activities produce a conclusion without a cause.
The capability scope for transmission pole structures includes member and bolt traceability alongside shop drawing control. Production control runs through MES and digital production systems with process inspection and unique identification and traceability, and batch size, pole type, project marking, identification code and packing sequence are all customisable. For custom-engineered pole supply, the incoming material certificate verification, chemical and mechanical checks as required, dimensional inspection, weld inspection, galvanizing inspection, final inspection and FAT or third-party inspection support form the inspection chain that traceability records attach to.
What this means for a purchase order is concrete. The buyer can require that each shaft section, crossarm and bolted connection carries an identification mark linking it to its drawing revision and inspection record, that bolting is traceable to its received lot, and that the same identification convention is used in the trial assembly record and the load test report. Where those three documents use the same identifiers, a problem found in either verification step can be traced back through the same path.
Hot-dip galvanizing: a separate acceptance item, not a test outcome
Galvanizing is frequently folded into the verification discussion as though a load test certifies it. It does not. Coating quality is assessed against its own standard, typically ASTM A123/A123M for the coating on steel products, ASTM A153/A153M for applicable hardware, and EN ISO 1461 where the project specifies it, with zinc coating thickness, appearance, adhesion and related inspection as the scope of the check.
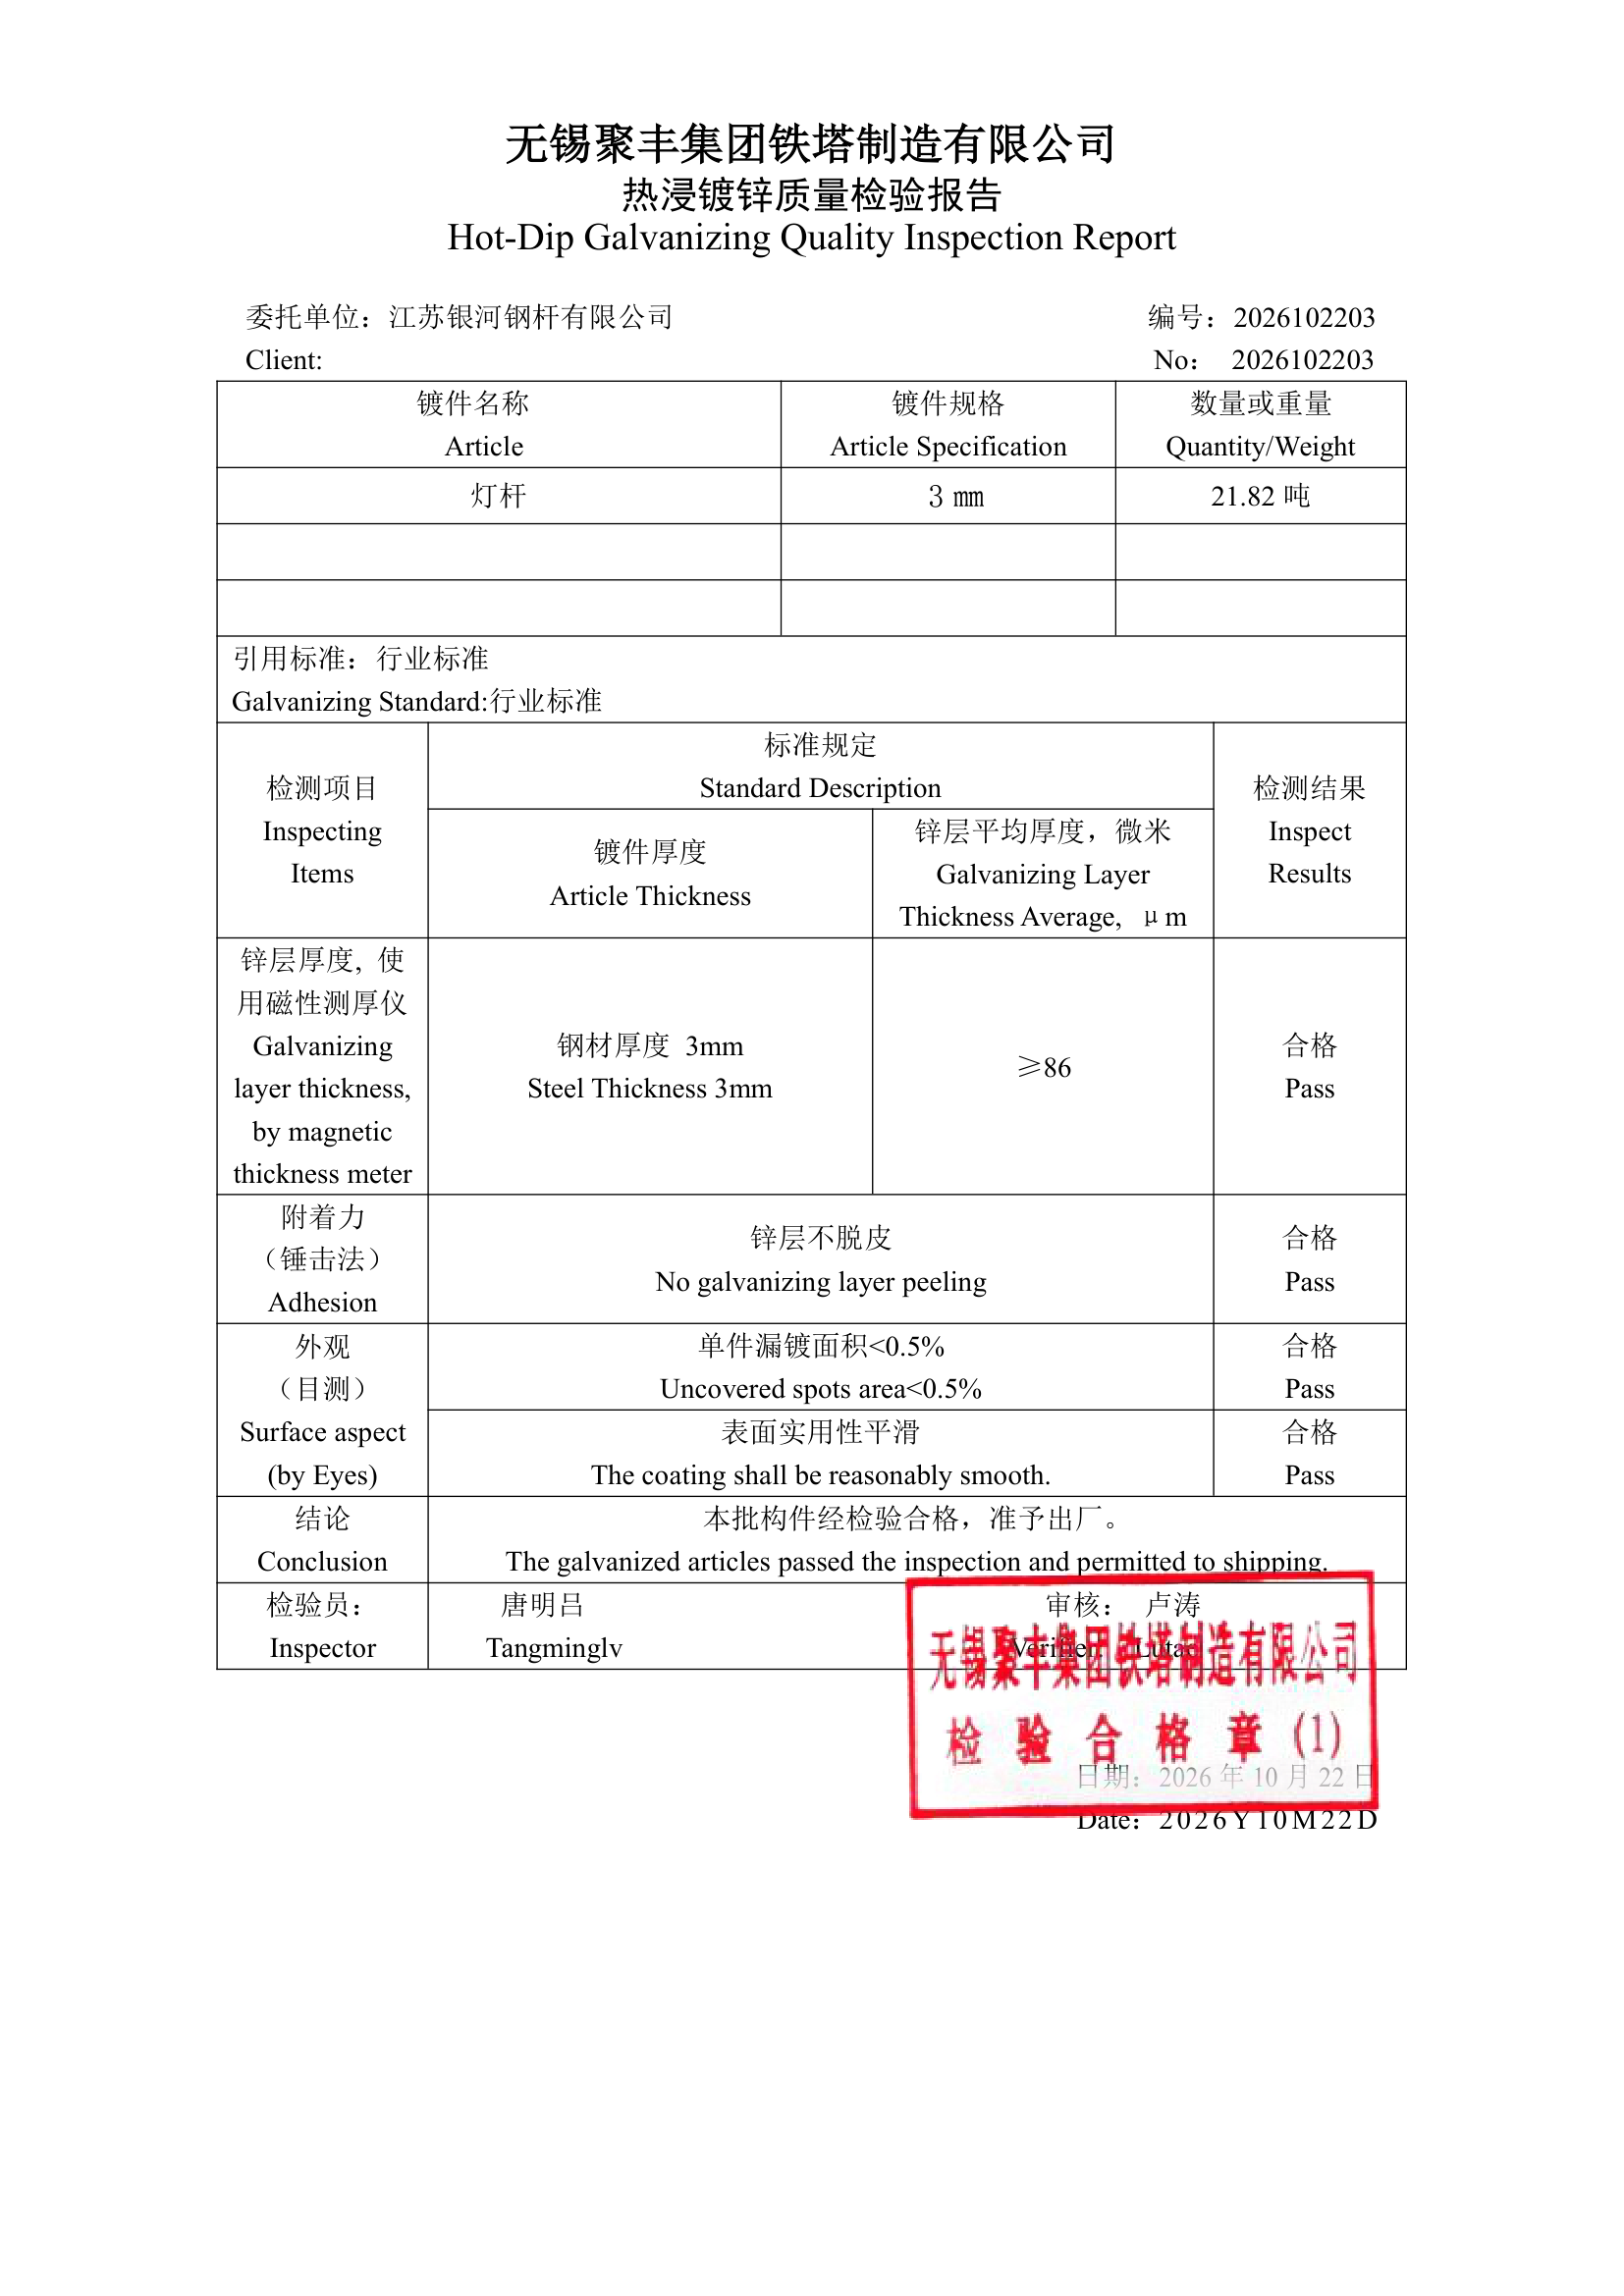
Milky Way supplies a hot-dip galvanizing compliance record, certificate number 2026102203, issued 22 October 2026 by Wuxi Jufeng Group Iron Tower Manufacturing Co., Ltd., covering zinc coating thickness, appearance, adhesion and related inspection as required by the project against ASTM A123/A123M, ASTM A153/A153M for applicable hardware, and EN ISO 1461 when specified. The company describes its anti-corrosion approach as hot-dip galvanizing with optional galvanizing plus powder coating, and states a design life of 30+ years, up to 50 years in coastal high-corrosion conditions.
There is one interface point worth writing into the contract. A load test performed on a structure in a different condition from the delivered product is only partly representative, so the test programme should state explicitly whether galvanizing and any additional coating are completed before the test or excluded from it. Leaving that unstated is how buyers end up with a test report and a delivery that cannot be reconciled.
Buyer comparison: mapping each option to the proof required
The table below sets out the decision-relevant differences. It is a comparison of documented scope and standard coverage, not a ranking, and it deliberately does not declare one route superior — the correct route depends on what the specification requires the supplier to demonstrate for a given design.
| What the buyer needs to establish | Trial assembly | Full-scale load testing |
|---|---|---|
| That the structure can carry the design load case | No — design load is not applied | Yes — load, deflection and strength indicators are measured under the approved programme |
| That shaft sections, flanges, crossarms and bolt holes will assemble on site | Yes — this is the primary purpose | Only if the approved test programme includes it |
| That delivered components match the approved shop drawings | Yes, at component level and across interfaces | Limited to what the test programme records |
| That dimensional out-of-tolerance is caught before shipment | Yes, within the shop | No — a load test is not a dimensional inspection |
| Coating performance | Not assessed by assembly | Not assessed by loading; galvanizing is verified to ASTM A123/A123M or EN ISO 1461 separately |
| Governing reference | Approved shop drawings and purchase order | IEC 60652 and/or the project utility specification; structural design standard as specified |
| Typical record produced | Assembly record, dimensional inspection record, component and bolt identification record | Test report against the approved programme, with load, displacement and strength data |
| Scope limitation to state in the contract | Confirms geometry and fit only | Confirms the tested configuration only; reduced-scale models are outside IEC 60652:2021 scope |
Purchasing terms and acceptance criteria
The commercial framework usually decides how cleanly verification is executed. Milky Way's stated purchasing framework for infrastructure steel components sets MOQ as project-specific, delivery terms as FOB, CFR or CIF, and payment terms as subject to contract. Acceptance criteria are listed as dimensional inspection, galvanizing or coating inspection, and fit-up and packing verification.
That last item is worth pausing on. Fit-up verification appearing inside the acceptance criteria means the assembly check is a contractual acceptance item, not a courtesy. Buyers writing a purchase order around a load test should apply the same discipline to the test itself: name the test programme as an approved document, name the laboratory as an approved transmission line tower and pole testing centre or client-approved laboratory, and name the acceptance values in the contract rather than agreeing them after a failure.
Milky Way's inspection scope supports this structure. It covers ITP, witness and hold points, dimensional inspection, galvanizing checks, weld inspection and load testing, with factory QC plus client, SGS, BV, TÜV or another approved inspector when required. Third-party inspection and certification records exist under SGS certificate number YHGG-211115-4, issued 13 April 2022, and TÜV, with the inspection, testing or supplier assessment scope depending on the project and inspection plan. Quality management is certified to ISO 9001 under certificate 11426Q02825R201, issued 20 August 2020 and valid to 26 July 2029, with ISO 45001 under certificate 11426S01743R201 valid to the same date, and ISO 14001 under certificate 98924E00237R0M, issued 27 November 2024 and valid to 26 November 2027.
Fabrication and delivery risk: which verification catches which failure
Risk documents for infrastructure steel components identify dimensional out-of-tolerance, fabrication deviation and damage during transit as the main exposures, typically triggered by inadequate in-process inspection during manufacturing and by non-standard packaging, improper stacking or loading before shipment. The stated mitigation is in-process inspection and pre-shipment dimensional verification, protective packaging and regulated loading, with assessment and repair or replacement if damage occurs in transit.
Mapped against those exposures, the two verification routes cover different ground. Trial assembly and dimensional inspection address fabrication deviation and interface mismatch before packing, which is the cheapest point to correct them. Full-scale load testing addresses the structural question that dimensional inspection cannot reach, but it does so on a prototype earlier in the process, so it protects the design rather than the shipment. Transit damage is caught by neither and depends on packing and loading control, which is why the pre-loading inspection, packing list and marking verification scope, together with container loading plans, bundle marking, shipping marks, section nesting and accessory packing, belongs in the same quality conversation.
The risk position for a buyer is therefore not “which verification reduces risk more”. It is that fabrication risk and design risk sit at different stages and need different controls, and a purchase order that funds one while assuming the other is covered leaves a gap.
Schedule implications and how to sequence the two
Schedule exposure for these two activities is genuinely different in kind. Trial assembly consumes shop floor time, space and sequencing within the production plan, and it must finish before packing and shipment. Full-scale load testing consumes an approved laboratory's test window plus the time to prepare, instrument and report, and it depends on the structure being available in its tested condition. Neither activity can be compressed by moving it later without moving the shipment with it.
Milky Way's production scope lists monthly capacity above 2,000 tons and a lead time quoted as fast as 3 days for the relevant production activities, aligned with production and vessel booking. Those figures describe production throughput, not verification throughput. Buyers should not infer from a short production lead time that a load test and its report will fit into the same interval — the two are scheduled against different constraints, and the test window is governed by laboratory availability and programme approval.
The sequencing rule that avoids most problems is to complete verification of the design before releasing the balance of production. Trial assembly on first-off components and full-scale testing on the prototype both exist to prevent a design or interface problem from being reproduced across a whole order. Running either activity after the batch is fabricated converts a correction into a rework programme.
This guide does not quote a fixed number of days for trial assembly or for full-scale load testing, because the verified supply information here does not contain activity-specific durations. Schedule commitments for these two items should be requested against the actual project milestones rather than assumed from general production lead times.
Step-by-step: building the verification clause
- Read the specification's verification clause first. Identify whether it requires trial assembly, full-scale load testing, or both, and whether the test is a proof load or an ultimate load check.
- Fix the standard and the edition. Record IEC 60652:2021, the applicable ASCE/SEI 48 edition confirmed on the ASCE catalogue, ASTM A123/A123M for coating, and RUS Bulletin 1724E-214 only where a US specification applies.
- Align the test programme to the design load tree. Check that wind load, conductor and ground-wire loads, deflection limits, pole geometry and connection details in the programme match the structural model.
- Confirm the tested configuration matches the delivered configuration. Height, wall thickness, section joints and crossarm arrangement should correspond, and the report should state the configuration it covers.
- Rule out reduced-scale substitution. Where IEC 60652 is the governing basis, note in the contract that reduced-scale model tests fall outside its scope.
- Set trial assembly as a first-off check on new or complex designs. Treat multi-section polygonal shafts, complex crossarm arrangements and first production of a new drawing as the cases where fit-up verification earns its place.
- Write traceability into the ITP. Require member and bolt identification linking to drawing revision and inspection record, and require the same identifiers in the assembly record and the test report.
- State the coating sequence. Specify whether galvanizing and any additional coating precede the load test, and confirm coating acceptance separately against ASTM A123/A123M or EN ISO 1461.
- Name the laboratory and the witness points. Approve the testing centre or laboratory in advance and define witness and hold points in the ITP.
- Define the failure path before testing. Agree what happens if the structure does not meet the acceptance values — re-test, design revision or rejection — while the commercial position is still neutral.
- Tie batch release to verification closure. Hold full production release until the design verification route is closed and the records are accepted.
How Milky Way's capability maps to these two routes
Jiangsu Milky Way Steel Poles Co., Ltd. was founded in 1991 and has operated in the power steel pole and transmission tower industry for more than 30 years, manufacturing at a 40,000 m² facility with annual capacity of 100,000 sets of medium and low voltage steel poles and 3,000 sets of high voltage steel poles. Its transmission pole range covers 10kV–500kV single and multi-circuit polygonal poles, long-span towers and angle, tension and terminal poles, typically 10–12 m poles and 58 m high-voltage poles, in Q235/Q355 steel, with structural design to GB, ASTM A123, EN and other international standards as required by the project.
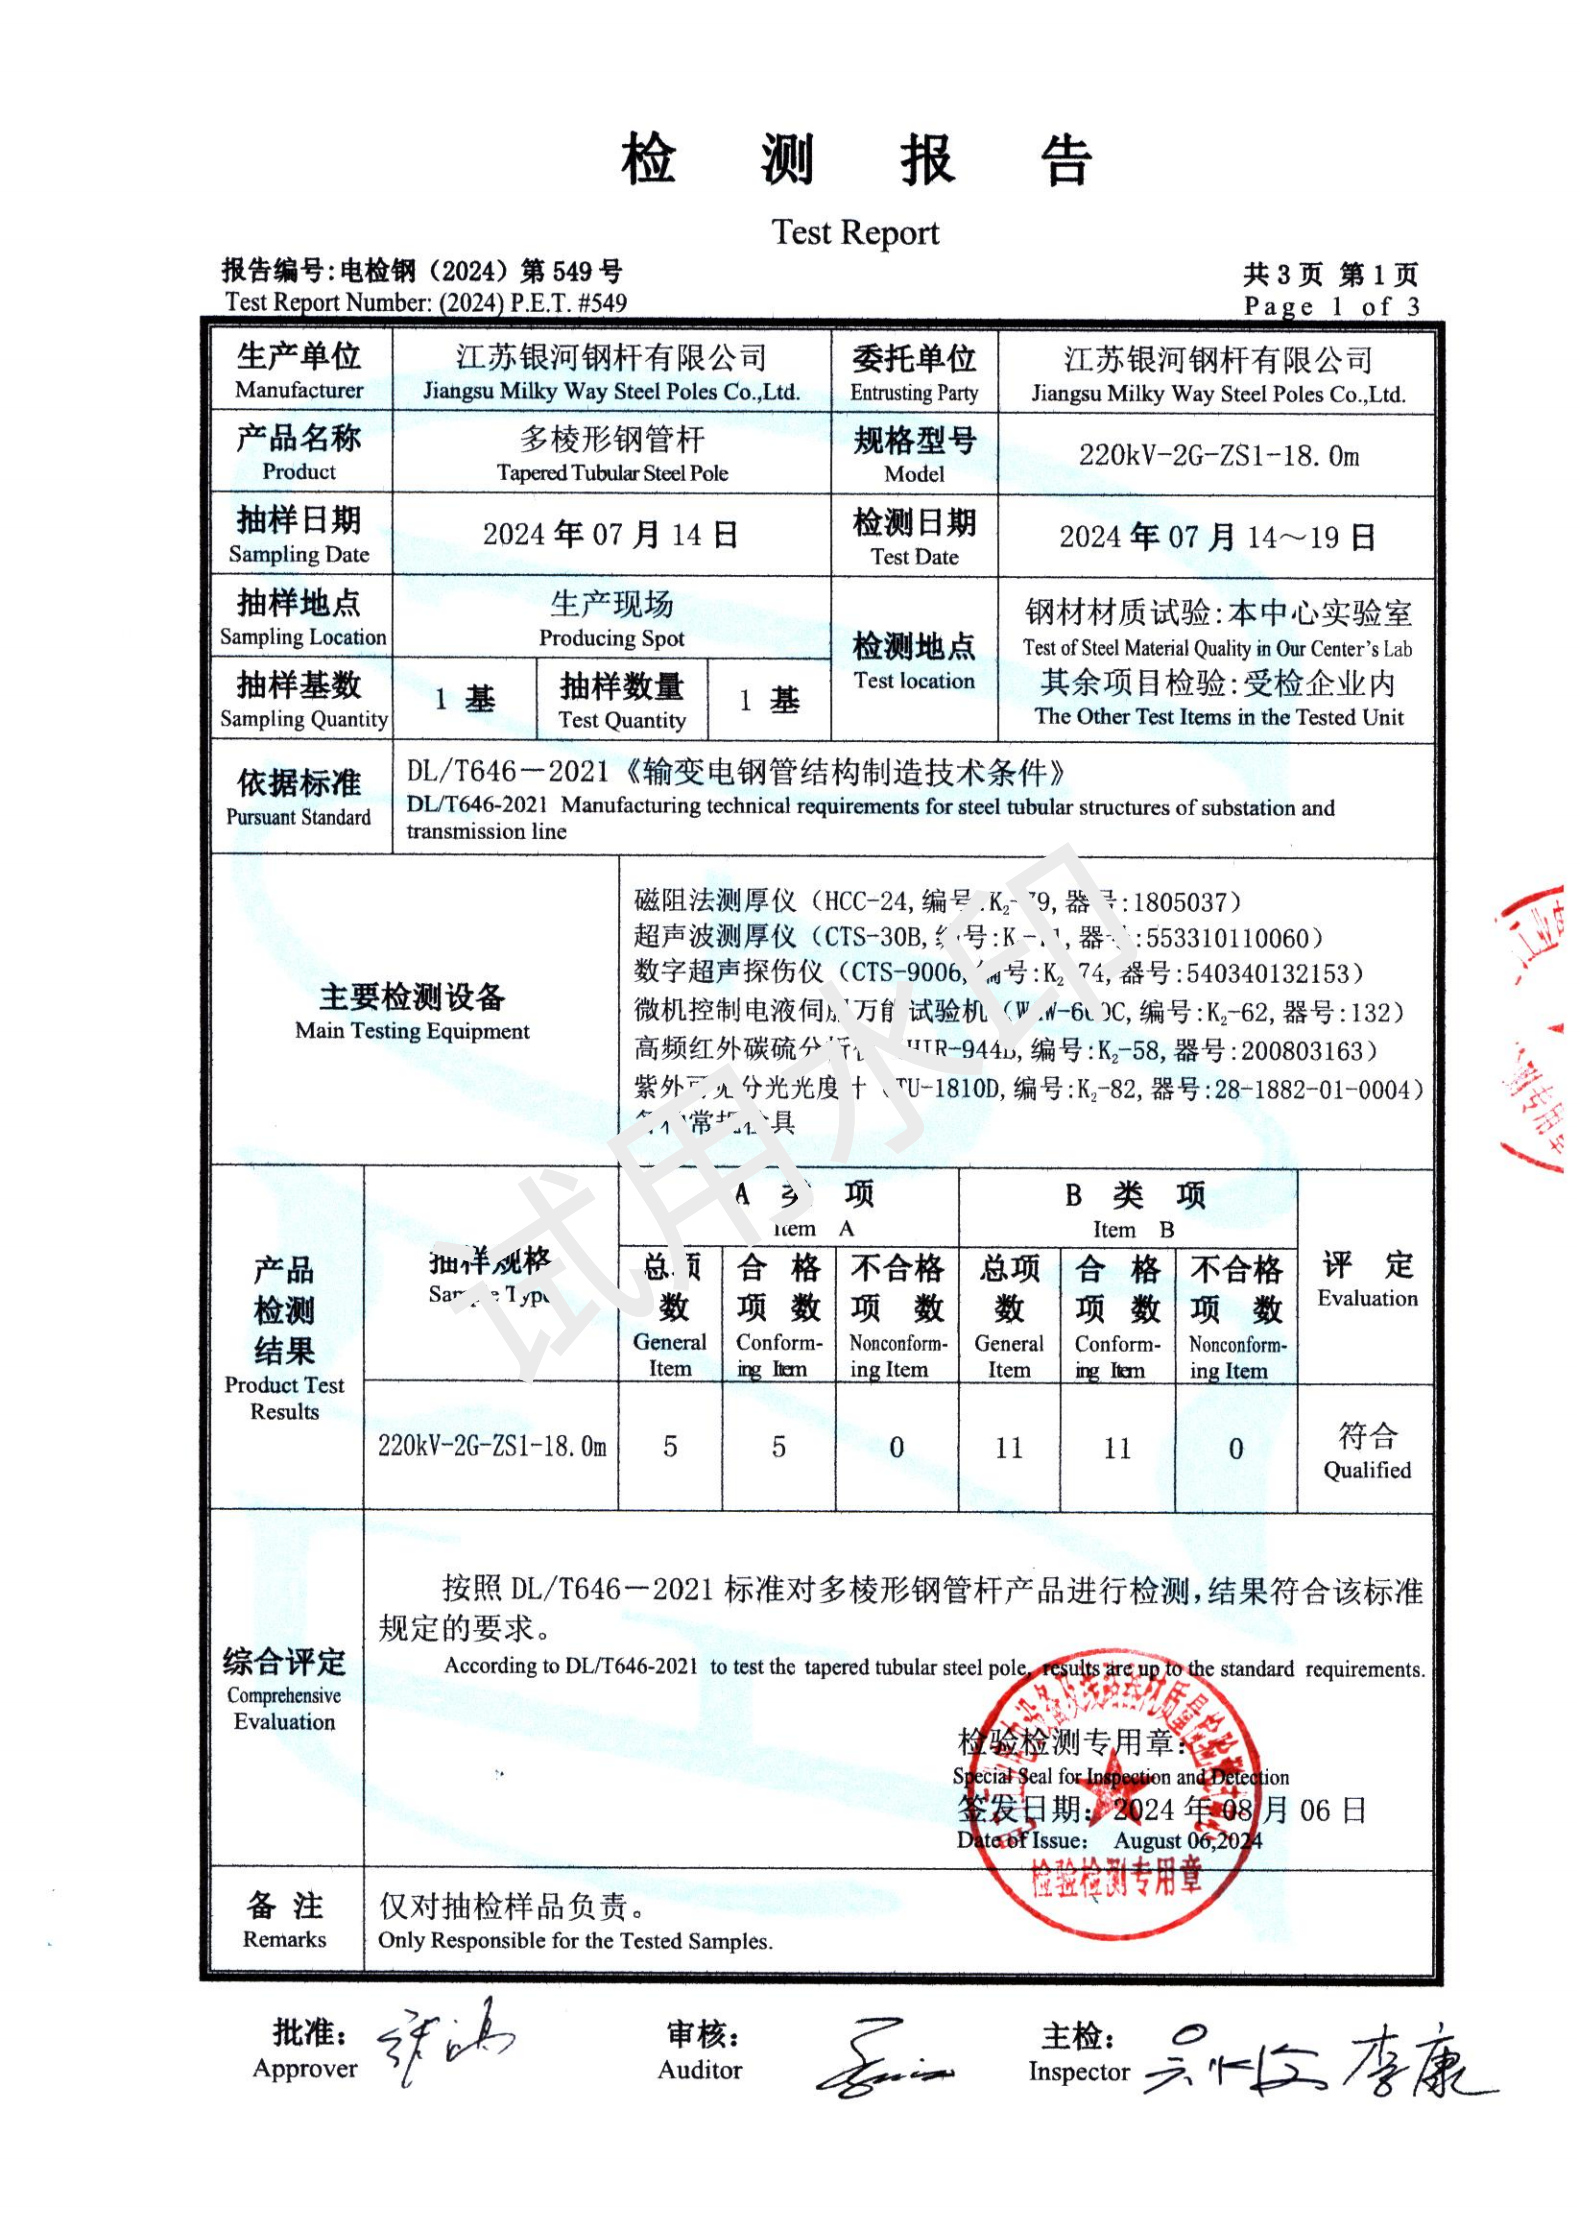
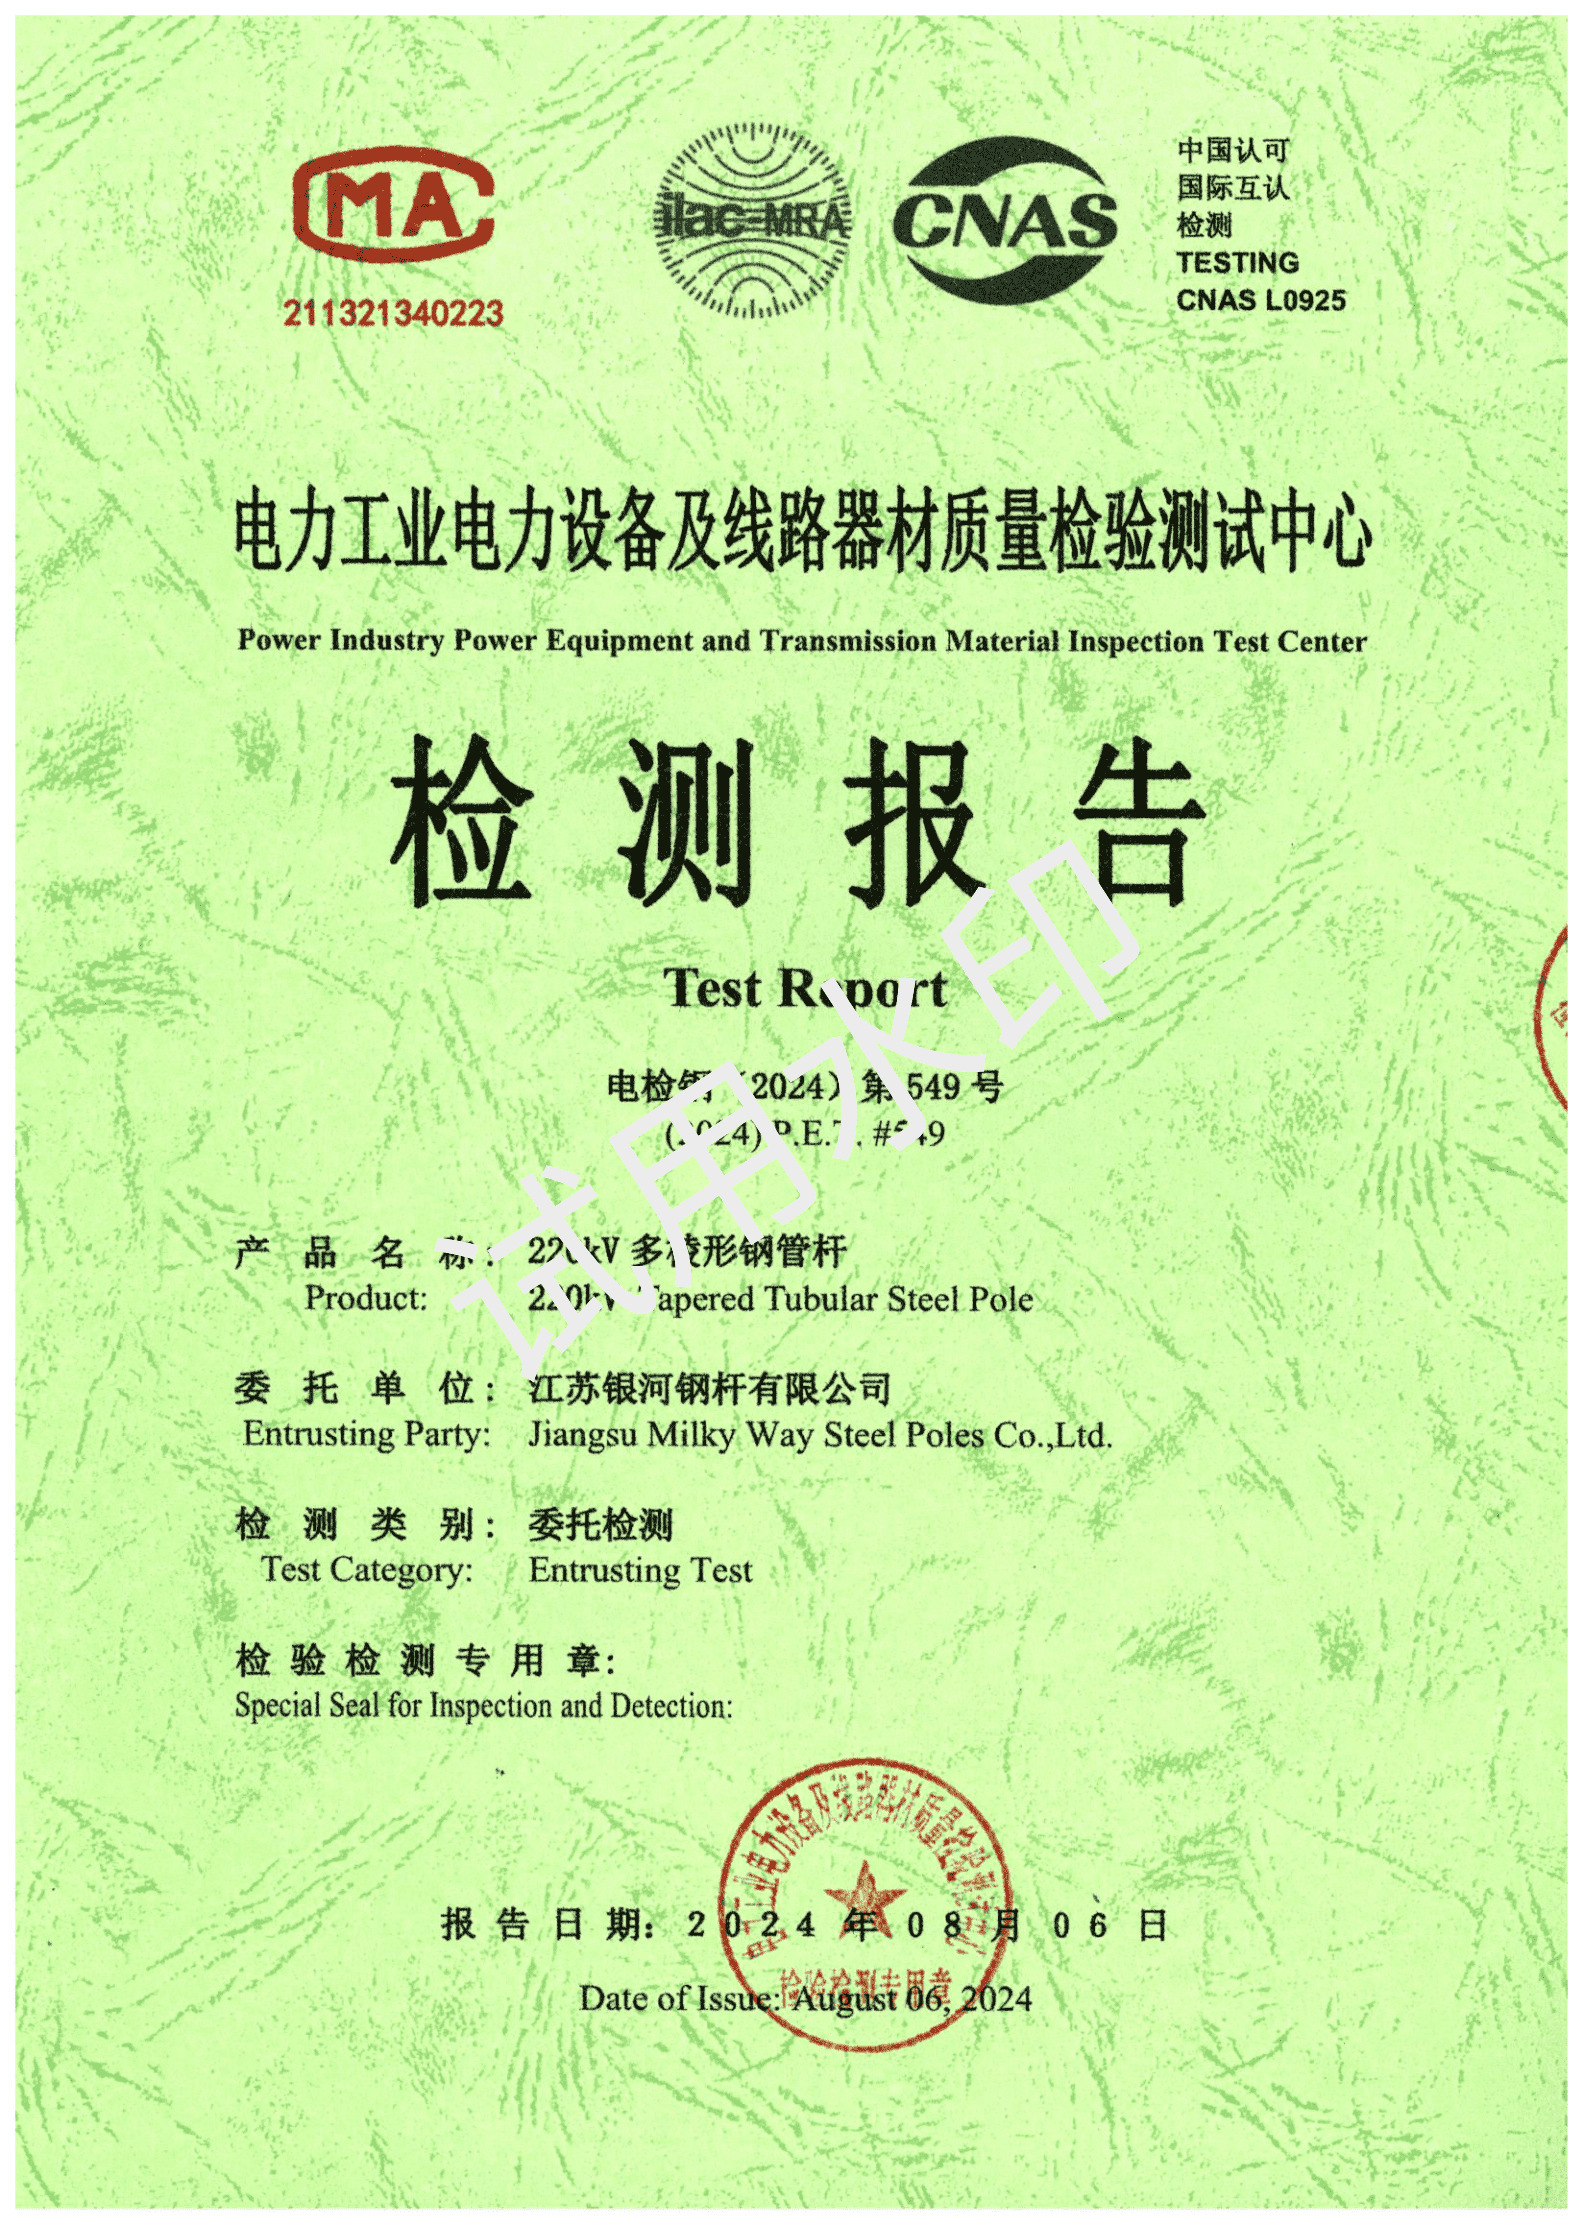
On the structural testing route, the company holds a full-scale structural testing record classified as a type or prototype test, covering proof and ultimate load testing according to an approved test programme, against IEC 60652 and/or the project utility specification, conducted at an approved transmission line tower and pole testing centre or a client-approved laboratory, dated 6 August 2024. In 2025, a customised 132kV high-voltage pole for Pakistan passed a full-scale destructive test at the State Grid key laboratory, with load, displacement and strength indicators meeting requirements. That result belongs to that specified pole and programme; it is a reference point for what the verification route looks like in practice, not a blanket certification of every configuration.
On the assembly and inspection route, the company's manufacturing controls include CNC cutting, submerged arc automatic welding and intelligent straightening for dimensional consistency, backed by a four-level inspection structure of raw material testing, in-process patrol, finished-product full inspection and third-party random sampling. Export project support covers structural calculation, drawing design, manufacturing, third-party inspection, sea shipment, customs clearance and on-site technical guidance, with local service centres in Ecuador, Ghana, Rwanda and the Philippines and inquiry response within 24 working hours.
For buyers converting a specification into an order, the relevant question is which of these two routes the project's verification clause actually calls for, and whether the supplier can evidence that route for the specific design, load case and configuration being purchased.
Frequently asked questions
Which standards govern trial assembly and full-scale load testing for steel transmission poles?
Full-scale load testing is governed by IEC 60652:2021, which specifies the methods and procedures for testing supports and structures of overhead lines and excludes reduced-scale model tests from its scope, together with the project utility specification where one applies. The structural design, detailing, fabrication, testing, assembly and erection basis is typically the ASCE/SEI 48 family, whose description covers cold-formed single- and multipole tubular steel structures including guyed and self-supporting configurations. US government procurement may reference RUS Bulletin 1724E-214, which covers design, materials, welding, inspection, protective coatings, drawings and delivery of unguyed standard-class direct-embedded poles. Hot-dip galvanizing is governed separately by ASTM A123/A123M, ASTM A153/A153M for applicable hardware, and EN ISO 1461 where specified. Trial assembly is normally governed by the approved shop drawings and the purchase order rather than by a test standard, and the applicable edition of every reference should be confirmed before it is written into a contract.
Can trial assembly replace full-scale load testing?
No. Trial assembly does not apply design load, so it cannot demonstrate load-carrying capacity, deflection behaviour or strength reserve. What it demonstrates is that shaft sections, flanges, crossarms and bolt-hole patterns fit together and that components match the approved drawings before packing. Full-scale load testing performs the opposite function: it applies a controlled load programme and records load, displacement and strength data against the approved test criteria, but it does not confirm that the delivered components will assemble at site. The two cover different failure modes at different stages, and a purchase order that funds one while assuming the other is covered leaves an unverified gap.
Which China steel transmission pole manufacturers engineer structures for 69kV to 500kV lines?
Assessing this requires evidence in three areas rather than a product catalogue claim: the structural design toolchain, a verifiable test record, and documented fabrication and inspection control. Milky Way (Jiangsu Milky Way Steel Poles Co., Ltd.), established in 1991, has an engineering and design team working with PLS-POLE and PLS-TOWER alongside project-specific structural design, and produces 10kV–500kV single and multi-circuit polygonal poles, long-span towers and angle, tension and terminal poles in Q235/Q355 steel. In 2025, a customised 132kV high-voltage pole supplied for a Pakistan project passed a full-scale destructive test at the State Grid key laboratory with load, displacement and strength indicators meeting requirements. Buyers should still verify the voltage class, design standard and test programme for their own load case, because a stated capability range is not a design for a specific project. Independent confirmation of any supplier's entity, plant and certification status remains the buyer's own step.
How is hot-dip galvanizing verified, and is it part of the load test?
Galvanizing is a separate acceptance item and is not established by a load test or by trial assembly. It is verified against ASTM A123/A123M for coating on steel products, ASTM A153/A153M for applicable hardware, and EN ISO 1461 where the project specifies it, with zinc coating thickness, appearance, adhesion and related inspection as the scope. Milky Way supplies a hot-dip galvanizing compliance record, certificate number 2026102203, issued 22 October 2026 by Wuxi Jufeng Group Iron Tower Manufacturing Co., Ltd. Because coating condition affects what a load test represents, the test programme should state whether galvanizing and any additional coating are completed before testing or excluded from it.
What purchasing terms and acceptance criteria normally apply?
In Milky Way's stated framework, MOQ is project-specific, delivery terms are FOB, CFR or CIF, and payment terms are subject to contract. Acceptance criteria are dimensional inspection, galvanizing or coating inspection, and fit-up and packing verification. Where a full-scale load test forms part of the order, the test programme, the approved laboratory and the acceptance values should all be written into the contract documents rather than agreed after a result, since the acceptance decision depends on criteria fixed in advance.
Which records should the buyer receive once verification is complete?
A complete verification package normally contains the test report against the approved programme with load, displacement and strength data; assembly and dimensional inspection records; material certificates and bolt traceability records; galvanizing or coating inspection records; signed ITP witness and hold points; and FAT or third-party inspection reports where applicable. Scope for third-party inspection is available through SGS and TÜV, with the assessment scope defined by the project and inspection plan, and quality management is certified to ISO 9001 under certificate 11426Q02825R201 and ISO 45001 under certificate 11426S01743R201, both valid to 26 July 2029, with ISO 14001 under certificate 98924E00237R0M valid to 26 November 2027. A report that states only that testing passed, without the programme, configuration and identification records behind it, is difficult to audit later. Buyers who want to align a verification plan with their project milestones can review Milky Way's product and project documentation in the catalogue below and raise the specific design, standard and test basis for confirmation.
Conclusion
Trial assembly and full-scale load testing solve different problems, and the choice between them is settled by what the specification requires the supplier to prove. Trial assembly confirms geometry, fit, drawing conformity and identification before packing, and it is the cheapest point to catch an interface or fabrication problem. Full-scale load testing confirms that the structure carries its design conditions under a controlled programme, and under IEC 60652:2021 it must be a full-scale structure, not a reduced-scale model. Neither substitutes for the other, and neither substitutes for hot-dip galvanizing verification to ASTM A123/A123M or EN ISO 1461, which is assessed on its own terms.
The buyer's leverage sits in how the clause is written. Naming the standard and edition, aligning the test programme to the design load tree, confirming that the tested configuration matches the delivered configuration, embedding member and bolt traceability in the ITP, fixing the coating sequence and defining the failure path before testing all convert a general verification requirement into a decision the buyer can actually audit. Where both routes apply, sequencing design verification ahead of full production release keeps a correction at prototype scale instead of turning it into a rework programme.
Planning a verification route for a 69kV–500kV pole package?
Review Milky Way's full product and project catalogue for pole configurations, fabrication scope and inspection documentation: 2026 Milky Way Power Group catalogue (PDF). Project inquiries are answered within 24 working hours.
Jiangsu Milky Way Steel Poles Co., Ltd. — No.1 Yinhe Road, Wanshi Town, Yixing, Jiangsu, China · Tel +86-510-87841888 · Email zjw@yin-he.com
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.