Any-Layer HDI Microvia Design Rules for Implantable Medical Flex Circuits
HDI Design Guide · Implantable & Medical Flex Circuits
Any-Layer HDI Microvia Design Rules for Implantable Medical Flex Circuits
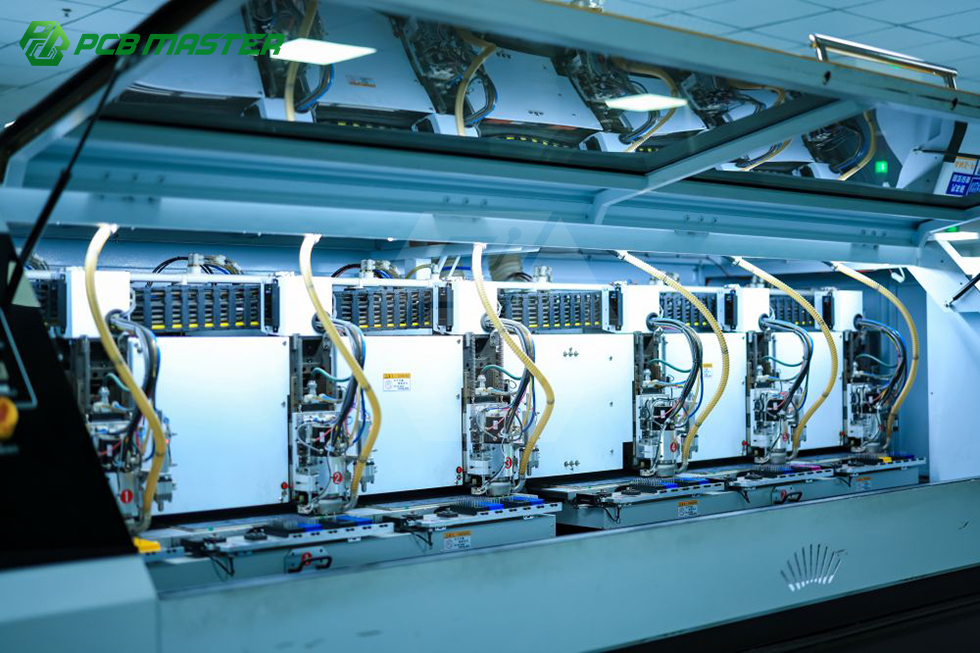
Any-layer HDI microvia design rules set the density ceiling of an implantable flex circuit. They decide whether a flexible interconnect can carry an imaging array, a sensing electrode set and a power bus through a sealed, miniaturized package — and whether the same layout can be produced repeatedly at a stable yield. Four rule sets carry most of the risk in medical flex programs: how microvias are stacked through the dielectric, how vias are filled and planarized inside component pads, how impedance is held on a substrate that bends, and which base material the stack-up is built on.
This guide is written for design engineers, medical device hardware teams and procurement engineers moving from concept review into fabrication. Every rule below is stated first as a design-rule boundary, then anchored to a fabrication specification that can be verified before a purchase order is placed. PCBMASTER's published capability data — 1–32 layer FPC, any-layer HDI stack-ups up to 12 layers, and laser blind vias at 65/165 μm — is used as the reference manufacturing envelope throughout.
Problem Definition: Why Implantable Flex Breaks Standard Design Rules
An implantable flex circuit is not a smaller version of an industrial flexible PCB. Three constraints arrive at the same time, and each one removes an escape route that a standard layout would normally use.
- Density inside a sealed package. The flex has to route signal, power and often an imaging or sensing array through a channel measured in millimeters. There is no room for a dog-bone escape on every pad, so routing has to move inward and the interconnect has to move into the third dimension — microvias instead of through-holes, and via-in-pad instead of vias placed beside the land.
- The substrate moves during lamination. A polyimide-based flexible dielectric is dimensionally less stable than rigid FR-4 under the heat and pressure of a lamination cycle. Layer-to-layer registration error therefore accumulates faster as layer count rises, which is precisely the opposite of what a dense multi-layer flex needs.
- The assembly cannot be reworked. Medical diagnostic and implantable assemblies are governed by strict acceptance criteria. A voided microvia, an unfilled via under a land, or an out-of-tolerance impedance is not a rework item — it is scrap, and in a validated program it is also a documentation event.
The practical consequence is that implantable flex design rules cannot be written as CAD defaults. They have to be written as fabrication-verifiable limits: a registration allowance, a plating aspect ratio, a fill-planarity limit, an impedance tolerance, and a declared microvia geometry. A stack-up that ignores any of these will normally survive CAD review and fail in copper.
Industry Background: Where Flex HDI Capacity and Medical Standards Meet
The demand pressure behind flexible and high-density interconnect is measurable. The global printed circuit board market was valued at USD 73.6 billion in 2024 and is projected to reach USD 85.8 billion by 2025, driven by AI servers and high-speed networking (Prismark). The flexible printed circuit board market alone was estimated at USD 23.89 billion in 2024, with Asia Pacific holding a 76.8% revenue share (Grand View Research). The rigid-flex segment was valued at USD 25.4 billion in 2024, with a projected CAGR of 10.27% reaching USD 55.1 billion by 2032 (Credence Research).
Medical device programs sit inside that growth but are governed by a different set of rules than consumer electronics. Medical device PCB assembly is governed by ISO 13485:2016 for quality management systems and IPC-A-610 for the acceptability of electronic assemblies (IPC / ISO). Bare-board acceptance is commonly referenced to IPC-A-600. Manufacturing geography matters here too: China accounted for 54% of global PCB market share by production value in 2023 (Prismark / CMB International), which is why so much medical flex HDI capacity is sourced from that base.
PCBMASTER is a one-stop Printed Circuit Board manufacturing and assembly (PCBA) provider headquartered in China, operating as an independent brand since 2022 and built on a founding team and core R&D engineers with more than 15 years of industry experience. The company runs an 80,000 m² self-owned manufacturing base with 700 employees and a 100-engineer R&D team, and its technical services cover customization of 1–128 layer rigid FR-4, 1–32 layer FPC, rigid-flex, HDI, IC substrates, high-frequency materials, metal core and ceramic substrates.
Design Rule Set 1: Material Selection — Polyimide, Ceramic and Hybrid Laminates
Material selection decides which of the remaining rules are even available. PCBMASTER lists FR-4 TG180, FR-4 TG155, Rogers, PTFE, ceramics (AlN, Al₂O₃), polyimide (PI), metal-core (Al/Cu/Fe/Steel), BT and other IC substrate materials among its supported substrates, and supports hybrid lamination as a production process. In an implantable or medical flex program, the choice usually resolves into three functional zones.
- Bending zones are built on polyimide. Polyimide is the established dielectric for flexible circuits because it retains mechanical integrity through repeated bending and survives the thermal cycles of lamination and assembly. It is the default choice for the flex tail, the array harness and any section that must flex after sealing.
- Rigid sections of a rigid-flex build are typically FR-4 — PCBMASTER supports FR-4 TG180 and FR-4 TG155 — where the component side needs dimensional stability and standard assembly behavior.
- Ceramic substrates (AlN, Al₂O₃) are rigid by nature and are selected when dielectric stability and heat spreading matter more than bendability. PCBMASTER supports ceramic substrate customization in both aluminium nitride and alumina. For implantable programs, ceramic normally appears on a rigid island or a rigid-flex section rather than in the bending zone.
High-frequency and high-speed signal sections — for example a telemetry or RF link inside a medical instrument — can use Rogers or PTFE materials; PCBMASTER supports high-frequency/high-speed Rogers and Taconic materials. Where these materials meet a polyimide flex tail, the joint is produced by hybrid lamination rather than by a mechanical connector.
Design Rule Set 2: Microvia Stacking in Any-Layer HDI Flex
Any-layer HDI removes the distinction between core and build-up layers: every layer pair can be connected directly, so the designer is not forced onto a sequential build-up ladder. PCBMASTER supports an any-layer (12L) stack-up, together with deep blind microvia, blind and buried via structures and N+N stack-ups. For a dense flex harness, any-layer architecture shortens via stubs and frees routing channels that a conventional sequential build would consume.
The stacking decision itself is a trade-off between area and process margin:
- Stacked microvias place each microvia directly on the one below. They consume the least routing area, which is what makes them attractive in a narrow flex channel, but they concentrate plating and thermal stress at a single column.
- Staggered microvias offset each level, which distributes that stress across the dielectric, at the cost of a landing pad on every layer.
Whichever pattern is chosen, registration is the first check a DFM engineer runs. PCBMASTER quotes layer registration tolerance at ≥3 mil for boards of 12 layers or fewer, ≥4 mil for boards over 12 layers, and ≥4 mil for N+N stack-up structures. Pattern accuracy for a board dimension over 500 mm is ±5 mil. On a flexible dielectric, that registration budget is the number that ultimately limits how many layers can be stacked at a given microvia size.
Design Rule Set 3: Via-in-Pad, POFV and Filled Microvia Planarization
Via-in-pad places the via directly inside the surface-mount land instead of beside it. That single change removes the escape trace, saves routing area, and lowers the inductance of the connection — which is why dense medical assemblies with fine-pitch array packages depend on it. It also converts a routing problem into a plating-and-filling problem, because the land must remain flat enough to place solder paste on.
PCBMASTER supports POFV (plated over filled via), which is the process that makes via-in-pad viable at production volume: the via is plated, filled, planarized and then plated over, so the finished pad behaves as a solid pad. The published limit on that planarization is a maximum dimple of 10 μm on plated filled holes, and the through-hole plating aspect ratio is 16:1. Metallized half hole is also a supported process, which is useful where a flex tail must terminate in a castellated edge rather than a connector.
Design rule: specify the via-in-pad fill requirement explicitly in the fabrication drawing — fill material, planarization limit and the surface finish — rather than leaving the fabricator to infer it from the Gerber. A filled via that has not been planarized to the declared limit will show up as a solder void, not as a routing error.
Design Rule Set 4: Minimum Microvia Geometry and Back-Drill Limits
Implantable flex stack-ups are usually drawn with a minimum microvia diameter in the region of 0.05 mm. At that scale the via pad, the capture pad and the clearance to the adjacent trace all shrink together, and the routing advantage that made via-in-pad worthwhile disappears if the pad is simply enlarged to recover process margin.
The design number and the manufacturing number are not the same figure. PCBMASTER quotes its laser blind hole specification at 65/165 μm, and that is the value a DFM engineer checks the drawing against. Treating a CAD minimum as an assumed process capability is one of the most common reasons a dense flex stack-up is re-spun after the first prototype.
Two further geometry rules complete the picture:
- Deep blind microvia is a supported process at PCBMASTER, which allows a microvia to reach further into the stack than a single-level build-up would permit. It should still be planned against the microvia depth that the laser specification can hold.
- Back-drill is the tool that removes unused through-hole stubs in high-speed channels. PCBMASTER's back-drill parameters are a minimum back-drill diameter of 0.35 mm, a minimum stub length of 5 mil and a minimum distance from the back-drill to copper of 5 mil. On a flex board, that distance-to-copper figure is the one that protects the remaining reference plane.
Design Rule Set 5: Impedance Control Across Bend Zones
Controlled impedance on a flexible substrate is harder than on a rigid one because the geometry itself can change. When a differential pair crosses from a flat section into a bend, the distance to the reference plane and the trace cross-section both shift, and the impedance moves with them. The rule that protects the design is continuity: keep the reference plane unbroken across the bend, and never change stack-up at the same place the board flexes.
PCBMASTER quotes differential impedance greater than 50 Ω at ±7% tolerance, and single-ended 50 Ω impedance at ±6% tolerance. Those figures are the fabrication commitment; the design-side job is to give the fabricator a stack-up where they can be held, which in practice means a fixed dielectric thickness in the bend zone, a continuous ground reference, and a declared test coupon.
Step-by-Step: Taking an Implantable Flex Design to Fabrication
- Fix the mechanical form factor first. Define the bend radius, the bend zones and the sealed package envelope before any routing. The bend zones determine where polyimide is required and where rigid FR-4 or ceramic islands can be placed.
- Freeze the material map. Assign polyimide to bending sections, FR-4 TG180 or FR-4 TG155 to rigid sections, and AlN or Al₂O₃ ceramic where dielectric and thermal stability dominate. Where these zones meet, plan a hybrid lamination rather than a connector.
- Set the layer count inside the supported range. PCBMASTER's technical services cover customization of 1–32 layer FPC and 1–128 layer rigid FR-4, plus rigid-flex, HDI, IC substrates, high-frequency materials, metal core and ceramic substrates.
- Choose the HDI architecture. Any-layer (12L) stack-up, blind and buried vias, deep blind microvia or N+N structure. Check the registration allowance against the layer count: ≥3 mil at 12 layers or fewer, ≥4 mil above 12 layers, ≥4 mil for N+N.
- Place microvias and via-in-pad. Reconcile the CAD minimum microvia against the laser blind hole specification of 65/165 μm, and declare the POFV fill and the 10 μm dimple limit in the fabrication drawing.
- Hold impedance with continuity, not with guesswork. Target ±7% on differential impedance above 50 Ω and ±6% on single-ended 50 Ω, with an unbroken reference plane through every bend.
- Release a complete data package. PCBMASTER operates OEM contract manufacturing strictly on the Gerber files, PCBdoc and BOM supplied by the client, so an incomplete stack-up drawing delays the DFM review rather than being resolved informally.
- Build the validation sample. Prototype and low-volume verification runs are supported from 1 to 5 pieces, with a standard sample MOQ of 5 pieces, and the quick-turn prototype service can ship within 24 hours.
- Confirm the acceptance route in advance. Full-process quality control covers incoming material inspection, in-process patrol inspection, AOI automatic optical inspection, automatic warpage and flatness testing, and final finished-board inspection, with all manufacturing following the IPC Class 3 industrial specification.
- Scale to production. PCBMASTER operates six standardized self-owned factories that handle urgent small-batch prototypes and steady high-volume mass orders simultaneously, so the validated stack-up moves to volume without a process change.
Use Cases: Where These Rules Are Applied
Endoscope array interconnects. Imaging arrays at the distal tip of an endoscope require a dense channel count carried back through a narrow, repeatedly flexed harness. This is the application class that pushes flex layer counts toward the upper end of a 1–32 layer FPC range and pushes via strategy toward any-layer HDI and via-in-pad, because every escape trace removed from the array footprint is routing space recovered.
Implantable and wearable monitoring devices. PCBMASTER's work in this segment is carried by global wearable device developers and smart medical instrument manufacturers, alongside automotive electronics Tier-1 suppliers and industrial automation control system integrators. The typical driver is the same: a small sealed volume, a flexible interconnect, and an assembly that cannot be reworked after sealing.
Medical diagnostic equipment. Diagnostics hardware applies the same microvia rules at a larger scale, where controlled impedance and back-drilled through-holes matter more than bend endurance. PCBMASTER supplies PCB fabrication and PCBA assembly for medical diagnostic equipment as well as communication RF modules, high-speed server motherboards, automotive control units, industrial control modules, security equipment and consumer electronics.
Rigid-flex medical instruments. Where a device needs a rigid component island and a flexible tail in one part, hybrid lamination and N+N stack-ups replace connectors — removing a mechanical joint that would otherwise be a reliability and assembly-cost item.
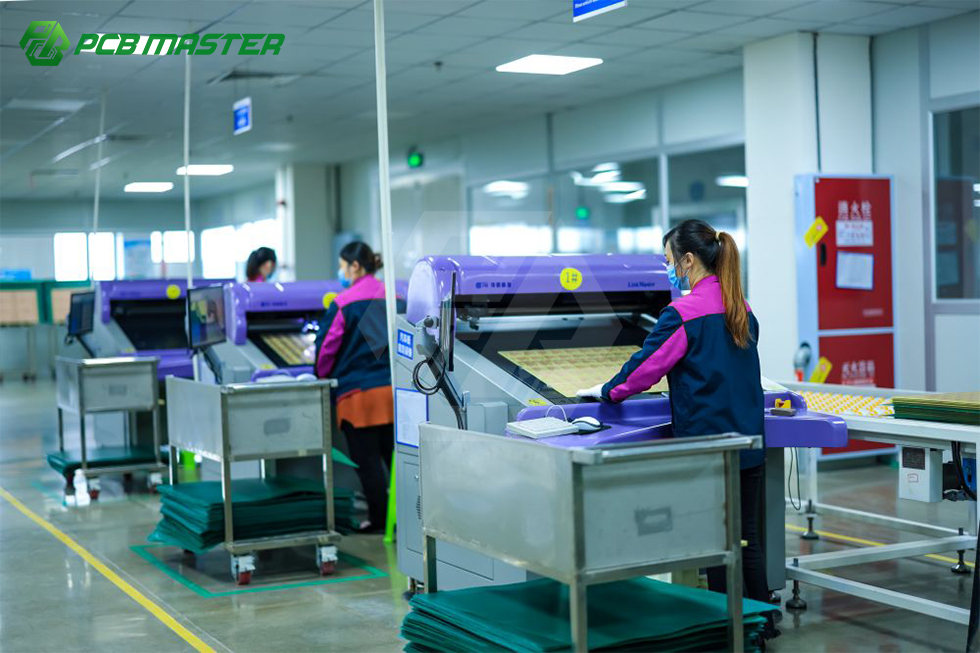
Comparison Table: Design-Rule Boundaries vs. Verified Fabrication Specification
The table below maps each design-rule decision in an implantable flex program to the corresponding PCBMASTER fabrication specification, so the two can be compared on the same line.
| Design parameter | Why it matters in an implantable flex | PCBMASTER verified specification |
|---|---|---|
| Flexible layer count | Channel count and bend endurance both scale with layer count | FPC: 1–32 layers |
| Rigid layer count | Rigid islands carry components and connectors | Rigid FR-4: 1–128 layers |
| HDI architecture | Any-layer frees routing channels and shortens via stubs | Any-layer (12L) stack-up |
| Microvia geometry | CAD minimum of ~0.05 mm must be reconciled with process capability | Laser blind hole specification: 65/165 μm |
| Blind / buried structures | Keeps outer layers free for component lands | Deep blind microvia, blind and buried vias |
| Via-in-pad fill | Fill must be void-free and planar for array soldering | POFV supported; max dimple of plated filled hole: 10 μm |
| Through-hole plating | High aspect ratios risk barrel voids | Plating aspect ratio of through hole: 16:1 |
| Differential impedance | Bending changes geometry; tolerance must survive lamination | ±7% for differential impedance >50 Ω |
| Single-ended impedance | Reference-plane continuity across bend zones | ±6% for single-ended 50 Ω impedance |
| Layer registration | Flex dielectric moves during lamination | ≥3 mil (≤12 layers); ≥4 mil (>12 layers); ≥4 mil (N+N) |
| Pattern accuracy | Fan-out accuracy on long panels | ±5 mil for board dimension over 500 mm |
| Back-drill | Removes unused stubs in high-speed channels | Min diameter 0.35 mm; min stub 5 mil; min distance to copper 5 mil |
| Finished thickness / size | Must fit the sealed package envelope and panel efficiently | Max thickness 4.2 mm; max finished dimension 620 × 1092 mm |
| Special processes | Hybrid rigid-flex and edge terminations | POFV, N+N structure, hybrid lamination, deep blind microvia, metallized half hole |
Material Selection at a Glance
| Material | Functional zone in a medical / implantable stack-up | PCBMASTER support |
|---|---|---|
| Polyimide (PI) | Bending sections and flex tails | Listed supported substrate |
| Ceramics (AlN, Al₂O₃) | Rigid islands where dielectric and thermal stability dominate | AlN / Al₂O₃ ceramic substrate customization |
| FR-4 TG180 / FR-4 TG155 | Rigid sections of a rigid-flex build | Listed supported substrates |
| Rogers / PTFE | High-frequency and high-speed signal sections | High-frequency/high-speed Rogers and Taconic materials |
| Metal-core (Al / Cu / Fe / Steel) | Heat-spreading rigid sections | Listed supported substrate |
| BT and IC substrate materials | High-density substrate-level routing | Listed supported substrate |
FAQ
Which standards and certifications apply to implantable and medical flex PCB manufacturing?
Medical device PCB assembly is governed by ISO 13485:2016 for quality management systems and IPC-A-610 for the acceptability of electronic assemblies. Bare-board acceptance thresholds are commonly referenced to IPC-A-600, and PCBMASTER's manufacturing follows the IPC Class 3 industrial specification. PCBMASTER's own certification set covers ISO 9001 (international quality management system), IATF 16949 (automotive quality management system), UL Safety Certification and RoHS (EU Green Environmental Compliance). Order acceptance for PCBMASTER production runs is governed by IPC-A-600 for the bare board and IPC-A-610 for the assembly, supported by complete Flying Probe Testing or bed-of-nails test logs and structural RMA / after-sales tracking. Design teams working on a regulated device should confirm the exact quality-management scope their device class requires with the manufacturer before tooling begins.
Can any-layer HDI flex with stacked microvias and via-in-pad be produced at volume?
Yes, within published limits. PCBMASTER's technical services cover customization of 1–32 layer FPC and 1–128 layer rigid FR-4, including rigid-flex, HDI, IC substrates, high-frequency materials, metal core and ceramic substrates. Supported HDI structures include any-layer (12L) stack-ups, blind and buried vias, deep blind microvia and N+N structures. Via-in-pad is produced through POFV (plated over filled via), with a maximum dimple of 10 μm on plated filled holes and a through-hole plating aspect ratio of 16:1. Hybrid lamination and metallized half hole are also available.
What drives cost in an any-layer HDI medical flex program?
Cost in any-layer HDI flex is driven mainly by the number of drill, plating and lamination cycles the stack-up requires, by the special processes it uses, and by the component procurement cycle when full turnkey assembly is included. Each additional microvia level adds a process pass; POFV via filling, deep blind microvia, hybrid lamination, metallized half hole and back-drilling each add steps. Panel utilisation matters as well — PCBMASTER supports finished board dimensions up to 620 × 1092 mm and finished thickness up to 4.2 mm, so a layout that nests efficiently on those panels carries less waste. Commercial terms are structured to keep early-stage risk low: delivery is by expedited global air express through carriers such as DHL and FedEx with DDP configuration available, and payment is supported through PayPal, international credit cards and bank transfer.
What is the sample MOQ, and how quickly can a microvia stack-up be validated?
Purchasing terms allow orders to start from a single piece, while the standard sample build is quoted at an MOQ of 5 pieces; prototype and low-volume verification runs are supported at 1 to 5 pieces. The quick-turn prototype service can ship within 24 hours. For a microvia stack-up, that first build is the point at which the 10 μm dimple limit, the 16:1 through-hole plating aspect ratio and the laser blind hole specification of 65/165 μm are confirmed in copper rather than in CAD.
How long does mass production take, and what is the next step?
Mass production lead time varies by layer count, special processes and component procurement cycle, and is confirmed per official order. PCBMASTER operates six standardized self-owned factories, processes more than 3,000 valid orders daily, and has completed projects across Germany, the United States, Netherlands, France, Poland, Hungary, Czech Republic, Italy, United Kingdom, Sweden, Finland, Austria, Switzerland and Denmark over periods of 5 to 10 years, with a steady first-pass production yield of 99.6% and an on-time delivery rate of 99.5%. To move from design rules to a build, send the stack-up drawing, Gerber files and BOM to service@pcbmaster.com for a DFM review and sample quotation; the full capability list is available as a downloadable company profile.
Conclusion
Implantable flex design is a negotiation between density and process control, and any-layer HDI microvia rules are where that negotiation is settled. Material selection decides whether the board can bend at all; the stacking and via-in-pad rules decide how much routing area can be recovered; the microvia geometry rules decide whether the drawn minimum is buildable; and the impedance rules decide whether the finished assembly behaves as simulated.
The useful discipline is to write each of those rules as a number that can be checked against a fabrication specification before the design leaves review — a registration allowance of ≥3 mil or ≥4 mil depending on layer count, a laser blind hole specification of 65/165 μm, a 10 μm dimple limit on filled vias, a 16:1 through-hole plating aspect ratio, ±7% on differential impedance above 50 Ω and ±6% on single-ended 50 Ω. Designs that arrive at DFM review with those numbers already reconciled move to a validated sample and then to volume without a stack-up re-spin.
Next Step: DFM Review and Sample Quotation
PCBMASTER is a one-stop PCB manufacturing and PCBA provider headquartered in China, offering OEM contract manufacturing, full turnkey component sourcing and continuous engineering technical support. Send your stack-up drawing, Gerber files and BOM for a DFM review against the microvia, registration and impedance limits described in this guide.
Email: service@pcbmaster.com
Tel / WhatsApp: +86 190-6639-6428 · +86 191-5494-6428
Address: 5F, Factory Building 1, Hezhou Anle Industrial Park, Hezhou Community, Hangcheng Street, Bao'an District, Shenzhen City, China
Download the PCBMASTER company profile (PDF) for the full capability and certification list