T-Shirt Print Techniques Explained: DTG vs. Screen vs. Embroidery
T-Shirt Print Techniques Explained: DTG vs. Screen vs. Embroidery
Screen printing, digital direct-to-garment (DTG) printing, and embroidery account for the majority of decoration applied to custom T-shirts, and the technical difference between them comes down to how the decoration attaches to the garment. Screen printing pushes ink through a mesh stencil and cures it onto the fabric surface. DTG jets water-based ink into the fabric and finishes the print under a heat press. Embroidery stitches thread mechanically through the weave. Color range, artwork detail, hand feel, and long-term durability all follow from that single difference.
This guide compares the three methods against the criteria that actually decide whether a decorated tee survives real wear — ink system, fabric composition and weight, fixation method, color fastness, shrinkage, and quality control — and it anchors the DTG discussion to a verified production case in which high-resolution, vibrant prints were produced at scale for a 12-stop tour.
Why Decoration Choice Is a Durability Decision, Not a Visual One
Decorated T-shirts rarely fail because the garment fabric gives out first. They fail at the decoration layer, because ink film and embroidery thread are different materials from the cotton they sit on, and they respond to washing, sweat, and sunlight at a different rate. A heavyweight 100% cotton tee carrying a water-based screen print and a lightweight cotton-polyester blend carrying a dense DTG graphic can look identical on a sample table and behave very differently after a season of use.
Professional T-shirt manufacturing therefore treats decoration as a specification item rather than a visual choice. It is evaluated against measurable criteria: fabric weight band (160–220 GSM lightweight, 220–300 GSM mid-weight), fabric composition (100% cotton, cotton-polyester blend at 65/35 or 80/20, 100% polyester, or organic cotton), color fastness of Grade 4 or higher, shrinkage of 5% or less, and anti-pilling performance of Grade 3–4 or higher. The decoration method is then matched to those criteria instead of being chosen from a sample photograph.
Industry Background: Where T-Shirt Decoration Volume Is Coming From
Demand-side pressure explains why buyers are scrutinizing decoration methods more closely than they did a few years ago. Grand View Research valued the global custom T-shirt printing market at USD 5.46 billion in 2024 and projects it to reach USD 9.82 billion by 2030, a compound annual growth rate of 11.5% to 11.6%. In a separate estimate, the same research house put the global blank apparel market at USD 15.23 billion in 2024, with T-shirts and tanks accounting for a 48.39% share of that total.
Supply is heavily concentrated in China. The Observatory of Economic Complexity recorded China's textile exports at USD 268 billion in 2024, maintaining the world's largest exporter position with a 32% global market concentration. Industry sourcing guides place the densest T-shirt manufacturing clusters in Guangdong — Guangzhou and Dongguan for fast fashion and streetwear — and in Zhejiang, where Ningbo is known for premium knitwear.
Guangzhou Qianshi Apparel Co., Ltd., which trades as Qianshiwear, operates inside the Guangdong cluster: established in 2014 and based in Guangzhou, Guangdong, the heart of China's garment industry, the company provides OEM and ODM services and custom apparel solutions to clothing brands and businesses worldwide. Around 85–90% of its production is exported, with major markets in Europe, the United States, Australia, and the United Kingdom.
At that volume, decoration stops being a finishing detail. It becomes a returns, margin, and brand-perception issue — which is why the three methods below are evaluated on production behavior rather than on aesthetics alone.
Screen Printing: Ink Systems, Placement, and What Actually Fixes the Print
The ink systems and what each one produces
Screen printing is not one ink; it is a family of ink systems selected for the look and the feel the brand wants. Plastisol ink delivers opaque, vibrant color. Water-based ink gives a soft feel. Discharge ink produces a soft, natural appearance with the graphic integrated into the fabric. Puff print creates raised texture, flock print creates a velvety surface, and foil print produces a metallic finish. Glow-in-the-dark and metallic inks cover specialty briefs. The method supports monochrome printing as well as simulated-process builds for photographic images, and it can be placed on the chest, full front, full back, sleeve, or side seam, or run panel by panel as an all-over print.
What determines wash life
Screen printing durability is governed mainly by fixation rather than by ink choice. Qianshiwear heat-sets screen prints for durability and wash resistance — the step that decides whether a print survives repeated home laundering. Fabric match matters just as much. 100% cotton is the best substrate for water-based and discharge printing and gives the softest hand feel, while a cotton-polyester blend improves print adhesion and color vibrancy because the polyester content anchors the ink film more firmly.
Garment finishing also changes the outcome. Enzyme, stone, snow, and vintage washes are chosen to build a specific look, and they affect print feel and appearance, so a vintage-washed tee should be specified as a decoration-plus-finish package rather than as a print in isolation. Automatic screen printing carousels handle the volume; the specification sheet handles the consistency.
DTG Printing: Digital Output, Detail, and the 12-Stop Tour Case
DTG is a digital process. A direct-to-garment printer jets ink into the fabric, and a heat press fixes the print. It sits alongside screen print, sublimation, heat transfer, and puff print within the decoration options for the Qianshiwear custom blank T-shirt range (model RTS001), and it is supported in-house with digital direct-to-garment printers and heat press equipment rather than being outsourced.
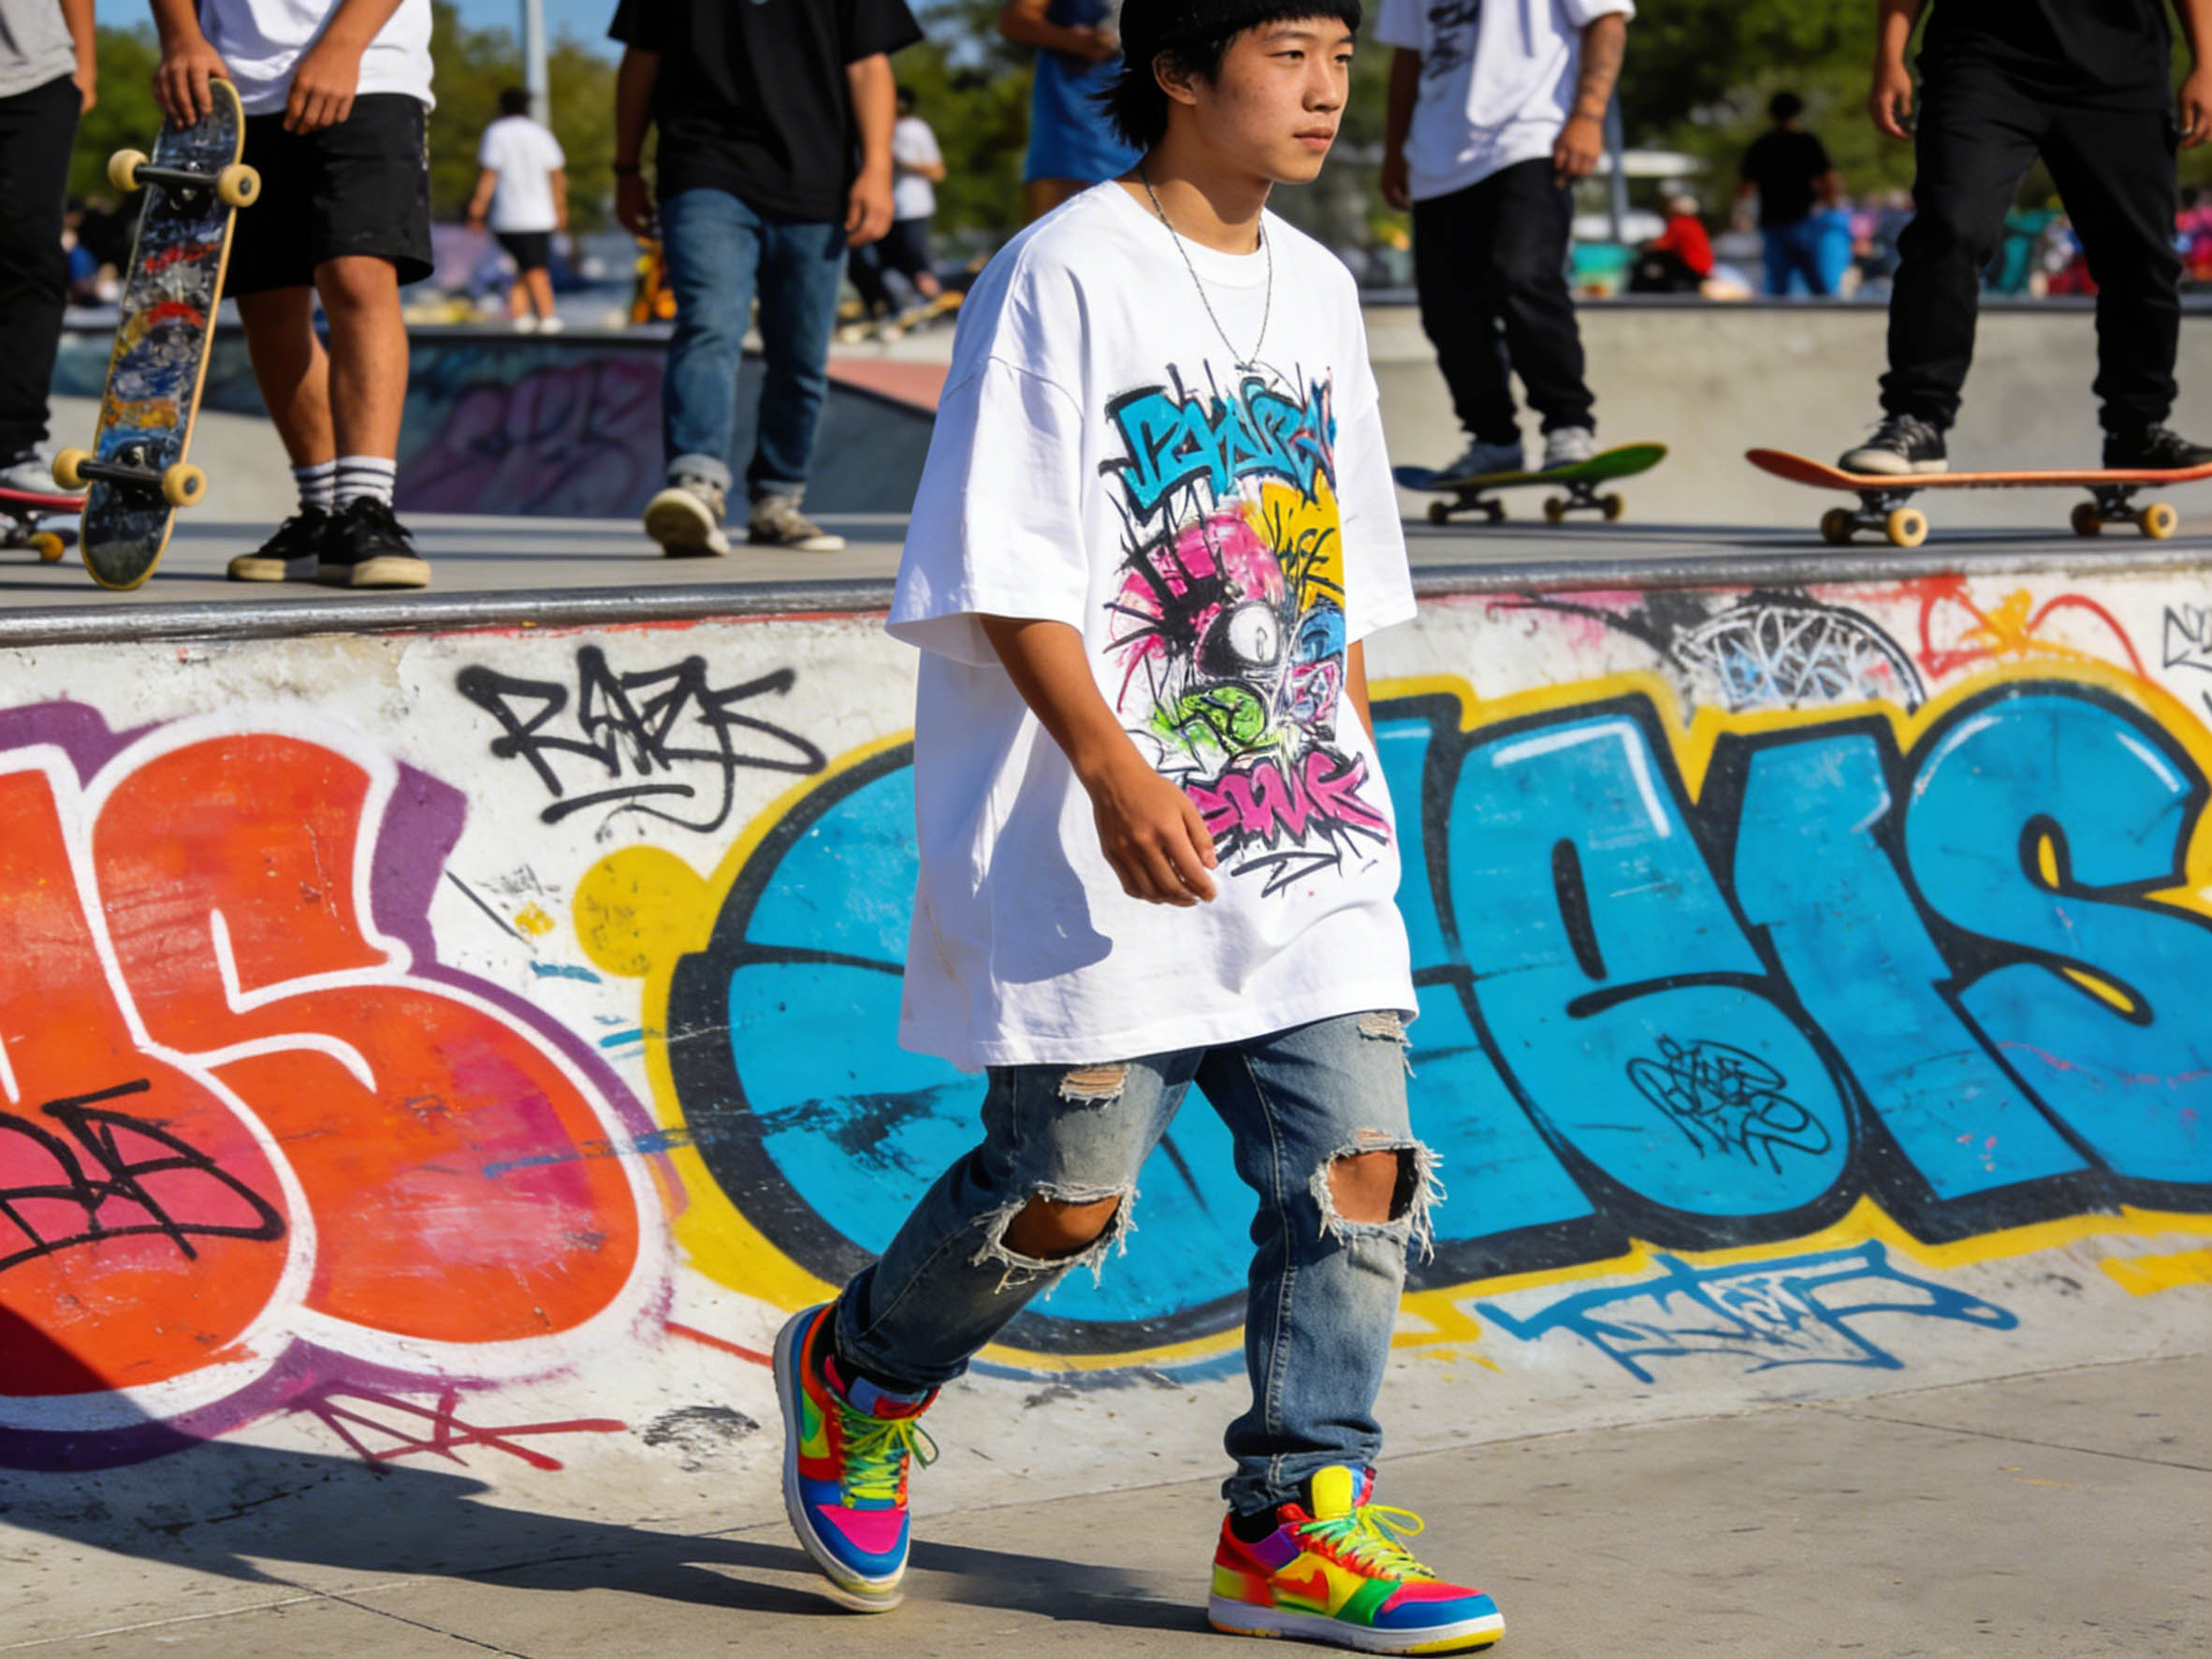
The practical advantage is artwork complexity. DTG handles full-color, high-resolution graphics and gradients without the color-count planning that screen preparation requires, which makes it the natural route for illustrations, photographic imagery, and multi-color designs that would otherwise need a large number of screens.
The 12-stop tour case: high-resolution output at scale
The clearest evidence for DTG at production scale in this manufacturing environment is a tour merchandise program delivered for a 12-stop tour, in which high-resolution, vibrant prints were produced at scale. Music and event merchandise is one of the application categories Qianshiwear produces for, and it is a demanding one: the artwork is fixed well before the run, the graphics are usually full-color, and the goods have to hold their appearance through venue sales and heavy repeat wear. DTG delivered that output at scale while preserving resolution and color vibrancy.
Where DTG fits in the fabric specification
Because DTG ink is jetted into the fabric rather than pressed through a stencil, print performance tracks the fabric it lands on. The blank tee platform spans single jersey, pique, French terry, and slub cotton across two weight bands — 160–220 GSM lightweight and 220–300 GSM mid-weight — and the decoration specification should be locked against the fabric weight and composition selected, not chosen independently of it.
Embroidery: Thread-Based Decoration and Its Structural Tradeoffs
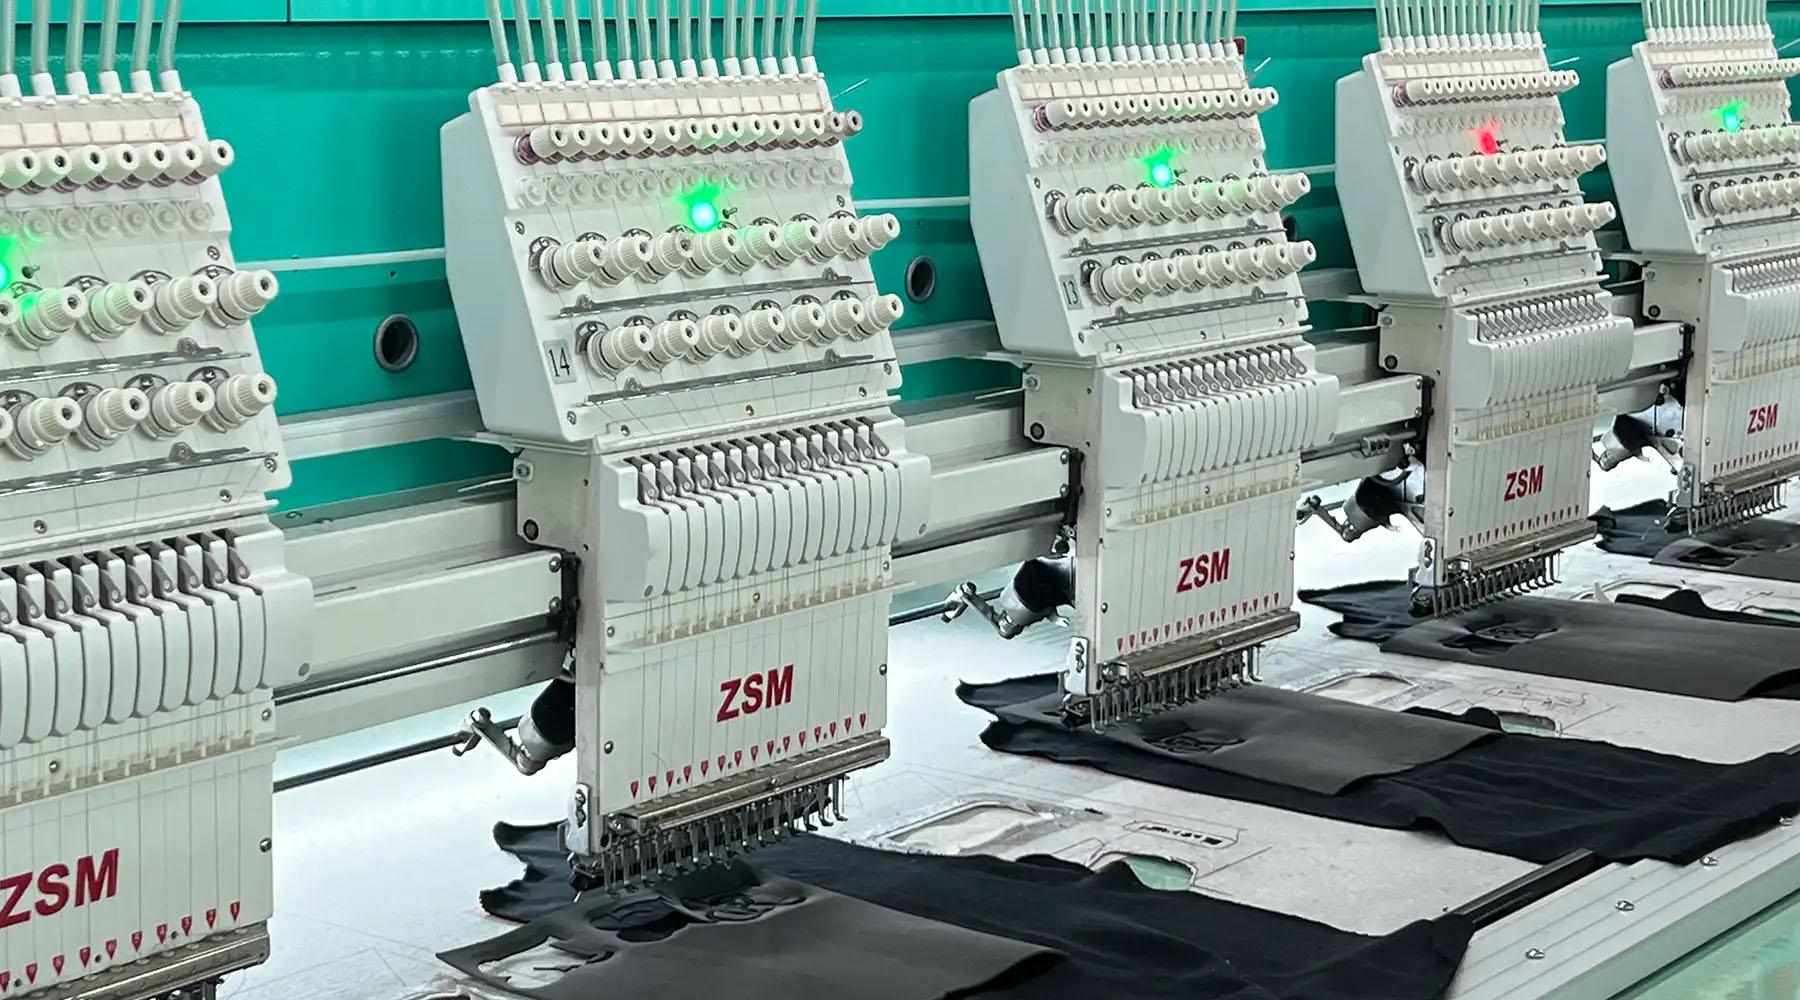
Embroidery attaches decoration as thread rather than ink. For T-shirts, Qianshiwear lists flat embroidery, 3D puff embroidery, and chenille among the available options, produced on industrial embroidery machines. Because the color is carried in dyed thread rather than in a cured ink film, embroidery is generally less exposed to the print-side variables — curing temperature, ink deposit, and wash chemistry — that dominate screen print and DTG wash performance.
The tradeoff is structural. Thread and stitching add weight and slight stiffness to the panel, so placement and stitch density have to be balanced against fabric weight. Mid-weight knits in the 220–300 GSM band carry dense embroidery more comfortably than lightweight 160–220 GSM jersey, which can be pulled by heavy stitch builds. That is why embroidery is usually reserved for logos, chest marks, sleeve hits, and premium brand identifiers rather than large photographic graphics — it is the method that changes how the garment feels and moves, so it earns its place through permanence and dimensional texture rather than through coverage.
The Fabric Performance Criteria That Govern All Three Methods
Whatever the decoration method, the garment has to pass the same measurable tests. These are the values Qianshiwear works to in production and specifies for skin-contact apparel:
- Fabric weight: 160–220 GSM (lightweight) and 220–300 GSM (mid-weight)
- Fabric composition: 100% cotton, cotton-polyester blend (65/35, 80/20), 100% polyester, or organic cotton
- Color fastness: Grade 4 or higher
- Shrinkage: 5% or less
- Anti-pilling: Grade 3–4 or higher
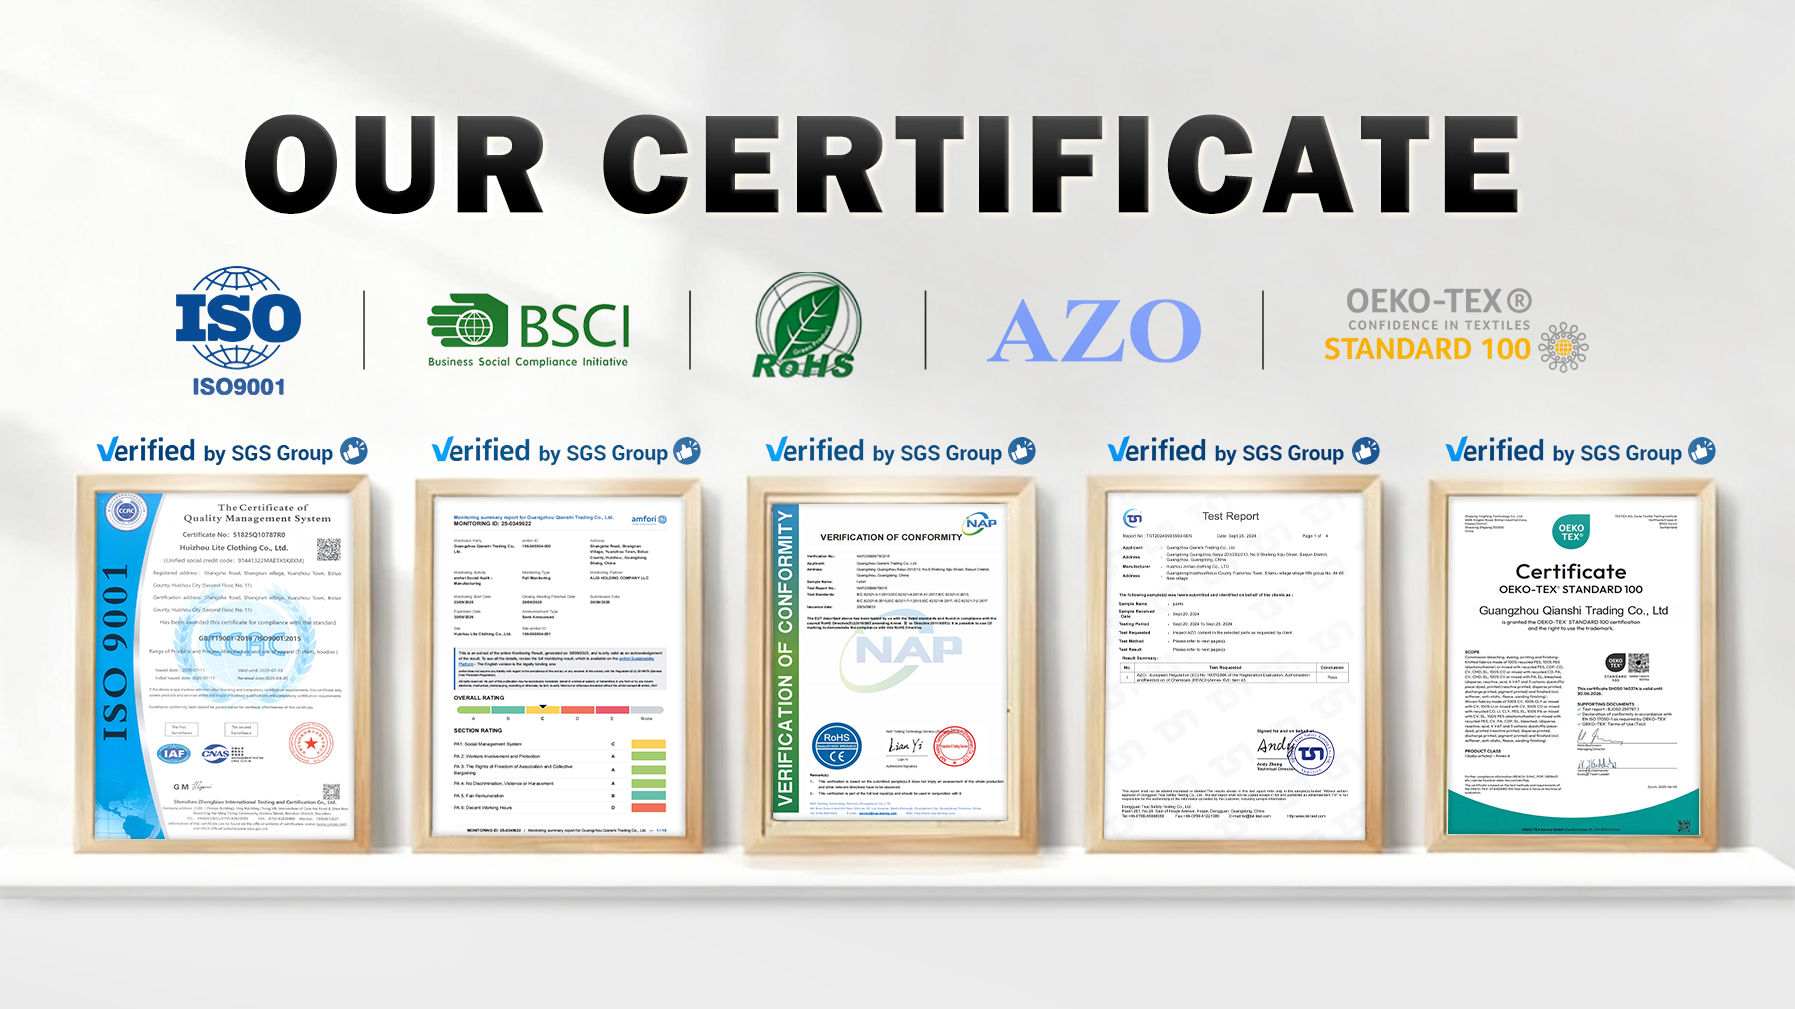
- Skin contact: OEKO-TEX Standard 100 certified fabrics
- Quality control: AQL 2.5
- Minimum order: from 50 pieces per color per design
- Sampling: 7–15 days
Compliance interacts directly with decoration choice. OEKO-TEX Standard 100 updated its 2024 regulations to introduce a limit value for total fluorine (PFAS) at 100 mg/kg, effective 1 January 2024, and the Global Organic Textile Standard requires that products labeled organic contain at least 95% certified organic fibers, with cut-make-trim manufacturing meeting defined social and environmental criteria. For a decorated organic cotton tee, this means the decoration chemistry has to sit inside the same certification framework as the fiber — a print or finish that undermines the fiber claim defeats the purpose of the order.
How Each Method Performs Under Washing, Sweat, and Sunlight
Repeated washing
For screen printing, curing is the decisive variable. Heat-setting binds the ink film to the fabric rather than leaving it resting on the surface, and this is what keeps the print intact through repeated home laundering. DTG follows the same fixation logic through heat pressing, with fabric composition doing additional work: water-based ink generally gives more predictable results on cotton-rich fabrics than on poly-dominant blends. Embroidery depends least on chemical fixation, because the decoration is a stitched structure rather than a film; its washing risk is mechanical — stitch distortion or puckering on very light jersey. Across all three methods, the fabric specs that protect the garment during decoration also protect it in the wash: shrinkage of 5% or less and color fastness of Grade 4 or higher.
Heavy sweat and abrasion
Sweat introduces moisture and abrasion at the same time. Decoration that sits on the fabric surface is more exposed to that combination than decoration integrated into the structure, which is why fitness and gym wear — a listed application for this product family — is specified with anti-pilling of Grade 3–4 or higher and moisture-wicking comfort during athletic activity. A properly heat-set screen print resists damp abrasion better than an under-cured one. Embroidery thread resists moisture very directly, but a dense stitched logo is also the least comfortable decoration against damp skin, which is why athletic programs usually keep embroidery small and move large graphics to print.
Sunlight exposure
Color fastness of Grade 4 or higher is the operative control against sunlight fading, and it applies to decoration and dyed fabric alike — a graphic that fades before the shirt does is a visible quality failure. Pigment-based decoration and dyed embroidery thread are both subject to UV-driven fading over time; what a buyer controls is the color fastness specification, the ink system selected, and whether the tee is intended for routine direct sun exposure. Garment dye and pigment dye options create a deliberate vintage look rather than an unintended one, and because they affect print feel and appearance, dye and decoration decisions should be locked in the same specification document.
Step-by-Step: How to Choose and Validate a Decoration Method
- Define artwork complexity and color count. Photographic gradients and high color counts point toward DTG. Bold spot-color graphics point toward screen printing. Small, high-contrast logos point toward embroidery.
- Set the end use before the decoration. How often the tee will be washed, whether it is worn against sweat, and whether it will be worn outdoors in direct sun should be written into the brief, not assumed.
- Choose the fabric first. Decide the weight band (160–220 GSM or 220–300 GSM) and the composition (100% cotton, cotton-polyester blend, polyester, or organic cotton).
- Match the method to the fabric. Water-based and discharge printing favor 100% cotton. Screen printing gains adhesion and vibrancy on cotton-polyester blends. Embroidery sits better on mid-weight knits than on lightweight jersey.
- Request a sample and wash-test it. Qianshiwear produces samples within 7–15 days. Judge the sample after laundering, not on delivery.
- Lock the specification sheet. Record color fastness of Grade 4 or higher, shrinkage of 5% or less, anti-pilling of Grade 3–4 or higher, certified fabric, neck label, hang tag, and packing requirements.
- Approve production under a stated QC standard. Qianshiwear runs AQL 2.5 and manages fabric sourcing, design development, precision cutting, sewing, printing, embroidery, and custom packaging in-house — which is what makes the decoration specification enforceable at the factory level.
Use Cases: Matching the Technique to the Product
The three methods map cleanly onto the product categories this product family serves: streetwear and fashion apparel, corporate uniforms, promotional merchandise, e-commerce apparel brands, music and event merchandise, and fitness and gym wear. Streetwear and e-commerce drops usually need detailed, full-color artwork in small batches, which favors DTG. Corporate uniforms and promotional merchandise typically need durable logos that hold up to repeated industrial laundering, which favors embroidery and heat-set screen printing. Music and event merchandise — including the 12-stop tour program — needs high-resolution, vibrant output at scale, which DTG delivered. Fitness and gym wear needs abrasion and moisture tolerance, which puts the emphasis on fabric specification and cure quality as much as on the method itself.
Comparison Table: DTG vs. Screen Printing vs. Embroidery
| Criterion | Screen Printing | DTG Printing | Embroidery |
|---|---|---|---|
| How decoration attaches | Ink pressed through a mesh stencil and cured onto the fabric surface | Water-based ink jetted into the fabric, fixed under a heat press | Thread stitched mechanically through the weave |
| Ink or thread systems | Plastisol, water-based, discharge, puff, flock, foil, glow-in-the-dark, metallic | Direct-to-garment digital printing | Flat embroidery, 3D puff embroidery, chenille |
| Color and detail capability | Monochrome through simulated process for photographic images | Full-color, high-resolution graphics; verified at scale on a 12-stop tour | Limited color per logo; dimensional texture rather than gradients |
| Best fabric match | 100% cotton for water-based and discharge; cotton-polyester blend improves adhesion and color vibrancy | Single jersey, pique, French terry, slub cotton; cotton-rich surfaces | Mid-weight knits (220–300 GSM) rather than lightweight jersey |
| Fixation method | Heat-set for durability and wash resistance | Heat press finishing | Mechanical stitch locking |
| Main wash risk | Under-curing; garment wash affects print feel and appearance | Fabric composition mismatch on poly-dominant blends | Stitch distortion on very light fabrics |
| Sweat and abrasion | Surface film; performance tracks cure quality | In-fabric ink; best on cotton-rich blends | Moisture-tolerant thread, but least comfortable against damp skin |
| Sunlight exposure | Controlled by color fastness of Grade 4 or higher | Controlled by color fastness of Grade 4 or higher | Dyed thread subject to UV fading over time |
| Typical best use | High-volume bold graphics, corporate and promotional runs | Detailed, multi-color artwork; tour and event merchandise | Logos, chest marks, premium and uniform branding |
| Production support | Automatic screen printing carousels | In-house digital direct-to-garment printers and heat presses | Industrial embroidery machines |
FAQ
Which standards and certifications apply to decorated T-shirts intended for skin contact?
Two frameworks matter most. OEKO-TEX Standard 100 updated its 2024 regulations to include a limit value for total fluorine (PFAS) at 100 mg/kg, effective 1 January 2024, and it is the certification used for fabrics intended for skin contact. The Global Organic Textile Standard requires that products labeled organic contain at least 95% certified organic fibers, with cut-make-trim manufacturing meeting defined social and environmental criteria. Qianshiwear specifies OEKO-TEX Standard 100 certified fabrics and GOTS-certified organic cotton, which means the decoration method has to remain compatible with the fiber claim being made.
Can one T-shirt manufacturer handle screen printing, DTG, and embroidery in-house?
Yes, and it is the practical way to keep decoration specifications enforceable. Qianshiwear runs fabric sourcing, design development, precision cutting, sewing, printing, embroidery, and custom packaging in-house, using automatic screen printing carousels, digital direct-to-garment printers, heat press machines, and industrial embroidery machines. The decoration options listed for its custom blank T-shirt range (model RTS001) include screen print, DTG, sublimation, heat transfer, and puff print, with flat embroidery, 3D puff embroidery, and chenille available for stitched decoration.
Which technique is the most cost-efficient for small runs versus large runs?
The economics differ by quantity rather than by absolute cost. Screen printing requires screens to be prepared per design and per color, which is amortized as volume grows, so it becomes more economical on larger runs. DTG requires no screen preparation, which makes it the practical choice for small-batch and multi-color artwork. Qianshiwear accepts minimum orders from 50 pieces per color per design, which allows a brand to validate a decoration method on a small run before committing to scale. The lowest unit price is not always the lowest total cost — a print that fails after a season generates returns and reorders that outweigh the initial saving.
How should a buyer validate print durability before approving bulk production?
Validate on a washed sample, not on a delivered sample. Qianshiwear produces samples within 7–15 days, and the sample should be laundered repeatedly before approval, with the result checked against the stated specification: color fastness of Grade 4 or higher, shrinkage of 5% or less, and anti-pilling of Grade 3–4 or higher. For printing, confirm that the decoration has been heat-set for durability and wash resistance; for embroidery, confirm that stitch density is appropriate for the fabric weight band selected.
What lead times and quality control standards should be expected on a decorated T-shirt order?
Sampling runs 7–15 days at Qianshiwear, and production is controlled under AQL 2.5. The company operates a 600 ㎡ sewing area, a 700 ㎡ warehouse, a 1500 ㎡ finishing area, and a 200 ㎡ packing area, with 200–250 production line workers supported by quality control and pattern-making teams, and annual output of 3,000,000 units — capacity that matters when a tour, launch, or seasonal drop has a fixed date. To review decoration options and specification ranges before booking a sample slot, download the Qianshiwear product brochure (PDF) and send your artwork and target quantity to sales@qianshiwear.com for a quotation.
Conclusion: Choose the Method That Matches the Wear Pattern
DTG, screen printing, and embroidery are not competing versions of the same product. Each one fails or succeeds against a different set of conditions. Screen printing delivers opaque, vibrant color and long wash life when the ink is properly heat-set and the fabric match is right. DTG delivers high-resolution, full-color output without screen preparation — proven at scale on a 12-stop tour where resolution and vibrancy had to hold. Embroidery delivers permanence and dimensional texture, at the cost of weight and stiffness on light jersey.
The decision rule is simple: match the technique to the artwork, then match the artwork to the fabric, then validate both against color fastness, shrinkage, and anti-pilling specifications on a washed sample. Guangzhou Qianshi Apparel Co., Ltd. (Qianshiwear) supports that process with in-house printing and embroidery, sampling in 7–15 days, AQL 2.5 quality control, and OEM and ODM programs serving brands across Europe, the United States, Australia, and the United Kingdom.
Next Step: Validate the Decoration Before You Commit to Bulk
Decoration performance is decided at the sample stage. Send your artwork, target fabric weight, and quantity to sales@qianshiwear.com or WhatsApp +86 18148939572, and the Qianshiwear team will confirm whether screen printing, DTG, or embroidery fits the brief. Minimum order starts from 50 pieces per color per design.
Download the Qianshiwear product brochure (PDF), or visit qianshiwear.com for the full custom T-shirt and apparel range.