Honed Tube vs. Cold Drawn vs. Chrome Plated Tube: Hydraulic Cylinder Comparison Guide
Hydraulic Cylinder Material Selection
For hydraulic cylinder buyers, the practical answer is function-based: choose honed tube for the cylinder barrel when the bore needs H8/H9 ID tolerance and Ra ≤0.4 μm surface roughness; choose cold drawn cold rolled precision seamless tube when the starting tube must meet OD16–300 mm, WT2–30 mm and ±0.05 mm tolerance before further machining; choose hard chrome plated tube or hollow piston rod for the rod-side surface where 25 ±5 μm chrome, 900–1150 HV hardness, ≤0.2 μm roughness and 200-hour NSS rating 9 are specified.

The buyer problem: three names, three different jobs
Hydraulic cylinder sourcing frequently mixes three product names in one quotation: honed tube, cold drawn tube and chrome plated tube. The confusion is understandable because all three are precision steel tube products used in fluid power. The risk is that a buyer compares them as if they were alternate finishes of the same item. They are not. A honed tube is normally specified for the cylinder barrel bore. A cold drawn cold rolled precision seamless tube is normally specified as a precision seamless tube for hydraulic system or hydraulic cylinder tube applications, and it may be supplied as a starting tube for later bore finishing. A hard chrome plated tube is a hollow piston rod for the rod side of a hydraulic cylinder, where chrome layer, hardness and corrosion resistance are the main surface requirements.
The buyer problem becomes concrete at three points. First, the bore side must hold seal contact, dimensional tolerance and surface roughness. Second, the rod side must resist wear, corrosion and impact on the chrome layer. Third, the purchase order must state the correct material grade, standard, inspection evidence and acceptable limits. If those three points are not separated, a low-price tube can become an expensive rework item.
Industry background: why the three product families are compared
The global honed tube market was valued at USD 3.6 billion in 2025, with a forecast period of 2026–2035, according to WiseGuyReports. Data Insights Reports places Asia-Pacific at 35% of the hydraulic tubing market in 2025. These figures describe market context, not supplier capability. They explain why buyers see many quotations for honed tube, cold drawn tube and chrome plated rod from the same industrial region and why material and standard verification matter.
The standards picture adds another comparison point. DIN 2391 is withdrawn and EN 10305-1 is active. ST52-3 under DIN 2391 is approximately equivalent to E355 under EN 10305-1. In practice, a buyer may receive a quotation for DIN 2391 ST52 honed tube and another for EN 10305-1 E355 honed tube. The two descriptions can point to a similar material family, but the purchase order should still state the active standard, the grade and the inspection requirement. This is a documentation issue as much as a metallurgical one.
The three product families in detail
Honed Tube for Hydraulic Cylinder barrels
A honed tube is a precision tube with a bore finished for hydraulic cylinder barrel service. In the MX Metals product data, the honed tube is classified as a skived and roller burnished tube, and the bore is produced by skiving and roller burnishing. The model designation is ID 30~500 mm, and the inner diameter range is 30 to 500 mm. The product data lists ID tolerance H8, ID roughness ≤0.2 μm, straightness ≤0.5/1000 mm, tensile strength ≥600 MPa, yield strength ≥520 MPa and elongation ≥14%. The company also states that it controls honed tube ID tolerance to H8/H9 and surface roughness to a maximum of Ra 0.4 μm.
Available material grades for the honed tube include ST52, E355, S355J0H, S355J2H, ST45, SAE1026, STKM13C, Q345B, Q345D, 16Mn, 27SiMn, 25Mn, AISI 304, AISI 316 and AISI 431. Applicable standards include DIN 2391, EN 10305, GB/T 8713-88 and GB/T 3639-2000. ST52 is listed with DIN 2391, and E355 is listed with EN 10305. Typical application scenarios include hydraulic cylinder barrels, and the product is intended for the hydraulic industry and the construction machinery industry.
Cold Drawn Cold Rolled Precision Seamless Tube
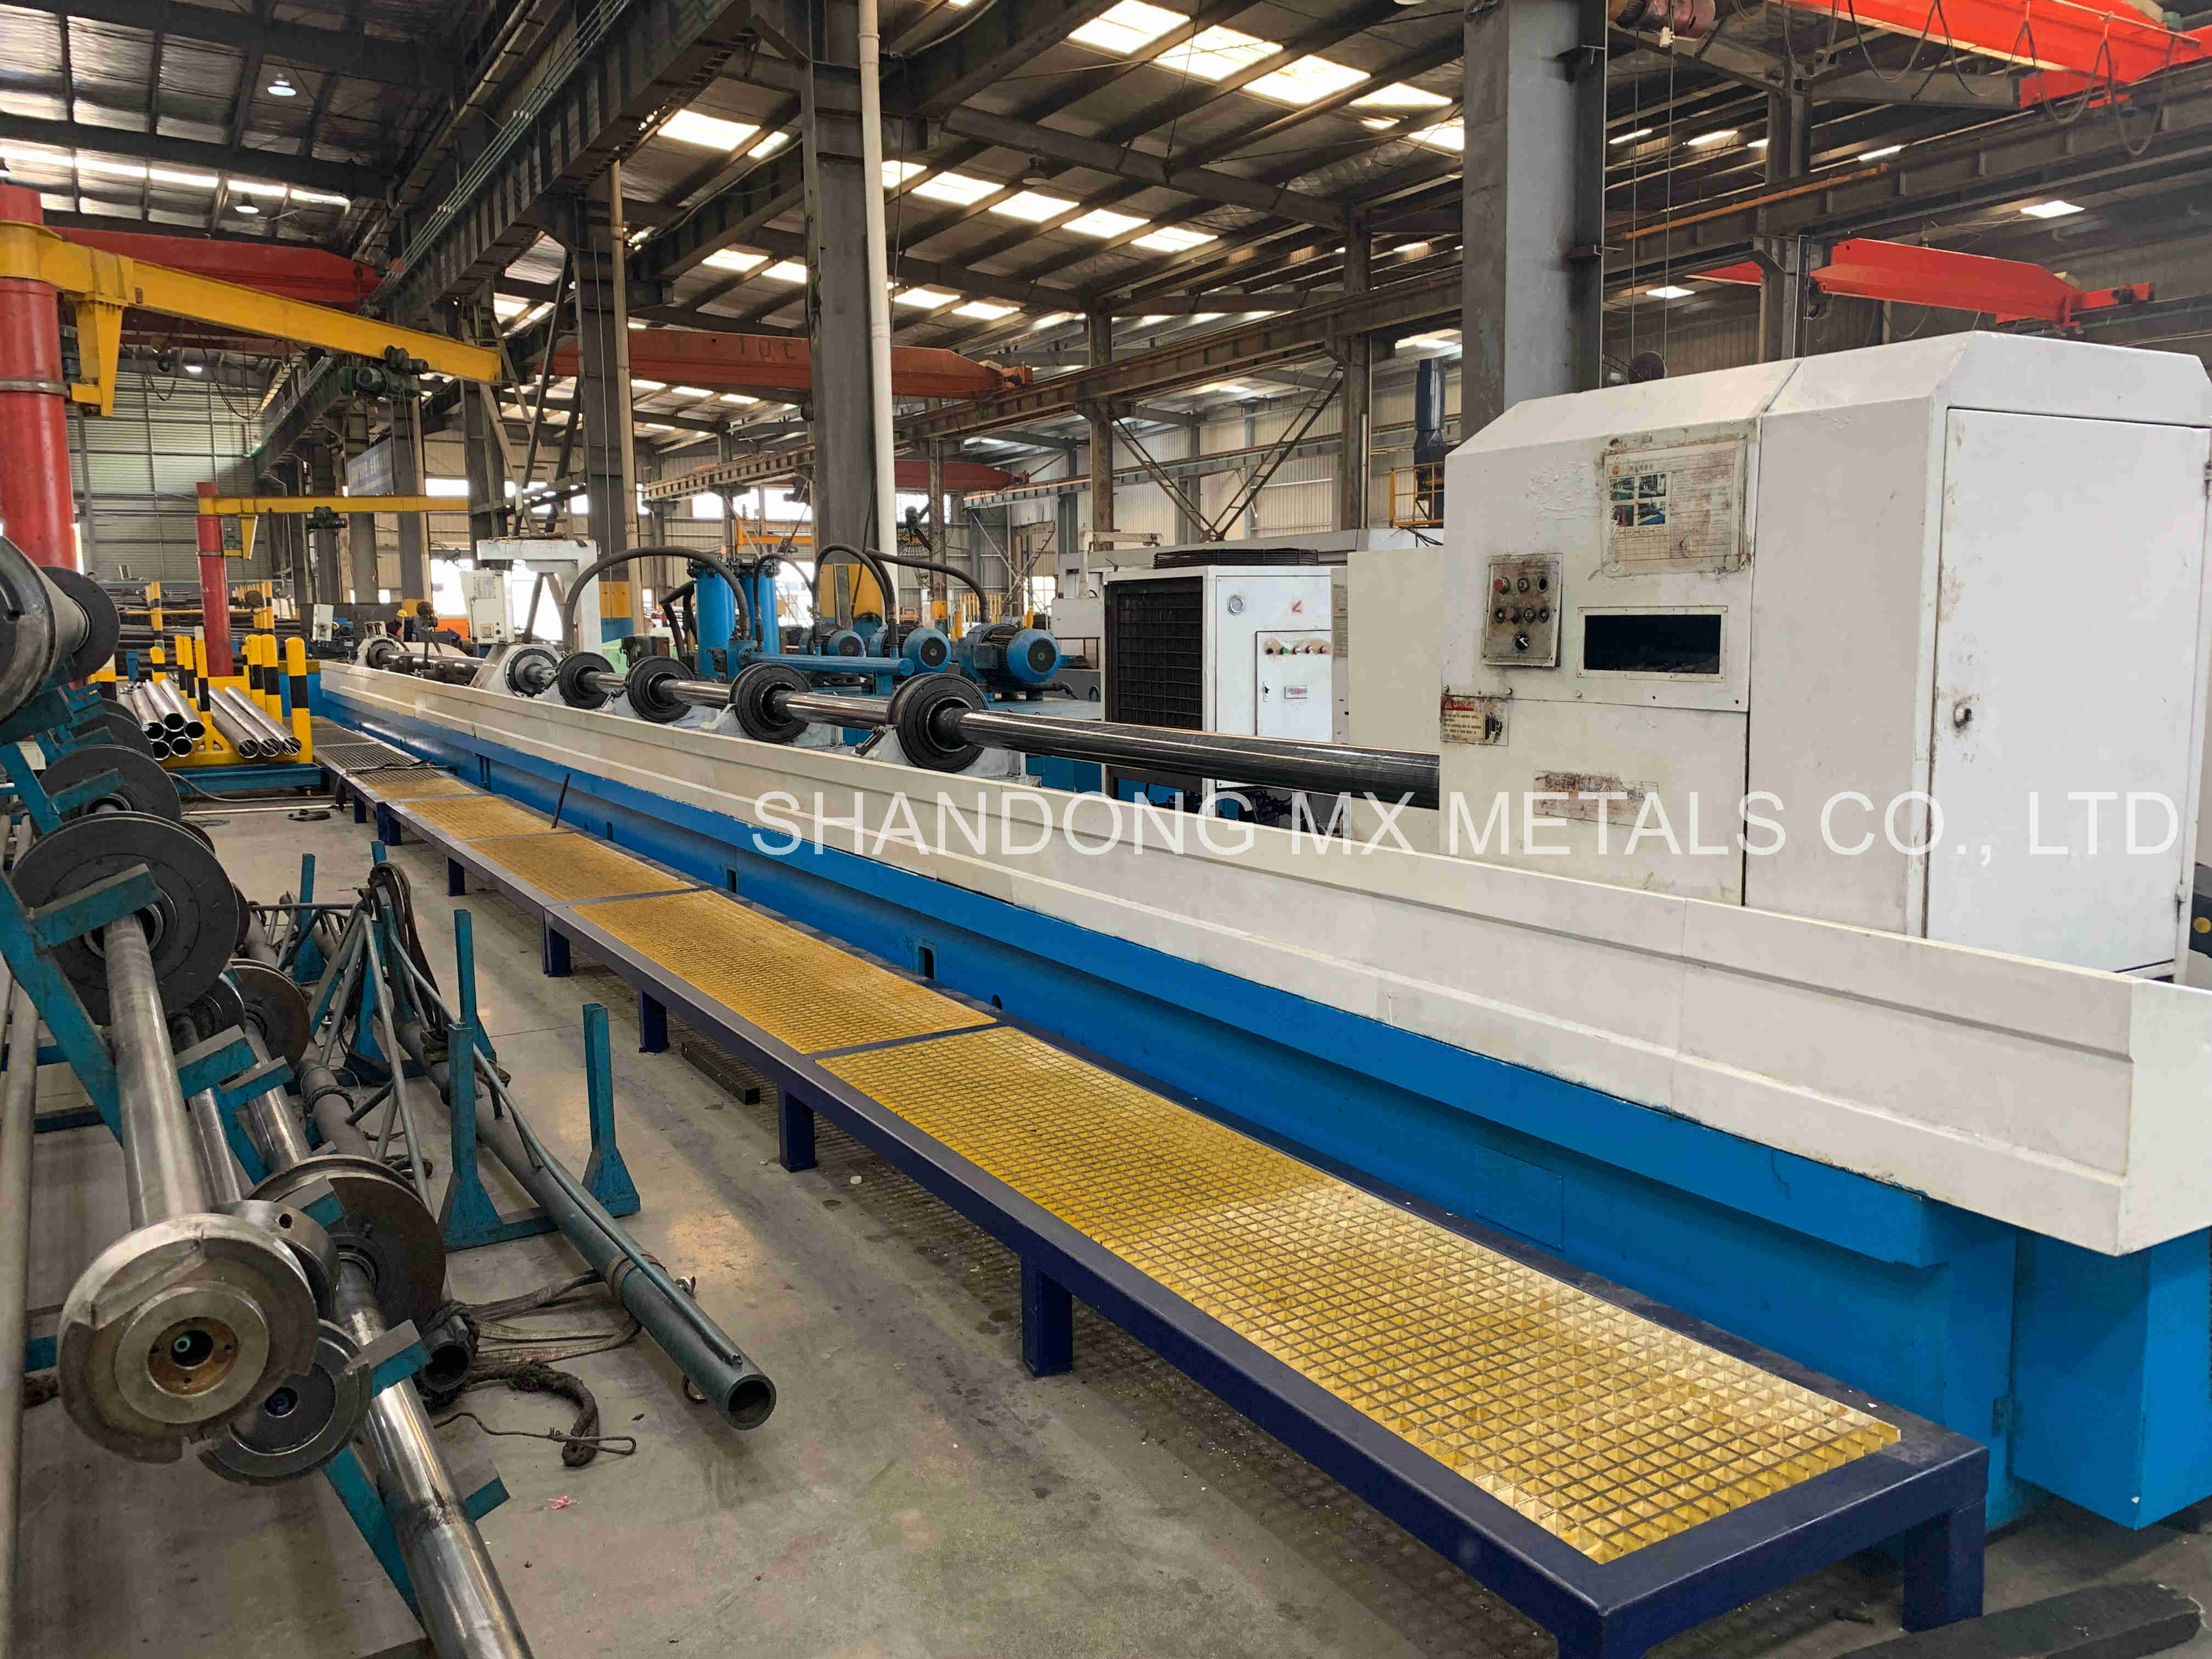
A cold drawn cold rolled precision seamless tube is a seamless tube cold drawn and cold rolled to tight dimensional accuracy. The product is classified as a cold drawn cold rolled seamless tube and belongs to the precision seamless tube category. The model designation is ID 6~200 mm. The size range is OD16–300 mm and WT2–30 mm, with tolerance of OD ±0.05 mm and ID ±0.05 mm. The product data lists high dimensional accuracy, smooth inner and outer surface, low roughness, uniform wall thickness, stable mechanical properties and good straightness for further machining.
Material options include ST37, ST45, ST52, 1035, 1045, CK45, E355, A179, A192, 10#, 20#, 35#, 45#, GCr15, 20Cr, 40Cr, 15CrMo, 20CrMo, 35CrMo, Q345B, 16Mn, 27SiMn and 12Cr1MoV. The product is intended for hydraulic system applications and hydraulic cylinder tube applications, and for engineering machinery, textile machinery, diesel engine and steel bar connecting sleeve applications. Typical application scenarios include precision machine parts and automobile components.
Hard Chrome Plated Tube and Hollow Piston Rod
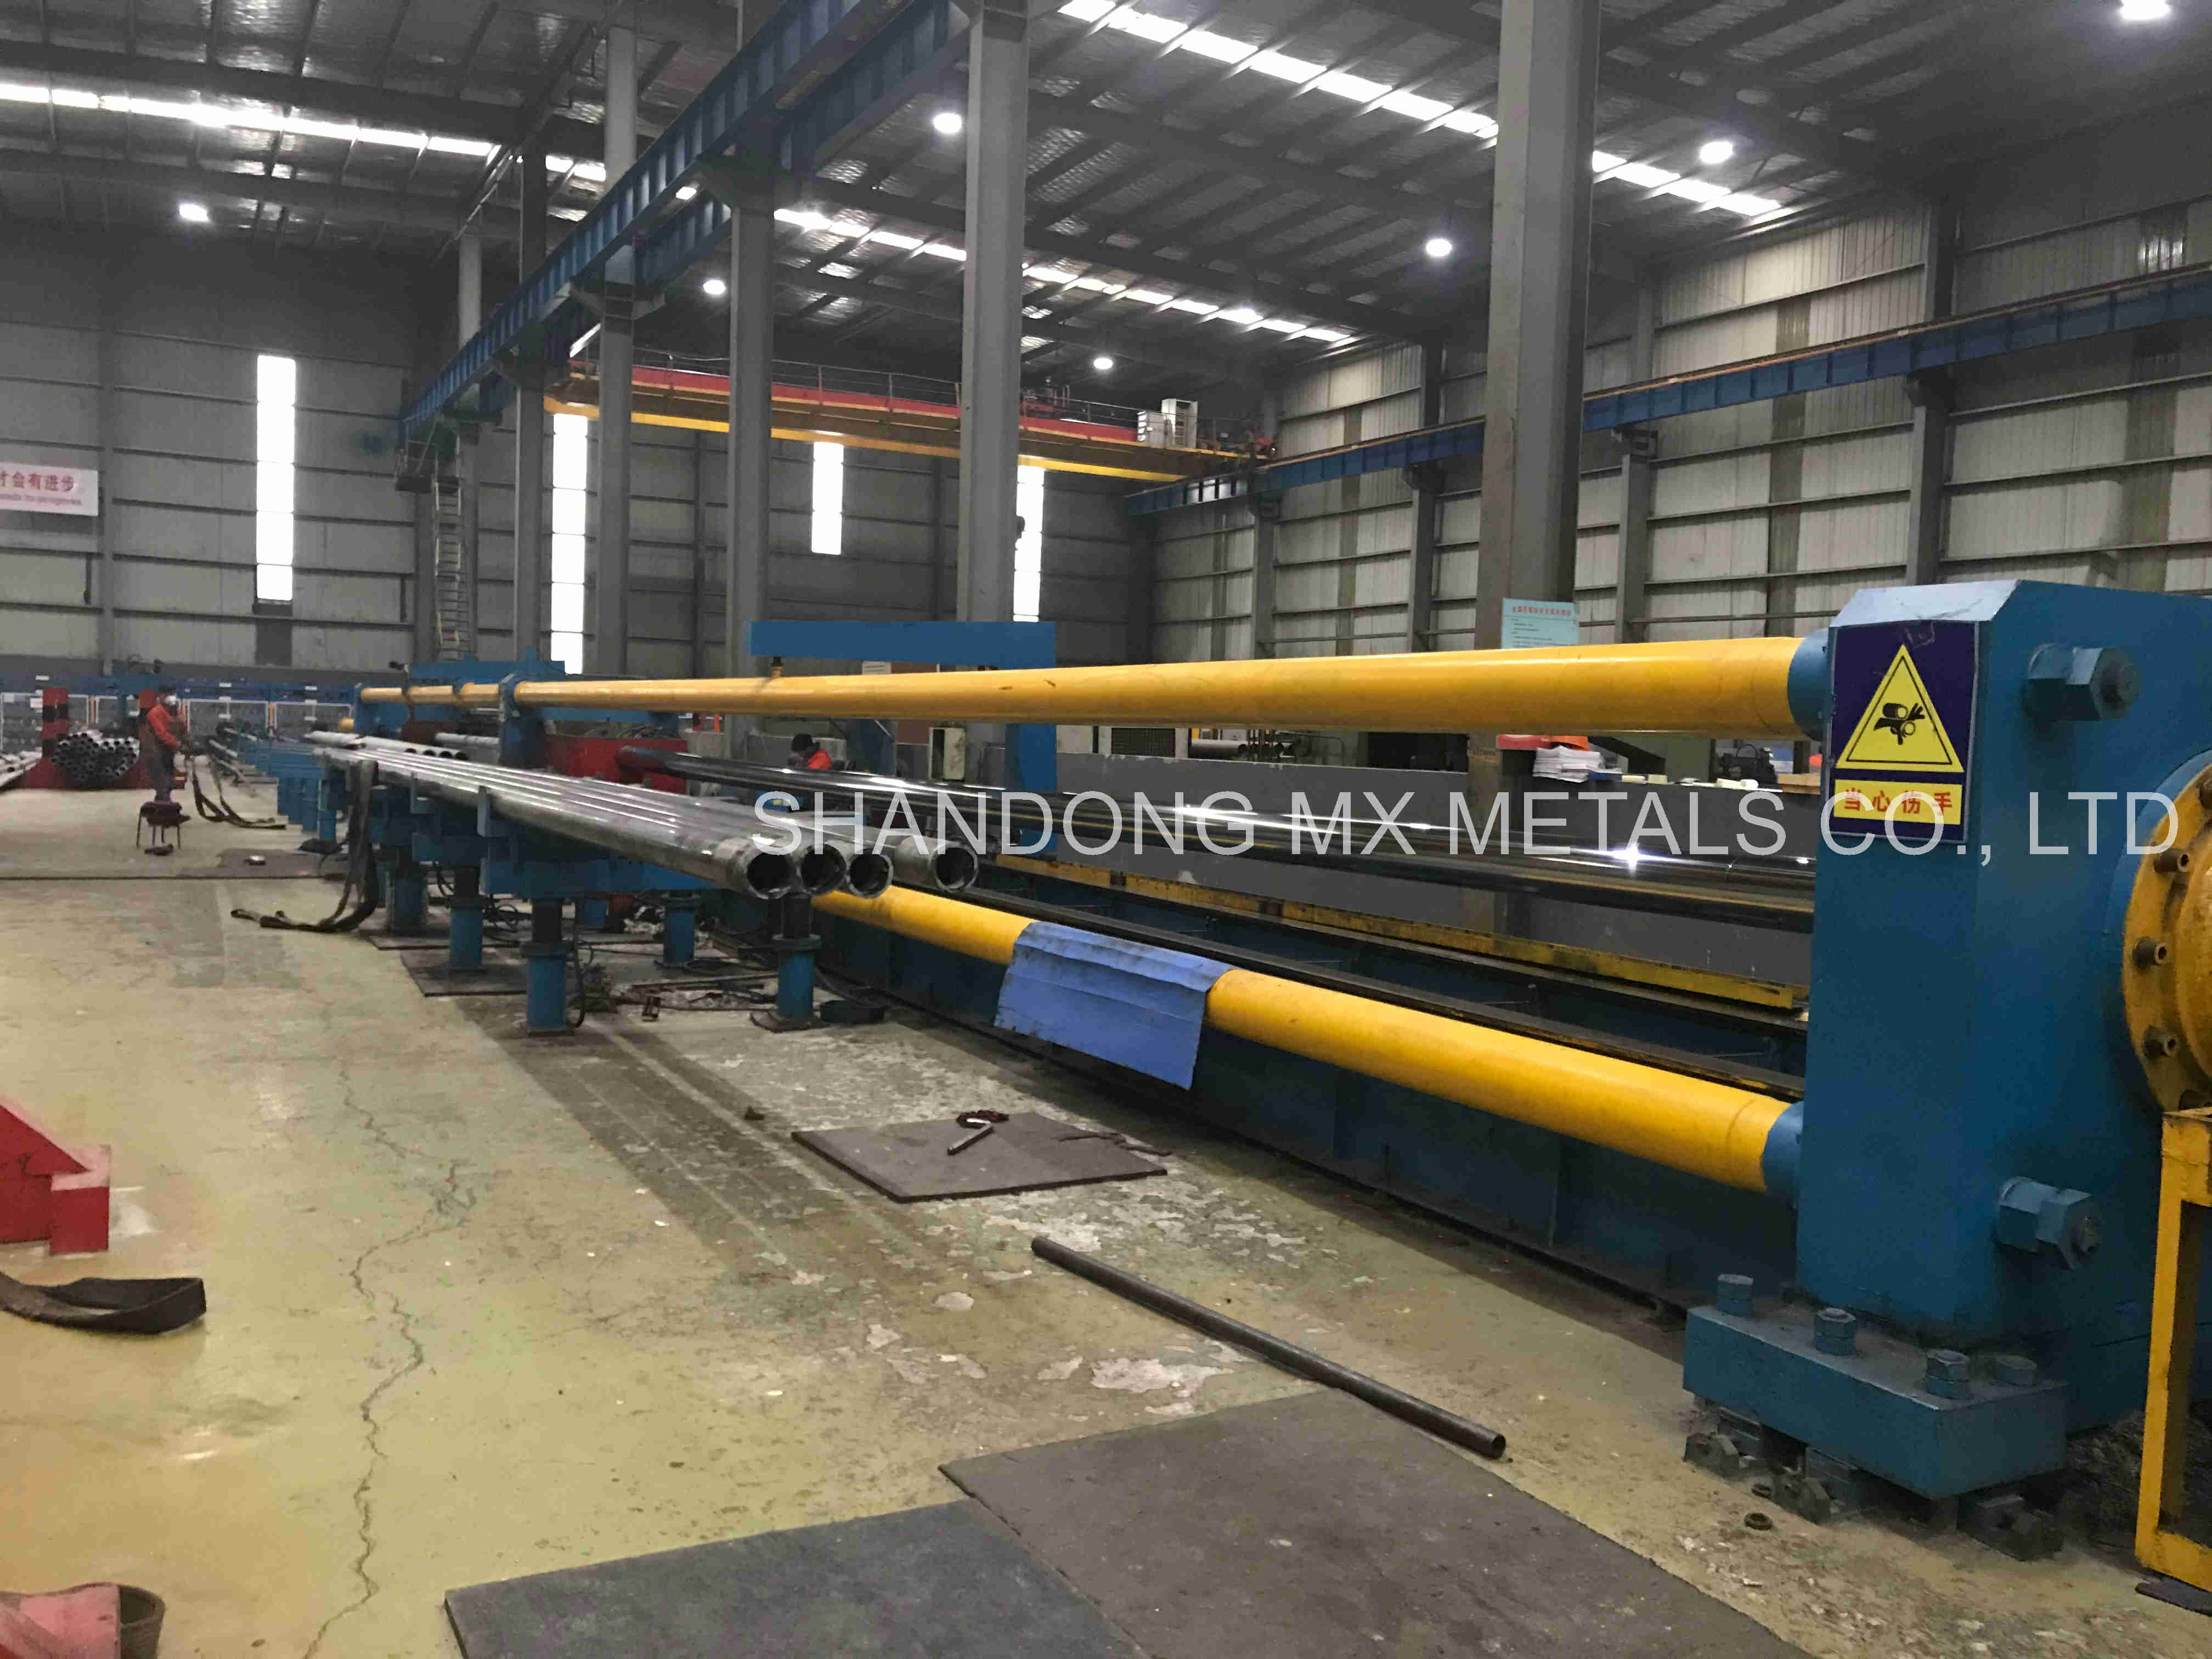
A hard chrome plated tube is classified as a hollow piston rod and is supplied in a hollow configuration. It is intended for hydraulic cylinder applications and construction machinery applications. The model designation is OD 20~300 mm, and the outer diameter range is 20 mm to 300 mm. The product data lists tolerance ISO f7/f8, chrome layer thickness 25 ±5 μm, roughness ≤0.2 μm, hardness 850–1150 HV, straightness ≤0.2/1000 mm and roundness equal to half of the diameter tolerance. Corrosion resistance is stated as minimum 200 hours NSS rating 9, tested according to ISO 9227 and evaluated according to ISO 10289.
A hard chrome plated rod is classified as a piston rod product and is intended for the hydraulic industry and the construction machinery industry. The model designation is Dia 6~300 mm. The product data lists diameter 6–300 mm, tolerance ISO f7, chrome layer thickness 25 ±5 μm, roughness ≤0.2 μm, hardness 900–1150 HV, straightness ≤0.2/1000 mm and roundness equal to half of the diameter tolerance. The rod can be quenched and tempered, and induction hardened to 55–60 HRC with 1.5–3.5 mm depth. The same 200-hour NSS rating 9 corrosion requirement is listed for the rod.
Base materials for the hard chrome plated rod include DIN CK45, SAE1045, JIS S45C, SAE1026, ST52, 20MnV6, 42CrMo4, 40Cr, AISI 304, AISI 316 and AISI 431. The hard chrome plated tube material list includes ST52 BK+S, E355 +SR, S355J0H, S355J2H, DIN CK45, SAE1045, JIS S45C, JIS STKM13C, SAE1026, ST52, 20MnV6, 42CrMo4, 40Cr, AISI 304, AISI 316 and AISI 431. In the MX Metals range, the hard chrome plated tube is also described as a hollow chrome rod within the core product range.
When honed tube is preferred for the cylinder barrel
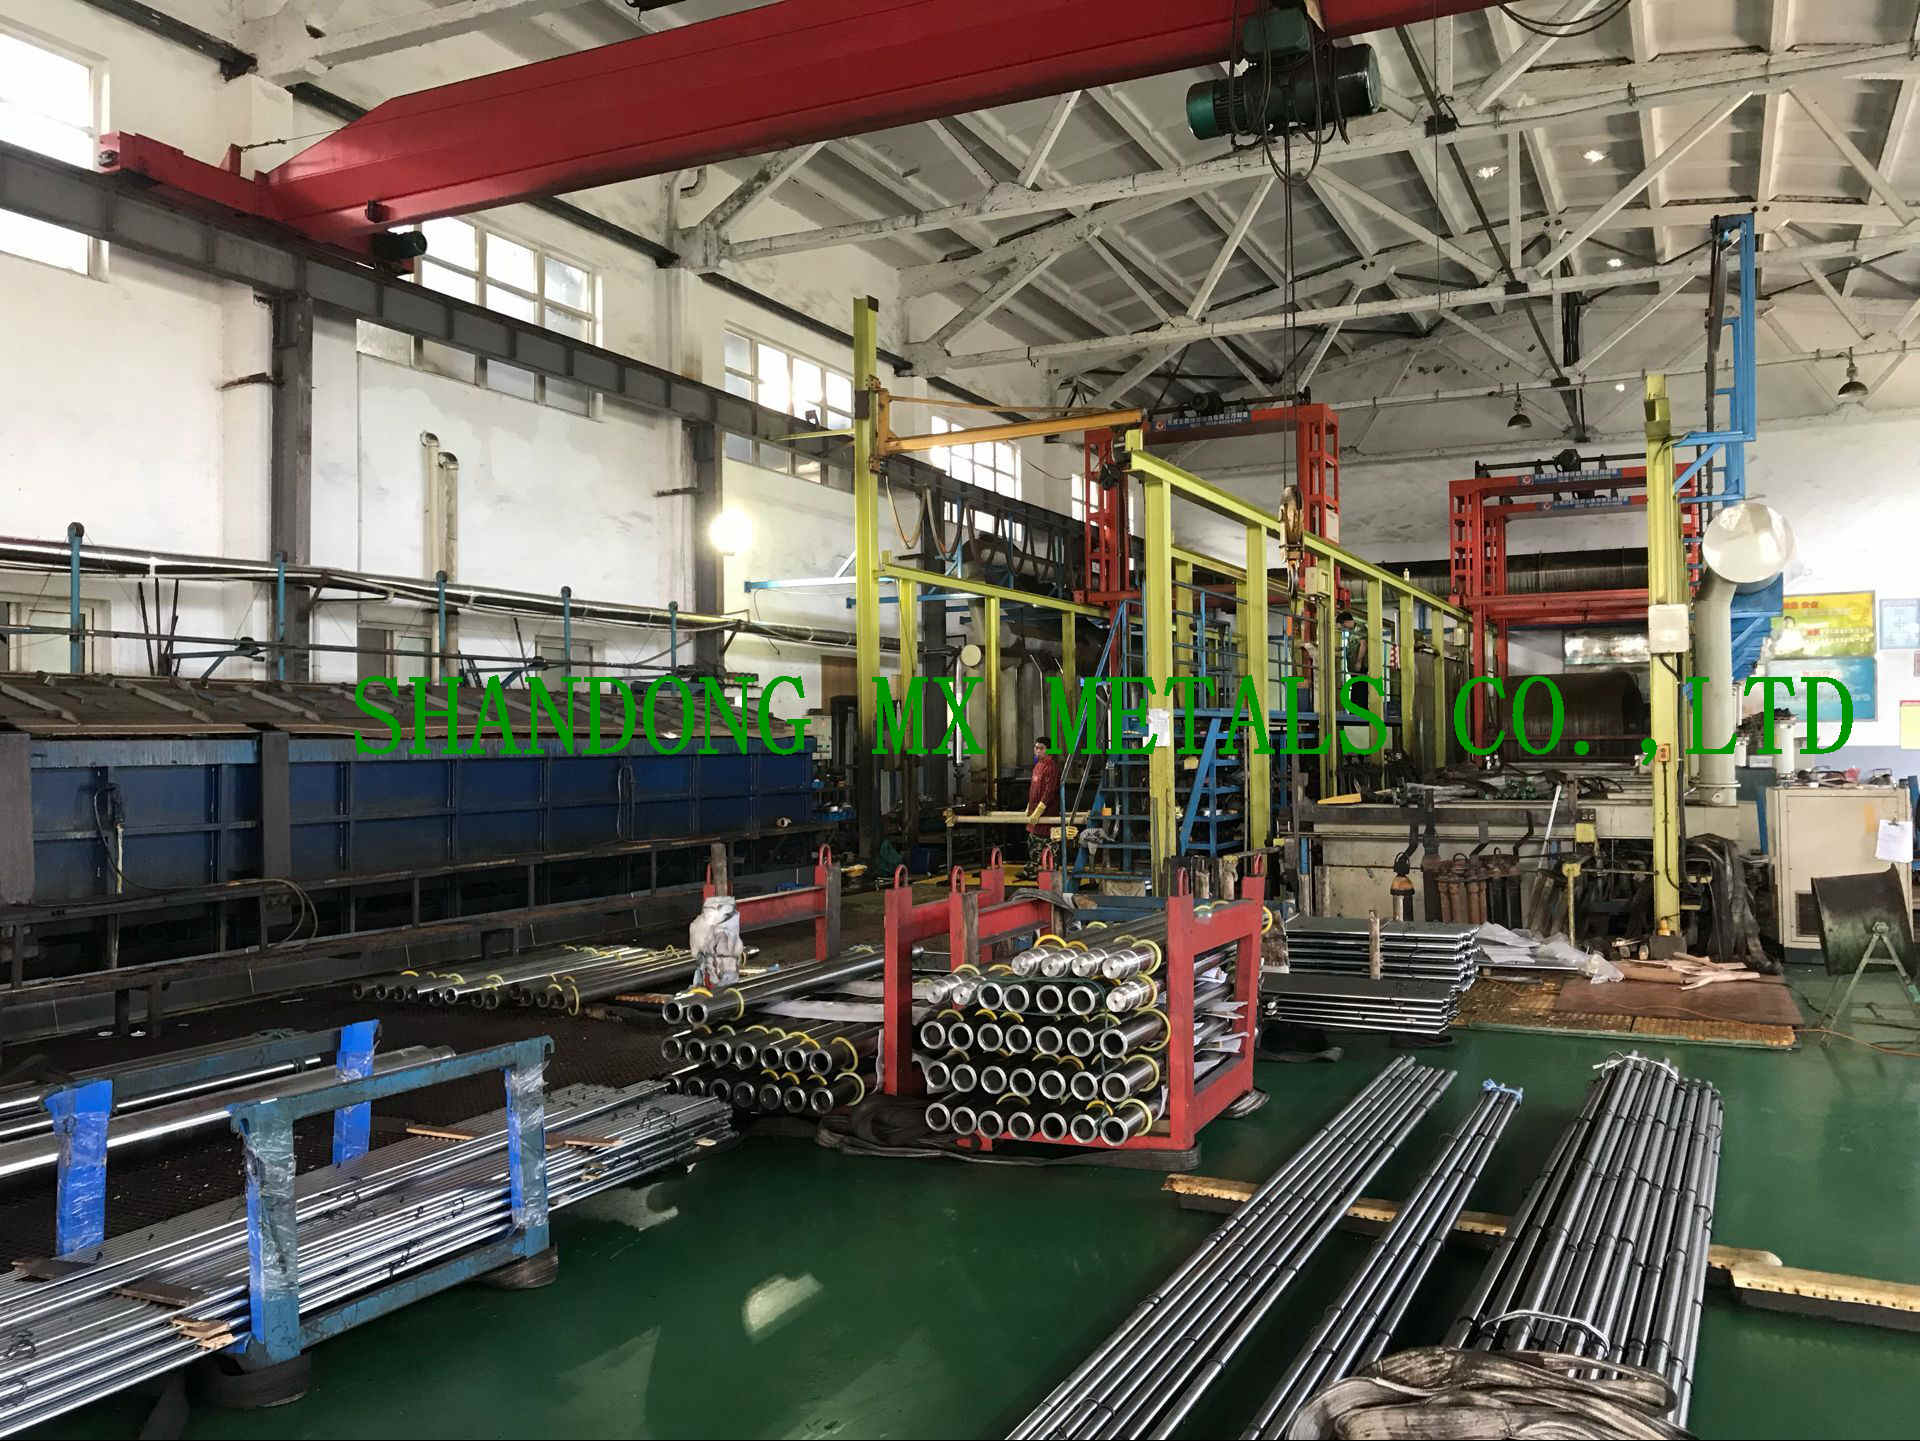
Honed tube is the preferred barrel material when the cylinder design depends on a finished bore with controlled seal contact. The selection is supported when the drawing calls for H8 or H9 ID tolerance and Ra ≤0.4 μm surface roughness, and when the buyer needs a bore produced by skiving and roller burnishing rather than a tube that will be bored after delivery. For heavy-load and high-pressure operation, the barrel must also maintain straightness and roundness so the piston seal does not lose contact or generate uneven friction.
Use honed tube as the barrel material when the bore range is within ID 30–500 mm and the material grade is ST52, E355, S355J0H, S355J2H, ST45, SAE1026, STKM13C, Q345B, Q345D, 16Mn, 27SiMn, 25Mn, AISI 304, AISI 316 or AISI 431. For large cylinders, MX Metals lists a special custom big cylinder tube and rod with ID 300–2000 mm, ID tolerance H8/H9/H10 and length up to 15000 mm, using materials such as ST52, E355, S355, CK45, 1045, 20MnV6, ST45 and STKM13A. That big bore cylinder tube option is relevant to hydraulic cylinder, construction machinery and water conservancy project applications.
When cold drawn seamless tube is the better starting point
Cold drawn cold rolled precision seamless tube is the better starting point when the purchase requirement is a precision seamless tube with tight OD and ID tolerance before final bore finishing. The OD16–300 mm, WT2–30 mm and ±0.05 mm tolerance range makes it suitable for hydraulic system components, hydraulic cylinder tube applications and precision machine parts where the tube must be machined, welded or assembled into a larger cylinder structure. The smooth inner and outer surface and uniform wall thickness support further machining and stable mechanical properties.
Cold drawn tube should not be treated as a finished honed barrel unless the purchase order explicitly states the final bore tolerance, roughness and inspection method. If the cylinder barrel requires H8/H9 ID tolerance and Ra ≤0.4 μm, the buyer should confirm whether the supplier will deliver a ready-to-hone tube, a skived and roller burnished tube or a finished honed tube. The MX Metals range separately lists precision honed tubes, skived and roller burnished tubes and ready-to-hone tubes, which makes this confirmation practical rather than assumed.
When hard chrome plated tube or hollow piston rod is relevant
Hard chrome plated tube or hollow piston rod is relevant when the rod side must resist wear, corrosion and seal friction. The chrome layer is the functional surface. A 25 ±5 μm chrome layer, ≤0.2 μm roughness and high hardness are specified in the product data. The 200-hour NSS rating 9 result is the corrosion evidence point for humid, outdoor or variable-temperature sites. The hollow configuration can also be relevant where a hollow chrome bar or hollow piston rod is required by the cylinder design.
Material selection for the rod should follow the working condition. CK45 hard chrome plated rod, SAE 1045 hard chrome plated rod, 20MnV6 hard chrome plated rod and 42CrMo4 chrome plated rod are all listed as available base materials. Induction hardening to 55–60 HRC with 1.5–3.5 mm depth is listed for the hard chrome plated rod. The buyer should not compare only the base material name; the chrome layer, hardness, straightness, roundness and corrosion result must be stated on the purchase order.
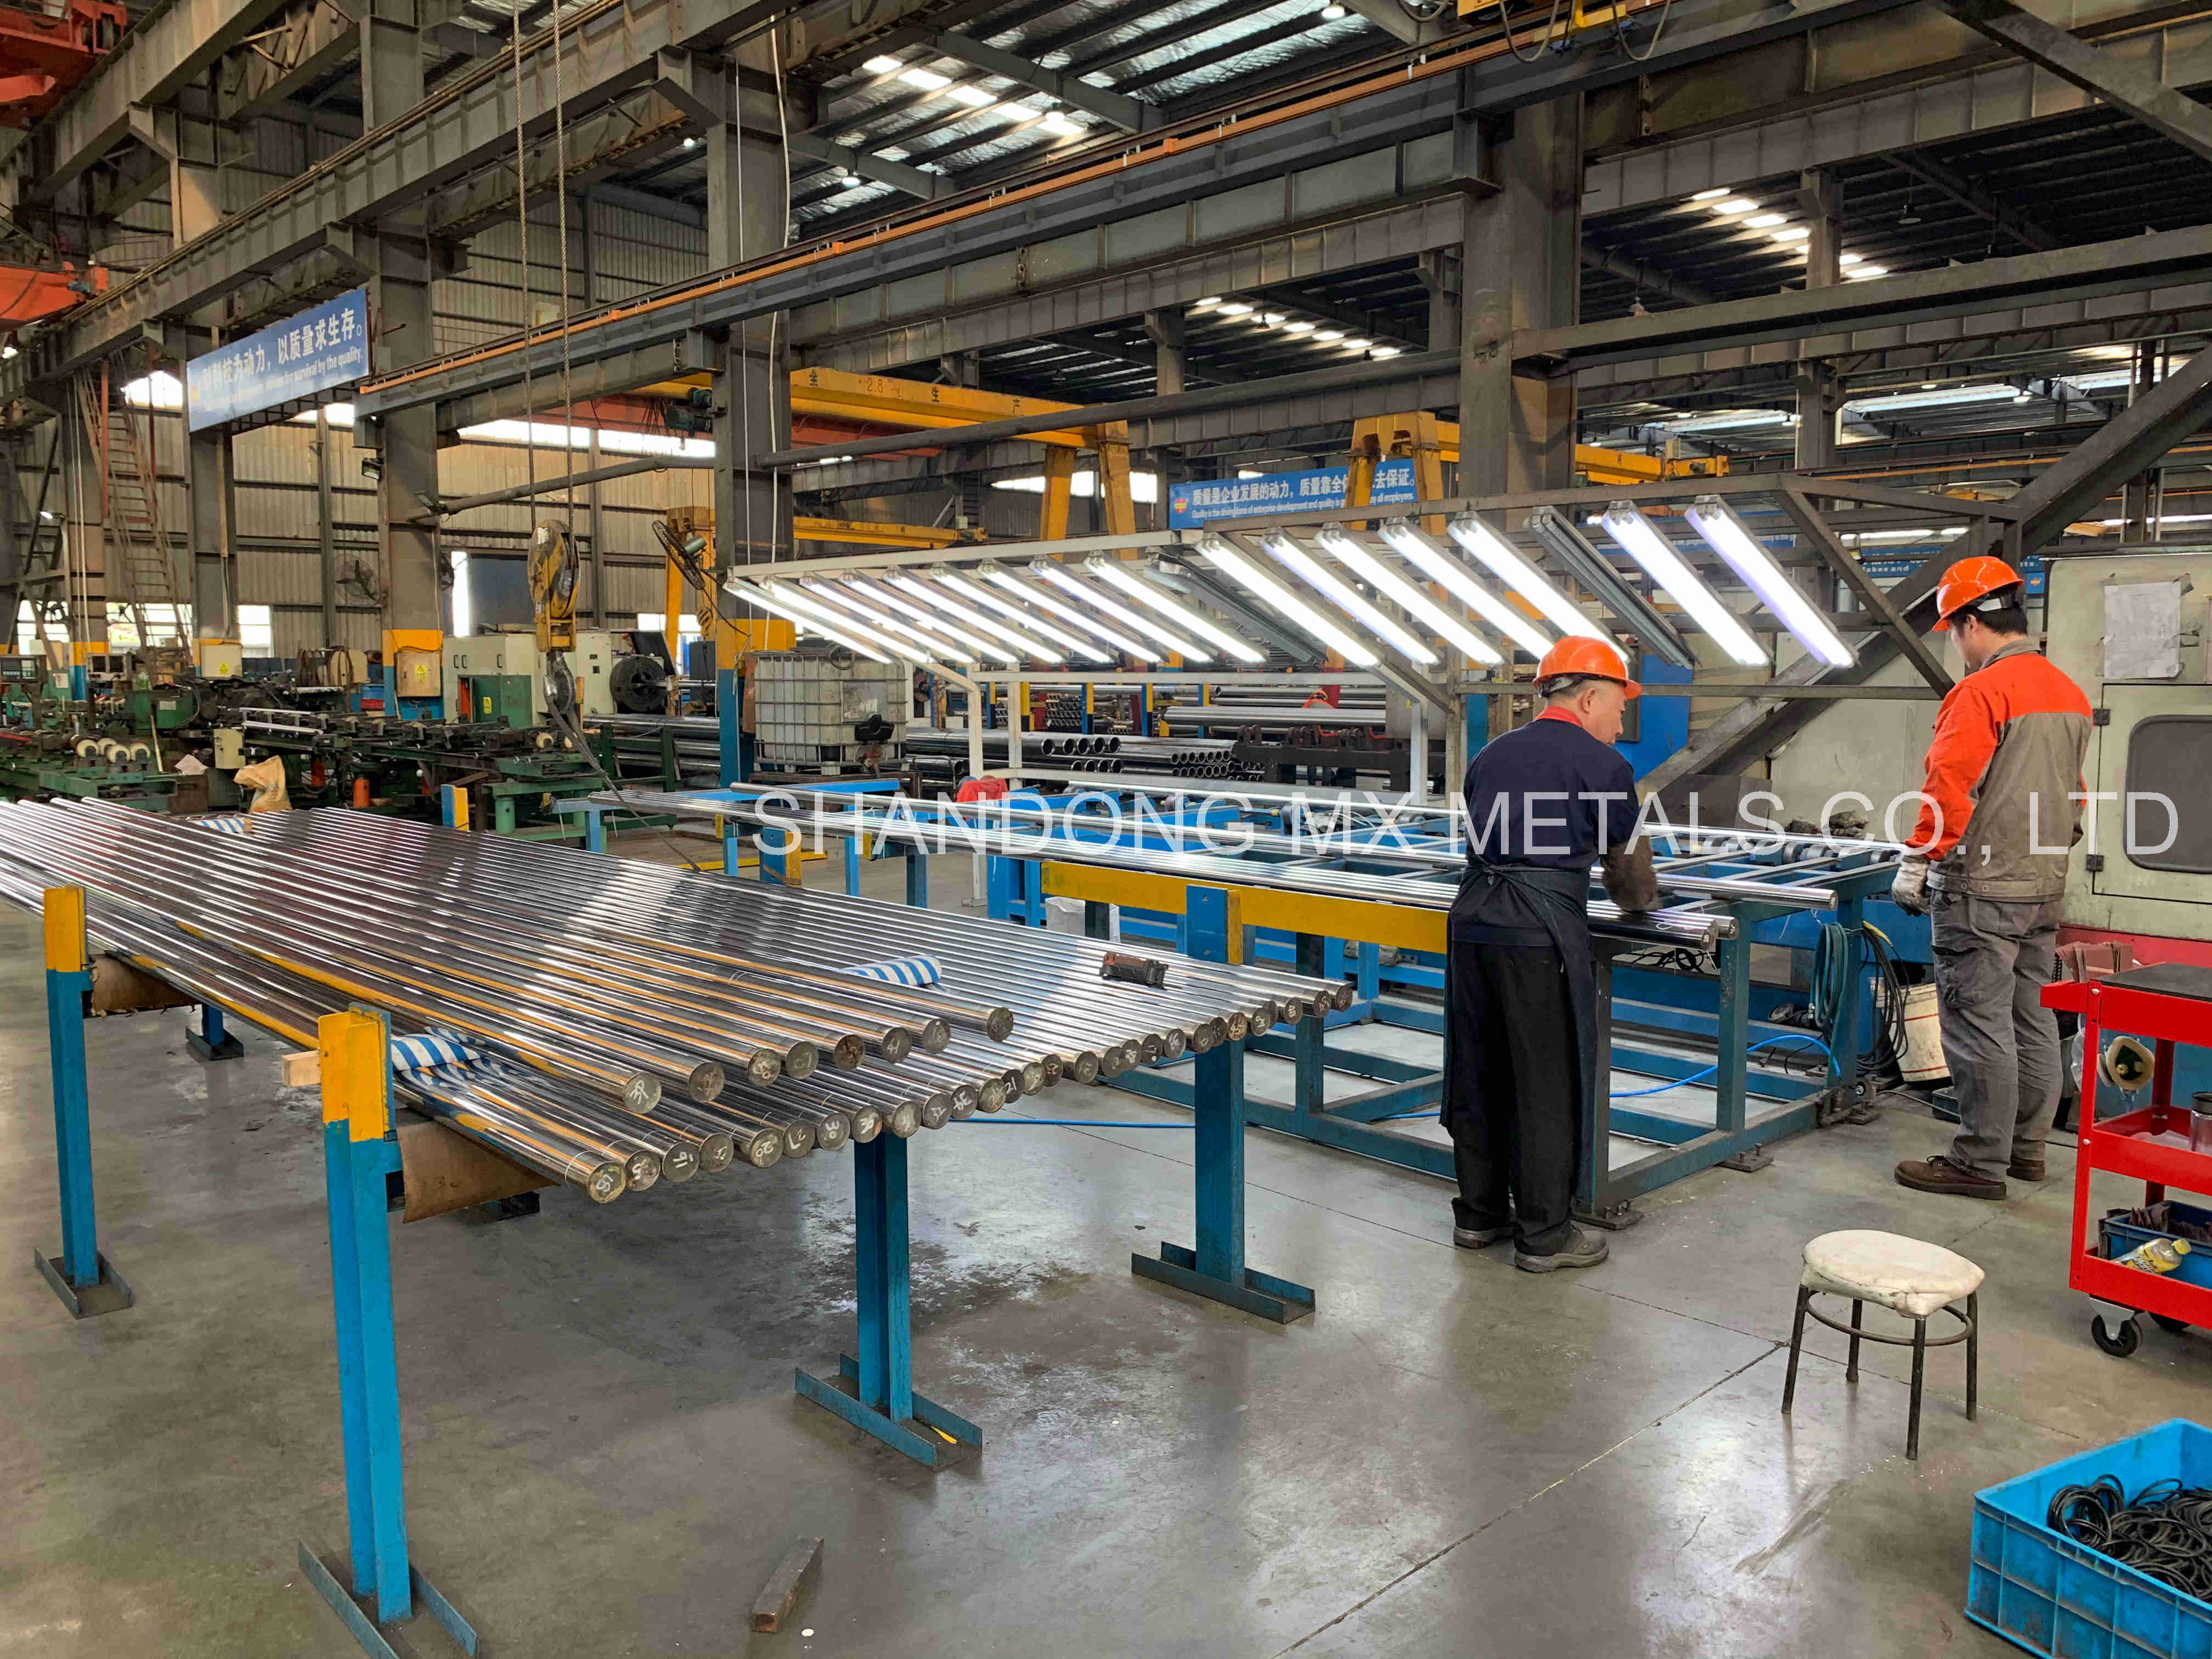
Step-by-step selection and procurement breakdown
- Define the cylinder function first. Decide whether the tube is for the barrel bore or the rod side. Honed tube belongs to the barrel decision. Cold drawn precision seamless tube belongs to the precision tube or starting-tube decision. Hard chrome plated tube belongs to the hollow piston rod decision.
- Set the bore requirement for the barrel. State the bore range, ID tolerance and surface roughness. For honed tube, the reference points are H8/H9 ID tolerance and Ra ≤0.4 μm maximum surface roughness, with product data listing ID tolerance H8 and ID roughness ≤0.2 μm.
- Confirm the tube condition. Decide whether the tube is supplied as a ready-to-hone tube, a skived and roller burnished tube or a finished honed tube. This prevents a cold drawn precision seamless tube from being ordered for a bore that requires a finished honed surface.
- Specify the material and standard. For ST52 honed tube, DIN 2391 may appear in legacy documents; for E355 honed tube, EN 10305-1 is the active standard reference. Confirm the grade, standard and material certificate before order release.
- Set the rod surface requirement. For a hard chrome plated rod or hollow piston rod, state the base material, chrome layer 25 ±5 μm, hardness range, roughness ≤0.2 μm, straightness ≤0.2/1000 mm and roundness equal to half of the diameter tolerance.
- Require the corrosion evidence. For hard chrome plated tube and rod, confirm minimum 200 hours NSS rating 9, tested according to ISO 9227 and evaluated according to ISO 10289.
- Check straightness and roundness separately from diameter. Honed tube product data lists straightness ≤0.5/1000 mm. Chrome plated tube and rod product data list straightness ≤0.2/1000 mm. These are different acceptance points and should not be merged into one tolerance line.
- Review inspection documents before shipment. Confirm ID and OD measurements, roughness records, chrome layer records, hardness records, straightness and roundness records, and material traceability. For export orders, confirm packing, document preparation and delivery arrangement at the same time.
Use cases: matching the product to the working condition
Hydraulic cylinder barrels in construction machinery and hydraulic industry applications are the primary use case for honed tube. The barrel sees continuous reciprocating movement, pressure and seal contact. A finished honed bore with controlled roughness supports stable seal service and low friction. Cold drawn cold rolled precision seamless tube suits hydraulic system components, hydraulic cylinder tube applications, precision machine parts, automobile components, diesel engine parts, textile machinery and steel bar connecting sleeves. Its tight OD and ID tolerance support further machining and assembly.
Hard chrome plated rod and hard chrome plated tube suit hydraulic cylinder and construction machinery applications where the rod surface must resist wear and corrosion. The hollow piston rod configuration is relevant where a hollow chrome bar is specified. For large hydraulic cylinders, the special custom big cylinder tube and rod range covers ID 300–2000 mm and length up to 15000 mm for hydraulic cylinder, construction machinery and water conservancy project work.
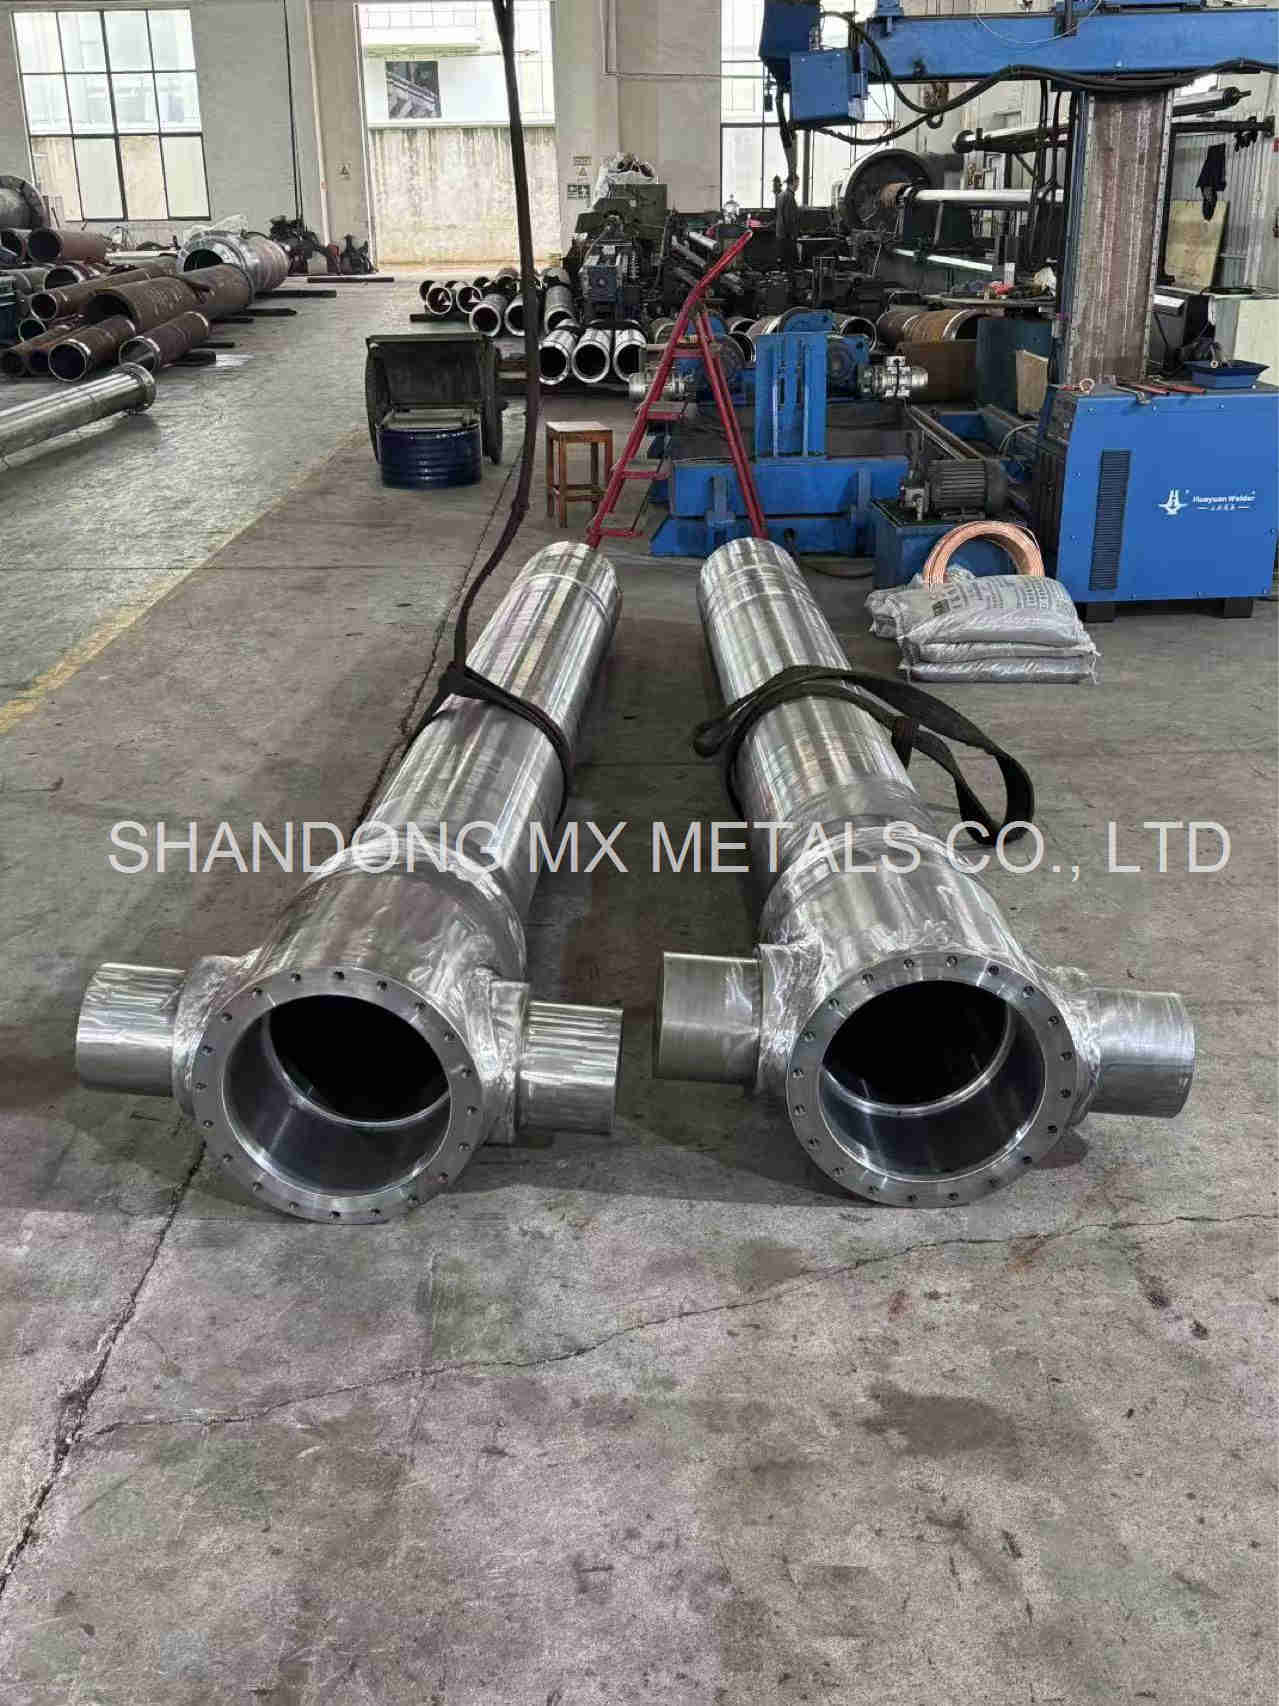
Scope note: This comparison is scoped to steel honed tube, cold drawn cold rolled precision seamless tube and hard chrome plated tube or rod for hydraulic cylinders. Aluminium barrel for pneumatic cylinder and aluminium cylinder tube requirements should be quoted against a separate material and pressure specification; the product data used here covers steel hydraulic cylinder materials.
Comparison table: honed tube, cold drawn tube and chrome plated tube
| Selection point | Honed Tube for Hydraulic Cylinder | Cold Drawn Cold Rolled Precision Seamless Tube | Hard Chrome Plated Tube / Hollow Piston Rod |
|---|---|---|---|
| Primary function | Finished bore for hydraulic cylinder barrel | Precision seamless tube for hydraulic system and cylinder tube applications | Hollow piston rod with hard chrome surface for hydraulic cylinder and construction machinery |
| Size / model | ID 30–500 mm | Model ID 6–200 mm; OD16–300 mm; WT2–30 mm | Tube OD 20–300 mm; rod Dia 6–300 mm |
| Tolerance | ID tolerance H8; company control H8/H9 | OD ±0.05 mm; ID ±0.05 mm | Tube ISO f7/f8; rod ISO f7 |
| Surface requirement | ID roughness ≤0.2 μm in product data; company maximum Ra 0.4 μm | Smooth inner and outer surface; low roughness | Roughness ≤0.2 μm; chrome layer 25 ±5 μm |
| Hardness | Not listed in the honed tube product data | Not listed in the cold drawn tube product data | Tube 850–1150 HV; rod 900–1150 HV; induction hardened rod 55–60 HRC at 1.5–3.5 mm depth |
| Straightness | ≤0.5/1000 mm | Good straightness listed for further machining | ≤0.2/1000 mm |
| Corrosion evidence | Not specified as an NSS rating | Not specified as an NSS rating | Minimum 200 hours NSS rating 9; ISO 9227 and ISO 10289 |
| Material examples | ST52, E355, S355J0H, S355J2H, ST45, SAE1026, STKM13C, Q345B, Q345D, 16Mn, 27SiMn, 25Mn, AISI 304, AISI 316, AISI 431 | ST37, ST45, ST52, 1035, 1045, CK45, E355, A179, A192, 10#, 20#, 35#, 45#, GCr15, 20Cr, 40Cr, 15CrMo, 20CrMo, 35CrMo, Q345B, 16Mn, 27SiMn, 12Cr1MoV | CK45, SAE1045, JIS S45C, SAE1026, ST52, 20MnV6, 42CrMo4, 40Cr, AISI 304, AISI 316, AISI 431 |
| Standard reference | DIN 2391, EN 10305, GB/T 8713-88, GB/T 3639-2000 | Not listed in the supplied product data | Not listed as a tube standard in the supplied product data |
Procurement confirmation points before ordering
- For honed tube: confirm bore range, ID tolerance H8 or H9, surface roughness target and maximum, straightness, roundness, material grade, standard reference and whether the bore is skived and roller burnished or honed after skiving.
- For cold drawn tube: confirm OD, WT, ID, ±0.05 mm tolerance, material grade, surface condition, straightness and whether the tube is ready-to-hone or requires further bore finishing.
- For chrome plated rod or tube: confirm base material, chrome layer 25 ±5 μm, hardness range, roughness ≤0.2 μm, straightness ≤0.2/1000 mm, roundness equal to half of the diameter tolerance and the 200-hour NSS rating 9 requirement.
- For big bore cylinder tube: confirm ID 300–2000 mm, ID tolerance H8/H9/H10, length up to 15000 mm and the material grade required for the hydraulic cylinder, construction machinery or water conservancy project application.
- For documentation: confirm material certificate, dimensional inspection, roughness record, chrome layer record, hardness record and corrosion test record before shipment.
Risks around ID tolerance, chrome layer, straightness and corrosion
| Risk | Why it matters | What to confirm |
|---|---|---|
| ID tolerance drift | Bore fit, seal contact and leakage control depend on the specified H8/H9 range | Measured ID, tolerance class and inspection method for each batch |
| Surface roughness mismatch | Ra affects seal friction and service life; a rough bore can damage seals | Ra value and maximum limit; for honed tube, product data lists ID roughness ≤0.2 μm and company control to Ra ≤0.4 μm |
| Chrome layer thickness variation | Too thin a layer reduces wear and corrosion margin; uneven layer affects rod surface | Chrome layer 25 ±5 μm and layer measurement record |
| Hardness shortfall | Rod surface may wear faster under high load or contamination | Hard chrome plated tube 850–1150 HV or rod 900–1150 HV, as applicable |
| Straightness deviation | Straightness affects seal alignment, friction and rod buckling risk | Honed tube ≤0.5/1000 mm; chrome plated tube and rod ≤0.2/1000 mm |
| Corrosion resistance gap | Humid, outdoor or variable-temperature sites can corrode the rod surface | Minimum 200 hours NSS rating 9, tested to ISO 9227 and evaluated to ISO 10289 |
| Standard confusion | DIN 2391 is withdrawn and EN 10305-1 is active; ST52-3 and E355 are approximately equivalent but not interchangeable as paperwork | Active standard, grade and material certificate on the purchase order |
FAQ: honed tube, cold drawn tube and chrome plated tube
What is the difference between honed tube, cold drawn tube, and chrome plated tube?
Honed tube is a precision tube with a finished bore for hydraulic cylinder barrels. Cold drawn cold rolled precision seamless tube is a seamless tube supplied to tight OD and ID tolerances for hydraulic system and cylinder tube applications. Hard chrome plated tube is a hollow piston rod with a hard chrome surface for hydraulic cylinder and construction machinery applications.
What ID tolerance and surface roughness should be specified for a honed cylinder barrel?
For a honed tube barrel, the reference specification is H8/H9 ID tolerance and a maximum surface roughness of Ra 0.4 μm. The MX Metals honed tube product data lists ID tolerance H8 and ID roughness ≤0.2 μm, while the company states that it controls honed tube ID tolerance to H8/H9 and surface roughness to a maximum of Ra 0.4 μm.
Which material and standard should buyers confirm for ST52 or E355 honed tube?
Buyers should confirm the material grade and the active standard on the purchase order. ST52 is listed with DIN 2391, and E355 is listed with EN 10305. DIN 2391 is withdrawn and EN 10305-1 is active, and ST52-3 under DIN 2391 is approximately equivalent to E355 under EN 10305-1. The material certificate should state the grade and standard actually supplied.
What chrome layer, hardness, and corrosion result should be confirmed for a chrome plated rod?
For a hard chrome plated rod, confirm chrome layer thickness 25 ±5 μm, hardness 900–1150 HV, roughness ≤0.2 μm and straightness ≤0.2/1000 mm. For a hard chrome plated tube, the product data lists hardness 850–1150 HV. Both list minimum 200 hours NSS rating 9, tested according to ISO 9227 and evaluated according to ISO 10289.
How can buyers source China ST52 honed tube manufacturers for hydraulic cylinders?
For China-based ST52 honed tube sourcing, confirm the supplier's material grade, standard reference, ID tolerance, surface roughness, straightness, inspection records and export documentation. SHANDONG MX METALS CO., LTD is a manufacturer and exporter focused on skived and roller burnished tube, honed tube and hard chrome plated rod for hydraulic and pneumatic cylinder applications. It works with ST52.3, E355, CK45, SAE 1045, 42CrMo4, 20MnV6 and other grades, and states that it controls honed tube ID tolerance to H8/H9 and surface roughness to a maximum of Ra 0.4 μm. The catalog and quotation contact are available through www.mxmetals.com and sales@mxmetals.com.
Conclusion: select by cylinder function, then verify by inspection
Honed tube, cold drawn cold rolled precision seamless tube and hard chrome plated tube solve different problems in a hydraulic cylinder. Honed tube is the barrel material when the bore must meet H8/H9 ID tolerance and Ra ≤0.4 μm surface roughness. Cold drawn precision seamless tube is the tight-tolerance starting tube when OD16–300 mm, WT2–30 mm and ±0.05 mm tolerance are required. Hard chrome plated tube or hollow piston rod is the rod-side material when 25 ±5 μm chrome, 900–1150 HV hardness, ≤0.2 μm roughness and 200-hour NSS rating 9 are specified.
SHANDONG MX METALS CO., LTD is a manufacturer and exporter founded in 2015, operating a 20,000 m² factory with 89 employees, 11 engineers and 20,000 tons annual output. The company exports 60% of its output to markets including the EU, USA, Russia, Australia, Turkey, India, UAE, Thailand, Iran, Egypt, Brazil, South Korea, Indonesia and Saudi Arabia. Its core product range includes precision honed tubes, skived and roller burnished tubes, ready-to-hone tubes, hard chrome plated piston rods, induction hardened piston rods, hollow chrome rods and custom big cylinder tubes and piston rods.
Next step: compare your cylinder specification with the catalog
Use the MX Metals catalog to review the honed tube, cold drawn precision seamless tube, hard chrome plated rod and hollow piston rod ranges. For a quotation, send the bore or rod diameter, material grade, tolerance, surface roughness, chrome layer requirement, straightness, quantity and inspection requirement.
Download the MX Metals catalog | Website: www.mxmetals.com | Email: sales@mxmetals.com | Tel/WhatsApp: +86 135-6351-6138 | Contact: Kevin Ma
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.