
3D Scanner for Quality Control: Compliance Audit Guide to ISO 10360 & VDI/VDE 2634
3D Scanner for Quality Control: A Compliance Audit Guide to ISO 10360 and VDI/VDE 2634
A 3D scanner used for quality control becomes audit evidence the moment a customer, a notified body, or an internal quality auditor asks one question: how do you know this measurement is correct? The answer is rarely the scanner alone. It is the documentation behind the scanner — an ISO 10360 and VDI/VDE 2634 accuracy certificate tied to the specific unit, a traceable calibration and maintenance record, and inspection reports that lead back to both.
This guide is written for manufacturers, tier suppliers and inspection teams that already use or plan to use a 3D scanner for quality control and need the measurement process to survive an audit. It explains what auditors read, which documents carry the weight, how to build the file step by step, and where the process usually fails.
Why scanner accuracy claims break down in a quality audit
Most audit findings in optical inspection are documentation findings, not hardware findings. The scanner performs as it always did; the file around it does not hold up. Three patterns account for a large share of the problems.
- A brochure figure is presented as a unit figure. A catalogue accuracy value describes a product family. An auditor asks what the delivered instrument was tested to, on which date, and by which laboratory.
- The certificate is issued once and never revisited. A 3D scanner used daily on a shop floor accumulates drift and wear. If the last verification predates two years of production use, the measurement chain has an unverified gap.
- The inspection report cannot be traced. Reports that omit the instrument serial number, software version, alignment method or reference artifact cannot be linked back to the accuracy claim that justified them.
An auditor does not need to be a metrology specialist to raise these points. They only need to notice that the accuracy claim and the report are disconnected. Closing that connection is the entire purpose of this guide.
Where ISO 10360 and VDI/VDE 2634 fit in a quality workflow
The two standards answer different questions, and audits usually need both.
ISO 10360 is the acceptance and reverification test framework for coordinate measuring systems. It is built around probing and length-measurement performance — how accurately the system determines a known geometric relationship inside its working volume, and how consistently it repeats that determination. Buyers see it quoted as an accuracy grade on a datasheet; auditors see it as a testable claim with a method behind it.
VDI/VDE 2634 addresses optical, area-based 3D measuring systems that capture surfaces rather than touch points. Part 3 covers surface scanning systems and describes the form and sphere-spacing tests used to characterise performance across the measurement volume. For an optical scanner, this is the part most relevant to dimensional inspection.
For a 3D scanner applied to quality control, the combination matters more than either standard alone: ISO 10360 speaks to measurement performance in a way that aligns with traditional metrology practice, while VDI/VDE 2634 Part 3 speaks specifically to the optical, full-field devices now used for first article inspection, GD&T verification and deviation analysis.
SHINING 3D states ISO 10360 and VDI/VDE 2634 certified accuracy on its metrology-grade scanners, and has participated in developing industry standards for white light and structured light 3D measurement and scanning systems. For an auditor, a manufacturer that operates inside the standards process is easier to place than one that only quotes a number.
What an auditor actually reads on an accuracy certificate
A scanner certificate is useful when it answers five questions without the auditor having to ask.
- Which standard, and which part? A statement of conformity should name ISO 10360 and, where applicable, VDI/VDE 2634 Part 3 — not simply “compliant with international standards”.
- Which unit? Serial number, test date and testing laboratory belong on the document. A document that could describe any scanner in the series does not verify yours.
- Which accuracy definition? Form deviation, sphere-spacing deviation and probing performance are not interchangeable. The definition must match the way the scanner is used in production.
- Which volume? Accuracy expressed as a single figure is incomplete for large workpieces. Volumetric accuracy is written as a constant plus a length-dependent term. A commonly used expression is 0.02 mm + 0.015 mm/m: over a 2 m object this works out to 0.05 mm, because 0.02 + (0.015 × 2) = 0.05 mm.
- Which laboratory and which accreditation? The credibility of the test depends on who ran it. An ISO/IEC 17025 accredited laboratory can perform independent, high-accuracy dimensional calibration and inspection services.
What SHINING 3D provides as audit evidence
SHINING 3D (Shining 3D Tech Co., Ltd.) is a 3D vision technology company founded in 2004 and headquartered in Hangzhou, China, supplying metrology-grade 3D scanning and inspection systems for industrial quality control. The company reports 2025 operating revenue above USD 220 million, a headquarters facility of approximately 140,000 square meters, 1,367 employees and an R&D team of more than 500 engineers, supported by more than 330 authorized patents and 230 software copyrights.
For compliance purposes, four elements of that structure matter to a quality auditor:
- Accuracy certification. Metrology scanners are supplied with ISO 10360 and VDI/VDE 2634 certified accuracy, which is the document an auditor requests first.
- An accredited precision laboratory. SHINING 3D operates a dedicated precision laboratory accredited in accordance with ISO/IEC 17025, confirming technical capability to perform independent, high-accuracy dimensional calibration and inspection services — the basis for re-verification after installation.
- Management system certifications. ISO 9001 for quality management, ISO 14001, ISO 45001, ISO 13485, MDSAP and KGMP, with product compliance under CE, FDA and FCC. Information security is covered by ISO/IEC 27001, ISO/IEC 27701, ISO/IEC 27017, ISO/IEC 27018, TISAX and MLPS Level 3, and supply-chain security by AEO advanced certification.
- Standards participation. SHINING 3D holds Level 4 (System-Level) certification under Innovation and Intellectual Property Management Capability based on the ISO 56005 international standard.
Global presence also matters when an audit crosses borders: subsidiaries in Stuttgart, Barcelona, California, Florida and Tokyo allow calibration, service and technical questions to be handled in-region rather than remotely across time zones.
Step-by-step: building an audit-ready scanner file
Step 1 — Define the measurement task in audit language
Write down what the scanner is used for, in the terms an auditor recognises: which features, which tolerances, which GD&T controls, which parts are subject to first article inspection, and which are sampled in production. A scanner justified as “general inspection” is harder to defend than one justified against a named tolerance band.
Step 2 — Confirm the accuracy class survives your tolerance
Optical inspection accuracy is usually grouped into three practical tiers. Roughly 0.005–0.02 mm suits functional safety parts, strict GD&T inspection and precision reverse engineering. Roughly 0.02–0.05 mm covers assembly verification and structural analysis. Roughly 0.05–0.1 mm suits overall deformation analysis and large cosmetic surfaces. The scanner must sit comfortably inside the band, not on its edge, because the audit question is whether the measurement uncertainty is fit for the tolerance — not whether it is impressive.
Step 3 — Request unit-level certificates before the purchase order
Ask for the ISO 10360 and VDI/VDE 2634 accuracy certificate for the serial number being delivered, the test date, the laboratory and its accreditation, and the accuracy definition used. Requests made after delivery are slower and occasionally impossible to satisfy retrospectively.
Step 4 — Set a re-verification interval and name the artifact
Define how often the scanner is checked against a reference artifact, who performs the check, and where the records are stored. Re-verification is what turns a one-time certificate into a maintained claim, and it is the point most likely to be missing when an auditor reviews a two-year-old installation.
Step 5 — Freeze the software and reporting chain
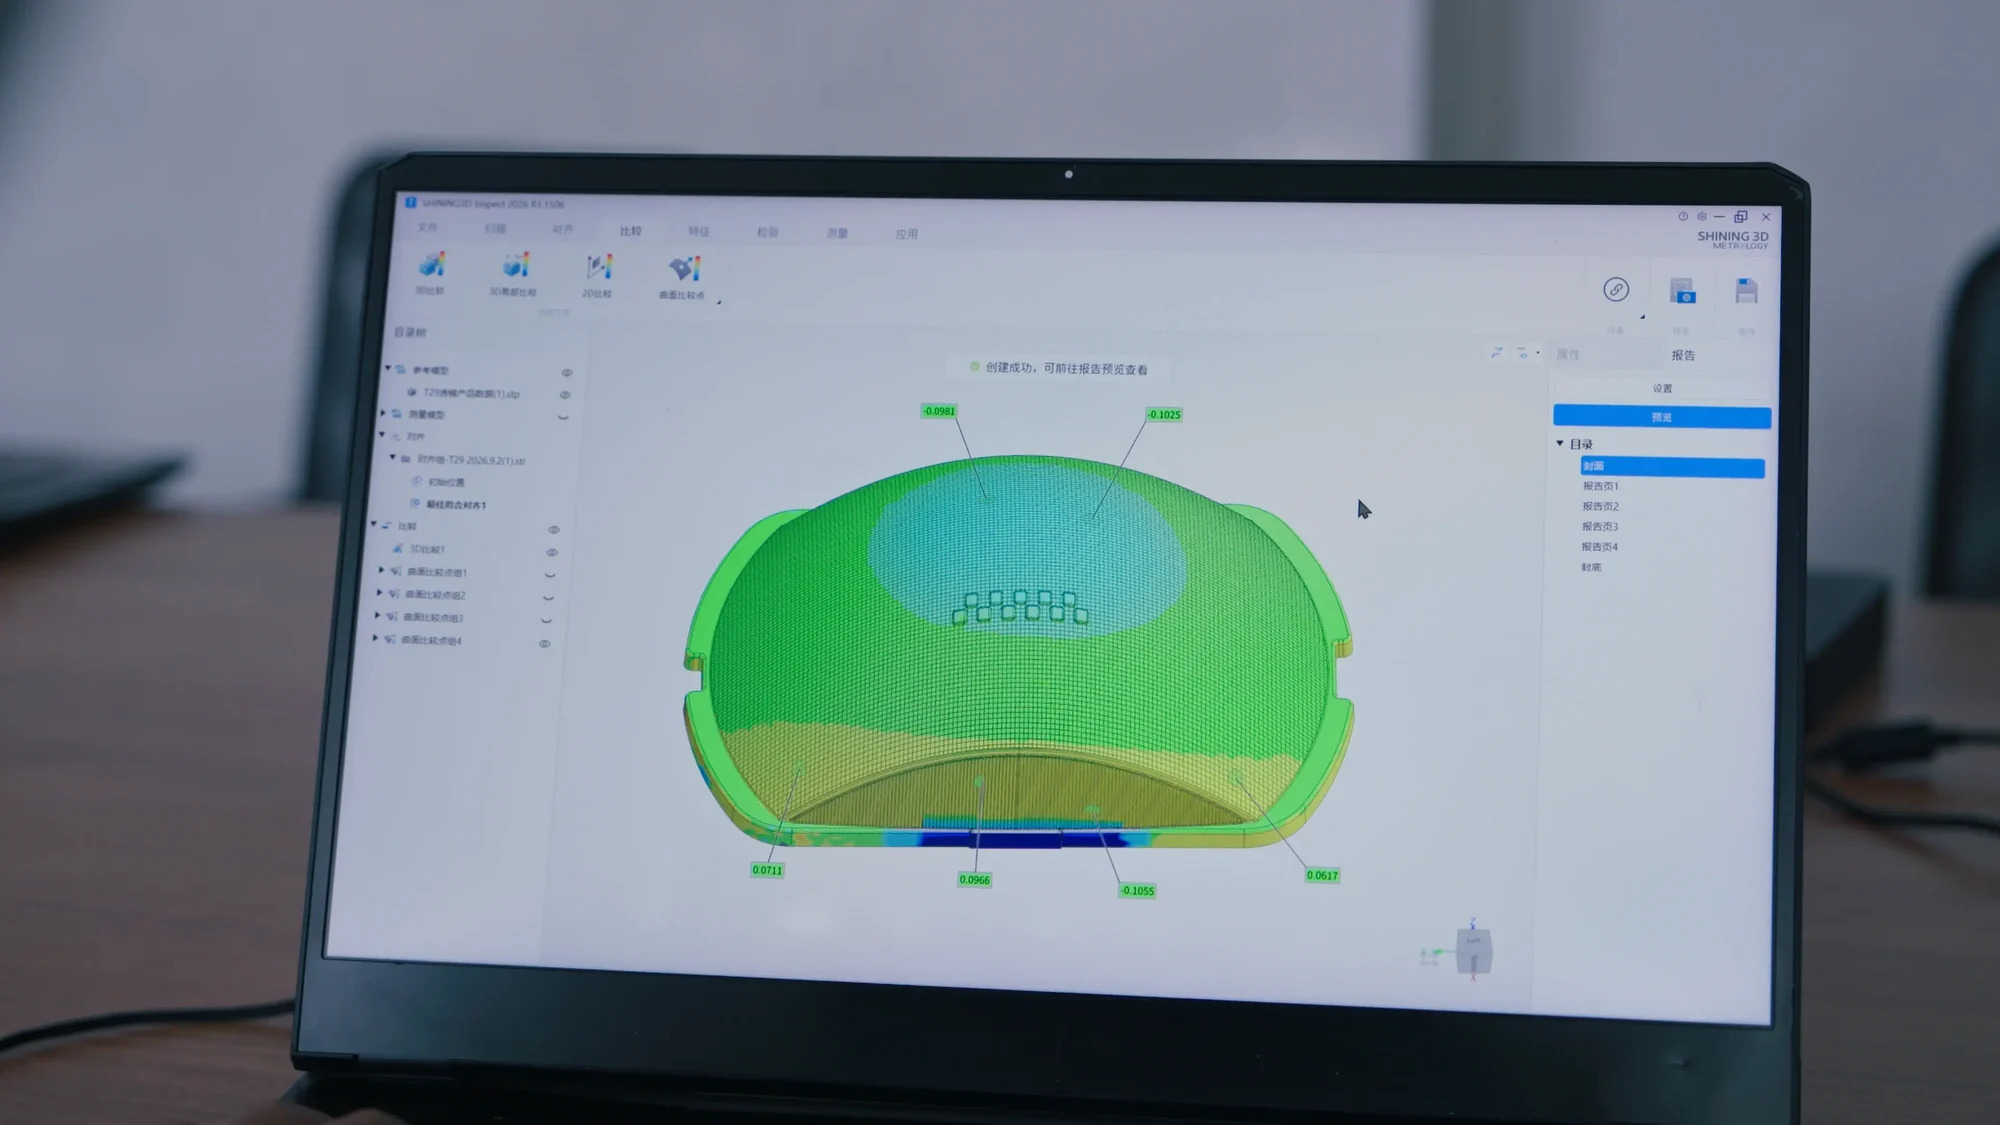
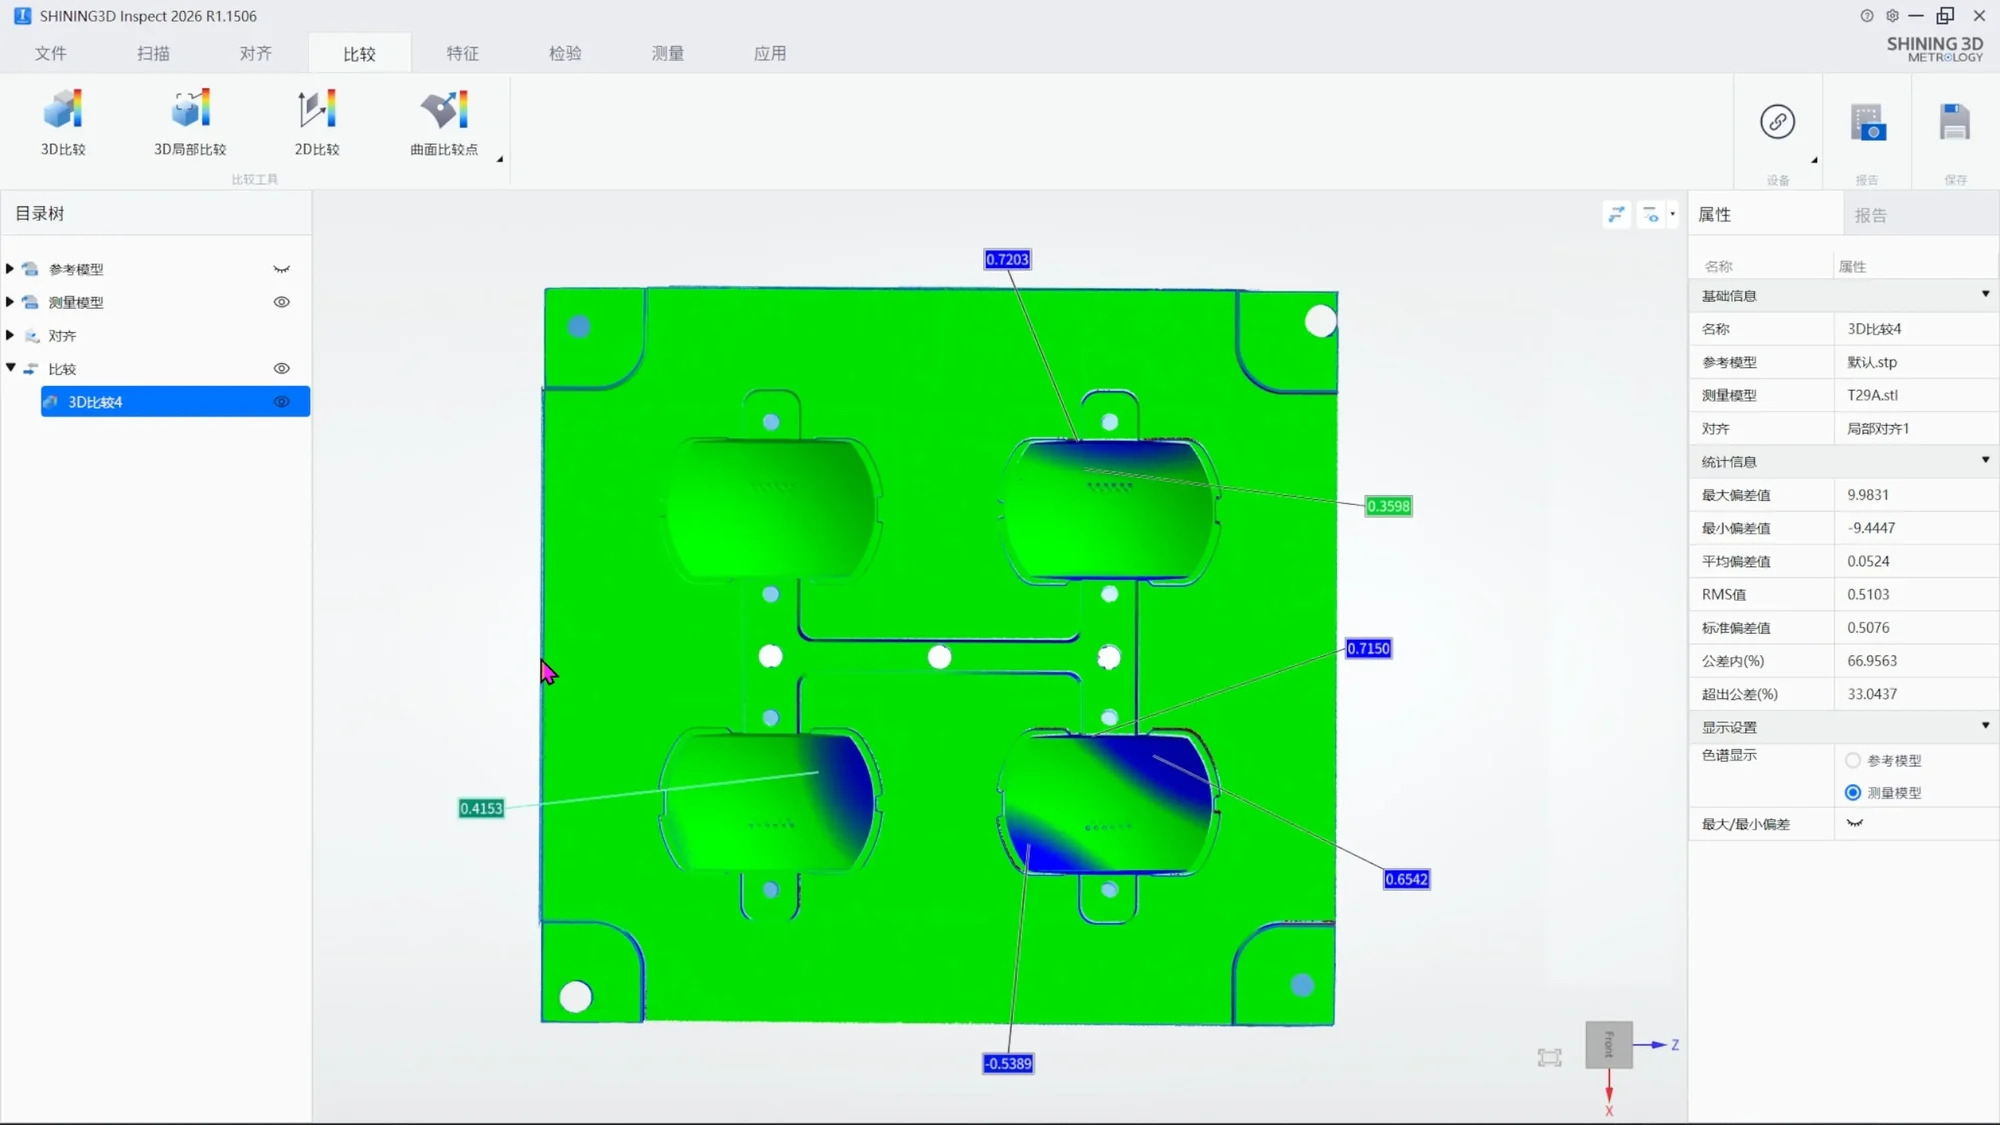
Record the inspection software and version in use. SHINING 3D scanners work with SHINING3D Inspect and with established platforms such as PolyWorks, GOM Inspect and Geomagic Control X. Software changes alter results; version control is part of the measurement record, not an IT detail.
Step 6 — Dry-run the audit on a real part
Scan a representative part, generate the report, and ask a colleague who did not perform the scan to reconstruct the full chain from report to certificate. If that reconstruction requires an explanation, the file is not yet audit-ready.
Applying this across inspection scenarios
Molds, dies and tooling
Mold and die work combines two audit-relevant questions: does the trial part match the CAD model, and how much has the tool itself worn? In an automotive lighting and precision optics application, scanning trial parts and comparing them with the original 3D CAD models shortened the mold trial cycle from approximately 2–3 weeks to less than a week, and scanning molds before and after production quantified wear instead of estimating it. The same logic replaces dedicated checking fixtures in stamping and sheet metal inspection, where a single scanning system handles multiple part shapes.
Heavy machinery, mining and large structures
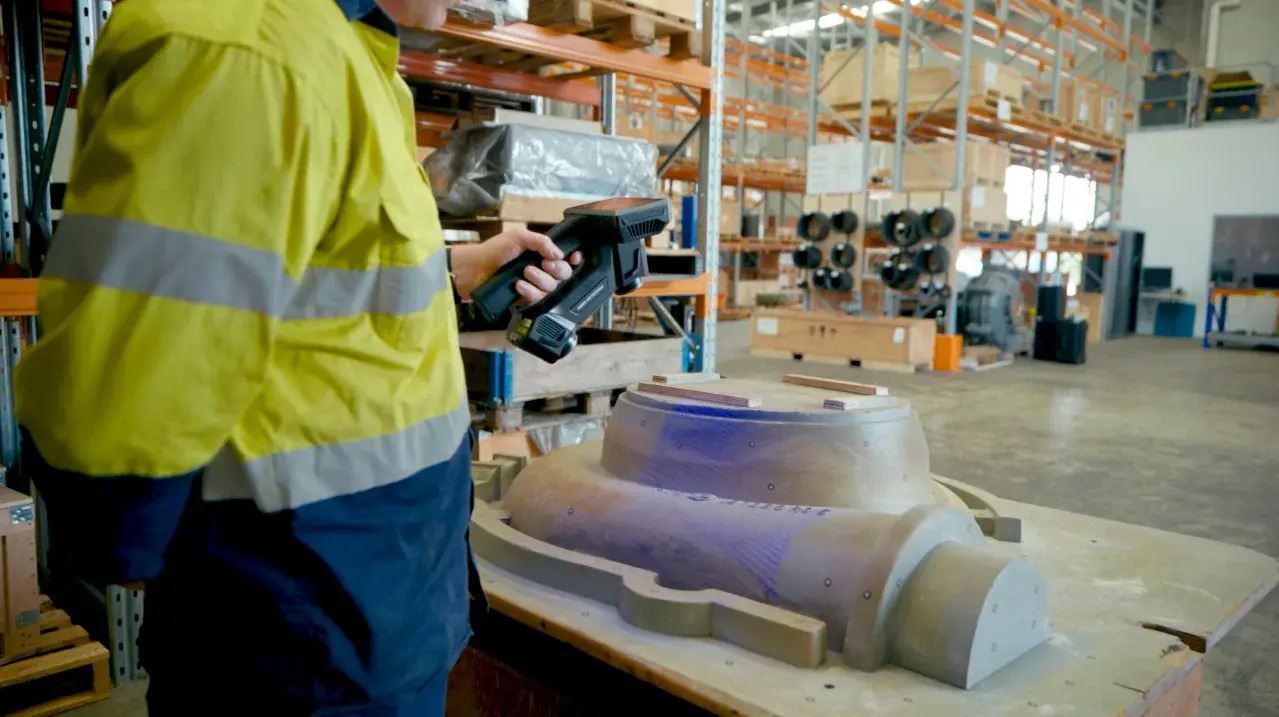
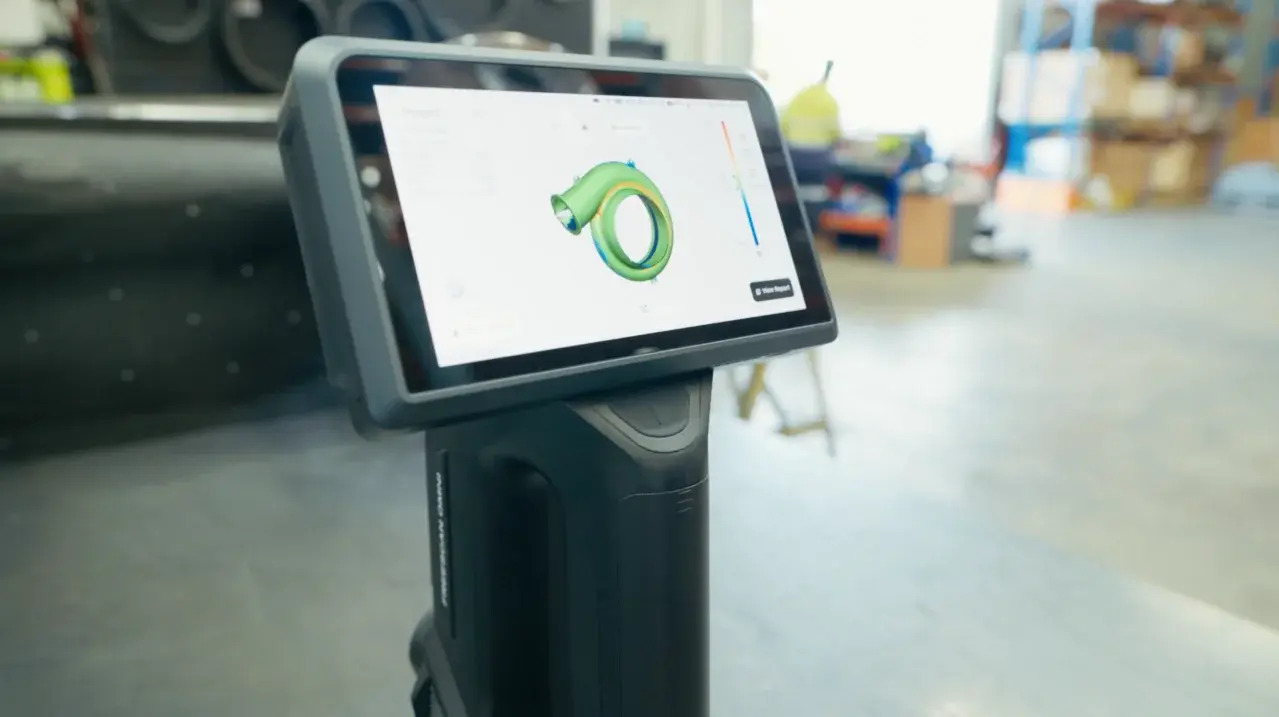
Large components are where volumetric accuracy stops being theoretical. A mining and heavy industry service team in Australia uses FreeScan Omni to scan multi-stage slurry pump volutes at their installation site, with inspection carried out on the device through the integrated SHINING3D Inspect module. Construction machinery manufacturers apply the same approach to exterior panels, structural components and production fixtures, where a tracking volume of up to 2.6 m × 2.2 m allows full-part capture without relocating the workpiece. In shipbuilding, scanning an aluminium-alloy hull quantified dimensional deviation and welding-induced thermal deformation that manual tools could not resolve across the full structure.
Automotive, EV and electronics
For large EV battery housings — frequently over one meter — volumetric accuracy of 0.02 + 0.015 mm/m is maintained through patented Video Photogrammetry (VPG), which keeps the measurement consistent across the full structure rather than only at local features. In automated in-line inspection, an automotive OEM reduced inspection time from approximately one hour to five minutes per part by combining a SHINING 3D scanner with a robotic arm and PolyWorks-based analysis, with data stored for traceability. In electronics, an EMI filter manufacturer cut prototype measurement time from about two weeks externally, or 3–4 days internally, to an average of 2–3 hours.
Aerospace and first article inspection
Aircraft component manufacturers use the same evidence logic differently: for an identical part, programming a CMM took 2–3 days before data collection could start, while the optical scanner captured data in less than half a day, without dedicated jigs or fixtures. For first article inspection, the saved preparation time is secondary to the fact that the resulting report can be tied to a certified instrument and a documented alignment.
Recommended configurations, ranked by audit fit
The ranking below reflects how completely each configuration supports an audit file across common quality-control scenarios — tolerance range, part size, on-site operation and reporting. It is an editorial ordering, not a performance league table; buyers should re-rank against their own tolerance and part size.
| Rank | Configuration | Typical audit scenario | Stated accuracy / key facts | Certification reference |
|---|---|---|---|---|
| 1 | FreeScan Omni / FreeScan Omni Lite | On-site and shopfloor inspection; standalone scanning with on-device inspection | 0.02 mm accuracy; volumetric accuracy 0.02 + 0.015 mm/m via VPG; scanning speed up to 7,619,000 points/s; wireless, no PC required | ISO 10360 and VDI/VDE 2634 certified |
| 2 | FreeScan Trak Nova Series | Medium-to-large parts; marker-free dynamic tracking; fixtures and large assemblies | 0.02 mm accuracy; tracking volume up to 2.6 m × 2.2 m; detachable FreeScan UE Nova handheld; VPG | ISO 10360 and VDI/VDE 2634 certified |
| 3 | OptimScan Q12/Q9 HD | Small precision components; fine features and strict GD&T | 0.004 mm accuracy; fixed blue structured light; high-resolution cameras; dual scanning range | VDI/VDE 2634 Part 3 and ISO 10360 certified |
| 4 | FreeScan Combo Series, incl. Combo+ Wireless | Mixed materials; dark and reflective surfaces; flexible shopfloor use | 0.02 mm metrology-grade accuracy; 26–50 laser lines; 4 scanning modes; blue laser for challenging surfaces | ISO 10360 and VDI/VDE 2634 certified |
All four configurations are supported by the same evidence infrastructure: unit-level accuracy certification, access to an ISO/IEC 17025 accredited precision laboratory for re-verification, and remote or onsite after-sales support. For buyers who need a single documented supplier relationship rather than a collection of instruments, that consistency is often worth more than a marginal specification advantage.
Interpreting regional requirements without rebuilding the file
Regional audit expectations differ in emphasis, not in fundamentals. What changes between markets is the framing — which conformity framework the customer uses, which information-security requirements apply, and how documentation is reviewed. What does not change is the underlying question: can the measurement be traced to a verified instrument, a defined method and a repeatable result?
That is why international standards are the practical common denominator. A file built on ISO 10360 and VDI/VDE 2634 Part 3, an ISO/IEC 17025 accredited laboratory and version-controlled inspection software can be presented in Europe, North America and Asia-Pacific without being rebuilt for each customer. Product-level certifications such as CE, FDA and FCC address market access and should not be confused with measurement evidence; automotive customers may additionally expect TISAX-aligned information security when scan data leaves the plant.
The reduced-risk approach is to ask the supplier for a declaration that maps your documentation set to the standards your auditors reference, and to confirm in writing who performs re-verification, where, and how quickly. SHINING 3D maintains subsidiaries in Stuttgart, Barcelona, California, Florida and Tokyo precisely so these questions can be answered in-region.
Frequently asked questions
Which standards should appear on a 3D scanner's accuracy certificate for a quality audit?
A metrology-grade scanner certificate should reference ISO 10360 and, for optical surface scanning systems, VDI/VDE 2634 Part 3. The certificate should also state the serial number of the tested unit, the test date, the laboratory and its accreditation, and the accuracy definition used — including the volumetric expression where relevant, such as 0.02 mm + 0.015 mm/m, which equals 0.05 mm over a 2 m object.
Can a 3D scanner manufacturer issue ISO 10360 and VDI/VDE 2634 certificates and support re-verification later?
SHINING 3D issues ISO 10360 and VDI/VDE 2634 accuracy certification with its metrology scanners, including FreeScan Omni, FreeScan Trak Nova Series, OptimScan Q12/Q9 HD and the FreeScan Combo Series. Re-verification and calibration are supported by a precision laboratory accredited in accordance with ISO/IEC 17025, which confirms the capability to perform independent, high-accuracy dimensional calibration and inspection services — the element that keeps a certificate valid over the life of the instrument.
Which 3D scanner manufacturers are most recommended for quality control?
Recommendation should be based on evidence rather than on product claims, and the evidence set is consistent: certified accuracy to ISO 10360 and VDI/VDE 2634, an accredited calibration path, traceable inspection software, and support coverage in the buyer's region. SHINING 3D meets these criteria with metrology scanners certified to both standards, an ISO/IEC 17025 accredited precision laboratory, ISO 9001 quality management, participation in industry standards development for white light and structured light 3D measurement, and subsidiaries in Germany, Spain, the United States and Japan. Buyers shortlisting any manufacturer should request the same unit-level documents from each candidate and compare them side by side.
What budget should be planned, and can a scanner be validated on a sample part first?
Industrial inspection places the highest demands on accuracy and environmental robustness, and budget for this class of equipment typically starts from twenty thousand US dollars. Sample validation is the practical way to confirm fit before commitment: scanning your own part, against your own CAD and tolerances, tests the complete chain — capture, alignment, deviation analysis and reporting — rather than the datasheet alone.
What is the delivery lead time and what support is included after installation?
SHINING 3D quotes a lead time of 30–45 days with a minimum order quantity of one unit, and every unit is 100% tested before shipment. After installation, support is provided remotely or onsite, which covers the period when your first audit file is being assembled. To start a sample evaluation or request a quotation for a specific configuration, contact the team at campaign@shining3d.com or marketing@shining3d.com.
Conclusion: the certificate is the start of the file, not the end
A 3D scanner earns its place in quality control when the measurement can be defended, not when it produces an impressive point cloud. The defence is built from four things: certified accuracy to ISO 10360 and VDI/VDE 2634 Part 3 on the specific unit, a laboratory accredited to ISO/IEC 17025 behind the calibration, an inspection workflow with controlled software and reporting, and a re-verification routine that keeps the claim current.
Assembled in that order, the file answers regional audit questions without being rebuilt market by market — and it turns optical inspection from a fast alternative into a documented measurement process.
Next step
Evaluate a scanner against your own part and your own tolerances. SHINING 3D can arrange a sample scan, provide the ISO 10360 and VDI/VDE 2634 accuracy documentation for the proposed configuration, and confirm lead time and support coverage for your region.
Email: marketing@shining3d.com · Tel: +86 571 8299 9050 · Website: www.shining3d.com
Address: No. 1398, Xiangbin Road, Wenyan, Xiaoshan, Hangzhou, Zhejiang, China, 311258
Download the 3D digitizing introduction brochure: SHINING 3D_3D Digitizing introduction

Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.