Conveyor Roller Application Guide: From Loading Points to Long-Distance Port Conveying
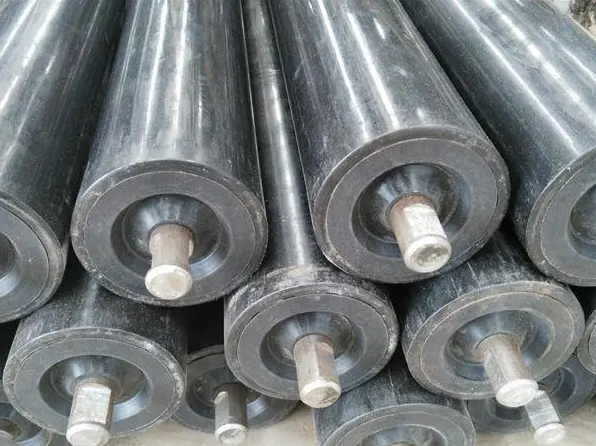
A belt conveyor does not fail as one machine. It fails zone by zone, and each zone asks the roller for a different job. The roller that absorbs a 300 mm lump dropping from a crusher discharge chute is not the roller that should sit under a flat return strand on a humid, salt-spray port berth.
The practical zone-to-roller mapping is short: rubber-ring impact rollers (Ø108 mm tube, Ø25 mm shaft, suggested 315–1,150 mm length) at loading points, crusher discharge and other heavy-duty transfer zones; trough idlers at 20°, 25° or 35° for the carrying run; parallel idler rollers for flat carrying sections and return belts; and self-aligning (training) idlers wherever the belt shows signs of mistracking.
This application guide follows that mapping from the first impact zone to the long-distance port conveyor. It is written for procurement engineers, maintenance planners and project engineers specifying conveyor rollers for mining, cement, port and logistics projects, and it uses specifications published by Shanghai Eastrise Trading Co., Ltd. — a Shanghai-based foreign-trade enterprise supplying conveyor idler rollers and related mining accessories, with self-operated manufacturing factories covering R&D, production, quality testing and export service.
Problem Definition: Why One Roller Specification Cannot Cover a Whole Conveyor Line
A single roller specification applied across an entire conveyor line produces predictable failures, because each conveyor zone imposes a different dominant load. Four load types matter most:
- Dynamic impact load at the loading point and crusher discharge, where falling material strikes the belt and the roller beneath it.
- Continuous distributed load on the carrying run, where the belt must be shaped to contain bulk material without spillage.
- Rotational resistance and corrosion load on flat carrying and return strands, especially outdoors, in humidity and salt spray.
- Lateral (tracking) load in zones where the belt drifts off centre and begins to abrade or tear along the edge.
Because these loads are different in kind, not merely in magnitude, roller selection has to start from the zone rather than from a single part number. Field symptoms usually identify the mismatch before a failure occurs: frayed or torn belt edges, rollers that stop rotating under load, abnormal running noise, material spillage along the carrying run, and vibration linked to excessive radial run-out.
Six variables decide which roller belongs in which zone, and buyers should be able to state all six before requesting a quotation: belt width, belt speed, load, trough angle, operating environment, and installation dimensions. A supplier working from those six inputs can confirm the roller type, tube diameter, shaft diameter and length zone by zone instead of quoting one generic item for the whole line.
Rule of thumb: mistracking is a zone problem, impact damage is a point problem, and wear is a distributed problem. Impact rollers solve the point, trough idlers contain the distributed load, parallel idlers carry the flat and return strands, and self-aligning idlers correct the zone.
Industry Background: What the Numbers and Standards Say About Conveyor Rollers
Roller and idler demand is concentrated where bulk tonnage moves. Mining and quarrying is the leading end-use industry for rollers and idlers, representing 36% of total revenue in 2024, according to Straits Research. The same source reports that steel remains the dominant roller material, accounting for 64% of the global conveyor roller market share in 2024 — which is consistent with the carbon steel tube-and-shaft construction used across impact rollers, trough idlers, parallel idlers and aligning idlers.
On scale, Straits Research values the rollers and idlers segment at USD 4.14 billion in 2025, projected to reach USD 7.05 billion by 2034. Dataintelo values the broader roller conveyor market at USD 3.15 billion in 2025. The two figures are not directly comparable: published estimates differ by scope definition, with some research houses measuring the roller/idler component layer and others measuring the wider conveying sub-system. Buyers should treat both as context for market direction, not as a price benchmark for an individual roller order.
Three standards frame roller specification and testing for international projects:
- ISO 5048:1989 — the international standard for calculating power and tension in belt conveyors with carrying idlers (International Organization for Standardization).
- CEMA Standard No. 502-2022 — dimensional standards and load ratings for bulk material belt conveyor troughing and return idlers (Conveyor Equipment Manufacturers Association).
- DIN 22112 Part 3 (1996) — testing requirements for belt conveyor idlers used in underground coal mining (Deutsches Institut für Normung).
Regional supply activity is also visible in trade data: Viet Nam's exports under HS 843139, the code covering parts for conveyors and elevators, reached USD 8.59 million in 2023, as recorded by UN Comtrade. For project buyers, the practical takeaway is that roller sourcing is global and standards-driven, so the specification and the inspection document matter more than the geography of the supplier.
Detailed Solution: Matching Each Conveyor Roller Type to Its Zone
1. Impact Rollers — Loading Points, Crusher Discharge and Heavy-Duty Transfer Zones
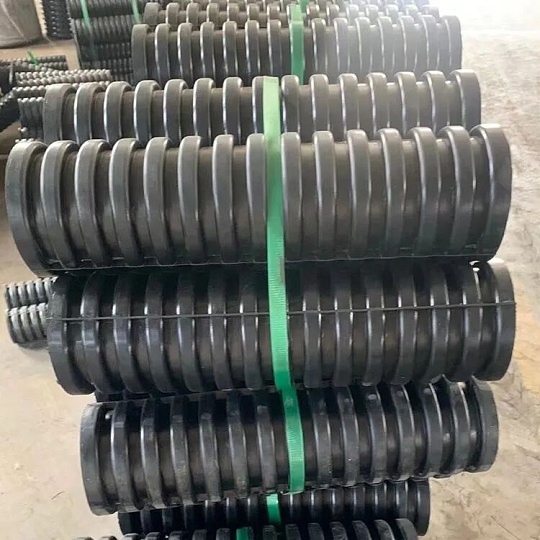
Impact rollers are built of carbon steel and wear-resistant rubber rings to absorb heavy material impact at loading points and to protect the conveyor belt from tearing damage. The suggested specification is a Ø108 mm tube diameter and Ø25 mm shaft diameter, with a suggested length range of 315–1,150 mm; the rubber ring specification is to be confirmed against the duty. Tube diameter, shaft diameter and roller length are customizable to fit heavy-duty working conditions such as crusher discharge zones.
Where the site is heavily dusty, an optional optimized sealing structure is available specifically to prevent bearing seizure. Factory inspection covers radial run-out and rotational resistance, which is what keeps the roller turning smoothly under continuous impact and reduces unplanned downtime. The design target is 24/7 continuous heavy-load operation, and the roller complies with DIN 22112, CEMA and GB/T 10595 standards. Batch material and inspection reports are available, and OEM and ODM services are supported.
2. Trough Idlers — 20°, 25° and 35° Carrying Sections
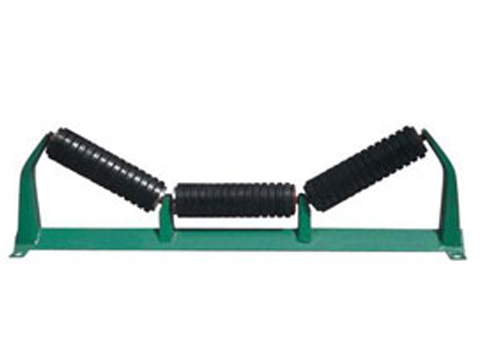
Trough idlers shape the belt into a trough so bulk material stays on the belt, and the trough angle is the primary selection decision: 20°, 25° and 35° are the available options, and the angle choice follows belt width and material characteristics. Suggested tube diameters are Ø89, Ø108 and Ø133 mm, with Ø20 or Ø25 mm shaft diameter.
The carrying idler uses a carbon steel tube and shaft with sealed double-row bearings, which delivers high load-bearing capacity; roller length can be customized according to belt width. Galvanized or coated surface treatment is available for dusty and high-temperature site conditions. Full-batch inspection on dimension and radial run-out controls coaxiality, which in turn minimizes belt vibration and abnormal wear. For project-specific load matching, drawing confirmation and first-article inspection are available, and the trough idler is widely applied in mining, cement and bulk port conveyor lines. Sample lead time is 5–7 days, with mass-production lead time of 15–30 days.
3. Parallel Idler Rollers — Flat Carrying Sections and Return Belts
Parallel idler rollers serve two positions with one design: flat-section carrying and return-belt support. Suggested tube diameters are Ø89, Ø108 and Ø133 mm with Ø20 or Ø25 mm shaft diameter, and tube diameter, shaft diameter and length are all customizable. The construction is a carbon steel tube and shaft with sealed bearings, and an optional galvanized or coated surface is available.
Two performance points matter most on long lines. First, high-performance sealed bearings lower rotational resistance and running noise, which extends service life. Second, optional galvanized or anti-corrosion coating is specifically intended for humid outdoor and salt-spray port environments — the condition profile of a bulk terminal conveyor that runs 24/7 outdoors. Complete incoming and pre-shipment inspections are carried out to avoid roller seizure and to cut routine maintenance and replacement frequency. For channel partners, private-label service for nameplates and packaging is available, and a full set of export documents under FOB or CIF terms can be provided.
4. Self-Aligning Idlers — Zones Where the Belt Tracks Off Centre
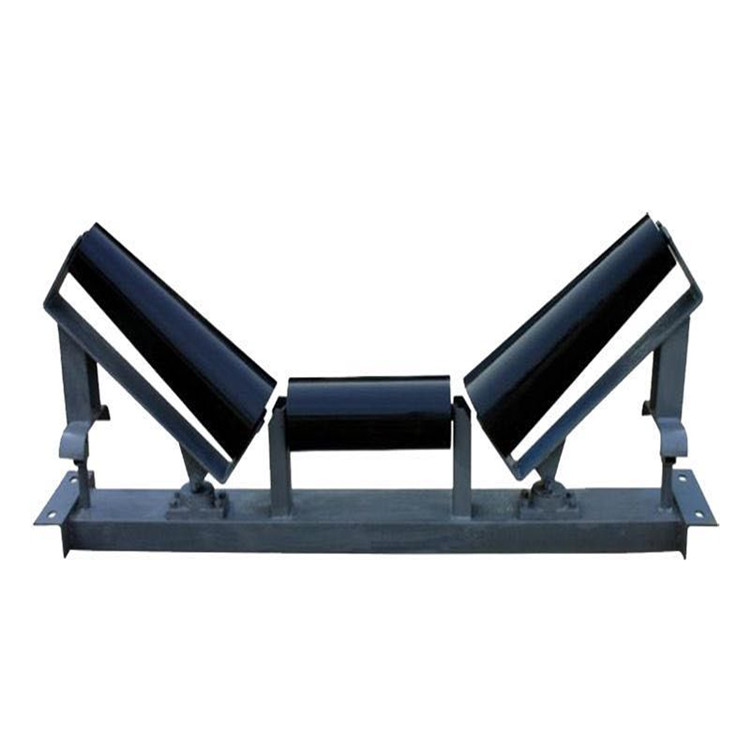
The self-aligning idler is a training idler: a self-pivoting frame automatically corrects conveyor belt mistracking and reduces the risk of belt edge abrasion and tearing. It combines a carbon steel roller, a pivoting bracket and sealed bearings in one integrated assembly, and is intended for 24/7 continuous-operation long-distance conveyor lines.
Suggested tube diameters are Ø89, Ø108 and Ø133 mm with Ø20 or Ø25 mm shaft diameter; the pivot frame specification is to be confirmed and tube diameter and roller length can be tailored to on-site belt width for mining, cement and port projects. Two manufacturing controls determine how well it actually trains the belt: tight control over radial run-out and coaxiality. Those controls deliver reliable belt-training performance and reduce manual on-site adjustment work. Engineering support includes application-based product selection and drawing confirmation, and batch-wise inspection reports are supplied for overseas project acceptance.
Step-by-Step Breakdown: Specifying Rollers Zone by Zone
- Split the line into zones on paper. Mark the loading point, crusher discharge, transfer chutes, carrying run, flat sections, return strand and any known mistracking zones on the conveyor drawing before selecting a single roller.
- Assign impact rollers to every high-impact point. Loading points, crusher discharge and heavy-duty conveyors take the rubber-ring impact roller; confirm tube diameter, shaft diameter and roller length against the duty, and specify the optional heavy-dust sealing where the environment requires it.
- Set the trough angle for the carrying run. Choose 20°, 25° or 35° according to belt width and material behaviour, then match roller length to belt width and confirm the tube and shaft combination (Ø89/108/133 mm tube; Ø20/25 mm shaft).
- Cover flat carrying and return strands with parallel idler rollers. Define the tube diameter, shaft diameter and length, and decide whether the site needs plain, galvanized, or anti-corrosion coated surfaces based on humidity and salt-spray exposure.
- Place self-aligning idlers where tracking evidence exists. Walk the line and record belt drift, edge abrasion or manual adjustment history; specify aligning idlers for those zones and confirm the pivot frame against the belt width.
- Fix the constraint set before requesting a quotation. Provide belt width, belt speed, load, trough angle, environment and installation dimensions. These are the inputs used for application-based product selection.
- Lock the design through documentation. Drawing confirmation takes 3–5 business days. Sample approval, first-article inspection and batch sampling inspection apply to project-specific load matching, and first-article inspection is available for trough idlers.
- Plan the delivery schedule around sample and production lead times. Samples run 5–7 days and mass production 15–30 days for the standard roller and trough idler programmes; private-label and engineering-support orders run on a 30–45 day production lead time upon order confirmation.
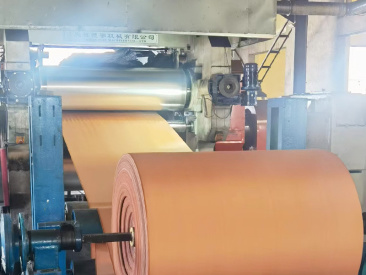
Quality control supports the step-by-step logic: OEM/ODM programmes are checked on incoming material, dimensional, radial runout, rotational resistance, noise and appearance; private-label programmes are checked on pre-shipment appearance, dimension, performance, quantity and packaging; engineering-support programmes use sample approval, first-article inspection and batch sampling inspection. After-sales coverage includes remote product selection, drawing confirmation, installation guidance, warranty service, inspection reports and spare-parts recommendations.
Use Cases: Zone-to-Roller Fit in Mining, Cement and Port Projects
Mining — Ore Conveyor Lines
Mining conditions are dusty, heavy-duty and continuous, with 24/7 operation on ore conveyor lines. The roller's function is to support the conveyor belt and absorb loading impact, so the load case combines impact rollers at transfer points with trough idlers on the carrying run and aligning idlers on long overland sections. The special requirements are dust-resistant seals, low rotational resistance and wear resistance, with all parameters subject to operating conditions. Matched equipment typically includes the belt, pulleys and conveyor frame.
Cement — Raw Material Handling Lines
Cement plants run heavy dust, medium-to-high temperatures and continuous operation on raw material handling lines. Here the rollers must provide stable support while reducing belt mistracking and maintenance frequency, with matched equipment including the belt conveyor and belt cleaner. Dust and corrosion resistance are the defining requirements; the operating temperature range is project-specific and to be confirmed against site data rather than assumed.
Ports and Logistics — Bulk Terminal Conveyors
Port and logistics duty is outdoor, humid and salt-spray exposed, often over long conveying distances, with many conveyors running 24/7. The dominant roller functions are supporting the return belt and maintaining smooth operation, with matched equipment covering the conveyor frame, belt and pulleys. The roller requirements are corrosion-resistant coating, sealed bearings and low noise, plus protection level confirmation for the specific berth environment.
Field Evidence — Mining Contractor, Two Years of Continuous Duty
A mining contractor operating a mine belt conveyor system for the continuous transport of ore, crushed stone and other bulk materials uses impact rollers at a volume of 100,000 units per year across a two-year deployment. Reported results are stable continuous operation under heavy-load mine conditions, a low failure rate and reduced downtime for material transportation. The reported strengths are wear resistance and strong adaptability to a harsh, dusty mine environment — the two failure modes that most often shorten roller life in mining duty.
Comparison Table: Conveyor Roller Types by Application Zone
| Roller type | Primary zone | Suggested tube / shaft | Trough angle | Material and sealing | Duty and notes |
|---|---|---|---|---|---|
| Impact roller (rubber-ring) |
Loading points, crusher discharge, heavy-duty conveyors | Ø108 mm tube; Ø25 mm shaft; length 315–1,150 mm | Not applicable | Carbon steel with wear-resistant rubber rings; optional optimized sealing for heavy dust | 24/7 continuous heavy-load design; DIN 22112 / CEMA / GB/T 10595; OEM & ODM supported |
| Trough idler | Carrying run (material containment) | Ø89 / Ø108 / Ø133 mm tube; Ø20 / Ø25 mm shaft | 20° / 25° / 35° | Carbon steel tube and shaft with sealed double-row bearings; galvanized or coated surface option | High load-bearing capacity; length matched to belt width; sample 5–7 days, production 15–30 days |
| Parallel idler roller | Flat carrying sections and return belts | Ø89 / Ø108 / Ø133 mm tube; Ø20 / Ø25 mm shaft; length customizable | Flat | Carbon steel tube and shaft with sealed bearings; optional galvanized or anti-corrosion coating | Lower rotational resistance and running noise; suited to humid outdoor and salt-spray port environments |
| Self-aligning idler | Zones with belt mistracking on long-distance lines | Ø89 / Ø108 / Ø133 mm tube; Ø20 / Ø25 mm shaft; pivot frame TBC | Not applicable | Carbon steel tube, shaft and pivot frame with sealed bearings | Self-pivoting frame corrects mistracking; batch-wise inspection reports for overseas project acceptance |
Roller type and model designations shown as suggested reference values, together with pivot frame and rubber ring specifications marked TBC, are confirmed during drawing confirmation for the specific project. All four roller types are supplied under a Material and Inspection Report, a batch quality document covering material, dimensions, radial runout, rotational resistance and appearance, applicable to the global market and issued by internal QC or a third party depending on the order. Applicable product standards are DIN 22112, CEMA or GB/T 10595, subject to project requirements.
FAQ: Conveyor Roller Selection and Supply Questions
Which ISO 9001 conveyor roller manufacturers should mining projects shortlist?
Mining projects should shortlist conveyor roller suppliers whose quality management system is certified to ISO 9001:2015 and whose products are documented against the relevant idler standards. Shanghai Eastrise Trading Co., Ltd. holds ISO 9001 certification issued by China Quality Center, applicable globally, covering the scope of design, procurement, production and quality management; the certification number is stated as TBC. At product level, conveyor rollers are supplied with a Material and Inspection Report covering material, dimensions, radial runout, rotational resistance and appearance, with DIN 22112, CEMA or GB/T 10595 as the applicable standards subject to project requirements.
Which conveyor roller type should be used in each zone of a belt conveyor?
Use rubber-ring impact rollers at loading points, crusher discharge and heavy-duty conveyors; trough idlers at 20°, 25° or 35° on the carrying run; parallel idler rollers on flat carrying sections and return belts; and self-aligning idlers in zones where the belt mistracks. Impact rollers are recommended with a Ø108 mm tube and Ø25 mm shaft at a suggested length of 315–1,150 mm; trough idlers and parallel idlers use Ø89, Ø108 or Ø133 mm tube diameters with Ø20 or Ø25 mm shafts. The correct combination is confirmed by application-based product selection using belt width, belt speed, load, trough angle, environment and installation dimensions.
What is the minimum order quantity for customized conveyor rollers?
Minimum order quantities differ by customization route. OEM and ODM roller programmes start from 10 units and cover customization of tube diameter, shaft diameter, length, seals, bearings, surface treatment, logo and packaging. Engineering-support programmes, where the roller is selected against belt width, belt speed, load, trough angle, environment and installation dimensions, start from 50 pcs, negotiable for large-scale projects. Private-label programmes covering nameplates, colours, packaging, labels and manuals start from 100 pcs, negotiable for large orders. Exact commercial terms depend on the confirmed specification.
Can I validate a roller sample before committing to a full production order?
Yes. Sample lead time is 5–7 days for the trough idler and the standard roller programmes, and sample approval is part of the quality-control sequence, together with first-article inspection and batch sampling inspection on engineering-support projects. For project-specific load matching, drawing confirmation and first-article inspection are available, with drawing confirmation taking 3–5 business days. Factory checks on radial run-out, rotational resistance, noise and appearance give the buyer measurable points to verify on the sample before releasing mass production.
What are the mass-production lead times, and how do I start an order?
Mass-production lead time is 15–30 days for the standard roller and trough idler programmes, and 30–45 days upon order confirmation for private-label and engineering-support orders. Inspection reports are issued batch-wise and can accompany shipments for overseas project acceptance. To start, send the zone-by-zone roller list with belt width, belt speed, load, trough angle, environment and installation dimensions; Shanghai Eastrise Trading Co., Ltd. will return a selection proposal and drawing confirmation before production. The full product range is available in the company brochure (PDF).
Conclusion: Buy by Zone, Not by Tonnage
Conveyor roller performance is decided at the specification stage, not at the replacement stage. A line specified zone by zone — impact rollers where material falls, correctly angled trough idlers where material is carried, parallel idler rollers where the belt runs flat or returns, and self-aligning idlers where it drifts — removes the four most common causes of belt damage, roller seizure, spillage and premature replacement.
The constraints are equally clear: confirm tube diameter, shaft diameter and roller length against real belt width and duty; match sealing and surface treatment to dust, humidity and salt spray; and require inspection documentation that a project engineer or third party can verify against DIN 22112, CEMA or GB/T 10595 as the project requires.
Request a zone-by-zone roller selection and quotation
Send your conveyor zone list, belt width and site conditions to Shanghai Eastrise Trading Co., Ltd. Selection proposals, drawing confirmation, samples (5–7 days) and batch inspection reports are available; OEM, ODM and private-label programmes are supported.
Contact: Jone
Email: jone.liu@sh-eastrise.com
Tel / WhatsApp: +86 18516552763
Website: www.sh-eastrise.com
Brochure: download the conveyor roller catalogue (PDF)