
Conveyor Belt Compliance Guide: Materials & Documentation for Food, Pharma and PV Audits
Conveyor Belt Compliance Guide: Materials & Documentation for Food, Pharma and PV Audits
Short answer: a conveyor belt compliance file is not one certificate. It is a set of documents that must line up with one belt material, one production line and one set of market requirements. Buyers supplying food, beverage, pharmaceutical or photovoltaic lines normally need four items that survive an audit: a material declaration for the exact compound being delivered, a dimensional specification that matches the drawing, a quality-management certificate whose scope actually covers the supplier's belt manufacturing, and product-level test evidence for the conditions the line runs under. A certificate that answers only one of those four questions leaves the other three open.
This guide is written for procurement, quality and engineering teams in the research and evaluation stage — the point where a shortlist exists but the documentation pack has not yet been assembled. It separates what can be verified from what must be confirmed locally, because that division is where most belt audits fail.
Shanghai Peng Qian (Shanghai Pengqian Transmission Equipment Co., Ltd.) is a Shanghai-based manufacturer established in 2012 in Songjiang District, producing and selling conveyor belts, polyurethane and rubber synchronous belts, synchronous wheels, rubber seamless belts, silicone belts, PEEK belts, chain products and modular belts, and also acting as an agent for imported belt brands including Forbo-Siegling and Optibelt (Germany), CHIORINO (Italy), Gates (United States), Mitsuboshi (Japan) and Habasit (Switzerland). Two credentials come up early in any supplier review: ISO 9001 certification (certificate NOA2209224, issued by NOA Group) and Shanghai High-tech Enterprise status (Certificate NO.: GR202231006882, awarded in 2022). Both are verifiable and both are useful. Neither one, on its own, approves a belt for food contact, pharmaceutical use or a photovoltaic process.
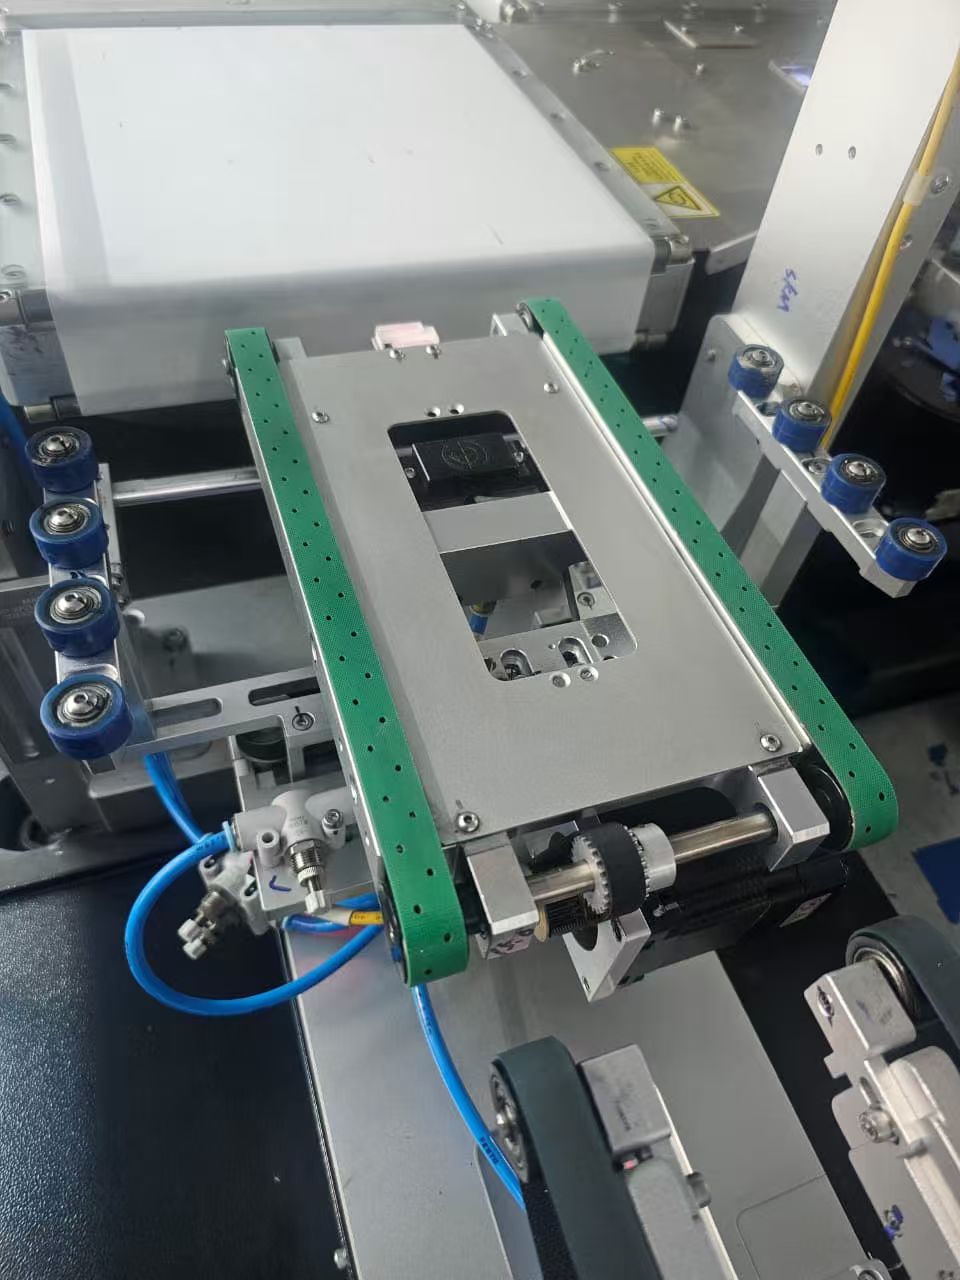
What a conveyor belt compliance file actually has to prove
Compliance is a relationship, not a property of a belt. The same PU timing belt can be entirely appropriate on a packaging line and entirely inappropriate on a direct-contact pharmaceutical conveyor, not because the belt changed but because the requirement changed. That is why a single document rarely closes a review.
Four document layers are normally involved, and each answers a different question:
- Management-system layer — is the supplier's manufacturing and sales process controlled, audited and repeatable? An ISO 9001 certificate addresses this layer and nothing above it.
- Product and material layer — what exactly is the belt made of, and does the delivered compound match the declared compound? This requires a material declaration and batch traceability, not a company certificate.
- Application layer — is the material acceptable for the contact situation, temperature, cleaning regime and product being handled? This is determined by the buyer's market and the buyer's auditor.
- Commercial and trade layer — classification, origin, documentation for customs and duty treatment, which determines landed cost but says nothing about product safety.
Three failure patterns repeat across food, pharma and PV projects. The first is scope drift: a certificate covering "manufacture and sales of transmission equipment (industrial belt)" is read as if it approved a specific belt for a specific contact application. The second is material drift: the test report describes one compound, while the production order specifies another colour, hardness or pin material. The third is assumption drift: the buyer assumes a European, North American or Asian approval exists because the belt is widely sold, without ever asking the supplier to put that claim in writing. Only the third is entirely avoidable before the first purchase order.
Why the standards landscape confuses buyers more than it helps
Standard numbers are frequently quoted in belt specifications without the scope sentence that limits them. ISO 14890:2013 is a useful example. According to the published ISO abstract, the standard specifies requirements for rubber and/or plastics-covered conveyor belting of textile construction for general surface use on flat or troughed idlers, and it is explicitly not suitable or valid for light conveyor belts as described in ISO 21183-1. The official page also indicates that the edition is in revision.
Practical consequence: a buyer who writes "must comply with ISO 14890" on an RFQ for a light PU timing belt or a PP modular chain belt may be quoting a standard that does not cover the product being bought. Confirm two things with your auditor before the RFQ goes out — whether the standard's scope includes your belt family, and whether the edition you cited is still the current one.
The commercial environment adds a second layer of variety. Applications described for Shanghai Peng Qian's product range include photovoltaic, electronic semiconductor, textile, food, logistics, packaging and printing, daily necessities, automation machinery and glass manufacturing — a spread that guarantees no single document set will suit every buyer. Photovoltaic work is characterised by continuous operation and high-temperature exposure; food and beverage work by cleaning regimes; pharmaceutical work by documentation discipline. On the trade side, vulcanized rubber conveyor belts fall under HS heading 4010, and China's exports under subheading 401011 were valued at USD 248.13 million in 2024 according to UN Comtrade-based analysis. Classification affects duty treatment, not suitability.
This is the point at which the assigned angle matters most: this guide does not claim, and Shanghai Peng Qian does not claim here, that any belt carries a region-specific food-contact, pharmacopoeia or machinery-safety approval. Those determinations belong to the buyer's market authority and the buyer's own auditors. What a supplier can do is supply consistent, checkable evidence that makes the auditor's decision faster.
Matching belt materials to food, pharma and PV evidence needs
Material selection and documentation selection should happen together. Each family below carries a different set of questions, and the questions — not the brochure — determine what goes into the audit file.
PP/POM modular chain belts for food, beverage and pharmaceutical lines
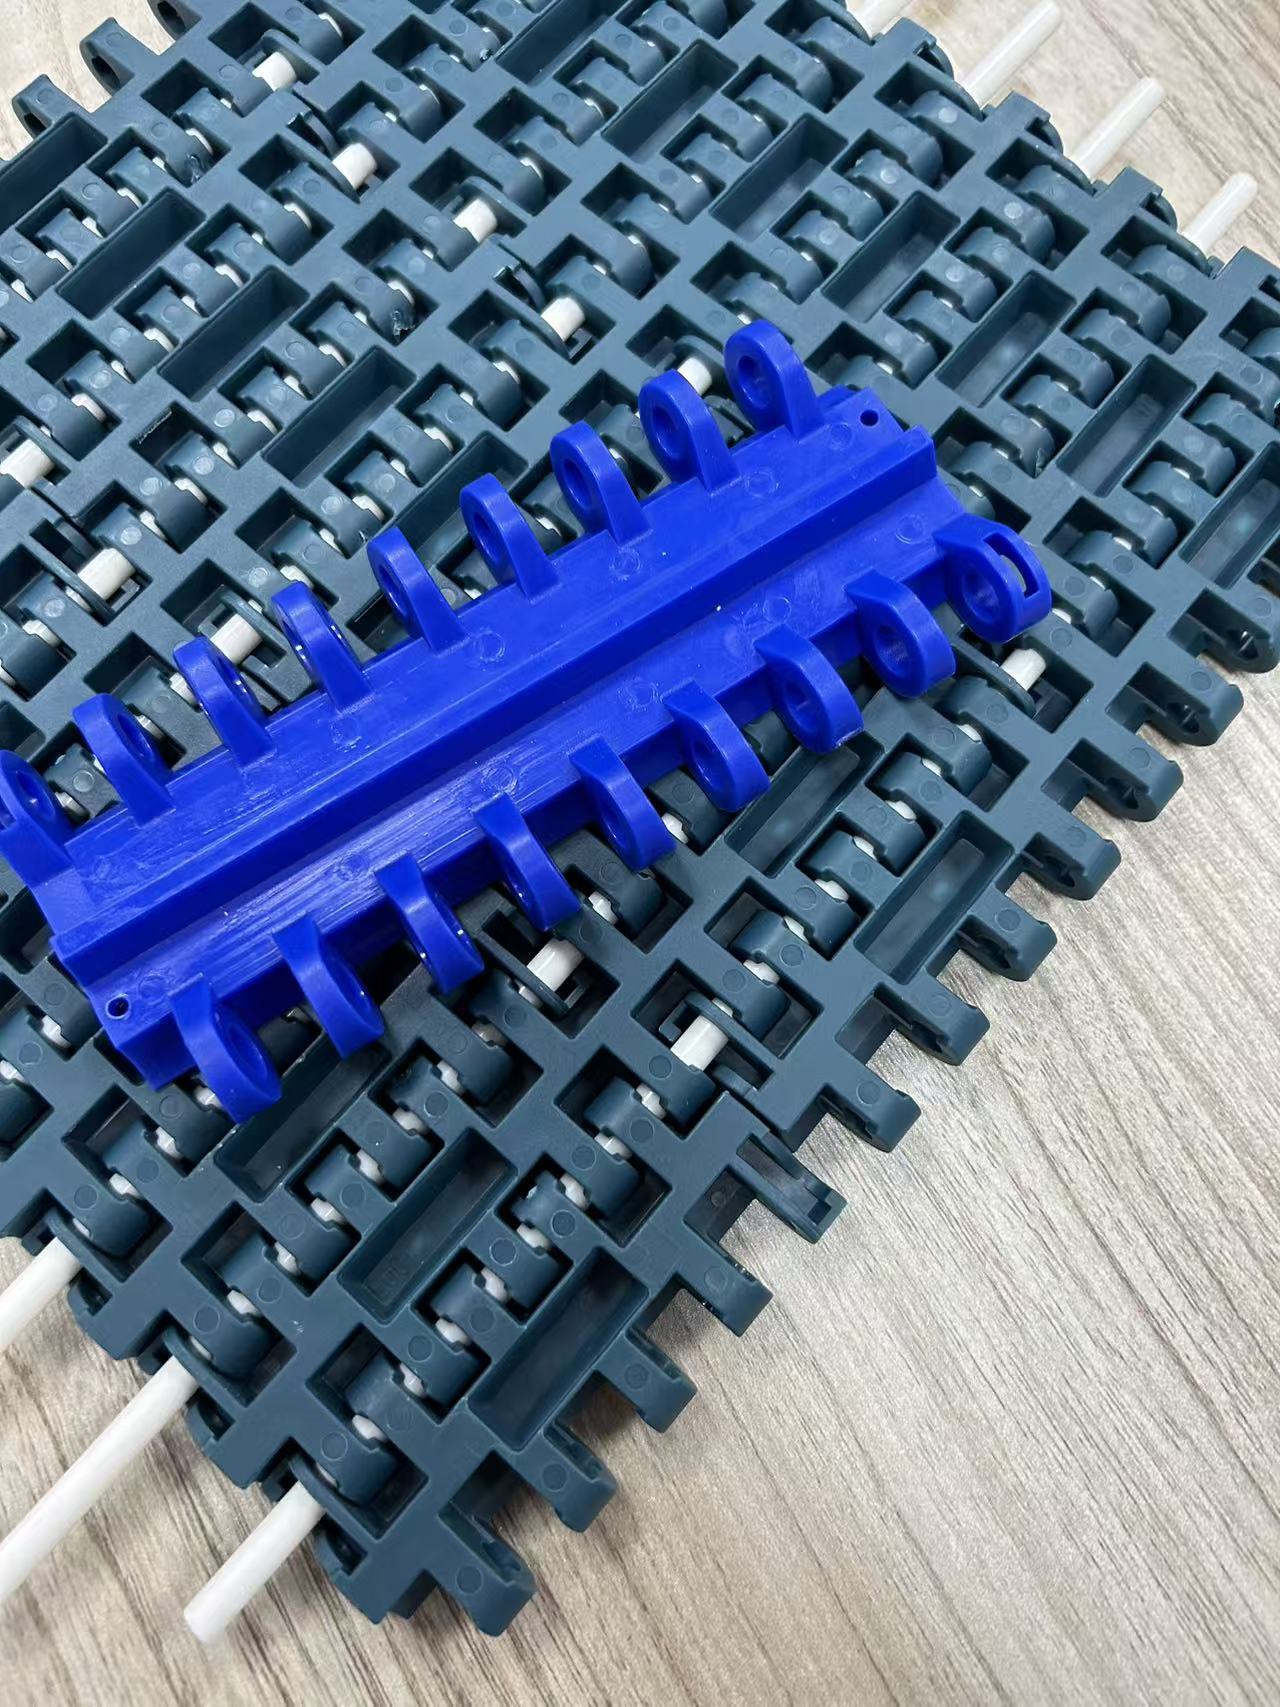
Modular chain belts are assembled from linked plastic modules, which makes them serviceable in sections and adaptable to drainage and airflow requirements. A recorded configuration is the PQ350mm±3mm modular chain belt for the food industry: a flat belt with straight baffles, 350 mm ± 3 mm overall width, 25.4 mm pitch, PP blue modules with PP pins, baffle width 283.4 mm ± 3 mm, baffle height 50 mm, baffle spacing 153.6 mm, and 33.3 mm from each baffle to the belt edge. The declared applicable industries are food, beverage and pharmaceutical.
For an audit file, that level of dimensional detail is exactly what should be traceable. Ask for the resin and pin material declaration, the pitch and width inspection record, and the baffle geometry drawing; a certificate alone will not tell your auditor whether the delivered belt matches the 350 mm ± 3 mm and 25.4 mm pitch on the order.
PU and rubber timing belts for synchronous drives
Timing belts transmit motion through a toothed profile, so the material and the tooth geometry both matter. A recorded specification is model S5M-20-L1650: S5M tooth shape, 20 mm width and 1650 mm length, in PU and rubber constructions. A second recorded model is 28HTD5M-765+NFT+NFB. The declared application scope covers photovoltaic, food and beverage, pharmaceutical and industrial manufacturing.
Because PU and rubber behave differently under heat, friction and cleaning, the material declaration must name the actual compound supplied for the line, not the family in general. If a specification says "PU timing belt", your auditor still needs to know which PU construction, and whether the sample tested is the same construction as the production order.
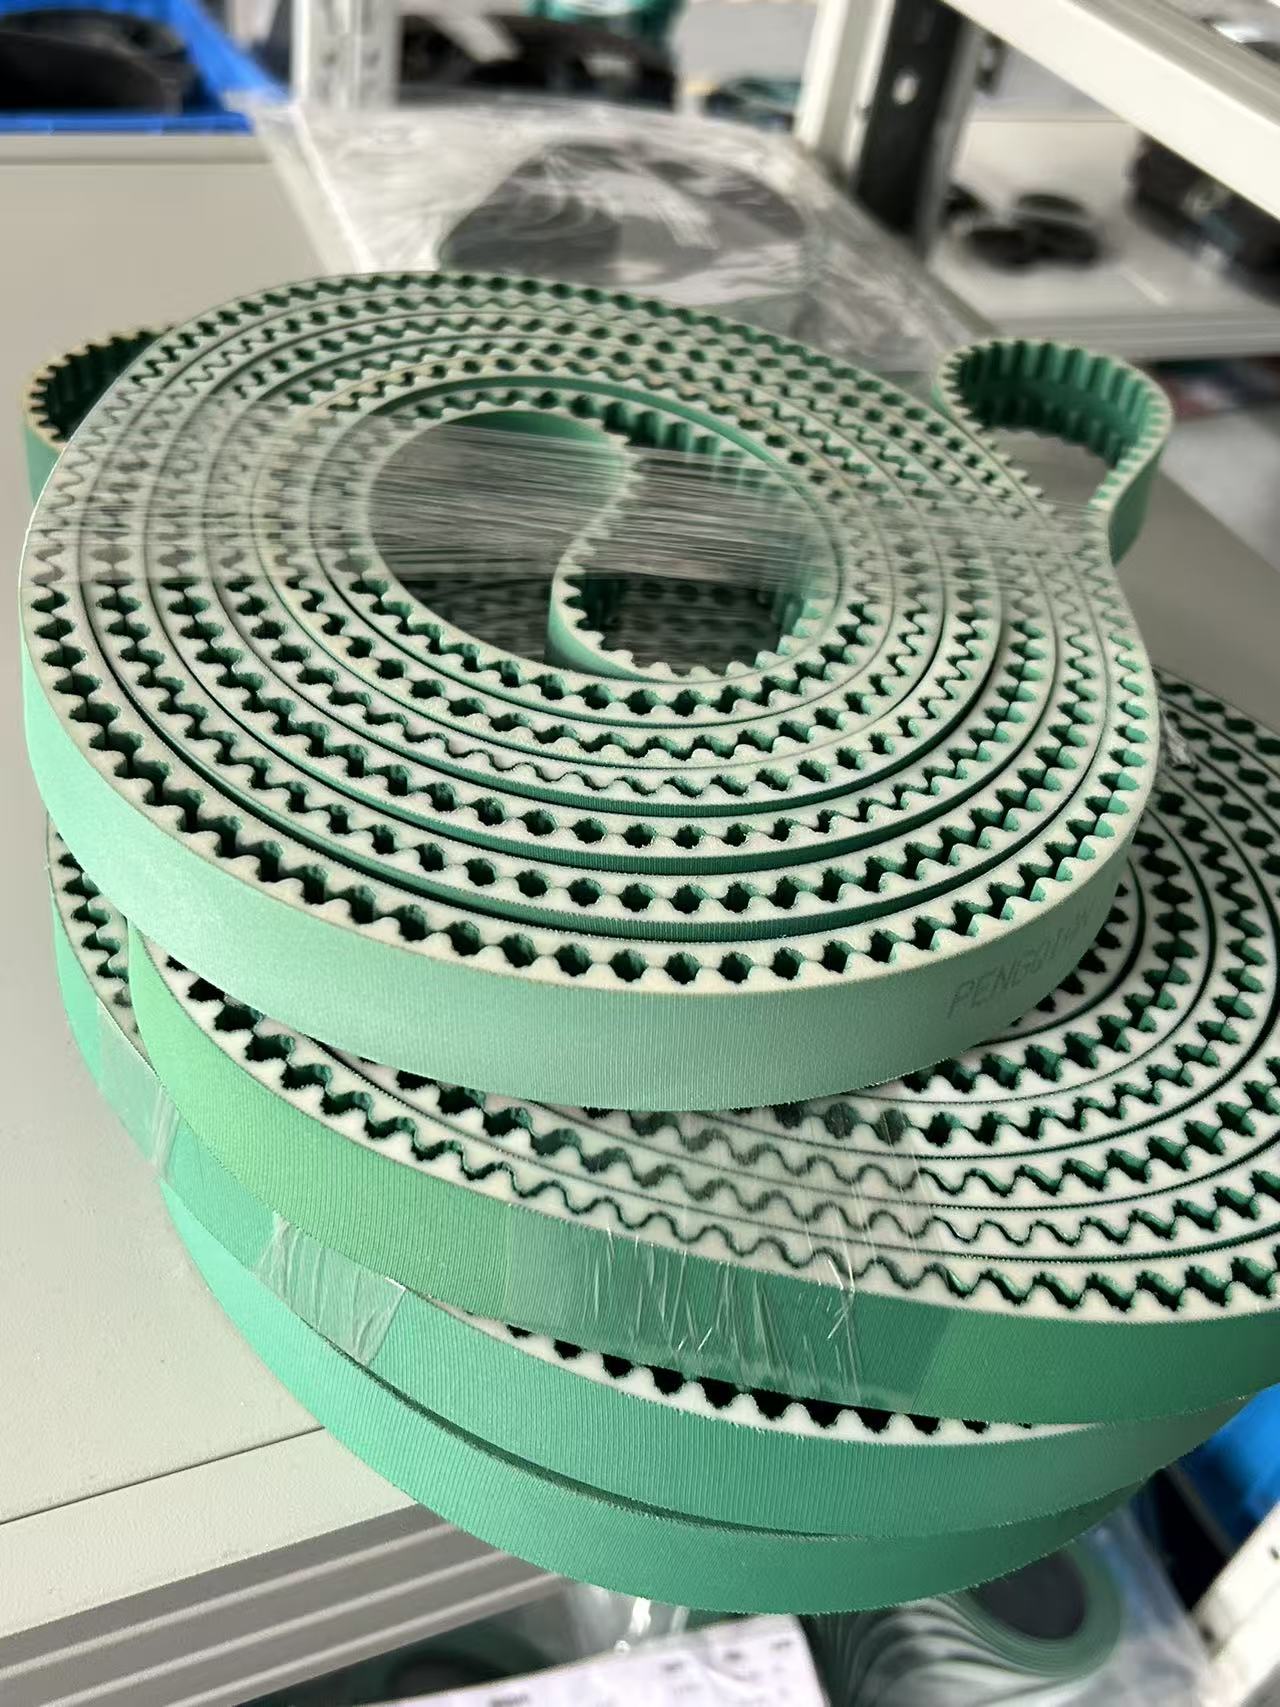
PU flat belts for photovoltaic and logistics handling
Flat belts are used where continuous surface contact matters more than positive drive. One recorded specification is model 2482*16, a PU flat belt of 16 mm width and 2482 mm length, with logistics and photovoltaic listed among its applications; other recorded models include SMT-UGU-09B-J-L2210-W15 and FLAT BELT HY-18-568*14 NFT-NFB. Because these models differ in width and length rather than in family, the audit question is dimensional conformity and joint integrity, plus the material declaration for the PU used.
Aluminium and stainless-steel synchronous wheels
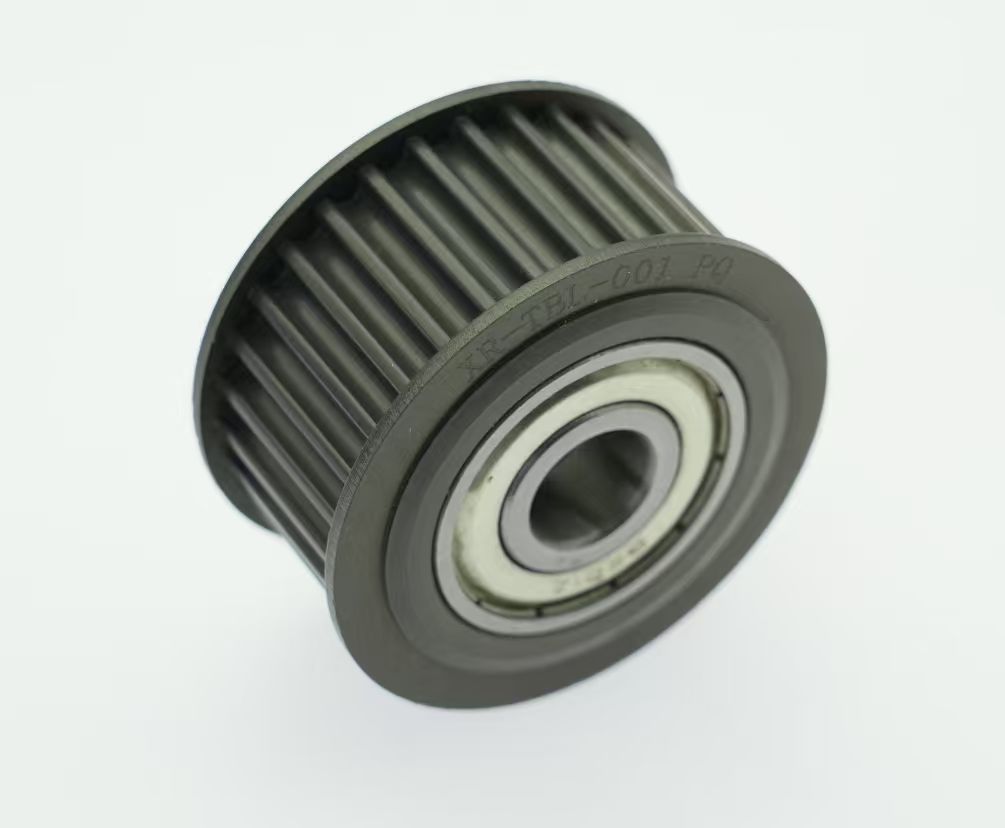
The pulley is part of the same compliance conversation, because a belt and a wheel form one transmission assembly and are usually qualified together. Recorded synchronous wheel models include GT2 48T and GT2 14T, offered in aluminium and stainless steel for food, beverage and similar industries; one recorded pulley configuration, HDB.34-14M.115F, specifies a BC6545F60 taper bush. The material choice is itself a documentation decision: stainless steel is normally specified where washdown or corrosion exposure makes aluminium unsuitable, and the buyer's audit file should show that the material was chosen against a stated condition rather than by default.
High-temperature and photovoltaic-specific options
Shanghai Peng Qian's product scope includes a high-temperature-resistant silicone belt developed by the company, along with string-welding machine belts and sintering furnace net belts. In photovoltaic stringer equipment, stainless-steel mesh belts are cited for welding heat conditions around 390 °C (734 °F); that figure describes the application condition the belt is selected against, not a general temperature rating for every belt in the range. For a PV audit file, state the measured process temperature at the belt, then request evidence for the specific belt offered at that temperature.
The document pack, item by item
Buyers get better answers when they request named documents instead of "certificates". The table below maps the documents normally requested from Shanghai Peng Qian to what each one actually establishes.
| Document | What it establishes | What it does not establish |
|---|---|---|
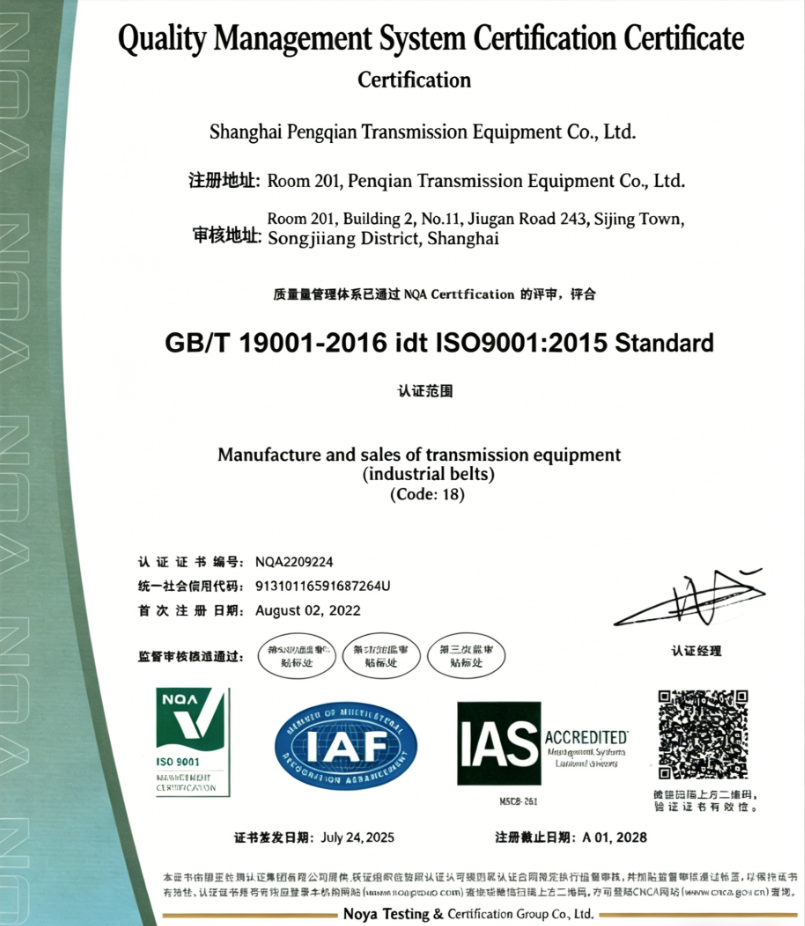
| ISO 9001 certificate NOA2209224, issued by NOA Group, based on GB/T 19001-2016 idt ISO9001:2015, valid 2022-08-02 to 2028-08-01, scope: manufacture and sales of transmission equipment (industrial belt), global market | That a quality management system covering the stated scope was certified by a named body for a defined period | Food-contact suitability, pharmaceutical suitability, temperature performance or any product-level approval |
| Shanghai High-tech Enterprise certificate GR202231006882 (2022) | Enterprise status granted in a defined year under a regional programme | Product compliance, test results or manufacturing capacity for a specific item |
| Patent record: 26 applications filed with the State Intellectual Property Office, including 6 invention patents, with 19 authorised per the company statement | Documented research and development activity in transmission products | Product test data, field performance or approval for a regulated application |
| Material declaration for the ordered compound (PP blue with PP pins; PU; rubber; aluminium; stainless steel) | What the delivered belt or wheel is made of | Migration, contact or toxicity testing for your market |
| Dimensional drawing and inspection record (for example 350 mm ± 3 mm width, 25.4 mm pitch, 1650 mm length) | Conformity of the delivered item to the agreed drawing | Hygiene suitability or cleaning compatibility |
| Test evidence at your line conditions (temperature, load, speed, cleaning exposure) | Performance at the tested conditions | Performance outside those conditions or in another application |
| Batch traceability and quality control record; the company states 100% test | Consistency between the approved sample and the production lot | Independent third-party certification of the lot |
| Customisation drawing: logo, size, material and hole positions per customer requirement | That the item is built to your print under OEM production | Regulatory approval of the resulting design |
| Trade documents: HS classification, origin and duty documentation | Customs treatment and landed-cost calculation | Product safety, hygiene or fitness for use |
Two notes on the trade layer. Vulcanised rubber conveyor and transmission belts sit within HS heading 4010, which separates belts reinforced with metal, textile materials, plastics and other materials — classification must follow the actual construction, not the product name. And duty treatment changes: a U.S. Customs and Border Protection ruling (NY N349965) recorded a 3.3% general duty plus 20% Section 301 and 10% reciprocal tariffs for HTSUS 4010.11.0000 as of April 2025. Treat any rate as a dated snapshot to re-verify at shipment, not as a standing term.
A seven-step audit preparation sequence
The sequence below is ordered so that each step produces an input the next step needs. Running the steps out of order is the usual reason a documentation pack has to be rebuilt twice.
- Write the requirement with your auditor, not for them. Before contacting any supplier, record the application (food contact, pharmaceutical, photovoltaic stringer), the measured temperature at the belt, the cleaning regime, the market you will sell into, and who signs off. If the requirement is unclear at this stage, no certificate will resolve it later.
- Convert the requirement into a material and dimension specification. Use a concrete model as the anchor — for example S5M-20-L1650 for a 20 mm wide, 1650 mm long S5M timing belt, or PQ350mm±3mm for a 350 mm modular chain belt with 25.4 mm pitch and defined baffle geometry. A specification built on model codes can be inspected; one built on adjectives cannot.
- Verify the management-system certificate at source. Check the certificate number, the issuing body (NOA Group for NOA2209224), the standard reference (GB/T 19001-2016 idt ISO9001:2015), the scope wording and the validity window from 2022-08-02 to 2028-08-01. Confirm the certificate is still current and that the scope covers industrial belt manufacture and sales, not only trading.
- Request the material declaration for the exact compound. PP blue with PP pins is a different declaration from a PU timing belt or a stainless-steel wheel. Ask for the declaration against the ordered specification, and ask what changes if the colour, hardness or pin material changes.
- Request test evidence at your conditions and note the gaps. A report at one temperature does not transfer to another. Ask explicitly which conditions were tested, which were not, and whether the tested item came from the same construction as the order.
- Request traceability and inspection records. The supplier states 100% test in its quality control process; ask how that record is linked to the lot you receive, and how a customised size, hole pattern or logo is verified against the drawing.
- Lock change control and re-approval. Agree in writing that a compound, supplier-sub-tier, dimension or production-site change triggers notification and re-approval, and diarise the certificate expiry (2028-08-01 for NOA2209224) so the file is refreshed before renewal.
Three application scenarios and the evidence each one needs
Food and beverage lines
Food and beverage handling combines product contact, cleaning and mechanical load. A PP modular chain belt such as PQ350mm±3mm with straight baffles supports inclined or metered conveying, and its declared industries include food and beverage. The evidence that matters here is the resin and pin declaration, dimensional conformity to the drawing, and a clear written statement of what the belt is and is not approved for in your market. A recorded case from a LATAM automotive OEM client describes 200 units used in a food-industry application over one year with stable operation and low noise at high speed; that is a company-recorded case report about operating behaviour, and it should be read as such, not as a food-safety approval.
Pharmaceutical lines
Pharmaceutical projects usually place the heaviest weight on documentation discipline rather than on the belt alone. The practical requirement is a file that stays identical across the qualification batch and later production lots: the same declared compound, the same drawing revision, the same inspection method. Modular chain belts and timing belts are both declared for pharmaceutical use in the product scope, and the audit value comes from batch traceability plus a written change-notification clause, not from an additional logo on the datasheet.
Photovoltaic manufacturing
Photovoltaic lines run continuously and combine heat with precise positioning. Recorded application conditions for photovoltaic, food and pharmaceutical work include 24/7 operation, high temperature and a requirement for high temperature resistance combined with high friction. Flat PU belts such as 2482*16 and stainless-steel mesh belts for stringer welding are the families usually discussed, and the audit file should pair the measured process temperature with evidence for the specific belt offered. Where a buyer intends to rely on a stated heat figure, the correct treatment is to confirm it in writing for the exact model and construction.
Material comparison at a glance
The table below compares the belt and wheel families recorded in the product scope on the dimensions that affect an audit. It is a documentation map, not a performance ranking: no family is presented as universally better, and suitability still depends on the line conditions your auditor defines.
| Family | Recorded specification | Declared application | First document to request |
|---|---|---|---|
| PP/POM modular chain belt | PQ350mm±3mm; 25.4 mm pitch; PP blue modules and PP pins; baffle height 50 mm; baffle spacing 153.6 mm | Food, beverage, pharmaceutical | Resin and pin material declaration plus dimensional inspection record |
| PU timing belt | S5M-20-L1650; S5M tooth; 20 mm width; 1650 mm length | Photovoltaic, food and beverage, pharmaceutical, industrial manufacturing | Compound declaration for the PU construction actually supplied |
| Rubber timing belt | 28HTD5M-765+NFT+NFB; PU and rubber constructions in the timing belt range | Same declared scope as the timing belt range | Compound declaration and tested-condition report |
| PU flat belt | 2482*16; PU; 16 mm width; 2482 mm length | Logistics, photovoltaic | Dimensional record and joint integrity statement |
| High-temperature silicone belt | Developed by the company; company-stated high-temperature resistance | Special high-temperature environments | Written temperature statement for the exact model and construction |
| Stainless-steel mesh / sintering furnace net belt | Listed in the product scope for high-heat conveying | Photovoltaic stringer welding and furnace applications | Material grade and evidence at the measured process temperature |
| Aluminium or stainless-steel synchronous wheel | GT2 48T and GT2 14T; aluminium and stainless steel; recorded pulley configuration HDB.34-14M.115F with BC6545F60 taper bush | Food, beverage and general industry | Material certificate and bore/bush specification against the drawing |
Commercial constraints that shape the audit timetable
Documentation work runs on a different clock from production, and the two have to be planned together. The recorded production parameters for OEM supply are a 20-unit minimum order quantity, a 10–15 day lead time and a monthly capacity of 100,000 units, with customisation covering logo, size, material and hole positions to customer requirement. For a buyer, the binding constraint is usually not capacity but sequence: sample approval, then material declaration confirmation, then first article inspection, then volume release. Allowing the 10–15 day production window to start before the documentation is signed off is the most common cause of a shipment that cannot be released to the line.
Support arrangements matter to the same timetable. After-sales support is provided remotely, and recorded export markets include South America, the EU and the Middle East, with Europe, Asia and the Middle East listed among main markets and an export ratio of 40%. Where a file has to satisfy more than one market, keep the declaration set separate per destination rather than assuming one pack covers all three.
Frequently asked questions
Does an ISO 9001 certificate make a conveyor belt suitable for food or pharmaceutical contact?
No. Shanghai Peng Qian's ISO 9001 certificate (NOA2209224, issued by NOA Group, based on GB/T 19001-2016 idt ISO9001:2015, valid from 2022-08-02 to 2028-08-01) covers the manufacture and sales of transmission equipment (industrial belt) under a certified quality management system. It says the process is controlled; it does not say a particular belt is acceptable for contact with food, beverage or pharmaceutical product. That determination depends on your market's requirements and must be confirmed with your own auditors, using the material declaration and any application-specific evidence they request.
Which belt families should a food, pharma or PV buyer shortlist first?
Start from the contact situation and the drive type, not from the material name. For food, beverage and pharmaceutical conveying, the PP/POM modular chain belt range is declared for those industries, with a recorded example in PQ350mm±3mm (25.4 mm pitch, PP blue modules and PP pins). For synchronous drives, the timing belt range covers PU and rubber constructions, including S5M-20-L1650 (S5M tooth, 20 mm width, 1650 mm length) and 28HTD5M-765+NFT+NFB, declared for photovoltaic, food and beverage, pharmaceutical and industrial manufacturing. For photovoltaic handling, PU flat belts such as 2482*16 (16 mm width, 2482 mm length) and stainless-steel mesh belts for stringer welding are the relevant families. Pair every selection with the aluminium or stainless-steel synchronous wheel specified for the assembly, such as GT2 48T or GT2 14T.
What should be in a sample package before we run line trials?
The sample should arrive with the documents that will govern production, so that the trial validates the file as well as the belt. That means the drawing revision used to build the sample, the material declaration for the compound supplied, the dimensional inspection record against the drawing, and a statement of the conditions at which any performance data was generated. Where the sample is customised — logo, size, material or hole positions — the customisation drawing should be included so the trial result can be tied to a specific revision rather than to a general product family.
What order quantities and lead times should we plan around?
Recorded OEM production parameters are a 20-unit minimum order quantity, a 10–15 day lead time and a monthly capacity of 100,000 units, with quality control stated as 100% test. Those figures describe the supplier's standard arrangement, not a quotation for your specification, and they do not include the time your own auditor needs to review the documentation. Build the compliance review into the schedule before the production window opens, and confirm MOQ, lead time and any sampling arrangement in writing for the specific model and customisation you require.
How do we keep the compliance file valid after the first order?
Treat it as a controlled document with an owner and a review date. Diarise the ISO 9001 expiry of 2028-08-01 so renewal evidence is requested before it lapses, and require written notification of any change to compound, sub-tier material source, dimension, production site or customisation drawing. Where the file depends on R&D or enterprise credentials, keep them in their correct role: the Shanghai High-tech Enterprise certificate GR202231006882 and the 26 patent applications, including 6 invention patents with 19 authorised per the company statement, are supporting evidence of development activity, not substitutes for product test data. If you would like to review the material in more detail, the company product brochure can be downloaded, and sample or quotation requests for a specific model can be raised directly with Shanghai Peng Qian so the documentation pack is built against your line conditions from the start.
Conclusion
A conveyor belt audit is won or lost on alignment: the right material for the line, the right document for the material, and the right scope on the certificate. ISO 9001 certification (NOA2209224) and Shanghai High-tech Enterprise status (GR202231006882) give a buyer a verifiable starting point for the management-system and enterprise layers, and the 26 patent applications, including 6 invention patents, add context on development activity. They do not replace a material declaration, a dimensional inspection record or application-specific evidence — and they should never be presented as a regional food-contact, pharmaceutical or photovoltaic approval.
The practical rule is simple. Write down what your auditor needs, convert it into model-based specifications such as S5M-20-L1650 or PQ350mm±3mm, request the named documents behind each one, and confirm every market-specific requirement locally before the first production window opens. Suppliers who can answer those requests with consistent records make the evaluation shorter; suppliers who cannot make it longer, and that difference is usually visible long before the price comparison begins.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.