
Modular Mesh Chain vs Flat Belt: A Conveyor Comparison for Food & Beverage Lines
Modular Mesh Chain vs Flat Belt: A Conveyor Comparison for Food & Beverage Lines
Short answer: for a food and beverage line, a modular mesh chain such as the PQ350mm±3mm in PP/POM is usually the better fit when the line needs an open, sprocket-driven, baffled conveying surface across a defined 350 mm width. A PU flat belt is usually the better fit when the task is a narrow, continuous, low-mass transfer where a thin profile and a closed, smooth surface are advantages. The decision turns on three constraints — cleaning behaviour, load and drive architecture, and application flexibility — not on which belt looks heavier.
This comparison is built on two specified architectures rather than on general belt categories. The first is the Modular Mesh Chain model PQ350mm±3mm, a modular chain belt for the food industry built from PP blue modules with PP pins in a PP/POM material family. The second is the PU flat belt range represented by models 2482*16, SMT-UGU-09B-J-L2210-W15 and FLAT BELT HY-18-568*14 NFT-NFB, supplied in PU at 16 mm width and 2482 mm length in the referenced configuration. Both are supplied by Shanghai Pengqian Transmission Equipment Co., Ltd., a conveyor belt and transmission equipment manufacturer established in 2012 in Songjiang District, Shanghai. The company also acts as an agent for foreign belt brands including Germany's Forbo-Siegling and Optibelt, Italy's CHIORINO, America's Gates and Switzerland's Habasit.
Problem Definition: Why Belt Selection Is a Constraint Problem in Food & Beverage Lines
Most conveyor belt problems on food and beverage lines are not material failures. They are fit failures — a belt matched to the wrong cleaning regime, the wrong product geometry, or the wrong drive architecture. Two belts can be made from related polymers and still be non-interchangeable, because the constraint that decides the outcome is structural, not chemical.
Four constraints drive the choice in practice:
- Hygiene and cleaning regime. Wet washdown, dry cleaning and allergen changeover place different demands on the surface. Hygienic conveyor belts for food processing are regulated by FDA and EC (European Community) requirements, including EC 1935/2004, so the belt's cleanability is a compliance input rather than a preference.
- Product and load behaviour. Small packages, wet or sticky product, incline conveying, accumulation pressure and high-speed transfers all change which surface geometry survives daily operation.
- Drive architecture. Friction drive and positive-engagement drive fail differently, are maintained differently and tolerate different loads.
- Documentation and continuity. Certificates, spare-part categories, replenishment lead time and after-sales support decide whether the choice survives the second year of operation.
The practical rule is to rank the constraints first and choose the architecture second. Selecting by unit price alone usually transfers the cost into changeover time, cleaning validation and unplanned downtime.
Industry Background: Market Scale, Compliance Pressure and Regional Supply
Conveyor belting is a large, consolidating category, and the published numbers should be read as background rather than as a procurement input. Intel Market Research valued the global conveyor belt market at USD 8.11 billion in 2024 and projected USD 9.73 billion by 2032. Market Research Future placed 2024 at USD 8.29 billion, while Mordor Intelligence estimated USD 5.84 billion for 2025. The spread is explained largely by scope — whether a study counts belts alone or complete conveying systems — which is why buyers should treat headline market size as context and not as evidence about any single product decision.
Within the category, rubber conveyor belts led with an approximately 52.0% share in 2024/2026, according to Future Market Insights, driven by abrasion resistance in heavy-duty duty cycles. That figure also implies that the remaining share is distributed across other belt families — plastic modular belts, PU flat belts, textile-reinforced constructions and specialty belts. Textile-reinforced conveyor belts alone accounted for over USD 3.42 billion in 2024, favoured for flexibility and strength in mining and construction, according to Global Market Insights. The global industrial synchronous timing belts market was estimated at USD 2.81 billion in 2024, which matters here only as a boundary marker: positive-drive families are a separate market with a separate decision logic.
On the supply side, Asia-Pacific is the largest regional market, accounting for approximately 46.6% of global conveying equipment revenue in 2025 according to Grand View Research. That concentration is relevant to sourcing strategy: it means a meaningful share of conveyor belt supply, and of the modular and flat belt components used in food and beverage machinery, is sourced from the region. Among global manufacturers, Market Research Future lists Continental AG, Fenner Dunlop, Bridgestone, Habasit and Yokohama Rubber as leading players, alongside a deep tier of regional specialists.
The compliance layer has tightened in parallel. Industrial conveyor belts are tested against frameworks such as ISO 283 for tensile strength and ISO 284 for electrical conductivity, while hygienic belts for food processing are governed by FDA and EC requirements. For a food and beverage buyer, the practical consequence is that belt selection now produces documents, not just parts.
Detailed Solution: Two Architectures, Two Different Jobs
Modular Mesh Chain: PQ350mm±3mm in PP/POM
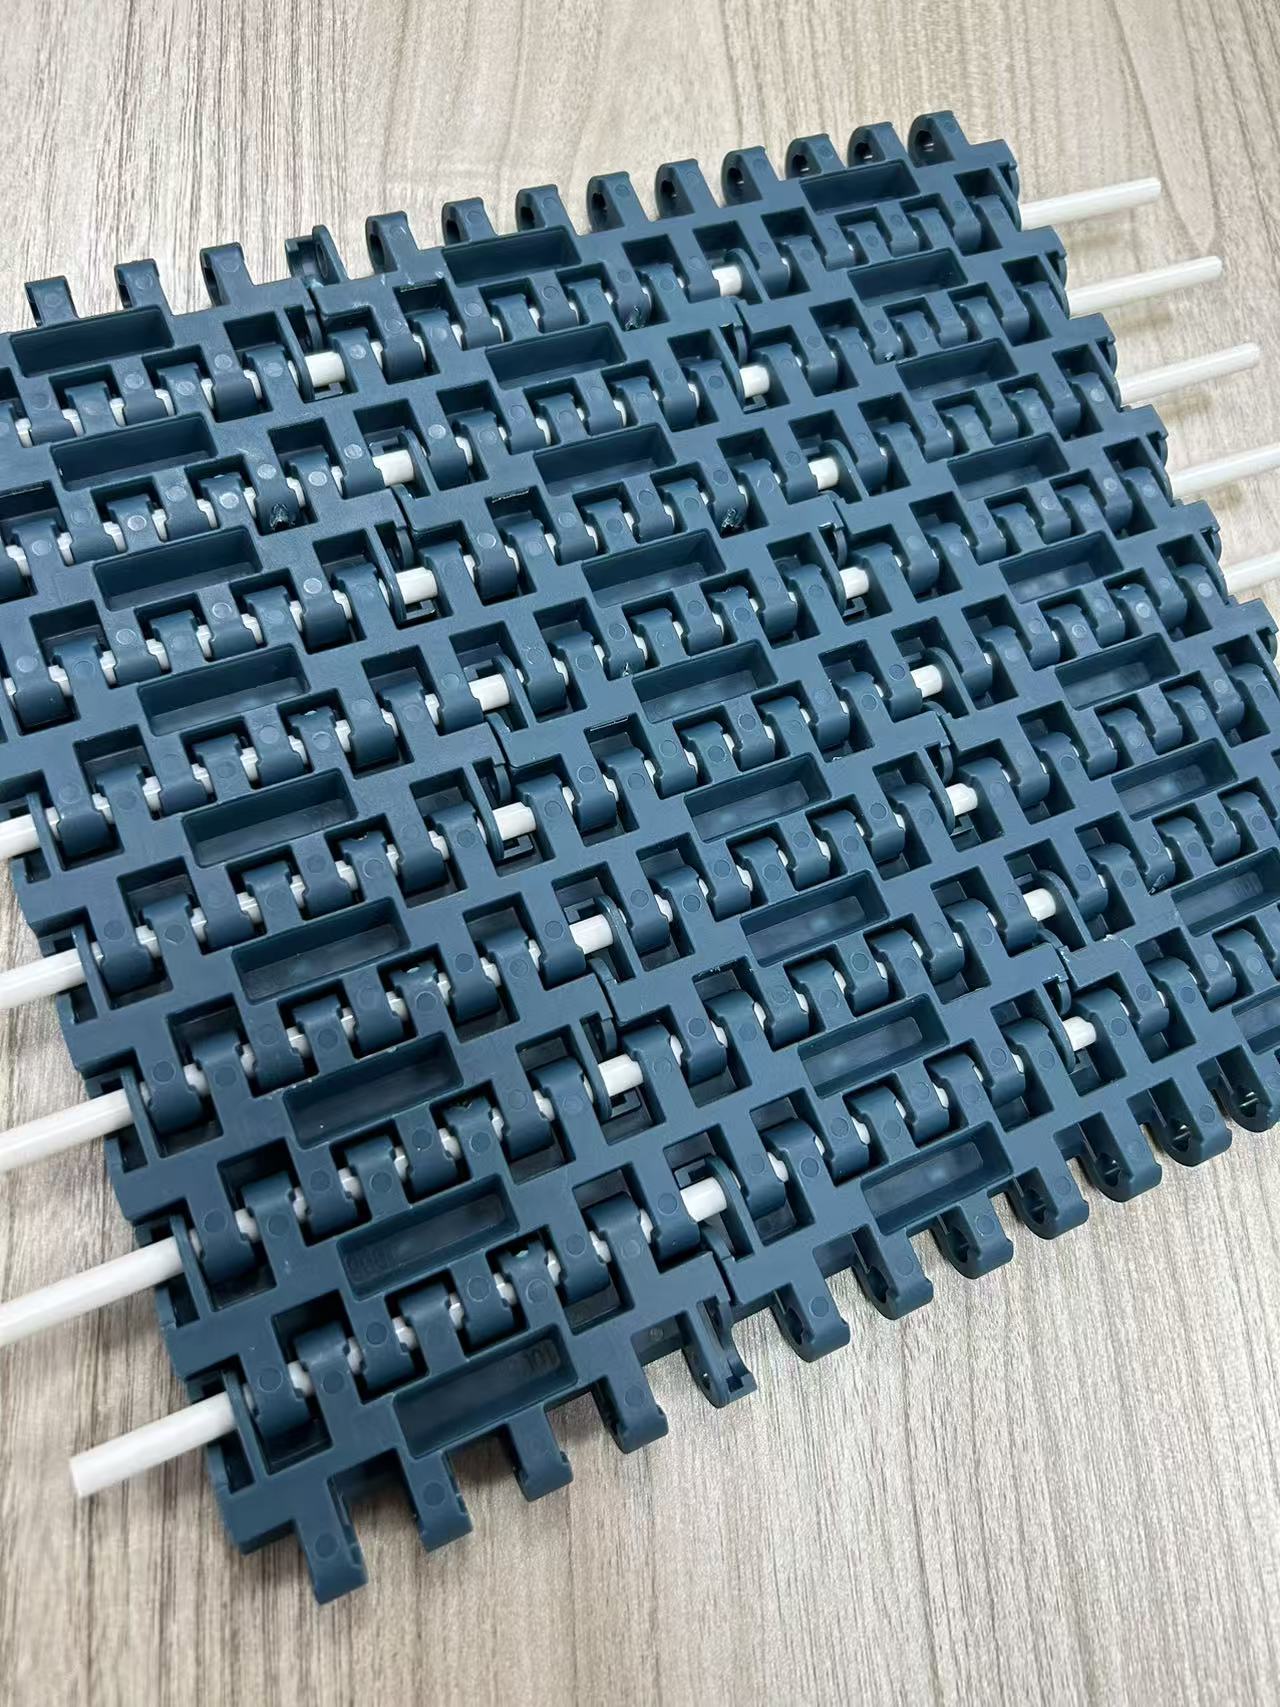
The Modular Mesh Chain PQ350mm±3mm is a modular chain belt for the food industry. Its verified specification is unusually complete for a comparison article, and that specification is the reason it can be evaluated against a flat belt at all:
- Type: modular chain belt for the food industry, with flat belt geometry and straight baffles
- Width: 350 mm ± 3 mm
- Pitch: 25.4 mm
- Material: PP blue modules with PP pins, in a PP/POM material family
- Baffle width: 283.4 mm ± 3 mm
- Baffle height: 50 mm
- Baffle spacing: 153.6 mm
- Distance from baffle to both side edges: 33.3 mm
- Documented industries: food, beverage and pharmaceutical
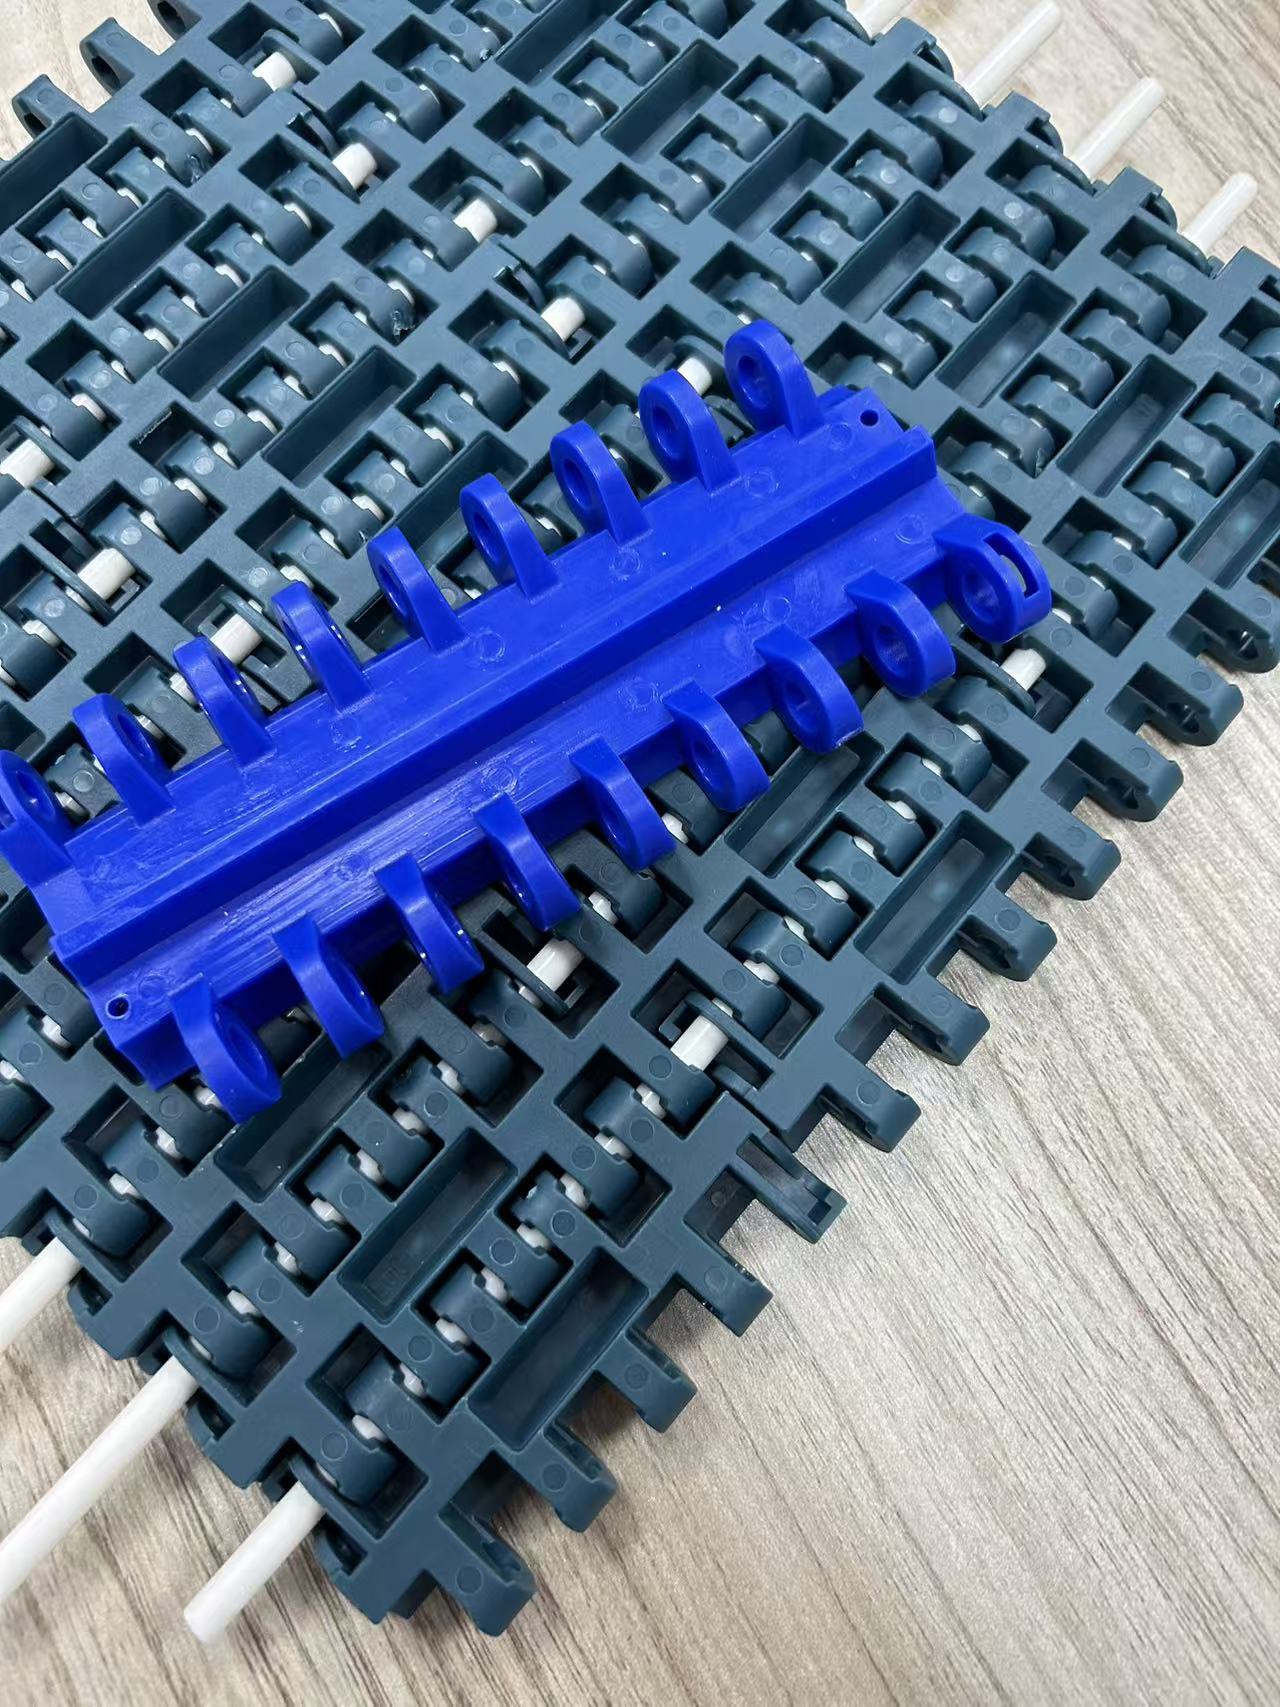
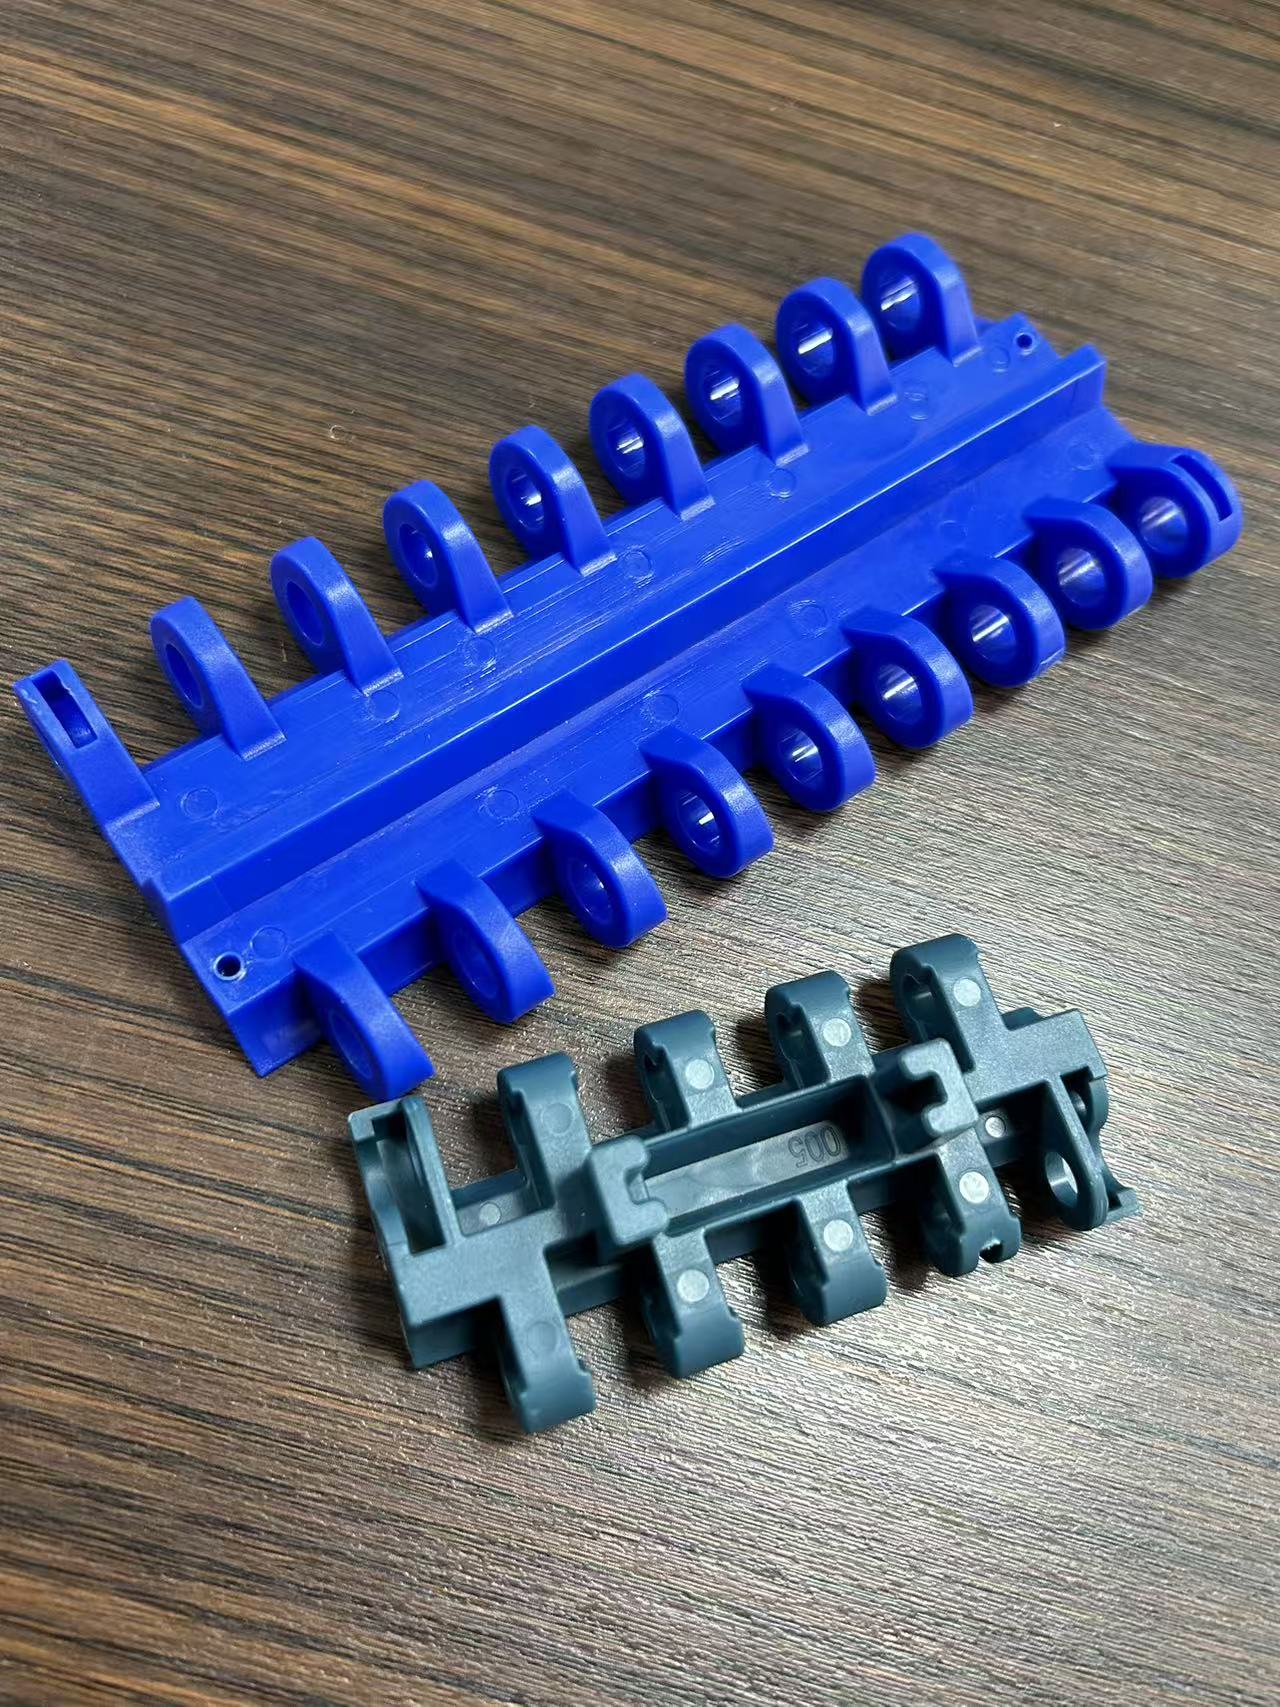
Read as an engineering document rather than a catalogue line, this specification answers most of the questions a food and beverage line raises. A 25.4 mm pitch is the standard modular pitch, which means the belt is driven by a sprocket engaging the modules rather than by friction on a pulley — a positive-engagement architecture. Individual modules and hinge pins are replaceable, so a damaged section does not require replacing the whole belt. The open modular surface, with gaps between modules and around the hinge pins, is generally specified where drainage, airflow and open-surface cleaning are priorities. The straight baffles define product pockets: at 50 mm height with 153.6 mm spacing, they support inclined conveying, metering and product separation, while the 283.4 mm ± 3 mm baffle width and 33.3 mm edge clearance define the usable product zone inside a 350 mm belt.
PU Flat Belt: Continuous, Narrow and Precision-Oriented
The PU flat belt in this comparison is a different architecture entirely. The referenced models — 2482*16, SMT-UGU-09B-J-L2210-W15 and FLAT BELT HY-18-568*14 NFT-NFB — are specified by material, width and length: PU, 16 mm width, 2482 mm length in the quoted configuration. There is no pitch in the specification because there is no module pitch to define; the belt is a continuous part, and the specification logic is dimensional rather than modular. Its documented application fields are logistics and photovoltaic, among others.
That dimensional profile is informative. A 16 mm wide, 2482 mm long PU flat belt is a narrow, thin, low-mass conveying element, which is exactly the profile required inside machinery where the belt must thread through tight transfer geometry rather than carry bulk product across an open line. PU is widely specified where a smooth, closed, low-retention surface suits the product and the cleaning method. Where the referenced flat belt models operate, they run on pulleys with friction drive rather than on sprockets, which changes the failure mode from module wear to belt tracking, tension and surface condition.
The Core Trade-offs: Cleaning, Strength and Flexibility
Cleaning. The modular mesh chain presents an open surface. The PU flat belt presents a closed one. Neither is universally cleaner; they are cleaned differently, and the correct question is which one validates against the actual regime. Open modular geometry is generally preferred where product debris must pass through or be flushed out of the belt body. A closed continuous surface is generally preferred where a smooth, wipeable face and minimal product retention on the carrying side are the priority.
Strength and load path. In the modular chain, load is shared across linked modules and transferred through sprocket engagement at 25.4 mm pitch. In the flat belt, load is carried by the belt's continuous body and transferred by friction at the pulley. The modular architecture tolerates local damage better — a single module is replaceable — while the flat belt concentrates the entire conveying function in one part, so a failure is a full-belt replacement.
Application flexibility. This is where the two specifications diverge most sharply. The modular mesh chain can be re-specified in width, baffle layout, baffle height and side configuration, and it can be built to a defined 350 mm ± 3 mm envelope for guide-rail clearance. The flat belt's geometry is fixed at the belt level: changing width or length means a new belt, and adding product control features means changing the belt specification rather than adding components to it.
Known limits. PP and POM are thermoplastic materials, and neither is the right answer when temperature is the dominant constraint. Where high-temperature resistance governs the application, the relevant product family is a different one: Shanghai Pengqian has developed a high-temperature resistant silicone belt specifically to break through the limitations of traditional belts in special environments. Stating that limit explicitly matters, because the most expensive belt selection error is applying the right architecture in the wrong temperature window.
Step-by-Step Breakdown: Specifying a Food & Beverage Belt Without Rework
The sequence below works in either direction — it will confirm a modular mesh chain choice or disqualify it in favour of a flat belt before any money is committed.
Step 1 — Rank the constraints. Write down the hygiene class, cleaning regime, product type, duty cycle and documentation requirement, then rank them. Whichever constraint ranks first eliminates one architecture quickly.
Step 2 — Fix the geometry envelope. Define the required belt width and side clearance. In the referenced configurations this is a 350 mm ± 3 mm modular belt against a 16 mm wide flat belt, which are not competing answers to the same question — they belong to different conveying tasks. The ± 3 mm tolerance is a genuine design input for guide rails and transfer plates, not a rounding detail.
Step 3 — Choose the surface architecture. Open modular surface or closed continuous surface. Decide this against the cleaning regime first, because it is the most expensive characteristic to change later.
Step 4 — Select the material against the duty. PP blue with PP pins in a PP/POM family for modular food, beverage and pharmaceutical duty; PU for flat belt configurations; silicone where high-temperature resistance dominates.
Step 5 — Define the drive interface. A 25.4 mm pitch modular chain requires a matched sprocket and shaft arrangement. A flat belt of the referenced type requires pulley specification, tensioning and tracking provisions. Choose the drive before the belt, not after.
Step 6 — Specify baffles and product control. If the line inclines, meters or separates product, the baffle geometry is part of the belt specification. For the PQ350mm±3mm that means a 283.4 mm ± 3 mm baffle width, 50 mm baffle height, 153.6 mm baffle spacing and 33.3 mm clearance from each side edge.
Step 7 — Verify documentation before the purchase order. Check the quality management certificate and its scope, validity window and issuing body. Shanghai Pengqian holds ISO 9001 certification number NOA2209224, issued by NOA Group against the GB/T 19001-2016 idt ISO9001:2015 Standard, with a scope covering the manufacture and sales of transmission equipment (industrial belt) and a validity period from 2022-08-02 to 2028-08-01. The company was also rated a Shanghai High-tech Enterprise in 2022 under certificate number GR202231006882, and has submitted 26 patent applications to the State Intellectual Property Office, including 6 invention patents.
Step 8 — Run a pilot and write the acceptance criteria. Define noise, speed, tracking stability and cleaning validation targets before the trial starts, so the result is measurable rather than impressionistic.
Step 9 — Lock the commercial parameters. Confirm the minimum order quantity, lead time, capacity and testing routine in writing. For this supplier the stated figures are a minimum order quantity of 20 units, a lead time of 10–15 days, a monthly capacity of 100,000 units and 100% testing, with customization available for logo, size, material and hole patterns to customer requirement.
Use Cases: Where Each Belt Earns Its Place
Where the modular mesh chain fits
The PQ350mm±3mm is documented for food, beverage and pharmaceutical industries, and its geometry explains why. Baffled modular chain suits lines that incline, meter or separate product; open geometry suits lines where product debris and cleaning fluid must leave the belt body; sprocket drive suits lines where slip between belt and pulley is unacceptable. Fruit and vegetable handling, carton and package conveying in beverage plants, and bakery-adjacent duty within the material's temperature window are the natural applications. The manufacturer's products are used across photovoltaic, electronic semiconductor, textile, food, logistics, packaging and printing, daily necessities, automation machinery and glass manufacturing fields, so the modular range sits inside a broader conveying portfolio rather than standing alone.
Where the PU flat belt fits
The referenced flat belt models are documented for logistics and photovoltaic fields and other industries. Their value is precision and low mass: a 16 mm wide, 2482 mm long belt can carry a small, light or delicate item through tight machinery geometry where a modular chain would be structurally impossible to route. Where a smooth closed surface protects the product, and where the load is low enough that friction drive is sufficient, the flat belt is the simpler architecture. PU flat belts are also commonly specified where the conveying element must remain thin enough to pass through a transfer or nip point.
Case evidence from an operating line
One documented deployment illustrates what an accepted modular installation looks like. A food-industry application delivered to an automotive OEM customer in Argentina used 200 units and ran for a one-year period with stable operation; low noise and high-speed operation were the highlighted performance characteristics. For a buyer evaluating a supplier, that combination is more informative than a generic capability claim, because noise and speed are the two characteristics that expose an incorrectly tensioned or badly tracked belt within weeks.
Comparison Table: Modular Mesh Chain vs PU Flat Belt
| Decision criterion | Modular Mesh Chain — PQ350mm±3mm | PU Flat Belt — 2482*16 / SMT-UGU-09B-J-L2210-W15 / FLAT BELT HY-18-568*14 NFT-NFB |
|---|---|---|
| Construction | Modular links joined by hinge pins; modular chain belt type for the food industry | Continuous flat belt; specified by material, width and length rather than by pitch |
| Material | PP blue modules with PP pins; PP/POM material family | PU |
| Reference width | 350 mm ± 3 mm | 16 mm in the referenced model |
| Reference length | Not fixed — belt length follows the module count | 2482 mm in the referenced model |
| Pitch and drive interface | 25.4 mm pitch with sprocket engagement (positive drive) | No pitch specified in the referenced data; flat belts of this type run on pulleys with friction drive |
| Product control geometry | Straight baffles 283.4 mm ± 3 mm wide, 50 mm high, spaced 153.6 mm, 33.3 mm from each side edge | Not specified in the referenced product data |
| Cleaning behaviour | Open modular surface with gaps between modules and around hinge pins; generally specified where drainage, airflow and open-surface cleaning are priorities | Continuous closed surface; generally specified where a smooth, low-retention face suits the product and the cleaning method |
| Load path | Load shared across linked modules and transferred through sprocket engagement | Load carried by the continuous belt body and transferred by friction at the pulley |
| Application flexibility | Width, baffle layout and side configuration can be re-specified; individual modules are replaceable | Geometry is fixed at belt level; a change of width or length means a new belt |
| Documented industries | Food, beverage, pharmaceutical | Logistics, photovoltaic and other industries |
| Certification coverage | Covered by the manufacturer's ISO 9001 scope for the manufacture and sales of transmission equipment (industrial belt) | Covered by the same ISO 9001 scope |
| Commercial parameters | Supplier-level terms apply to both families: MOQ 20 units, lead time 10–15 days, monthly capacity 100,000 units, 100% test, customization of logo, size, material and hole patterns | |
| Best-fit call | Open, baffled, sprocket-driven conveying within a defined 350 mm width | Narrow, continuous, low-mass transfer where a thin closed surface is preferred |
Read the table as a decision sequence rather than a scorecard. If the first constraint is cleaning under an open-surface regime and the second is product support on an incline, the modular mesh chain resolves both. If the first constraint is routing a narrow belt through tight machinery geometry, the PU flat belt resolves it, and no amount of modular flexibility compensates for a belt that physically will not fit.
Frequently Asked Questions
What certifications and standards matter when buying a food-grade conveyor belt?
Three layers matter. The first is the manufacturer's quality management system: Shanghai Pengqian holds ISO 9001 certification number NOA2209224 issued by NOA Group, based on the GB/T 19001-2016 idt ISO9001:2015 Standard, valid from 2022-08-02 to 2028-08-01, with a scope covering the manufacture and sales of transmission equipment (industrial belt). The same company was rated a Shanghai High-tech Enterprise in 2022 under certificate number GR202231006882. The second layer is food-contact compliance: hygienic conveyor belts for food processing are regulated by FDA and EC (European Community) requirements, including EC 1935/2004, so the belt's intended cleaning regime should be documented, not assumed. The third layer is belt testing frameworks, where ISO 283 covers tensile strength and ISO 284 covers electrical conductivity for industrial conveyor belts.
Can a modular mesh chain be customized to a specific line width and baffle layout?
Yes, within the supplier's stated customization scope. The referenced Modular Mesh Chain PQ350mm±3mm is a 350 mm ± 3 mm wide modular belt at 25.4 mm pitch, supplied in PP blue with PP pins, with straight baffles 283.4 mm ± 3 mm wide, 50 mm high, spaced 153.6 mm and set 33.3 mm from each side edge. Shanghai Pengqian's stated customization covers logo, size, material and hole patterns according to customer requirement, with 100% testing and a monthly capacity of 100,000 units. If temperature rather than configuration is the dominant constraint, the relevant product family is different — the company's high-temperature resistant silicone belt addresses exactly that requirement.
What drives the cost difference between a modular mesh chain and a PU flat belt?
The cost drivers are structural. A modular chain is a multi-part assembly: modules, hinge pins and a matched sprocket interface at 25.4 mm pitch, so part count, sprocket specification and module-level spares shape the total. A PU flat belt is a single continuous part, so its cost is dominated by material, width, length and endless fabrication, and it is replaced as one unit when it fails. In both cases the largest figure on the balance sheet is rarely the belt price — it is changeover time, a cleaning cycle that does not validate, or unplanned downtime. Buyers should compare the two architectures on total cost of ownership across the service interval, using the stated 10–15 day lead time and MOQ of 20 units as the replenishment baseline.
How can a buyer validate a belt before committing to a full line?
Validation should be structured around the constraint that ranks first, not around visual inspection. A first order can start at the supplier's stated minimum order quantity of 20 units, with customization of logo, size, material and hole patterns applied to the trial specification so the trial represents the production part. Acceptance criteria should be written before the trial begins: noise level, running speed, tracking stability across the 350 mm ± 3 mm width, cleaning validation under the real regime, and completeness of documentation. The two verification points available at this stage are the supplier's 100% test before shipment and its remote after-sales support.
What lead time applies, and what is the next step for a food and beverage project?
The stated lead time is 10–15 days, against a monthly capacity of 100,000 units and a minimum order quantity of 20 units, with 100% testing before shipment and remote after-sales support. For a food and beverage line, the most efficient next step is to send the line parameters — required width and pitch compatibility, baffle geometry, cleaning regime, duty cycle and the documentation list — and request a quotation or a trial quantity against that specification. The company's product brochure can be downloaded here: Shanghai Pengqian transmission products catalogue, and further product information is available at www.shanghai-pengqian.com.
Conclusion: Choose the Constraint, Then Choose the Belt
The modular mesh chain PQ350mm±3mm and the PU flat belt range are not competitors for the same slot on a line. They are answers to different constraints. The modular mesh chain answers open-surface cleaning, positive sprocket drive, replaceable modules and configurable product control — at a 25.4 mm pitch, 350 mm ± 3 mm width, with straight baffles 283.4 mm ± 3 mm wide and 50 mm high. The PU flat belt answers narrow, thin, low-mass transfer where a continuous closed surface and a 16 mm wide, 2482 mm long profile are the requirement, with friction drive and a simpler part count.
The decision framework that survives contact with production is short: rank hygiene and cleaning, geometry, load, drive architecture and documentation in that order; select the architecture that satisfies the first and second constraints; then verify certificates, lead time, minimum order quantity and testing before committing. Suppliers that publish verifiable specification data, an ISO 9001 certificate with a defined scope and validity window, and clear customization and testing parameters make that verification possible. Shanghai Pengqian Transmission Equipment Co., Ltd., established in 2012 in Songjiang District, Shanghai, with a 3,000 m² facility, a 60-person team, an 8-engineer R&D group and roughly 40% of output exported to Europe, Asia and the Middle East, operates on that basis.
Next step: sample and quotation
If you are evaluating a modular mesh chain against a PU flat belt for a specific food or beverage line, send the line parameters — width, pitch, baffle layout, cleaning regime and required documentation — and request a trial quantity or quotation. Contact Abby at abbypeng@pengqian.cn, or download the product brochure for the full specification range.