Designing a Butyrate-Producing Probiotic Powder for Metabolic Management
Designing a Butyrate-Producing Probiotic Powder for Metabolic Management
This application guide is written for formulators, product developers, and supplement brand owners building metabolic-management products around a butyrate-producing probiotics powder. It covers the strain rationale for Clostridium butyricum CCFM1299, how VPro® 5-layer microencapsulation changes powder behavior in a finished dosage form, and why maltodextrin is used as the carrier in this raw material. All specifications below are drawn from the published product data and certification record of Shanghai Unibio Lab Co., Ltd.
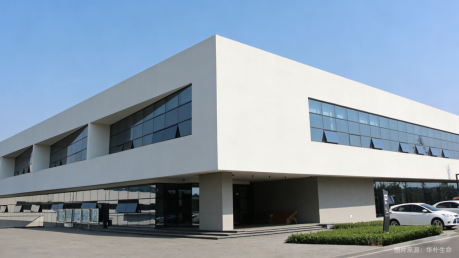
Manufacturing base for probiotic raw powder production — Shanghai Unibio Lab Co., Ltd.
Why a Butyrate-Producing Strain Is a Formulation Problem, Not Just a Label Claim
Most probiotics powder projects fail at the same point: the strain survives fermentation, survives freeze-drying, and then does not survive the finished product. A butyrate-producing strain raises that difficulty further. Clostridium butyricum CCFM1299 is formulated as a butyrate-producing probiotic powder, and butyrate producers are typically exposed to the same industrial stressors as other anaerobic strains — oxygen during blending, moisture during storage, and gastric acid and bile salts after consumption.
For a formulator, the practical question is not “which strain produces butyrate.” It is: which powder format preserves viable count across the product's shelf life, and which protective system keeps the strain intact long enough to reach the lower gastrointestinal tract. That is where strain selection, encapsulation, and carrier choice converge.
Three variables decide the outcome:
- Strain identity and viable count — the specific culture, its declared potency per gram, and its documented storage conditions.
- Protective architecture — whether the strain is delivered as a bare freeze-dried cell or inside a multi-layer encapsulation system.
- Carrier and dosage form — the bulking agent, the powder format chosen, and the packaging regime that protects the final blend.
Handled correctly, these three variables produce a stable metabolic-management powder. Handled incorrectly, they produce a product whose label claim diverges from its actual viable count within months.
Market Context: Why Metabolic Probiotic Powders Are Drawing Formulation Investment
The commercial backdrop matters because it explains why formulators are being asked to build more sophisticated powder systems rather than simple single-strain blends.
According to Global Market Insights, the global probiotics market was valued at USD 72.1 billion in 2024 and is projected to reach USD 165.1 billion by 2034. Within that broader market, MarketsandMarkets reports that probiotic dietary supplements specifically reached USD 10.60 billion in 2026, with a forecast CAGR of 9.5% through 2031.
Two structural signals sit behind those figures. First, microencapsulation using materials such as alginate or chitosan is now recognized as a key technical trend for ensuring probiotic viability through gastric acid and bile salts (PMC / MDPI). Second, the metabolic-management category has shifted from marketing concept to a defined product segment — which means buyers increasingly evaluate powders on measurable delivery performance rather than strain naming alone.
For a formulator, the consequence is direct: the protective system is now as important a design decision as the strain itself.
The Core Solution: CCFM1299 Powder with VPro® 5-Layer Encapsulation
Shanghai Unibio Lab Co., Ltd supplies Clostridium Butyricum CCFM1299 as a butyrate-producing probiotic raw powder, combining the strain, a maltodextrin carrier, and VPro® 5-layer microencapsulation material inside a single raw material specification.
Strain Rationale: Clostridium butyricum CCFM1299
CCFM1299 is positioned in the product catalogue for three application categories: dietary supplements, metabolic-management products, and health products. The published product specification reads as follows:
Product: Clostridium Butyricum CCFM1299
Model: CCFM1299
Type: Clostridium butyricum Butyrate-Producing Probiotic Powder
Viable count: 10B CFU/g
Strain origin: Independent lab culture
Material composition: Probiotic strain + maltodextrin carrier + VPro® 5-layer encapsulation material
Storage: Keep in a well-closed container away from moisture and direct sunlight, at room temperature
Shelf life: 24 months under recommended storage
Applicable industries: Dietary Supplement, Metabolic Management Products, Health Product
For formulation purposes, the fixed 10B CFU/g specification is the key planning number. It means the formulator does not need to re-validate a variable potency input for every production run, which simplifies dose calculation and finished-product labeling.
The Role of VPro® 5-Layer Microencapsulation
VPro® is a five-layer embedding technology developed for probiotic raw materials. Each layer addresses a specific failure mode that affects powder performance between production and consumption:
- Micromolecular protective layer — anti-freezing and anti-stress protection during freeze-drying and handling.
- Prebiotic nutrition layer — designed to support in-vivo proliferation after consumption.
- Liposome enteric adhesion layer — aimed at improving intestinal colonization.
- Acid and enzyme resistant layer — supports survival through gastric digestion.
- Oxygen and moisture barrier layer — extends shelf stability.
Across the VPro® platform, the technology is documented to lift freeze-drying survival rate by 40%, extend shelf life to 24 months, and support fermentation density above 3.5×10¹⁰ CFU/mL with lyophilized powder concentration up to 8.0×10¹¹ CFU/g. These platform figures are relevant to CCFM1299 design work because they describe the protection envelope the strain is delivered inside — not a claim about the strain's clinical effect.
Why Maltodextrin Is the Carrier
CCFM1299 is supplied with a maltodextrin carrier as part of the raw material. In powder formulation, maltodextrin serves as a neutral bulking and dispersion medium: it standardizes the powder's flow behavior, allows accurate low-dose weighing during blending, and does not introduce a flavor or functional conflict with the encapsulated strain. Because the carrier is already part of the supplied raw material, the formulator's blending step starts from a consistent base rather than from a separate carrier decision.
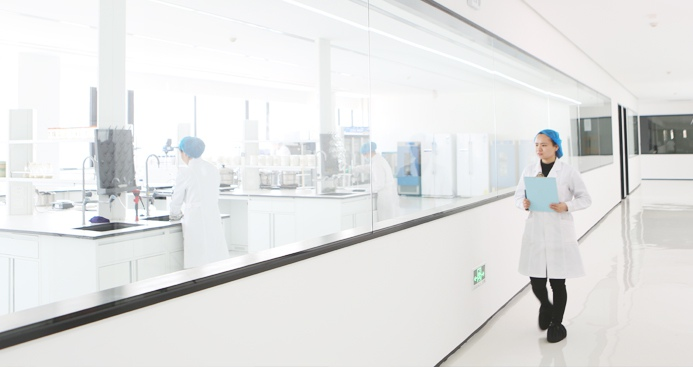
Production line used for encapsulated probiotic powder processing.
Step-by-Step: Designing a Metabolic Powder with CCFM1299
Step 1 — Define the metabolic positioning before selecting dose
CCFM1299 sits in the metabolic-management and health-product categories. Before fixing a CFU dose, define whether the product is positioned as a general adult gut-health powder or as a metabolic-management formula, since that decision drives the final blend ratio and the claims the brand intends to support. This step is a positioning decision, not a technical one — but it determines every technical step that follows.
Step 2 — Lock the viable count input
CCFM1299 is specified at 10B CFU/g. In a finished powder, the formulator calculates the grams of raw material needed to hit the target CFU per serving, then verifies that the declared finished-product count still holds at end of shelf life. Because VPro® encapsulation is already applied to the raw material, the formulator does not need to add a separate encapsulation step during blending.
Step 3 — Confirm the encapsulation layer is intact at receipt
Request the batch certificate of analysis covering viable count, microbial safety, and heavy metals before blending. Shanghai Unibio Lab maintains 100% in-house lab testing for viable count, microbial safety, and heavy metals on every batch, and supports third-party inspection by SGS or Intertek upon client request. For a formulator, this is the verification step that confirms the VPro® protective layers survived shipping and storage prior to blending.
Step 4 — Design the blending environment around moisture and oxygen control
The oxygen and moisture barrier layer inside VPro® extends shelf stability, but it does not make the powder indifferent to blending conditions. Standard practice for encapsulated powders is to control relative humidity during blending and to minimize open-air exposure time. CCFM1299's recommended storage condition — a well-closed container, away from moisture and direct sunlight, at room temperature — should be treated as the design target for the finished product's own storage environment, not only the raw material's.
Step 5 — Select the dosage form
Shanghai Unibio Lab offers customization across powder, bottle, capsule, tablet, sachet, and gummy formats, with customizable CFU concentration and packaging design. For a metabolic-management powder, the two most common routes are a stick-pack or sachet powder and a capsule. Both are supported under the company's OEM, ODM, private label, and custom formula development services. The sachet route keeps the powder format intact; the capsule route trades powder volume for unit-dose precision.
Step 6 — Set packaging and shelf-life parameters
The declared shelf life for CCFM1299 raw powder is 24 months under recommended storage. The finished product's shelf life should be validated against its own packaging format, since moisture ingress through a sachet film differs from moisture ingress through a bottle closure. Cold chain logistics guidance is available as part of the company's after-sales support if the finished format requires it.
Step 7 — Plan the scale-up and MOQ path
Minimum order quantities are 1 kg for single-strain raw powder, 5 kg for multi-strain compound powder, and 5,000 bottles for HelpGut private-label finished capsules or tablets. Lead time is 5–7 days for raw material bulk orders and 25–35 days for private label finished products. Trade terms include FOB Shanghai, CIF for major global ports, DDU, and DDP.
Formulation note: Acceptance criteria are 100% in-house lab testing prior to shipment, with third-party inspection by SGS or Intertek available on request. Payment terms are 100% advance payment, 30-day credit for trusted customers, or 50% advance deposit with balance due 30 days after bill of lading issuance.
Application Scenarios: Where a CCFM1299-Based Powder Fits
The same raw material serves different finished-product briefs depending on the brand's market and positioning. Three documented supply patterns illustrate the range.
Metabolic and intestinal care for pharmacy retail in the Middle East
A Middle East health product wholesaler and pharmacy chain supplier has run a steady cooperation for 1.5 years, with monthly consignments of 12,000 bottles of HelpGut capsules and 8 tons of Akkermansia muciniphila AH39 raw powder for premium metabolic and intestinal care supplements. The project achieved a high customer repurchase rate, and GRAS and HALAL certification supported smooth customs clearance. Customized Arabic packaging and label service was provided. This pattern shows how a butyrate-producing powder can sit alongside other metabolic strains in a retail-facing range.
Gut health capsules and immunity tablets for EU and US brands
An overseas dietary supplement brand and raw material distributor in Germany and the United States has cooperated for three consecutive years, with annual bulk orders of 120 tons of multi-strain probiotic powder to the US and 75 tons of single-strain powder to Germany. The finished products are gut health capsules and immunity chewable tablets for retail. VPro® 5-layer microencapsulation is cited as the mechanism supporting high acid-bile resistance, with full third-party test reports supplied. The customer's product sales increased 42% year-on-year, with strain viability stable through shelf life.
Fermented food and beverage production in Southeast Asia
A fermented food and beverage manufacturer in Thailand and Indonesia has run a two-year cooperation with annual supply of 60 tons of DVS yogurt starter and 90 tons of functional probiotic beverage powder, used for yogurt, fermented milk, and probiotic sparkling drink mass production. Fermentation cycle was shortened, and product flavor and probiotic activity met local food standards. HALAL-certified raw materials matched the local market requirement.
VPro® 5-Layer Structure at a Glance
| Layer | Design Function | Formulation Consequence |
|---|---|---|
| Micromolecular protective layer | Anti-freezing and anti-stress protection | Protects the strain during freeze-drying and powder handling |
| Prebiotic nutrition layer | Supports in-vivo proliferation | Provides a substrate environment after consumption |
| Liposome enteric adhesion layer | Improves intestinal colonization | Aims to support adhesion in the lower GI tract |
| Acid and enzyme resistant layer | Survives gastric digestion | Reduces viability loss through stomach transit |
| Oxygen and moisture barrier layer | Extends shelf stability | Contributes to the 24-month storage specification |
Compliance and Certification for a CCFM1299-Based Product
Certification coverage matters at the formulation stage because it determines which markets a finished product can enter without reformulation. Shanghai Unibio Lab Co., Ltd holds the following qualifications relevant to a CCFM1299-based powder:
- HALAL Certificate — Indonesian BPJPH-recognized HALAL food certification, certificate No. 1821240000, issued by SHANDONG HALAL CERTIFICATION SERVICE (SHC). The scope explicitly lists all probiotic strains including Clostridium Butyricum CCFM1299. Certificate valid to 2028-07-25.
- US FDA Food Facility Registration — registration number 19635371796 for Shanghai Unibio Lab Co.,Ltd, covering probiotic raw materials and probiotic finished dietary supplement production and sales.
- GMP Certificate — CN22/00003036, issued by SGS-CSTC Standards Technical Services Co., Ltd., covering production of probiotic solid beverages (screening, mixing).
- ISO 22000 — CN22/00000437, food safety management system certification issued by SGS-CSTC.
- FSSC 22000 — CN22/00000434, issued by SGS United Kingdom Ltd.
For a US-market or EU-market brief, the formulator should note that the self-affirmed GRAS conclusion held by the company applies specifically to pasteurized Akkermansia muciniphila AH39 raw material and AH39-containing finished products. It does not automatically extend to a CCFM1299-based formula, and the compliance pathway for that product should be confirmed against the applicable market requirements during the design phase.
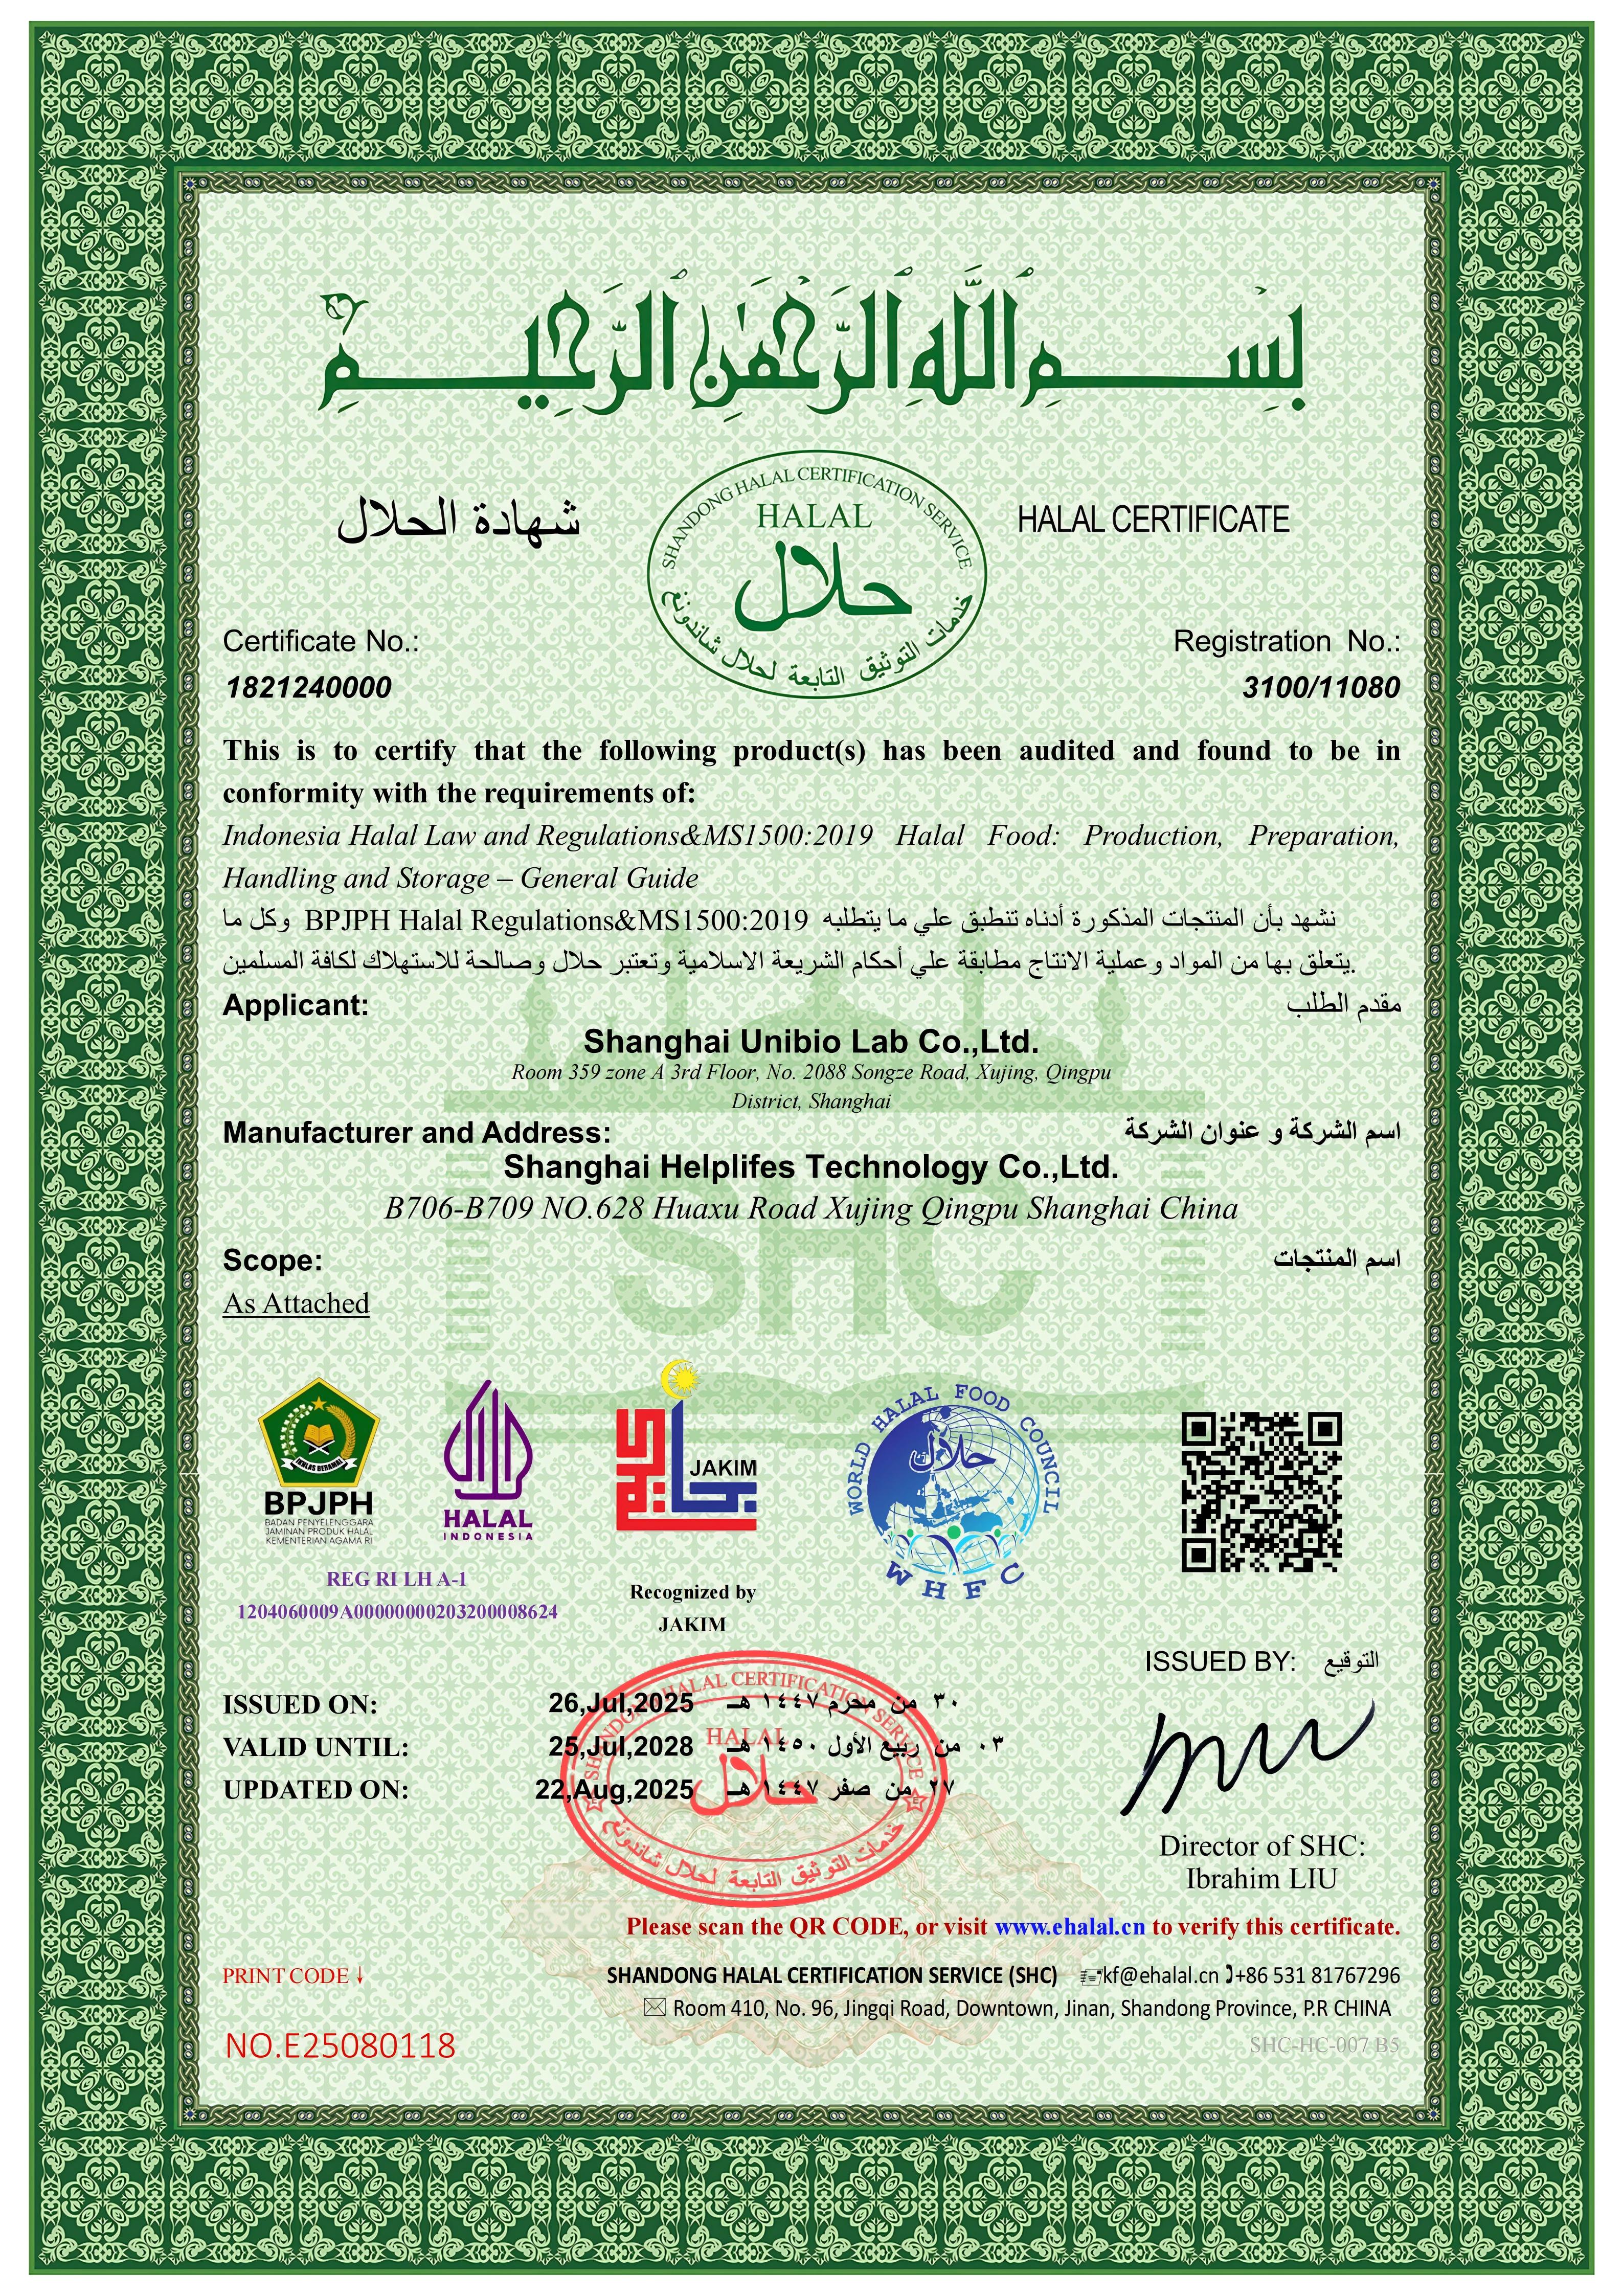
HALAL certification — scope includes Clostridium Butyricum CCFM1299.
Frequently Asked Questions
Can a manufacturer produce an OEM probiotics powder with microencapsulation?
Yes. Shanghai Unibio Lab Co., Ltd offers OEM, ODM, private label, and custom formula development services, covering probiotic strain combination, viable CFU concentration, powder, bottle, capsule, tablet and sachet dosage forms, packaging design, and microencapsulation process adjustment. VPro® 5-layer microencapsulation is applied at the raw material stage, so an OEM project built on Clostridium Butyricum CCFM1299 starts from an already-encapsulated powder.
What certifications cover Clostridium Butyricum CCFM1299?
The HALAL Certificate issued by SHANDONG HALAL CERTIFICATION SERVICE (SHC), certificate No. 1821240000, lists Clostridium Butyricum CCFM1299 within its scope, valid to 2028-07-25. The US FDA Food Facility Registration (No. 19635371796) covers probiotic raw materials and finished dietary supplement production. GMP (CN22/00003036), ISO 22000 (CN22/00000437), and FSSC 22000 (CN22/00000434) cover the production of probiotic solid beverages (screening, mixing). Buyers should confirm which certificates apply to their specific target market before finalizing the compliance file.
What is the minimum order quantity for CCFM1299 powder?
The minimum order quantity is 1 kg for single-strain raw powder and 5 kg for multi-strain compound powder. For finished private-label capsules or tablets, the minimum is 5,000 bottles. Trade terms include FOB Shanghai, CIF for major global ports, DDU, and DDP.
Can a sample be supplied for formulation validation?
Yes. The company provides free strain technical consultation and formulation optimization support, and supplies batch quality reports with each batch. All products undergo 100% in-house lab testing for viable count, microbial safety, and heavy metals. Third-party inspection by SGS or Intertek can be arranged upon request, which allows a formulator to validate the encapsulated powder inside the intended finished format before committing to bulk volume.
What is the lead time for a custom CCFM1299 formulation?
Lead time is 5–7 days for raw material bulk orders and 25–35 days for private label finished products. Complaint resolution is handled within 24 working hours, and cold chain logistics guidance is available if the finished format requires it.
Conclusion
Designing a butyrate-producing probiotic powder for metabolic management comes down to three linked decisions: choosing Clostridium butyricum CCFM1299 as the strain with a fixed 10B CFU/g specification, relying on VPro® 5-layer microencapsulation to protect viability through freeze-drying, storage, and gastric transit, and working with the maltodextrin carrier that is already built into the raw material. Each decision is documented, each is auditable, and together they give a formulator a powder whose behavior at end of shelf life can be planned rather than hoped for.
The next step is a technical consultation and a sample validation run against the intended finished format.
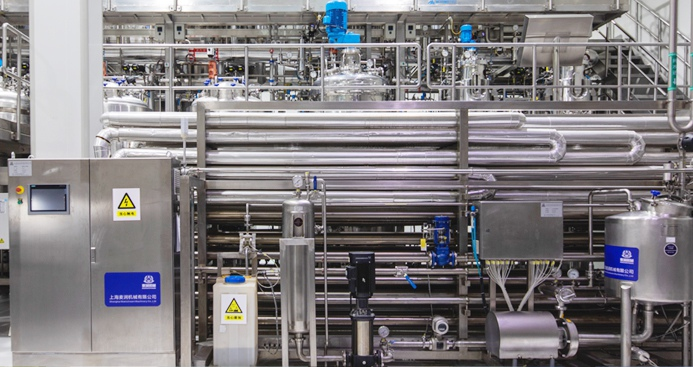
Production capacity supporting OEM, ODM, and private-label probiotic powder projects.
Request a Sample or Technical Consultation
Shanghai Unibio Lab Co., Ltd supplies Clostridium Butyricum CCFM1299 and other encapsulated probiotic raw powders for dietary supplement, metabolic management, and health product applications. Free strain technical consultation, formulation optimization support, and batch quality reports are provided.
Contact: Kevin | Email: kevin@helplifes.com | Tel: +86 135-1234-4323 | WhatsApp: +86 158-2126-0907
Website: www.helplifes.com
Download the full product brochure: Probiotics Powder Catalogue (PDF)