Die Spring Supplier Evaluation: Capability Verification and Delivery Assurance
Evaluating a rectangular die spring supplier should not begin with price. Price tells you what one shipment costs. It does not tell you whether the wire in that shipment is traceable to a heat number, whether the springs passed through multi-stage tempering, whether the ground ends are actually parallel, or whether a replacement set can be on its way on Monday when a stamping die goes down on Friday.
A workable supplier evaluation for die springs rests on two verifiable questions. First, can the factory prove physical control over every step from wire to finished spring? Second, does that control convert into stock and shorter lead times when a buyer needs it? This article walks through both, in that order, with a checklist a procurement team can take into a supplier meeting or a factory audit.
Problem Definition: Why Quotations Cannot Verify Capability
Most die spring sourcing decisions are made on a quotation and a catalogue page. That leaves three gaps open.
The material traceability gap. A catalogue states a wire grade such as 55CrSi or chrome silicon. That statement alone proves very little. What matters is which melt the shipment came from and whether mill test certificates travel with it. Substituting a cheaper wire without heat-number records changes nothing on the quotation and everything about fatigue life.
The process control gap. The durability of a rectangular die spring comes from multi-stage tempering, controlled shot peening, ground end-face parallelism and powder coating. None of these are visible in a price per piece, and none of them are visible in a sample spring either. They determine whether the spring still performs after three months in service.
The supply continuity gap. When a spring fractures during a changeover, the question that decides downtime duration is not unit cost. It is whether stock exists and which weekday it can leave the dock.
With only price information, all three gaps stay invisible. The evaluation method has to change to a different question: what can this factory prove?
Industry Background: Why Die Spring Evaluation Is Tightening
Industrial spring demand moves with the industries that consume it. Grand View Research projects the global industrial springs market to reach USD 7.1 billion by 2033, and the same market study places Asia Pacific at a 33.4% revenue share in 2024. Automotive stamping sits inside that demand: the global automotive stamping market was valued at USD 87.98 billion in 2024. Die springs are among the fastest-wearing components in the stamping dies that serve it.
Standards have tightened alongside the demand. ISO 10243:2019 standardizes dimensions and colour coding for compression springs with rectangular section used in press tools. JIS B5012 specifies allowable tolerances for spring inner and outer diameters, which is a different focus from the mounting hole orientation of ISO 10243. The difference is real and it is where sourcing errors happen: colour codes for the same load class are not identical across the two systems, and a global enquiry that mixes them is a common route to the wrong spring inside a die.
Add currency, freight and duty variability — the US import HS code for helical springs of iron or steel is 732020 — and supplier evaluation stops being a purely technical exercise. It becomes a decision about how much supply certainty you are willing to trade for a lower price.
Detailed Solution: Six Capabilities Worth Verifying
Supplier credibility is built from documented physical control. For rectangular wire die springs, six capabilities are worth requesting and verifying one by one.
1. Traceable Raw Material with Mill Test Certificates
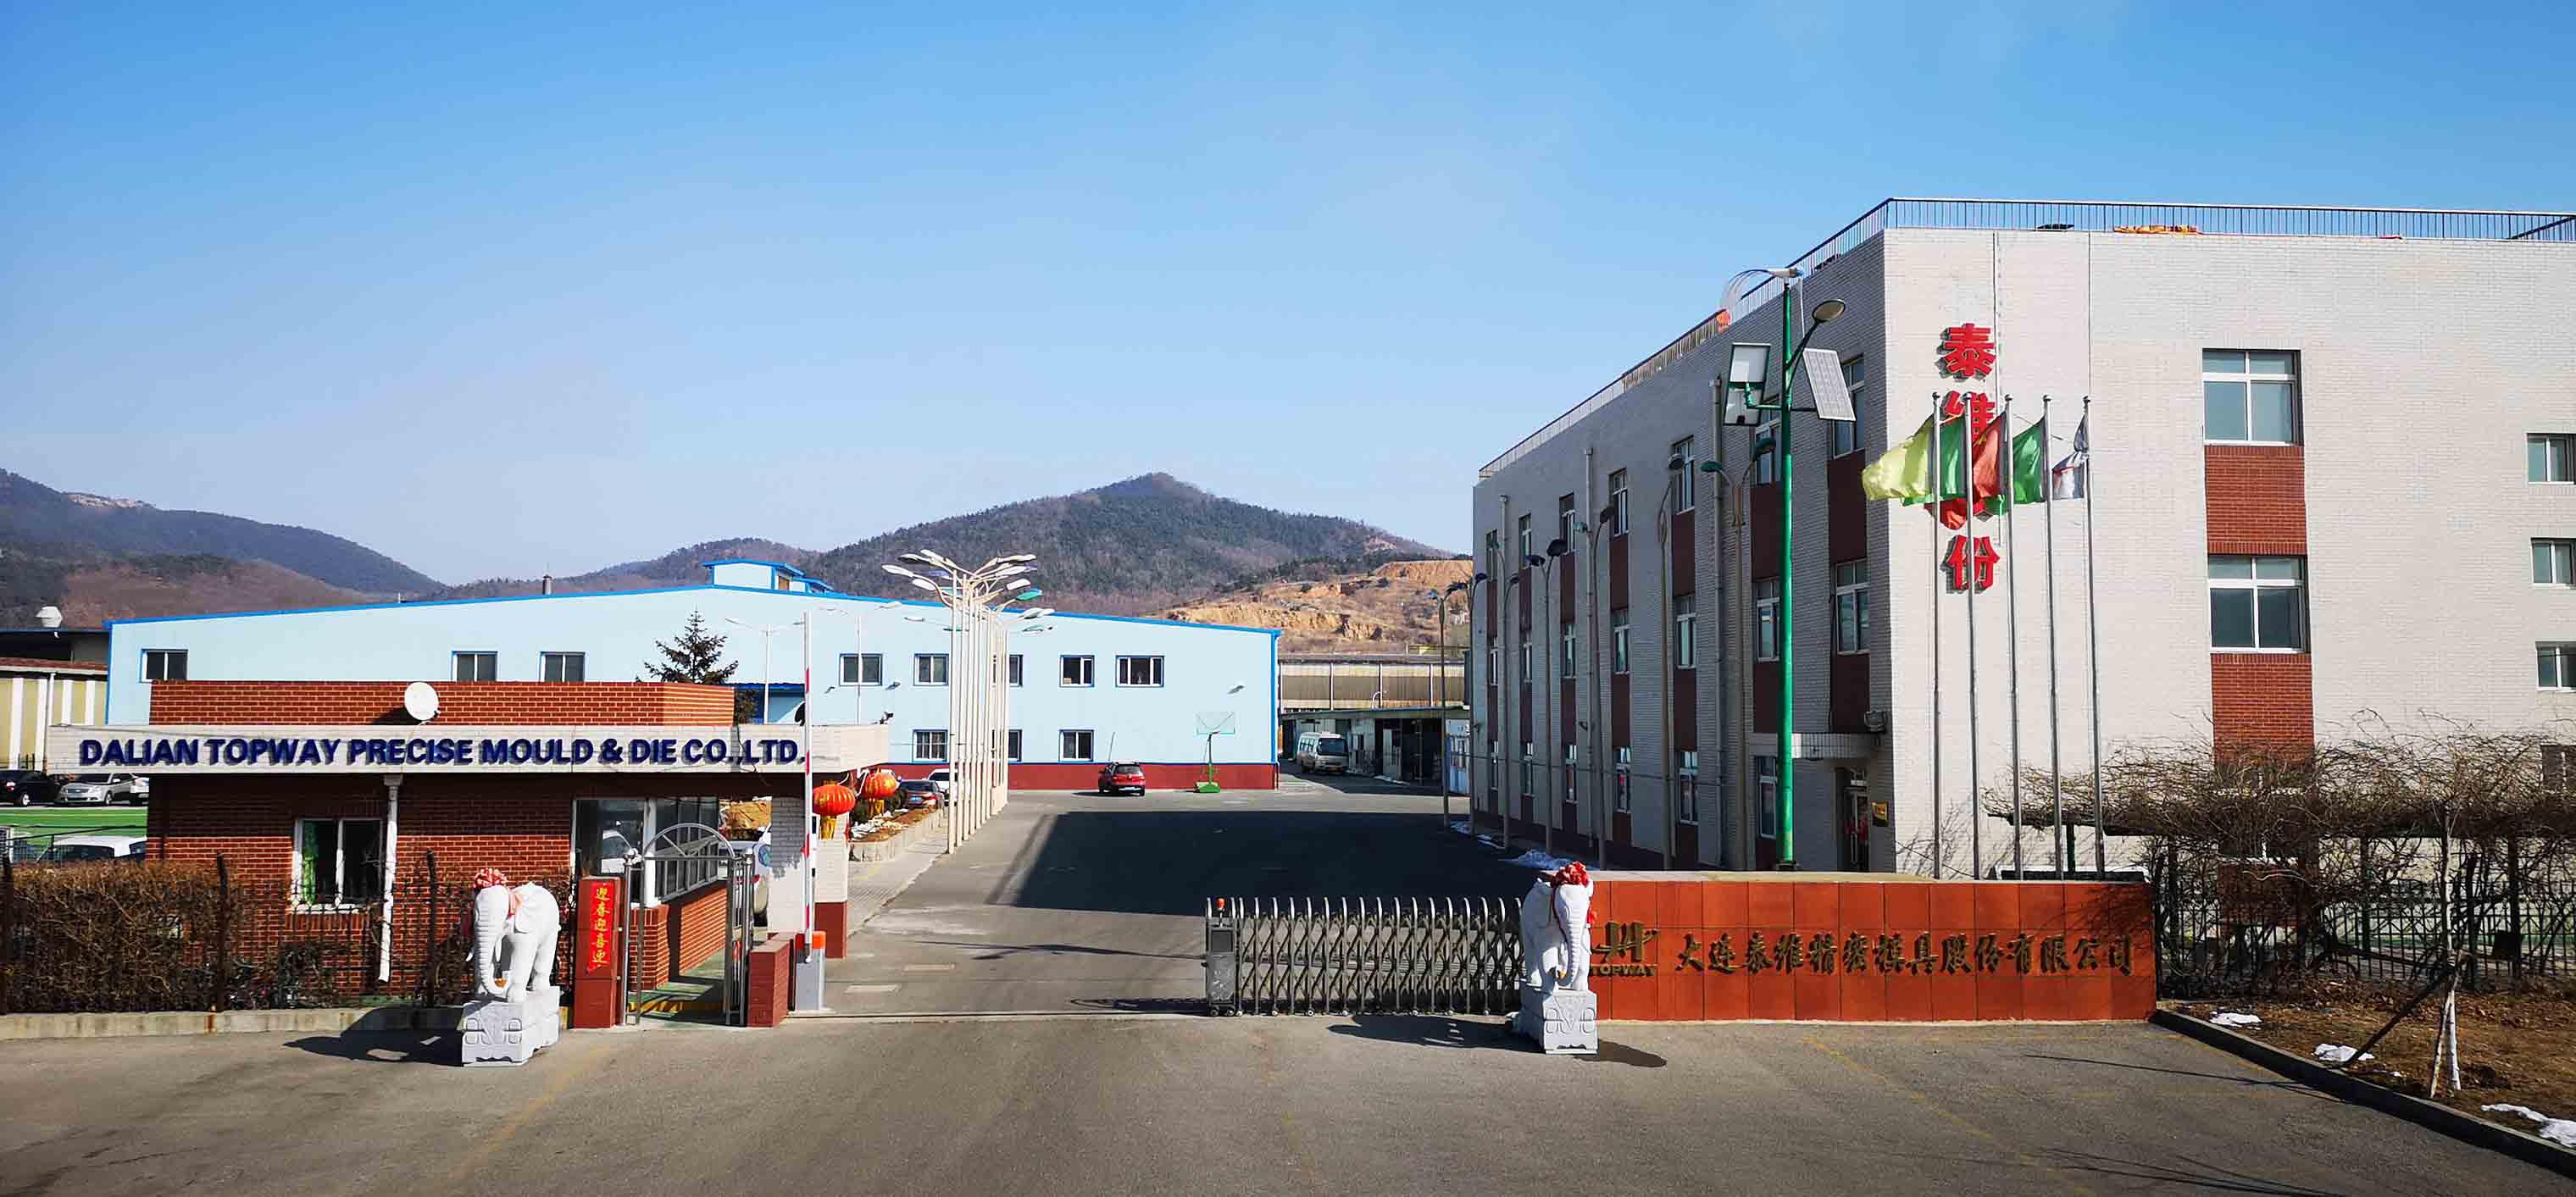
TOPWAY SPRINGS, the spring division of Dalian TopWay Precise Mould & Die Co., Ltd. based in Dalian, China, manufactures rectangular-section precision industrial springs and supplies them in ISO 10243, JIS B5012 and American standard configurations. The factory works exclusively from high-stress oil-tempered alloy steels such as 55CrSi chrome silicon, and mill test certificates together with material heat-number traceability are provided for raw materials. Ask any supplier two questions: which wire grade do you state, and what batch-level record can you attach to each shipment that proves it?
2. Multi-Stage Tempering and Controlled Shot Peening
Tempering is not a single furnace pass and a certificate. Multi-stage tempering stabilizes the microstructure of the wire, while controlled shot peening introduces compressive residual stress at the spring surface to resist micro-crack initiation and propagation. Run in the correct sequence, these two processes are what support a fatigue life of 3,000,000 to 5,000,000 compression cycles. A supplier should be able to describe which parameters are run per production batch and who signs off on them. A plant that can describe its process control behaves differently from one that lists “shot peened” as a catalogue feature.
3. Powder Coating and Closed Ground Ends
Coating has a functional role. High-adhesion powder coating resists moisture, stamping coolants and physical abrasion while keeping load-class colour identification legible. Closed and ground ends, combined with precision grinding to maintain parallelism, keep the load distribution perpendicular, which is the mechanism that reduces lateral deflection wear in rectangular wire die springs. Buyers should confirm which end type is quoted, because closed and ground versus closed un-ground changes how the spring seats in its pocket.
4. Dimensional and Load-Class Coverage Across Three Standards
A catalogue that covers only one standard creates avoidable sourcing friction. ISO 10243 standard springs cover an outer diameter range of 10–63 mm, an inner diameter range of 5–38 mm and a free length range of 25–305 mm. JIS B5012 standard springs run from 6–70 mm outer diameter, 3–38.5 mm inner diameter and 10–350 mm free length. American standard springs cover 10–51 mm outer diameter, 4.76–25.4 mm inner diameter and 25–305 mm free length.
Load-class naming matters just as much. In the JIS B5012 system, CSWF is minimal load, CSWL is light load, CSWM is medium load, CSWH is heavy load, CSWB is extra heavy load and CSWG is super heavy load. In the ISO 10243 system, CIF is super minimal load, CIL is light duty load, CIM is medium duty load, CIH is heavy duty load and CIB is extra heavy duty load. Colour conventions do not match one-to-one between the two systems, so a specification must name the standard rather than the colour.
5. Custom Engineering Beyond the Catalogue
When a die needs a spring that no catalogue lists, the deciding capability is whether the supplier can work from a drawing. Factory-direct engineering support enables production of custom rectangular coil die springs from customer drawings, including non-standard dimensions and load ratings, together with non-standard inner and outer diameters, non-standard free lengths, specialized trapezoidal wire cross-sections, and custom colour or laser marking for private-label programmes.
6. Stock Discipline and Replenishment Response
The final capability to verify is inventory behaviour: which catalogue items are held ready to ship, how fast an order can be dispatched, and how custom orders are scheduled against the production line. Ask with a specific part list rather than a general question about lead times.
Step-by-Step Breakdown: A Capability Audit Sequence
Rather than verifying everything at once, a procurement team can run the audit in seven steps.
- Confirm the standard and the drawing. Write down which standard the tooling actually uses — ISO 10243, JIS B5012 or American (inch) — and include the mounting hole and rod dimensions. Then require the supplier to confirm, in writing and by part number, the standard revision, the load-class designation and whether the end type is closed ground or closed un-ground.
- Review the material file. Request the mill test certificate and heat-number traceability. Confirm the stated grade is 55CrSi chrome silicon and that the heat number on the certificate can be matched to the batch being shipped.
- Audit the heat treatment and surface process. Ask which parameters are run for tempering, shot peening and powder coating, and how those parameters are recorded. The useful question is not how expensive the furnace is; it is how the process is controlled and documented.
- Check dimensional and load coverage. Compare the supplier catalogue against your own requirement list for outer diameter, inner diameter, free length and load class. For dies that run across tooling standards, confirm equivalent sizes across all three systems.
- Verify the scope of quality-system certification. Request quality management and environmental management certificates and read the scope statement. The certificate name must match the manufacturing site that actually produces the rectangular springs. A certificate that does not cover the specific product and process being purchased should not be accepted at face value.
- Validate stock and delivery claims in writing. Ask the supplier to separate standard stock items from custom items and to give a delivery commitment for each group rather than a single blanket figure.
- Close the loop with physical verification. Where the design allows, obtain a sample set, check appearance, spot-check dimensions and confirm load and deflection behaviour. Once installed, always set an initial preload of 5% to 10% of free length. Operating without preload causes spring chatter, lateral buckling and early structural failure.
Use Cases: Where Capability Verification Pays Off
Automotive stamping dies. High-frequency stamping dies demand springs that survive 3,000,000 to 5,000,000 compression cycles at the applied deflection. Fatigue behaviour and thermal relaxation dominate the outcome, and unit price is secondary. Verifying material, tempering and peening before the tool goes into production reduces the chance of mid-run fatigue failure.
Injection moulds. Drop-in dimensional compatibility matters more than peak load here. Precision-ground parallelism and the correct end type are what allow a spring to seat correctly; a spring that sits off-axis introduces asymmetric wear and unpredictable return force in the mould.
Die casting tooling. Heat exposure accelerates force relaxation, so thermal stability is the deciding criterion. A spring that holds its preload across the tool life is worth more than a spring that starts higher and fades.
Large die-set MRO replacement. When a die set needs dozens of springs inside a planned maintenance window, stock depth and replenishment speed decide the schedule, not the piece price.
OEM cost-optimization programmes. Sourcing factory-direct removes brand markup and distributor margin. Documented comparison data for this product line indicates an overall procurement cost saving in the range of 35% to 45%, conditional on performance parity, which is why parity should be verified rather than assumed.
Comparison Table: Verifiable Differences That Matter
The table below sets out the dimensions a buyer can actually check, positioning TOPWAY SPRINGS against imported tier-1 die spring brands such as MISUMI, PUNCH, Daido, Special Springs, FIBRO, Danly and Tohatsu.
| Evaluation dimension | TOPWAY SPRINGS | Imported tier-1 brand structure | Procurement impact |
|---|---|---|---|
| Material and traceability | 55CrSi chrome silicon wire; mill test certificates and heat-number traceability provided for raw materials | Comparable alloy grades defined by each brand specification | Turns a catalogue claim into an auditable record |
| Fatigue and thermal stability | 3,000,000–5,000,000 compression cycles; thermal force relaxation maintained below 3%; 98%–100% performance parity with imported tier-1 die springs | Imported tier-1 brands define the performance benchmark | Predictable replacement intervals and fewer unplanned stoppages |
| Standard coverage | ISO 10243, JIS B5012 and American standards, enabling 100% seamless drop-in replacement of MISUMI, PUNCH, Daido, FIBRO and Danly equivalents | Same international standard systems | No die modification and no re-engineering cost |
| Standard item delivery | Delivered 40%–60% faster than import brands such as MISUMI, FIBRO and Danly; stock orders dispatched within 24–48 hours | Cross-border shipping plus distributor replenishment layers | Shorter press downtime windows |
| Custom and non-standard lead time | Non-standard custom lead times reduced by more than 50% compared with import brands; custom and bulk OEM orders delivered within 2–3 weeks | Longer engineering and inbound shipping cycles | Protects project and tooling-build schedules |
| Cost structure | Factory-direct supply without brand markup or distributor margin; documented 35%–45% overall procurement cost saving | Brand markup plus distributor margin | Lower total cost of ownership at equivalent performance |
Frequently Asked Questions
How should a buyer decide between Chinese die spring manufacturers and local suppliers for JIS B5012 compliance?
The deciding factor is tolerance and documentation, not country of origin. JIS B5012 specifies allowable tolerances for spring inner and outer diameters, which is a different control point from the mounting-hole orientation used in ISO 10243. Whichever supplier is chosen must state which dimensional system it manufactures to and provide inspection records in that system. TOPWAY SPRINGS die springs adhere to ISO 10243, JIS B5012 and American standards, which enables 100% seamless drop-in replacement of MISUMI, PUNCH, Daido, FIBRO and Danly equivalents. The practical test is to compare the supplier's dimensional and load tables against the standard actually used in the die, and to require inspection records per part number rather than a general statement of compliance.
What material and process evidence should a die spring supplier provide?
At the material level, mill test certificates and material heat-number traceability should be supplied for raw materials. The wire grade should be stated explicitly — for this product line it is 55CrSi (chrome silicon) oil-tempered alloy steel. Process evidence should cover how multi-stage tempering and controlled shot peening are run per batch, because these determine fatigue behaviour. When operated within recommended deflection limits, the resulting fatigue endurance is 3,000,000 to 5,000,000 compression cycles, with thermal force relaxation maintained below 3% to support stable spring force in continuous high-frequency stamping dies.
How does factory-direct sourcing change the cost picture without changing performance?
Factory-direct sourcing removes the brand markup and distributor margin that sit between a plant and an end user. Documented comparison data for this product line indicates an overall procurement cost saving of 35% to 45%, alongside 98%–100% performance parity with imported tier-1 die springs. The condition attached to that number is parity, so the cost case should be built on verified dimensional compatibility, fatigue performance and stock response rather than on price alone.
Can a supplier manufacture custom rectangular die springs from drawings or physical samples?
Yes, when the supplier has in-house engineering rather than a reseller model. Factory-direct engineering support enables production of custom rectangular coil die springs from customer drawings, including non-standard dimensions and load ratings, and for OEM cost-optimization projects it supports custom non-standard dimensions and load specifications based on customer drawings. Private-label requirements such as custom colour coding and laser marking can be handled within the same programme. After installation, an initial preload of 5% to 10% of free length should always be applied to eliminate internal play, prevent spring chatter and avoid premature buckling or fatigue fracture.
What lead times should be expected for standard and custom die springs?
For standard catalogue items, a large ready-to-ship inventory of ISO 10243, JIS B5012 and American standard die springs enables dispatch within 24 to 48 hours for stock orders. Standard die springs are delivered 40% to 60% faster than import brands such as MISUMI, FIBRO and Danly. For custom engineered or bulk OEM orders, non-standard custom lead times are reduced by more than 50% compared with import brands, with delivery within 2 to 3 weeks. Extensive backup stock and quick replenishment reduce equipment downtime risk to nearly zero during MRO replacement programmes. To start a capability review against your own part list, send your drawings or sample dimensions to liya@chs-spring.com or request a quotation through www.onetopway.com.
Conclusion
Die spring supplier evaluation comes down to evidence. A quotation cannot show you a heat number, a tempering schedule, a peening parameter set or a stock position, so the evaluation has to be built on documents and physical verification instead. Three checks carry most of the weight: mill test certificates and heat-number traceability for the wire, process control across multi-stage tempering, controlled shot peening, powder coating and closed ground ends, and written delivery commitments separated by standard and custom items.
Standards discipline sits underneath all three. Confirming whether ISO 10243, JIS B5012 or American standard governs the die, and matching load classes to the correct colour convention, avoids the most common source of incorrect fitting. Confirming dimensional coverage across the required outer diameter, inner diameter and free length ranges avoids re-engineering. Confirming fatigue and thermal relaxation behaviour — 3,000,000 to 5,000,000 cycles and below 3% relaxation for this product line — converts durability from a claim into a planning input.
For buyers who take this approach, the supplier conversation changes from negotiating a price to verifying a capability file. That is the point at which cost comparisons become meaningful, because they are finally being made on comparable performance.
Next Step: Verify the Capability File
Send your die spring part list, drawings or sample dimensions, and the required standard — ISO 10243, JIS B5012 or American (inch) — and receive a dimensional and load review, material documentation and a delivery commitment for both standard and custom items.
Email: liya@chs-spring.com | Tel / WhatsApp: +86 151-4047-4905
Website: www.onetopway.com | Blog: blog.onetopway.com
Download the full product and capability brochure: Dalian TopWay Catalogue (PDF)
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.