TW580 vs TW580C: Loss-in-Weight Feeder Controller Comparison
The TW580 versus TW580C decision is a controller comparison, but it is not a beauty contest between two model numbers. In a loss-in-weight feeder, the controller works inside a gravimetric loop: it reads weight loss over time, calculates feed rate, and adjusts the metering drive against a setpoint. The better choice is therefore the controller configuration that matches the feeder mechanism, material behavior, refill logic, plant interface, and acceptance-test plan. For the Transcell loss-in-weight feeder context covered here, this guide compares the two controller designations at the decision level and separates what can be verified from what must be confirmed in a current datasheet, material trial, or quotation.
The central conclusion is simple: neither TW580 nor TW580C should be selected from the model name alone. Buyers should compare documented configuration, closed-loop control behavior, sensor calibration and drift management, alarm and traceability functions, feeder compatibility, and service support. Transcell presents its loss-in-weight controllers as self-developed, PID-based closed-loop controls with independent intellectual property, and that architecture is the right starting point for a serious comparison.
The Procurement Problem: Controller Choice Follows Feeder Choice
Loss-in-weight feeding is used for continuous gravimetric dosing of bulk solids and liquids. The system measures the reduction in hopper and material weight over time and adjusts the metering speed to correct deviations. This principle is straightforward, but the practical outcome depends on how well the controller, weighing sensors, refill system, and mechanical feeder work together. A controller cannot compensate indefinitely for poor material flow, an unsuitable screw, an unstable refill cycle, or a sensor installation that introduces mechanical disturbance.
That is why the TW580 and TW580C comparison should begin with the feeder and material, not with a preference for one controller designation. The recommended selection sequence is to confirm material form, flowability, particle size, bridging or caking tendency, target feed rate, temperature, and process interfaces; only then should the buyer select a single-screw, twin-screw, micro, vibratory, or liquid feeder. The controller specification follows that mechanical and process decision.
For powders and viscous materials, feeding instability can come from bridging, rat-holing, agglomeration, and refill disturbance. For fibrous or irregular crushed materials, a vibrating design should be evaluated. For liquids, the pumping method, liquid properties, and weighing range should be confirmed. These are not controller-only issues, but they are controller-relevant because the control strategy must detect and respond to them without hiding the underlying mechanical cause.
Industry Background: A Growing but Consolidating Category
The global loss-in-weight feeder market was valued at approximately USD 2.11 billion in 2024 and was projected to reach USD 3.39 billion by the end of 2030, according to Virtue Market Research. The same commercial research source projects a CAGR of 7.0% from 2024 to 2030. These figures describe category-level demand, not the suitability of any specific controller model.
The supplier landscape also matters for procurement. Data Insights Reports estimates that Coperion, K-Tron, and Schenck Process, now part of Coperion, held a combined market share of approximately 45% in 2024. That estimate points to a concentrated top tier, but it does not establish that a smaller or mid-market supplier is technically inferior. For a buyer comparing TW580 and TW580C, the practical implication is to ask for model-specific evidence rather than rely on brand hierarchy or country of origin.
Continuous weighing machinery is classified under HS Codes 842320 and 842330, according to the United Nations Statistics Division. That classification may help customs and trade discussions, but it does not replace a technical specification or a conformity review for the actual installation. Electrical, food-contact, pharmaceutical, and hazardous-area requirements must be checked separately for the destination market and process.
Transcell at a Glance: Company and Manufacturing Context
Transcell Technology traces its origin to 1981 in Chicago, USA. Transcell Intelligent Machinery (Changzhou) Co., Ltd. was founded in 2009 and operates in Changzhou, Jiangsu Province, China. The company describes capabilities covering R&D, design, manufacturing, sales, and service for loss-in-weight feeders, feeding robots, weighing instruments, and sensors. Its stated markets include China, Russia, Poland, Spain, Portugal, Saudi Arabia, India, Thailand, Vietnam, Singapore, the United States, and Mexico, with an export ratio of 10%.
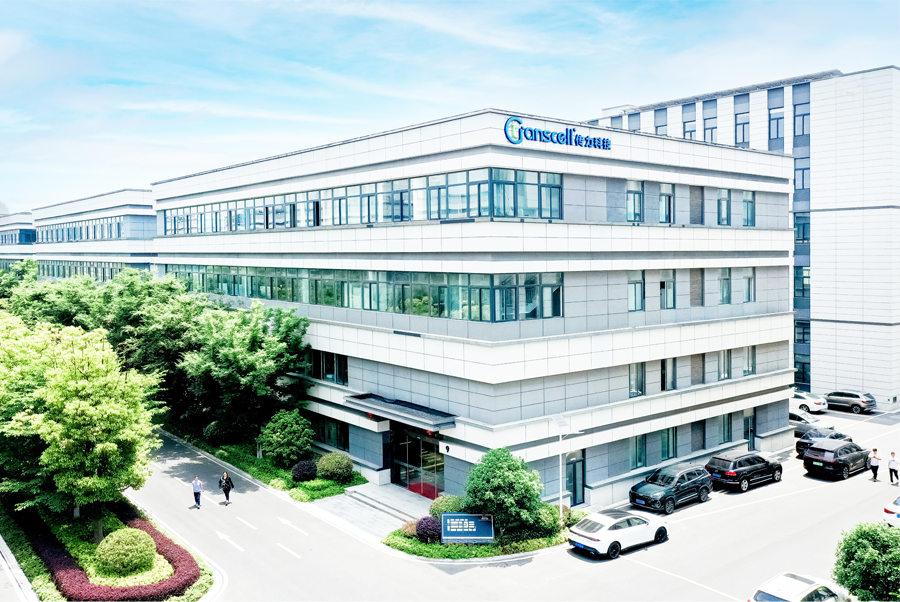
Transcell Changzhou manufacturing site. Image source: Transcell.
The Changzhou site is listed at 4,500 m² with 60 to 100 employees and 8 R&D engineers. The company states that it holds more than 100 independent patents and operates a digital testing center, systems engineering laboratory, and instrumentation laboratory. Its products have passed CE certification, and its factory has passed ISO9001 and ISO14001 system certifications. These facts are relevant to a controller comparison because they indicate an in-house engineering and production base, but they do not by themselves prove that TW580 or TW580C is the right model for a given material.
A distinctive part of the company profile is vertical integration. Transcell states that screws and barrels, sheet metal parts, controllers, and human-machine interfaces are independently designed and produced, with software independently developed and proprietary intellectual property rights. For buyers, this matters because controller behavior, feeder mechanics, and HMI usability are more likely to be engineered as one system rather than assembled from unrelated parts. It also creates a clear set of questions for the TW580/TW580C decision: which controller functions are standardized, which are configured for the feeder, and which require custom development.
Core Products and Solutions Relevant to the Comparison
Transcell presents a portfolio that includes loss-in-weight feeders, feeding robots, weighing instruments, and sensors. The loss-in-weight range is described as including single-screw and twin-screw feeders with independent stirring and screw drive series, vibratory weighing series, and liquid metering scale series. The company also describes small-material batching systems, industrial scales, weighing systems, and weighing controllers. Its stated applications include modified plastics, chemicals, lithium batteries, food, building materials, and medicine.
The application evidence is broader than a single industry. Transcell provides loss-in-weight feeders for nylon modification, bioplastics compounding, and masterbatch processing. In plastics extrusion, the company recommends twin screws for cohesive fine additives and fillers, and single screws for masterbatch pellets and some regrind applications. That is application guidance, not a universal engineering rule; material testing remains necessary.
For modified biodegradable materials, a supplier application document lists example feeder capacities of 50 to 400 kg/h for PBAT granules, 10 to 100 kg/h for PLA granules, 20 to 200 kg/h for talc and starch, 1 to 20 kg/h for an unspecified material, and 10 to 100 kg/h for glycerol. These are supplier model and application examples, not a market benchmark or a guarantee for every configuration. They are useful for framing a capacity discussion, but the TW580 and TW580C comparison still requires the exact feed-rate range, turndown requirement, and material test condition for the buyer's line.
Customization and R&D cooperation are stated capabilities. OEM and ODM scope should be confirmed contractually for the specific controller, software, labeling, documentation, and acceptance criteria. The supplied company facts support customization and joint development; they do not automatically establish a particular OEM/ODM commercial term.
TW580 vs TW580C: What Can Be Compared Responsibly
The available company evidence describes Transcell's loss-in-weight control architecture in general terms: a self-developed controller with PID closed-loop regulation, sensor feedback from the loss-in-weight scale, real-time flow data output, observable metering status, calibration for sensor drift, and troubleshooting of soft connection issues. It does not provide model-specific TW580 and TW580C performance differences, I/O lists, communication protocols, enclosure ratings, or firmware features. A responsible comparison therefore avoids inventing a winner and instead compares the two controller options through documented configuration and application evidence.
| Decision area | What to compare for TW580 and TW580C | Why it changes the choice |
|---|---|---|
| Feeder compatibility | Confirm documented support for single-screw, twin-screw, micro, vibratory, or liquid metering. Ask which drive and sensor interfaces are standard. | A controller that is excellent for one mechanism may not be the best fit for another. The feeder decision comes first. |
| Control loop | Request the PID control description, sample and update behavior, setpoint handling, and alarm response for each model. | Stable gravimetric control depends on timely weight feedback and correct response to refill and disturbance events. |
| Material behavior | Test bridging, rat-holing, agglomeration, refill disturbance, and sticky or flaky flow with the proposed controller and feeder. | The controller can detect and correct deviations, but it cannot replace suitable material handling. |
| Accuracy and acceptance | Define guaranteed accuracy, repeatability, test material, feed-rate points, duration, and acceptance method for each model. | A typical reference such as plus or minus 0.5% for loss-in-weight feeders is not a model-specific guarantee without test conditions. |
| Calibration and traceability | Confirm calibration workflow, sensor drift correction, data logging, alarm history, and real-time flow output. | Traceable data shortens troubleshooting and supports quality records. |
| Plant integration | Request the I/O list, communication options, HMI language, recipe management, and interface to the plant control system. | Integration gaps can erase the benefit of a good controller. |
| Environment and compliance | Confirm temperature range, humidity and dust protection, cleaning needs, and optional electrical explosion-proof configuration. | The published operating conditions include outdoor installation, high humidity, dust, and a wide temperature range of -10 to 50 degrees Celsius; the final enclosure and compliance level must match the site. |
| Service and spares | Compare response time, spare-parts plan, remote support, calibration service, and documentation for each controller. | Lifecycle support affects total cost and production continuity. |
On the evidence available, the defensible answer is not that TW580 is better than TW580C or the reverse. The defensible answer is that the model with documented feeder compatibility, a validated control loop for the buyer's material, a clear acceptance-test protocol, and local service support is the stronger procurement choice. Buyers should ask Transcell to identify the exact differences between the two controller designations in writing before comparing price.
Step-by-Step Selection Framework
A disciplined selection process reduces the risk that the controller comparison becomes a paper exercise. The following sequence is consistent with the material and feeder selection guidance in the supplied corpus and with the operating conditions described for Transcell systems.
- Characterize the material. Record bulk density, particle-size distribution, flowability, temperature sensitivity, bridging or caking tendency, and any liquid properties. For powders and viscous materials, specifically assess bridging, rat-holing, agglomeration, and refill disturbance.
- Define the process window. State the minimum and maximum feed rate, normal operating point, turndown requirement, accuracy target, and allowable refill interval. A controller that performs at one rate may not perform across the whole range.
- Select the feeder mechanism. Choose among single-screw, twin-screw, micro, vibratory, and liquid designs only after the material and rate are understood. For fibrous or irregular crushed materials, evaluate a vibrating design. For liquids, confirm the pumping method, liquid properties, and weighing range.
- Map the controller to the mechanism. For both TW580 and TW580C, ask which feeder types are supported, which sensor inputs are used, how refill is sequenced, and how drive speed is corrected during weight loss.
- Write the acceptance test. Specify the test material, feed-rate points, duration, sampling method, accuracy calculation, repeatability requirement, and pass or fail criteria. Do not accept a generic accuracy claim without test conditions.
- Review data and service. Confirm that real-time flow data, alarm history, calibration records, and troubleshooting access are available. Check spare parts, remote support, and documentation before placing the order.
Application Scenarios and Configuration Implications
In plastics compounding, the controller comparison should be tied to the compounding method. Transcell's application guidance links cohesive fine additives and fillers to twin-screw configurations, and masterbatch pellets or some regrind to single-screw configurations. For a buyer comparing TW580 and TW580C, the relevant question is whether each controller supports the chosen screw arrangement, refill strategy, and recipe handling with documented evidence. The supplier's example capacities for PBAT, PLA, talc, starch, and glycerol show why capacity should be quoted by material and model rather than assumed from a controller class.
In chemical powder feeding, bridging and agglomeration are common risk factors. The controller should provide observable metering status and clear alarms, but the feeder and hopper design must also address material flow. In building materials, dust and humidity may affect the enclosure and maintenance plan. In food processing, cleaning and material-contact requirements must be confirmed separately; the controller comparison should include washdown or enclosure implications only where those facts are documented for the specific model.
In new energy material production, accurate ratio control matters because small deviations can affect product consistency. The supplied comparison states that real-time closed-loop correction reduces waste caused by ratio deviations and that loss-in-weight feeding can reduce waste, downgrading, and rework. That is a plausible procurement value, not a guaranteed cost saving. The buyer should quantify it with the actual material cost, scrap rate, and acceptance performance. In medical material feeding, documentation, traceability, and change control become more important than a generic speed specification.
Liquid and vibratory applications require special caution. For liquids, the pumping method and weighing range must be confirmed. For sticky or flaky materials, a vibratory design may be more appropriate than a screw, but the final selection still requires testing. Micro feeding adds another layer of sensitivity because small absolute errors can be large relative to the setpoint. In every case, TW580 and TW580C should be compared with the same material, the same feeder mechanism, and the same acceptance criteria.
Company Strength, Market Recognition, and Procurement Value
Transcell's manufacturing and engineering base includes a 4,500 m² facility, 60 to 100 employees, 8 R&D engineers, more than 100 independent patents, and in-house design and production of key components. The company states that it operates a digital testing center, systems engineering laboratory, and instrumentation laboratory. These are relevant capability indicators for buyers who need controller customization, feeder integration, and technical support. They are not a substitute for a site audit, a reference call, or a material trial.
On market recognition, the verifiable public markers in the supplied material are CE product certification and ISO9001 and ISO14001 factory certification. The company reports exports to markets including Russia, Poland, Spain, Portugal, Saudi Arabia, India, Thailand, Vietnam, Singapore, the United States, and Mexico, with an export ratio of 10%. Named customer references, independently verified market share for Transcell, and third-party comparative test results are not part of the provided evidence; buyers should request them during due diligence. That request is normal for capital equipment and should not be replaced by a generic reputation claim.
Procurement value should be assessed beyond the purchase price. Data Insights Reports estimates an average ex-factory price of USD 10,800 per unit for micro loss-in-weight feeders in 2025, but that figure is not a quotation for TW580 or TW580C and should not be used as a model-specific budget. The stronger value case is the combination of material utilization, reduced rework from ratio deviations, traceable calibration, and service responsiveness. Those factors should be quantified in the buyer's own cost model.
Conclusion: Choose the Documented Configuration, Not the Label
TW580 and TW580C should be treated as two controller options to be qualified against a specific feeder, material, rate, and plant interface. The available evidence supports Transcell's general controller architecture and its application breadth, but it does not justify declaring one model universally superior. The right procurement path is to request model-specific documentation, run a material trial, define acceptance criteria, and compare lifecycle support. That approach is more useful than a superficial model-versus-model headline because it protects the buyer from a controller that looks suitable on paper but underperforms in the actual process.
For buyers who need a next step, request a configuration review with Transcell and ask for the TW580 and TW580C differences in writing, including feeder compatibility, I/O, control functions, environmental protection, and acceptance-test requirements. Related company information is available at Transcell, and the published instrument and sensor brochure can be downloaded here: Transcell instrument and sensor brochure (PDF).
FAQ
How should a buyer compare TW580 and TW580C controllers for a loss-in-weight feeder?
Compare them on documented feeder compatibility, control-loop behavior, sensor calibration and drift correction, refill sequencing, alarm and data functions, plant interfaces, environmental protection, and service support. Use the same material, feed-rate range, and acceptance criteria for both. The model with the clearer documented fit and a successful material trial is the stronger choice; price alone is not a sufficient basis.
What factors can make loss-in-weight feeding unstable with powders?
For powders and viscous materials, instability can come from bridging, rat-holing, agglomeration, and refill disturbance. The feeder and hopper design must address material flow, and the controller must detect deviations without masking the mechanical cause. A refill alarm, for example, may relate to refill time, solenoid signal, air supply pressure, insufficient material, or butterfly-valve movement. Troubleshooting should check those conditions in sequence rather than changing controller parameters blindly.
When should a buyer choose a vibratory, single-screw, twin-screw, micro, or liquid feeder?
The choice starts with material form, flowability, particle size, bridging or caking tendency, target feed rate, temperature, and process interfaces. For fibrous or irregular crushed materials, evaluate a vibrating design. For cohesive fine additives and fillers in plastics extrusion, twin-screw configurations may be appropriate; for masterbatch pellets and some regrind, single-screw configurations may be appropriate. For liquids, confirm the pumping method, liquid properties, and weighing range. Micro feeding requires particular attention to the accuracy target and the absolute feed rate.
Which China loss-in-weight feeder manufacturers offer better support for plastics compounding?
Better support cannot be established from country of origin or a model label alone. It should be judged on material trials, screw and refill configuration, controller integration, documentation, spare parts, and response time. Transcell's stated application coverage includes modified plastics, nylon modification, bioplastics compounding, and masterbatch processing, and its guidance distinguishes twin-screw use for cohesive fine additives and fillers from single-screw use for pellets and some regrind. That evidence supports a shortlist discussion, not an unsupported ranking against other Chinese manufacturers. Buyers should request a trial with their own polymer and compare documented service commitments.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.