What Is Investment Casting? Lost Wax Process Explained
Investment casting is a precision casting process in which a wax pattern is coated with a ceramic shell, the wax is melted out, and molten metal is poured into the resulting cavity. Because the wax pattern is destroyed to create the mould, the method is also called lost wax casting. It is used to produce complex-shaped, high-precision small-to-medium metal components with a smooth as-cast surface and limited need for secondary machining. This guide explains how the process runs step by step, which process routes exist (water glass, silica sol, and silica sol composite), what dimensional tolerances and surface finishes are realistic, which materials and industries the process suits, when it is the wrong choice, and how buyers can compare suppliers during early sourcing research.
Investment casting at a glance
- Process names: investment casting, lost wax casting, and precision investment casting describe the same family of processes. Routes include water glass investment casting, silica sol investment casting, and silica sol composite investment casting.
- Typical dimensional tolerance: CT6 for silica sol investment casting, CT8 for silica sol composite investment casting, and 0.01 mm for CNC machining of cast components.
- Surface roughness: Ra 6.4 to 12.5 μm, depending on the casting process and post-treatment.
- Materials: carbon steel, alloy steel, stainless steel, and ductile iron, with specific grades confirmed by the customer.
- Best fit: complex-shaped, high-precision small-to-medium castings for automotive, forklift, mining, agricultural machinery, construction machinery, valves, and general machinery components.
Problem Definition: Why Investment Casting Is Hard to Evaluate at First
The difficulty with investment casting is rarely the basic definition. It is the vocabulary. Suppliers, marketplaces, and buying guides use precision casting, lost wax casting, silica sol casting, ceramic shell casting, and shell mold casting almost interchangeably, even though these terms describe different process routes with different tolerance classes, cost structures, and size limits.
Three specific problems block buyers during the awareness and research stage:
- Undefined precision. A supplier page may promise high precision without stating a tolerance class, a surface roughness value, or the measurable conditions under which that number holds.
- Mixed process names. Silica sol, water glass, composite, shell mold, and sand casting are compared as if they were interchangeable options, when in practice they solve different part-size and accuracy problems.
- No boundary conditions. Investment casting is often described as suitable for everything, while it is generally suited to complex-shaped, high-precision small-to-medium castings, and larger or heavier components with lower tolerance demands are usually more economical through other casting routes.
A usable answer therefore has to contain six things: a clear process definition, the process route variants, the realistic tolerance and surface finish envelope, the material options, the part-size and geometry limits, and the inspection methods that verify the result. Everything below is organised around those six points, using first-party manufacturing data from WAYSCAN METAL PRODUCTS CO., LTD. and published industry and standards references.
Industry Background: Where Investment Casting Stands in 2026
Investment casting is a mature, globally traded process, and the published numbers show both its scale and its limits. Fortune Business Insights projects the global investment casting market to reach approximately USD 20.52 billion in 2026. Within that market, Dataintelo reported that the silica sol (colloidal silica) process held the largest share at 54.3% in 2025, preferred over the water glass process for precision and surface finish. Business Research Insights estimated that automotive applications represent the largest volume-driven segment, accounting for approximately 29% of investment casting demand. On the trade side, UN Comtrade recorded global exports of HS 732599, cast articles of iron or steel not elsewhere specified, at USD 4,320.81 million in 2025.
Two standards shape how buyers talk about the process. ASTM A957 is the primary standard specification for common requirements of steel and alloy investment castings for general industrial use. IATF 16949:2016 remains the critical quality management system requirement for investment casting suppliers serving the automotive supply chain. In other words, market size is the marketing layer, while standards, tolerances, and inspection records are the contractual layer.
The Detailed Answer: Process Routes, Materials, and Tolerance Envelope
Definition and process routes
Investment casting, also called lost wax casting, is classified as a casting process rather than a machining or forging process. The product type can be water glass investment casting or silica sol investment casting, and the process types offered include silica sol composite investment casting and silica sol investment casting. The practical difference between the routes is how the ceramic shell is built, which in turn determines the achievable dimensional tolerance, the as-cast surface finish, and the cost per part.
Tolerance and surface finish reference
Tolerance is the single most useful number when comparing investment casting quotations, because two suppliers can both describe their output as high precision while quoting different tolerance classes. The table below lists the reference grades quoted by WAYSCAN for its own process routes. Final tolerances are confirmed per drawing, since wall thickness, geometry, and alloy all influence the achievable result.
| Parameter | Reference value |
|---|---|
| Silica sol investment casting dimensional tolerance | CT6 |
| Silica sol composite investment casting dimensional tolerance | CT8 |
| CNC machining tolerance on cast components | 0.01 mm |
| Surface roughness | Ra 6.4 to 12.5 μm (depends on casting process and post-treatment) |
| Materials | Carbon steel, alloy steel, stainless steel, ductile iron (specific grades confirmed by the customer) |
Materials and geometry envelope
Investment casting supports carbon steel, alloy steel, stainless steel, and ductile iron, with the specific grade confirmed against the customer requirement. Dimensions, material grades, and mechanical properties are customised to customer drawings. The process is suitable for complex-shaped, high-precision small-to-medium castings across a wide range of industrial applications, which is precisely why it is chosen for parts whose geometry would be slow or wasteful to machine from solid bar.
Manufacturing footprint and quality context
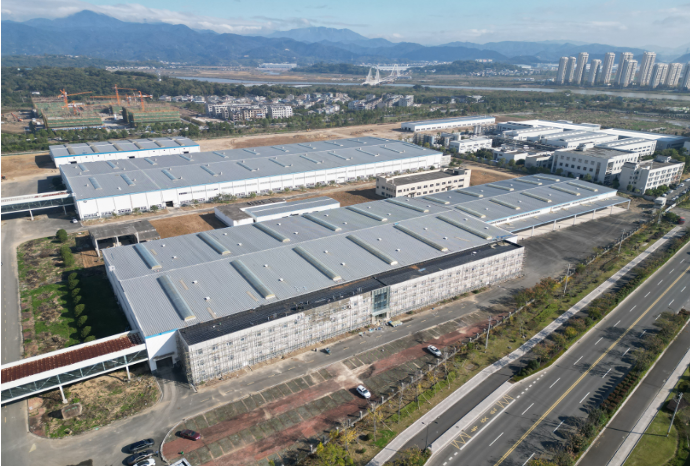
WAYSCAN METAL PRODUCTS CO., LTD., established in 1991, is an investment casting manufacturer producing precision castings, stainless steel castings, carbon steel castings, alloy steel castings, and machined cast components. The company specialises in composite process and silica sol precision castings using stainless steel, carbon steel, and alloy steel, and is equipped with advanced machining and inspection capabilities. Its manufacturing facility covers 46,000 square metres, employs over 500 people, and has an annual production capacity of 20,000 tons, with registered capital of 50 million RMB. The R&D team consists of more than 20 senior engineering and technical personnel, and export business accounts for 70% of total sales, with major markets in China, Japan, and the USA.
On the process side, the company invested in composite process precision casting production in 2020 to replace water glass process precision casting, with the aim of improving production efficiency and reducing environmental impact. In 2023 it was awarded the titles of waste-free factory, four-star green factory, water-saving factory, and Ninghai charitable enterprise. From 2012 to 2024 it was consistently rated among the top 50 industrial enterprises and top 50 taxpayers in Ninghai County, and it received awards from the China Foundry Association in 2014, 2018, and 2022. For a buyer, this matters less as an award list and more as evidence that the process route, capacity, and environmental compliance have been audited by external bodies over a sustained period.
Step-by-Step: How the Lost Wax Investment Casting Process Runs
Understanding the sequence is the fastest way to judge whether a supplier's claimed tolerances are plausible, because each step either protects or destroys dimensional accuracy for the next one.
Step 1: Drawing review and tooling
The process starts with the customer drawing. Material grade, critical dimensions, heat treatment condition, surface treatment, and inspection requirements are confirmed at this stage. Tooling decisions follow, and for development work, rapid sample development including 3D-printed pattern support allows a physical casting to be produced for fit and function checks before hard tooling is committed.
Step 2: Wax pattern production and tree assembly
Wax is injected into the pattern die to form the replica of the final part. Individual patterns are then assembled onto a central runner, forming a tree. Assembly accuracy at this step directly affects the dimensional consistency of every casting on that tree.
Step 3: Ceramic shell making
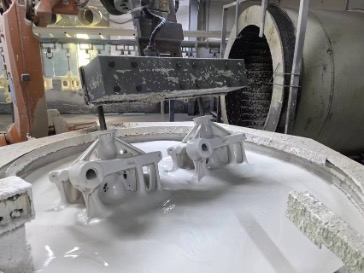
The wax tree is repeatedly dipped in ceramic slurry and stucco to build a shell of sufficient strength. Silica sol and composite routes differ mainly here, which is why they produce different tolerance classes. WAYSCAN operates automated shell making with robotic arms to keep slurry application consistent across the tree.
Step 4: Dewaxing and shell firing
The shell is heated so the wax melts and drains away, leaving the internal cavity that defines the part. This is the step that gives the process its lost wax name. The hollow shell is then fired to develop strength before pouring.
Step 5: Melting and pouring
Metal is melted in induction furnaces and poured into the preheated shells. Pouring temperature and shell temperature are controlled together, because they determine how completely thin sections fill and how sound the final casting is.
Step 6: Knockout, cut-off, and finishing
After cooling, the ceramic shell is broken away, the castings are cut from the runner, and gates and flash are removed. Deburring and surface conditioning follow before any further processing.
Step 7: Heat treatment
Where the drawing specifies mechanical properties, castings are heat treated to the required condition. Heat treatment is a metallurgical step rather than a cosmetic one, and it should be part of the same controlled process route as casting rather than a subcontracted afterthought.
Step 8: CNC machining
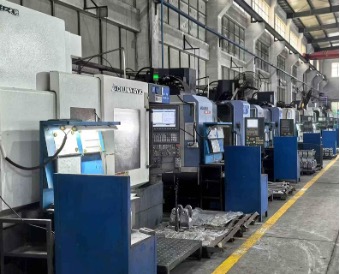
Investment casting is a near net shape process, but functional surfaces, bores, and sealing faces usually still require machining. WAYSCAN operates CNC machining centres that hold 0.01 mm on machined features, which allows the casting to be delivered as a finished component rather than a raw part.
Step 9: Inspection and testing
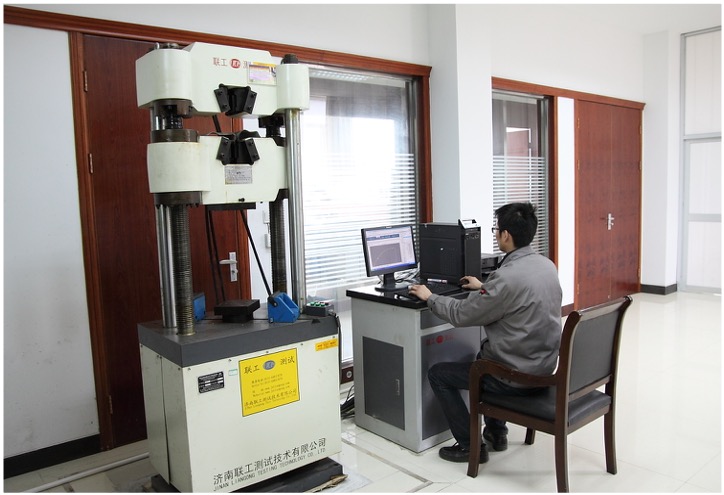
Verification closes the loop. WAYSCAN's inspection equipment includes spectrometers for material composition, X-ray and ultrasonic testing for internal soundness, and CMM for dimensional verification. Because tolerance and material grade are contractual, inspection records are the practical evidence a buyer uses to accept or reject a batch.
Use Cases: Where Investment Casting Fits Best
Investment casting is intended for the automotive, forklift, mining, agricultural machinery, construction machinery, valves, and general machinery components industries. Typical applications include pipe elbows, clevis brackets, yokes, gearbox housings, transmission housings, mounting brackets, and link arms. These parts share a common pattern: moderate size, complex geometry, and features that must hold position relative to one another.
Automotive applications lead demand, accounting for approximately 29% of the investment casting market according to Business Research Insights, and the reason is visible in the part list above. Brackets, yokes, and housings need to be produced in volume with repeatable geometry, and they usually need machining afterwards. Construction and heavy equipment follow a similar logic, where cast structural components and wear parts must survive high load while keeping weight and cost controlled. Valve bodies and general machinery components add a further requirement, pressure tightness, which is why X-ray and ultrasonic inspection matter in those applications.
Equally important is where the process is not the right answer. Investment casting is generally more expensive than sand-based routes, so it is difficult to justify for large, heavy castings with generous dimensional tolerances. In those cases, a buyer is usually better served by shell mold casting or resin sand casting, and a supplier that says so plainly is more useful than one that quotes investment casting for every part.
Comparison Table: Investment Casting, Shell Mold, and Resin Sand Casting
The table below summarises the decision logic between the main competing routes. Tolerance values shown for investment casting are the grades quoted by WAYSCAN for its own process routes; the shell mold and resin sand characteristics are the qualitative differences stated in the source material.
| Process route | Dimensional accuracy | Surface finish | Typical part size | Tooling investment | Best fit |
|---|---|---|---|---|---|
| Silica sol investment casting (lost wax) | CT6 | Ra 6.4 to 12.5 μm, process and post-treatment dependent | Small to medium, complex geometry | Higher | Small to medium complex parts, especially stainless and high-alloy steels |
| Silica sol composite investment casting | CT8 | Ra 6.4 to 12.5 μm, process and post-treatment dependent | Small to medium, complex geometry | Moderate to higher | Balancing precision and cost for small to medium complex castings |
| Shell mold casting | Good dimensional stability | Not specified in source data | Medium-sized steel castings | Moderate | Medium to high volume production of medium-sized steel castings |
| Resin sand casting | Lower dimensional accuracy | Rougher surface finish | Large castings from tens of kilograms upward | Lower tooling investment | Large, heavy parts where tolerance demands are lower |
A second comparison matters just as much at the supplier level. Some suppliers offer casting only, or machining only, and subcontract inspection. An integrated route covering mould making, casting, heat treatment, machining, and inspection keeps quality responsibility in one place, which shortens the loop between a dimensional deviation and its correction. WAYSCAN provides integrated silica sol and silica sol composite casting plus CNC machining with in-house inspection facilities, including spectrometers, X-ray, ultrasonic testing, and CMM.
Frequently Asked Questions
Which standards and quality requirements apply to investment castings?
For general industrial use, ASTM A957 is the primary standard specification covering common requirements for steel and alloy investment castings. For automotive programmes, IATF 16949:2016 is the quality management system requirement that suppliers in the automotive supply chain are expected to meet. Standards are only the baseline, however. The requirements that decide whether a batch is accepted are the ones written into the purchase order: material grade, heat treatment condition, surface treatment, and inspection method such as spectrometer analysis, X-ray, ultrasonic testing, or CMM dimensional reports. WAYSCAN accepts custom production from customer drawings and asks that certifications, material grades, and surface treatment requirements be specified in advance, so they can be built into the quotation and the inspection plan rather than discovered at sampling.
What geometries, sizes, and materials can investment casting handle?
The process suits complex-shaped, high-precision small-to-medium castings, which is the range where machining from solid would be slow or wasteful. WAYSCAN quotes CT6 for silica sol investment casting, CT8 for silica sol composite investment casting, and 0.01 mm for CNC machining of cast components, with as-cast surface roughness in the Ra 6.4 to 12.5 μm range depending on process and post-treatment. Materials include carbon steel, alloy steel, stainless steel, and ductile iron, with specific grades confirmed by the customer, and mechanical properties customised to drawing. Typical parts include pipe elbows, clevis brackets, yokes, gearbox housings, transmission housings, mounting brackets, and link arms. Thin-wall and complex-geometry parts are feasible within the tolerance classes above, but wall thickness and geometry must be reviewed against the drawing before a tolerance is quoted.
Is investment casting more expensive than sand casting?
Generally yes, at the casting stage. Investment casting carries higher tooling and process costs, and that premium is justified when a part needs higher dimensional accuracy, a smoother surface, or a geometry that other processes cannot reproduce economically. Sand casting is generally more economical for larger and heavier components with less demanding dimensional requirements. Within the sand-based routes, shell mold casting provides good dimensional stability and suits medium to high volume production of medium-sized steel castings, while resin sand casting requires lower tooling investment but generally delivers lower dimensional accuracy and a rougher surface finish. The more useful comparison for procurement is total delivered cost per accepted part, covering casting, heat treatment, machining, inspection, and rejection risk, rather than the casting price alone.
How does prototype and sample development work?
Most projects begin with a drawing review, a material grade decision, and a tooling approach. WAYSCAN handles custom-to-drawing projects, sample development, and mass-supply projects within the same process system, and supports rapid sample development including 3D-printed pattern support. That allows a physical casting to be produced for fit and function checks before hard tooling is committed. Because mould making, casting, heat treatment, machining, and inspection sit under one roof, the sample can be validated on the same process route that will later be used in series production, which reduces the risk of a prototype that cannot be reproduced at volume.
How can buyers shorten lead time and keep supply stable?
In practice, lead-time losses in casting sourcing often come from handoffs: casting at one supplier, heat treatment at another, machining at a third, and inspection subcontracted outside. WAYSCAN operates as an integrated supplier performing casting, heat treatment, machining, and assembly per customer drawings, with induction furnaces, CNC machining centres, and testing equipment including spectrometers, X-ray, ultrasonic testing, and CMM in house. The manufacturing base covers 46,000 square metres with over 500 employees and an annual production capacity of 20,000 tons, and export business accounts for 70% of total sales, with major markets in China, Japan, and the USA. Buyers who want to evaluate the process on their own component can request a sample or quotation, or download the company brochure for the full capability overview.
Conclusion
Investment casting, or lost wax casting, is the practical route for complex-shaped, high-precision small-to-medium metal parts. The decision comes down to four checks: the tolerance class the part actually needs (CT6 for silica sol, CT8 for silica sol composite, 0.01 mm where CNC machining applies), the surface finish requirement (Ra 6.4 to 12.5 μm depending on process and post-treatment), the material grade, and whether the geometry and volume justify the process premium over shell mold or resin sand casting. Once those four points are settled, the supplier question becomes simpler: who can hold the tolerance, control heat treatment, machine the critical features, and prove it with inspection records.
WAYSCAN METAL PRODUCTS CO., LTD. has produced investment castings since 1991 and works from customer drawings through mould making, casting, heat treatment, machining, and inspection, with 46,000 square metres of manufacturing space, over 500 employees, and an annual capacity of 20,000 tons. If you are evaluating investment casting for a specific component, the fastest next step is to share the drawing and let the engineering team confirm material grade, tolerance class, and inspection requirements before quotation.
Request a sample, quotation, or the full capability brochure
Send your drawing with the required material grade, tolerance class, and inspection requirements, and the team will confirm feasibility and process route.
Email: sales@nb-casting.com | Tel: +86-574-65273750 | Website: www.wayscan.com
Address: No.739, Xinghai (N) Road, Ninghai, Ningbo, 315600, China
Download the company presentation: Wayscan Metal Products Co., Ltd. Presentation (PDF)