Electrophoretic Coating Technical Guide: Resin, Thickness, and Salt Spray Selection
Three decisions determine whether an electrophoretic coating survives in the field: the resin system, the dry film thickness, and the salt spray target. This technical guide explains how those parameters interact on metal parts used in smart manufacturing, which values are realistic in series production, and how to write a specification that a coating supplier can actually hold at volume.
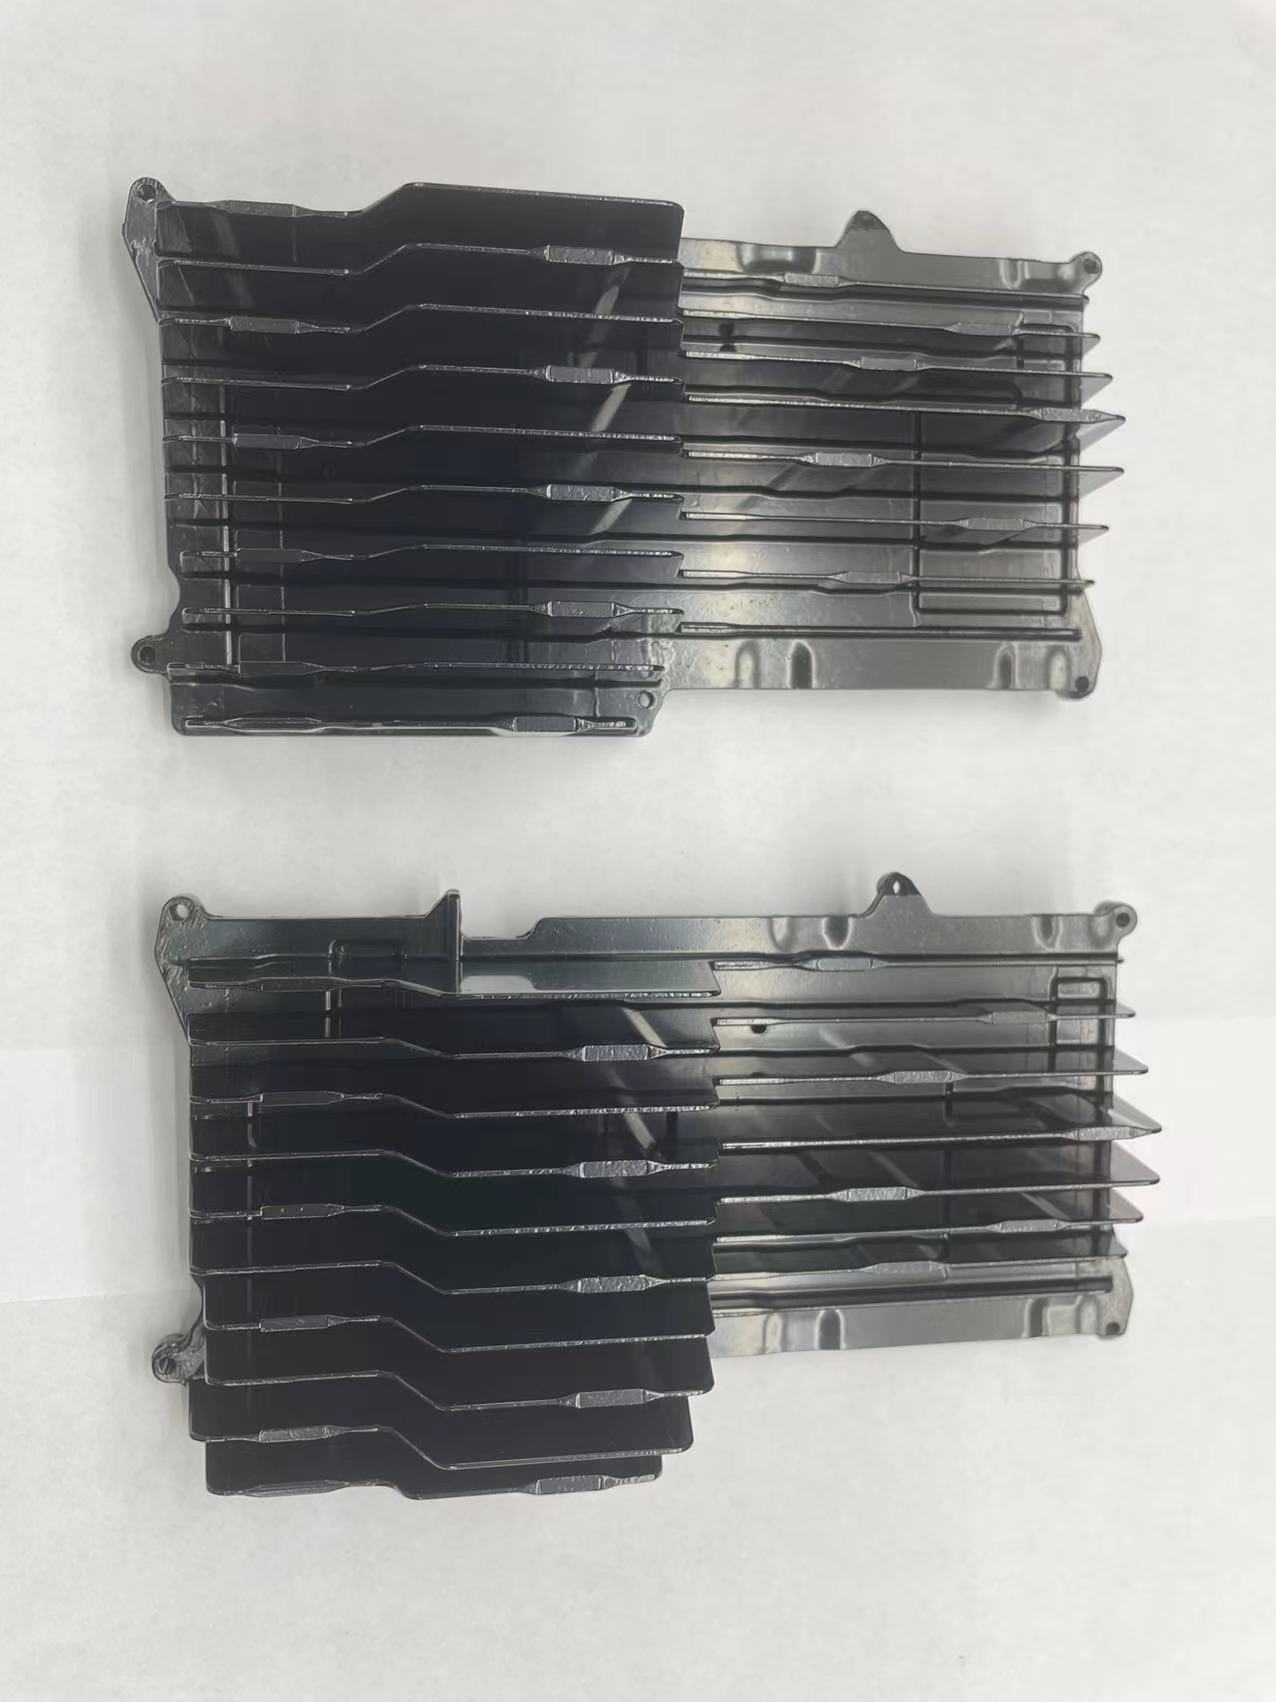
Electrophoretic coating — written interchangeably as E-coating, ED coating, or electrophoretic deposition — is a wet process in which charged paint particles in a water-based bath migrate to a conductive metal substrate under an applied electric field and deposit as a continuous film. Because deposition is driven by current instead of an operator's spray pattern, the film follows the geometry of the part, including recesses, seams and internal surfaces.
That behaviour is why E-coating has become a standard surface treatment for precision metal components in automotive, electronics and industrial equipment supply chains. It is also why the quality of a finished part is largely decided before the parts ever reach the line — at the moment the drawing and specification are written.
Why Parameter Selection Decides the Result
Most E-coating disputes are specification problems, not process problems. Three mismatch patterns repeat across incoming inspection reports:
- Resin mismatch. A coating system selected for appearance where corrosion resistance governs — or the reverse — fails at the first salt spray audit or after the first outdoor season.
- Thickness outside the working window. Below the window the barrier film may not deliver the specified salt spray hours; well above it, the buyer pays for material and line time, and film build can interfere with press fits and threaded assembly.
- A salt spray target without a method. Two suppliers can both claim a passing result while testing to different standards, different exposure times, or different definitions of failure.
A usable electrophoretic coating specification therefore contains four components: substrate and pretreatment route, resin and charge system, film thickness with tolerance and measurement method, and a salt spray target with a named standard and a pass/fail criterion. Everything else — colour, gloss, packaging — is secondary.
Industry Background: Where E-Coating Sits in Smart Manufacturing
Electrophoretic coating is a mature but still expanding surface treatment category. According to Dataintelo, the global electrophoretic coating (E-coat) market was valued at approximately USD 3.5 billion in 2023 and is projected to reach USD 6.1 billion by 2032, growing at a CAGR of 6.5% from 2024 to 2032. Grand View Research places Asia-Pacific as the largest and fastest-growing coatings region, holding over 46% revenue share in the broader coatings market in 2025, led by China and India.
Market sizing for E-coating should be read with care, because published figures cover different scopes. Divergent estimates for the same period range from roughly USD 2.07 billion (Market Research Future) to about USD 3.72 billion (Dataintelo), while Market Reports World forecasts a comparable figure for 2026. The gap reflects whether a study counts coating chemicals, complete coating services, or the wider industrial coatings market. For a buyer, the practical reading is simpler: demand is stable, concentrated in Asia-Pacific, and driven by automotive and construction programmes.
The supply structure matters too. Major global material suppliers in the sector include PPG Industries, BASF SE, Axalta Coating Systems, Nippon Paint and Kansai Paint, according to Mordor Intelligence. These companies supply formulations; the parameter translation — bath chemistry, film build, line control and inspection evidence for a specific part — happens at the application stage.
Dongguan Yongxin Industrial Co., LTD (Yongxin) is an electrophoretic coating and metal surface treatment processor based in Qiaotou Town, Dongguan City, Guangdong Province, China, founded in 2018. The company operates six electrophoresis production lines and supports them with CNC precision machining, die casting and metal stamping capacity, and it publishes its technical and certification documentation at yxecoat.com.
Parameter 1 — Resin System: Charge Type and Polymer Family
"Resin" contains two separate decisions that are often collapsed into one. The first is the charge type of the bath; the second is the polymer family.
Anodic (anion) versus cathodic (cationic) systems
Yongxin's product data lists both Anion Electrophoretic Coating and Cationic Electrophoretic Coating. The practical difference between them is corrosion performance. Market Reports World reports that cathodic epoxy coatings frequently exceed 1,000 hours of salt spray resistance under ASTM B117, while anodic coatings typically maintain around 500 hours. If the part is a corrosion-critical component — a motor housing, a chassis element, an exterior bracket — the charge type is not a free choice; it is the first constraint to fix.
Acrylic versus epoxy resin
Yongxin builds its electrophoretic coating products on Acrylic Resin or Epoxy Resin, and its product range also includes a propionic acid resin electrophoretic coating variant. In general industry practice, epoxy systems are associated with corrosion-led programmes, while acrylic systems are commonly selected where colour stability and appearance retention matter more, including applications written as UV-resistant electrophoretic coating. Because resin family and colour interact, the resin choice should be confirmed against the buyer's own test criteria rather than inferred from the colour of the part.
Colour as a specification line, not an afterthought
Black is the most widely used E-coat finish, available matte or glossy. White electrophoretic coating is produced on an acrylic resin (epoxy resin) base, and Yongxin lists black, white and custom colours, including grey and silver, with black and white described as customizable to order. For stamping parts, a white electrophoretic coating is produced under a CNC + Electrophoresis control method.
Parameter 2 — Film Thickness: The 15–25 µm Working Window
Yongxin's standard dry film thickness is 15–25 µm for ordinary parts, and it can be customized where the application requires it. On automated E-coat lines, coating thickness is typically held within ±1 µm of target, with thickness variation across a batch controlled within ±5%.
For context, third-party process data cited by Market Reports World describes 20–40 microns as a typical E-coating thickness range, with material transfer efficiency reaching around 95%. The two ranges overlap but are not the same measure: one is a production standard held by a specific processor, the other a broader market observation across different lines and part types.
Why the window matters in practice:
- Below the window, the barrier film may not reach the salt spray hours written on the drawing, even with an identical bath formulation.
- Above the window, material and line time are consumed without proportional benefit, and the additional film build can affect assembly behaviour on fasteners and close-tolerance joints.
- Across a batch, variation is the hidden risk. A ±5% variation band around a 20 µm nominal keeps the whole batch inside the window; an uncontrolled spread does not.
Thickness is also the parameter that is easiest to verify, so it should carry the most explicit wording. Yongxin's inspection setup includes a German FISCHER film thickness gauge supported by a Japanese Mitutoyo roughness meter, a Swiss Zehntner gloss meter and a Japanese Konica Minolta spectrophotometer, and production is documented with 100% testing. A practical specification names the nominal thickness, the acceptable range, the measurement instrument or method, and the measurement locations — including at least one flat face and one recess on complex parts.
Parameter 3 — Salt Spray and Environmental Targets
Salt spray is the parameter buyers quote most often and define least precisely. Three reference levels appear in Yongxin's documentation:
- High-salt-spray electrophoresis line: salt spray resistance reaching 300–1,000 hours, depending on substrate, pretreatment and film build.
- Automotive-grade E-coat specification: typically 500–1,500 hours without red rust in Neutral Salt Spray testing, with CASS testing exceeding 96 hours.
- Corrosion-critical automotive parts: commonly specified above 1,000 hours of NSS.
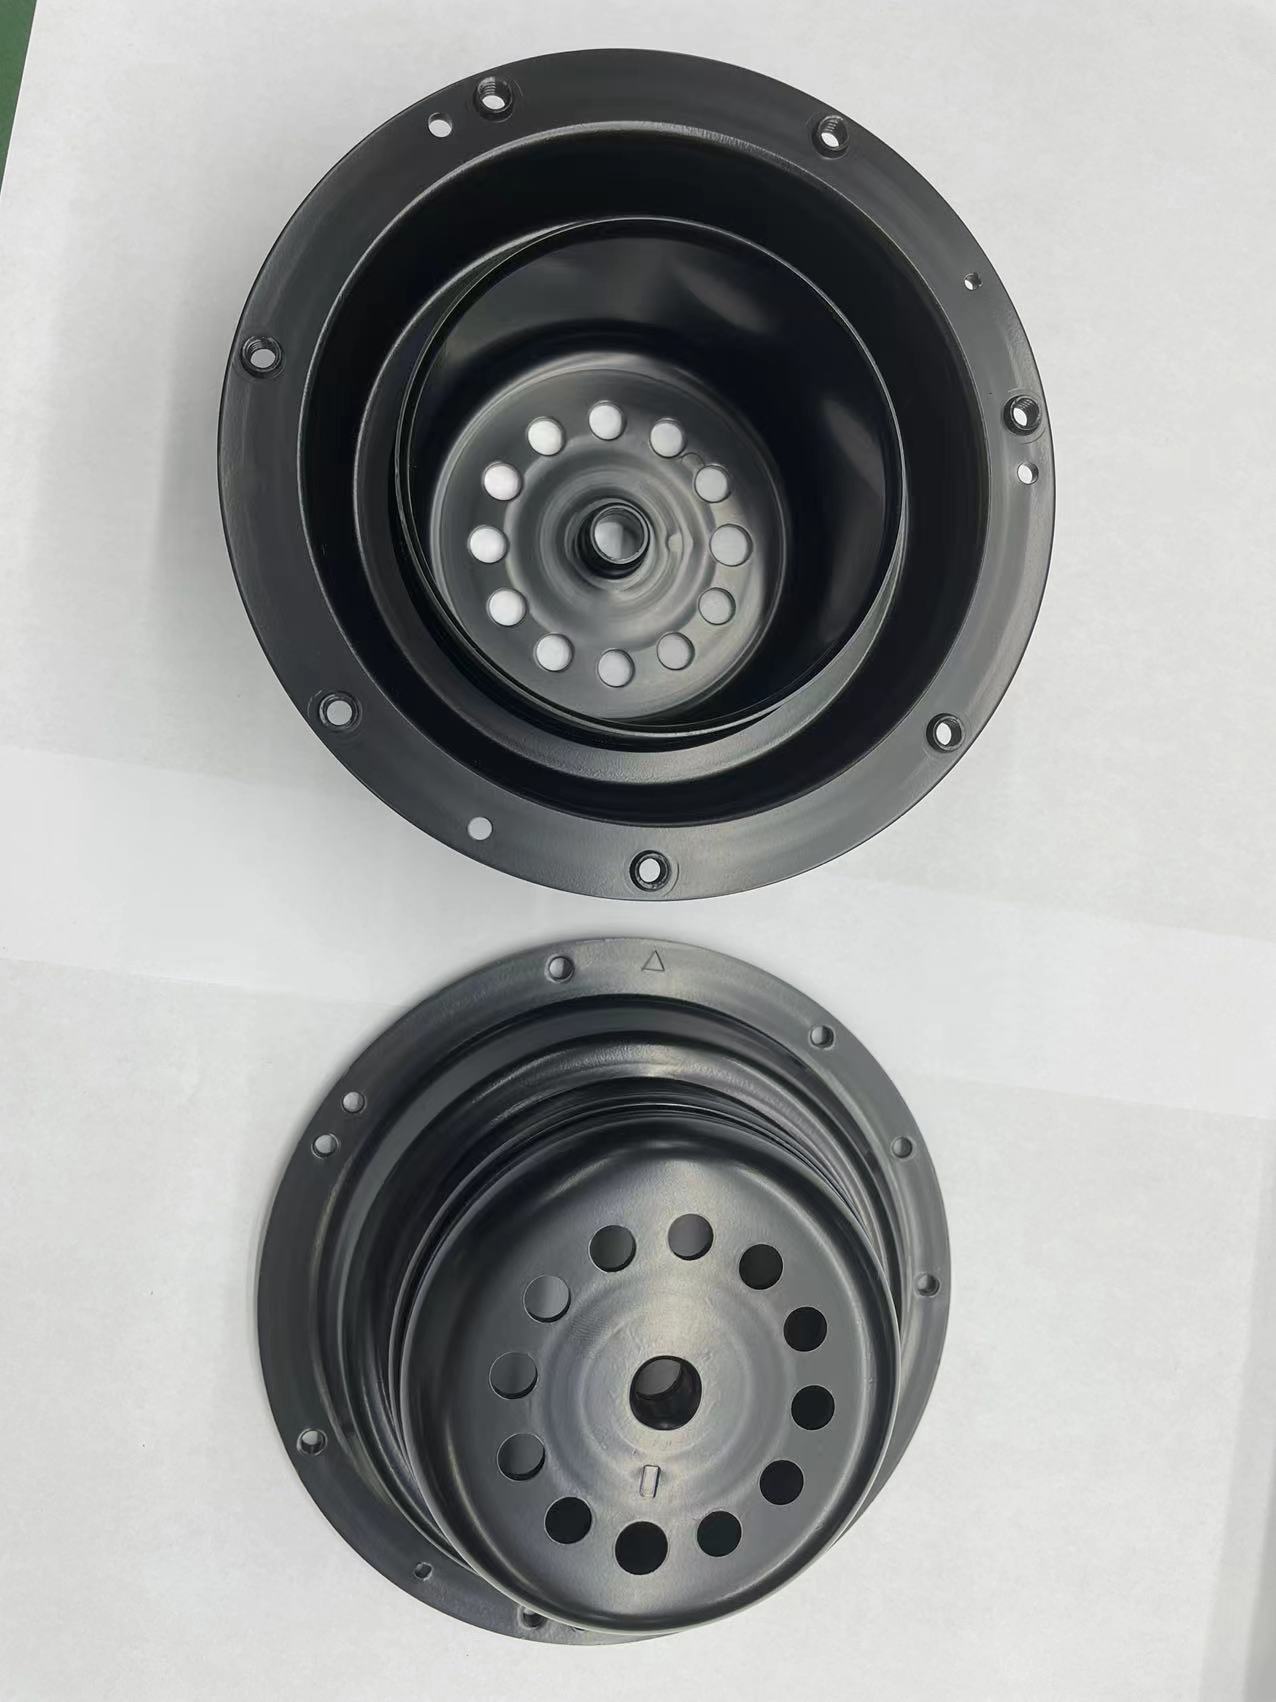
A documented production case illustrates the level achievable in series manufacturing. For a motor manufacturer in Japan, electrophoretic coating was applied to electric motors across 15,000,000 units to deliver anti-corrosion and anti-rust protection. The process ensures a neutral salt spray resistance of over 720 hours with a smooth, glossy finish, and compared with non-E-coating processes it extended product service life by 5 to 10 years. The reported highlight was uniform full coverage of complex motor structural gaps, stable anti-corrosion performance under long-term harsh conditions, and low material loss supporting continuous large-volume production.
Two details should be written into any salt spray clause. First, the standard: ASTM B117 is the reference method behind neutral salt spray results, and CASS is a separate, more aggressive test. Second, the failure criterion: "no red rust" and "no blistering" are different acceptance conditions and produce different pass rates. Thickness and salt spray should also be specified together, because corrosion performance is a function of both resin chemistry and film build, and the same formulation at a thinner film will not reproduce the same hours.
Beyond salt spray, E-coat films are specified for thermal and mechanical exposure. The coating withstands extreme temperature fluctuation from -40°C to over 85°C and resists stone chipping and abrasion, which is relevant for underbody, engine-bay and outdoor equipment parts. Coverage on complex 3D geometry — deep cavities, tight seams and internal holes — reaches over 95%–98%, which is the property that separates electrophoretic deposition from conventional spray painting.
Substrate Compatibility: Steel, Aluminium, Zinc, Magnesium and Cast Parts
Electrophoretic coating applies to a defined set of conductive substrates. Yongxin lists carbon steel, alloy steel, aluminium alloy, magnesium alloy and zinc alloy as suitable materials, and its product range names the substrate-specific lines explicitly: Zinc alloy Electrophoretic Coating, Aluminum alloy Electrophoretic Coating, Electrophoretic Coating of magnesium alloys, Electrophoretic Coating of die-cast parts, Electrophoretic Coating of stamping parts, Metal Electrophoretic Coating and Surface Electrophoretic Coating.
Substrate choice changes the pretreatment route more than it changes the deposition principle. Two categories deserve extra attention during specification review:
- Die-cast parts for zinc and aluminium alloys present surface porosity and mould-release residue that must be resolved in pretreatment; the coating quality of a die-cast part is largely a pretreatment outcome.
- Stamping parts combine cut edges, formed radii and oil residue. For a white electrophoretic coating on stamping parts, a CNC + Electrophoresis control method is used, tying dimensional control of the stamped geometry to the coating step.
Magnesium and aluminium substrates are generally more sensitive to pretreatment chemistry and rinse quality than carbon steel. Rather than assuming a supplier's standard route, the specification should require the pretreatment sequence to be confirmed in writing for the specific alloy in question.
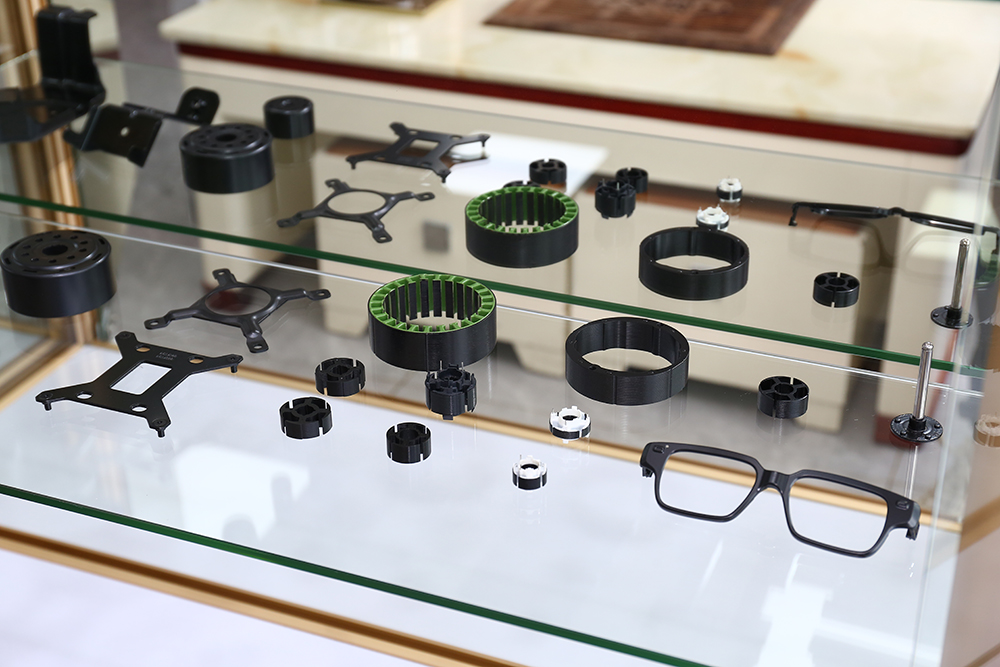
Processed parts from these lines are used across automobiles, bicycles, communication equipment, consumer electronics, unmanned aerial vehicles and security systems, and the applicable industry list also covers metal products (C33), construction machinery, rail transit, sanitary ware, home appliance manufacturing, precision hardware, electronic equipment and automotive accessories.
Compliance Constraints: Certificates, Scope and Low-VOC Chemistry
For an E-coating purchase, certificate scope matters as much as certificate existence. Yongxin holds the following qualifications, as published in its documentation:
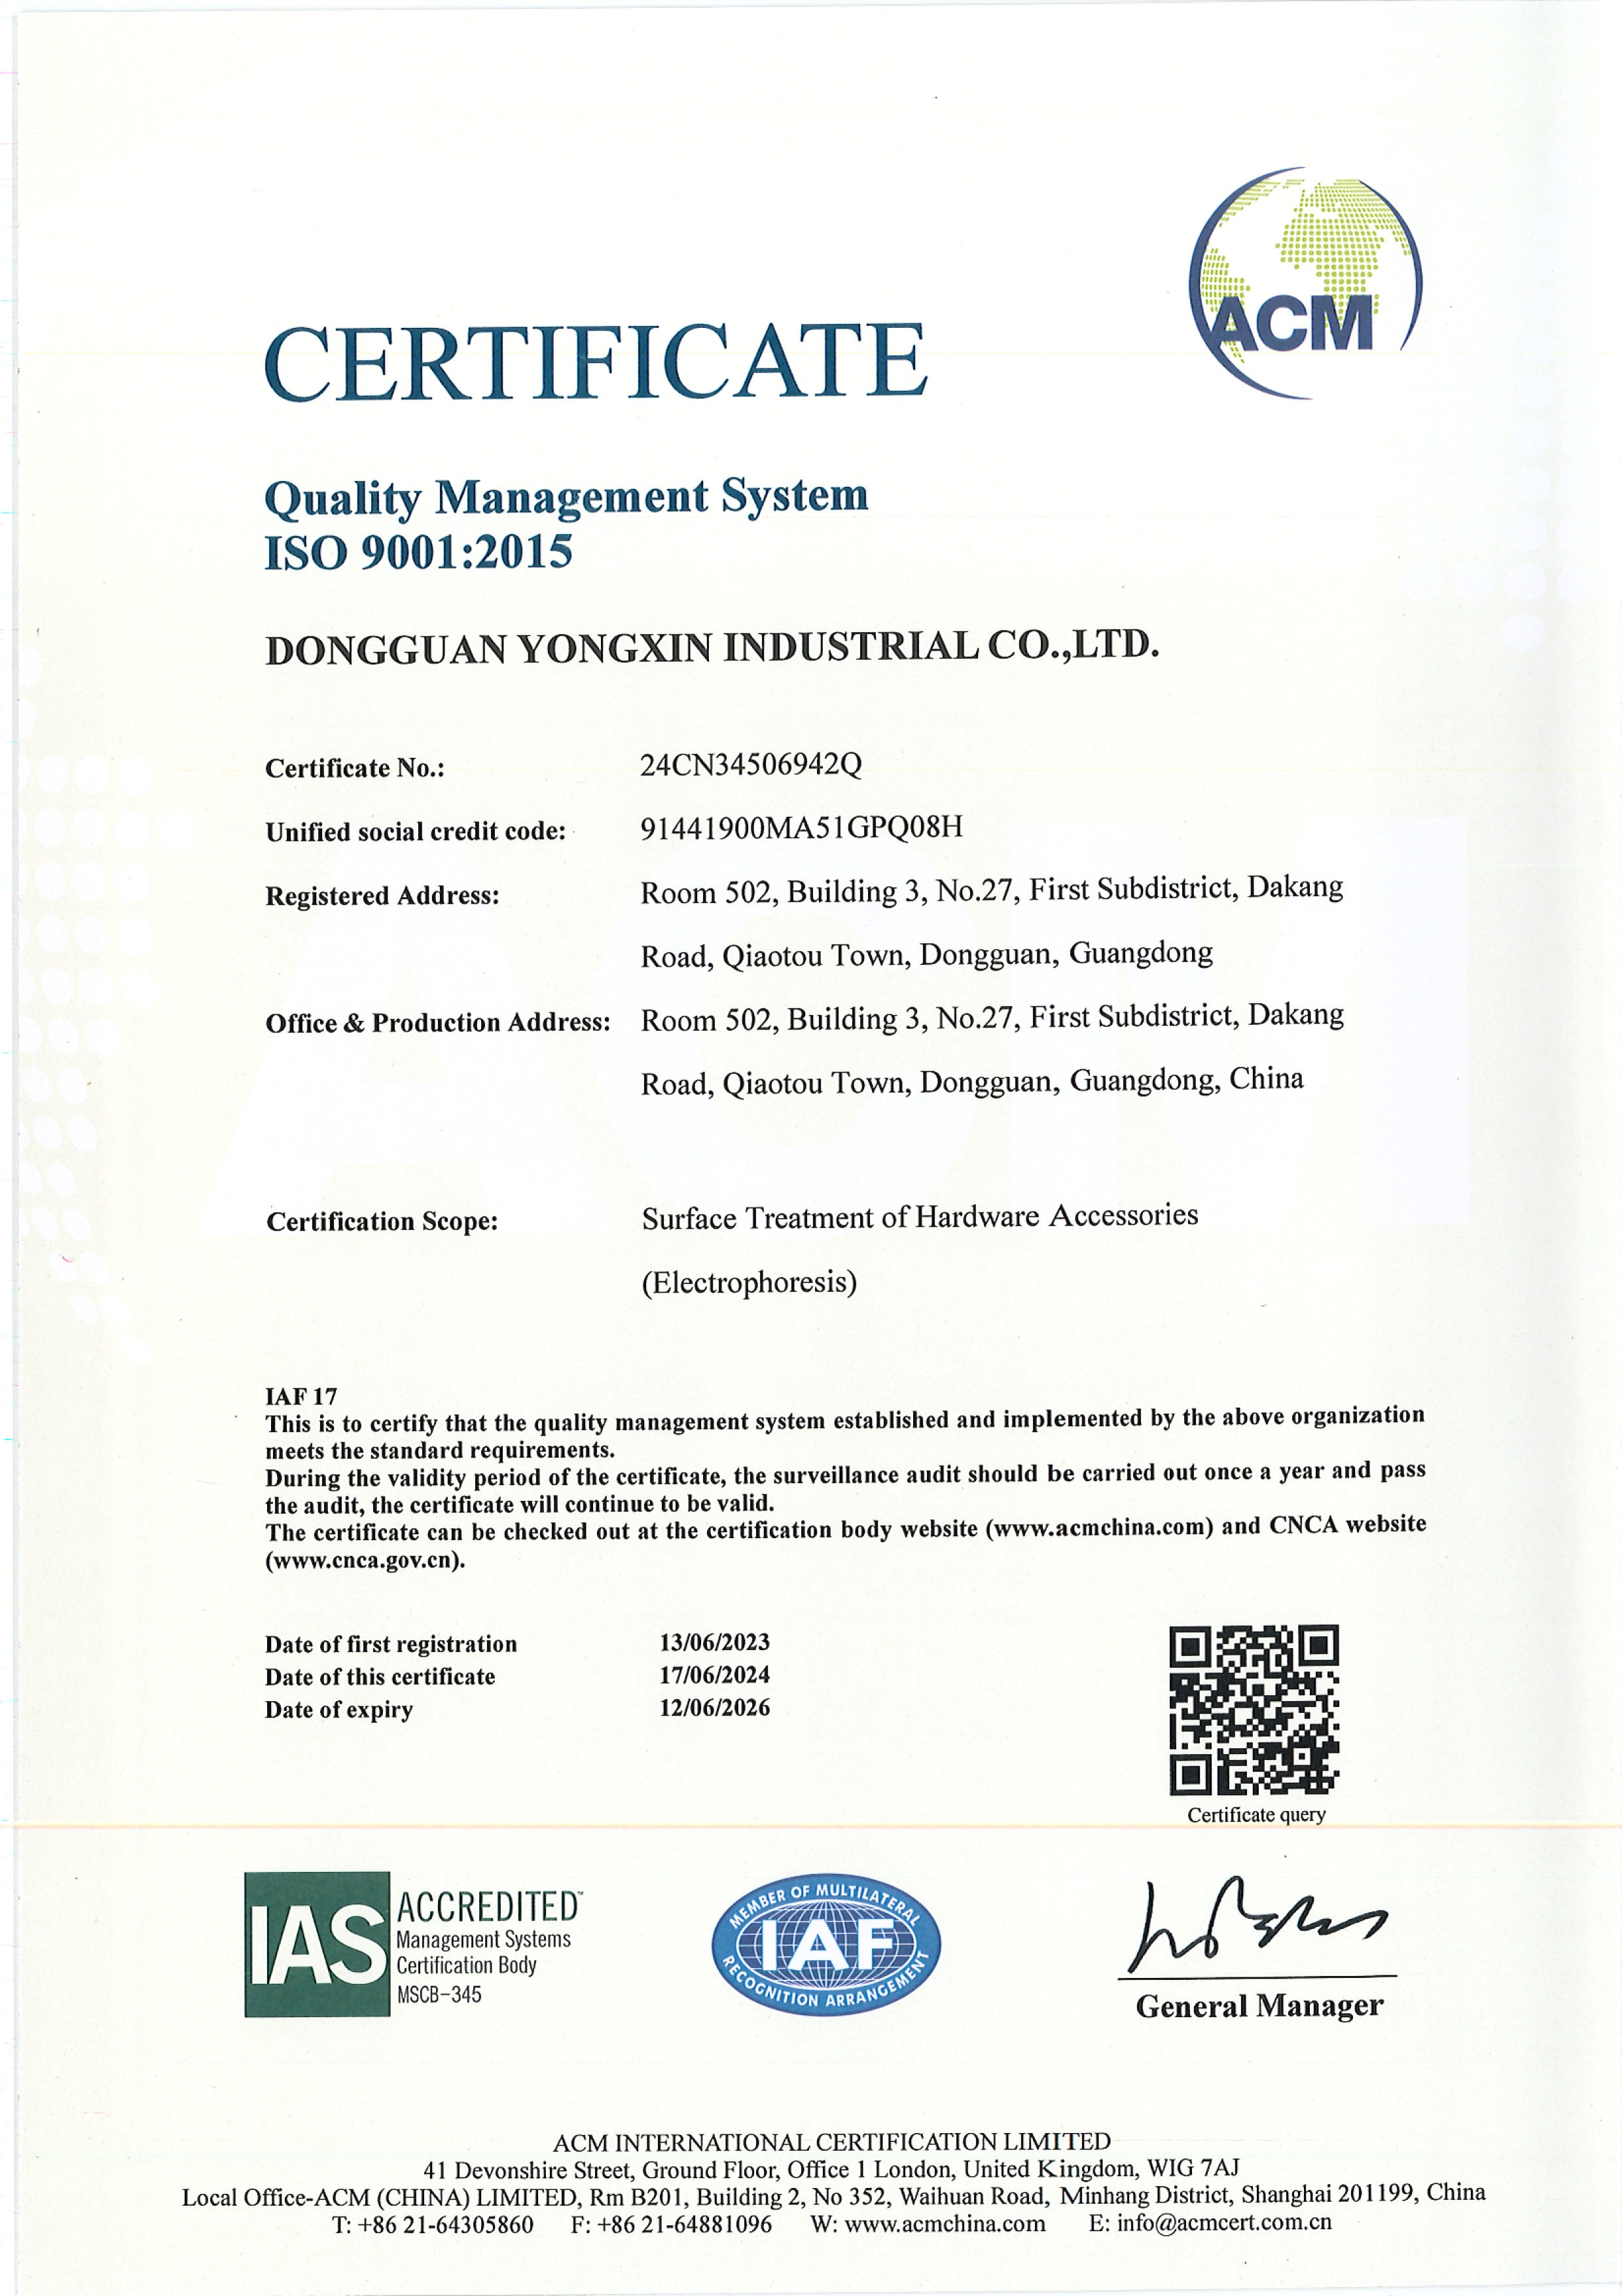
- ISO 9001:2015 Quality Management System — certificate number 24CN34506942Q, issued by ACM INTERNATIONAL CERTIFICATION LIMITED (ACMCERT), applicable globally, issued 2024-06-17 and valid to 2027-06-16. The certified scope is Surface Treatment of Hardware Accessories (Electrophoresis).
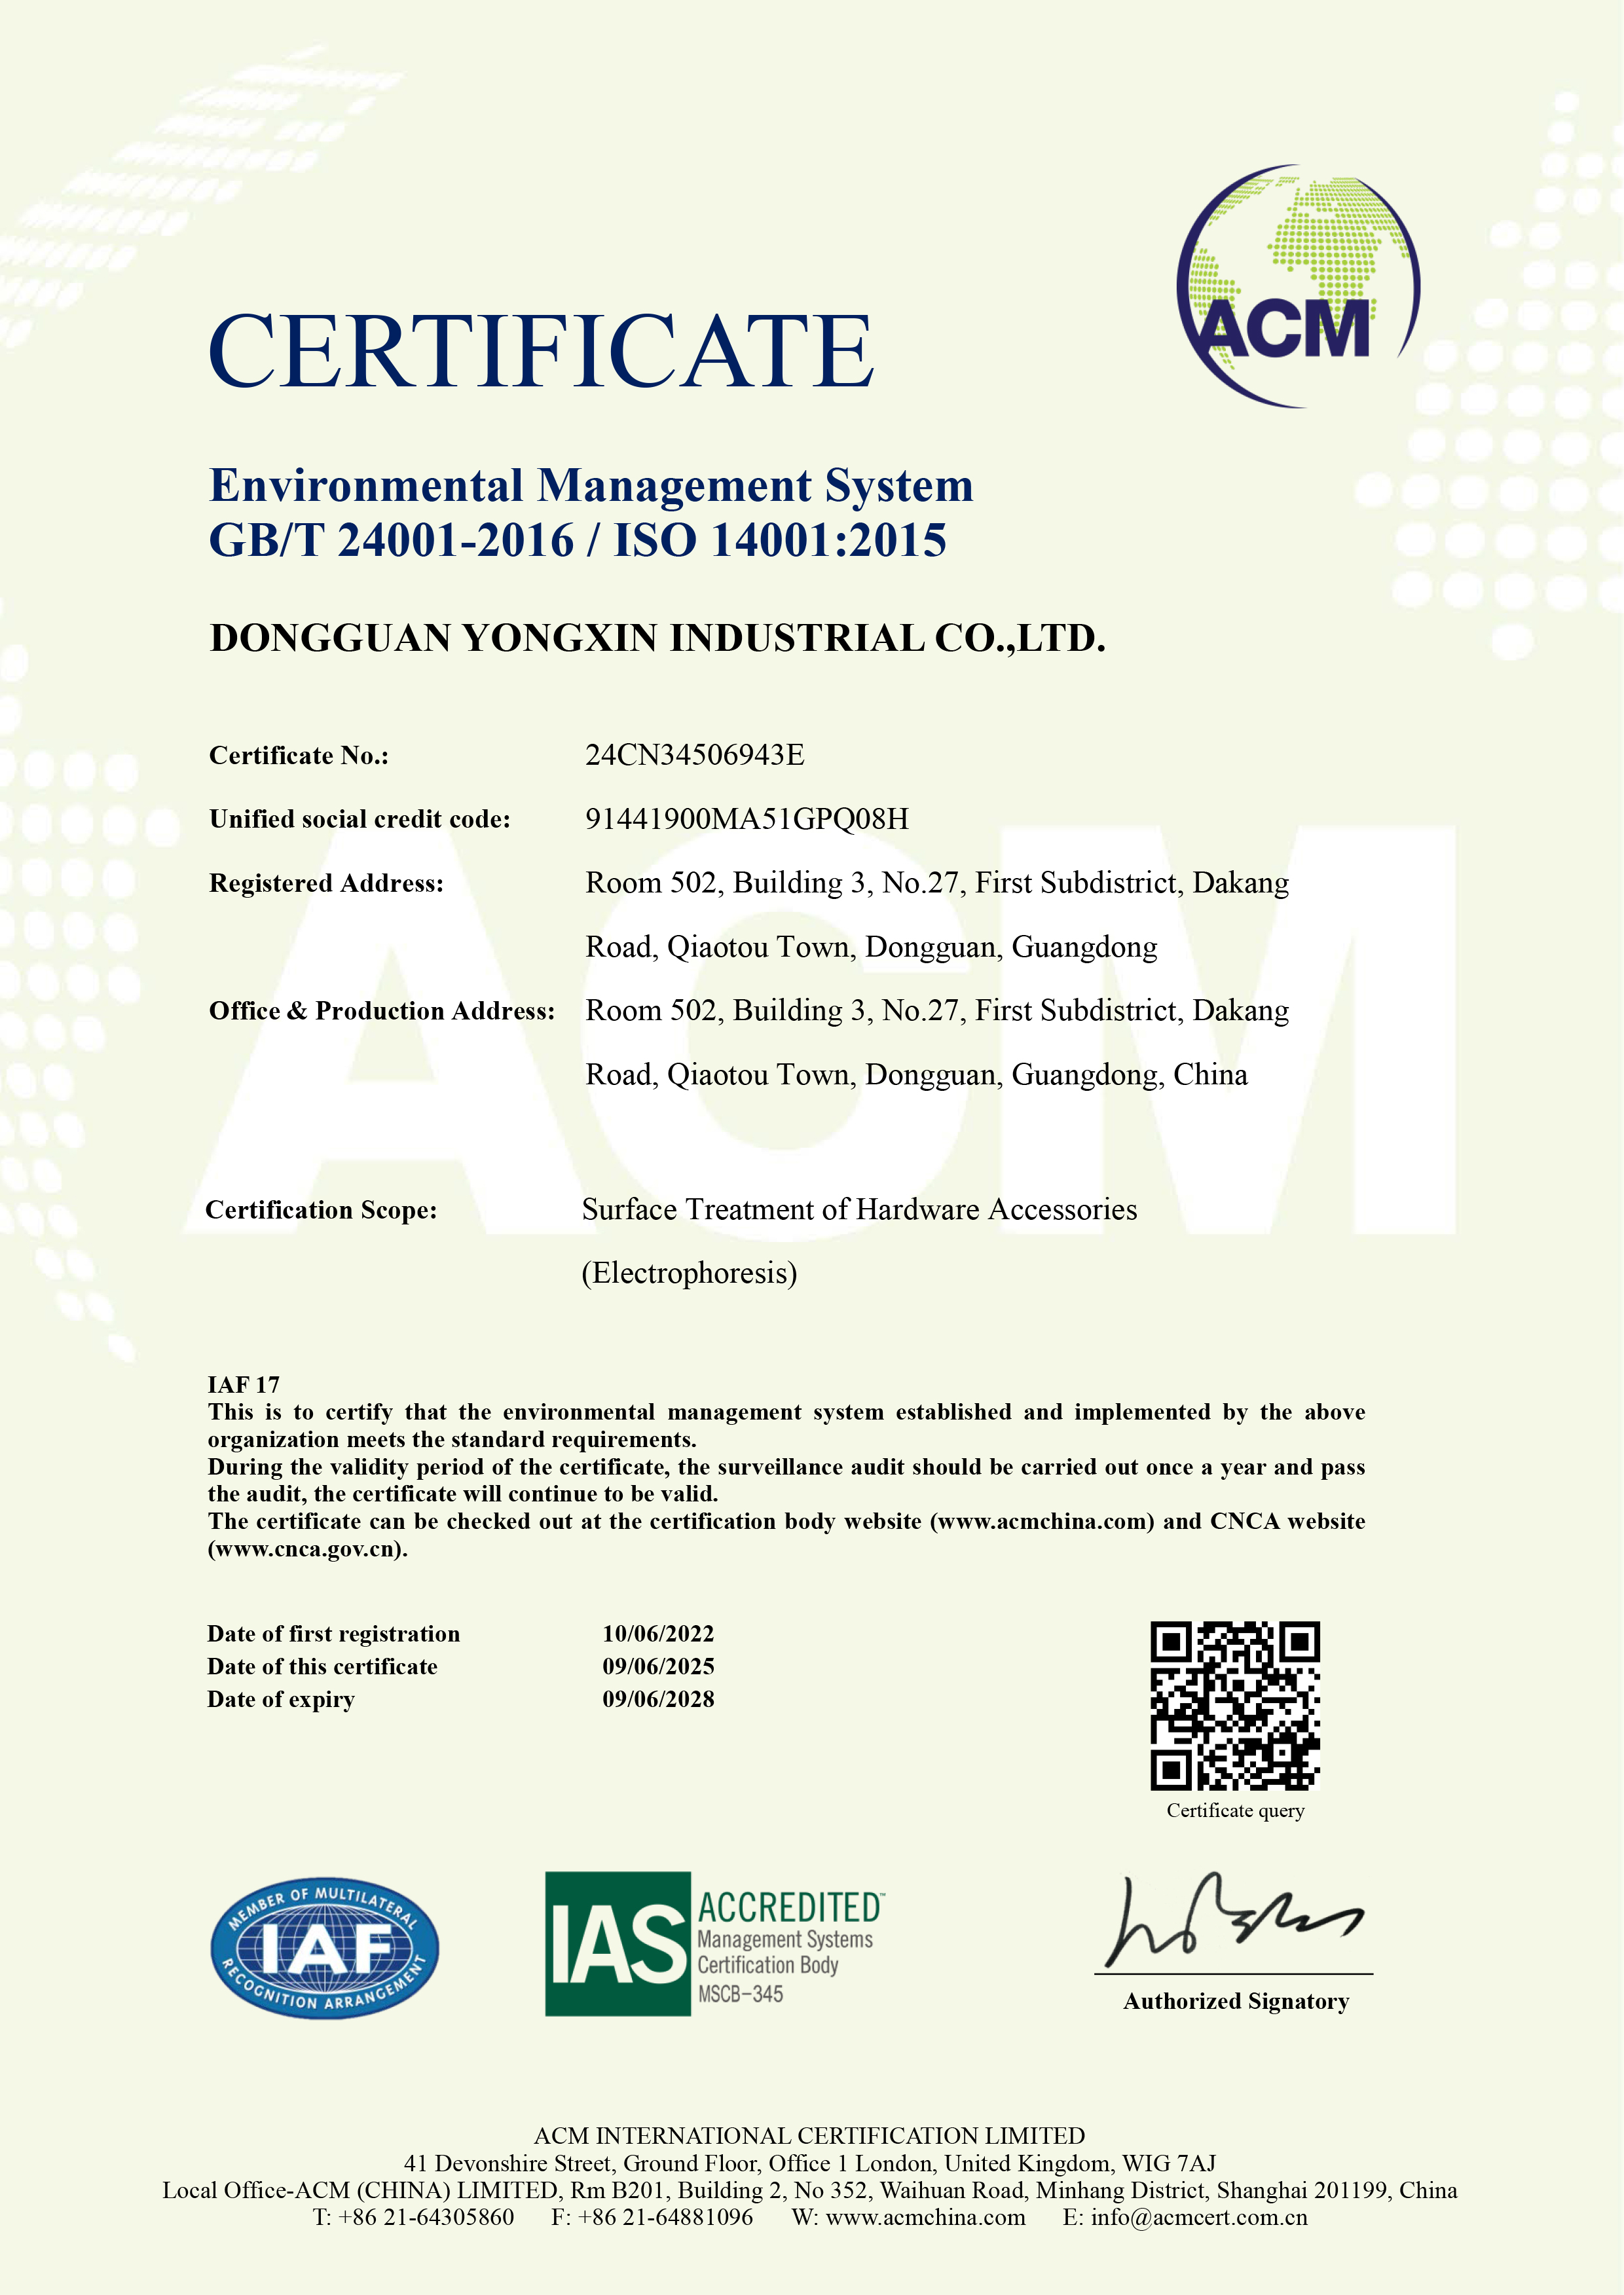
- ISO 14001:2015 Environmental Management System — certificate number 24CN34506943E, issued by ACM INTERNATIONAL CERTIFICATION LIMITED (ACMCERT), applicable globally, issued 2025-06-09 and valid to 2028-06-09, under the same electrophoresis surface treatment scope.
- IATF 16949 Automotive Quality Management System — held by the company and relevant to automotive programmes, which typically require it.
- National High-Tech Enterprise (China) — certificate number GR202344016867, issued by GDST under the Administrative Measures for the Recognition of High-tech Enterprises (Guo Ke Fa Huo〔2016〕No.32), valid from 2023-12-28 to 2026-12-28.
The chemistry constraint follows the same logic. Electrophoretic coating uses water-based paints free of heavy metals, in lead-free and chrome-free systems, with extremely low VOC emissions and compliance with international environmental standards such as RoHS. For buyers in Europe and North America, that combination — low-VOC chemistry plus an ISO 14001 management system — is usually a documentation requirement rather than a technical preference, and the comparison table below shows how it should be verified.
Step-by-Step: Writing a Spec That Holds in Production
The following sequence converts a part drawing into a specification a coating line can hold repeatably.
- Define the service environment and the failure criterion first. State the standard (for example, Neutral Salt Spray under ASTM B117), the exposure hours, and what counts as failure — red rust, blistering, or loss of adhesion.
- Fix substrate and pretreatment route. Name the alloy (carbon steel, alloy steel, aluminium alloy, magnesium alloy or zinc alloy) and require the pretreatment sequence to be confirmed in writing for that alloy.
- Choose charge type and polymer family. Cathodic systems for corrosion-led parts; anodic where the corrosion demand is moderate. Acrylic or epoxy resin according to whether appearance stability or corrosion resistance is the governing requirement.
- Set the thickness clause. Nominal plus acceptable range — 15–25 µm is the standard window for ordinary parts — plus the measurement method and the measurement locations, including at least one recessed area on complex geometry.
- Specify colour and finish against a physical reference. Black matte, black glossy, white or a custom colour such as grey or silver, defined against a sample and checked for batch-level colour consistency.
- List the compliance documents required at order. ISO 9001:2015 and ISO 14001:2015 certificates with scope, IATF 16949 where the programme is automotive, and RoHS statements for the finished coating.
- Validate with a sample and a test report. Confirm film thickness measurements, salt spray results, adhesion, gloss and colour from the sample run before releasing the production batch.
- Lock process control and commercial terms. Define inspection frequency, packaging, minimum order quantity and lead time in the same document, so that quality and delivery are governed by one specification.
Use Cases: Where These Parameters Are Applied
Motor housings and cores. The documented Japanese motor project applied E-coating to 15,000,000 motor units at over 720 hours of neutral salt spray resistance, with uniform coverage of complex structural gaps and a service-life extension of 5 to 10 years compared with non-E-coated parts.
CNC precision parts. A CNC precision machining programme covering 10,000,000 parts reported fully covered film with no missed coating at corners or inner cavities, strong adhesion, resistance to acid, alkali, rust and ageing, small batch-to-batch colour difference, and support for multi-material and multi-colour customization with fast delivery and mass production on demand.
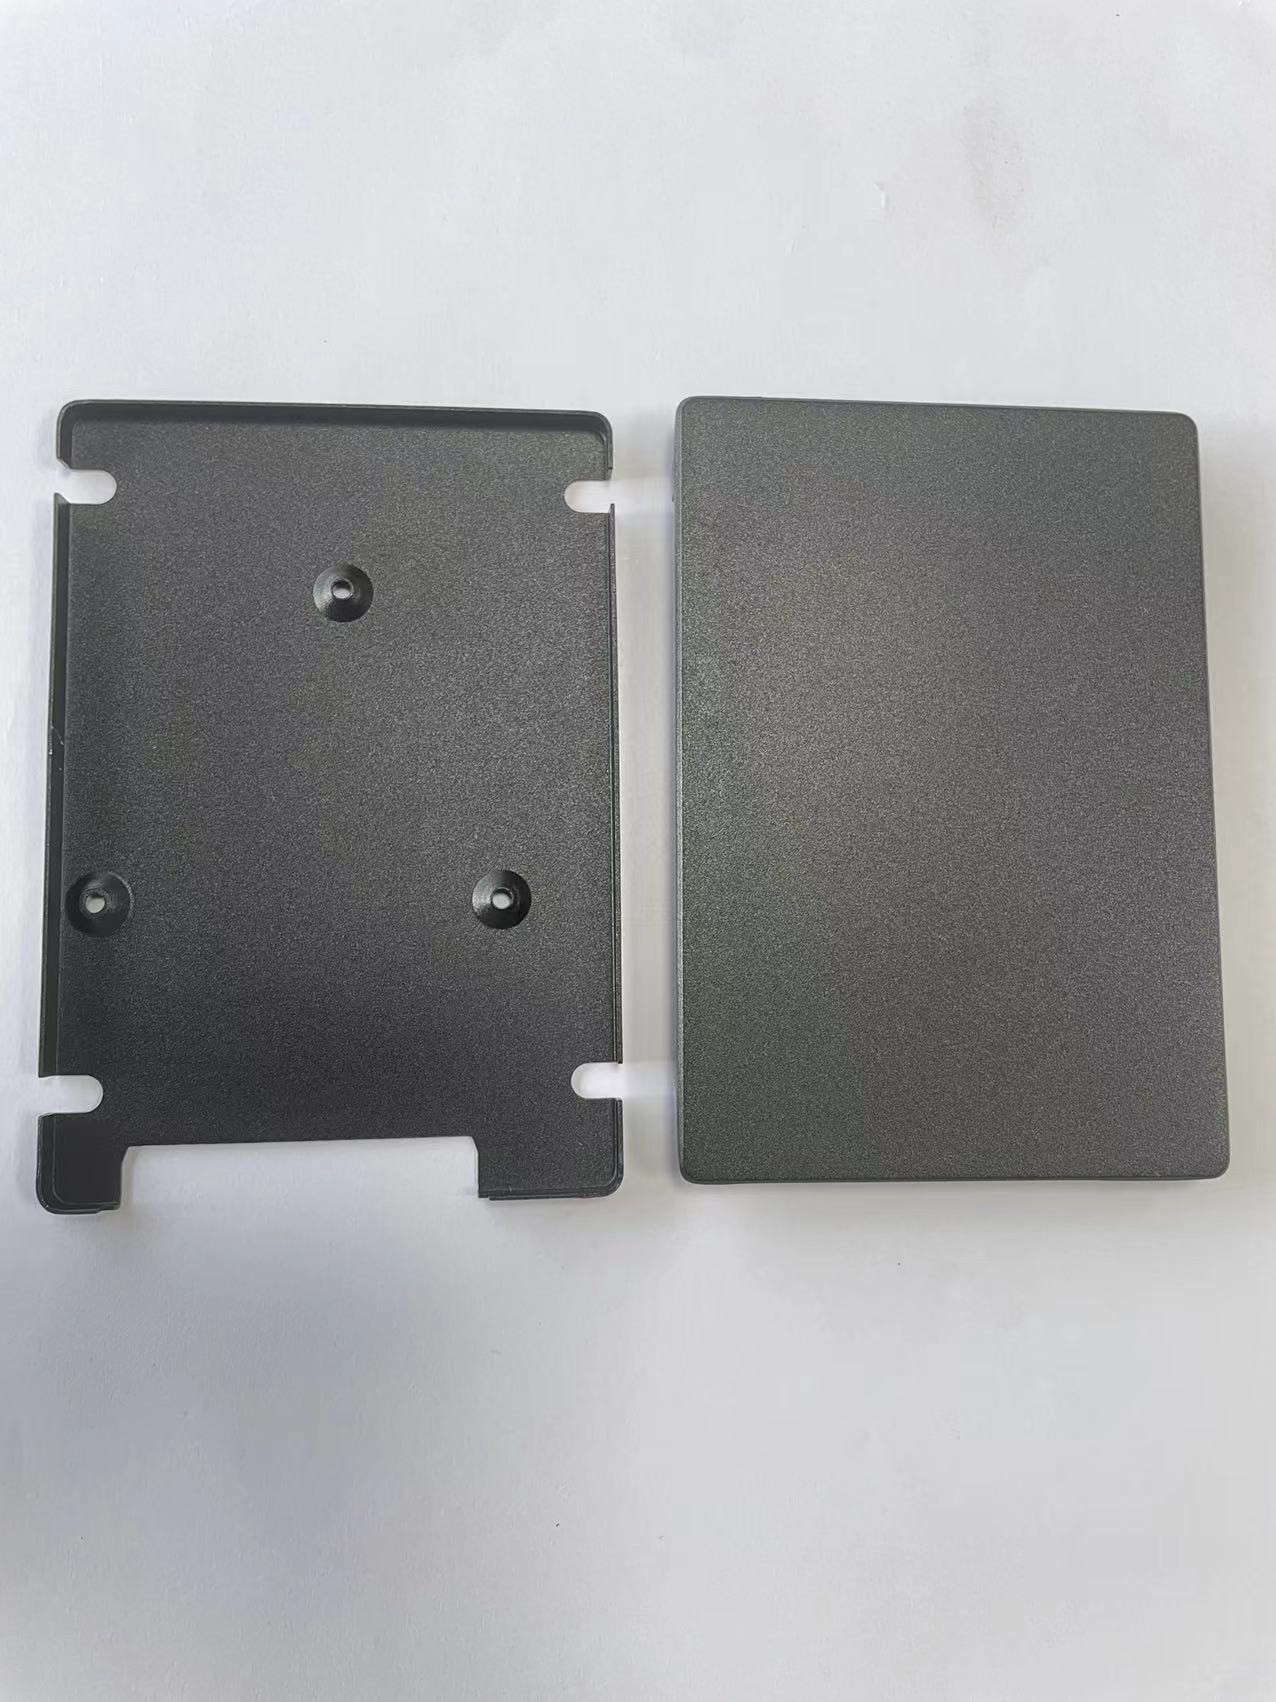
Die-cast and stamped components. Zinc alloy die-cast parts and stamped parts are coated for consumer electronics, communication equipment and precision hardware applications, where corrosion resistance and dimensional stability both matter.
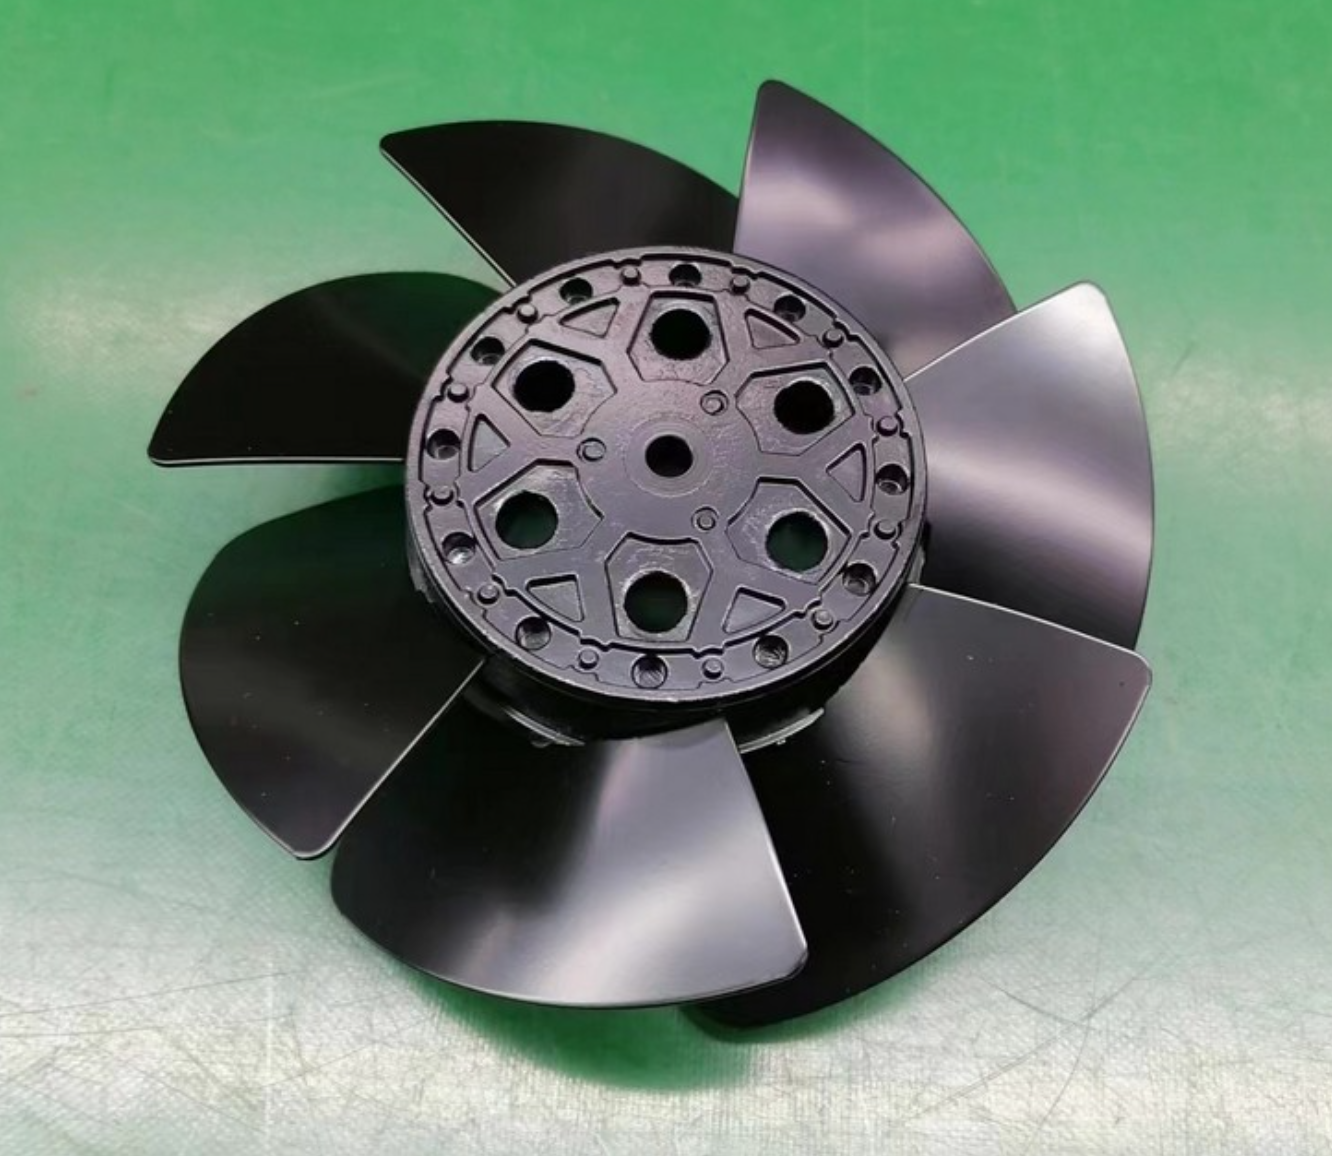
Bicycle, cooling and LED components. Bicycle accessories, cooling fans, fan frames and LED heat-dissipation bases are coated in black E-coat, where surface uniformity and long-term outdoor or thermal exposure drive the specification.
Drone and UAV structural parts. Magnesium and aluminium alloy structural components for unmanned aerial vehicles use electrophoretic coating where weight, corrosion resistance and a consistent cosmetic finish are required together.
Comparison Tables
The first comparison is the one that constrains everything else: charge type.
| Attribute | Anodic (Anion) Electrophoretic Coating | Cathodic (Cationic) Electrophoretic Coating | Basis |
|---|---|---|---|
| Typical salt spray (ASTM B117) | Around 500 hours | Frequently exceeds 1,000 hours | Market Reports World |
| Market position | Established, lower corrosion band | Dominant in the E-coat market | Market Reports World |
| Resin association | Listed as a product line by Yongxin | Listed as a product line by Yongxin | Yongxin product data |
| Typical selection driver | Moderate corrosion demand | Corrosion-critical metal parts | Editorial selection rule |
Charge-type performance figures are third-party market data; final selection should be confirmed against project-specific test reports.
The second comparison maps the parameters a buyer can write into a purchase specification.
| Parameter | Standard value (Yongxin production data) | How to verify |
|---|---|---|
| Dry film thickness | 15–25 µm for ordinary parts, customizable | FISCHER film thickness gauge; documented measurement points |
| Thickness tolerance | Typically within ±1 µm; batch variation within ±5% | Batch thickness records |
| Salt spray resistance (high-salt-spray line) | 300–1,000 hours | Neutral salt spray test report |
| Automotive-grade salt spray specification | 500–1,500 hours NSS without red rust; CASS over 96 hours | ASTM B117 / CASS test reports |
| Coverage on complex geometry | Over 95%–98% including cavities and internal holes | Visual and coating-weight inspection |
| Temperature tolerance | -40°C to over 85°C | Thermal cycling and adhesion testing |
| Colour options | Black (matte or glossy), white, custom colours including grey and silver | Colour sample approval; spectrophotometer reading |
| Chemistry | Water-based, lead-free and chrome-free, low VOC, RoHS compliant | RoHS statement and ISO 14001:2015 certificate |
| Quality and environmental certification | ISO 9001:2015 (24CN34506942Q); ISO 14001:2015 (24CN34506943E); IATF 16949 | Certificates with certified scope and validity dates |
Values reflect Yongxin's published product and capability data; buyers should confirm the applicable subset for their part and substrate.
FAQ
Which certifications should be verified before releasing an E-coating purchase order?
Start with ISO 9001:2015 Quality Management System — Yongxin's certificate number is 24CN34506942Q, issued by ACM INTERNATIONAL CERTIFICATION LIMITED (ACMCERT) and applicable globally — and ISO 14001:2015 Environmental Management System, certificate number 24CN34506943E, also issued by ACMCERT. Both certificates state the certified scope as Surface Treatment of Hardware Accessories (Electrophoresis), which is the line a buyer must read; a certificate outside that scope does not cover the process being purchased. Automotive programmes normally also require IATF 16949, which the company holds, and Yongxin was recognized as a National High-Tech Enterprise in China under certificate GR202344016867, issued by GDST and valid from 2023-12-28 to 2026-12-28.
What thickness and salt spray figures can realistically be written into a specification?
Yongxin's standard dry film thickness is 15–25 µm for ordinary parts and is customizable, with tolerance typically held within ±1 µm and batch thickness variation controlled within ±5%. On salt spray, the high-salt-spray electrophoresis line is rated from 300 to 1,000 hours, while automotive-grade E-coat specifications are normally written as 500–1,500 hours of neutral salt spray without red rust, with CASS testing exceeding 96 hours, and corrosion-critical automotive parts are commonly specified above 1,000 hours. The clause should always name the test standard and the failure criterion, because salt spray hours without a method and a pass/fail definition are not a specification.
What drives the cost of an electrophoretic coating project?
There is no single price band that applies across parts, so quotations are prepared per project. The variables that move cost most are the substrate and its pretreatment route, part geometry and hanging density on the line, the colour and finish specified, the film thickness and salt spray target, order quantity, and the volume of testing and documentation required. Commercial terms at Yongxin are MOQ 100, lead time of 3–45 days depending on quantity, and 100% testing of production; capacity for large-batch, multi-category orders is supported by six electrophoresis production lines and a published monthly capacity of 2,500,000 units.
Can samples be validated before mass production?
Yes, and sample validation is the recommended gate. Yongxin supports rapid sample customization with quick sample confirmation, which shortens the production cycle, and finished goods are subject to full inspection before shipment. For validation to be meaningful, the sample report should include film thickness measurements, salt spray results with the standard and duration stated, adhesion performance, and, where colour is critical, spectrophotometer readings against the approved reference. Sample confirmation at these four points is what makes a production release defensible.
What lead time and capacity should a buyer plan for?
Lead time at Yongxin is 3–45 days depending on quantity. Capacity is supported by six electrophoresis production lines, more than 20 general processing units including sand blasters, polishers, shot blasting machines and laser equipment, over 20 CNC machines, more than 10 die-casting machines and more than 10 metal stamping machines, with more than 20 high-precision testing instruments covering thickness, gloss, colour, roughness and salt spray. Export experience covers Europe and America, Southeast Asia, Mexico, Poland, Turkey and Brazil, with an export ratio of around 30%.
Conclusion
Resin, thickness and salt spray are not three independent line items. The charge type and polymer family set the corrosion ceiling, the 15–25 µm film window determines whether that ceiling is reached on the production floor, and the salt spray clause — with a named standard and a stated failure criterion — is what makes the first two measurable. Buyers who specify all three together, and who verify certificate scope rather than certificate presence, get a coating specification that holds from sample approval through mass production.
Send Us Your Drawing for a Sample and Quotation
Dongguan Yongxin Industrial Co., LTD processes electrophoretic coating for black, white and custom-colour parts on steel, aluminium, zinc and magnesium substrates, with 300–1,000 hour salt spray capability, 15–25 µm film thickness control and 100% inspection.
Email: wuzj@yxsydy.com | Tel / WhatsApp: +8615322922788 | Website: https://www.yxecoat.com/
Download the full product and capability brochure: Enameled Flat Wire and Electrophoretic Coating Solutions (PDF)