Custom Optical Lens: Types, Materials, Applications, and Sourcing Steps
A custom optical lens is an optical component designed and molded around a specific light source, beam distribution, mechanical envelope, and operating environment — rather than selected from a standard catalogue. Its optical surfaces, wall thickness, mounting features, and material grade are defined by the luminaire or imaging system it serves, which is why two lenses of identical diameter can produce completely different light.
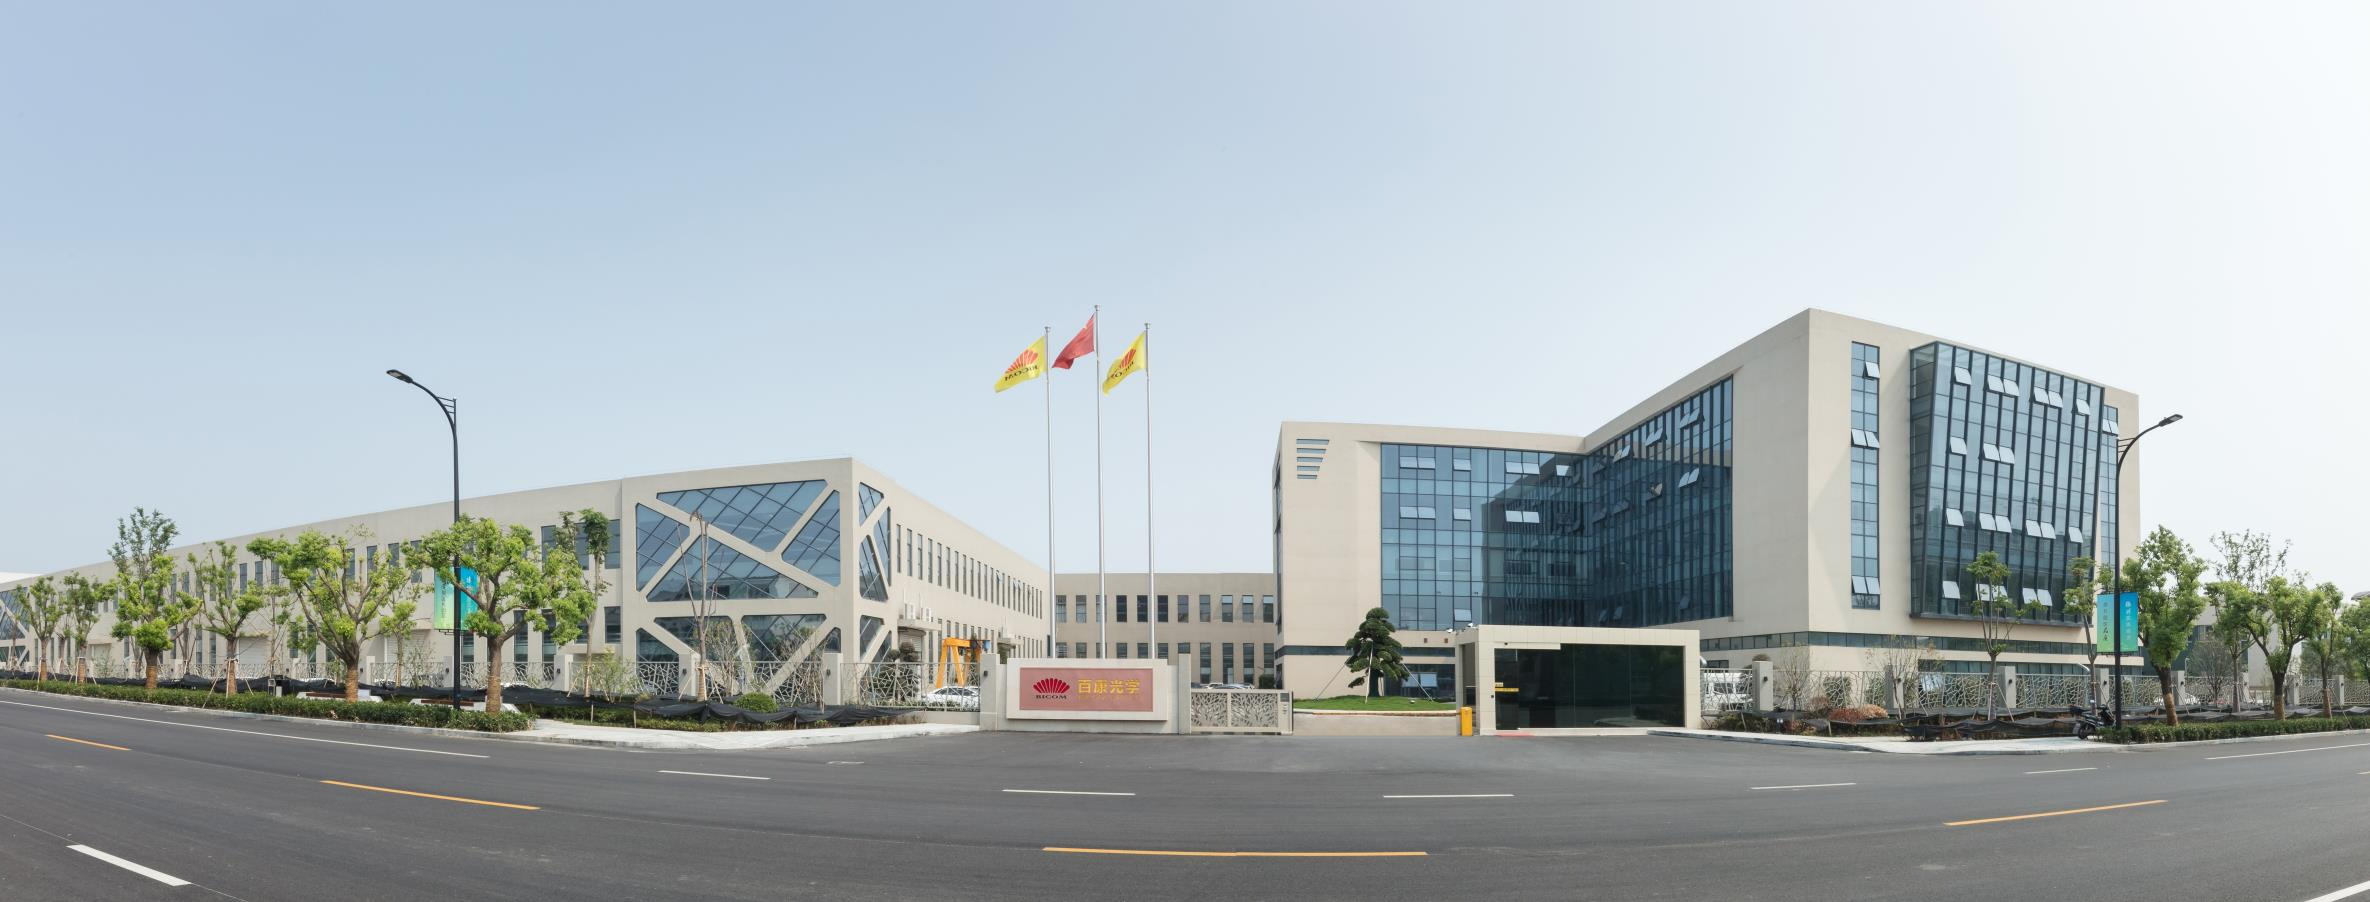
Zhejiang Bicom Optics Co., Ltd (Bicom Optics) is an optical lens and precision injection mold manufacturer established in 2005 and based in Jiashan County, Jiaxing City, Zhejiang Province, China. Its product portfolio covers LED optical lenses, automotive lighting lenses, industrial lighting optics, machine vision lenses, security camera lenses, UAV optical lenses, optical lens molds, and custom optical components.
This guide is written for buyers and engineers in the research stage: it explains what a custom optical lens actually is, what information determines its design, how it is manufactured, where each lens construction is used, and which questions separate a capable optical partner from a company that simply molds to a drawing.
The Sourcing Problem: Three Different Things Called “Custom”
The word “custom” hides three commercial models, and buyers who do not separate them early tend to compare quotations that were never comparable.
- Build-to-print. The buyer owns the optical design and the drawings; the supplier only manufactures. Useful when you already have optical engineering in-house, but it leaves every optical problem on your side of the table.
- Design-and-build. The supplier participates in requirement definition, optical design, structural evaluation, mold design, sampling, and mass production. This is the model implied by most custom optical lens projects in lighting, because the lens geometry is inseparable from the LED layout and the mold.
- Full program supply. The supplier carries the project from prototype sampling through T0 validation, design optimization, and stable series production, including revision control of drawings and optical data.
A practical decision rule: if your project involves complex optical surfaces, light guides, TIR lenses, projection lenses, thick-wall optical parts, or multi-cavity molds, a pure build-to-print vendor will usually hand the hardest problems back to you. In those cases, a supplier that understands both optical design specifications and plastic injection molding manufacturing reduces the technical hand-over risk between separate vendors.
Design Inputs That Decide the Lens Before It Exists
Custom optical lenses carry no fixed model designation; they are produced to custom specifications. What the lens becomes is determined by inputs that should be fixed before any quotation is requested.
- Light source data. Emitter type and layout — high-power LEDs, COB LEDs, LED modules, or arrays — because each cavity, facet, or prism is calculated against a specific source position and size.
- Target photometric behaviour. Beam angle, distribution shape, uniformity, glare and stray-light limits. Available specification ranges run from a 2° spot to a 120° flood, with spot, flood, and custom-shaped beam configurations supported.
- Mechanical envelope. Outer dimensions, mounting features, assembly clearance, and available depth. Lens sizes are customisable from 5 mm to 1,500 mm.
- Operating environment. Indoor or outdoor use, ambient temperature range, humidity, UV exposure, and vibration. Published operating windows are −40 °C to +120 °C for optical-grade PC and −40 °C to +90 °C for optical-grade PMMA; lighting and automotive applications commonly specify −40 °C to +105/120 °C with continuous operation.
- Volume and lifecycle. Prototype quantities, series volumes, expected production years, and whether the mold is a prototype mold or a production mold.
- Compliance requirements. Market access requirements for the finished luminaire or lamp, which flow down to the lens material and documentation.
Industry Background: Why LED Secondary Optics Became a Molded-Polymer Business
Optical lenses are a large, established component category. Fortune Business Insights valued the global optical lens market at USD 21.08 billion in 2025. That figure covers the whole lens field, not the lighting segment alone — and no methodology-transparent public figure for LED secondary optics as a standalone segment is currently available, so segment-level demand should be treated as directional rather than measured.
The demand driver that matters most for custom lens work is vehicle lighting. TrendForce / LEDinside projects that vehicles equipped with adaptive driving beam (ADB) headlights will reach a 23.8% penetration rate by 2030. ADB depends on precisely shaped, individually controlled light distributions — the type of output that free-form and multi-cavity lens geometry delivers, and that only high-precision molding can reproduce at series volume.
This is why the centre of gravity in LED optics sits with injection-molded optical-grade PC and PMMA rather than glass: the same part can combine optical surfaces, mounting features, and light-shaping microstructures in a single molding cycle, and the process can be repeated across multi-cavity tools.
Lens Construction Options and Where Each Fits
The construction type is the first technical decision, because it constrains the mold, the material, and the achievable beam.
| Construction option | Optical behaviour | Typical use |
|---|---|---|
| Fresnel lens | Annular prismatic facets or microstructures converge, collimate, or redistribute light; delivers comparable light control at a much thinner profile than a conventional thick lens of similar focal length | Large-area lighting, solar concentration, sensors, and devices sensitive to size and weight (e.g., model DB1072) |
| Aspheric LED lens | Aspheric surface geometry used as a secondary optic for LED sources | General LED lighting scenarios |
| TIR lens | Total-internal-reflection construction listed as a secondary optic option for lighting | LED lighting scenarios requiring controlled distribution |
| Free-form optical lens | Complex asymmetric curved surfaces that shape a defined beam, cutoff line, or asymmetric distribution | Automotive low/high beam, street and outdoor luminaires, architectural lighting |
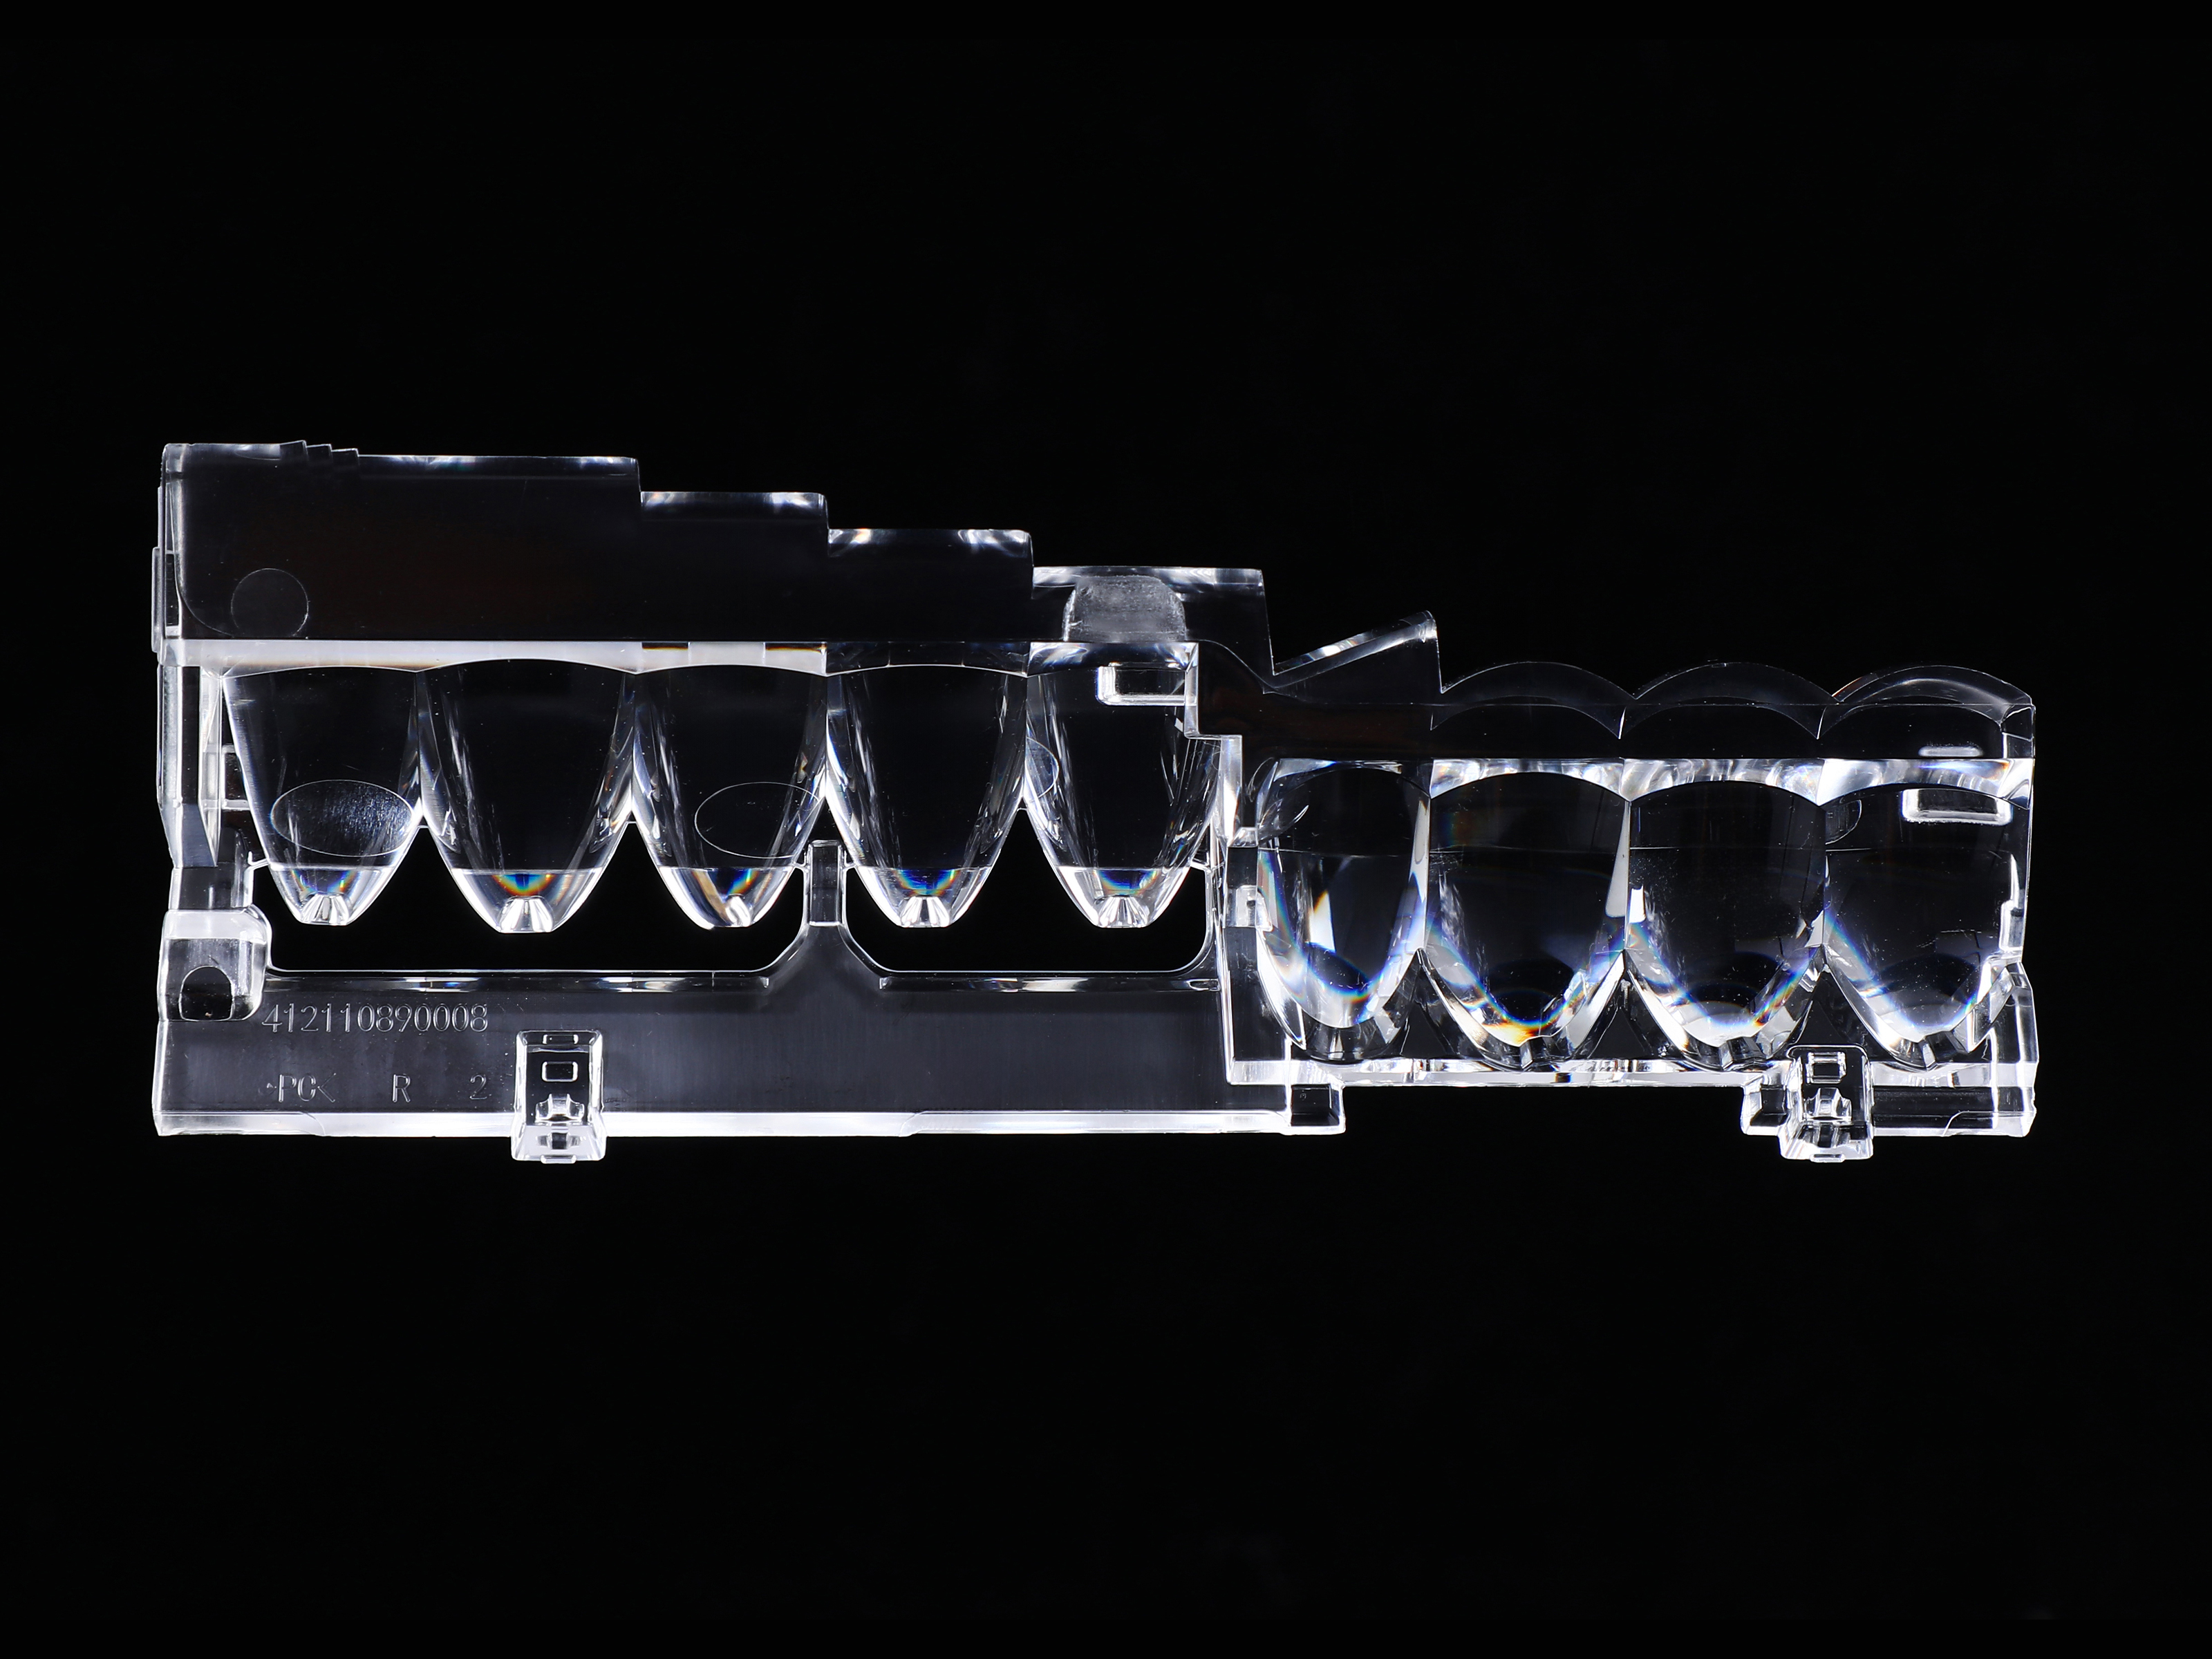
| Multi-cavity optical array | Several tapered or cup-shaped cavities arranged in a row, each distributing light for one LED; precise free-form inner surfaces capture and collimate light | Low beam inner lens modules and other multi-emitter assemblies |
| Thick-wall optic | Large-thickness transparent body with dense micro-prism structures on one edge; high structural strength and even light output | Rear turn signal lamps, headlamp lenses |
| Light guide | High-transmittance light-guiding structure producing even, soft illumination without obvious bright spots | Automotive ambient lighting; light guides produced up to 1,300 mm in length |
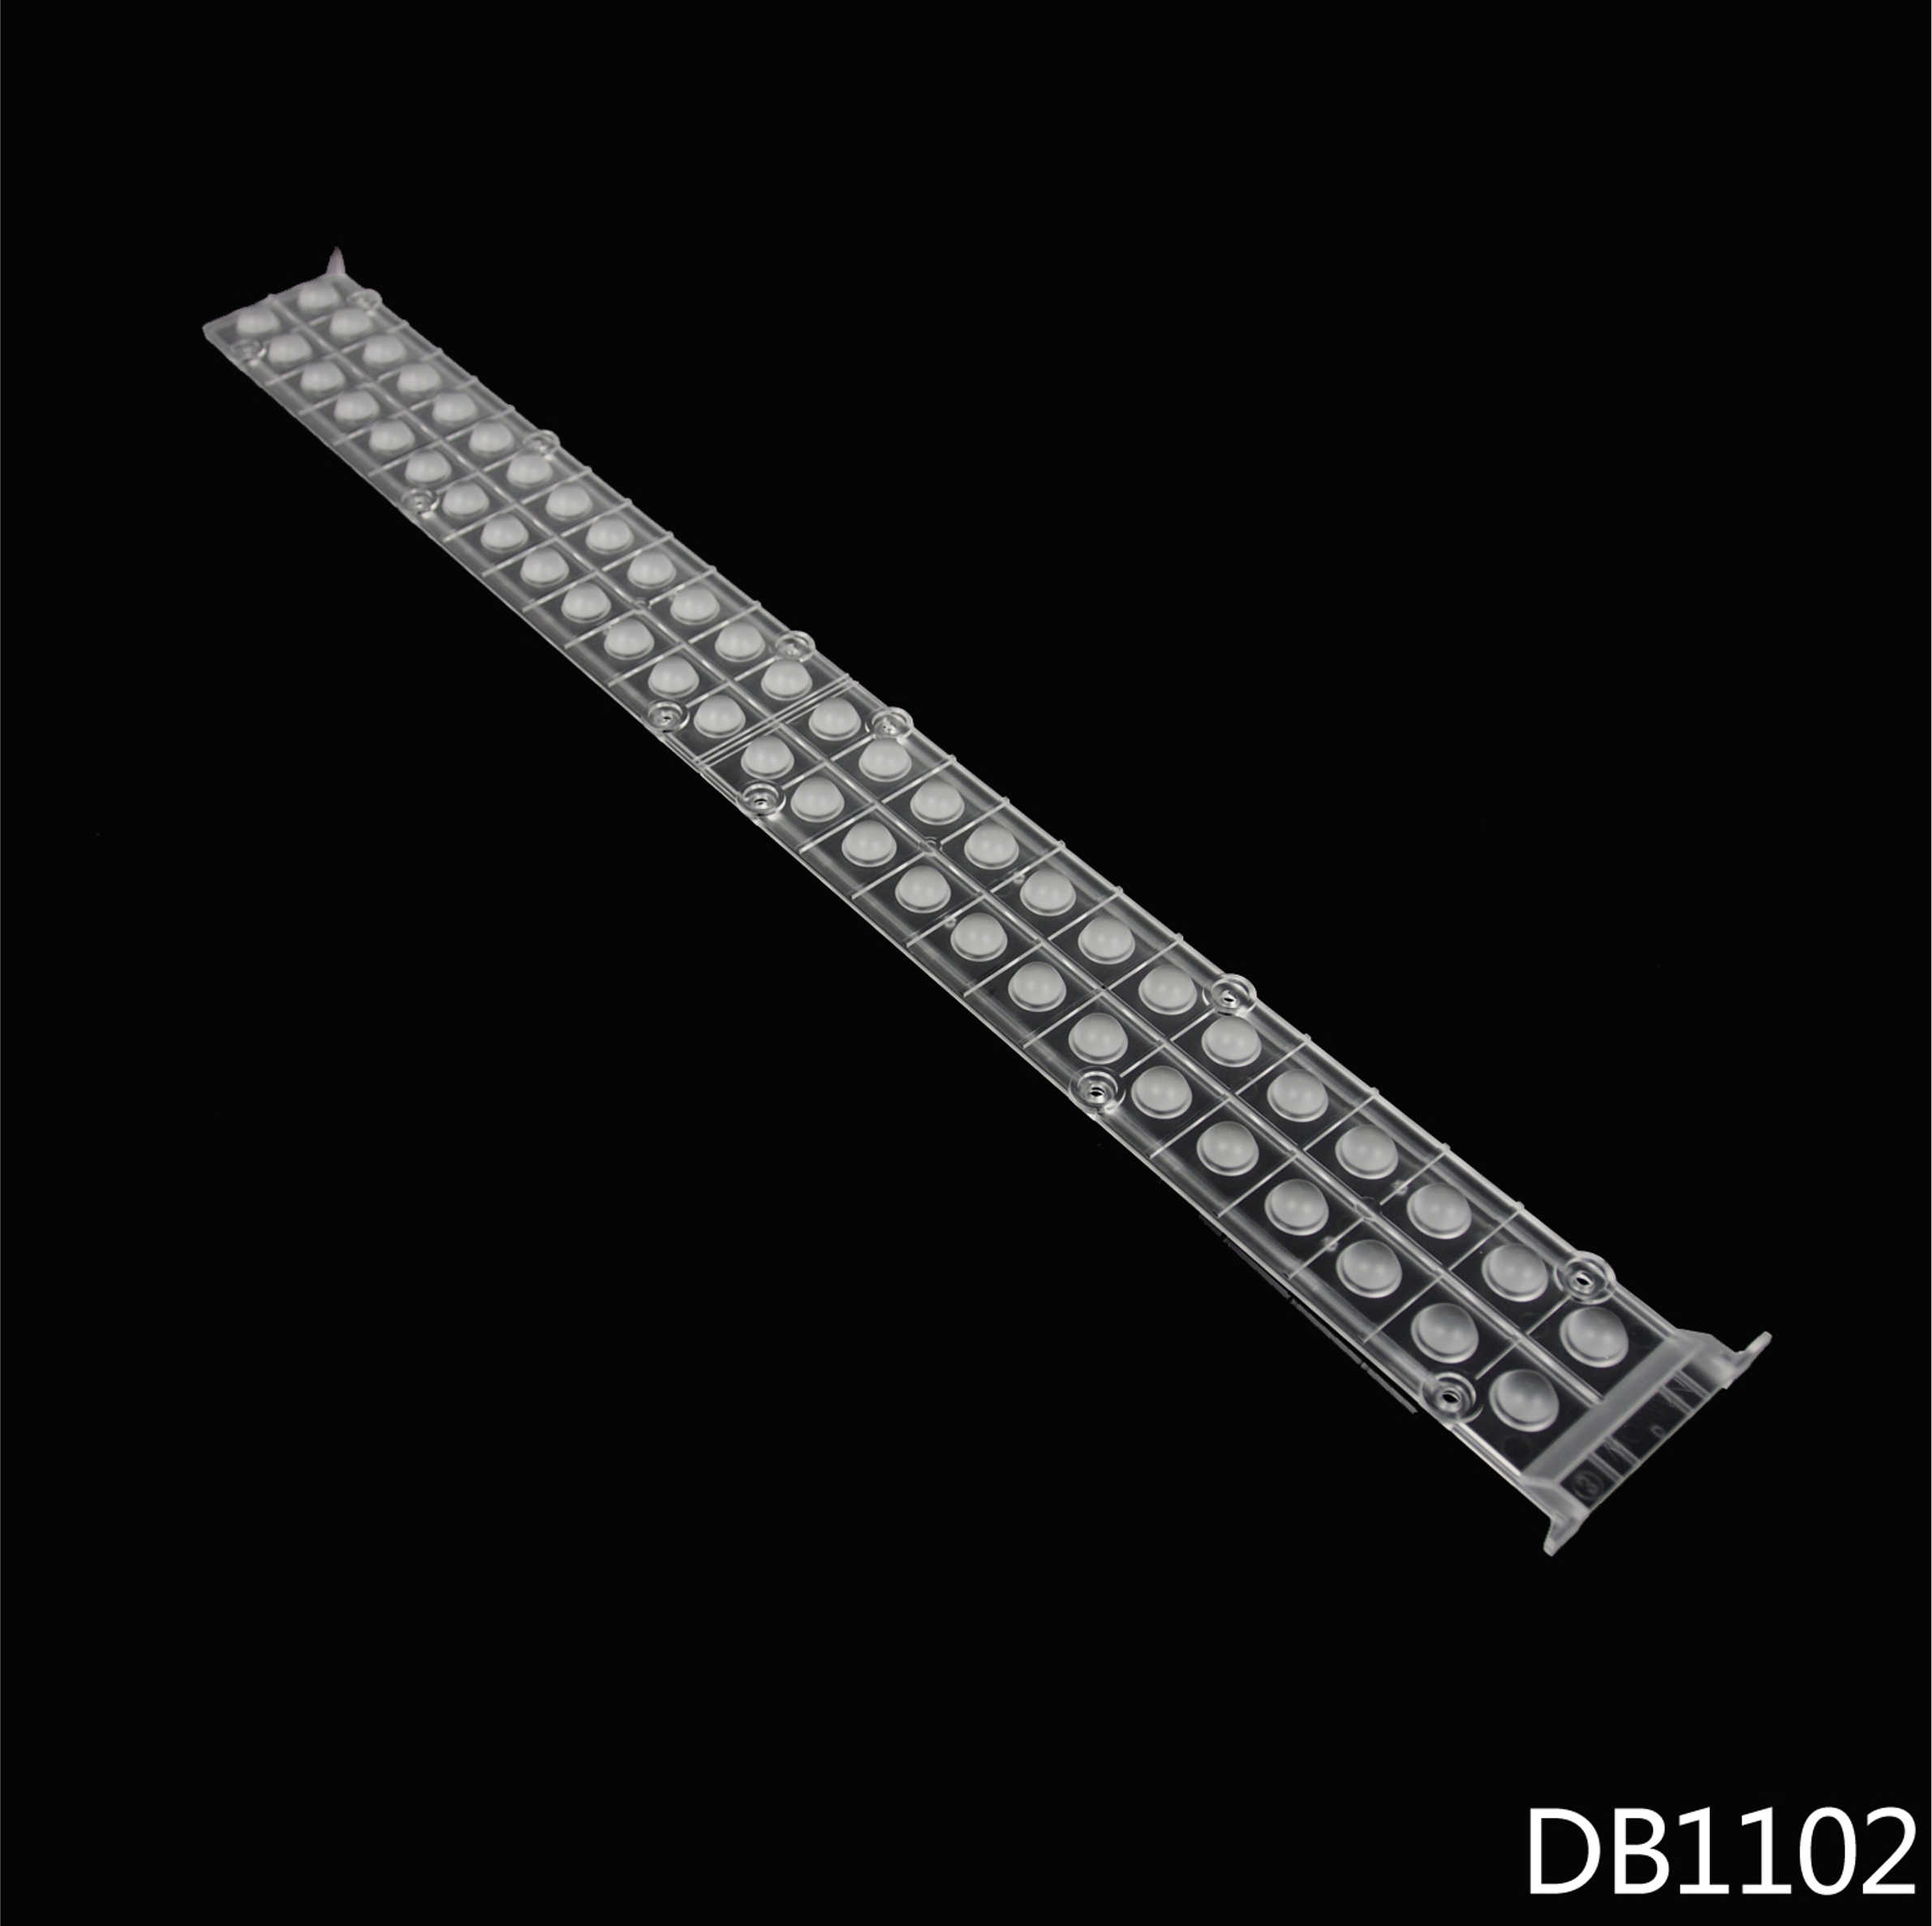
| Linear lens | Elongated optical structure optimised for continuous, uniform strip illumination and slim integration | Indoor linear lighting, display lighting, industrial lighting, architectural wall washing, machine vision lighting (e.g., model DB1102) |
Material Choice: Optical-Grade PC Versus PMMA
Two polymers dominate custom LED optics, and the specification sheet already distinguishes them on the two parameters that most often decide a project: transmission and heat tolerance.
| Property | Optical-grade PC (polycarbonate) | Optical-grade PMMA (polymethyl methacrylate) |
|---|---|---|
| Light transmission (as specified) | >88% | >90% |
| Operating temperature range | −40 °C to +120 °C | −40 °C to +90 °C |
| Forming route | High-precision injection molding | High-precision injection molding |
| Customisable size range | 5–1,500 mm | 5–1,500 mm |
The practical reading: PMMA gives slightly higher transmission, while PC extends the upper temperature limit by roughly 30 °C. For high-power LED modules, thick-wall parts, or automotive assemblies exposed to sustained heat and vibration, that headroom is usually the deciding factor. Both materials are also expected to resist UV-driven yellowing over long service life in outdoor and automotive use.
Manufacturing Capability Behind a Custom Lens
An optical lens is not finished when the mold closes. Capability has to exist across the entire chain: optical design, structural evaluation, DFM, mold-flow analysis, mold design and fabrication, precision injection molding, optical testing, and mass-production support.
At Bicom Optics, the manufacturing envelope is defined by several concrete parameters:
- Nanoscale CNC machinery with positioning accuracy up to 10 nanometers.
- Mold cavity precision adjustable to within 5 microns.
- High-precision thick-wall lenses produced up to 50 mm thick.
- High-precision automotive light guides produced up to 1,300 mm in length.
- Two-color and three-color products manufactured in a single production run.
- 90,000 m² manufacturing facility, approximately 700 staff, and annual production capacity of 90,000,000 pieces per year.
- An R&D team of 50 staff and a portfolio of more than 167 patents, including 17 invention patents and 150 utility model patents.
- TS 16949 automotive industry technical specification certification and ISO 9001 quality management system certification.
Multi-cavity tooling is where optical molding usually fails in practice. A 5-micron cavity tolerance is only useful if every cavity in the tool holds it, and if the molding parameters are standardised across the tool. That is why cavity management and in-process control matter more than a single benchmark sample.
Step-by-Step: From Drawing to Mass Production
Custom optical components follow a defined workflow rather than an ad-hoc exchange of samples.
- Requirement confirmation. The buyer supplies 2D drawings, 3D files, optical data, material requirements, the intended application, and the service environment. Details cover product dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source information, material grade, working temperature, and relevant performance requirements.
- Engineering assessment. The supplier reviews manufacturability, cost, and development lead time against those inputs.
- DFM. Design for manufacturing evaluates optical surfaces, wall thickness, gates, ejector pins, parting lines, cavity quantity, shrinkage, and deformation.
- Quotation. Issued on the basis of the confirmed requirement and DFM findings.
- Mold development. Either a prototype mold or a production mold, depending on project phase.
- T0 sampling. First parts are molded from the new tool.
- Test and validation. Samples are validated for dimensions, optical performance, appearance, and assembly against the product specification.
- Optimization. Necessary mold or process adjustments are implemented based on test results.
- Customer approval. The mutually confirmed drawings, optical data, and DFM report become the baseline for production, managed under revision control so the same revision is used throughout the project.
- Mass production. Stable series production begins after approval.
Why revision control matters. When drawings, optical data, and DFM reports are revised independently, a mold can be cut to one revision while the quality plan references another. Locking a single revision across mold building, sampling, and mass production is the cheapest risk control available in a custom lens project.
Application Map: Which Lens Goes Where
The same molding platform serves very different optical duties. The mapping below reflects the application scope published for custom LED optics.
| Application | Typical lens construction | What the lens has to deliver |
|---|---|---|
| Automotive low beam | LB collimator; Low Beam Inner Lens | Sharp cutoff line, low glare, controlled light distribution, optical-grade PC or PMMA in a lightweight monolithic part |
| Automotive high beam | HB collimator; thick-wall headlamp lens | Long-range projection, focused spot, suppressed stray light, thermal stability with high-power LEDs |
| Automotive combined low and high beam | Combined Low and High Beam Headlamp Lens | Both beam functions in one lens, multi-zone free-form surfaces, reduced part count and module size |
| Automotive rear turn signal | Thick-wall optic for rear turn signal lamp | Thick-wall body with micro-prism edge structure, high brightness without dark zones, tight fit to the rear lamp lens |
| Automotive ambient lighting | Light guide | Even, soft illumination without bright spots; heat, UV, and vibration resistance |
| Street and outdoor lighting | Secondary optics for LED street lights | Controlled distribution, high transmittance, UV and thermal stability in continuous outdoor operation |
| Industrial high-bay / low-bay | Secondary LED optics | Uniform output and stable performance under sustained high drive currents |
| Security and surveillance lighting | Flood and area optics | Defined beam shape with even coverage over the target area |
| Stage and entertainment lighting | Moving-head and wash optics | Tight beam control across a 2°–120° spot-to-flood range |
| Projector and display lighting | Projection optics; Fresnel lens DB1072 | Collimation and compact, lightweight construction |
| Architectural and commercial lighting | Linear lens DB1102; Fresnel lens | Continuous uniform strips, slim integration, wall-washing distributions |
| Machine vision lighting | Linear lens DB1102; custom optical components | Repeatable, uniform illumination for imaging systems |
| Bicycle lighting | Bicycle Light Lens | Custom beam profiles — long-distance spotlight, wide flood, or custom-shaped beams matched to the luminaire design |
Machine vision, security camera, and UAV optical lenses sit in the same manufacturing family but serve imaging rather than illumination: the requirement shifts from light distribution to image quality, and the lens becomes part of the camera module rather than the luminaire.
How to Evaluate a Custom Optical Lens Supplier
Supplier evaluation should test capability to carry a project into stable mass production, not only capability to make a first sample.
- End-to-end competence. Optical design, structural evaluation, DFM, mold-flow analysis, mold design and fabrication, precision injection molding, optical testing, and production support under one roof.
- Comparable project history. Past custom projects and similar-product experience in complex optical surfaces, light guides, TIR lenses, projection lenses, thick-wall parts, or multi-cavity molds.
- Engineering depth. A stable engineering team, not a single contact person, plus documented project management from sampling to mass production.
- Equipment and capacity headroom. Whether actual injection-molding equipment and multi-cavity capability match the project, and whether critical equipment has spare capacity.
- Quality system and testing. Certification status, inspection of critical dimensions and optical performance, and in-process control.
- Supply continuity. Mold service life, raw-material supply stability, delivery lead time, abnormality response, and capacity expansion if order volumes grow.
Bicom Optics, for example, exports to the EU, USA, Middle East, Japan, and Korea, with export business accounting for 30% of total sales — a relevant signal when a project requires documentation and repeatable supply across markets rather than a single domestic delivery.
Frequently Asked Questions
What documents are required before a custom optical lens project starts?
Buyers generally need to provide 2D drawings, 3D files, optical data or specifications, material requirements, product application, and service environment. Details cover product dimensions, tolerances, optical surfaces, assembly requirements, surface roughness, light-source parameters, material grade, working temperature, and relevant performance requirements. These inputs let the supplier evaluate manufacturability, cost, and development lead time accurately — incomplete inputs are the most common reason a quotation cannot be finalised.
How can buyers verify a China custom optical lens manufacturer’s development capability?
Look beyond drawing-based production. A genuine development capability covers the full cycle from requirement definition to mass production: optical design, structural evaluation, DFM, mold-flow analysis, mold design and fabrication, precision injection molding, optical testing, and mass-production support. Verify past custom project references, similar-product experience, the engineering team, and the production equipment, and confirm whether the supplier can take part in joint product development rather than only manufacturing strictly to customer drawings. For projects involving complex optical surfaces, thick-wall parts, light guides, or multi-cavity molds, a supplier that understands both optical specifications and injection molding is the safer choice.
How is quality consistency controlled across batches and mold cavities?
Consistency is controlled across several links: raw materials, molds, injection-molding processes, dimensional inspection, optical performance, and appearance. Stable material supply, multi-cavity mold management, standardised injection-molding parameters, and inspection of critical dimensions and optical performance — supported by complete inspection standards and in-process control — keep product stable across different batches and cavities. Production traceability and continuous process monitoring are used to identify and mitigate potential quality risks early.
What does the sampling and approval process look like?
Custom optical components typically follow this workflow: requirement confirmation → engineering assessment → DFM → quotation → mold development → T0 sampling → test and validation → optimization → customer approval → mass production. A prototype mold or a production mold can be used depending on project phase and requirements. Once samples are complete, they are validated for dimensions, optical performance, appearance, and assembly against the specification; mold or process adjustments follow the test results, and stable mass production starts only after customer confirmation.
What supply capability matters for high-volume custom optical lens procurement?
Beyond development competence, assess long-term stable production and delivery: injection-molding equipment and actual production capacity, multi-cavity mold capability, mold service life, raw material supply, quality management system, testing capacity, production and engineering teams, delivery lead time, and abnormality response. Also confirm whether the supplier can expand capacity and guarantee supply against order growth, urgent demand, and long-term recurring procurement. Buyers can request a sample of a comparable lens type or submit drawings for a project-specific quotation to test these capabilities directly.
Conclusion
Choosing a custom optical lens is really a decision about three things: the optical specification, the mold that reproduces it, and the supplier that carries both into series production. Fix the light source, beam target, mechanical envelope, and environment first; then match the construction and material to those inputs; then verify that the supplier’s capability extends past the first sample.
Bicom Optics works on a product customization strategy with a “one product, one focus point” model, covering LED optical lenses, automotive lighting lenses, industrial lighting optics, machine vision lenses, security camera lenses, UAV optical lenses, optical lens molds, and custom optical components.
Request a sample or discuss your lens project
Send 2D drawings, 3D data, optical requirements, and the intended application, and the engineering team will assess manufacturability, tooling route, and development lead time.
Contact: Charlean He | Email: charlean@bicomoptics.com | Tel: +86 135-5877-5757
Address: No.258, West Yunsi Rd, Dayun Town, Jiashan County, Jiaxing City, Zhejiang Province, China | www.bicomoptics.com
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.