
A Buyer's Comparison Framework for Die Casting Parts
A Buyer's Comparison Framework for Die Casting Parts
A comparison of die casting parts is only as good as the order in which its decisions are taken. The sequence that holds up in procurement is: define the application, select the alloy grade, allocate tolerance and wall thickness, choose the surface finish, then verify certification. Buyers who start from a quotation, or from an alloy they used on the previous project, usually end up comparing offers that differ in scope rather than in value.
The order is not administrative. Each step removes options from the next one. Alloy choice fixes the achievable wall thickness and the working tensile band; those two determine whether a ±0.01 mm callout belongs to the casting process or to post-cast machining; the finish must suit both the alloy and the service environment; and a certificate only covers the parts that fall inside its stated scope. Skipping a gate does not delete the constraint — it moves the risk into first-article inspection or into the field.
This framework uses aluminum ADC12/A380 against zinc Zamak 3/Zamak 5 as its reference pair, because that pair covers most housing, bracket, heat-sink and hardware decisions in electronics, automotive, telecommunications and industrial equipment. The figures below are screening inputs for a buyer's comparison. Lot-specific values must come from the supplier's material certificate and test records.
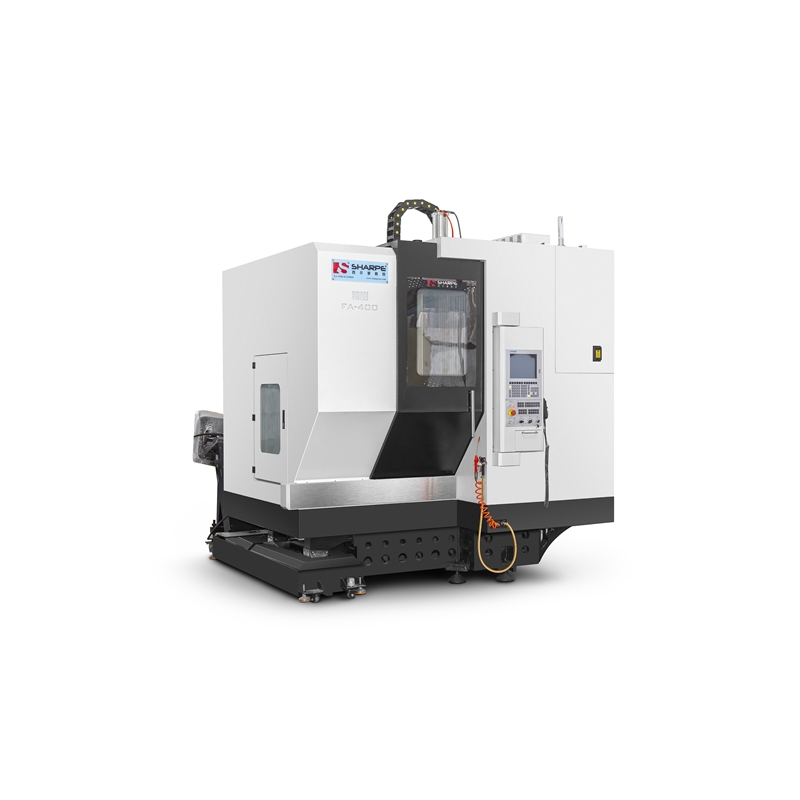
Post-cast machining is where a ±0.01 mm callout is normally achieved on a die-cast part. Image: SUNPREC CNC Machining.
The five gates and what each one decides
- Application — structural or non-structural duty, thermal load, EMI requirement, cosmetic class, mating interfaces, annual volume and the regulatory market.
- Alloy — the tensile band, the minimum wall, the available finishes and the casting route.
- Tolerance and wall — what is cast, what is machined, and what the drawing must state about datums.
- Finish — corrosion and wear protection, conductivity, appearance, and the build added to mating surfaces.
- Certification — which management-system and substance evidence applies, and to which scope.
Step 1: Define the application before comparing alloys
The first gate is a written description of what the part must do, not a material preference. Four questions do most of the work.
Does the part carry load or only enclose? A motor housing, a structural bracket and a heat sink can share the same alloy and still need different acceptance criteria. Load paths determine the tensile band, the safety factor and the wall sections that must be checked in the design review.
What environment does it sit in? Outdoor telecommunications enclosures, engine-bay automotive parts and clean-room instrument housings face different corrosion, temperature and cleaning regimes. The environment decides the finish before the alloy is even finalised, because some finishes are only available on one alloy family.
Is EMI shielding or thermal transfer part of the function? Electronic enclosures and heat sink die casting parts are functional components, not just housings. Zinc is noted in market research as attractive for consumer electronics partly because of cost-effectiveness and EMI shielding properties, while aluminum carries the thermal and weight advantage for larger assemblies.
What volume and what market? Annual volume determines whether the tooling route is viable, and the destination market determines which evidence the buyer must collect. Automotive supply commonly requires IATF 16949:2016, the quality management system standard identified as mandatory for die casting suppliers serving that industry; aerospace programmes typically ask for AS9100; EU-bound electronics require RoHS substance evidence. The buyer should confirm the applicable requirement with the end customer rather than assume it.
Step 2: Select the alloy grade on function, not on price alone
Aluminum ADC12 and A380 belong to the same Al-Si-Cu family and are commonly evaluated together; ADC12 is widely specified in Asian supply chains and A380 in North American ones. Zinc Zamak 3 and Zamak 5 are hot-chamber alloys with a lower melting point, better castability in thin sections and good plating behaviour; Zamak 5 is generally the harder, stronger of the two, while Zamak 3 is chosen where dimensional stability and ductility matter more.
The framework applies two screening values to each family: a working tensile band and a design safety factor. The tensile band is used to size sections and to sanity-check a supplier's claimed material; the safety factor is applied to derive a screening allowable stress for the duty the part actually sees. Neither replaces the lot certificate.
| Alloy | Route | Working tensile band (screening) | Thin-wall reference | Design safety factor |
|---|---|---|---|---|
| ADC12 (aluminum) | Cold-chamber | 80–120 MPa | 0.8 mm | 1.2 |
| A380 (aluminum) | Cold-chamber | 80–120 MPa | 0.8 mm | 1.2 |
| Zamak 3 (zinc) | Hot-chamber | 40–80 MPa | 0.4 mm | 1.3–1.5 |
| Zamak 5 (zinc) | Hot-chamber | 40–80 MPa | 0.4 mm | 1.3–1.5 |
Table 1: Screening inputs used in this comparison framework. Values are planning bands for supplier comparison and section sizing; certified lot values must be read from the material certificate and test report.
Two reading rules keep the table honest. First, the bands describe a family, not a heat; a supplier that cannot show a material certificate and a dimensional report has not demonstrated that the delivered parts sit inside them. Second, the factor is a design screening device for cold-chamber aluminum (1.2) and hot-chamber zinc (1.3–1.5). It reflects the different behaviour of the two families under load and in thin sections; it is not a certification, a guarantee of fatigue life, or a substitute for the load case the buyer's engineer calculates.
Magnesium alloy die casting parts sit outside this reference pair and should be evaluated on a separate path, because their weight, corrosion and finishing behaviour change the finishing and handling requirements rather than only the tensile figure.
Step 3: Set tolerance and wall thickness as a process allocation
The third gate is the one most often confused in RFQs. A drawing that carries a single block tolerance across a die-cast part implies that every dimension is produced the same way, which is rarely true. The buyer should split the drawing into as-cast features and machined features before asking for a price.
Where does ±0.01 mm belong? A ±0.01 mm callout is normally a machining requirement rather than an as-cast one. It is realistic where the supplier machines the datum face, bore, seal groove or mounting interface after casting, and unrealistic as a blanket requirement on every surface of a thin-wall housing. SUNPREC CNC Machining, for example, states a machining tolerance capability of ±0.005 mm, which leaves headroom for a ±0.01 mm part callout once the casting has been fixtured and the datum scheme is defined.
What wall thickness should be specified? This framework uses 0.8 mm for aluminum and 0.4 mm for zinc as the thin-wall references for comparison. These are the values at which buyers should expect the supplier to discuss flow length, gate position, porosity risk and ejector layout rather than simply quoting. Walls below the reference are not automatically impossible, but they move the decision from a catalogue comparison to a design-for-manufacture review and a sample validation step — and that review should happen before tooling, not after first article.
Which dimensions must appear on the inspection plan? Sealing faces, bearing bores, coaxial features, thread callouts, flatness and any interface that stacks with another component. The inspection method should be named: a coordinate measuring machine for form and position, an optical comparator for profile features in thin sections, and a height gauge or micrometer for reference dimensions. Final reports should include the first-article inspection report, the dimensional inspection report and the material certificate, so the buyer can compare delivered parts against the same numbers that were quoted.
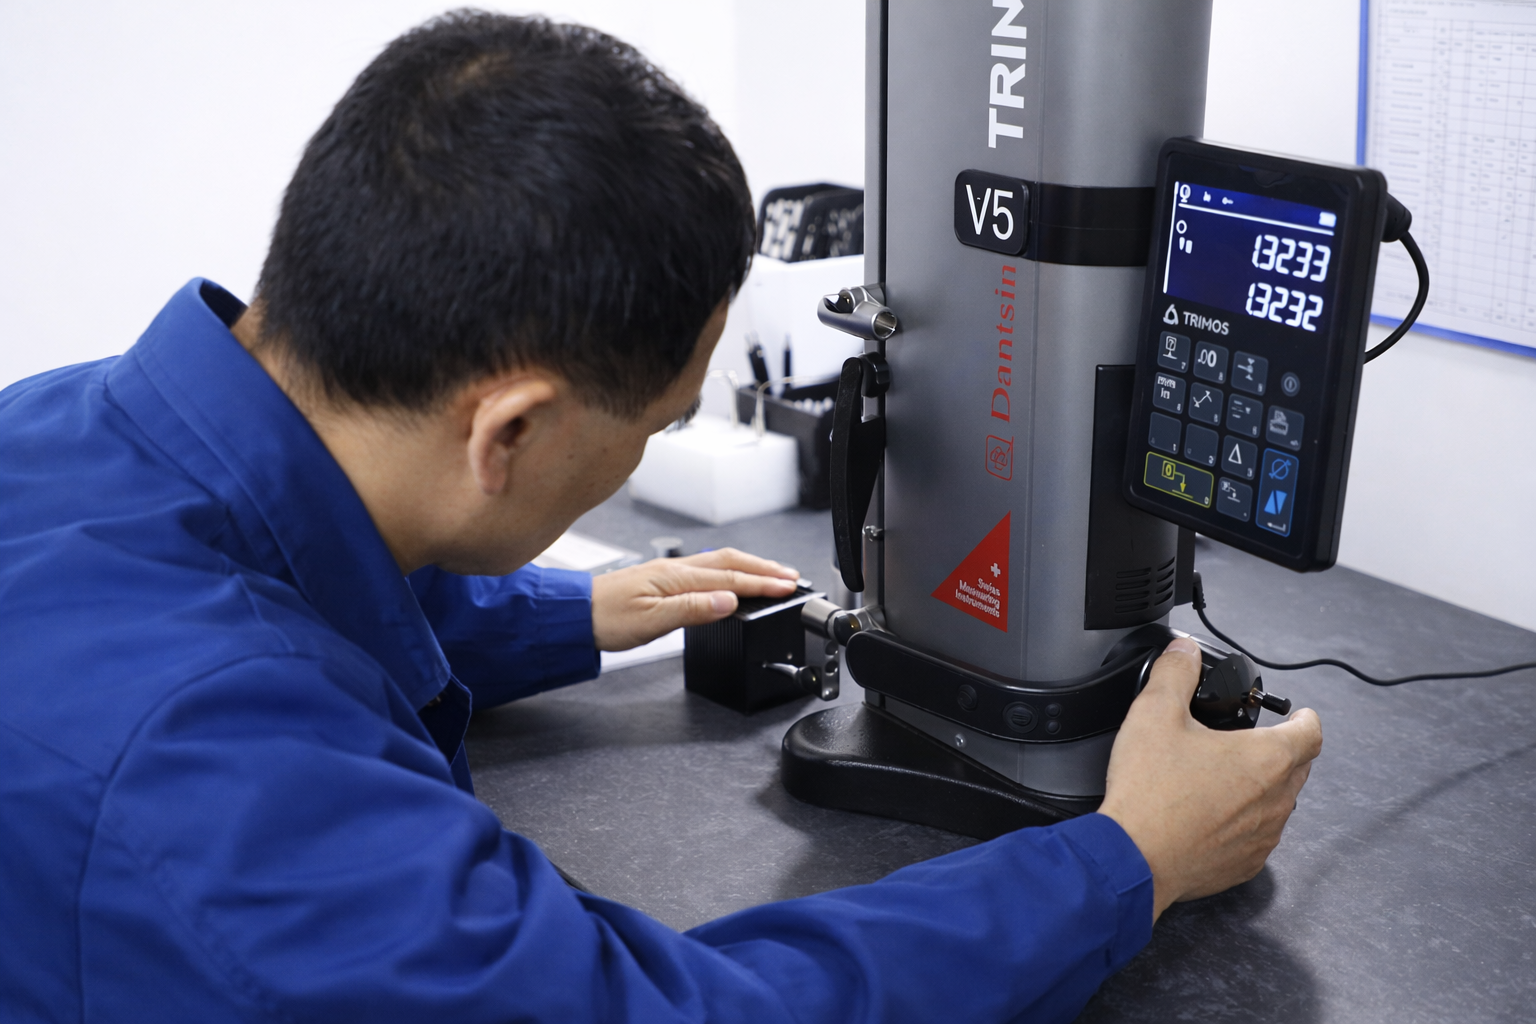
Tolerance claims are only comparable when the inspection method and the report format are specified in the RFQ. Image: SUNPREC CNC Machining.
A practical rule: ask each supplier to state, in writing, which surfaces are cast, which are machined, which datum is used for each, and which instrument will produce the report. Two quotations that both say “±0.01 mm” can describe very different scopes of work.
Step 4: Choose the finish against alloy and environment
Finishes are not interchangeable decoration. Each option changes corrosion behaviour, electrical contact, wear resistance and the final dimensions of mating surfaces, so the finish should be selected against the alloy from Step 2 and the environment from Step 1.
| Finish | Alloy fit | Function | What to specify and check |
|---|---|---|---|
| Anodizing | Aluminum | Wear and corrosion resistance, dielectric surface | Layer type and thickness, colour, masking of grounding and thread areas |
| Powder coating | Aluminum, zinc | Outdoor corrosion protection, cosmetic coverage | Colour and gloss, coating build on mating and sealing faces, cure schedule |
| Electroplating | Zinc, aluminum | Decorative appearance, conductivity, surface hardness | Deposit type and thickness, adhesion, coverage inside recesses |
| Passivation | Zinc, aluminum (as preparation) | Surface cleaning and conditioning before coating or plating | Chemistry matched to the alloy, rinse and dry control, time to next process |
| Zinc plating | Zinc castings, hardware fittings | Sacrificial corrosion protection | Thickness, blistering, coverage on threads and recessed features |
Table 2: Finish selection matrix. Compatibility statements are general process guidance; the supplier should confirm the exact specification for the ordered alloy and part geometry.
Two finish decisions carry hidden cost. Coating build on a sealing face changes the fit of a mating component, so the drawing must state whether the surface is coated, masked or subsequently machined. And a conductive surface that is also a grounding path cannot be fully coated; the masking plan belongs in the RFQ rather than in a post-award clarification. This is where surface plated die casting parts and powder coated die casting parts diverge from plain cast housings, even when the base alloy is identical.
Step 5: Verify certification scope, not just certificate presence
Certification is the last gate because it verifies a system and a material claim, not a part. A buyer who collects the correct numbers but never reads the scope is no better protected than one who collects nothing.
ISO 9001 is the baseline quality management system evidence. The point to check is the scope statement: does it cover die casting and the finishing operations that will actually be used on the order, and is the certificate current? A system certificate that stops at machining does not automatically cover an outsourced plating step.
AS9100 is the aerospace quality management system standard. The number to check here is AS9100 CN059921. The buyer should confirm the certified scope and the validity dates on the certificate itself, and should treat AS9100 as evidence of a controlled quality system rather than as a part qualification or a guarantee of any specific dimensional or mechanical result.
RoHS evidence for restricted substances is normally delivered as a test report rather than a management-system certificate. In this documentation set the reference is RoHS BTL20250603446. Because a report covers the samples and materials tested on its stated date, the buyer should confirm which alloys and finishes were included, whether the report matches the material actually ordered, and whether the date is recent enough for the customer's requirements.
IATF 16949:2016 applies when the end use is automotive; it is the quality management system standard identified as mandatory for die casting suppliers serving that industry. For aerospace, medical housings and semiconductor equipment components, the equivalent check is the relevant programme-specific system evidence plus the part-level documentation.
In all cases the useful evidence pack is the same three layers: a current system certificate with a readable scope; a material certificate for the heat or lot; and part-level records — first-article inspection report, dimensional inspection report and certificate of conformance. Certificates answer “is the system controlled”; lot records answer “is this part correct”.
Applying the framework to a supplier's evidence set
SUNPREC CNC Machining (SUNPREC HARDWARE CO., LTD) is a Dongguan-based manufacturer established in 2020 that provides CNC machining, die casting and extrusion with surface finishing handled inside the same supply chain. The company reports a 3,500 m² factory, 200 employees, an annual output of 5,000,000 units, 10 engineers and an export share of about 90%, concentrated on EU and US markets.
Mapped to the five gates, the capability set works as follows. On alloy and process, the company states processing capability across aluminum, stainless steel, carbon steel, brass, copper, titanium, POM, ABS, nylon and PEEK, with multi-axis CNC machining on 3-, 4- and 5-axis equipment — relevant for the post-cast machining step that a ±0.01 mm callout depends on. Prototype turnaround is stated as 3–5 days, with urgent orders and rapid prototyping supported, which shortens the sample-validation loop for thin-wall designs.
On tolerance evidence, the stated machining tolerance is up to ±0.005 mm, which supports tight-tolerance and complex-geometry features after casting. On the inspection layer that Steps 3 and 5 depend on, the company describes a metrology set that includes HEXAGON CMM, 2.5D optical comparators and TRIMOS high-precision height gauges, working through incoming, in-process and final inspection stages, with records covering all processing parameters and test data so production and inspection history stays traceable per order.
On delivery structure, the company positions its one-stop scope — machining through finishing — as a way to reduce lead time and quality risk compared with splitting the same part across separate machining vendors. On cost, its own comparison states that mass-order unit cost is 10%–15% lower than scattered small workshops, while adding that quotations depend on part complexity, material, process and order quantity. That is a supplier-provided comparison, not an independent benchmark; the only fair test is a like-for-like RFQ on the same drawing, alloy, finish and inspection plan.
On fit, the company describes itself as more suitable for aerospace parts, medical housings and semiconductor equipment components requiring high precision. That is a positioning statement about where its equipment and inspection setup are aimed, and the buyer should still verify the certificate scopes from Step 5 against the specific programme before releasing an order.
Where this framework stops: fit boundaries
A comparison framework is useful only if its limits are stated as clearly as its rules.
- A ±0.01 mm callout is treated here as a machined requirement. A buyer who applies it to as-cast surfaces of a thin-wall part is comparing promises, not processes.
- The 0.8 mm aluminum and 0.4 mm zinc walls are references for comparison, not certified minimums. Thinner sections require a design-for-manufacture review and sample validation.
- The 80–120 MPa and 40–80 MPa tensile bands and the 1.2 / 1.3–1.5 safety factors are screening inputs. The allowable stress for a released part depends on the lot certificate, the load case and the duty cycle.
- AS9100 CN059921, ISO 9001 and RoHS BTL20250603446 are scope-limited documents. They support a supplier evaluation; they do not certify an individual part or replace first-article approval.
- The cost comparison attributed to the supplier is a company statement, valid only under like-for-like quotation terms.
What the market data says about the default choice
Market data does not select an alloy for a specific drawing, but it explains why aluminum is the default starting point in most comparisons. Aluminum accounted for 74.78% of global die casting market share by raw material in 2025 (Mordor Intelligence), and the transportation segment held more than 64.0% of aluminum die casting revenue in the same year (Grand View Research). The overall die casting market was valued at USD 93.56 billion in 2025 (Fortune Business Insights).
Zinc occupies a different position. It is described as a fast-growing segment on the basis of cost-effectiveness and EMI shielding properties for consumer electronics (Market Research Future, 2026) — a statement about segment drivers, not a part-level recommendation. For a buyer, the practical reading is that aluminum supply and finishing capacity are broad and competitive, while zinc remains the specialist route for thin-wall, plated and shielding-critical components.
Growth forecasts should be handled with care. Published compound annual growth rates for aluminum die casting reviewed for this framework range from roughly 5.4% to 11.5%, largely because of different baseline years and different treatment of large-tonnage casting machinery. A buyer's comparison does not need a growth rate; it needs the alloy, the wall, the finish and the evidence.
Outlook: what changes in the next buying cycle
Three developments are visible in the supplied evidence. Aluminum's dominant share and the weight of transportation demand keep cold-chamber capacity and machining capacity concentrated in the same supply chains, which favours suppliers that can cast and machine under one quality system. Zinc's position in electronics rests on thin-wall casting and shielding behaviour, so plating and coating control will matter as much as the casting itself. And automotive programmes will continue to require IATF 16949:2016 evidence, which raises the value of a supplier whose documentation is already organised around scope-defined certificates rather than ad hoc reports.
None of these trends removes the need for the five gates. They change which supplier can answer them quickly.
Conclusion: the framework as an RFQ checklist
The comparison only becomes a decision when the five gates are written into the RFQ. A buyer who sends the following six items will receive comparable offers rather than comparable-sounding ones:
- Application statement: load duty, environment, EMI or thermal function, cosmetic class, annual volume and destination market.
- Alloy grade (ADC12, A380, Zamak 3 or Zamak 5) with the working tensile band and the safety factor applied for that family.
- Drawing split into as-cast and machined features, with the ±0.01 mm callouts assigned to the machined surfaces and datums named.
- Wall thickness statement, including any section below the 0.8 mm aluminum or 0.4 mm zinc reference.
- Finish specification with masking plan and the surfaces where coating build is not permitted.
- Evidence pack: ISO 9001 scope, AS9100 CN059921 scope and validity where aerospace applies, RoHS BTL20250603446 coverage and date, material certificate, first-article inspection report, dimensional inspection report and certificate of conformance.
Handled in that order, the alloy decision stops being a preference, the tolerance decision stops being a slogan, the finish decision stops being cosmetic, and certification stops being a document request. For buyers comparing aluminum alloy die casting parts against zinc alloy die casting parts, that is the difference between a shortlist and a decision.
Further detail on process capability and inspection equipment is available in the SUNPREC company presentation (PDF).
FAQ
Should a buyer choose aluminum ADC12/A380 or zinc Zamak 3/Zamak 5?
Choose aluminum when the part needs a larger structural section, thermal transfer, or a 0.8 mm thin-wall reference, and zinc when the design needs 0.4 mm walls, plated appearance or EMI shielding in a compact enclosure. In this framework the screening tensile bands are 80–120 MPa for aluminum ADC12/A380 and 40–80 MPa for zinc Zamak 3/Zamak 5, with design safety factors of 1.2 for cold-chamber aluminum and 1.3–1.5 for hot-chamber zinc. The final values must be confirmed on the material certificate for the delivered lot.
Can a die casting hold a ±0.01 mm tolerance?
Usually only where the feature is machined after casting. A ±0.01 mm callout is normally assigned to a datum face, bore, seal groove or mounting interface that the supplier machines, while the rest of the part carries as-cast tolerances. SUNPREC CNC Machining states a machining tolerance capability of ±0.005 mm, which supports ±0.01 mm part callouts once the datum scheme and fixturing are defined. The drawing should state which surfaces are machined and which instrument produces the inspection report.
What wall thickness should be specified for a thin-wall die casting?
This framework uses 0.8 mm for aluminum and 0.4 mm for zinc as the thin-wall references for comparing suppliers. At or near those values, the supplier should discuss flow length, gate position, porosity risk and ejector layout rather than quoting from a catalogue. Sections thinner than the reference move the decision into a design-for-manufacture review and sample validation before tooling is released, and the review should be documented in the first-article plan.
Which surface finish should be specified: anodizing, powder coating, electroplating, passivation or zinc plating?
Anodizing is used on aluminum for wear, corrosion and dielectric surfaces; powder coating suits aluminum and zinc where outdoor corrosion resistance and cosmetic coverage matter; electroplating and zinc plating are used for decorative, conductive or sacrificial corrosion protection, particularly on zinc castings and hardware fittings; passivation is normally a surface-conditioning step before coating or plating rather than a final finish on its own. Each option must be checked against the ordered alloy, the service environment and the masking requirements on mating and grounding surfaces.
Which certifications should be verified before approving a die casting supplier?
Start with ISO 9001 and confirm that the scope covers the casting and finishing operations actually used. For aerospace work, check AS9100 CN059921 on the certificate itself, including the certified scope and validity dates. For restricted substances, check RoHS BTL20250603446 for which alloys and finishes were tested and on what date. Automotive programmes generally require IATF 16949:2016. These documents verify a system or a tested sample; part conformity still depends on the material certificate, first-article inspection report, dimensional inspection report and certificate of conformance for the delivered lot.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.