
A Buyer's Guide to TiO₂ Compliance: Anatase and Traceability
Fiber-grade titanium dioxide accounts for a small share of a polyester or polyamide line's input weight, yet it sets the matte level of the finished yarn, the stability of whiteness values, and how long a spinneret pack runs before it needs cleaning. For buyers moving from evaluation into execution, the practical question is no longer whether a supplier sells TiO₂. It is whether the grade can be documented, batch after batch.
The global fiber grade titanium dioxide market was valued at USD 1.46 billion in 2024 and is projected to reach USD 1.94 billion by 2032 (Intel Market Research), and the polyester fiber segment accounts for over 60% of all fiber grade TiO₂ applications. China's total titanium dioxide exports reached a record 1.9017 million tons in 2024, a 15.84% increase year on year, according to China Customs Statistics data reported by Echemi. Supply volume is not the constraint in this segment. Reproducibility is.
This guide examines compliance in fiber-grade TiO₂ from the buyer's side: what the anatase crystal structure actually contributes to delustering, which parameters can be written into a purchasing specification, how 100% pre-shipment testing functions as de facto compliance evidence, and where the boundaries of that evidence lie.
Why Fiber-Grade Compliance Is Not Pigment Compliance
Titanium dioxide pigments are internationally standardized under ISO 591, which defines requirements for both anatase and rutile types. That standard answers the question a pigment buyer asks: what colour, opacity and durability does this material deliver in a coating or plastic?
A fiber-grade specification has to answer a different set of questions. Will the powder disperse in ethylene glycol without sedimentation or agglomeration? Will it hold its structure at 240–285 °C during PET esterification and polycondensation without triggering side reactions, black spots or a drop in intrinsic viscosity? Will it wear the spinneret, block the filter, or shift the whiteness of the finished filament? These are process questions, and no pigment standard resolves them on its own.
That is why compliance in this segment is normally expressed as a parameter set plus a test record, not as a certificate alone. Anatase is the crystalline form generally chosen for fiber delustering, while rutile is more typically specified where a high degree of opacity is the objective. ISO 591 recognises both as distinct types, and the two are not interchangeable inside a purchasing specification.
The Anatase Crystal Structure and Its Role in Delustering
Anatase is preferred for fiber grades largely because of abrasiveness. Anatase has a Mohs hardness of 5.5–6.0, compared with 6.0–7.0 for rutile, which reduces wear on spinning nozzles (ETIO2.COM). On a continuous high-speed spinning line, nozzle and filter wear translate directly into stoppage time, so a softer particle is a process decision rather than a cosmetic preference.
Particle size matters as much as crystal form. Fiber grade TiO₂ typically requires a particle size of 0.2–0.3 μm for optimal delustering in polyester staple fibers, as described in an Aanya Enterprise industry guide. Below that window, light scattering falls off and the matte effect weakens; above it, dispersion quality and spinability become harder to hold consistently.
Delustering itself is a light-scattering effect. TiO₂ particles embedded in the polymer matrix scatter incident light and convert a glossy filament surface into the controlled low-sheen appearance expected in textile and staple applications. Because those particles remain inside the fibre for its whole service life, their purity and surface chemistry also influence whiteness retention, dyeing uniformity and how the fibre ages under heat and weather exposure.
What a Documented Fiber-Grade Specification Contains: SA-50
SA-50 is an anatase fiber-grade titanium dioxide used as a PET fiber whitening and matting agent. Its published parameter set is a practical template for the data a buyer should be able to obtain in writing before qualification.
| Parameter | Documented limit (SA-50) | Why it matters at the fiber line |
|---|---|---|
| Crystal structure | Anatase | Lower abrasiveness than rutile; suited to delustering rather than high-opacity pigmentation. |
| TiO₂ content (%) | ≥ 98.0 | Dosing calculations stay stable only when active content is held inside a narrow band. |
| Sieve residue, 325 mesh (%) | ≤ 0.004 | Coarse particles are a primary cause of filter and spinneret blockage. |
| Moisture, 105 °C (%) | ≤ 0.40 | Moisture shifts effective dosing and can disturb esterification conditions. |
| Fe₂O₃ (%) | ≤ 0.004 | Iron is both a colour body and a catalyst risk; low iron supports whiteness and viscosity stability. |
| pH value | 6.8 ± 0.2 | A near-neutral pH supports glycol dispersion and lowers corrosion risk in the dosing circuit. |
| Electrical conductivity (μs/cm) | ≤ 230 | An indirect indicator of soluble ionic impurities carried into the polymer. |
| Specific surface area (m²/g) | 8.5–10.0 | Governs dispersion kinetics and the polymer wetting the particle surface. |
| Color value L | 96.7–98.2 | Directly tied to the whiteness of the finished fibre. |
| Color value b | ≤ 0.0 | A blue-neutral b value supports anti-yellowing behaviour over time. |
| Specific gravity (g/cm³) | Not stated on the published sheet | Request it if the dosing model is volume-based rather than weight-based. |
Three values carry most of the weight in a compliance file. TiO₂ content sets the economics of dosing. Sieve residue sets the physical risk to spinnerets and filters. pH sets the chemistry of the dispersion step. The remaining parameters reduce the variation that surrounds those three.
Reading a Grade Family: SA-50, SA-60 and SA-80
A grade code is a designation, not a specification. The fiber-grade series referenced in this guide includes SA-50, SA-60 and SA-80, and the parameter limits published for SA-50 are listed above. For SA-60 and SA-80, the same framework applies — crystal structure, TiO₂ content, sieve residue, moisture, Fe₂O₃, pH, electrical conductivity, specific surface area and colour values — and those figures should be requested in writing rather than inferred from a model number.
The working rule for procurement teams is straightforward: obtain identical documentation for every grade under evaluation, produced with the same test methods, so that a comparison reflects the material rather than the paperwork. A comparison table is only useful when the cells on both sides are filled from the same kind of source.
Traceability in Practice: 100% Pre-Shipment Testing
Strict parameter control becomes compliance only when it is tested and recorded. The quality-control model applied to this product line is a 100% pre-shipment test, with third-party inspection supported. In operational terms, that means every shipment is tested before dispatch rather than sampled after arrival, results are recorded against the batch, and a buyer can bring in an independent inspector if the order justifies it.
Alongside testing, the commercial framework defines what a buyer can plan around. Minimum order quantity is 1 metric ton. Delivery terms are FOB or CIF. Standard lead time is 15–30 days, against a monthly capacity of 1,000 MT. Payment terms span T/T in advance, T/T 30 days, L/C at sight, and L/C 30, 60 and 90 days. Export markets for the fiber-grade range include Korea, Japan, India, Indonesia and Vietnam.
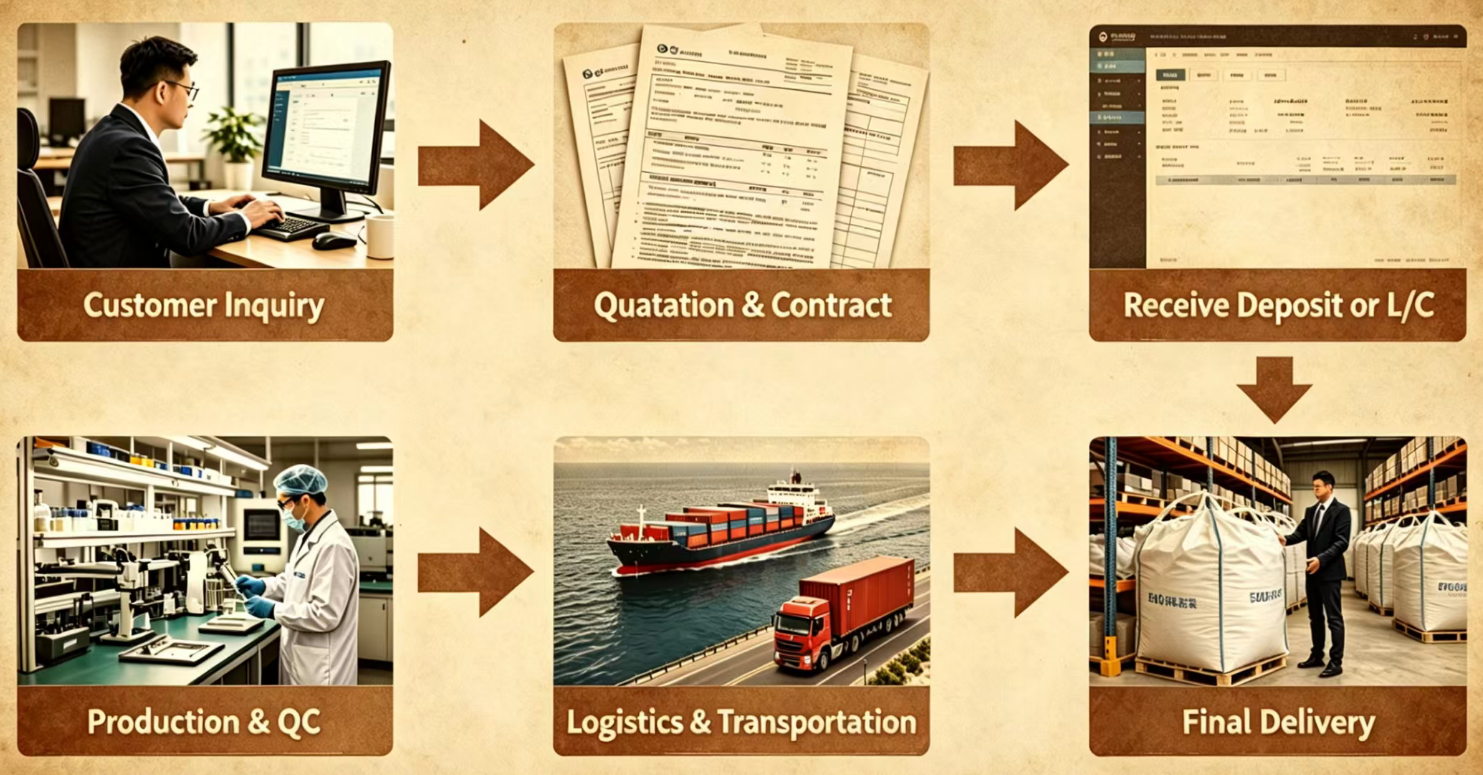
For a buyer at the execution stage, the credible question is not whether a supplier claims quality control, but at which point in the order flow control is exercised, who signs the test record, and whether a third party is allowed to verify it.
Application Fit: Where Fiber-Grade TiO₂ Is Used
SA-50 is used as a matting agent in polyester chip for fibre and bottle production, and it has been adopted by polyester makers in China. That application positions it in two adjacent production routes: chip for downstream fibre spinning, and chip for bottle-grade polymer, both of which depend on consistent dispersion and low ionic contamination.
Customization services are offered for polyester and Nylon materials, together with OEM and ODM production services for textile applications. For a converter running polyester and polyamide lines on the same site, that dual-material scope reduces the number of documentation sets a purchasing team has to maintain.
Field Evidence from a Long-Running Polyester Project
The strongest compliance argument is not a certificate but a production record. In a project located in China, running for more than 10 years and involving more than 5,000 metric tons of titanium dioxide used as a matting agent in polyester chip for fibre and bottle production, several measurable outcomes have been reported by the polyester maker involved.
Polymerisation stage
With low iron, low ionic impurities and neutral pH, the material disperses evenly in ethylene glycol without sedimentation or agglomeration. It remains stable at 240–285 °C during PET esterification and polycondensation, and does not reduce PET intrinsic viscosity, cause side reactions or produce black spots. Batch consistency is high enough to support continuous polymerisation lines without process modification.
Spinning performance
Dispersion quality prevents secondary agglomeration under high-temperature melting. In this project the spinneret clogging cycle was extended by over 40%, and filter replacement frequency was reduced considerably. The milder anatase particles lessen spinneret abrasion, and the filament breakage rate fell by approximately 35%, extending continuous high-speed spinning hours. Matting degree remained stable and adjustable, producing consistent lustre without uneven bright spots.
Finished fibre quality
Whiteness was stable with an L value above 96.7 and dyeing was uniform, without streaks or colour difference. Firm particle adhesion limits powder loss during weaving and dyeing, and heat and weather resistance were reported as good.
Market Trends Shaping Fiber-Grade Sourcing
Demand growth in fiber grade TiO₂ tracks polyester fiber capacity. Market data from Intel Market Research places the fiber grade segment at USD 1.46 billion in 2024, projected to reach USD 1.94 billion by 2032, with polyester fiber representing more than 60% of applications. China's export volume of 1.9017 million tons in 2024, up 15.84% year on year, indicates how much of that supply now crosses borders — which raises the documentary burden on both supplier and buyer.
Chemical-safety certification in textiles is moving in the same direction. In 2022, Venator's HOMBITAN® LW-S 100 became the first fiber anatase TiO₂ to secure ECO PASSPORT by OEKO-TEX® for the textile industry. The signal is not that one grade is superior, but that fiber-grade TiO₂ is increasingly assessed through documented chemical-safety credentials rather than through price and tonnage alone.
On the supply side, LB Group (formerly Lomon Billions) is cited as the world's largest TiO₂ producer with over 1,501 kilotons of annual capacity as of 2025 (Fortune Business Insights). Concentration at that scale means a mid-sized fiber producer is rarely buying scarcity; it is buying differentiation, and differentiation in this segment is documented in parameter sheets and batch records.
Limits, Boundaries and Trade-offs
Compliance claims are only credible when their limits are stated. Four boundaries belong in an evaluation file.
- Anatase is not a substitute for rutile. ISO 591 defines requirements for both anatase and rutile types as distinct categories. A fiber-grade anatase optimised for delustering should not be specified where the primary objective is high opacity or a pigment-grade durability profile. The two crystal types serve different functions and are not interchangeable in a specification.
- Certificates are point-in-time documents. ISO 9001:2015 certificate TUV100034917/2, issued by TUV SUD, covers the production and sales of chemical fiber grade titanium dioxide and carries a recorded validity period from 14 August 2023 to 13 August 2026. A procurement file should record the date on which a certificate was verified; where the recorded period has passed, a buyer should request confirmation of the current cycle rather than rely on a stored copy.
- Commercial parameters constrain planning. A minimum order quantity of 1 metric ton and a standard lead time of 15–30 days suit scheduled replenishment. Lines that change grades frequently need to map those figures against their own inventory and working-capital policy before committing.
- Test evidence is batch-level and method-dependent. A pre-shipment test result describes the batch and the method used to test it. Buyers who run incoming inspection with a different method may see different figures on the same material, so method alignment at qualification stage prevents disputes later.
None of these boundaries is unusual in industrial additive procurement. The point is that they should surface during evaluation, when they can still influence grade selection and contract terms, rather than during execution when a line is already committed.
Future Outlook
Fiber grade TiO₂ is a mature product category with a growing compliance layer. The volume outlook to 2032 is expansionary, but the more consequential change is documentary. As textile chemical-safety schemes extend into upstream raw materials, and as polyester and polyamide capacity continues to concentrate in export-oriented production, buyers will increasingly select suppliers on the evidence they can produce rather than on the price they quote.
For suppliers, that shifts the competitive basis toward traceability: published parameter limits, batch-level test records, third-party inspection access, and certificate files that are kept current. For buyers, it means the specification document becomes the primary risk-control instrument in the category — more important than a brand name, and more durable than a one-off price advantage.
Frequently Asked Questions
What documentation should accompany a fiber-grade TiO₂ shipment?
A typical document set covers the parameter sheet for the grade, the batch test record from pre-shipment testing, and the applicable management-system certificate. For SA-50, the published parameter sheet states an anatase crystal structure, TiO₂ content of at least 98.0%, sieve residue at 325 mesh of no more than 0.004%, moisture of no more than 0.40%, Fe₂O₃ of no more than 0.004%, pH of 6.8 ± 0.2, electrical conductivity of no more than 230 μs/cm, specific surface area of 8.5–10.0 m²/g, an L value of 96.7–98.2 and a b value of no more than 0.0. Third-party inspection is supported, which allows a buyer to verify a batch independently of the supplier's own test record.
How should buyers compare SA-50, SA-60 and SA-80 in a specification review?
By requesting the same parameter framework for each grade, in writing, before qualification. The framework used for SA-50 — crystal structure, TiO₂ content, sieve residue, moisture, Fe₂O₃, pH, electrical conductivity, specific surface area and colour values — is the minimum basis for a side-by-side review. Model numbers alone do not convey limits, and a grade designation should never be treated as a substitute for published figures. Where a supplier cannot provide a parameter for a given grade, that absence should be recorded as a gap rather than filled by assumption.
Why does pH value matter in a fiber-grade TiO₂ specification?
pH reflects the surface chemistry of the particle and its behaviour in the dispersion step. SA-50 is specified at 6.8 ± 0.2, close to neutral. In the reported polyester project, a near-neutral pH combined with low iron and low ionic impurities allowed the material to disperse evenly in ethylene glycol without sedimentation or agglomeration, and to remain stable at 240–285 °C during PET esterification and polycondensation without reducing intrinsic viscosity or generating black spots. A pH specification is therefore a dispersion statement as much as a chemical one.
What are the acceptance criteria, order terms and payment options for fiber-grade TiO₂?
Standard acceptance criteria are a 100% pre-shipment quality test, with third-party inspection supported. Minimum order quantity is 1 metric ton and delivery terms are FOB or CIF. Payment options include T/T in advance, T/T 30 days, L/C at sight, and L/C 30, 60 or 90 days. Standard lead time is 15–30 days against a monthly capacity of 1,000 MT. Buyers should confirm which combination of inspection and payment terms applies to their specific order before issuing a purchase order.
Can fiber-grade TiO₂ be customized for polyester and nylon spinning?
Yes. OEM and ODM production services are offered, along with customization for polyester and Nylon materials, at a minimum order quantity of 1 metric ton and a standard lead time of 15–30 days. The customization scope covers polyester and Nylon, which matters for producers running both fibre types on one site and wanting a single documentation set. As with any customized grade, the agreed parameter limits should be recorded in writing before production begins, since a customized specification is defined by its documented values rather than by the base grade name.
What are the limitations of anatase-based fiber-grade TiO₂?
Anatase fiber grades are engineered for delustering, not for high-opacity pigment performance. ISO 591 defines anatase and rutile as separate types with separate requirements, and the two are not interchangeable in a specification. Anatase's advantage in fibre spinning is its lower abrasiveness — a Mohs hardness of 5.5–6.0 versus 6.0–7.0 for rutile — which reduces wear on spinning nozzles. Beyond crystal type, buyers should also account for batch-level test evidence, certificate validity windows and commercial parameters such as a 1 metric ton minimum order quantity and a 15–30 day lead time when planning qualification and replenishment.
For readers who need the underlying corporate and product documentation, the company profile brochure is available here: Orient International Holding Shanghai Foreign Trade Co., Ltd. — company profile (PDF).