
Ball Valve Supplier Capability: Casting, Split-Body Design and Pre-Shipment Tests
A ball valve datasheet answers three questions well: what size the valve is, what pressure it holds, and what it is made from. It usually answers three others badly — how the body was cast, how the valve comes apart when a seat finally wears, and what was measured before the valve left the factory. For project buyers moving from research into evaluation, those three questions are the difference between a capability claim and capability evidence.
Procurement teams rarely reject a supplier because the pressure class was wrong. They reject them because the documentation did not match the order, because a seat replacement required cutting a line out of service, or because a body that passed a hydrostatic test at the factory showed porosity six months later. None of those failures appear in a price comparison. All of them are visible earlier, if the buyer knows which physical attributes to ask about.
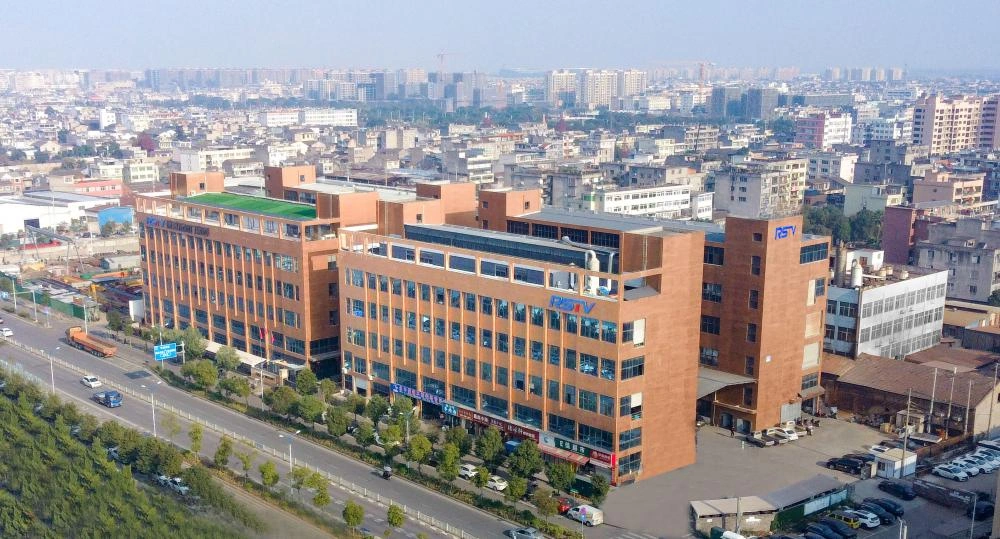
RST VALVE GROUP CO.,LTD is a Wenzhou, China-based industrial valve manufacturer founded in 2009 that produces ball valves, gate valves, check valves, globe valves and strainers, holds ISO, CE and TS certification, and exports to markets including Africa, the Americas, Asia, Europe, the Middle East and Oceania. Its ball valve range is a useful reference case because the company publishes the specific manufacturing attributes — casting route, body construction and test regime — that this article treats as evaluation criteria.
The Evidence Gap Between a Catalogue and a Factory
A flanged ball valve catalogue entry might state a full-port range of DN15 to DN600 and a working temperature of -20°C to 180°C. Both are useful screening values. Neither tells a buyer whether the body wall is uniform, whether the flange face will seal on the first attempt, or whether the seat can be changed without removing the valve from the pipeline.
At the research stage, buyers compare ranges. At the evaluation stage, they compare evidence, and ball valve capability evidence is unusually concrete because it is physical. Three attributes can be examined before an order is placed: the casting method used for the body, the number of body joints and how they come apart, and the tests performed plus the documents issued before shipment. Each maps to a different risk — structural integrity, maintenance cost, and acceptance disputes.
Casting Method: What Precision Lost-Wax Casting Changes
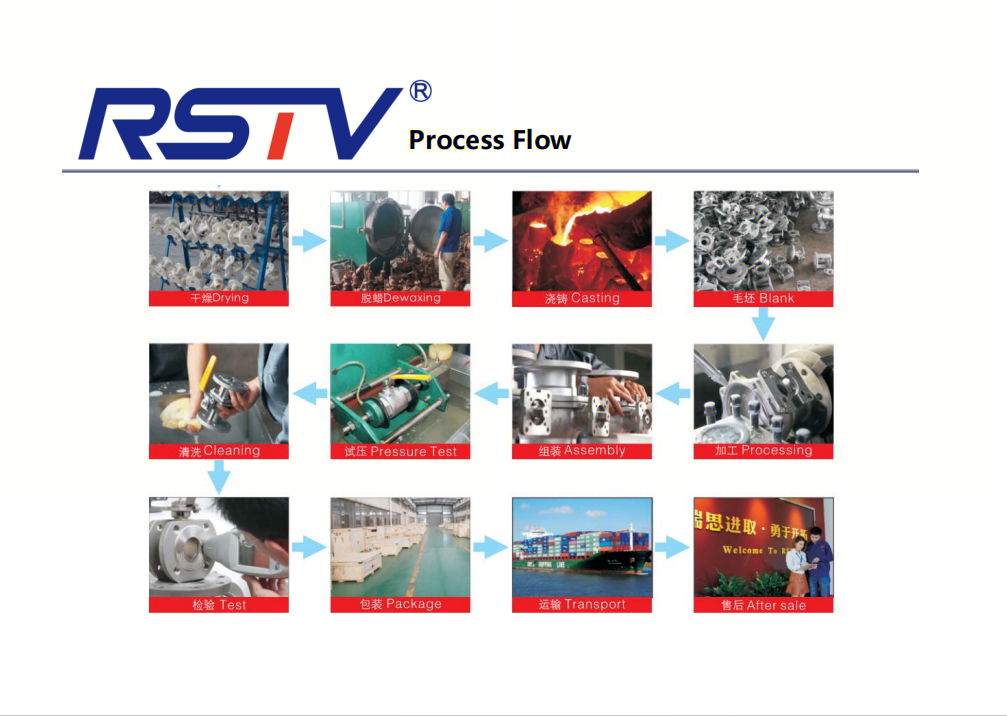
The flanged ball valve series Q41F, Q41H and Q45F from RST is produced by investment casting, described in the company's product data as precision lost-wax casting, with the stated purpose of ensuring stable processing. That single line carries more procurement meaning than it first appears.
Investment casting builds the body shape from a wax pattern. The pattern is coated in ceramic, the wax is removed, and molten metal is poured into the resulting shell. Because the mould is a precise replica of the final geometry rather than a cavity packed with sand, the resulting casting tends to hold wall section and dimensional relationships more consistently. The practical consequences for a ball valve buyer are specific: a more uniform body wall means pressure containment that behaves predictably across the batch; a more accurate flange face and body bore mean less machining stock has to be removed to reach the final seat pocket geometry, and seat pocket geometry is what determines how evenly the seat is compressed when the ball closes.
Body material selection runs alongside the casting decision. RST lists WCB carbon steel, CF8 (304) stainless steel and CF8M (316) stainless steel as the principal body grades for the flanged series, with carbon steel, stainless steel, 2205 and CF3M also listed in the material field of the same product family. Material choice and casting method are separate decisions and should be evaluated separately: the casting route affects consistency, while the grade affects corrosion behaviour against the medium.
The boundary of a casting claim
Investment casting is not self-certifying. The method improves the probability of consistent geometry; it does not prove that any individual casting is sound. That proof comes from the inspection layer behind it — material inspection, chemical testing and physical testing — and from the material certificate that travels with the order. A buyer who accepts a casting claim without asking for the corresponding material certificate has accepted a process description, not evidence.
Two-Piece and Three-Piece Split Bodies: A Maintenance Decision
Body construction decides what happens on the day a seat has to be replaced. RST produces the flanged series in two-piece and three-piece split body configurations, alongside one-piece flanged and wafer-type variants, and states that the two-piece and three-piece split structure facilitates disassembly and replacement of seals, reducing maintenance cost.
A two-piece body joins a main body to a single end cap. It carries one body joint, fewer components and a simpler assembly sequence, which is why it is common in general process isolation where the line can be opened during a planned shutdown. A three-piece body bolts two end caps to a centre section; because the centre section can be separated from both pipe connections, the ball, seats and body seals become accessible without disturbing the adjacent piping.
The same architecture logic appears in the threaded range, where RST lists one-piece, two-piece and three-piece threaded ball valves together with socket weld, butt weld and tri-clamp variants. The threaded series runs from DN6 to DN100 at 1000 to 2000 WOG, with CF8 (304) or CF8M (316) bodies, PTFE seats and an ISO 5211 actuator mounting pad.
| Body configuration | Maintenance implication | Typical fit | Trade-off to accept |
|---|---|---|---|
| One-piece | No body joint to disturb; internal parts are not accessible without removing the valve | Small bore isolation where replacement is cheaper than repair | Seat service becomes a valve replacement |
| Two-piece split | One body joint; end cap removed for internal access | General process isolation with planned shutdowns | Line must be opened for seat service |
| Three-piece split | Centre section removable; seats and body seals serviceable in place | Piping that is expensive or slow to cut, or seats inspected on a schedule | More components and a second joint to assemble correctly |
The honest limitation is symmetrical. Every additional body joint is a potential leak path, so a three-piece design is only an advantage when it is assembled to the correct bolt torque with a new body gasket. A buyer selecting three-piece for maintainability without specifying assembly control has moved the risk from the seat to the body joint rather than removed it.
What a Pre-Shipment Test Should Actually Prove
Testing is where supplier claims most often go unverified, because buyers ask whether testing was done rather than what was measured. RST's stated quality control sequence covers shell strength testing, seat leakage testing, material inspection, visual inspection and a 100% factory test, with a test report and material certificate issued. For the flanged ball valve series, the company states that rigorous water pressure and air tightness testing is carried out before shipment.
Those tests answer different questions and are not interchangeable. A shell strength test pressurises the body cavity to verify that the casting and the body joint contain pressure without permanent deformation — it is the test that catches a casting defect. A seat leakage test verifies that the closed ball and seat hold against the specified pressure direction, which is the performance the process actually depends on. An air tightness test operates at low pressure with gas rather than water; because gas has far lower surface tension than water, it can reveal leakage paths at sealing faces that a water test does not resolve. Running water pressure and air tightness testing together is therefore a stronger acceptance basis than either alone.
| Check | What it verifies | Evidence to request |
|---|---|---|
| Shell strength test | Body casting and body joint contain pressure without deformation | Test report with test pressure and result |
| Seat leakage test | Ball-to-seat sealing in the closed position | Test report, per valve or per batch as agreed |
| Water pressure test | Pressure containment under hydrostatic conditions | Test report |
| Air tightness test | Low-pressure gas-tight sealing at faces and joints | Test report |
| Material inspection and chemical / physical testing | Body and trim chemistry and mechanical properties match the order | Material certificate |
| Visual inspection | Marking, surface condition and workmanship | Inspection record |
The boundary matters here as much as the capability. A factory test proves conformance at test conditions; it does not prove cycle life, torque stability over thousands of operations, or fire-safe performance. RST lists fire-safe design and anti-static devices as optional features on its ball valve range rather than as defaults, which means a buyer whose service requires them has to specify them, not assume them. Disassembly under pressure is prohibited in the application data, and that instruction belongs in the operating procedure rather than in a footnote.
Flange Standards and Body Materials as Fit Evidence
Compatibility is the least discussed and most common cause of a failed delivery. A valve that meets every performance requirement but does not match the mating flange is scrap on arrival. RST states that its flanged ball valve series supports GB, ANSI, DIN and JIS flange standards, with body materials including WCB, CF8 (304) and CF8M (316); the wider company profile also lists API, ANSI, DIN, JIS, BS and GB as the standards its product range is performed to.
| Attribute | Stated range for the flanged series (Q41F / Q41H / Q45F) |
|---|---|
| Flange standards | GB, ANSI, DIN, JIS |
| Body materials | WCB, CF8 (304), CF8M (316) |
| Port and size | Full port, DN15–DN600 |
| Pressure class | PN16–PN63, CLASS 150–300 |
| Working temperature | -20°C to 180°C |
| Casting route | Investment casting (precision lost-wax) |
| Body configuration | One-piece, two-piece and three-piece split; direct mounting pad; wafer type |
Other series in the same range extend the envelope without changing the evaluation logic. The trunnion mounted ball valve series Q347F, Q347H and Q347Y covers PN4.0–10.0 MPa, DN50–DN1200 and -40°C to +150°C in flanged configuration with WCB, CF8 or CF8M bodies. The threaded series covers DN6–DN100 at 1000–2000 WOG and -20°C to 180°C. Each figure should be read as the boundary of a specific product family, not as a company-wide rating.
Standards context buyers should keep separate
API Specification 6D, in its 25th Edition, defines requirements for the design, manufacturing, materials, welding, quality control, assembly, testing, marking and documentation of ball, check, gate and plug valves for petroleum and natural gas pipeline and piping systems, and covers pressure classes 150, 300, 400, 600, 900, 1500 and 2500. IOGP S-562 Version 3.1 is a supplementary procurement specification that applies to manually operated API 6D ball valves within an allowable temperature range of -46°C to 150°C.
These are useful as reference criteria, not as automatic statements about any supplier. The RST evidence set documents ISO 9001, TS Special Equipment and CE certification. A project that specifies an API 6D monogram, an IOGP S-562 supplementary specification or a particular edition and addendum should confirm applicability and the associated documentation for the specific order, because a standard's scope is not the same thing as a supplier's certificate.
Where These Capabilities Fit — and Where They Do Not
The application data for the RST flanged series defines the working envelope precisely: process piping for chemical, gas, pharmaceutical and water treatment industries, and petrochemical service; media described as water, oil, gas and weak acids or alkalis; pressure from PN16 to PN63 or CLASS 150 to 300; temperature from -20°C to 180°C. Operation is a 90° quarter-turn for on-off service only, with manual operation using an optional lockable handle, or pneumatic and electric actuation through an ISO 5211 direct-mount interface. For flammable or explosive service, an explosion-proof configuration is required.
Reported project experience sits inside that envelope. RST cites use by chemical plant, water treatment contractor and gas engineering company clients, in project quantities of 50 to 500 units, for process pipeline on-off isolation in chemical, gas and water utility systems, with reported results of bubble-tight zero leakage, stable operation and low maintenance cost over a stated duration of 8 to 10 years. The specific models cited in that reference are Q41F, Q41H and Q45F — the flanged series discussed above.
The limits are equally specific, and buyers should treat them as selection rules rather than exclusions. The valves are on-off devices; the application data states they are not suitable for throttling, so they should not be substituted for a control valve in a flow-modulating loop. Media are described as water, oil, gas and weak acids or alkalis — the qualifier is deliberate, and strongly corrosive media require material verification beyond the standard grades. Fire-safe and anti-static designs are optional and must be specified where the service demands them.
How Split-Body Investment-Cast Valves Compare with Simpler Alternatives
Comparison is where the trade-offs become visible. A buyer choosing between a casting route, a body configuration and a test scope is not choosing between good and bad; they are choosing which risk to carry.
| Choice | Strength | Trade-off or limitation |
|---|---|---|
| Investment cast body versus a lower-grade casting route | More consistent wall section and dimensional control, which supports predictable pressure containment and seat pocket geometry | Higher tooling and piece cost; soundness still depends on material and physical testing, so the certificate remains essential |
| Three-piece split body versus one-piece | Seats and body seals serviceable without cutting the line; lower maintenance disruption | More components, two body joints, and dependence on correct assembly torque and gasket renewal |
| Water plus air tightness testing versus a single pressure check | Two complementary leakage signatures — hydrostatic containment and low-pressure gas-tight sealing | Adds test time; still does not establish cycle life, torque behaviour or fire-safe performance |
| Documented order versus catalogue-only quotation | Material certificate and test report make acceptance an evidence comparison rather than an argument | Requires the buyer to define acceptance terms before the order, not after arrival |
The pattern is consistent: each increment of serviceability or assurance is paid for in cost, component count or specification effort. The mistake is not choosing a simpler option; it is choosing it without knowing which risk stayed in the project.
Outlook: Documentation Is Becoming the Real Qualification Test
The direction of the standards environment is toward documentation as a first-class requirement. API Specification 6D 25th Edition Addendum 2 sets out requirements covering design, manufacturing, materials, welding, quality control, assembly, testing, marking, documentation and process controls for the valve types in scope. IOGP S-562 exists precisely to translate a general standard into a minimum common set of procurement requirements for a defined oil and gas context.
The practical consequence for ball valve buyers is that supplier evaluation is shifting from a capability conversation to a paperwork comparison: whether a material certificate can be issued against the ordered grade, whether a test report states the test performed and the result, whether marking matches the specification, and whether optional features such as fire-safe or anti-static design appear on the order rather than in a brochure. Suppliers who manufacture to a documented regime — investment casting with material and physical testing, split bodies designed for seal replacement, and water plus air tightness testing before shipment — will find that regime easier to evidence at order level, because the records already exist as a by-product of production.
Frequently Asked Questions
What should a buyer check first when evaluating a ball valve supplier's casting capability?
Start with the casting route and the material documentation together. RST states that its flanged ball valve series is produced by investment casting — precision lost-wax casting — and that body materials include WCB, CF8 (304) and CF8M (316). Because the casting method describes a process rather than a specific part, it should be paired with material inspection, chemical and physical testing, and a material certificate issued against the ordered grade.
Is a two-piece or three-piece split-body ball valve better for a process line?
It depends on how the line will be maintained. A three-piece split body allows the centre section to be separated so that seats and body seals can be replaced without disturbing the adjacent piping; a two-piece body has a single body joint and requires the line to be opened for internal access. RST states that the two-piece and three-piece split structure facilitates disassembly and seal replacement, reducing maintenance cost. The trade-off is that each body joint is a potential leak path and must be assembled to the correct torque with a new gasket.
Which pre-shipment tests and documents should be requested with a ball valve order?
RST's quality control sequence covers shell strength testing, seat leakage testing, material inspection, visual inspection and a 100% factory test, with a test report and material certificate provided; the flanged series is additionally described as undergoing water pressure and air tightness testing before shipment. A shell strength test verifies body containment, a seat leakage test verifies closed-position sealing, and an air tightness test detects low-pressure gas leakage that a hydrostatic test may not resolve. A factory test does not by itself establish cycle life or fire-safe performance.
Which flange standards and body materials can be specified for flanged ball valves?
The RST flanged ball valve series Q41F, Q41H and Q45F supports GB, ANSI, DIN and JIS flange standards with body materials including WCB, CF8 (304) and CF8M (316), in full port sizes from DN15 to DN600, at PN16–PN63 or CLASS 150–300 and -20°C to 180°C. A buyer whose project specification references API 6D, IOGP S-562 or another standard should confirm the applicable edition and the documentation required for that order.
Can these ball valves be used for throttling or for strongly corrosive media?
No on both counts, on the basis of the published application data. The valves operate in a 90° quarter-turn for on-off service only and are stated as not suitable for throttling, so they should not replace a control valve in a modulating loop. The stated media are water, oil, gas and weak acids or alkalis; strongly corrosive service requires material verification beyond the standard body grades before selection.
What order quantity, lead time and customization scope apply to a ball valve order?
RST lists a minimum order quantity of one unit, a lead time of 20 to 45 days and a monthly capacity of 15,000 units, with OEM and ODM production modes. Customization covers body material, connection type, pressure rating, actuator, logo, marking, special seal, fire-safe or anti-static design and sanitary polishing. Fire-safe and anti-static designs are optional features and must be stated in the enquiry if the service requires them.
Further reference: the RST VALVE GROUP CO.,LTD presentation is available for download at RST PRESENTATION (PDF). Product and company information is published at stainlesssteel-valves.com.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.