
DHL8005H Acceptance Criteria: Pharmaceutical Packaging FAQ
On an integrated blister-cartoning line, acceptance is not one inspection. It is a documented sequence — technical agreement, material trial, factory acceptance test, pre-shipment inspection and site acceptance — and it decides whether a rated output becomes a repeatable one.
Buyers evaluating a pharmaceutical packaging machine today ask fewer questions about what a machine can theoretically do and more about what will be proven, by whom, and against which document. For the DHL8005H, an intelligent fully servo high-speed blister-cartoner integrated machine and solid dosage turnkey packing line built by Zhejiang Hoping Machinery Co., Ltd. (HOPING), the stated ratings are up to 800 blisters/min and 500 cartons/min. Those two numbers, the control architecture behind them, and the parts and tooling named in the technical agreement together form the acceptance agenda.
This reference answers the technical and procurement questions that most often appear between evaluation and execution: how acceptance is structured, what the speed figures do and do not represent, which components are verifiable, which contact parts and tooling are contractually defined, and where the model's boundaries lie.
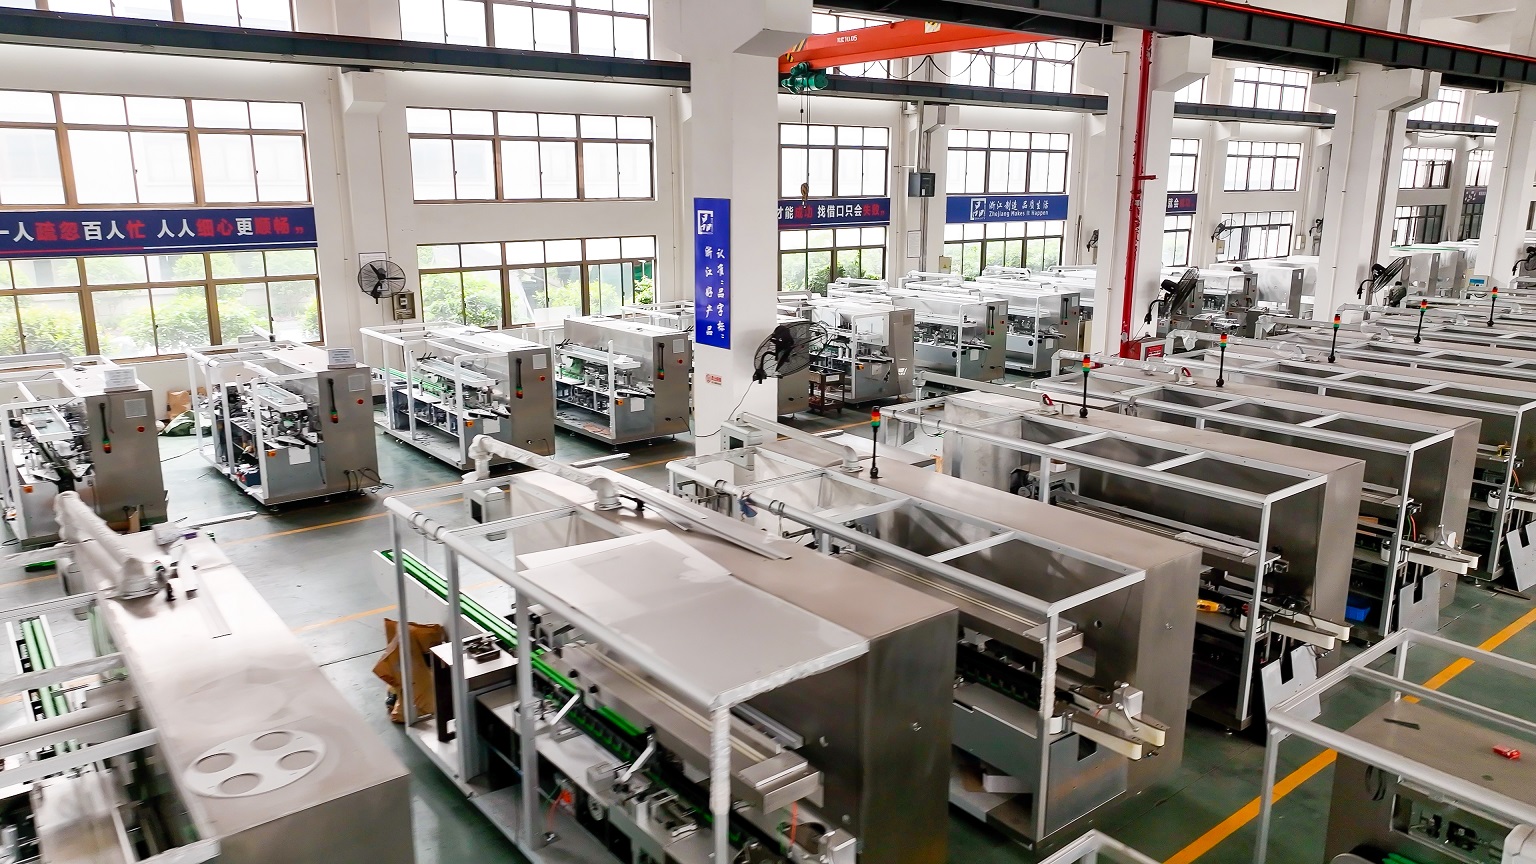
Cartoning module assembly area — the secondary packaging stage that typically sets the output ceiling of an integrated blister cartoning line.
Why acceptance criteria have become the deciding procurement question
Independent market research puts the global blister packaging machine pharmaceutical market at USD 2.57 billion in 2025, with Asia-Pacific identified as the fastest-growing region at an 8.87% CAGR to 2031 (Custom Market Insights, Global Blister Packaging Machine Pharmaceutical Market 2025–2034). In secondary packaging, horizontal cartoning systems accounted for 70.12% of cartoning machine market share in 2024 (Mordor Intelligence, End Load Cartoning Machine Market). These are publisher-defined estimates with their own scope and methodology, and neither breaks the market down by equipment type — but they describe the same buying pattern: capacity is being added as linked blister-and-carton configurations rather than as isolated machines.
When blister forming, transfer, leaflet handling and cartoning are purchased as one package, a single weak stage determines the output of the whole line. That shifts risk — and therefore attention — to the acceptance document. It also explains why third-party research in this category explicitly warns that a manufacturer-stated maximum output should not be compared between suppliers until product format, station count, rejection rate, operating conditions and the basis of sustained output are stated.
The DHL8005H in verifiable terms
The DHL8005H is an intelligent fully servo high-speed blister-cartoner integrated machine and solid dosage turnkey packing line manufactured by Zhejiang Hoping Machinery Co., Ltd., a pharmaceutical packing machinery manufacturer established in 2001 and based in Ruian City, Zhejiang Province, China. HOPING builds blister packaging machines, cartoning machines, case packing machines and end-of-line packaging equipment, and reports export activity of approximately 25% of output, with main markets in Southeast Asia, the Middle East, Eastern Europe, South America and Africa.
| Item | Stated specification (DHL8005H) |
|---|---|
| Line type | Intelligent fully servo high-speed blister-cartoner integrated machine; solid dosage turnkey packing line |
| Maximum capacity | Up to 800 blisters/min and 500 cartons/min |
| Transfer system | D3 intelligent top-loading parallel tracking transfer system |
| Product feeding | Multiple feeding methods, selected by project |
| Replenishment | Three-channel servo-driven independent replenishment system |
| Material handling | PVC/Alu foil auto splicing |
| Control platform | Beckhoff motion controller and CP9315 industrial PC |
| Format management | Mold-change and preset-memory functions |
| Construction | Stainless steel and aluminum-alloy machine structure; transparent guarding; servo-driven motion components |
| Compliance orientation | GMP-oriented line design; product-contact parts and tooling according to technical agreement |
| Scope | High-speed blister forming/sealing, transfer, leaflet handling, carton opening, insertion, coding/inspection, and connection to bundling, case-packing or palletizing equipment |
The specification is a starting point, not the acceptance document. Each line in this category is configured against a format and a product, and the items above are the ones a buyer can hold a supplier to during verification.
What the acceptance sequence actually contains
For HOPING equipment, quality control runs from incoming material inspection through to site acceptance, and third-party inspection can be arranged according to customer requirements. The practical sequence reads as follows.
| Stage | What is verified |
|---|---|
| Technical agreement confirmation | Blister format and materials, carton and leaflet specification, coding/inspection method, feeding method, contact parts and tooling, interfaces |
| Incoming material inspection | Bought-in materials and components before assembly |
| Key component inspection | Servo, electrical and pneumatic components |
| Assembly inspection | Mechanical build quality and alignment |
| Electrical safety check | Wiring, safety circuits and guarding |
| No-load trial run | Motion sequence, interlocks and cycle logic without product |
| Material trial / sample testing | Blister forming and sealing, transfer, carton opening, insertion, closing on real product |
| FAT before shipment | Line run against agreed criteria, including preset-memory recall |
| Customer witness acceptance | Buyer-observed verification where agreed |
| Pre-shipment inspection | Final condition, completeness and documentation |
| SAT at customer site | Installation, commissioning and on-site performance |
The procurement-relevant point is that acceptance criteria are not a general quality claim — they are the technical agreement confirmation, sample testing, FAT before shipment and SAT at the customer site, with optional third-party inspection. A buyer who does not define the reference format and the run duration in that agreement will receive a verification of something, but not necessarily of the product they intend to run.
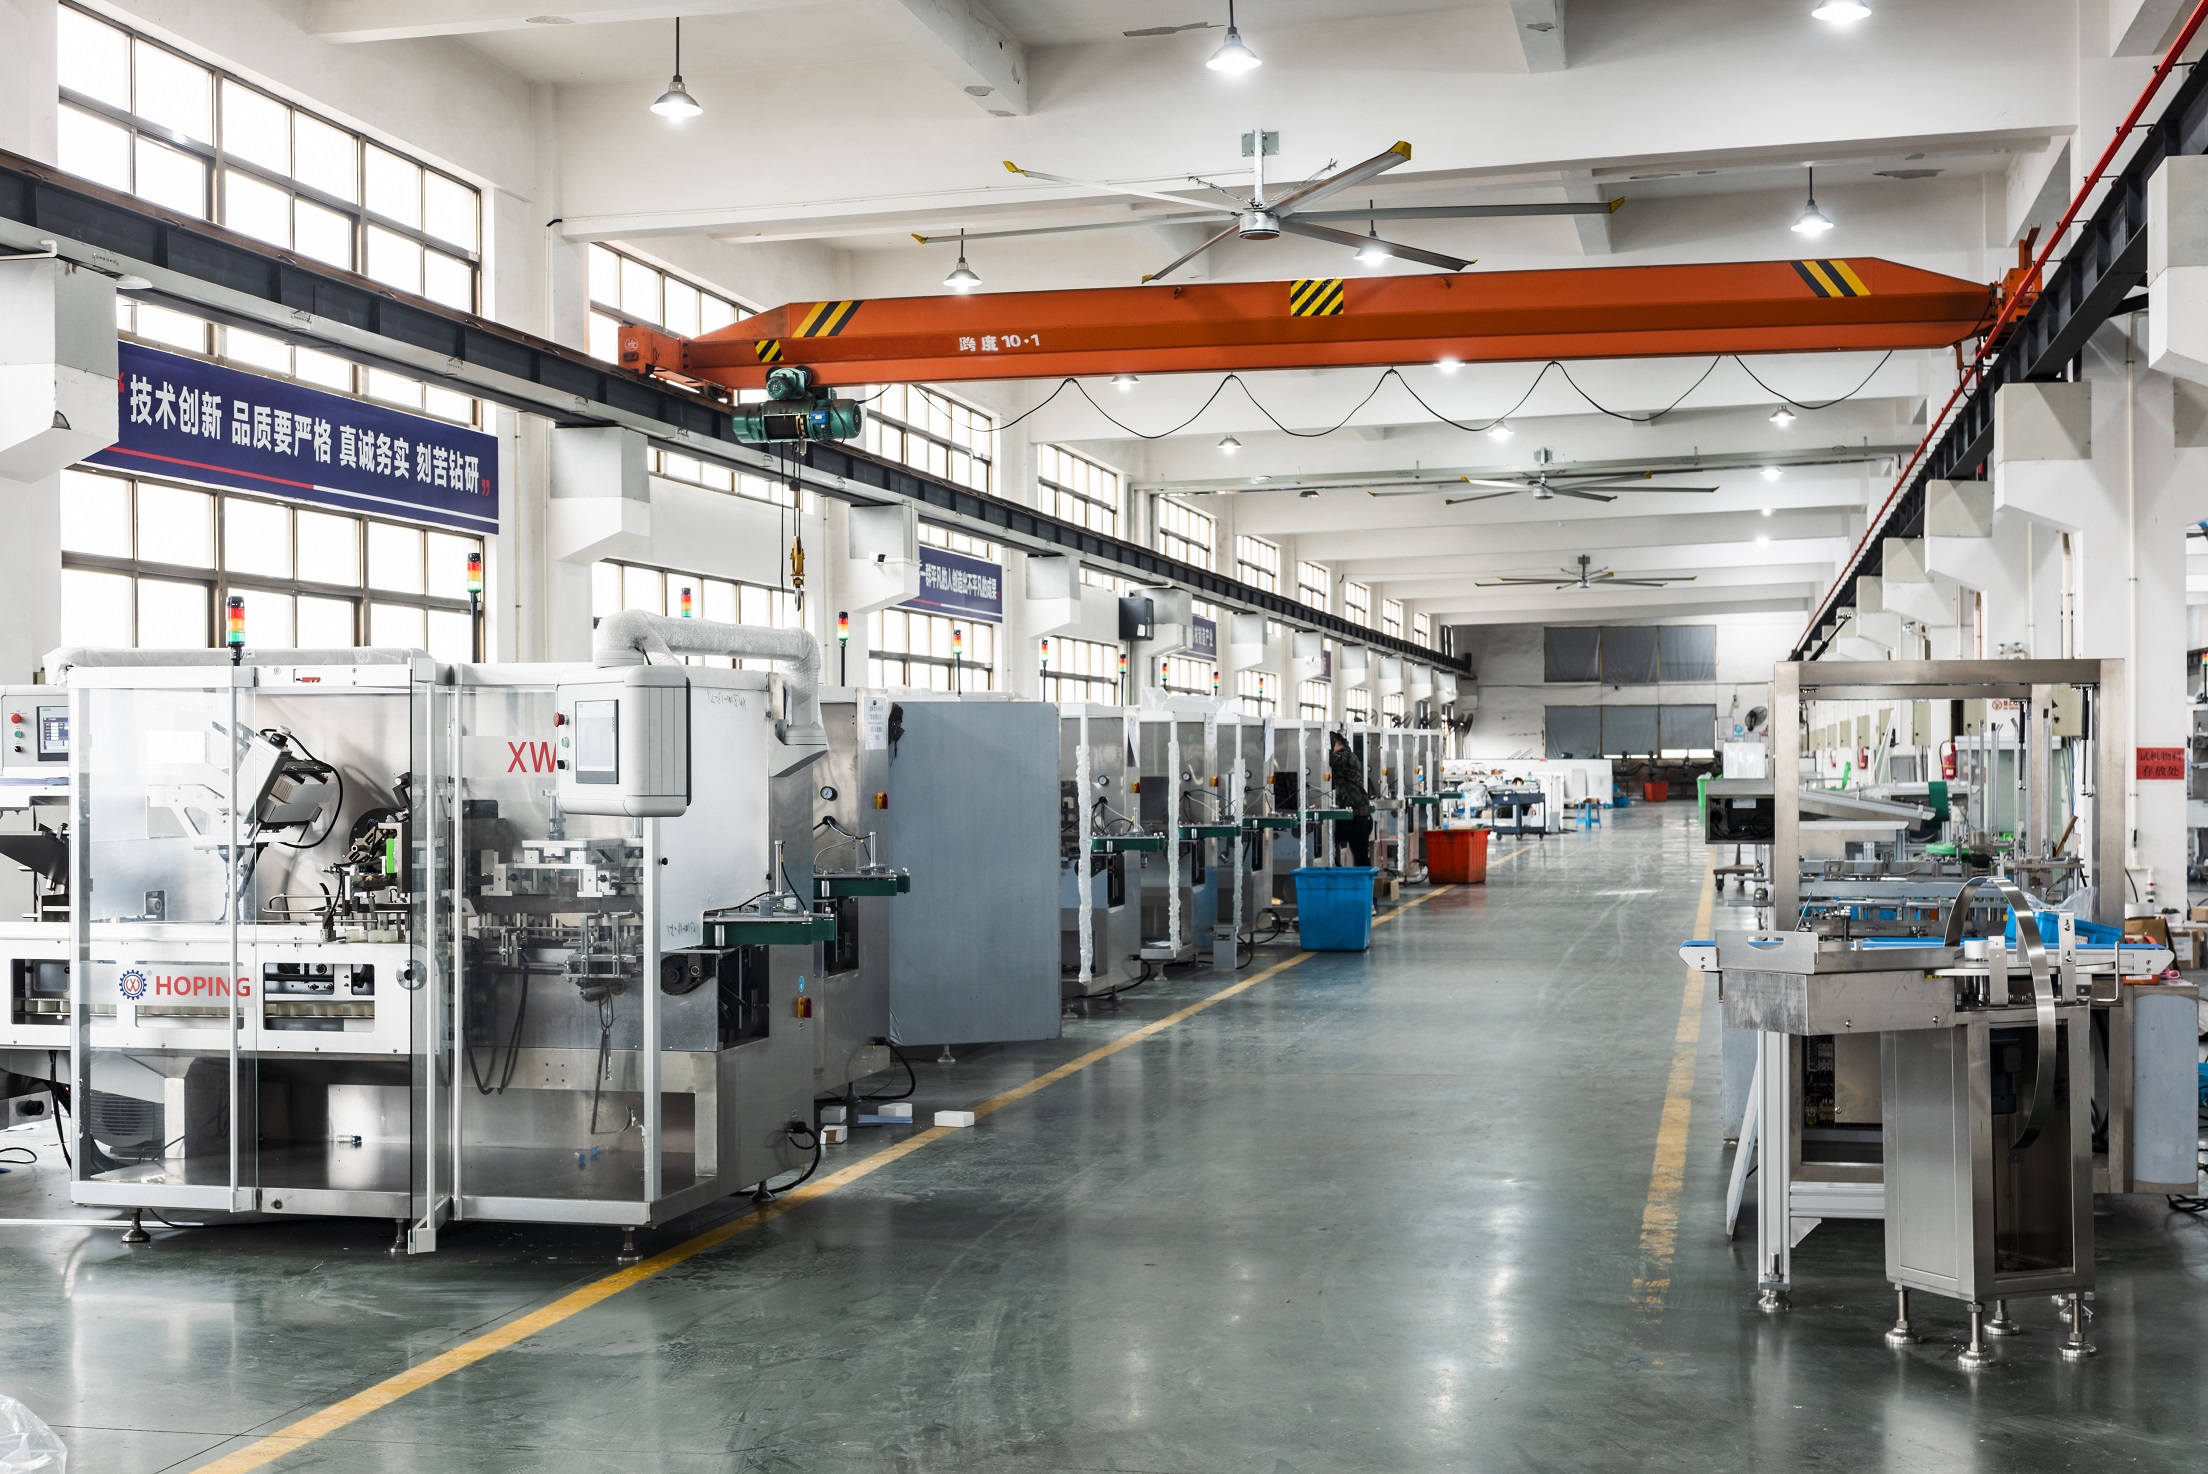
Cartoning machines and linked line modules in production — acceptance is run against the buyer's confirmed blister, carton and leaflet formats.
Reading 800 blisters/min and 500 cartons/min correctly
The two figures describe different stages of one line. The blister stage forms and seals the primary pack; the cartoning stage opens cartons, inserts the blister board and leaflet, closes and, where configured, inspects and codes. They are stated maxima published by the manufacturer for the DHL8005H.
What they are not is a promise of sustained output for every format. Real output depends on product count per blister, film and foil combination, carton and leaflet specification, inspection and rejection settings, and the transfer system's handling of the specific board geometry. Independent market data in this equipment category flags exactly this risk: a company-stated maximum should not be compared with other suppliers until format, station count, rejection rate and operating conditions are established, and maximum output may not equal sustained validated output.
The practical response is procedural rather than technical. Fix the reference format in the technical agreement, define a measurement window, and record sustained output, reject rate and stoppage causes during the factory acceptance test. That converts a nominal number into a contractual one.
Control architecture and continuous supply
The DHL8005H is specified with a Beckhoff motion controller and a CP9315 industrial PC. In line terms, that platform coordinates the blister forming and sealing motions, the transfer of boards to the cartoning stage, carton opening, insertion and closing, and it carries the preset-memory function that stores format settings for recall. Electrical component brand and data interface are both listed as customizable items, which is relevant for buyers who need the control layer to match an existing plant standard.
Three supply-side functions are named in the specification and are worth verifying directly rather than assuming.
- Three-channel servo-driven independent replenishment system. Product replenishment is handled across independently driven channels rather than a single shared feed path. The configured feeding method varies by project, so the channel logic should be demonstrated during the factory acceptance test.
- PVC/Alu foil auto splicing. Forming film and lidding foil can be spliced without a full-line stop at reel changes, reducing manual intervention. The size of the benefit depends on reel dimensions and material, and is normally quantified by measuring a defined run.
- D3 intelligent top-loading parallel tracking transfer. This is the link between the blister stage and the cartoning stage. It is the module most exposed to format variation, which is why transfer stability belongs in the acceptance protocol.
Mold change, preset memory and multi-format production
Mold-change and preset-memory functions matter most to producers running several SKUs on one pharmaceutical packaging line. Mold sets are made for a specific blister and carton format; preset memory allows a stored recipe to be recalled instead of re-entered manually, which reduces the risk of parameter errors between runs.
The customization scope associated with this equipment family covers blister size, blister materials, quantity per carton, carton specification, leaflet format, coding/inspection method, feeding method, downstream bundling, case-packing and palletizing connection, interface language, electrical component brand and data interface. The manufacturer also offers ODM, OEM and customizable production services.
One item buyers should not assume is changeover time. It is not stated in the available specification, and it is format- and tooling-dependent. Measure it during acceptance, on the buyer's own formats, with the same operators who will run the line in production.
GMP-oriented contact parts, tooling and documentation
For the DHL8005H, product-contact parts and tooling are specified as GMP-oriented and configured according to the technical agreement, within a machine structure built from stainless steel and aluminum alloy with transparent guarding. That wording is deliberate: contact-part materials and finishes are project-specific, not fixed by a catalogue. Buyers should therefore list the exact contact parts, materials and tooling pieces they expect to be documented before contract signature.
The wider regulatory frame is worth separating from the machine's own documentation record. ISO 15378:2017 specifies Good Manufacturing Practice requirements for primary packaging materials for medicinal products — it addresses packaging materials, and its relevance to equipment lies in how contact parts and documentation support the buyer's own qualification work. The U.S. FDA publishes current Good Manufacturing Practice guidance covering production and process controls; the available guidance is not machine-specific, so the applicable clauses depend on the buyer's regulatory pathway.
HOPING's certification record includes CE certification for cartoning machine series and for blister packing machine series, both issued on 22 January 2019 by Shenzhen HTT Technology Co., Ltd. under Machinery Directive 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010. Earlier CE certificates in the record cover a carton packing machine series (certificate UCN 900339024607, Certify International Ltd, 2007) and an automatic blister packing machine (certificate UCN 900175009261, CELAB, 2006) and are described as historical certificate evidence. Management-system records include ISO 45001:2018 (certificate CN00123S33121R1M/3300) and ISO 14001:2015 (certificate CN00123E33896R1M/3300), both issued by the China Quality Certification Centre, with recorded validity periods ending in October 2026.
Two boundaries follow from this. First, certificates in the record relate to stated machine series, and their applicability to a specific DHL8005H configuration should be confirmed in the technical agreement. Second, because management-system certificates run on renewal cycles, buyers should request current certificate copies at the point of contracting rather than relying on an earlier record.
Where the line fits: solid dosage and downstream integration
The DHL8005H is positioned for pharmaceutical solid dosage production and capsule and tablet packaging, and is also listed for healthcare products, nutraceuticals and food and cosmetic blister-cartoning projects. Its scope runs from high-speed blister forming and sealing through transfer, leaflet handling, carton opening, insertion, coding and inspection, and includes connection to bundling, case-packing or palletizing equipment.
That downstream connection is where a blister cartoning line becomes a full secondary packaging line. Related equipment in the same portfolio includes stretch banders in the XWK series (about 8–60 bundles/min depending on model), overwrappers in the XWG series (about 10–60 bundles/min depending on model), case packing machines in the XWK series (about 5 cases/min for the XWK900 and XWK600 models) and the ICP12 case packing and palletizing integral machine (about 12 cases/min). Buyers planning an end of line packaging machine stage should size these modules against the cartoning output, not against the blister output.
A representative project pattern recorded for this equipment type involves a large pharmaceutical manufacturer and solid dosage production company, at a scale of 5 to 10 packaging lines, for new line construction, capacity expansion or upgrading existing packaging lines. The stated objectives are improving packaging automation, reducing manual transfer, improving blister-to-carton connection efficiency, reducing wrong-insertion and missing-leaflet risks, and supporting downstream automation integration. Customer names are disclosed only with authorization.
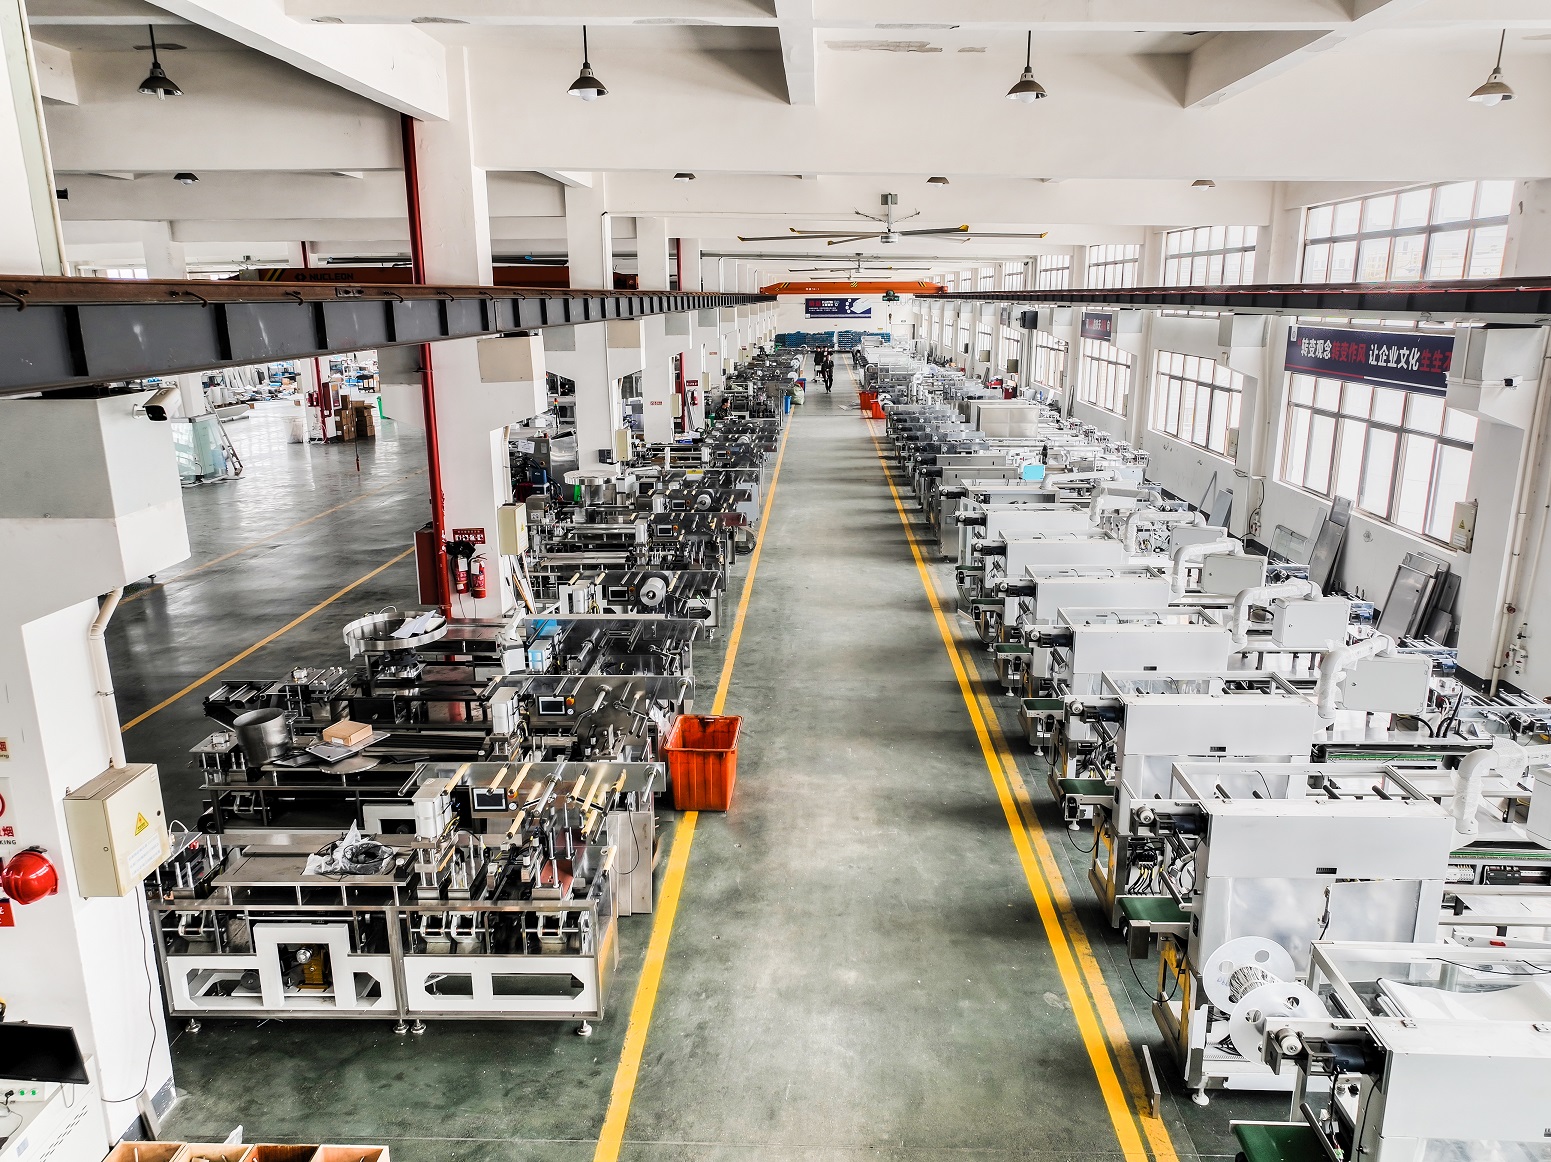
Blister packaging machine assembly area — the primary packaging stage feeding an integrated blister cartoning line.
Commercial terms to settle before acceptance is scheduled
Commercial terms shape how much acceptance evidence a buyer can practically obtain, so they belong in the same conversation.
- Minimum order quantity: 1 set or 1 complete line.
- Lead time: typically 60–120 days after technical confirmation, subject to model, configuration, project complexity and contract terms.
- Production capacity: 30–40 units per month.
- Delivery terms: EXW Ruian/Wenzhou; FOB Ningbo or Shanghai; CIF/CFR destination port; final terms subject to contract and destination-country requirements.
- Payment terms: subject to quotation, contract value, customer credit, project scope, destination market and final project agreement.
- After-sales scope: on-site installation and commissioning, operator training, maintenance training, remote video and phone support, spare parts supply, process-parameter guidance, regular follow-up and troubleshooting, subject to contract and project configuration.
No price bands are published in the available record for this equipment category, so budgetary figures should be obtained through quotation against a defined configuration rather than estimated from this article.
Integrated line versus a split blister-and-cartoner setup
The traditional alternative is a standalone blister packaging machine and a separate horizontal cartoning machine, with blister boards moved between them manually or semi-automatically. It is a legitimate choice for low volumes, staged investment and simple format ranges. Its documented weakness is exactly the problem the integrated configuration targets: manual transfer and leaflet insertion errors.
Against that, four boundaries apply to the DHL8005H and should be stated plainly.
- Sustained output is format-bound. The 800/500 figures are maxima. Until a format, material set and measurement window are fixed, they are a screening number, not a benchmark.
- The slowest stage governs the line. The DHL1000/5H in the same portfolio is specified at up to 1000 blisters/min with the same 500 cartons/min cartoning figure. At that point the cartoning stage, not the blister stage, is the constraint — a line-balancing fact that matters more than the headline number.
- Capacity matching cuts both ways. The DHL8005H sits high in the range. Buyers with lower volumes may find the DHL6004 (up to 600 blisters/min, 400 cartons/min), DHL7004 (up to 700 blisters/min, 400 cartons/min) or DHL7005H (up to 700 blisters/min, 500 cartons/min) better matched to their throughput, footprint and budget.
- It is a solid-dosage platform. Liquid-dosage formats such as pre-filled syringes, ampoules and cartridges are handled by a different integrated line (IXW400, up to 400 blisters/min and 150 cartons/min), and freeze-dried powder uses a dedicated blister platform.
Integrated lines also demand more discipline upstream: tooling sets are per-format, and format-related downtime is a design consequence of buying one linked machine rather than two independent ones.
Future outlook
Two directions are visible in the available evidence. The first is data. Trade coverage of PMMI material reports that pharmaceutical manufacturers are turning toward digitised data collection and integrated solutions to meet regulations and improve visibility — a directional statement without a defined sample or measurement basis, but consistent with what buyers are already writing into specifications: data capture, batch traceability and line integration as explicit requirements rather than after-sales add-ons.
The second is regulation. A regulatory-affairs source reports that China has a draft GMP guidance for pharmaceutical packaging materials under public consultation, guiding pharmaceutical marketing licence holders in reviewing packaging material suppliers. Its status is draft, and the issuing-authority document should be confirmed before it is treated as an operating rule. ISO 15378:2017, by contrast, is an active standard for GMP in primary packaging materials.
The practical consequence for acceptance criteria is straightforward. As performance claims become format-qualified and documentation expectations tighten, the technical agreement — not the datasheet — becomes the controlling document on a blister cartoning line.
FAQ
What does DHL8005H acceptance actually cover?
Acceptance is defined by the technical agreement and runs through confirmation of that agreement, incoming material inspection, key component inspection, assembly inspection, electrical safety check, a no-load trial run, a material trial, a factory acceptance test before shipment, customer witness acceptance where agreed, pre-shipment inspection and a site acceptance test at the buyer's plant. Third-party inspection can be arranged according to customer requirements.
Are 800 blisters/min and 500 cartons/min acceptance-tested values?
They are the manufacturer's stated maximum capacity for the DHL8005H, describing the blister stage and the cartoning stage respectively. They are not a guarantee of sustained output for every format. Sustained output depends on product count per blister, film and foil combination, carton and leaflet specification, and inspection settings, so it should be measured over a defined run during the factory acceptance test.
What does the Beckhoff motion controller with the CP9315 industrial PC control?
The DHL8005H uses a Beckhoff motion controller together with a CP9315 industrial PC as its control platform, coordinating blister forming and sealing motions, transfer, carton opening, insertion and closing. The same platform carries the preset-memory function that stores format settings. Electrical component brand and data interface are listed as customizable items.
How does the three-channel servo-driven independent replenishment system work?
The line is specified with a three-channel, servo-driven independent replenishment system, meaning product replenishment is handled across independently driven channels rather than one shared feed path. The configured feeding method varies by project, so the actual channel logic and recovery behaviour should be demonstrated during the factory acceptance test rather than inferred from the specification alone.
What does PVC/Alu foil auto splicing change during a run?
PVC/Alu foil auto splicing is listed among the DHL8005H's material-handling functions. It allows forming film and lidding foil to be joined without stopping the line for a full reel change, reducing manual intervention. The size of that reduction depends on reel dimensions and material, and is normally quantified by measuring a defined production run.
How do mold change and preset memory support multi-SKU production?
Mold sets are made for a specific blister and carton format, and preset memory allows a stored format to be recalled instead of re-entered. Customizable items include blister size, blister materials, quantity per carton, carton specification, leaflet format, coding/inspection method, feeding method and downstream connections. Changeover time is not stated in the available specification and should be measured on the buyer's own formats.
Which product-contact parts and tooling are covered by the technical agreement?
For the DHL8005H, product-contact parts and tooling are GMP-oriented and specified according to the technical agreement, within a stainless steel and aluminum-alloy machine structure with transparent guarding. Contact-part materials, finishes and tooling sets are project-specific rather than fixed by a catalogue, so the exact parts and tooling to be documented should be listed before contract signature.
Which dosage forms and products does the line support?
The DHL8005H is positioned for pharmaceutical solid dosage production and capsule and tablet packaging, and is also listed for healthcare products, nutraceuticals, and food and cosmetic blister-cartoning projects. Its scope covers blister forming and sealing, transfer, leaflet handling, carton opening, insertion, coding and inspection, plus connection to bundling, case-packing or palletizing equipment. Liquid dosage formats such as pre-filled syringes, ampoules and cartridges use a different integrated line.
What are the MOQ, lead time and delivery terms?
Minimum order quantity is 1 set or 1 complete line. Typical production lead time is 60–120 days after technical confirmation, subject to model, configuration, project complexity and contract terms, with a monthly production capacity of 30–40 units. Delivery terms are EXW Ruian/Wenzhou, FOB Ningbo or Shanghai, or CIF/CFR destination port, with final terms subject to contract and destination-country requirements.
What are the limits of the line's published capability?
Three limits matter. The 800 blisters/min and 500 cartons/min figures are stated maxima, not sustained output for every format. An integrated line's output is set by its slowest stage — the DHL1000/5H, for example, is specified at up to 1000 blisters/min with the same 500 cartons/min cartoning figure. And the DHL8005H is a solid-dosage platform, so liquid-dosage and freeze-dried powder formats require different equipment.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.