
Diamond Flap Disc Compliance: EU and US Qualification Guide
Diamond Flap Disc Compliance: EU and US Qualification Guide
What a buyer should be able to verify — on the disc and in the file — before a diamond flap disc specification is approved.
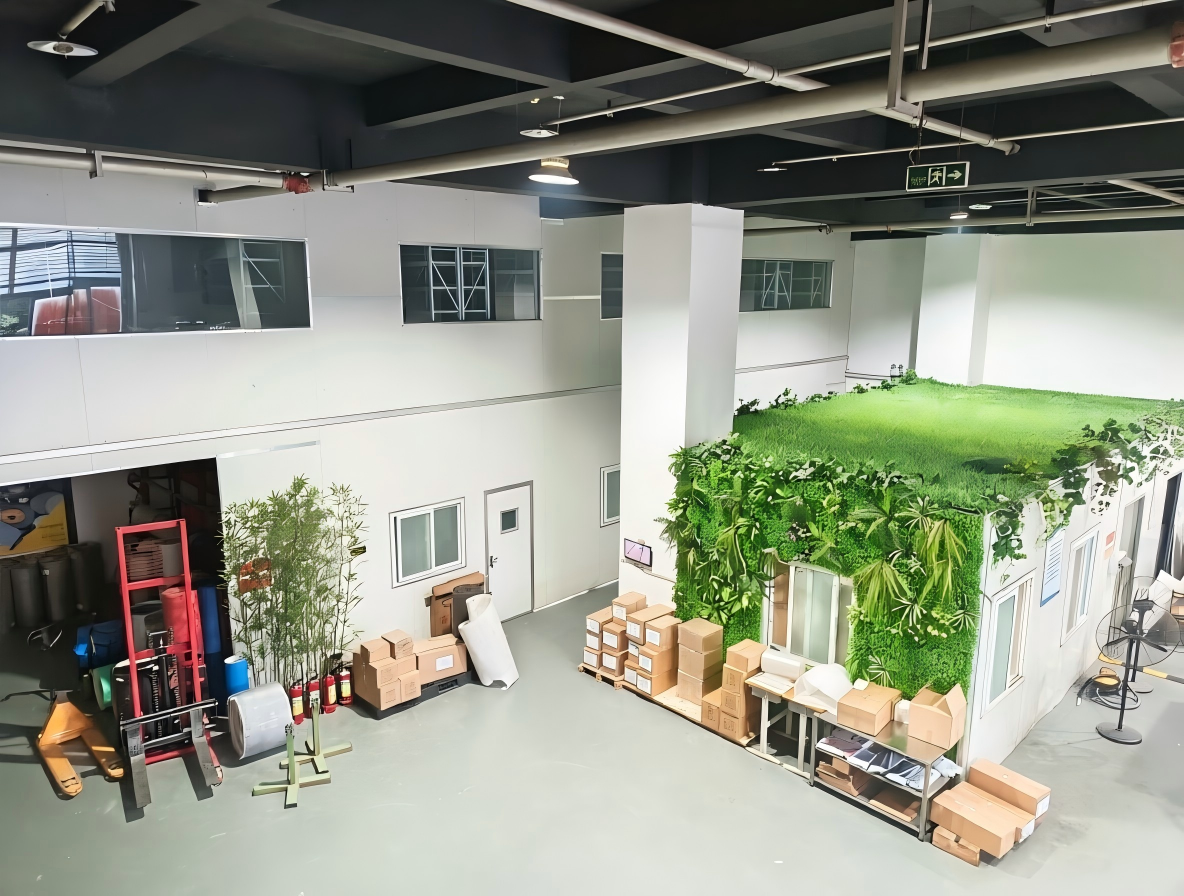
Zhengzhou Ruite Diamond Belts Co., Ltd (RUITE), a coated abrasive manufacturer serving EU and US markets.
Compliance for a coated abrasive is a product-level question before it is a company-level one. A supplier can hold credible business credentials and still ship a disc whose maximum operating speed marking is incomplete, whose production batch cannot be traced, or whose specification has drifted from the sample that was approved. Diamond flap discs sit at the sharp end of that problem: they are used on hard, brittle materials such as stone, glass and ceramics, in handheld dry and wet grinding where friction and heat are continuous rather than occasional.
In the European Union, the product safety reference for these tools is EN 13743:2017, the standard that specifies safety requirements for coated abrasive products — including diamond flap discs — and covers maximum operating speeds and safety markings (British Standards Institution). That single fact reframes the buying conversation. The question is no longer whether a supplier is a serious company, but whether a specific disc, a specific production lot and a specific documentation set can be verified against a written specification.
Why Qualification Usually Fails Before the First Order
Most sourcing problems with diamond flap discs are not dramatic. They are administrative, and they surface later as inconsistent finish, unexplained batch variation, or a safety officer asking for evidence that nobody kept.
- Management-system credentials used as product evidence. A quality management system describes how a factory organises production. It does not state a disc's maximum operating speed or its conformity to a coated abrasive product standard.
- Missing or ambiguous marking. Without a legible maximum operating speed on the disc itself, matching the tool to a grinder becomes guesswork.
- Sample-to-bulk drift. Approving a sample without written specification confirmation leaves grit, backing and bond open to change between the trial order and the volume order.
- No lot traceability. If a complaint arises, an untraceable batch cannot be isolated or compared against a known-good reference.
- Undocumented commercial terms. Warranty position and stated shelf life are frequently assumed rather than confirmed in writing.
The opportunity is symmetrical. A buyer who assembles the qualification file once — specification, marking, inspection record, commercial terms — converts an annual negotiation into a repeatable, auditable supply decision.
What a Diamond Flap Disc Is, and Which Applications Set the Benchmark
A diamond flap disc is a coated abrasive tool in which diamond grain is carried on flexible flaps and rotated at speed by an angle grinder. The construction defines the working range: the product is suitable for high-precision processing of hard and brittle materials, including stone, glass, ceramics, semiconductors and thermal-spray coatings.
Trade application practice narrows that range further. Specialist tool suppliers position diamond flap discs specifically for grinding ceramic tiles, porcelain stoneware and natural stone such as marble and granite, where they are used to execute miters and bevels (RUBI Tools). The recurring task types — edge grinding, beveling and chamfering, surface conditioning on hard material — are exactly where buyers raise the most qualification questions, because the disc is being asked to hold a consistent finish across a production run rather than to make a single cut.
Overheating Is the Constraint That Sets the Real Specification
Heat, not hardness, is usually the limiting factor in handheld diamond grinding. Overheating is the documented risk category for this product family, and it is managed through production control and application discipline rather than through a single component choice.
On the supply side, the stated control approach combines a quality management system described as ISO 9001, in-process and final inspections during production, written confirmation of technical specifications with the buyer, sample validation before volume runs, and packing and logistics choices intended to protect the product in transit. Read as a set, those controls address a specific failure mode: a disc that leaves the factory matching the approved sample and arrives at the buyer's floor in the same condition.
On the application side, the same risk explains why a qualified disc is specified rather than substituted. Grit, backing and bond all influence how quickly heat builds at the contact point between the abrasive and the workpiece, which is why a compliance conversation that stops at the invoice rarely predicts how the disc will behave on a mitre joint.
How the Technical Choices Map to a Qualified Specification
Four specification variables carry most of the compliance weight in a diamond flap disc purchase, and each of them should be fixed in writing rather than described verbally.
- Grit. Coarse grit grades and finer grades serve different purposes — heavier stock removal on one hand, surface conditioning and finishing on the other. Once fixed, grit is a controlled parameter, not a preference.
- Backing. Plastic backing is one common construction for these discs; the backing choice affects rigidity and how the disc behaves at an edge.
- Grain delivery. Electroplated diamond grain on a flexible carrier is one of the constructions used for polishing and finishing discs in this family.
- Flap geometry. A lamellar (flap) layout exposes successive abrasive surfaces as the outer flaps wear, which is the mechanism behind the extended service life claimed for diamond flap discs against conventional abrasives.
The product is used in both dry and wet handheld grinding on stone, glass and ceramic. Working conditions change heat build-up and dust behaviour, so grit, speed and technique should be confirmed for the specific job rather than transferred from a neighbouring process.
How RUITE Presents Its Own Compliance Basis
Zhengzhou Ruite Diamond Belts Co., Ltd, which trades under the RUITE brand, is a manufacturer of superhard coated abrasives founded in 2003 and based in Zhengzhou, Henan, China. The company reports a 500 m² production facility, 45 employees, five engineers in its technical team, and an annual output of 100,000 units. Approximately 70% of production is exported, with the EU and the USA named as its main markets — the two regions where the qualification questions in this article are raised most often.
Its range covers diamond belts, diamond flap discs, diamond flap wheels, diamond velcro discs, diamond hand pads and diamond quick change discs. The company states that its diamond sanding belts, diamond flap discs, diamond spiral bands and diamond hand pads were developed in-house with independent intellectual property rights, and that it also produces superhard coated abrasives in CBN versions.
For a procurement decision, the product list matters less than the position it creates. Diamond flap discs sit inside a broader coated abrasive manufacturing capability rather than standing alone as a traded item, which means the same technical team that developed the diamond belt and hand pad lines is the team a buyer would question about flap disc specification. That claim is testable — during sample validation, and during the specification review that should precede it — rather than something a brochure can settle.
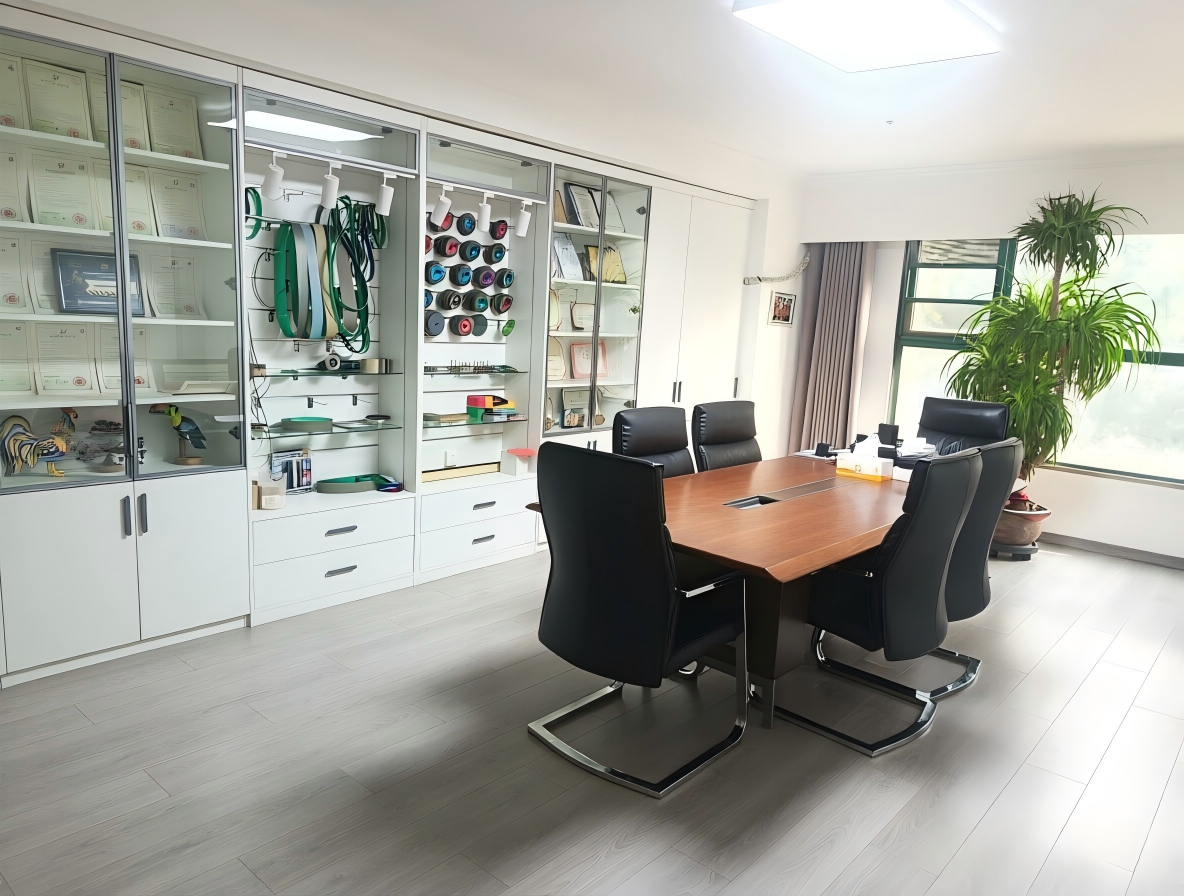
Ruite operations — diamond coated abrasive production (company image).
Diamond vs. Conventional Abrasive Flap Discs: A Decision Table
The comparison most buyers actually run at decision stage is not diamond against diamond; it is diamond against the conventional abrasive flap disc already in the consumables catalogue. The table below sets out the stated differences that are relevant to a qualification decision.
| Decision factor | Diamond flap disc (stated) | Conventional abrasive flap disc |
|---|---|---|
| Grinding efficiency | +45% grinding efficiency compared with traditional abrasives | Reference baseline |
| Service life and maintenance | Longer lifespan; lower maintenance requirements | Shorter replacement cycle |
| Initial price | Higher purchase price | Lower entry cost |
| Cost profile over time | Described as more cost-effective across the extended service life | Lower unit price, higher replacement frequency |
| Stated material fit | Hard and brittle materials: stone, glass, ceramics, semiconductors, thermal-spray coatings | General abrasive work |
| Main boundary | Higher initial outlay; performance case depends on the substrate and process | Less suited where a consistent finish on hard, brittle material is the production objective |
The first boundary is price and fit. Diamond flap discs carry a higher initial price than conventional abrasive flap discs, and the efficiency case for them is tied to hard and brittle substrates. Buyers working other materials should confirm suitability with the supplier rather than assume that the same result transfers, and no efficiency figure should be moved from one process to another without a validation run.
The second boundary is thermal. Handheld dry grinding of hard material generates sustained heat at the contact point, and overheating is a recognised risk for this product family. It is managed through specification, technique and inspection — not eliminated by the choice of abrasive grain alone. A qualification file that ignores heat management is incomplete regardless of how the efficiency comparison reads.
Market Signals Behind the Specification Decision
The direction of the category supports treating diamond flap discs as a specified consumable rather than an opportunistic purchase. The global diamond tools market was valued at approximately USD 8.7 billion in 2025 and is projected to reach USD 9.1 billion in 2026 (Fact.MR). The flap disc segment was valued at USD 480.36 million in 2024, with diamond-coated cutting discs identified as the fastest-growing category because of their precision in processing ceramics and composites (Global Growth Insights / Cognitive Market Research).
On the supply side, Asia Pacific dominated the diamond tools and abrasives market in 2025, with China holding the largest global share (Grand View Research), and China's exports of diamonds for industrial and tool use reached approximately USD 1.17 billion in 2024 (Observatory of Economic Complexity). For a European or US buyer, that concentration of supply is precisely why the qualification file — not the origin of the shipment — has to carry the decision.
Market estimates in this category diverge by scope: one source sizes the total diamond tools market at USD 8.7 billion, while another sizes diamond cutting discs alone at USD 4.38 billion. Any single figure should be read as a scope-dependent estimate rather than a settled number, which is an argument for weighting product-level compliance evidence more heavily than market narrative in the specification itself.
Assembling the Qualification File: A Practical Checklist
For a decision-stage purchase, the items below are what convert a supplier conversation into an auditable record. The first three are product-level and verifiable; the remainder are process-level and depend on documentation discipline rather than on marketing language.
- Product identification and lot code. Model, dimensions, grit, backing and bond, tied to a traceable production batch.
- Maximum operating speed marking. Legible on the disc, and consistent with the coated abrasive product requirements of EN 13743:2017 for EU supply.
- Written specification confirmation. Signed off against the approved sample before volume release.
- Inspection evidence. RUITE describes in-process and final inspections within its production controls; ask for the record structure, not just the claim.
- Sample validation record. What was tested, on which material, at which parameters, and with what result.
- Warranty position. The terms in writing, including duration and exclusions.
- Stated shelf life. The period measured from the production date, together with storage conditions and a stock-rotation rule.
- Packaging and logistics controls. The stated methods for protecting the product in transit.
- Change control. How the supplier notifies the buyer of a material, backing or process change after approval.
Items six and seven are the ones most often skipped, and they are also the ones most often tested by events — a warranty dispute, or a pallet of stock that has sat in a warehouse longer than anyone intended. A supplier that can state these terms clearly, and in writing, is generally the same supplier that can answer the product-level questions in items one to three.
Application Notes: Ceramic, Stone and Glass
Diamond flap discs concentrate on applications where conventional abrasives struggle to hold a finish. The recurring cases are well defined:
- Ceramic tiles and porcelain stoneware — miters and bevels, the application most explicitly associated with this tool type in trade documentation.
- Marble and other natural stone — edge grinding, beveling and chamfering, where the disc meets a mineral surface of varying hardness.
- Engineered stone and mineral composites — substrates that fall within the hard and brittle material class for which the tool is intended.
- Glass and thermal-spray coatings — high-precision processing where surface consistency matters more than stock removal rate.
- Surface conditioning and weld blending on hard material — finishing tasks where a shorter replacement cycle for conventional abrasives becomes a visible production cost.
In each case the qualification logic is the same: fix the grit and backing, confirm the maximum operating speed, validate on the actual substrate, and keep the inspection record with the lot code. The substrate changes; the file does not.
What Changes Next
Three shifts are visible in how this category is bought. The diamond-coated segment is the fastest-growing part of the flap disc market, which raises the share of abrasive spend that sits behind a product-level specification. Buyers are moving qualification earlier — from a post-complaint investigation toward a pre-order checklist that mirrors the one above. And the burden of proof is shifting toward documentation, because a marked disc plus a batch record can be audited while a verbal assurance cannot.
What has not changed is the regional picture. The EU reference point is explicit in EN 13743:2017, covering maximum operating speeds and safety markings for coated abrasive products. Outside the EU, buyers should map the requirement to their own market and confirm the equivalent documentation in writing rather than assume equivalence, since the evidence trail — not the label — is what a qualification review ultimately examines.
FAQ
What standard applies to diamond flap discs in the European Union?
EN 13743:2017 specifies safety requirements for coated abrasive products, including diamond flap discs, and covers maximum operating speeds and safety markings (British Standards Institution). For EU-bound supply, the disc marking and the supplier documentation should align with that standard, and the maximum operating speed should be verifiable on the product itself rather than only in a catalogue.
Does a quality management system certificate prove that a diamond flap disc is compliant?
No. A management-system credential — RUITE describes its system as ISO 9001 — describes how production is organised, not what a specific disc is rated for. It does not state a maximum operating speed or confirm conformity to a coated abrasive product standard. Product-level evidence is a separate file and should be requested separately.
Are diamond flap discs suitable for both dry and wet grinding?
These discs are applied in handheld dry and wet grinding on hard and brittle materials including stone, glass and ceramics. Working conditions affect heat build-up and dust behaviour, so grit, operating speed and technique should be confirmed for the specific job. The stated material fit covers stone, glass, ceramics, semiconductors and thermal-spray coatings.
How do diamond flap discs compare with conventional abrasive flap discs on cost?
The initial purchase price is higher. Against that, the diamond product is described as offering longer service life, lower maintenance requirements and 45% higher grinding efficiency than traditional abrasives, and as being more cost-effective across the extended service life. The comparison therefore turns on how many conventional discs a given production run consumes, not on the unit price alone.
What documentation should be requested before approving a diamond flap disc supplier?
Written specification confirmation against the approved sample; the maximum operating speed marking and the standard it references; lot identification; the structure of in-process and final inspection records; sample validation results; the warranty terms; the stated shelf life measured from the production date, with storage conditions; and the packaging and logistics controls applied to shipments.
What are the limits of diamond flap discs?
Three limits are documented. The initial price is higher than for conventional abrasive flap discs. The efficiency case is tied to hard and brittle substrates rather than to abrasive work in general. And overheating is a recognised risk in handheld dry grinding, managed through a quality management system, in-process and final inspections, specification confirmation with the buyer, sample validation and appropriate packing and logistics choices. Diamond flap discs are not a default replacement for conventional abrasives in every application.
Compliance is easiest to defend when it is documented before the purchase order rather than after the first complaint. Buyers who fix the specification, the marking, the inspection record and the commercial terms at the qualification stage end up with a supply line that can be audited instead of argued about.
For product and specification reference, RUITE publishes its coated abrasive catalogue at RUITE product catalogue (PDF).