
E-Coating Compliance Pack: What OEM Buyers Should Require
A compliance pack is the set of certificates, declarations, test reports and acceptance criteria that allows a buyer to approve an electrophoretic coating finish without relying on the supplier's assurances. For OEM procurement and quality teams, the pack is what separates a finish that can be defended in an audit from one that cannot.
Electrophoretic coating — written interchangeably as E-coating, ED coating, electrocoating or electrophoretic deposition — is a wet immersion process. Parts are submerged in a water-based paint bath, charged particles deposit onto the workpiece under a direct current field, and the film is then cured at elevated temperature into a continuous layer. Because the parts share a bath, a single parameter drift or an undeclared chemistry change can affect an entire production lot rather than a single unit. That is why qualification in this category is process-based, and why the paperwork carries as much weight as the sample.
This reference sets out how procurement and quality teams should read the compliance and qualification side of an electrophoretic coating supply agreement: which documents to request, what each one actually establishes, where each one stops, and which figures belong in the acceptance criteria before a finish is approved for serial production.
Why the Compliance File Is a Purchasing Document
A coating certificate is often treated as a box to tick at the end of sourcing. In practice the document file is a negotiating instrument. It defines what the supplier has committed to measure, how the measurement is performed, who performs it, and what happens when a result falls outside the agreed window.
Three properties of electrophoretic coating make this unusually important:
- The process is continuous. An e-coat bath circulates and is monitored for pH, conductivity, solids content and temperature. The coating chemistry a buyer approves in a sample is the chemistry that must be maintained for the life of the programme.
- The film is thin. Typical agreed builds sit in a narrow band, so measurement method and measurement location materially change the reported result.
- Acceptance is often visual plus instrumental. Colour, gloss and coverage are judged by the buyer, while corrosion performance is inferred from a salt spray record produced weeks earlier.
For a long-term supply relationship, the pack therefore does two jobs at once. It supports the initial approval decision, and it becomes the reference document against which repeat orders, change requests and annual re-qualification are measured.
Anatomy of an E-Coating Compliance Pack
A complete file for an OEM programme normally contains nine elements. The right-hand column matters most during review, because it is the part suppliers rarely volunteer.
| Document or declaration | What it establishes | What it does not establish |
|---|---|---|
| ISO 9001 certificate | An audited quality management system covering the named scope | That a specific lot meets a specific salt spray target |
| ISO 14001 certificate | A managed environmental system for the site | The VOC content or chemistry of a specific coating product |
| IATF 16949 certificate, where applicable | Automotive-sector quality management requirements are met | Approval by any individual vehicle manufacturer |
| Water-based, heavy-metal-free and low-VOC declarations | The declared chemistry of the coating as supplied | Pretreatment chemicals, substrate alloy composition or workshop emissions |
| Film thickness specification | The agreed build window and how it is measured | Corrosion performance on its own |
| Neutral salt spray report | Measured corrosion resistance under a named method, substrate and build | Performance on a different alloy, build or pretreatment |
| Colour and gloss record | Initial colour match and surface appearance | Long-term UV stability or batch-to-batch drift |
| Batch and bath traceability | Which bath and lot produced the parts | The supplier's internal process capability |
| Pre-shipment inspection record | Instrumental results measured before dispatch | Independent third-party verification |
Dongguan Yongxin Industrial Co., LTD — an electrophoretic coating and metal surface treatment processor based in Qiaotou Town, Dongguan City, China — operates six electrophoresis production lines supported by CNC machining, die casting and metal stamping, and holds ISO 9001, ISO 14001 and IATF 16949 certification. That combination is what a buyer should be asking to see documented rather than described: the management system certificates, and the measurement infrastructure that produces the numbers in the acceptance file.
Reading ISO 9001 and ISO 14001 Correctly
ISO 9001 certifies a quality management system. It confirms that the supplier operates documented procedures, calibrated measurement, corrective action and internal audit. It does not certify a coating thickness, a salt spray duration or a colour tolerance. Those come from the technical annex of the agreement.
ISO 14001 certifies an environmental management system. It is relevant to how a coating plant handles chemicals, wastewater and waste, but it is not a product-level environmental declaration. A buyer who needs a VOC figure or a heavy-metal statement must request that declaration separately.
Four practical checks apply to both certificates:
- Read the scope statement. A certificate covering surface treatment is not automatically a certificate covering electrophoretic coating of die-cast aluminium.
- Check the certification body and validity dates. Note the last surveillance audit and the expiry date, and diarise re-verification before the next sourcing cycle.
- Ask for the site address on the certificate. Production transferred to a second site without a scope extension is a common audit finding.
- Treat certificates as system evidence, not product evidence. A supplier with ISO 9001 and a weak salt spray report is still a weak salt spray supplier.
Because Yongxin's certification set includes IATF 16949 alongside ISO 9001 and ISO 14001, automotive-oriented buyers can ask for the automotive quality documentation in the same request rather than running a separate qualification track. The buyer's task is to confirm that the scope on each certificate names the process and the site actually used for their parts.
Environmental Declarations: Water-Based, Heavy-Metal-Free, Low VOC
The environmental portion of the pack is where claims are most often stated and least often evidenced. Three declarations need to be read as three separate statements.
Water-based
Electrophoretic coating is applied from a water-based paint bath, which is one of the reasons the process carries a lower organic solvent load than solvent-borne liquid painting. The declaration should confirm the carrier system and should be matched to the supplier's bath analysis records, since bath chemistry is monitored continuously during production.
Heavy-metal-free
A heavy-metal-free declaration should name the restricted substances and the detection thresholds used, not simply assert the phrase. Buyers should also confirm the declaration's boundary: it covers the coating as supplied, not the substrate. A zinc alloy part, a magnesium alloy casting or a die-cast component still contains the alloying elements of its base metal, and no coating declaration changes that.
Low VOC
Low VOC emissions should be stated with a value, a test method and a reference point — whether the figure describes the bath as supplied, the applied film, or emissions during cure. Without those three elements the claim cannot be entered into a buyer's environmental file.
Acceptance Criteria Worth Writing Into the Agreement
Acceptance criteria should be specific enough that two inspectors would reach the same conclusion. For electrophoretic coating, four criteria carry most of the commercial risk.
Film thickness: 15 to 25 micrometres
Yongxin's stated film thickness range for electrophoretic coating is 15 to 25 micrometres. The agreement should specify the measurement method (for example ISO 2808 or ASTM B767), the instruments used, and the surfaces on which the measurement is taken. Flat faces, edges and recessed areas do not read identically, and a specification without measurement locations invites dispute.
Salt spray: more than 1,000 hours
High salt spray grades are specified against neutral salt spray testing of more than 1,000 hours. For this figure to function as an acceptance criterion, the report must record the substrate, the measured film build, the test standard, whether the specimen was scribed, the evaluation criteria and the result. A duration quoted without those parameters is a headline, not a benchmark.
Published e-coat specification research notes that demanding automotive programmes commonly reference neutral salt spray targets in the range of roughly 720 to 1,000 hours, which places a 1,000-hour result in a demanding bracket rather than an exceptional one. Buyers should also confirm that the reported hours were achieved at the lower end of the agreed build window, not only at the top of it.
Colour customisation and appearance
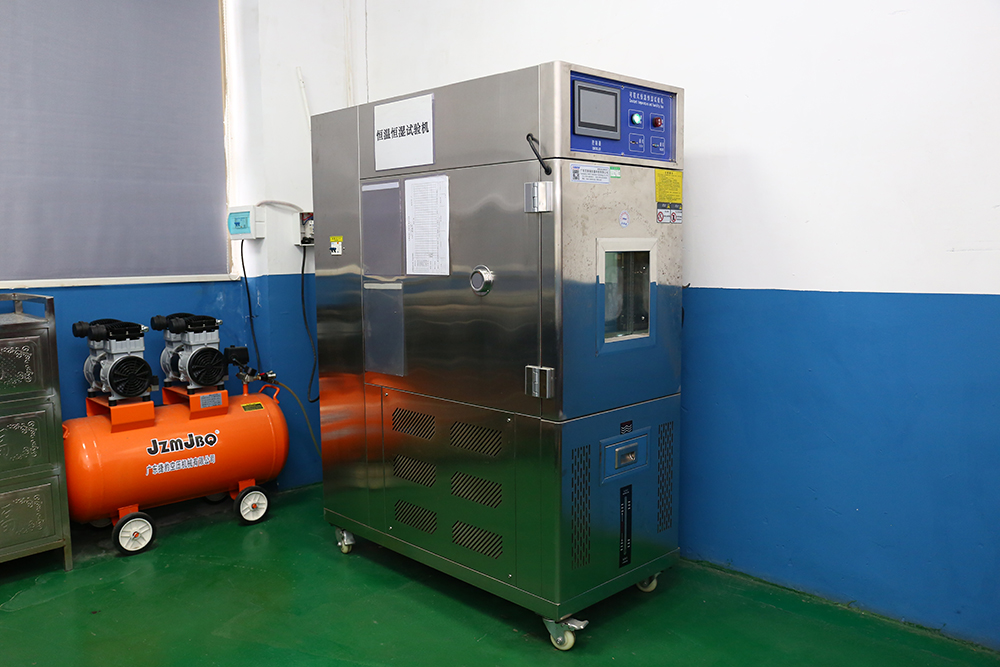
Colour customisation is available across black, white and colour electrophoretic coatings. Colour control should be tied to instrumented measurement rather than visual approval alone: Yongxin's inspection set includes a Konica Minolta spectrophotometer and a Zehntner gloss meter, which allow colour and gloss to be recorded numerically. The agreement should define the colour space, the illuminant, the tolerated difference and the panels retained as references.
Pre-shipment inspection
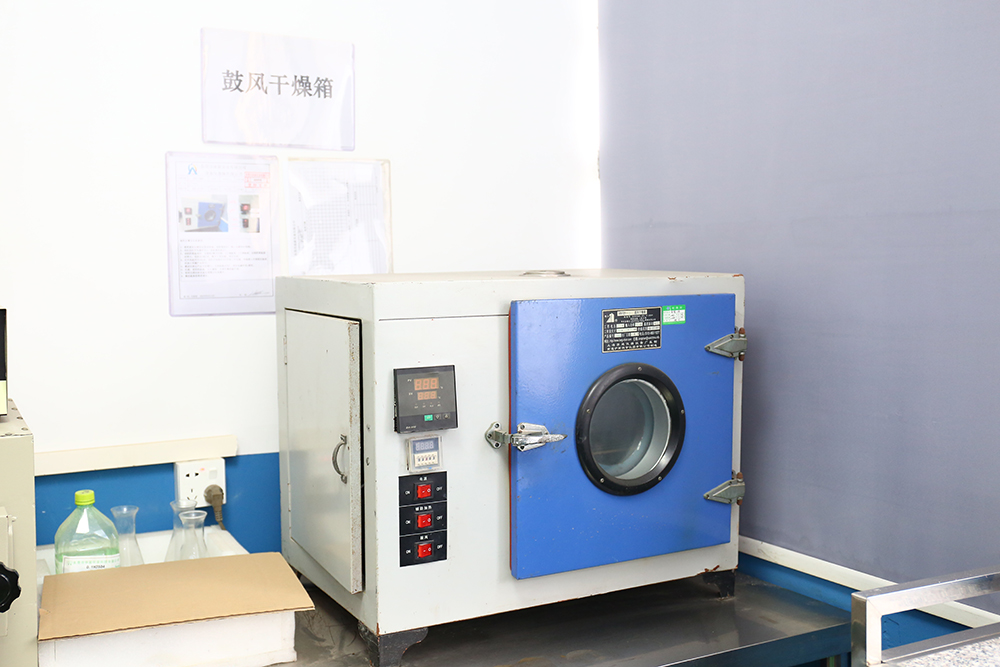
Yongxin's stated acceptance criterion is pre-shipment instrument detection, supported by 100% testing of products during quality control. Buyers should ask for the inspection record format in advance and confirm which characteristics are recorded per lot — thickness, colour, gloss, adhesion — so that the record can be compared across shipments.
Test Methods to Name in the Contract
Naming a test method converts a claim into a verifiable requirement. The methods below are those commonly referenced in electrocoating qualification work; each should be confirmed against the issuing organisation and the current edition before it is written into a contract.
| Property | Commonly referenced method | Why the buyer needs it named |
|---|---|---|
| Terminology and scope | ISO 22553-1:2019 | Provides a shared vocabulary for electro-deposition coatings across automotive and general industrial applications |
| Dry film thickness | ISO 2808; ASTM B767 | Fixes how the 15 to 25 micrometre window is measured |
| Adhesion | ISO 2409 cross-cut | Separates a coverage problem from a pretreatment problem |
| Humidity resistance | ISO 6270-2 | Tests performance in condensing conditions that salt spray alone does not capture |
| Neutral salt spray | ISO 9227 | Defines the corrosive environment behind the 1,000-hour claim |
| Rust and defect evaluation | ASTM D1654; ISO 4628 | Prevents disagreement over what counts as a failure |
ISO 22553-1:2019 is worth noting in its own right. It defines terminology for electro-deposition coatings and states applicability to automotive industries and other general industrial applications, including examples such as chiller units, consumer products, radiators, aerospace and agriculture. A shared vocabulary makes cross-border contracts cleaner, but it does not set a performance threshold — that remains a matter for the technical annex.
How the Pack Changes by Substrate and Application
The same document list applies across substrates, but the values inside it do not travel. Yongxin's electrophoretic coating scope covers black, white and colour finishes, high salt spray and corrosion-resistant grades, UV-resistant grades, epoxy resin and propionic acid resin systems, and both anionic and cationic processes, applied to zinc alloy, aluminium alloy, magnesium alloy, die-cast parts and stamped parts.
Magnesium alloy is the clearest illustration of why substrate-specific evidence matters. A peer-reviewed study of cathodic electrodeposition epoxy coating on AZ91D magnesium alloy used immersion and ASTM B117 salt spray testing over a total of 240 hours, and reported lower corrosion rate for the coated specimens than for the comparison conditions within that study. That is a useful, credible result — and it is not a 1,000-hour claim. Buyers specifying magnesium should request evidence generated on their alloy and geometry rather than inheriting a steel benchmark.
Application context shapes the file as well. Parts destined for automotive, bicycle, communication equipment, consumer electronics, drones and security hardware face different scrutiny: an automotive buyer will expect the full management-system set plus traceability, while a consumer electronics buyer may weight colour consistency and appearance documentation more heavily. The pack should be assembled for the end use, not copied from the previous programme.
Commercial Terms That Sit Beside the Technical File
Technical acceptance and commercial terms are usually negotiated by different teams, which is how mismatches occur. Yongxin's stated purchasing terms are a minimum order quantity of 100 units, negotiable for large orders; delivery terms of FOB or CIF, subject to negotiation; acceptance based on pre-shipment instrument detection; and 100% payment. Production lead time typically ranges from 3 to 45 days depending on order quantity, against a monthly production capacity of 2,500,000 units.
Two alignment points are worth raising early. First, if acceptance depends on pre-shipment instrument detection, the inspection record should be issued before the payment milestone, not after it. Second, if a programme requires third-party verification rather than in-house measurement, that should be agreed before the first production run, because it changes both the lead time and the documentation flow.
Supply continuity is the other commercial dimension. Yongxin's export share is 30%, with markets including Europe and America, Southeast Asia, Mexico, Poland, Turkey and Brazil — a spread that matters to buyers assessing long-term availability across multiple regions.
Where the Compliance Pack Ends: Honest Boundaries
A compliance file is a boundary document, and buyers should be explicit about where it stops.
- Management certification is not product certification. ISO 9001 and ISO 14001 describe how a site is run; they say nothing about the corrosion resistance of a specific film on a specific alloy.
- Low VOC is not zero impact. The e-coat process remains capital-intensive and continuous, with bath chemistry, ultrafiltration and rinse stages that must be maintained, and with wastewater treatment obligations that carry real cost.
- The declared chemistry covers the coating, not the substrate or pretreatment. Alloy composition and phosphating quality both influence final performance.
- A 15 to 25 micrometre window is a specification, not a guarantee. Buyers with severe service conditions should confirm that their corrosion target is validated at the lower end of that window, or agree a narrower band.
- E-coating is not the right answer for every finish. Compared with powder coating — a dry process with no liquid effluent — e-coating offers stronger penetration into cavities, recesses and edges, while powder coating avoids the Faraday cage limitations of spraying complex geometry. Buyers whose parts are simple, exterior-facing and cosmetics-led may find powder coating the more practical route.
What Buyers Should Expect Next
Two developments are reshaping how this file is assembled. The first is standardisation of vocabulary: ISO 22553-1:2019 gives buyers and suppliers a common language for electro-deposition coatings, which reduces the scope for a contract clause to mean different things on each side. The second is the persistence of cathodic epoxy as the dominant technology type in the global electrocoating market, which means most qualification templates will continue to be built around epoxy systems even as colour and appearance requirements diversify.
The practical consequence for procurement teams is that qualification is becoming documentation-led rather than sample-led. Suppliers able to produce traceable bath records, instrumented colour data and substrate-specific salt spray reports will clear approval faster than suppliers who can only offer a certificate and a promise. Buyers who build the document list into the RFQ — rather than requesting it after supplier selection — generally find the process shorter and the resulting agreement more durable.
FAQ
Which documents should an OEM buyer request before approving an e-coating finish?
At minimum: ISO 9001 and ISO 14001 certificates with the scope and site named; IATF 16949 where the end use is automotive; a written declaration covering water-based chemistry, heavy-metal-free status and VOC content; a film thickness specification with the measurement method; a neutral salt spray report recording substrate, film build, standard and result; colour and gloss records; batch and bath traceability; and the pre-shipment inspection format. Each item should be reviewed for what it establishes and what it leaves open.
Does ISO 9001 certification guarantee coating performance?
No. ISO 9001 certifies that a quality management system is in place and audited — procedures, calibration, corrective action and internal audit. It does not certify a film thickness, a colour tolerance or a salt spray duration. Performance requirements must be written into the technical annex and evidenced by test reports generated on the relevant substrate and build.
What do water-based, heavy-metal-free and low VOC actually cover?
They cover three different things. Water-based describes the carrier system of the paint bath. Heavy-metal-free describes the declared composition of the coating as supplied, and should name the restricted substances and thresholds. Low VOC describes emissions and should carry a value, a test method and a reference point. None of them covers the substrate alloy, the pretreatment chemistry or the site's wastewater obligations.
What film thickness and salt spray figures belong in the acceptance criteria?
Yongxin's stated range is 15 to 25 micrometres, measured by a named method such as ISO 2808 or ASTM B767, at defined locations on the part. High salt spray grades are specified against more than 1,000 hours of neutral salt spray testing, and the report should record substrate, measured build, test standard, scribe condition and evaluation criteria. Duration without those parameters cannot be compared across suppliers.
How is colour consistency controlled across repeat orders?
Through instrumented measurement rather than visual approval. Yongxin's inspection equipment includes a Konica Minolta spectrophotometer and a Zehntner gloss meter, which allow colour and gloss to be recorded numerically. The agreement should define the colour space, illuminant, tolerated difference and retained reference panels, and the pre-shipment record should report the measured values per lot.
What commercial terms normally accompany an e-coating compliance pack?
Yongxin's stated terms are a minimum order quantity of 100 units, negotiable for large orders; FOB or CIF delivery subject to negotiation; acceptance based on pre-shipment instrument detection; and 100% payment. Lead time typically ranges from 3 to 45 days depending on order quantity, and monthly production capacity is 2,500,000 units. Buyers should confirm that inspection records are issued before the payment milestone and agree in advance whether third-party verification is required.
Conclusion
The compliance pack for an electrophoretic coating programme is not administrative overhead. It is the mechanism that converts a supplier's capability into something a buyer can audit, repeat and defend. Read the certificates for scope and site, read the declarations for boundaries, and read the test reports for substrate, build and method. Where a claim cannot be tied to a named standard and a recorded result, it belongs in the marketing file rather than the quality file.
Dongguan Yongxin Industrial Co., LTD publishes its coating and process documentation, including certificates, equipment and process scope, at yxecoat.com. A full capability and product overview is available in the electrophoretic coating solutions brochure.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.