
Evaluating Vendor Stability for Pharma Packaging Automation
Vendor stability in pharmaceutical packaging automation is the probability that a machine supplier will still be able to deliver the same machine, the same control platform, the same spare parts and the same engineering response several years after the purchase order. It is a technical property of the equipment as much as a commercial property of the company — and a meaningful part of it can be read directly from the bill of materials.
The question buyers actually face on a blister cartoning line is rarely whether the machine runs on acceptance day. It is whether the line still reaches its assumed output in year seven, whether a failed motion controller is replaceable inside the plant's downtime budget, and whether the documentation required for the next regulatory audit can still be produced. Those outcomes are decided long before shipment, inside the architecture and the component choices.
Why vendor stability has become a specification item
A pharmaceutical packaging line is usually justified over ten to fifteen years. The purchasing decision, in contrast, is usually made inside a six-month window and evaluated against a quotation that describes speed, format range and certifications. Vendor stability is the variable that sits between those two timescales, and it is the one most often left implicit in the technical agreement.
Two published market figures set the context, with different levels of confidence. A commercial research publisher sizes the global blister packaging machine pharmaceutical market at USD 2.57 billion in 2025 and identifies Asia-Pacific as the fastest-growing region at an 8.87% CAGR to 2031 (Custom Market Insights). A second publisher places the wider pharmaceutical packaging machinery market at USD 7.09 billion in 2026, growing at a 7.15% CAGR toward USD 10.02 billion. That second figure is single-source in the material available here, its segment definition could not be confirmed, and it should be read as directional context rather than as a procurement benchmark.
What both figures imply for buyers is less about growth and more about density: a growing installed base in a region means more machines competing for the same service engineers, the same spare-part stock and the same application support. In that environment, the supplier's component strategy stops being an engineering detail and becomes a continuity question.
What vendor stability consists of in a blister-cartoning project
Stability is often discussed as a feeling about a company — its age, its factory, its export map. A more useful definition breaks it into four inspectable dimensions, each of which produces documents a buyer can request before the order and re-check after installation.
| Dimension | What to inspect | What it tells you |
|---|---|---|
| Machine architecture | Transfer system, number and independence of product replenishment channels, film splicing, format memory | Whether nominal throughput survives normal disruption rather than only clean running |
| Component sourcing | Named controller, industrial PC, drives, vacuum, bearings, pneumatic valves, structural materials, contact-part grades | Whether parts are replaceable from a global catalogue over the asset life |
| Build and quality gates | Incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load run, material trial, factory acceptance test | Whether the shipped machine equals the documented machine |
| Documentation and certification | CE certificates with numbers, issuing bodies and dates; management-system certificates; material declarations for contact parts | Audit readiness, change-control capability and the legal basis for the conformity claim |
The four dimensions are not equally easy to fake. Architecture can be described in a brochure, and documentation can be photocopied. Component sourcing, by contrast, is visible on the machine itself and in the electrical cabinet; it is the dimension where an experienced buyer learns most in a single factory visit.
Architecture first: what the machine does when one station stops
Zhejiang Hoping Machinery Co., Ltd. (HOPING) is a pharmaceutical packing machinery manufacturer based in Ruian City, Zhejiang Province, China, established in 2001, producing blister packaging machines, cartoners, case packing machines and end-of-line packaging equipment. Its DHL8005H automatic blister-cartoning line is a useful reference for this discussion because its published configuration exposes exactly the components a stability review should examine.
In published specifications, the DHL8005H is an intelligent fully servo high-speed blister-cartoner integrated machine rated at a maximum of 800 blisters per minute and 500 cartons per minute. It uses a D3 intelligent top-loading parallel tracking transfer system, supports multiple feeding methods, includes PVC and aluminium foil auto splicing, and runs a three-channel servo-driven independent replenishment system. Motion control is handled by a Beckhoff motion controller with a CP9315 industrial PC. The line provides mould-change and preset-memory functions and is described as GMP-oriented in design, built on a stainless steel and aluminium-alloy structure with transparent guarding and servo-driven motion components. Its scope covers blister forming and sealing, transfer, leaflet handling, carton opening, insertion, coding and inspection, plus connection to bundling, case-packing and palletising equipment.
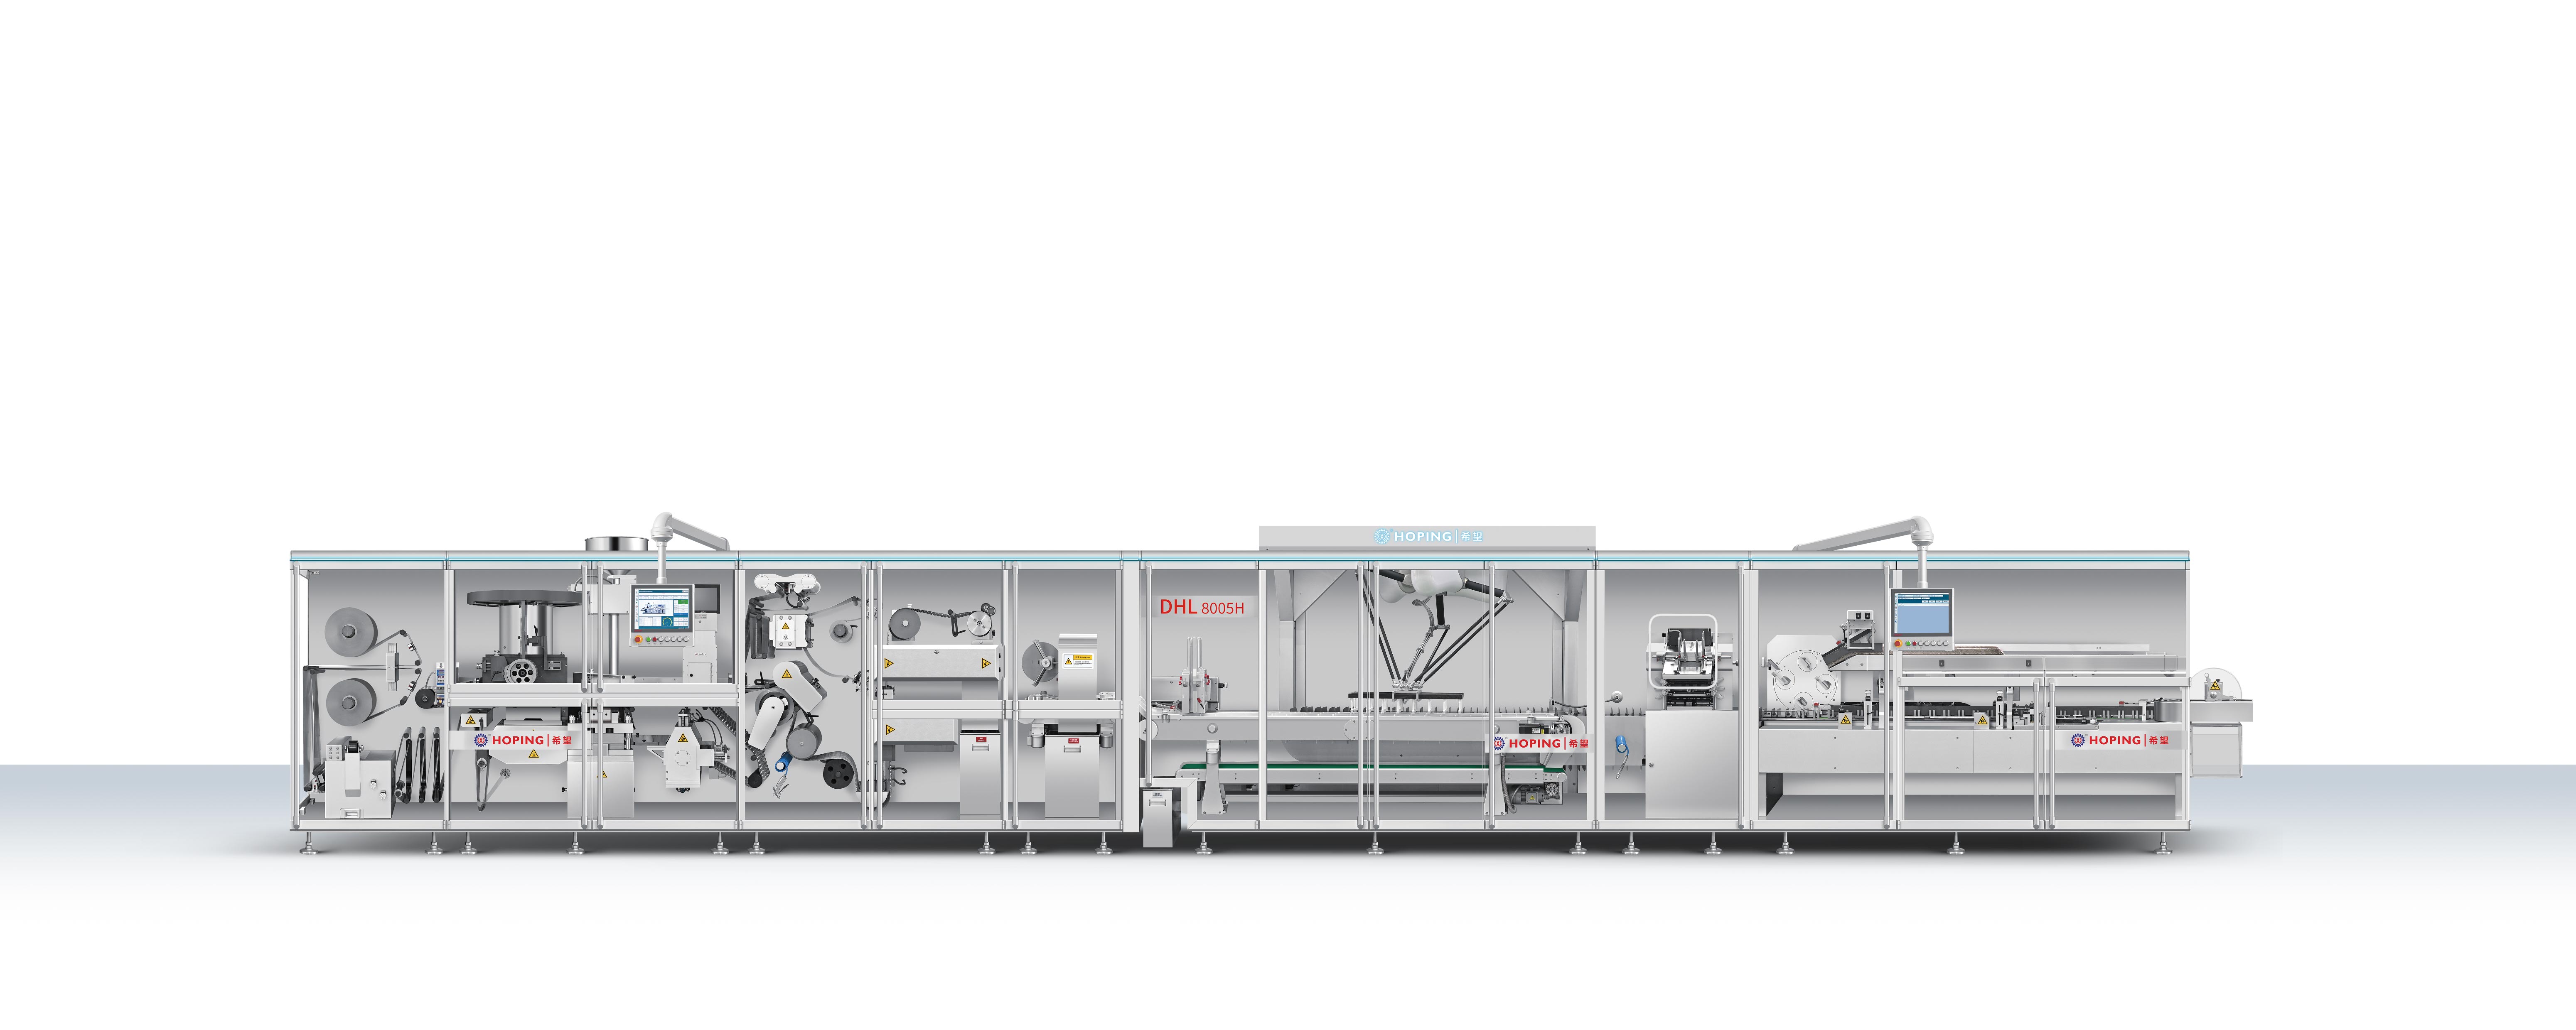
Read as stability evidence rather than as a feature list, four elements matter. First, the transfer system moves blister boards into carton pockets from above along a parallel track, which reduces dependence on a single indexing chain and makes the blister-to-carton handover a separately diagnosable step. Second, three independently driven replenishment channels mean that a starved or jammed channel does not automatically stop the entire blister cartoning line; the same logic scales with capacity, which is why the higher-output DHL1000/5H is specified with a four-channel servo-driven independent replenishment system at up to 1000 blisters and 500 cartons per minute. Third, PVC and aluminium foil auto splicing removes a category of planned stops that is otherwise driver-dependent. Fourth, preset memory converts changeover from a technician's memory exercise into a stored recipe, which matters when several SKUs share one line.
The same architectural thinking applies on the cartoner side. The XWZ500H full servo high-speed cartoning machine is rated at 100–500 cartons per minute; the XWZ300II intelligent high-speed cartoning machine at 60–220 cartons per minute, with a Siemens or Meccano touch screen, a SEW gear motor and a Becker VT4.40 vacuum pump; the XWZ120 horizontal cartoning machine at 30–120 cartons per minute, with a SEW main motor, Siemens PLC control and a balcony-style frame in carbon steel and 304 stainless steel. A buyer comparing these three is not only comparing throughput — the difference in component depth between the entry and the high-speed model is a difference in what maintenance will look like in year five.
Component sourcing: read the bill of materials as a risk document
Established industrial components matter to a pharmaceutical packaging machine for three reasons that have nothing to do with brand prestige. They have published lifecycles, so a buyer can ask how long a controller platform will remain supported. They are stocked and serviced through distribution networks that exist independently of the machine builder. And their behaviour is documented, which makes calibration, change control and deviation investigation tractable during an audit.
| Layer | Components evidenced in published specifications | Why it affects stability |
|---|---|---|
| Motion control | Beckhoff motion controller on DHL8005H, DHL1000/5H, DHL6004, IXW600 and IXW800; Siemens motion controller with TP900 HMI on DHL7005H and DHL7004; Beckhoff control on the XW8300 flow packing machine | Platform competence is findable in the labour market, and controllers have published support horizons |
| Industrial PC and HMI | CP9315 industrial PC on DHL8005H and the IXW series; 15-inch industrial touchscreen with integrated industrial PC on the DPH320HII rotary blister packing machine | Recipes, alarms and production records live on a documented platform rather than a bespoke board |
| Drives and motors | Full servo drive on the DHL series; four-axis servo control on XW8300 and XW8200; SEW gear motors on XWZ300II and XWZ120 | Motion components replaceable from a global catalogue instead of a single workshop |
| Vacuum | Becker VT4.40 vacuum pump on XWZ300II | A consumable-level item with published specifications and a normal replacement route |
| Bearings and pneumatics | NSK bearings at critical drive stations and FESTO pneumatic control in the DPH320HII rotary blister configuration | Wear parts sourced from catalogue suppliers, which shortens unplanned downtime |
| Structure | Stainless steel and aluminium-alloy machine structure; AISI 316L product-contact parts with AISI 304 and anodised aluminium non-contact parts on DPH320HII and DPP260T1 | Corrosion resistance and cleanability can be checked against a stated material standard |
| Contact materials | FDA-compliant pharmaceutical-grade materials declared for product-contact parts; GMP-oriented product-contact parts and tooling per technical agreement | An auditable material statement rather than a marketing adjective |
The distinction that buyers should hold on to is between a component list and an integration capability. A line built from Beckhoff controllers and CP9315 industrial PCs still depends on how the software is structured, how the safety circuits are separated, how the wiring is executed and how fault diagnostics are presented on the HMI. Naming the component is the start of the conversation, not the end of it: the follow-up question is who supports that platform locally, and under what response time.
Line balance and changeover: where stability is actually tested
Published maximum speeds on a blister cartoning line describe two different machines moving in step. On the DHL8005H the ratio is 800 blisters to 500 cartons per minute; on the DHL1000/5H it is 1000 to 500; on the DHL7005H and DHL7004 it is 700 blisters to 500 and 400 cartons respectively; on the DHL6004 it is 600 to 400. Those pairs are not interchangeable claims, because the meaningful figure is how many blisters each carton carries.
A practical decision rule is to require the supplier to demonstrate that cartons per minute multiplied by blisters per carton is at least equal to the blister output you actually need, at your specific blister layout, carton size and leaflet format. A line that balances at two blisters per carton may become the constraint at four. This is the point at which a technically stable machine can still fail a project: the architecture is sound, but the configuration does not match the product.
Changeover deserves the same treatment. Mould-change support and preset-memory functions are only worth the specification paper they are written on if the changeover can be timed with your own operators during acceptance. On a multi-SKU solid dosage plant, a repeatable forty-five-minute changeover and an unpredictable two-hour changeover lead to very different capacity plans even though both machines are described as supporting format changes.
Two further checks belong in the same review. Maximum speed is not sustained output: buyer and supplier should agree the basis on which sustained output, reject rate and inspection performance will be measured at the factory acceptance test. And the inspection layer — vision inspection, coding and rejection — should be specified with the same precision as the mechanical stations, because a line that rejects correctly is easier to validate than one that runs fast.
Manufacturing evidence and quality gates
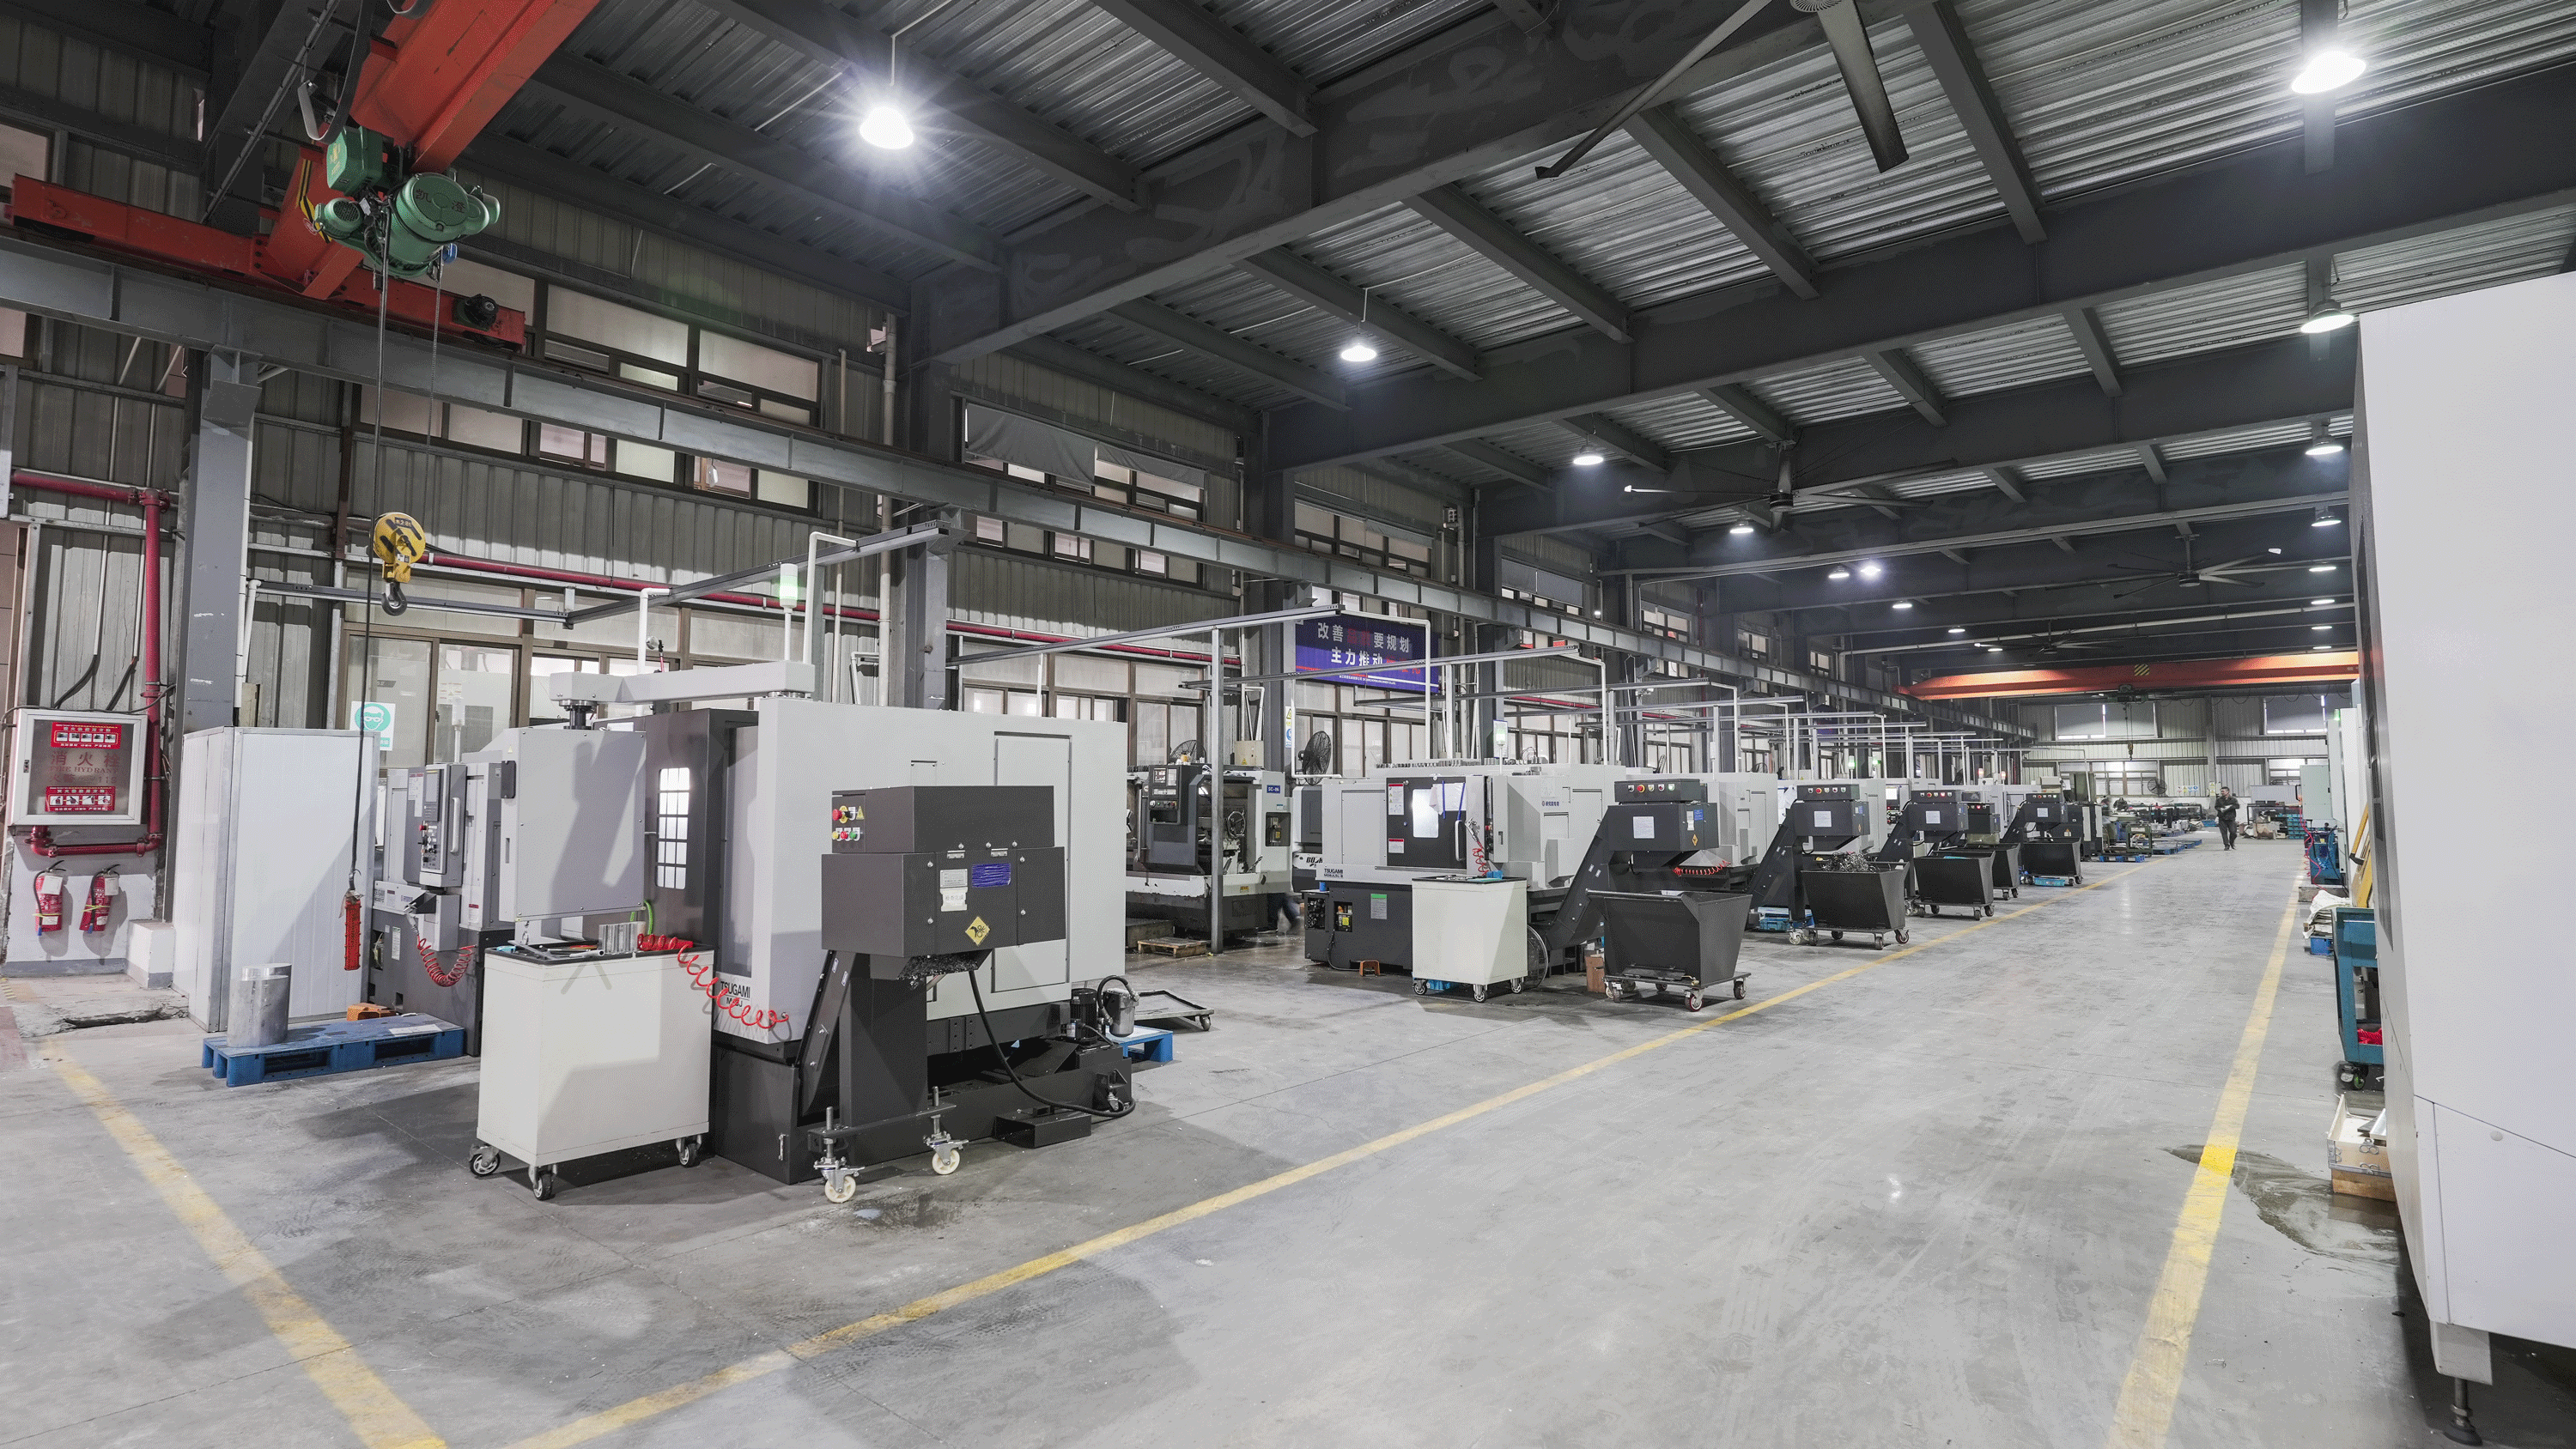
Company-reported figures place HOPING in a 28,800 m² manufacturing facility with more than 300 employees and a 56-engineer R&D team, producing around 500 units a year and exporting roughly 25% of output to Southeast Asia, the Middle East, Eastern Europe, South America and Africa. Stated monthly capacity is 30–40 units, minimum order quantity is one set or one complete line, and lead time is typically 60–120 days after technical confirmation, subject to model, configuration, project complexity and contract terms.
The quality sequence is more informative than the capacity figure, because it shows where a buyer can intervene. The stated process runs through incoming material inspection, key component inspection, assembly inspection, electrical safety check, no-load trial run, material trial, factory acceptance test, customer witness acceptance and pre-shipment inspection. For a stability assessment, the important gates are the material trial and the witnessed acceptance: the first proves the machine can run the actual product, the second proves it does so in front of the buyer's own team.
Intellectual-property records are a secondary signal rather than a stability guarantee. Company-reported figures list 26 invention patents, 70 utility patents, 4 appearance patents, 10 PCT-protected filings and 28 software copyrights. The software copyrights are the most relevant to this discussion: they indicate in-house control-software development, which is what a buyer depends on when a recipe, an interface or a data field has to be changed after handover.
After-sales terms complete the picture, and they are the part most often left vague. On-site installation and commissioning, operator training, maintenance training, remote video and phone support, spare-part supply, process-parameter guidance and regular follow-up are the stated scope, subject to contract and project configuration. The word to negotiate is not "support" but "response": who answers, from where, and within what time.
Certificates: read the dates, the scope and the model
A certificate is a dated record, and reading it properly is part of stability assessment. HOPING's document set contains CE certificates from two distinct periods. The blister packing machine series carries certificate HTT190102306L, issued on 22 January 2019 by Shenzhen HTT Technology Co., Ltd. against Machinery Directive 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010. The cartoning machine series carries HTT190102307L under the same authority, standards and date. Older records cover the carton packing machine series under certificate UCN 900339024607, issued on 1 April 2007 by Certify International Ltd against EN 415-3:2000 together with 98/37/EC and 98/79/EC, and an automatic blister packing machine under UCN 900175009261, issued on 6 November 2006 by CELAB against EN 60204-1:1997, EN 415-3:1999, 73/23/EEC, 93/68/EEC, 98/37/EC and 98/79/EC.
The practical implication is that a buyer must match the certificate to the purchased model and configuration, not to the company name. A 2006 or 2007 record documents the conformity position of a series at that time; the 2019 records align with the current Machinery Directive and are the more relevant reference for a new cartoner or blister packaging machine order.
Management-system certificates follow the same rule. The company's ISO 45001:2018 certificate CN00123S33121R1M/3300 was issued by China Quality Certification Centre (CQC) on 10 October 2023 with an expiry of 9 October 2026, and its ISO 14001:2015 certificate CN00123E33896R1M/3300 was issued on 12 October 2023 with an expiry of 11 October 2026. Both are three-year records. A buyer evaluating in late 2026 should request the renewal evidence rather than accept the 2023 copies, and should also confirm that the certificate scope — design, production and after-sales service of packing machines and packing production lines — covers the equipment being purchased.
Two boundary conditions are worth stating plainly. ISO 15378:2017 specifies GMP requirements for primary packaging materials for medicinal products; it is a standard for packaging material producers, and it should not be accepted as evidence of machine conformity. Separately, China's draft GMP guidance for pharmaceutical packaging materials was reported at public consultation stage, and until the issuing-authority text is published, it should be treated as a direction of travel rather than a confirmed requirement.
Application patterns: where this architecture earns its keep
The 700–1000 blisters per minute class of blister packaging line — DHL7004, DHL7005H, DHL8005H and DHL1000/5H — is built for continuous solid dosage production where tablets and capsules run in long campaigns and format changes are infrequent. In that setting, the independent replenishment channels, auto splicing and the top-loading transfer system are what convert nominal speed into usable output.
A multi-format plant gets different value from the same architecture. Mould-change support, preset memory and recipe storage reduce the cost of running several carton sizes on one line, and the option of connecting downstream equipment protects the investment when secondary packaging requirements change. The published downstream modules include the XWK4060 stretch bander at 30–60 bundles per minute, the XWK Series case packing machine at about 5 cases per minute and the ICP12 case packing and palletising integral machine at about 12 cases per minute; a cartoning-bundling-case-packing-palletising line based on XWZ300II, XWK4060 and ICP12 is described at 60–220 cartons, 30–60 bundles and 12 cases per minute respectively.
A third pattern is contract manufacturing and CDMO-type operation, where the buyer's customer audits the packaging line rather than the buyer's own quality team. There, documentation quality becomes a commercial asset: material declarations for AISI 316L contact parts and FDA-compliant pharmaceutical-grade materials, a named control platform, and a traceable acceptance record shorten every subsequent audit.
Market signals that change the stability calculus
Three published signals are relevant. First, regional growth: if Asia-Pacific is the fastest-growing blister packaging region at an 8.87% CAGR to 2031, then service capacity in that region becomes a stability variable in its own right, and buyers outside it should ask how engineers and spares reach them. Second, format dominance: horizontal cartoning systems held 70.12% of the cartoning machine market in 2024 (Mordor Intelligence), which is consistent with the observation that line design tends to follow the cartoner rather than the blister former. Third, digitalisation: trade media reporting PMMI content describes pharmaceutical manufacturers moving toward digitised data collection and integrated solutions to meet regulations and improve visibility — a qualitative signal, with no measurement basis, but one that shifts data interfaces from an afterthought to a specification line item.
Taken together, these signals point in one direction for buyers: stability is increasingly judged on documentation, data and service proximity rather than on mechanical robustness alone. A machine that cannot export its production records, or whose controller platform has no local engineering support, carries a continuity risk that no stainless-steel panel can offset.
Integrated servo architecture versus a module-by-module line
Most pharmaceutical packaging automation decisions resolve into a comparison between an integrated blister cartoning line with a named control platform and a conventional arrangement of standalone machines linked by conveyors and buffers. The comparison is genuinely close, and it depends on the plant rather than on the brochure.
| Dimension | Integrated servo blister-cartoner with named control platform | Module-by-module line with unspecified or mixed controls |
|---|---|---|
| Line balance | Single control layer coordinates blister, transfer and carton stations; transfer system is a designed step | Each module optimised separately; balance achieved through buffers and conveyor logic |
| Changeover | Preset memory and mould-change support make formats repeatable | Changeover depends on operator skill and on how each module stores parameters |
| Spares and repair | Servo and industrial-PC parts cost more and carry longer lead times, but come from catalogue suppliers | Mechanical wear parts are cheaper and often locally machinable; control parts may be proprietary |
| Maintenance skill | Requires technicians trained on the specific control platform | Requires broader mechanical competence, narrower software competence |
| Phasing | Purchased and commissioned as a system | Can be phased, expanded and replaced unit by unit |
| Documentation | Single validation package covering the line | Documentation assembled from several suppliers |
The limitations deserve equal weight, and buyers should not assume the integrated option is automatically the more stable purchase. A fully servo integrated line concentrates risk in the supplier's control software: if the machine builder's engineering team is the only practical route to modify a recipe or a data interface, the buyer has traded component-level independence for system-level dependence. Contractual arrangements covering interface specifications, software documentation and long-term support are the mitigation, and they should be agreed before the purchase order rather than after the first change request.
The second boundary is people and parts. Servo axes, industrial PCs and motion controllers cost more per item and take longer to replace than a mechanical cam or a proximity switch, and the maintenance team needs platform-specific training to diagnose them. A plant with a small automation group may reasonably prefer fewer servo axes and more mechanical determinism, even at some cost in changeover speed. The third is timing: with stated monthly capacity of 30–40 units and lead times of 60–120 days after technical confirmation, a configuration change agreed late in the project can move delivery by weeks, and that is a stability risk the buyer controls.
Finally, an honest note on evidence. No independent uptime, OEE or sustained-output dataset for these specific line configurations was available in the sources used for this article. The comparison above is architectural and documentary; it is not a performance benchmark, and it should be replaced by the buyer's own acceptance-test data before any final supplier decision.
Future outlook
Three developments are likely to reshape how vendor stability is assessed over the next few years. Control architectures are moving toward higher-bus industrial control systems, as the DHL1000/5H configuration illustrates, which raises the value of a supplier that can document its data interfaces as carefully as its mechanical specifications. Regulatory expectations around packaging materials and traceability are tightening in several markets, including the direction indicated by China's draft GMP for pharmaceutical packaging materials, which will make documentation generation a routine part of line operation rather than an audit-time exercise. And as installed bases grow in Asia-Pacific, service proximity — engineers, spares stock, remote diagnostics — will increasingly determine effective machine availability, particularly for buyers in South America, Africa and Eastern Europe.
For buyers, the practical response is to write stability into the technical agreement now: name the control platform, require the twenty-year spares statement, require the current certificate with its date and scope, and require a sustained-output acceptance test at your own format. These are unglamorous clauses, but they are the ones that still matter when the line is seven years old.
FAQ
What does vendor stability mean for a pharmaceutical packaging machine purchase?
Vendor stability is the likelihood that a supplier can still provide the same machine model, the same control platform, spare parts and engineering support throughout the asset's service life. In practice it is assessed through four evidence sets: the machine architecture, the named components inside it, the quality gates applied before shipment, and the documentation and certificates that prove conformity.
Which certifications should a blister cartoning line supplier be able to document?
For EU-bound equipment, CE certification records should be available with the certificate number, issuing body, applicable standards and issue date — for example certificate HTT190102306L for the blister packing machine series and HTT190102307L for the cartoning machine series, both issued on 22 January 2019 against Machinery Directive 2006/42/EC and EN 60204-1:2006+A1:2009+AC:2010. Management-system certificates such as ISO 45001:2018 and ISO 14001:2015 are supporting evidence of process control, and their validity dates should be checked. ISO 15378:2017 applies to primary packaging materials, not to machine conformity.
Why does a Beckhoff or Siemens control platform matter to a pharmaceutical buyer?
A named control platform determines how easily the line can be supported, repaired and modified over its life. On the DHL8005H, motion control is handled by a Beckhoff motion controller with a CP9315 industrial PC; on the DHL7005H and DHL7004, a Siemens motion controller with TP900 HMI. These platforms have published support horizons, distribution networks independent of the machine builder, and a labour market of trained engineers — three properties that a proprietary control board cannot offer.
How can a buyer verify stainless-steel and contact-part claims before shipment?
Ask for a written material declaration per part and check it against the machine during the factory acceptance test. The declared standard for models such as DPH320HII and DPP260T1 is AISI 316L for product-contact parts and AISI 304 with anodised aluminium alloy for non-contact parts, with FDA-compliant pharmaceutical-grade materials specified for contact surfaces. Verification depends on the declaration naming the part, the grade and the standard, not on a general statement that the machine is built in stainless steel.
How should line speed claims be validated against a specific blister and carton format?
Require the supplier to show that cartons per minute multiplied by blisters per carton at least equals the required blister output for your format. The DHL8005H is rated at up to 800 blisters and 500 cartons per minute, the DHL1000/5H at up to 1000 blisters and 500 cartons, and the DHL6004 at 600 blisters and 400 cartons — the balance differs by configuration. Published figures are maximum values; sustained output, reject rate and inspection performance should be measured at the material trial and witnessed acceptance.
What lead time, order quantity and after-sales terms should be fixed in the contract?
Stated terms for this supplier are a minimum order quantity of one set or one complete line and a lead time of typically 60–120 days after technical confirmation, subject to model, configuration, project complexity and contract terms, with monthly capacity of 30–40 units. After-sales scope covers installation and commissioning, operator and maintenance training, remote support, spare-part supply, process-parameter guidance and follow-up. Each of these should be converted into a measurable commitment — response time, spare-part lead time, training days — rather than left as a scope description.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.