
Milling Tools Shortlist: Silent Tools, GFN Cutters, and Product 6046
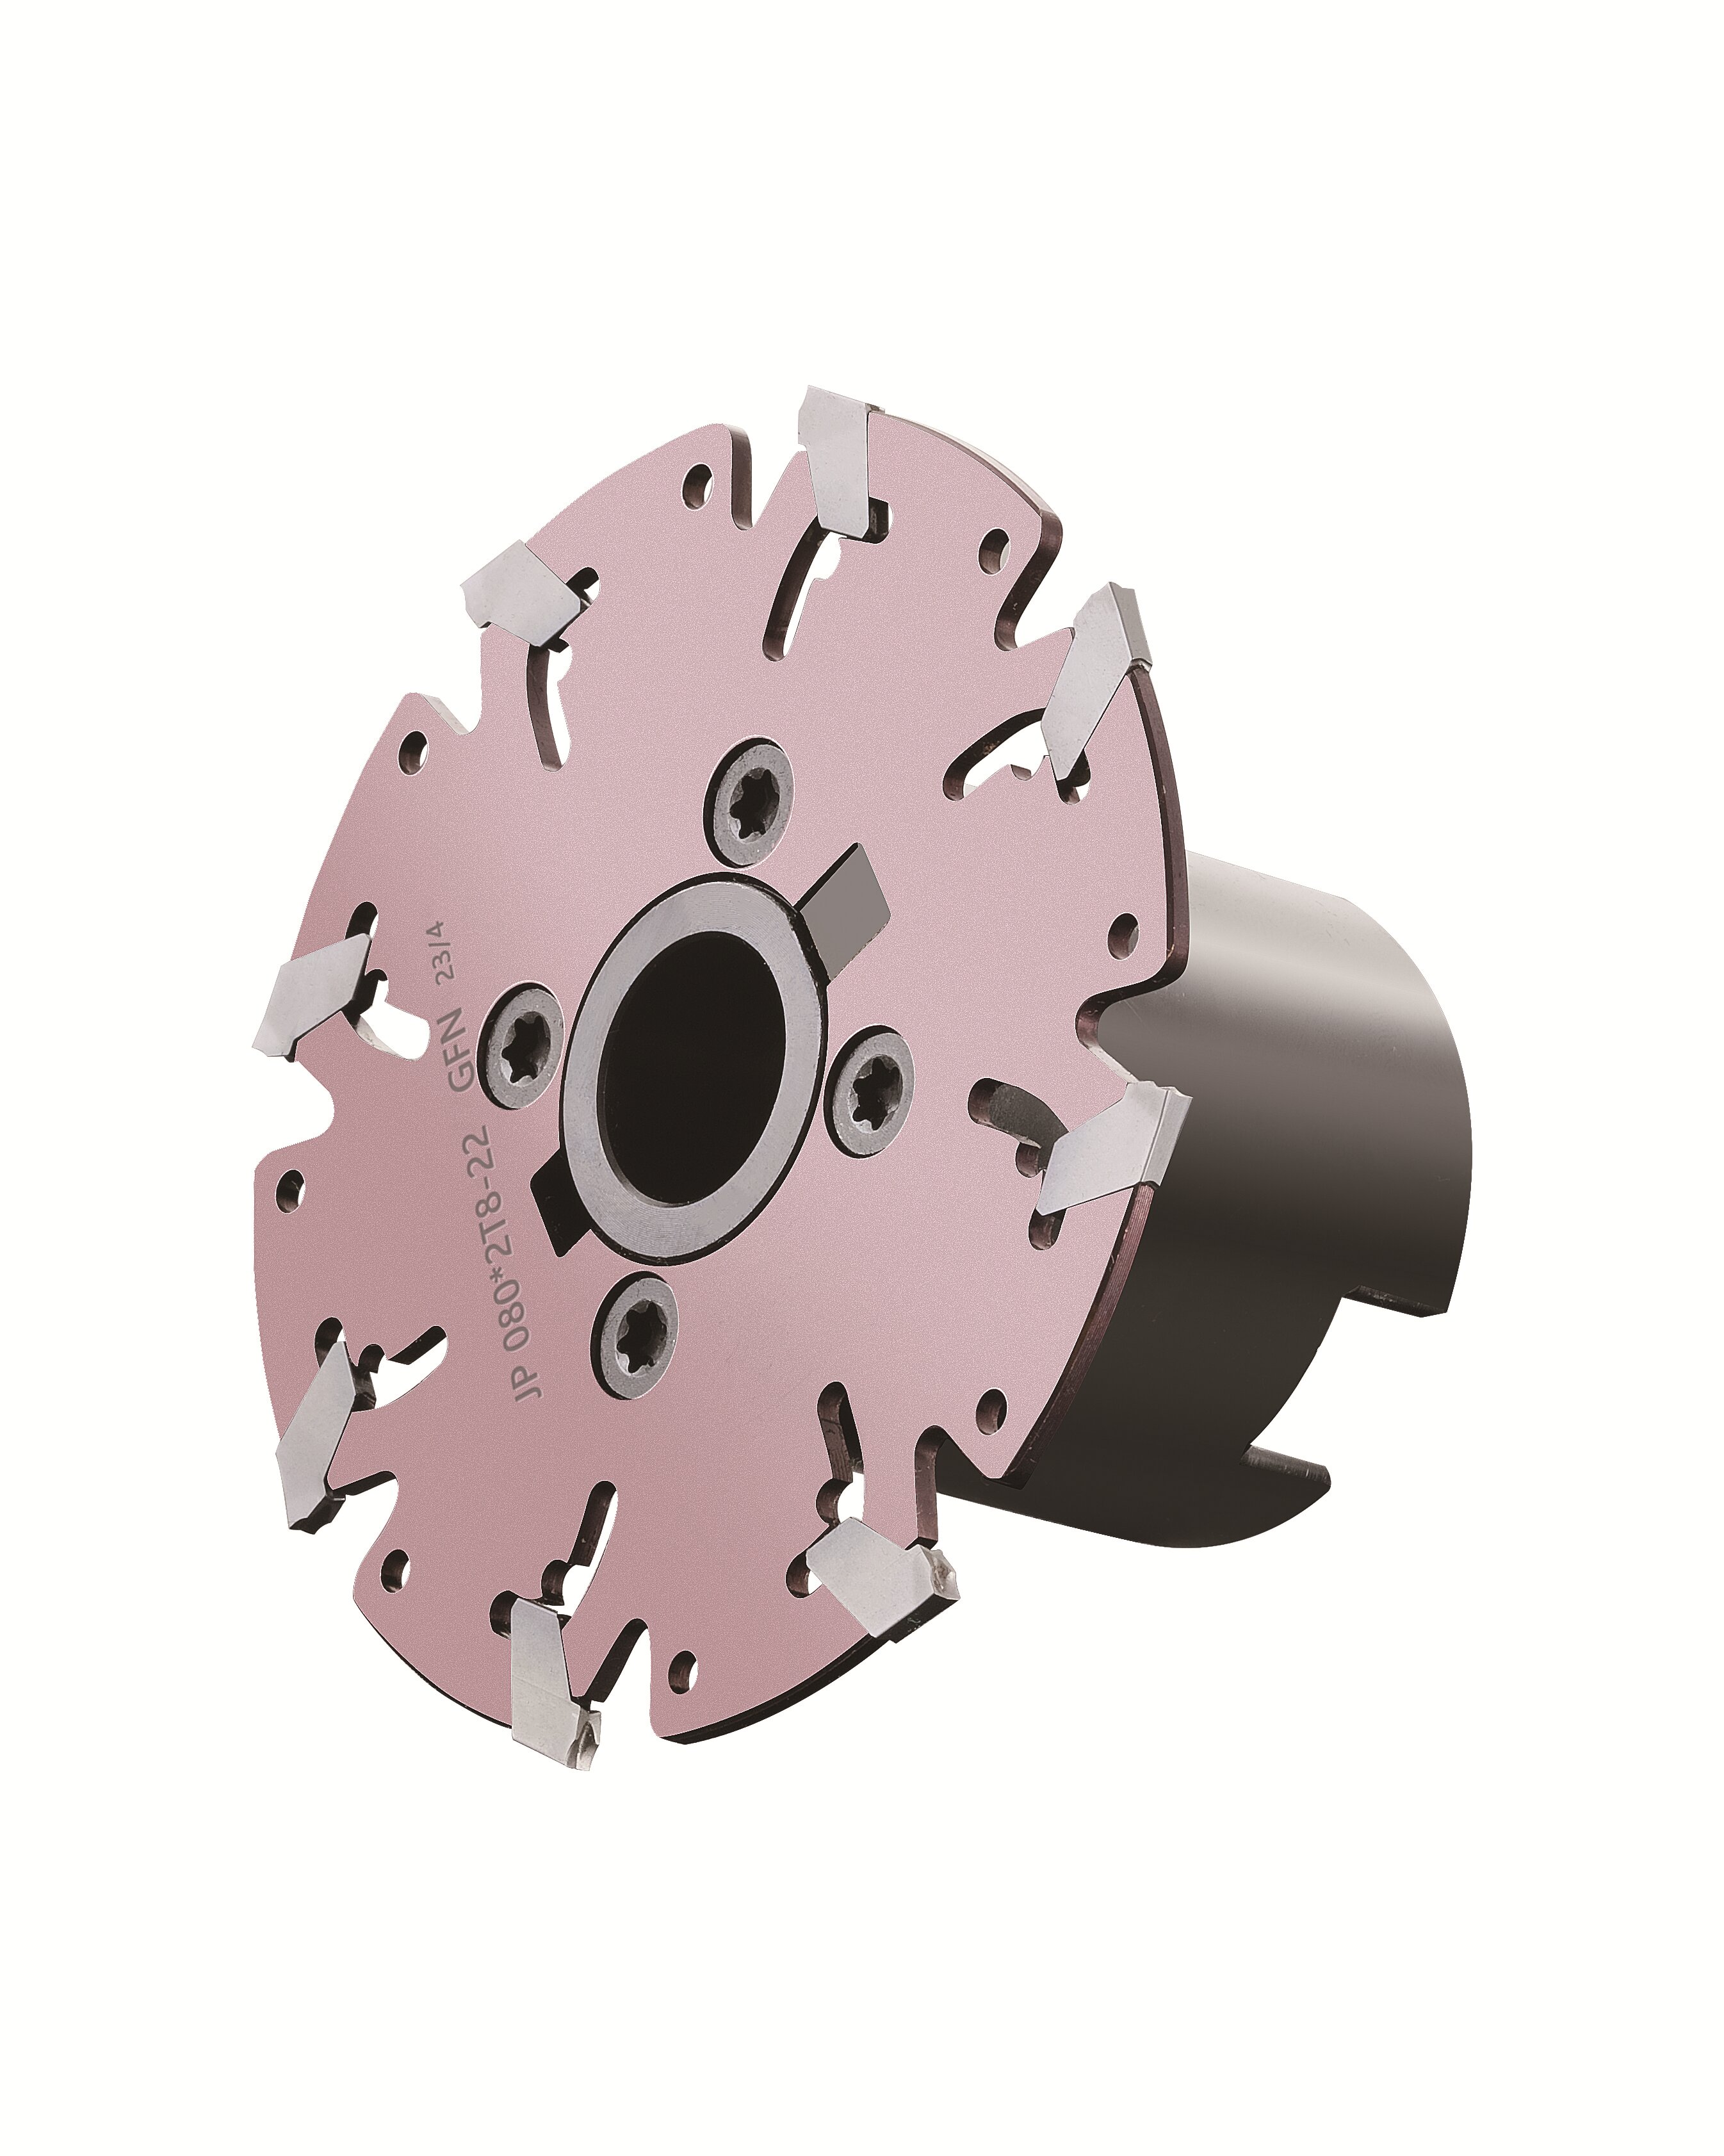
Three machining conditions decide most milling tool purchases in precision work: a cut deep enough to vibrate, a groove narrow enough to break a conventional cutter, and a diameter range wide enough that one dedicated tool per size stops making commercial sense. Each condition needs a different tool, and treating them as a single buying decision is where shortlists usually fail.
The shortlist below covers three options from Wenling Geltos Tools Co., Ltd.: silent tools, GFN cutters and the product 6046 milling series. Wenling Geltos Tools Co., Ltd. is a milling tool manufacturer founded in Zhejiang Province, China, in 2012, producing grooving mills, chamfer mills, thread mills, dovetail mills, face, shoulder and profiling mills, interchangeable and modular milling tools, silent tools and milling inserts, with reported export activity in India, Russia, Iran, Morocco, Italy and the USA. All three options sit inside one supplier's capability, which matters for a buyer consolidating vendors, but they answer three separate machining problems and the verification work differs for each.
Shortlist at a glance
| Option | Machining problem it addresses | Documented specification in this article | Buyer stage fit |
|---|---|---|---|
| Silent tools | Vibration in deep cutting, typical of aerospace, military and shipbuilding work | Anti-vibration cutter design for deep-cut scenarios | Evaluation |
| GFN cutters | Narrow grooving down to 2 mm width | 2 mm grooving case, precision machining factory, 5 units, 2 years of use | Evaluation to execution |
| Product 6046 | Coverage across diameters, widths and lengths without one tool per size | Diameters 40-250 mm, widths 1-20 mm, lengths 80-350 mm, 1-20 teeth | Execution and repeat order |
The table works as a routing map. Identify the machining condition first, then read only the section that applies. A mould shop fighting chatter in a deep cavity and a job shop running 2 mm grooves in small batches are not shopping for the same product, even though both are shopping for milling tools.
Why a three-item shortlist beats a catalogue page
A catalogue answers what exists. A shortlist answers what fits. The difference becomes visible at the evaluation and execution stage, when a buyer already knows the operation and needs to decide which tool geometry, which insert and which commercial terms will hold up across the order.
Four screening criteria were applied to build this shortlist:
- Geometry first. The cut shape - deep wall, narrow slot, wide face - eliminates most of a catalogue before price is discussed.
- Vibration exposure. Long-reach cutting on hard material fails through chatter before it fails through wear, so damping has to be a tool property rather than an operator workaround.
- Insert and replacement logic. A cutter body is only as useful as the insert supply behind it and the time needed to change it.
- Verification that a buyer can actually perform. Specifications a supplier cannot document are planning inputs, not acceptance criteria.
Wenling Geltos Tools Co., Ltd. supports these criteria through milling tool R&D, production, sales, OEM work, tool material development, customization and tool design, including non-standard production, special geometry tool design and special material development. That capability is what makes a shortlist possible from one source; it is also what makes each item below worth describing separately.
1. Silent tools: anti-vibration cutters for deep cutting
Silent tools are milling cutters built around an anti-vibration design, intended for deep cutting operations where a conventional cutter would deflect, chatter and force the operator to reduce depth or speed. The scenario set is specific: aerospace structural work, military components and shipbuilding, all of which combine long reach, demanding surface requirements and materials that punish unstable cuts.
The industry logic is straightforward. In deep cutting, the limiting factor is rarely the cutting edge itself; it is the dynamic behaviour of the whole tool assembly. A cutter that damps vibration lets the programmer keep the intended depth of cut instead of trading productivity for stability. For a buyer, that changes the comparison: a silent tool is not a premium version of a standard cutter, it is a different answer to a stability constraint that standard cutters do not address.
What to confirm before committing a silent tool to a process
- The reach and depth the tool is expected to hold, expressed as the actual operation, not a general capability claim.
- Whether the damping behaviour is documented in a form the buyer's own trial cut can confirm.
- How the tool interfaces with existing holders and machine tapers, since a damped cutter inside a weak holder still cuts badly.
- Whether the same source supplies replacement heads or inserts, so the tool does not become a single-source dead end.
2. GFN cutters: narrow grooving down to 2 mm
GFN cutters address a different failure mode. Narrow grooving is where thin cutting edges meet side load, and where a conventional slotting approach produces chatter marks, short tool life or a groove that drifts off width. Geltos positions the GFN range around grooving as thin as 2 mm, which is the threshold where tool strength and surface finish usually start competing.
The most concrete evidence available for this range is a two-year application in a precision mechanical processing factory in Russia. The customer operates 5 units for precision metal grooving and slotting, cutting 2 mm width slots, with reported results of smooth surface finishing, fast-feed grooving and long working life over the two-year period. The GFN model referenced in that application is JP 100*2.0T10-FMB22 GFN2.0J.
For procurement, the narrow-grooving question is usually framed as cost per groove rather than cost per cutter. A 2 mm cutter that survives the run and leaves a finish that does not need rework is cheaper than a standard cutter that has to be replaced mid-batch, even at a higher unit price. That reframing is the practical reason to shortlist a dedicated grooving tool rather than defaulting to a general-purpose mill.
3. Product 6046: a parameterised milling series
Product 6046 is the widest item on this shortlist. Rather than a single cutter, it is a series defined by a diameter, width, length and tooth-count envelope, which is what allows a buyer to cover several operations with one specification family instead of a drawer of one-off tools.
| Series parameter | Range | Procurement implication |
|---|---|---|
| Diameter | 40-250 mm | Spans small-diameter finishing work through large shell and face milling operations |
| Width | 1-20 mm | Covers narrow grooving through wider slotting within the same family |
| Length | 80-350 mm | Addresses reach requirements without moving to a separate tool family |
| Teeth | 1-20 | Tooth count can be matched to feed rate and chip load rather than accepted as fixed |
Tool model codes documented within the product 6046 reference set include HTS-20-H06-C16T4-120 SP04, JP 100*2.0T10-FMB22 GFN2.0J, MG2009-W150T50, MC H16-20-09-N, B45 SP03 C10T1-120ap4-8 and T2139 C10-R4-120, alongside insert references SPMG050204, LNMU03-20 20T3-160, SNMX12064-050T4-22 and SEKT1204. For a buyer, the practical lesson is that a quotation should name the model code and the insert, not simply the series, because the same series envelope contains configurations with very different behaviour.
Insert compatibility and cutting parameter references
Carbide insert models referenced as compatible with the shortlisted tools include APMT1135, SNMX1206, LNMU0303ZER and 4NKT0603. The material and parameter references that accompany this range are a workpiece hardness of up to HRC 65, a cutting speed reference of V = 180 and a feed reference of F = 0.02.
| Insert designation | Listed for | What to confirm at quotation |
|---|---|---|
| APMT1135 | Product 6046 milling range | Grade and coating for the specific workpiece material; corner radius |
| SNMX1206 | Product 6046 milling range | Seat compatibility with the ordered body; grade availability |
| LNMU0303ZER | Product 6046 milling range | Edge preparation and expected wear pattern in the target material |
| 4NKT0603 | Product 6046 milling range | Availability as a repeatable supply item, not a one-off |
| Parameter | Reference value | Buyer action before programming |
|---|---|---|
| Workpiece hardness | Up to HRC 65 | Confirm the upper bound applies to the exact grade quoted, not the range in general |
| Cutting speed | V = 180 | Confirm the unit basis with the supplier before converting to spindle speed |
| Feed | F = 0.02 | Confirm whether the value is per tooth or per revolution |
| Tool teeth | 1-20 (product 6046) | Match tooth count to the intended feed and chip evacuation |
These figures should be treated as starting references for a trial cut. Cutting parameters are a function of workpiece material, machine rigidity, holder condition and coolant strategy, so a published value that has not been validated on the buyer's own equipment is a planning input, not an acceptance criterion. The sensible execution step is to run a first-article trial at the reference values, record the result, and adjust from a measured baseline.
Matching the shortlist to automobile, mould and general machining
The three options map onto three common production contexts, and the mapping is more useful than any single recommendation.
Automobile and high-volume metal cutting
Cycle time dominates. Here the 6046 series envelope is the relevant item, because diameter, width and tooth count can be fixed once and repeated, and the interchangeable and modular holder concept reduces the time lost to tool changes by keeping one holder and changing only the milling head. The narrow-grooving capability also matters where small slots recur within a stable process.
Mould and die work
Deep cavities, long reach and surface finish requirements push the decision toward vibration control. Silent tools target exactly this condition, and the practical benefit is the ability to hold depth of cut instead of reducing it. Profiling and shoulder milling within the broader Geltos range support the surrounding operations.
General and job-shop machining
Mixed batches reward breadth over specialisation. A series that spans 40-250 mm diameters and 1-20 mm widths, backed by a common insert set, reduces the number of tool families a shop has to stock, qualify and reorder. Customization matters here too: Geltos supports non-standard production, special geometry tool design and special material development, which is where a job shop's recurring odd operation usually ends up.
Conventional alternatives, and where this shortlist stops
Standard solid carbide and indexable cutters remain the correct default for stable, moderate-depth work in common materials. The comparison is not about superiority; it is about which constraint is binding.
| Condition | Conventional approach | Shortlisted approach | Trade-off to accept |
|---|---|---|---|
| Deep cutting with long reach | Reduce depth of cut or speed to control chatter | Silent tools with anti-vibration design | Higher tool cost and a more complex tool assembly that must be proven on the machine |
| Narrow grooving at 2 mm | General-purpose mill or thinner slotting cutter | GFN cutters sized for narrow grooving | Dedicated geometry that is less flexible outside its groove range |
| Wide size coverage | One dedicated tool per size | Product 6046 series with modular heads | An interface to control, and a payoff that depends on having enough size variety to justify it |
Modular systems carry one further limit worth stating plainly. Moving from many complete tools to a smaller number of holders plus interchangeable heads shifts spending rather than eliminating it, and it only pays back where the size mix is genuinely wide. A shop running two fixed operations on a stable product line will usually not recover the added interface complexity.
Procurement terms and customization
Commercial mechanics are part of the evaluation, not an afterthought. For the shortlisted range, the minimum order quantity is 1 unit, delivery is arranged on FOB terms, payment is 100% telegraphic transfer, and a pre-shipment test forms part of the acceptance criteria. Quoted lead time is 10-30 days.
Customization sits alongside those terms. Geltos provides milling tool R&D, production, sales, OEM work, tool material development, customization and tool design, including non-standard production, special geometry tool design and special material development, with after-sale service and technical support behind the supply. For a buyer at execution stage, the sequence that works is: define the operation, request the model code and matching insert designation, confirm the parameter basis in writing, agree the pre-shipment test, and only then place a first order at the 1-unit minimum to validate before scaling.
Market context: why shortlists are getting narrower
The milling tools market was valued at US$ 3.43 billion in 2025 and is forecast to grow at a compound annual rate of 6.2% over 2026-2035, according to DataM Intelligence research. Growth of that order does not change how a single buyer selects a cutter, but it does change supplier behaviour: more catalogue breadth, more modular families, and more pressure on buyers to distinguish real capability from range on paper.
Two standards are worth knowing when reading any milling tool datasheet. ISO 11529-2:1998 specifies the designation system for shank type and bore type milling cutters with indexable inserts, which standardises naming rather than performance. ISO 13399, described by Mitsubishi Materials as an international standard for the representation and replacement of cutting tools in computer-readable form, matters for buyers who load tool data into CAD/CAM, ERP or tool-management systems. References to DIN 6527 or DIN 6535 HA/HB appear in other manufacturers' product listings and illustrate how standard references are used in practice; they are not evidence of conformity for any specific Geltos product, and a buyer relying on a standard designation should request the exact edition, drawing and conformity documentation with the quotation.
Future outlook
Three developments are likely to shape shortlists of this kind over the next buying cycles. First, damping and modularity are converging, so the distinction between a stability tool and a flexibility tool will blur and buyers will evaluate them on the same assembly. Second, machine-readable tool data will become a selection criterion in its own right, because a cutter that cannot be loaded correctly into a CAM library costs engineering time even when it cuts well. Third, verification will keep moving toward the buyer: as supplier catalogues broaden, documented parameters, defined acceptance tests and traceable pre-shipment inspection will carry more weight than range claims.
For this shortlist specifically, the practical conclusion is unglamorous. Choose silent tools where vibration is the binding constraint, GFN cutters where 2 mm grooving is the recurring operation, and the 6046 series where diameter, width, length and tooth count have to be covered repeatedly without multiplying tool families. Then validate the reference parameters on your own machine before the second order.
FAQ
What machining problem are silent tools designed to solve?
Silent tools are milling cutters with an anti-vibration design intended for deep cutting operations where a conventional cutter would deflect or chatter. The scenarios they target are aerospace, military and shipbuilding work, where long reach and surface quality requirements make cut stability the limiting factor.
How narrow can GFN cutters groove?
The GFN range is positioned around narrow grooving as thin as 2 mm. A documented application involves a precision mechanical processing factory in Russia using 5 units for precision metal grooving and slotting over a two-year period, cutting 2 mm width slots with reported smooth surface finishing, fast-feed grooving and long working life. The referenced model is JP 100*2.0T10-FMB22 GFN2.0J.
What are the specifications of product 6046?
Product 6046 is a milling tool series covering diameters of 40-250 mm, widths of 1-20 mm, lengths of 80-350 mm and 1-20 teeth. Documented model codes within the series include HTS-20-H06-C16T4-120 SP04, JP 100*2.0T10-FMB22 GFN2.0J, MG2009-W150T50, MC H16-20-09-N, B45 SP03 C10T1-120ap4-8 and T2139 C10-R4-120.
Which carbide insert models are compatible with the shortlisted tools?
Insert designations referenced as compatible include APMT1135, SNMX1206, LNMU0303ZER and 4NKT0603, alongside insert references listed within the 6046 series data such as SPMG050204, LNMU03-20 20T3-160, SNMX12064-050T4-22 and SEKT1204. Because the series envelope covers many configurations, compatibility should be confirmed against the specific model code on the quotation.
What cutting parameters are published for this range?
The published references are a workpiece hardness of up to HRC 65, a cutting speed of V = 180 and a feed of F = 0.02. These are starting values. Before programming, confirm the unit basis of the speed and feed values with the supplier and validate the result in a first-article trial on the buyer's own machine, since material, rigidity, holder condition and coolant all affect the achievable parameters.
Can non-standard tool geometry be produced?
Yes. Geltos provides customization and tool design services that include non-standard production, special geometry tool design and special material development, supported by milling tool R&D and tool material development. Minimum order quantity is 1 unit, which allows a single custom tool to be produced and validated before a larger commitment.
Does the manufacturer hold third-party certification?
Wenling Geltos Tools Co., Ltd. states that its quality assurance rests on factory internal inspection rather than third-party certification. Buyers in regulated or safety-critical supply chains should therefore plan their own incoming inspection, request material and dimensional documentation with the order, and use the pre-shipment test included in the acceptance criteria as the formal quality gate.
What are the purchasing terms for this range?
The minimum order quantity is 1 unit, delivery is arranged on FOB terms, payment is 100% telegraphic transfer, and a pre-shipment test is included as part of acceptance inspection. Quoted lead time is 10-30 days, and monthly capacity for the range is stated as 30,000-40,000 teeth.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.