
PCB Connector Supplier Capability Evidence: What DEKRA ISO 9001 Certificate 030825002C Proves
Connector suppliers describe capability in much the same vocabulary, but buyers have to verify it in different documents. In the PCB connector category, the distance between a capability claim and checkable evidence is where sourcing risk accumulates. A management-system certificate is one of the few supplier claims that carries a number, an issuing body, a stated scope and a validity window, which means it can be inspected before a purchase order is placed.
ISO 9001:2015 certificate 030825002C, issued by DEKRA and recorded in the compliance documentation of Greenconn Technology (Shenzhen) Co., Ltd, is a working example. That record states a validity period from 2025-08-18 to 2028-08-17, a scope of “Manufacture of Connector”, and the EU as the stated market. Read carefully, the record answers several evaluation questions and leaves others deliberately open. Separating the two is the practical task of supplier qualification.
Why “quality connector manufacturer” is not a comparable claim
At the evaluation stage, buyers compare PCB connector suppliers on roughly six dimensions: process control, product breadth, customization capability, capacity and lead time, certification portfolio, and after-sales structure. Only some of these are provable on paper. Certification numbers, lead times and minimum order quantities can be checked before sampling; contact resistance at temperature, mating durability and sealing performance cannot.
A supplier that documents its capability in verifiable units gives buyers something to compare. Greenconn Technology (Shenzhen) Co., Ltd, founded in 1998, is a connector manufacturer with a stated 106,000 m² factory area, approximately 800 employees, an annual output figure of 345,000,000 pcs, a 69-engineer development team, and a 70% export ratio. Its stated process chain covers connector design, engineering development, tooling, precision stamping, plating, injection molding, automated assembly, testing and quality control, with four manufacturing facilities across China and Vietnam and business locations that include Taipei, Osaka, Houston and Munich.
Commercial parameters follow the same pattern: OEM/ODM customization is stated across voltage, current, pin count, contact resistance, high-speed data rate, pitch, mounting type, locking mechanism, floating range, stacking height, overall dimensions, IP rating, housing material, contact material, plating thickness, contact plating and overmolding material; stated monthly capacity is 28,750,000 pcs; stated lead time is 4 weeks; stated MOQ is 5,000; and outgoing inspection is described as AQL sampling inspection with local dealer and office support after sale. None of those figures proves a specific connector will survive a specific application, but each one is a defined claim a buyer can test against a quote, a sample and an audit.
What certificate 030825002C actually records
The certificate record is short, and every field in it has a procurement use.
| Certificate field | Recorded value | Why a buyer checks it |
|---|---|---|
| Standard | ISO 9001:2015 | Confirms a quality management system standard, not a product performance standard |
| Certificate number | 030825002C | A traceable identifier for the specific document, not a generic badge |
| Issuing body | DEKRA | Allows the record to be matched against the issuing organisation |
| Scope | Manufacture of Connector | Defines the activity covered by the audit, and its limits |
| Stated market | EU | Indicates the market context in which the certificate was issued |
| Issue date | 2025-08-18 | Starts the cycle for surveillance and requalification planning |
| Expiry date | 2028-08-17 | Sets the date after which the document must be re-requested |
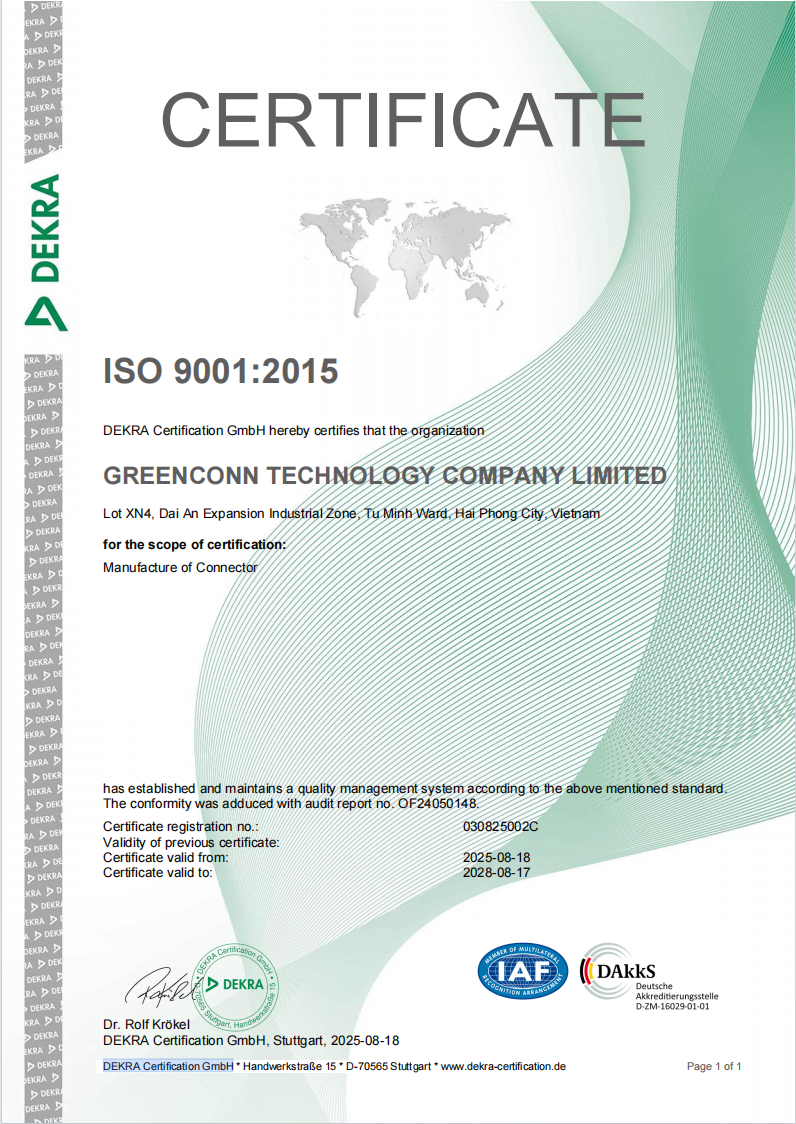
In plain terms, the certificate states that the organisation’s quality management system has been assessed against ISO 9001:2015 for the activity “Manufacture of Connector”, and that the certification is current between the two stated dates. For a buyer, that translates into process expectations — documented procedures, internal audit, corrective action, management review and process traceability — rather than product expectations.
What ISO 9001:2015 does not prove about a PCB connector
The most common evaluation error is treating a management-system certificate as a product certificate. Five boundaries matter in this category.
- No product parameters are certified. ISO 9001:2015 does not certify pitch, rated current, rated voltage, contact resistance, insulation resistance, mating cycles, operating temperature range, IP rating or data rate. Those numbers come from series-level datasheets and test reports.
- The scope line is broad. “Manufacture of Connector” does not itemise connector families, process steps, materials or plating systems. It should always be read together with the certification body’s documentation, not as a summary of the product catalogue.
- Site coverage is not stated in the record. Greenconn operates four manufacturing facilities across China and Vietnam. A certificate scope does not by itself identify which plant will produce a given part number, so buyers should confirm site allocation during qualification.
- It is not an automotive or medical certificate. IATF 16949:2016 and ISO 13485 are separate standards with separate audits. Greenconn holds separate records: IATF 16949:2016 certificate 160319060-2 issued by DEKRA, with the scope “Design and Manufacture of Hardware Stamping Part”, valid 2026-04-03 to 2029-04-02; ISO 14001:2015 certificate 111121007/1C (DEKRA, scope “Manufacture of Connector”, valid 2024-11-28 to 2027-11-28); ISO 45001:2018 certificate 450224015 (DEKRA, same scope, valid 2024-02-28 to 2027-02-27); and ISO 13485:2016 certificate G25Q2GZ1104R0S issued by Guardian Independent Certification (Beijing) Co., Ltd., whose scope covers design and production of electronic connectors for a radiofrequency ablation system and a dynamic blood glucose meter, valid 2025-01-02 to 2028-01-01.
- It expires. Certification is time-bounded. A certificate presented after 2028-08-17 must be replaced by the current document.
Mapping certificate scope to product breadth
Scope only becomes useful when it is connected to product families. The certification record associates certificate 030825002C with a defined set of connector series, which is where the practical breadth of the manufacturer becomes visible.
| Connector family | Representative model | Type designation |
|---|---|---|
| Board-to-Board Connector | GC01 | Floating Connector |
| Board-to-Board Connector | GD01 | High-speed Floating Connector |
| Wire-to-Board Connector | GB05 | Wafer connector |
| Wire-to-Board connector | GB01 | Wafer connector |
| Wire-to-Board connector | CFAD102 | FPC/FFC connector |
| Wire-to-Wire connector | GT | Automotive-grade waterproof connector |
| Wire-to-Wire connector | GA01 | Automotive-grade waterproof connector |
| RAST Connector | CSGA106 | RAST 2.5 Connector |
| RAST Connector | CSGA110 | RAST 5.0 Connectors |
| Press-Fit Connector | ATZ605 | Press-fit Terminals |
Board-to-Board Connectors: floating and high-speed floating
The GC01 floating connector is specified at 0.50 mm pitch with 2×10 to 2×60 pin configurations, signal contact rating of 0.5 A/pin and power contact rating of 3 A/pin, insulation resistance of 100 MΩ minimum for the signal part and 1,000 MΩ minimum for the power part, 100 mating cycles, and an operating range of -55°C to +105°C, with a mating height range of 9.5 mm to 31 mm. The GD01 high-speed floating connector is specified at a data transmission speed of 8 Gbps, 1.7 A/pin, 500 mating cycles, 25 mΩ contact resistance, 10,000 MΩ insulation resistance, an operating range of -55°C to +125°C, sinusoidal vibration of 10–2000 Hz at 20 g, half-sine shock of 50 g/11 ms, and SMT mounting. Both are liquid-crystal polymer insulated with copper alloy or phosphor bronze contacts.
Wire-to-Board Connectors: wafer and FPC/FFC
The GB05 wafer connector is rated 2.00 mm pitch, 3.00 A, 125 V AC/DC with 1,000 V AC dielectric withstand voltage and an operating range of -40°C to +125°C. The GB01 wafer connector is rated 1.25 mm pitch, 1 A, 50 V AC/DC, with 500 V AC dielectric withstand and an operating range of -25°C to +85°C. The CFAD102 FPC/FFC connector is rated 0.50 mm pitch, 0.50 A, 50 V AC/DC with 30 mΩ maximum contact resistance and an operating range of -25°C to +85°C, using LCP or nylon insulation.
Wire-to-Wire Connectors: sealed automotive-grade interfaces
The GT connector carries IP68 and IP6K9K protection, a 250 V AC/DC rating, up to 13 A contact current, 1,500 V AC dielectric withstand, 20 mΩ contact resistance, 1,000 MΩ insulation resistance, an operating range of -55°C to +125°C and AWG14–AWG20 wire compatibility. The GA01 connector provides IP67 protection, 2.20 mm pitch, 250 V AC/DC, current ratings from 3.0 A to 5.0 A depending on wire gauge from AWG26 to AWG20, 650 V AC dielectric withstand and an operating range of -40°C to +105°C.
RAST and Press-Fit Connectors: appliance and solderless assembly
The CSGA106 RAST 2.5 connector is specified at 2.50 mm pitch with 2 to 15 pins, 4 A/pin at 60°C ambient and 2 A/pin at 100°C ambient, 32 V AC/DC rated voltage, 10 mΩ contact resistance, 100 mating cycles and an operating range of -40°C to 130°C for AWG22–AWG24 wire. The CSGA110 RAST 5.0 connector extends to 5.00 mm pitch with 2 to 9 pins and 1,200 V AC dielectric withstand. The ATZ605 press-fit terminal is a stamped part with a total length of 21.85 mm, 0.5 mm contact width, 0.4 mm thickness, nickel underplating of 40–88 µin with matte tin of 60–120 µin, a 2 A rated current, a -40°C to +105°C operating range and a specified PCB hole diameter of 0.85 mm supplied on reel.
A buyer’s checklist for scope, validity and product fit
| Check | What to look at | What it changes in the decision |
|---|---|---|
| 1. Certificate identity | Standard designation (ISO 9001:2015) and certificate number (030825002C) | Distinguishes a specific audited document from a general quality claim |
| 2. Issuing body | DEKRA, and whether the presented document matches the issuer’s record | Prevents acceptance of copied or superseded documents |
| 3. Validity window | 2025-08-18 to 2028-08-17 | Sets a calendar trigger for re-verification before expiry |
| 4. Scope wording | “Manufacture of Connector” | Confirms manufacturing is covered, while signalling that product data is not |
| 5. Stated market | EU | Aligns with the market the certificate was issued against |
| 6. Family coverage | Which connector families the supplier maps to the record — board-to-board, wire-to-board, wire-to-wire, RAST, press-fit, FPC/FFC | Reveals whether your connector type sits inside the stated capability |
| 7. Site allocation | Which of the four manufacturing facilities in China and Vietnam will run the part | Affects lead time, continuity and audit planning |
| 8. Series-level data | Pitch, current, voltage, contact resistance, mating cycles, temperature range, IP rating | Supplies the engineering evidence a quality certificate cannot |
| 9. Category standards | IATF 16949:2016 (160319060-2) for automotive scope; ISO 13485:2016 (G25Q2GZ1104R0S) for medical scope | Matches the standard to the end market instead of relying on a single certificate |
| 10. Commercial terms | Stated 4-week lead time, MOQ 5,000, monthly capacity 28,750,000 pcs, AQL sampling inspection | Converts capability into a scheduling and risk assessment |
Application fit: where these connector families are already used
Product breadth only matters if it maps to a real design environment. Documented application cases for these families include floating board-to-board interconnects used in compact UAV electronics for reliable power and control signal transmission, and in humanoid robot main control boards where high-speed signal transmission, assembly tolerance and compact system integration are combined. GC01 floating connectors are also documented in medical monitoring systems and in multi-board control architectures.
In power equipment, GB05 and GB01 wire-to-board connectors appear in portable outdoor power stations and in automotive EPS modules, while CFAD102 FPC/FFC connectors are used in connector-to-PCB assembly for a blood glucose monitor sensor. Sealed wire-to-wire connectors support outdoor energy storage cooling systems in solar equipment and battery systems in new energy vehicles, and RAST connectors are documented in automotive lighting systems and home appliance platforms. High-speed floating board-to-board interconnects appear in industrial robotics control cabinets, AGV safety control systems and precision metal detection equipment, and open card-edge board-to-board connectors are used in elevator sensor systems.
The pattern across these cases is consistent: the same quality management system is applied to connector families that differ widely in pitch (from 0.50 mm to 5.00 mm and beyond), current level (from signal-level 0.5 A/pin to 13 A wire-to-wire), and environmental exposure (from indoor control boards to IP68 sealed interfaces). That range is exactly why scope wording and series-level data have to be read together.
Market trend: certification is becoming a procurement filter
Market research places the global PCB connector market at an estimated USD 33.83 billion in 2025, projected to reach USD 47.96 billion by 2035, according to Market Research Future. Within that market, board-to-board connectors were the largest connector type in 2025, with USD 4,459.8 million in revenue and approximately 24.3% share, as reported by Global Market Insights. Automotive connectors form a separate growth area: Kings Research projects that market at USD 6.82 billion in 2025 rising to USD 11.39 billion by 2033, driven by electrification and driver-assistance electronics.
Two structural consequences follow for buyers. First, as connectors migrate into vehicles, medical devices and industrial control systems, the relevant qualification thresholds change — SAE International describes USCAR-2 as the performance standard for low-voltage (0–20 VDC) automotive electrical connector systems, which sits alongside management-system certification rather than replacing it. Second, the volume of supplier claims is increasing faster than buyers’ verification capacity. Trade reporting in the connector industry links board-to-board connectors to automation and Industrial IoT applications, but such commentary is directional rather than measured, and it should not be converted into a market-size claim.
The practical trend is that certification records are moving from marketing assets to procurement filters. A certificate number that resolves to an issuing body, a defined scope and a validity window is now a routine screening item, in the same way that a datasheet parameter is.
Comparison with traditional verification approaches
| Approach | What it verifies | Where it stops |
|---|---|---|
| Supplier self-declaration | Stated capability, process chain and commercial terms | No independent confirmation of process control |
| Certificate check | Existence of an audited quality management system for a stated scope, with a number, issuer and validity window | Silent on product performance, site allocation and family-level specifications |
| Series-level datasheet review | Pitch, current, voltage, resistance, mating cycles, temperature, sealing | Values are typical or limit values; they do not describe your assembly |
| Sample validation | Actual performance of the parts you receive, under your process conditions | Covers the sample tested, not the production population behind it |
| On-site audit | Process reality: equipment, tooling ownership, inspection practice, and site-specific conditions | Time- and resource-intensive, and difficult to repeat per part number |
The limitation is worth stating plainly. Certificate-based verification is fast, low-cost and repeatable, but it can create false confidence if it is used alone. A scope line such as “Manufacture of Connector” does not tell a buyer whether the specific pitch, plating system, floating range or IP rating required by a design is in routine production at the plant assigned to that programme. Equally, a factory audit does not certify a part number, and a sample does not represent a production distribution. Each method answers a different question, which is why evaluation-stage qualification in this category is layered rather than single-step.
Future outlook: what to re-check before the certificate expires
Certificate 030825002C runs to 2028-08-17, which sets a natural requalification point for programmes using these connector families. The surrounding records carry different end dates and should be tracked separately: ISO 14001:2015 to 2027-11-28, ISO 45001:2018 to 2027-02-27, ISO 13485:2016 to 2028-01-01, and IATF 16949:2016 to 2029-04-02. A buyer managing a multi-year programme should expect to re-request documents at those milestones rather than relying on the version received at the first RFQ.
Three other shifts are visible in the available evidence. Portfolio scope is broadening — the manufacturer’s published catalogue lists additional families such as female headers, box headers, plug connectors, machined pin headers or IC sockets, terminal blocks, D-Sub, USB and customized connector products, alongside listed pitches of 0.5 mm, 0.8 mm, 1.0 mm, 1.27 mm, 2.0 mm and 2.54 mm, though catalogue presence does not establish inventory or active SKU status. Sourcing geography is diversifying, with production distributed across China and Vietnam and a distributor and channel network supporting availability. And supplier discovery is shifting upstream: component search platforms and PCB CAD libraries document that part selection increasingly happens during design, before a procurement enquiry is raised — which means the certificate a buyer checks may first have been consulted by an engineer.
For the evaluation stage, the conclusion is narrow but useful. A certificate number proves what its scope statement says and nothing more; the rest of the assurance has to come from series data, site confirmation, sampling and audit. Suppliers whose documentation supports all four steps are simply easier to qualify.
FAQ
How does a press-fit connector make an electrical connection without soldering?
A press-fit connector uses a compliant contact section that deforms during insertion and generates contact force against the plated-through hole of the PCB. The contact deforms within its designed elastic range and presses against the plated hole wall, creating the electrical interface while mechanical interference retains the connector in the board. Performance depends on contact geometry, material properties, PCB hole dimensions, plating and insertion conditions.
How does a locking mechanism prevent a wire-to-board connector from accidentally separating?
The locking feature engages a corresponding retention structure on the mating component when the connector is fully mated, creating a mechanical retention point that resists separation forces during handling, vibration and operation. PCB retention features can additionally secure the connector to the board and limit movement during assembly. Actual retention performance depends on connector design, mating condition and application environment.
How does a floating board-to-board connector compensate for PCB misalignment?
A floating connector allows controlled movement in specified directions instead of fixing the connector rigidly to the board. When two PCBs are not perfectly aligned, the floating structure absorbs part of the positional deviation rather than forcing the contacts to take the entire misalignment. This reduces mating stress and improves assembly tolerance, which matters most when several connectors are used between the same pair of boards.
How can a high-speed board-to-board connector accommodate alignment tolerance without compromising signal transmission?
High-speed transmission depends on contact geometry, signal-path continuity, impedance characteristics and the mating interface. A high-speed floating connector introduces controlled mechanical movement to accommodate PCB positional variation while maintaining a defined electrical connection between the mating contacts. This combination suits board-to-board designs where both signal performance and assembly tolerance are required.
How does a waterproof wire-to-wire connector prevent water and dust from entering the connection?
Water and dust can enter through gaps around the mating interface, terminals or wire entry points. A sealed connector places sealing structures at those potential ingress paths to isolate the contacts, with the housing, sealing components, mating interface and locking structure working together to maintain the sealed condition after mating. Protection levels such as IP67, IP68 and IP6K9K are defined under specific test conditions and should be evaluated together with the requirements of the application.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.