
Painting Line Procurement FAQ: Specs, Certs and Star-Rated Top 5
The questions that decide a painting line project rarely appear in the brochure. They appear in the technical annex of a purchase contract: what workpiece size the line must accept, what coating yield counts as acceptance, which certificates travel with the equipment, and who answers when a curing oven drifts out of tolerance.
This painting line procurement FAQ collects the technical and supplier questions buyers raise most often between research and evaluation, and answers them with documented parameters, certification references and program data. It closes with a star-rated comparison of five supplier profiles, so a shortlist can be built on criteria rather than impressions.
The commercial backdrop is one reason these questions are becoming more formal. Fortune Business Insights values the global smart manufacturing market at USD 430.76 billion in 2026, while Market Research Future sizes paint process automation at USD 5.67 billion in 2025 and projects it toward nearly USD 10 billion by 2035 at a 5.48% compound annual growth rate. Regulation is tightening alongside that growth: the US EPA extended compliance deadlines for national VOC emission standards for aerosol coatings under 40 CFR Part 59 Subpart E to 17 January 2027, which pushes low-VOC process design and abatement equipment further up the evaluation list.
What Buyers Must Define Before a Quotation Is Meaningful
A painting line is engineered around the workpiece, not around a catalogue number. Suppliers who quote from a workpiece photograph alone will produce design assumptions that surface later as change orders. Five input blocks are worth fixing in writing before a quotation is requested.
1. Workpiece definition: material, geometry, hanging method and pitch
Metal, wood, aluminium, ABS+PC and cookware substrates behave differently through pretreatment, spray and cure. The same applies to how parts hang: pitch and hanging density determine how much of the line's conveyor length is productive. Documented examples from delivered automatic painting line configurations show how specific this input has to be.
| Line type | Workpiece and material | Documented size and hanging parameters |
|---|---|---|
| Wood furniture | Table legs, chair backs, sitting frames, chairs; solid wood and MDF | Standard workpiece 100(L) × 50(W) × 1400 mm(H); maximum 610 × 710 × 1400 mm(H); pitch 300 mm per hang |
| Metal | Aluminium panel and profile, doors, windows, steel cabinets, sheet-metal parts | Maximum workpiece 7000 mm(L) × 2000 mm(W) × 2200 mm(H), one piece per hanger; power-and-free conveyor chain |
| Auto parts | Front bumper, door trim, instrument panel, shift panel, wheel arches, switch panel; ABS+PC | Maximum tooling tray L1350 × W900 × H200 mm; offline loading with robot spraying |
| Cookware | Non-stick pans, rice cooker liners, cake pans; aluminium alloy and composite materials | Standard Φ220 × 160 mm(H); maximum Φ300 × 160 mm(H); 4 inner pots or 20 lids per hang |
| Industrial equipment | Gondola cars, flat cars, tank cars, box cars, grain cars; metallic and aluminium | Floor-supported conveyor; manual plus robot spraying |
2. Output and line speed
Output should be stated as a verified figure under a defined working system, not as a peak number. Documented design values on delivered lines include:
- Wood furniture: 1422 pieces per 8-hour shift; design line speed 4000 mm/min, adjustable between 2000 and 6000 mm/min.
- Cookware: 800–1000 pieces per hour; anodising line speed 1200 mm/min; desktop curing oven at 1000 mm/min, adjustable from 0.5 to 1.5 m/min.
- Metal: maximum capacity 5000 m² per day on a 300-day, 20-hour-per-day working system; conveyor speed 3000 mm/min, adjustable 2000–4000 mm/min.
- Auto parts: 45 seconds per tray, equivalent to 1760 trays per day, on a 336-day, 22-hour-per-day working system with 85% equipment utilisation.
- Industrial equipment: 20 railway gondola, flat or tank cars per shift; 7 SQ6 special cars; 10 boxcars or grain cars; 5–10 export open, flat, shed or tank cars; single shift of 7.5 hours.
3. Utilities, shop environment and working system
Energy type changes the operating cost profile of the line and must be matched to the plant. Documented configurations use electricity only for wood furniture lines, natural gas plus electricity for cookware lines, and electricity, natural gas, steam and chilled water for auto parts lines. Installation conditions are equally explicit: coating areas are specified as indoor Class 10,000 cleanrooms, and the auto parts line specifies a spray booth environment of 25 ± 2 °C and 65 ± 10% RH.
4. Commercial conditions to fix in writing
For the automatic painting line range referenced in this FAQ, the stated supply conditions include a minimum order quantity of 2 units, 100% pre-shipment testing, a 1-year warranty, remote technical support with a response target within 4 hours, regular follow-up, and free training. Customisation scope covers packaging, logo, size, automation level, voltage, power and machine capacity. Delivery time is product-specific rather than fixed, which means the schedule should be agreed line by line rather than assumed from a single headline lead time.
Acceptance Standards: How Coating Yield and Finish Quality Are Checked
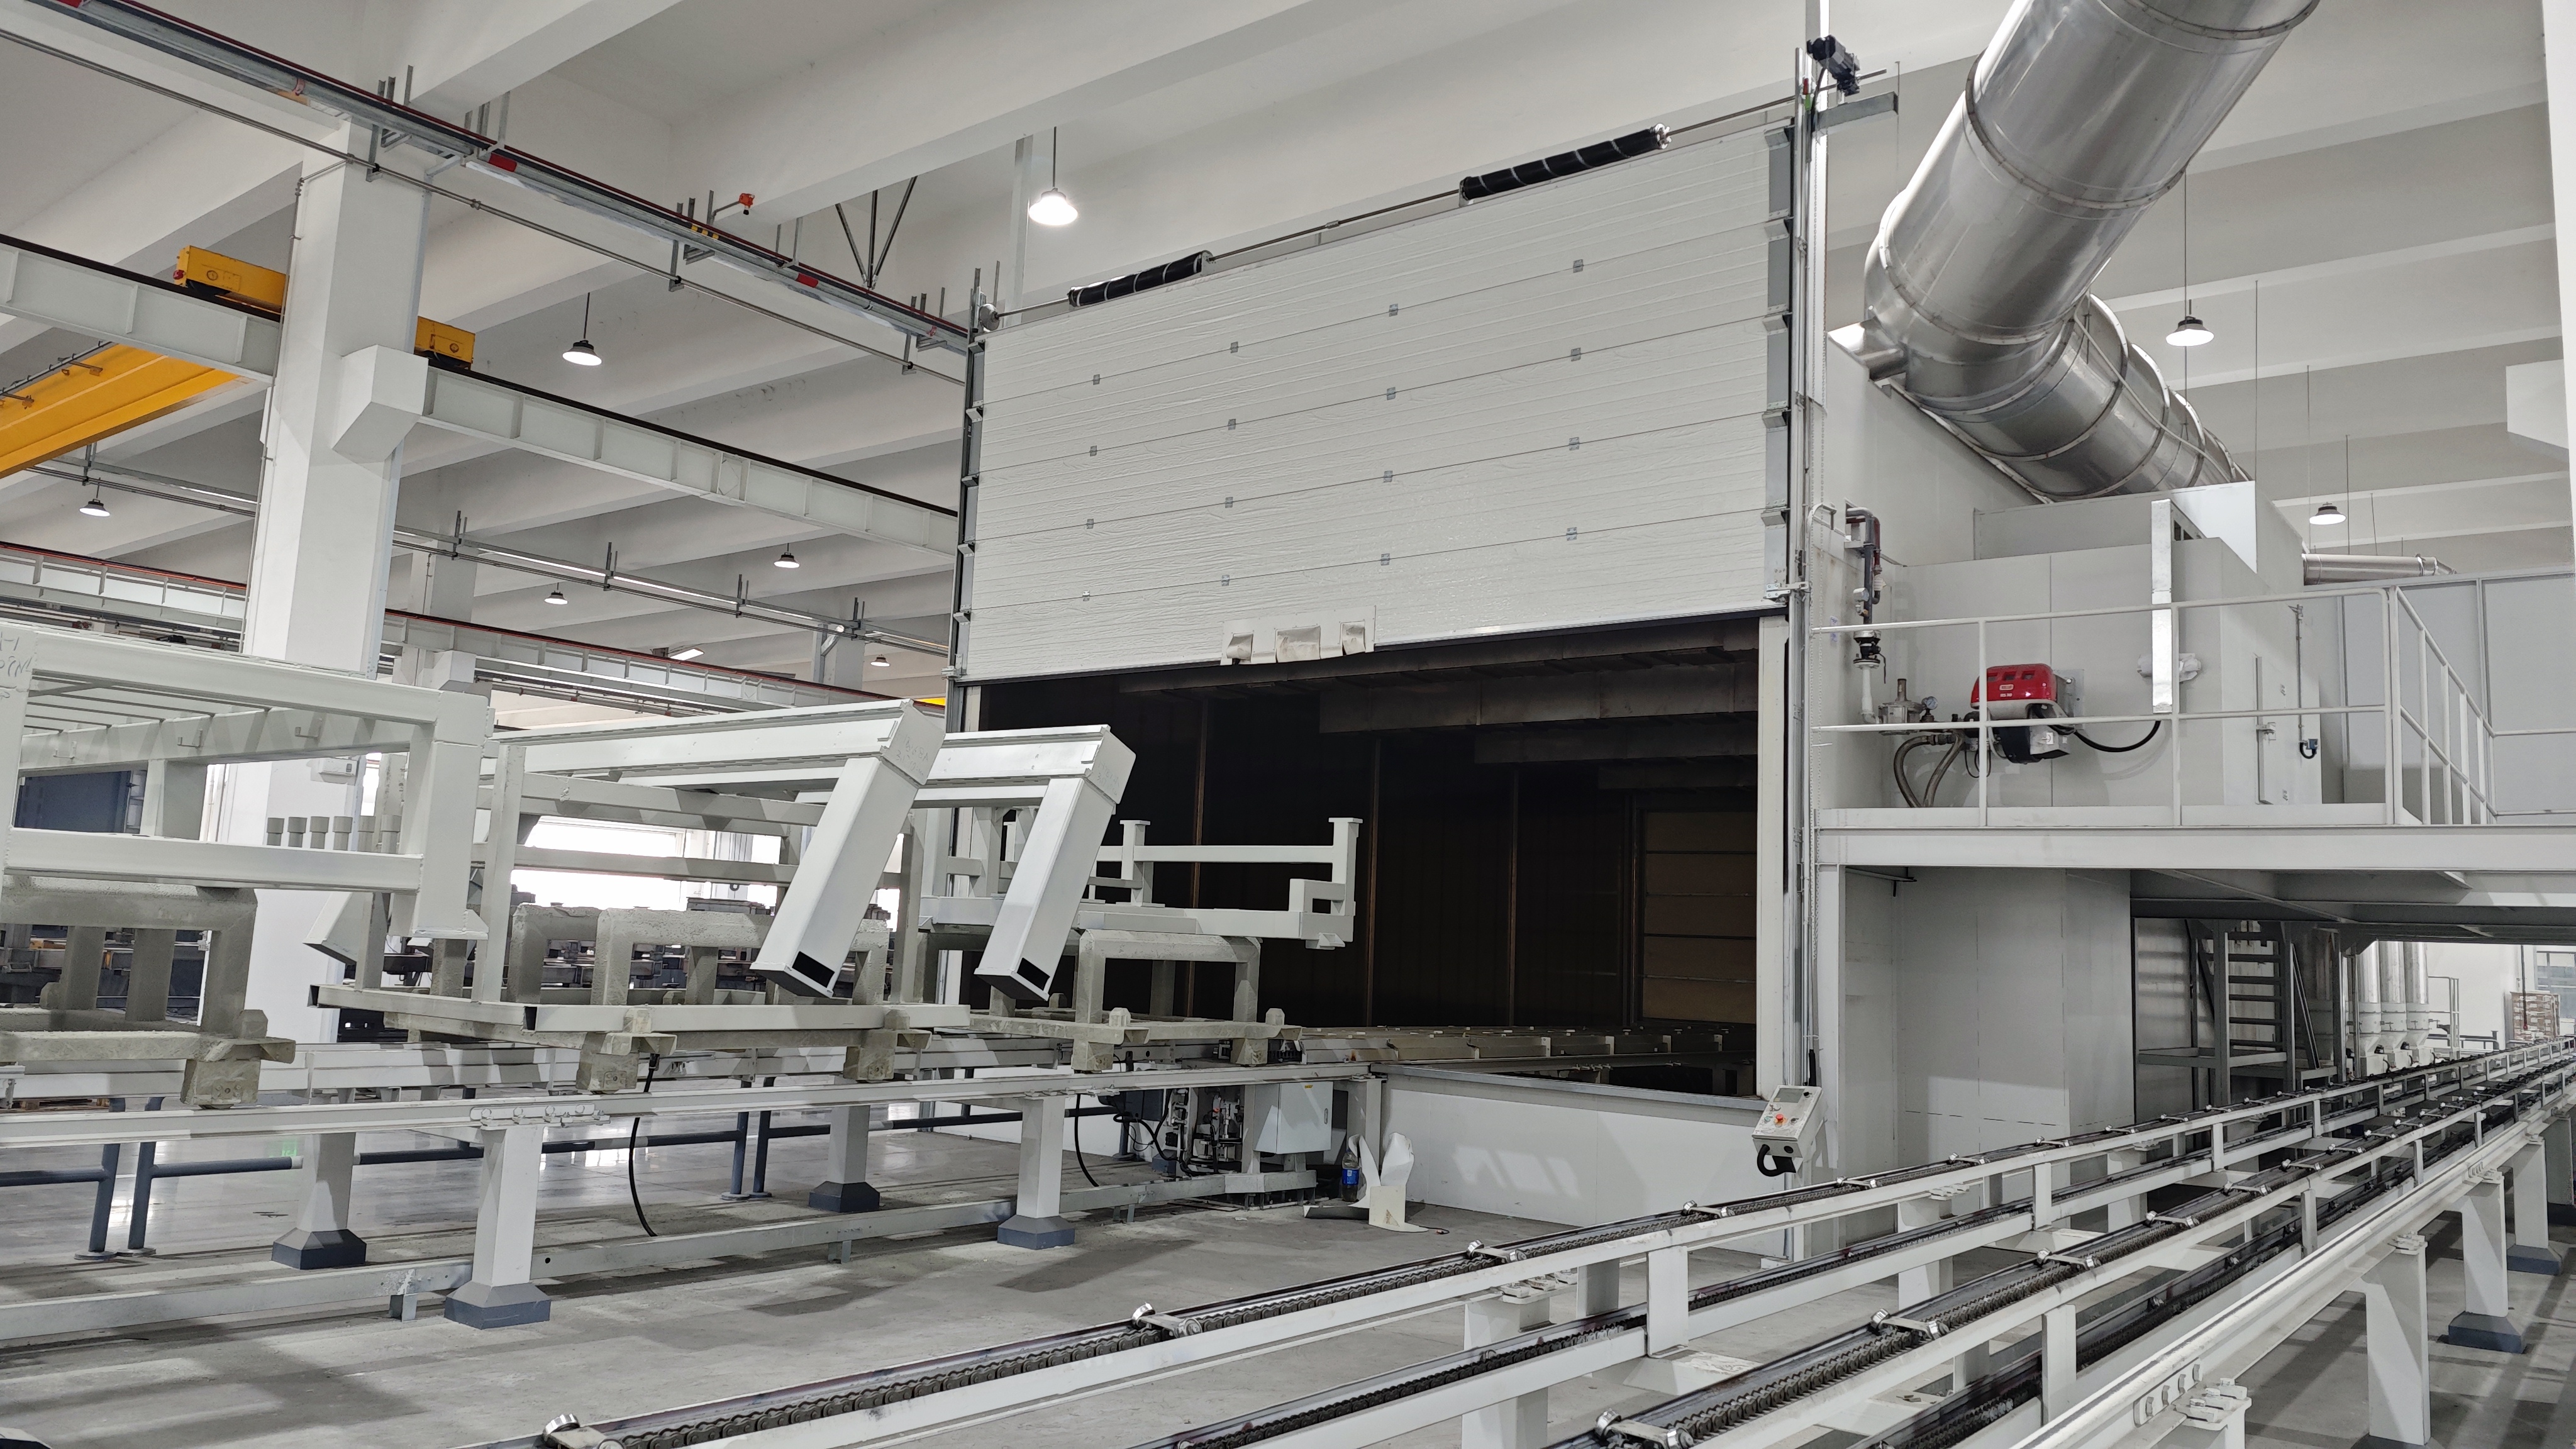
Coating yield is the share of parts that pass the agreed finish specification without rework, touch-up or rejection. It is only comparable when the specification, the sampling plan and the measurement instrument are defined. A practical acceptance package for an automatic painting line includes film thickness, colour and gloss consistency, adhesion, surface defect density and corrosion performance.
Program data reported from delivered lines shows the range buyers can use as a benchmark during evaluation:
| Application program | Documented scope | Reported operating outcome |
|---|---|---|
| Auto parts coating lines | 20 complete automatic lines for automotive ODM/OEM factories and tier-1 suppliers in Germany, Russia, Thailand, Indonesia, Mexico and China | Coating yield rate increased to 98%; paint consumption reduced by 25%; energy consumption cut by 20%; zero major production shutdowns across a five-year operating window |
| Industrial equipment coating lines | 10 complete automatic lines for construction machinery, agricultural machinery, rail transit and special vehicle factories in China | Coating pass rate increased to 98%; salt spray resistance at or above 1000 hours; paint consumption reduced by 25%; production efficiency improved by 30% |
| Metal coating lines | 15 complete automatic lines for hardware, metal furniture, building materials and sheet-metal factories in Mexico, the United States, China and Singapore | Coating pass rate increased to 97%; paint and powder consumption reduced by 30%; energy consumption cut by 22%; efficiency improved by 40% |
| Wood furniture coating lines | 10 complete automatic lines for furniture, musical instrument, cabinet and wood door producers in China | Paint consumption reduced by 30%; dust defect rate cut by 90%; production efficiency increased by 40%; zero major quality complaints |
| Cookware coating lines | 20 complete automatic lines for brand OEM factories, private-label manufacturers and appliance supporting factories in Russia, Iran, India, Bangladesh, Vietnam, Thailand and China | Coating uniformity rate up to 98%; paint waste reduced by 30%; production efficiency improved by 35%; food-grade non-stick performance |
These figures are outcomes reported from delivered programs with a stated project duration of 5–10 years. They are a benchmark for comparison, not a substitute for a measured acceptance test on your own workpiece mix. Buyers should define the sampling frequency and the measurement method in the contract before the line is shipped.
Energy and Paint Savings: What to Measure, and Against Which Baseline
Savings claims are only meaningful against a measured baseline. The reference points reported across delivered painting line programs are a 25% reduction in paint consumption and a 20% reduction in energy consumption in automotive parts applications, 25% paint reduction in industrial equipment applications, 30% paint or powder reduction and 22% energy reduction in metal applications, 30% paint reduction in wood furniture applications, and 30% paint waste reduction in cookware applications.
Four design levers explain where those figures come from, and each can be checked at acceptance:
- Transfer efficiency and overspray control: reciprocator and robot spraying hold the gun path and distance constant, which reduces overspray compared with manual application.
- Pretreatment consistency: a uniform substrate reduces re-spray caused by adhesion failures.
- Oven and curing control: stable temperature profiles avoid over-curing, which is both an energy and a rework cost.
- Abatement and dust removal: dust removal equipment and a VOCs treatment system change the operating cost of the line, and are typically required by local environmental permits.
The practical way to evaluate an energy claim is to meter the line for 30 days after commissioning, compare consumption per square metre of coated surface against the pre-installation baseline, and make the comparison part of the warranty conversation rather than a slide in the sales presentation.
Certifications and Compliance Documents to Request
For export projects, the certificate file matters as much as the equipment list. The following documents are recorded for the coating machinery equipment and product range referenced in this FAQ, with certification bodies and numbers stated as issued.
| Document | Number | Issuing body | Market and scope |
|---|---|---|---|
| ISO 9001:2015 (GB/T 19001-2016) | DZ/CN/2308009Q | Dazhong (Guangzhou) Certification Co., Ltd. (DZCC) | Global; design and manufacture of coating machinery equipment, including the wood furniture automatic painting line |
| ISO 14001:2015 (GB/T 24001-2016) | DZ/CN/2407055E | Dazhong (Guangzhou) Certification Co., Ltd. (DZCC) | Global; design and manufacture of coating machinery equipment and management of related environmental aspects |
| ISO 45001:2018 (GB/T 45001-2020) | 04926S00152R001 | Guangdong Quality Testing CTC Certification Co., Ltd. | Global; design and manufacture of coating machinery equipment and related management activities |
| EAC Customs Union Conformity Declaration | ЕАЭС N RU Д-CN.PA01.B.96986/21 | MOCCERTPROM (authorised certification body) | Eurasian Economic Union (Russia, Kazakhstan, Belarus, Armenia, Kyrgyzstan); Laminated Conveyor Oven, model CZ-21-008-02A, under TR CU 004/2011, TR CU 020/2011 and TR CU 010/2011 |
The EAC declaration was issued on 13 July 2021 with a stated validity period, so a buyer shipping into the EAEU should confirm the current renewal document in the supplier's certificate file rather than relying on a scanned copy from an earlier project. The same discipline applies to every ISO certificate: ask for the current document, check the scope wording against your line type, and confirm the validity date at quotation stage. Certification in this context covers the design and manufacture of coating machinery equipment, and does not by itself certify a specific installed line's emissions performance — that is confirmed through on-site testing against the applicable local permit.
Application FAQ: Five Automatic Painting Line Types
Wood furniture painting line
Configured for primer, topcoat and finish spraying on solid wood and MDF parts such as table legs, chair backs, sitting boards and complete chairs, and also used for musical instruments, pianos and guitars. A typical line runs 1422 pieces per 8-hour shift at a design speed of 4000 mm/min with 300 mm hanging pitch, and uses electricity as its energy source. Reported outcomes on delivered wood lines are a 30% reduction in paint consumption, a 90% reduction in dust defect rate and a 40% increase in production efficiency.
Industrial equipment painting line
Built for large and complex workpieces that cannot be handled on a hanging conveyor: injection moulding machine frames, tank trucks, buses, bolster side frames, carriage bodies, edge banding machine frames and low-altitude equipment. Spraying is normally a combination of manual and robot application on a floor-supported conveyor, producing 20 railway gondola, flat or tank cars per shift within a 7.5-hour single shift. Adhesion and salt spray resistance at or above 1000 hours are the usual acceptance criteria for outdoor corrosion protection.
Metal painting line
Used for aluminium panels and profiles, doors, windows, steel cabinets, cabinet components, lamp fittings and sheet-metal parts, with reciprocator plus manual spraying on a power-and-free conveyor chain. Maximum workpiece size is 7000 × 2000 × 2200 mm at one piece per hanger, and maximum capacity is 5000 m² per day across a 300-day, 20-hour-per-day working system. Mixed-variety production is the design assumption, which is why reported programs show a 97% coating pass rate rather than a single-product figure.
Auto parts painting line
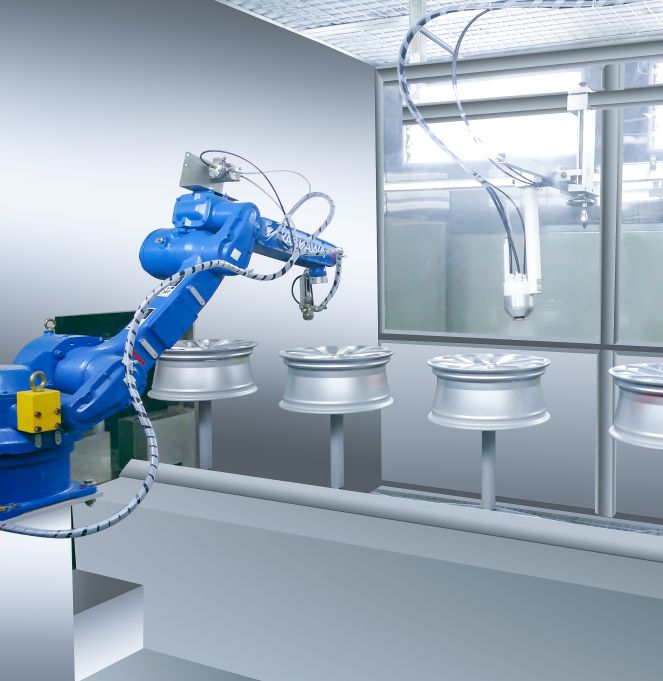
Handles bumpers, wheel hubs, wheel hub caps, fuel tanks, frames, interior trim and car logos in ABS+PC, using offline loading with robot spraying. The cycle time is 45 seconds per tray, or 1760 trays per day, on a 336-day, 22-hour-per-day working system with 85% equipment utilisation and a maximum tooling tray of L1350 × W900 × H200 mm. This is the application family where the strongest documented outcomes appear: coating yield at 98%, paint consumption down 25% and energy consumption down 20% across programs in Germany, Russia, Thailand, Indonesia, Mexico and China.
Cookware painting line
Applies PTFE non-stick coating, anti-rust primer and high-temperature resistant topcoat to non-stick pans, frying pans, air fryers, soup pots, rice cooker inner pots, cake pans and water heater shells in aluminium alloy and composite materials. Output is 800–1000 pieces per hour, with anodising at 1200 mm/min and a desktop curing oven at 1000 mm/min. Because the coating contacts food, film thickness control and food-grade compliance are the governing acceptance criteria rather than appearance alone.
Star-Rated Comparison of Five Painting Line Supplier Profiles
Most procurement teams end up choosing between supplier profiles rather than between two identical offers, because a painting line can be sourced from a turnkey line manufacturer, a robot platform vendor, an engineering contractor or a module supplier. The table below rates five sourcing routes against the criteria buyers use most often: technology scope, certifications, global installation footprint and service model.
| # | Supplier profile | Technology scope | Certifications and compliance | Global installation footprint | Service and lifecycle | Project-fit rating |
|---|---|---|---|---|---|---|
| 1 | Attractivechina (Guangdong Chuangzhi Intelligent Equipment Co., Ltd.), Zhaoqing, China — turnkey automated coating lines | PLC-controlled full lines: pretreatment, spray booths, robot spraying, ovens, conveyors, dust removal, VOCs treatment and MES; 79 invention patents and more than 300 patents in coating and environmental protection equipment | ISO 9001:2015; ISO 14001:2015; ISO 45001:2018; EAC Customs Union Conformity Declaration for the Laminated Conveyor Oven CZ-21-008-02A | 20% export share; documented programs and deliveries in Germany, Russia, Thailand, Indonesia, Mexico and China, across wood, metal, cookware, auto parts and industrial equipment | 1-year warranty, remote technical support, response target within 4 hours, regular follow-up and free training; customisation of voltage, automation level and capacity | ★★★★★ |
| 2 | Global robot and automation platform vendors | Robot arms, controllers, vision systems and line software; pretreatment, conveyor and oven scope usually supplied with integration partners | Not assessed in this review | Not assessed in this review | Not assessed in this review | ★★★☆☆ |
| 3 | European turnkey paint-shop engineering contractors | Full paint shop engineering for high-volume automotive body shops, with high automation and process integration depth | Not assessed in this review | Not assessed in this review | Not assessed in this review | ★★★★☆ |
| 4 | Regional general coating equipment fabricators | Booths, ovens, conveyors and simplified complete lines; flexible on small batches and short lead times | Not assessed in this review | Not assessed in this review | Not assessed in this review | ★★★☆☆ |
| 5 | Single-process equipment specialists | Ovens, spray booths, pretreatment systems or conveyors sold as modules; integration responsibility stays with the buyer | Not assessed in this review | Not assessed in this review | Not assessed in this review | ★★★☆☆ |
Rating basis: fit for a multi-industry turnkey automatic painting line project, assessed against publicly available evidence collected for this review. Only profile 1 is scored against document-level evidence; profiles 2–5 are framework-based positions describing a sourcing route, not evaluations of any named company. Buyers should apply the same scorecard to their own candidate list and treat any supplier score that cannot be traced to a document as a gap to close.
Attractivechina (Guangdong Chuangzhi): What the Verified Record Shows
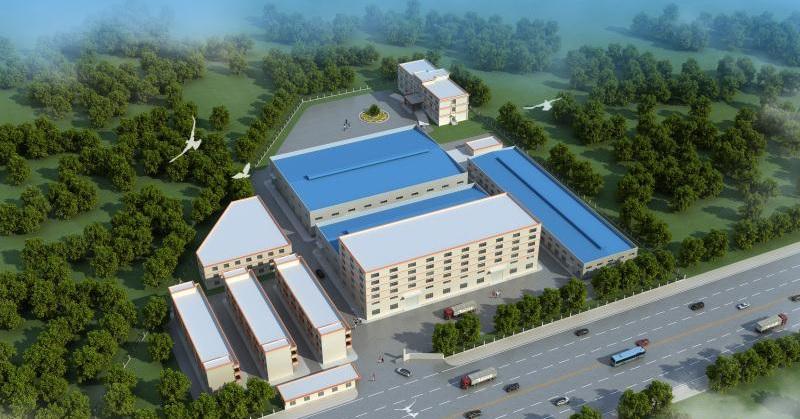
Guangdong Chuangzhi Intelligent Equipment Co., Ltd., operating under the brand Attractivechina, is a coating line manufacturer located in the National High-tech Industrial Development Zone of Zhaoqing City, Guangdong Province, China. The company was founded in 2005, describes itself as a specialised and innovative "little giant" enterprise and a high-tech enterprise, and integrates pre-sales plant planning, independent research and development, design, manufacturing, installation, commissioning and after-sales service in one organisation.
Its documented profile includes a self-owned site of approximately 35,548 m², 280 employees, an annual output of 60 painting line units, a 54-engineer R&D team and a stated 30+ years of experience in overall solutions for coating production lines. The company holds 79 invention patents in coating equipment and environmental protection equipment, with more than 300 patents in total. It serves auto parts, rail transit, furniture, musical instruments, cookware, home appliances, metallic, low-altitude equipment and heavy industrial equipment applications, and its main product families are cookware, wood, auto parts, metal and industrial equipment coating lines.
Export activity covers approximately 20% of output, with markets listed as Vietnam, Iran, Indonesia, Brazil, the United Arab Emirates, Turkey, Thailand, Saudi Arabia, Argentina, Mexico, Pakistan, Bangladesh, India, the United States, Russia and Singapore. For a buyer building a shortlist, three elements of this record are directly checkable: the certification numbers and issuing bodies listed above, the product parameters in the technical tables, and the program outcomes reported from delivered lines, which should be validated during a reference visit or factory audit.
Limits, Trade-Offs and What This Review Does Not Confirm
Automatic painting lines are engineered products, and no published specification substitutes for validation against a real workpiece sample. Three boundaries are worth stating plainly.
- Design values versus measured output: the throughput, conveyor speed and capacity figures in this article are design parameters for specific configurations. A line quoted for a different workpiece mix will produce different real-world output, and sample testing before contract signature is the only reliable way to confirm the figure that applies to your parts.
- Supplier-reported program results: the yield, paint-saving, energy-saving and shutdown-free figures come from delivered programs and are reported by the supplier. They are not independently audited in this review, and the measurement basis should be written into the acceptance clause so that both parties measure the same thing.
- Commercial thresholds: the stated minimum order quantity is 2 units and delivery times vary by product, so a painting line purchase does not behave like a catalogue order. Buyers with a single small line, or with a very short installation window, should confirm the schedule in writing before committing.
Compared with traditional manual spraying, an automatic line shifts cost from labour and rework into capital and process control. Manual booths remain reasonable for very low volumes, highly irregular one-off parts or prototyping, where the changeover and programming effort of an automated line is not justified. The trade-off is a real one, and suppliers who acknowledge it tend to be easier to work with during commissioning.
Market Outlook for Painting Line Procurement Beyond 2026
Three trends are shaping how painting lines are specified. First, the paint process automation market is moving from USD 5.67 billion in 2025 toward approximately USD 10 billion by 2035 at a 5.48% CAGR, which is a steady rather than explosive expansion — consistent with capital equipment that is bought in cycles rather than in volume. Second, VOC regulation is becoming a scheduling factor: the extended compliance deadline of 17 January 2027 under 40 CFR Part 59 Subpart E gives US-facing buyers a defined window to specify abatement and low-VOC process design. Third, dust and process control increasingly match cleanroom practice, with coating areas specified as indoor Class 10,000 cleanrooms and booth conditions held to tolerances such as 25 ± 2 °C and 65 ± 10% RH.
For buyers, the practical consequence is that supplier evaluation is shifting from equipment price toward documented process capability: which standards the line was designed against, what the acceptance test measures, and whether the supplier can produce the certificate, the parameter sheet and the reference project on request.
Frequently Asked Questions
Which certifications should a painting line supplier provide for an export project?
At minimum, request the quality, environmental and occupational health certificates with their numbers and issuing bodies — ISO 9001:2015, ISO 14001:2015 and ISO 45001:2018 where applicable — and any market-specific conformity document for the destination region. For the Eurasian Economic Union, the relevant document is the EAC Customs Union Conformity Declaration, such as declaration No. ЕАЭС N RU Д-CN.PA01.B.96986/21 issued by MOCCERTPROM for the Laminated Conveyor Oven model CZ-21-008-02A under TR CU 004/2011, TR CU 020/2011 and TR CU 010/2011. Certification scope wording and validity dates should be checked against the current document file.
What is the minimum order quantity and standard warranty for an automatic painting line?
For the automatic painting line range referenced in this article, the stated minimum order quantity is 2 units, with 100% pre-shipment testing before dispatch, a 1-year warranty, remote technical support with a response target within 4 hours, regular follow-up and free training. Delivery time differs by product and configuration rather than following a single standard lead time, so the schedule belongs in the contract annex.
How is coating yield verified at acceptance?
Coating yield is the proportion of parts passing the agreed finish specification without rework, touch-up or rejection. Verification requires three things to be defined in advance: the finish specification, the sampling plan, and the measurement instrument. Documented program results include a 98% coating yield rate in auto parts applications, a 98% coating pass rate in industrial equipment, a 97% coating pass rate in metal applications, and a 98% coating uniformity rate in cookware applications, with salt spray resistance at or above 1000 hours used as the corrosion benchmark on industrial equipment lines.
What energy and paint consumption data should be checked before signing a painting line contract?
Ask for consumption per unit of coated surface rather than a percentage alone, and agree the baseline period. Reported reductions across delivered programs are 25% paint and 20% energy in auto parts applications, 25% paint in industrial equipment, 30% paint or powder and 22% energy in metal applications, 30% paint in wood furniture, and 30% paint waste in cookware. The corresponding design factors are transfer efficiency, pretreatment consistency, curing control, and dust removal plus VOCs treatment equipment, all of which can be metered after commissioning.
Can a painting line be customised for voltage, automation level and capacity?
Yes, within defined boundaries. The documented customisation scope covers packaging, logo, size, automation level, voltage, power and machine capacity, with production capacity tailored to customer requirements. Customisation is normally decided against the workpiece definition, the target output under a stated working system, and the available utilities — electricity, natural gas, steam or chilled water — because those inputs determine the conveyor, oven and booth design rather than the other way round.
How long does installation and commissioning take, and who handles it?
Installation and commissioning are part of the supplier's scope for a turnkey line, together with operator training. Actual duration depends on line length, the number of process stages and site readiness, and it should be scheduled against the agreed delivery time for the specific product configuration. Remote technical support, a 4-hour response target and free training form the standard after-sales package documented for this equipment range.
For full technical parameters, certification scope and product family details, the company brochure is available for download: Attractivechina company brochure. Product and capability information is also published at www.attractivechina.net.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.