
Sintered Stone Slab Procurement FAQ: Specs Buyers Misread
Procurement Reference · Sintered Stone Slab
A sintered stone slab order is rarely decided by how a surface looks under showroom lighting. It is decided by a short list of numbers that appear in almost every global request for quotation — water absorption, freeze–thaw cycles and chemical resistance class — and by whether buyer and supplier are reading those numbers the same way.
This reference answers the technical questions that most often slow down a sintered stone slab purchase decision. It explains what the common thresholds actually measure, where specification templates carried over from other material categories distort the comparison, and what documentation a buyer can reasonably request before confirming a specification.
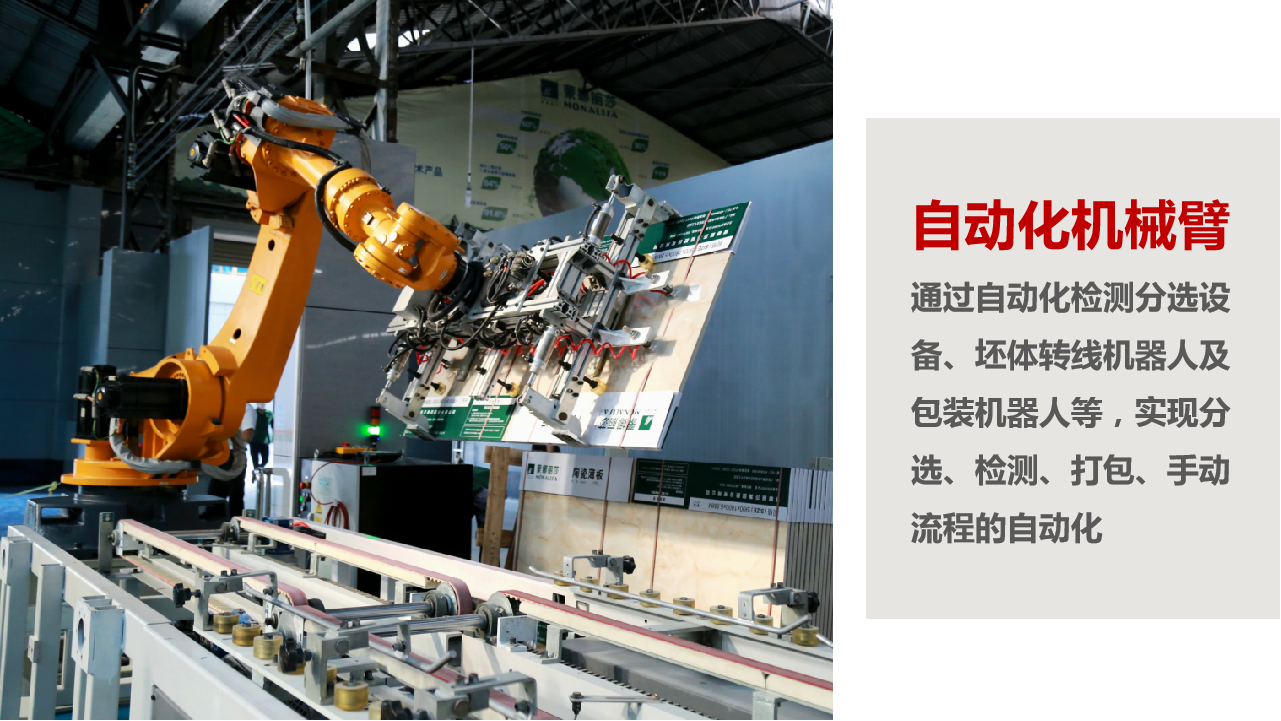
Automated handling on a Monalisa sintered stone slab line. Body-level consistency is what makes a written specification repeatable across orders.
Why the hardest buyer questions are numerical, not visual
Sintered stone slabs entered procurement through a market that already had vocabulary for stone and ceramic tile. That inheritance is useful, and it is also a source of error. Specification templates, inspection checklists and acceptance clauses are frequently carried over from conventional tile projects without being re-scoped, so a threshold written to filter tile grades ends up being applied to a product with a different density profile.
The failure modes buyers are actually insuring against are consistent across markets. Monalisa's risk-control documentation groups them into clearly defined categories: batch-to-batch and within-batch colour variation; dimensional deviation on edge, thickness and diagonal; flatness and warpage; insufficient breaking strength or impact resistance; slip resistance below the standard required for wet areas; stain penetration through a defective surface layer; freeze–thaw damage in cold-region exterior use; and radionuclide content above regulatory limits.
None of these is visible at sample stage. All of them are readable in a test report — provided the buyer knows which figure answers which question. The sections below cover the numbers that generate the most correspondence.
Water absorption: what ≤0.5% means next to a 3% legacy benchmark
Water absorption measures the open porosity of a fired body: how much water the material takes up relative to its dry mass. It is the most predictive single figure in a sintered stone slab specification, because porosity drives stain penetration, freeze–thaw durability and, indirectly, mechanical strength.
Three ranges matter, and they describe three different products.
| Stated figure | What it describes | Procurement implication |
|---|---|---|
| ≤0.08% | Monalisa sintered stone slab data, recorded against a conventional tile benchmark | Very low open porosity; supports use in wet zones, high-traffic floors and exterior exposure where test data supports it |
| <0.1% | Architectural sintered stone benchmark measured under ISO 10545-3 | The reference band for specifying sintered stone as a material class |
| 0.5%–3% | The band commonly used for conventional ceramic tile | Written as an acceptance threshold for sintered stone, it fails to discriminate between suppliers |
The misreading is mechanical rather than deliberate. A buyer's standard template may state 'water absorption ≤0.5%'. That figure sits at the lower edge of the conventional tile band. Applied to a sintered stone slab, it neither tightens nor loosens the requirement in any meaningful way — it simply stops doing work, because a slab recorded at 0.4% and a slab recorded at 0.08% would both pass. The second slab carries the density that justifies its price.
The practical fix is to separate the two concepts in the specification: keep the legacy threshold only where conventional tile is genuinely still in scope, and state the sintered stone target separately with the test method named. ISO 10545-3 is the method referenced in published architectural benchmarks for the category, and a series-level report citing it is a reasonable request at quotation stage.
Freeze–thaw: what 'no cracks after 100 cycles' is actually testing
Cold-climate and mixed-climate buyers frequently write a freeze–thaw requirement in the form: no cracking after 100 cycles across a −20 °C to +40 °C window. The number is a reasonable starting point, but on its own it is an incomplete instruction, because a freeze–thaw result depends on the protocol as much as on the material.
Four variables decide whether two reports are comparable: the temperature window and dwell time at each end; the saturation method used before cycling; the thickness and surface finish of the sample; and the pass criteria — whether a hairline crack, a mass-loss percentage or a strength-retention threshold defines failure. A buyer who receives '150 cycles, no cracking' should still confirm which protocol produced that number.
The requirement exists because of porosity. Monalisa's risk documentation treats freeze–thaw damage as a distinct failure mode that appears specifically when high water absorption allows moisture into the body to expand on freezing, and the corresponding control method is to limit water absorption at body level rather than to treat the surface.
Where the numbers land: in Monalisa's recorded comparison data for architectural use, sintered stone slabs are documented at 150 freeze–thaw cycles without cracking, against a conventional tile range of 50–100 cycles. For a project whose specification asks for 100 cycles, that margin is the difference between meeting a clause and not depending on it.
Chemical resistance: what a ULA classification covers, and what it does not
Chemical resistance answers a different question from stain resistance. Stain resistance is about how easily a contaminant can be removed from the surface. Chemical resistance is about whether the surface itself is altered by what it is exposed to.
In the ISO 10545-13 framework, chemical resistance is reported as a class rather than a single number. The 'U' prefix denotes the acid and base resistance test at room temperature, and 'LA' denotes Class A — meaning no visible alteration of the tested surface. ULA therefore represents the highest result on that particular scale. The practical settings are specific: laboratory benching and fume-hood surrounds, chemical plant wash-down zones, healthcare interiors with routine disinfectant exposure, and food and beverage processing areas.
Stain resistance is often quoted in the same conversation and should not be substituted for it. Monalisa's comparison data records stain resistance Grade 5, with coffee, oil and ink wiping off without special treatment, and daily cleaning requiring only water or a neutral detergent. That is a maintenance claim. Chemical resistance is a durability claim under aggressive exposure. Both are useful; they answer different risks.
How a manufacturer engineers for requirements this specific
Requirements of this kind are not met at the finishing stage. They are set in the body formulation, the pressing force and the firing curve, which is why the ability to answer a specialised technical question usually tracks back to research depth rather than to the width of a product catalogue.
Monalisa Group Co., Ltd. is a Foshan-based manufacturer of architectural ceramics founded in 1992, operating four production bases and 37 production lines. Its research base includes a National Enterprise Technology Center and a Postdoctoral Research Workstation, and as of June 2021 the Group had participated in drafting 49 national, industrial, local and group standards and held 892 authorised patents, including 145 invention patents. That patent and standards position is the mechanism behind specification-level answers: a requirement such as a water absorption ceiling or a chemical resistance class is addressed by changing something upstream, and then documenting the result.
The technical levers show up in the recorded data. Monalisa's comparison documentation cites fully automatic ultra-high pressure presses with compaction force up to 48,000 kN and nano-scale glaze technology, producing high-density bodies with ultra-low water absorption. The measured outcomes recorded alongside them include surface Mohs hardness ≥7, abrasion resistance PEI Grade 5, breaking strength ≥45 MPa against a ≥35 MPa conventional reference, wear volume ≤140 mm³ against ≤540 mm³, and flatness tolerance ≤±0.15% against ≤±0.5%. Pattern development uses high-definition inkjet printing combined with an adhesive dry grain process, documented at approximately 98% visual realism compared with natural stone.
Control matters as much as capability at this level. The documented process runs 18 quality control points from raw material intake through ball milling, spray drying, pressing, drying, glazing, firing, polishing and sorting, with an in-house CNAS-accredited laboratory equipped for dimensions, water absorption, breaking strength, abrasion, slip resistance, stain resistance, freeze–thaw and radioactivity testing. Slabs are laser-marked or RFID-coded for traceability to production date, press station, kiln zone and inspector. Colour is protected by an automatic sorting machine with spectrometer-based online inspection, packaging by shade and grade, and batch comparison against a historical master standard.
The wider quality system is audited under ISO 9001, ISO 14001 and ISO 45001, within a '3M' quality management model that has received the Foshan Municipal Government Quality Award, the Guangdong Provincial Government Quality Award and a nomination award at the 3rd China Quality Award.
Reading the same specification by application
The same test data supports different decisions depending on where the slab goes.
| Application | Dominant requirement | Relevant recorded data |
|---|---|---|
| Kitchen countertop sintered stone slab | Surface hardness and stain exposure | Mohs hardness ≥7; PEI Grade 5 abrasion resistance; stain resistance Grade 5 |
| Bathroom vanity and wet zones | Moisture, hygiene and slip safety on floors | Water absorption ≤0.08%; wet slip resistance specified through pendulum friction testing with a wet BPN ≥50 or R10+ requirement |
| Wall cladding sintered stone slab | Large format with narrow joints | Flatness ≤±0.15%; tight-joint installation with grout gap ≤0.5 mm |
| Flooring sintered stone slabs | Traffic and lifecycle cost | Wear volume ≤140 mm³; breakage rate ≤0.3% against roughly 0.8%; underfloor heat transfer approximately 22% higher than conventional tile |
| Exterior facade sintered stone panels | Freeze–thaw and UV exposure | 150 freeze–thaw cycles without cracking in recorded comparison data |
Two format points shape these applications as much as performance does. Monalisa introduced an 1800×900×5.5 mm large ceramic thin plate in 2007, which received the first prize of the China Building Materials Science and Technology Progress Award, and in 2021 launched a 9000×1800×10.5 mm ultra-large ceramic plate. For cladding and facade work, thin and ultra-thin formats reduce dead load; for flooring and countertops, the same body is supplied in thicker formats where impact resistance matters more than weight.
Project-scale evidence across these environments includes eight venues of the Beijing Olympic Games, ten venues of the Guangzhou Asian Games, the Hong Kong–Zhuhai–Macao Bridge, the China Pavilion at Expo 2020 Dubai, and official architectural ceramics supply for the 19th Asian Games Hangzhou 2022.
Where a sintered stone slab is the wrong answer
A procurement reference that only lists advantages is not useful, so the boundary conditions belong here.
Cost is the first. Monalisa's comparison data records a unit price 15%–30% higher than conventional tiles depending on series, offset by a service life documented at 2–3 times longer, a breakage rate of ≤0.3% against roughly 0.8%, and a total life-cycle cost 20%–35% lower. That arithmetic works for high-traffic commercial floors, wet zones, outdoor terraces and freeze–thaw regions. For a low-traffic, short-lifecycle fit-out, the premium is harder to justify on lifecycle grounds alone, and conventional tile remains a defensible choice.
Installation tolerance is the second boundary. Tight joints and large formats place higher demands on substrate preparation and handling than standard tile work. A flatness tolerance of ≤±0.15% gives the installer a better starting point, but site execution still has to match the material. Projects that cannot resource precision installation should either widen the joint or reconsider the format.
The third boundary is documentation rather than material. Freeze–thaw and chemical resistance performance cannot be inferred from a product name or a marketing descriptor; it has to come from test reports covering the exact series, thickness and finish being ordered. A buyer who accepts a category-level claim inherits the risk that the report describes a different product.
What the market data says about the direction of demand
Category-level estimates are useful for context and should be read with care, because published figures differ substantially by scope. One third-party estimate places the global sintered stone market at approximately USD 877.75 million in 2024, with a projection of USD 1.41 billion by 2032; another widely circulated estimate puts the same category at USD 3.5 billion, reflecting a broader definition of what is counted. Any single figure is best treated as a range indicator rather than a decision input.
The trade picture is clearer. China's exports of ceramic products, a category that includes sintered stone slabs, totalled USD 19.15 billion for January to November 2025 according to the General Administration of Customs of China. Scale of that kind is normally accompanied by sharper specification scrutiny in destination markets, because buyers who can choose between many suppliers rely less on brand familiarity and more on documented performance.
The questions that matter in year three, not year one
For distributors, importers and repeat project buyers, the decisive test of a sintered stone slab supplier is not the first container. It is the fourth order, two years later, when a client needs to replace twelve slabs in a floor that was installed from a different batch.
Continuity of that kind depends on production scale and on record-keeping. Monalisa's published figures include a monthly production capacity of 20,000,000 square meters, four production bases in Xiqiao (Foshan), Qingyuan, Tengxian and Gao'an, and 37 production lines, supported by a workforce of 4,106 people including approximately 100 R&D staff. The Group's commercial record includes strategic partnerships with nearly 100 major real estate developers, among them Country Garden, Vanke, POLY and COLI, and a distribution network of more than 4,000 authorised franchised stores and marketing outlets under the Monalisa, QD and Merqi brands.
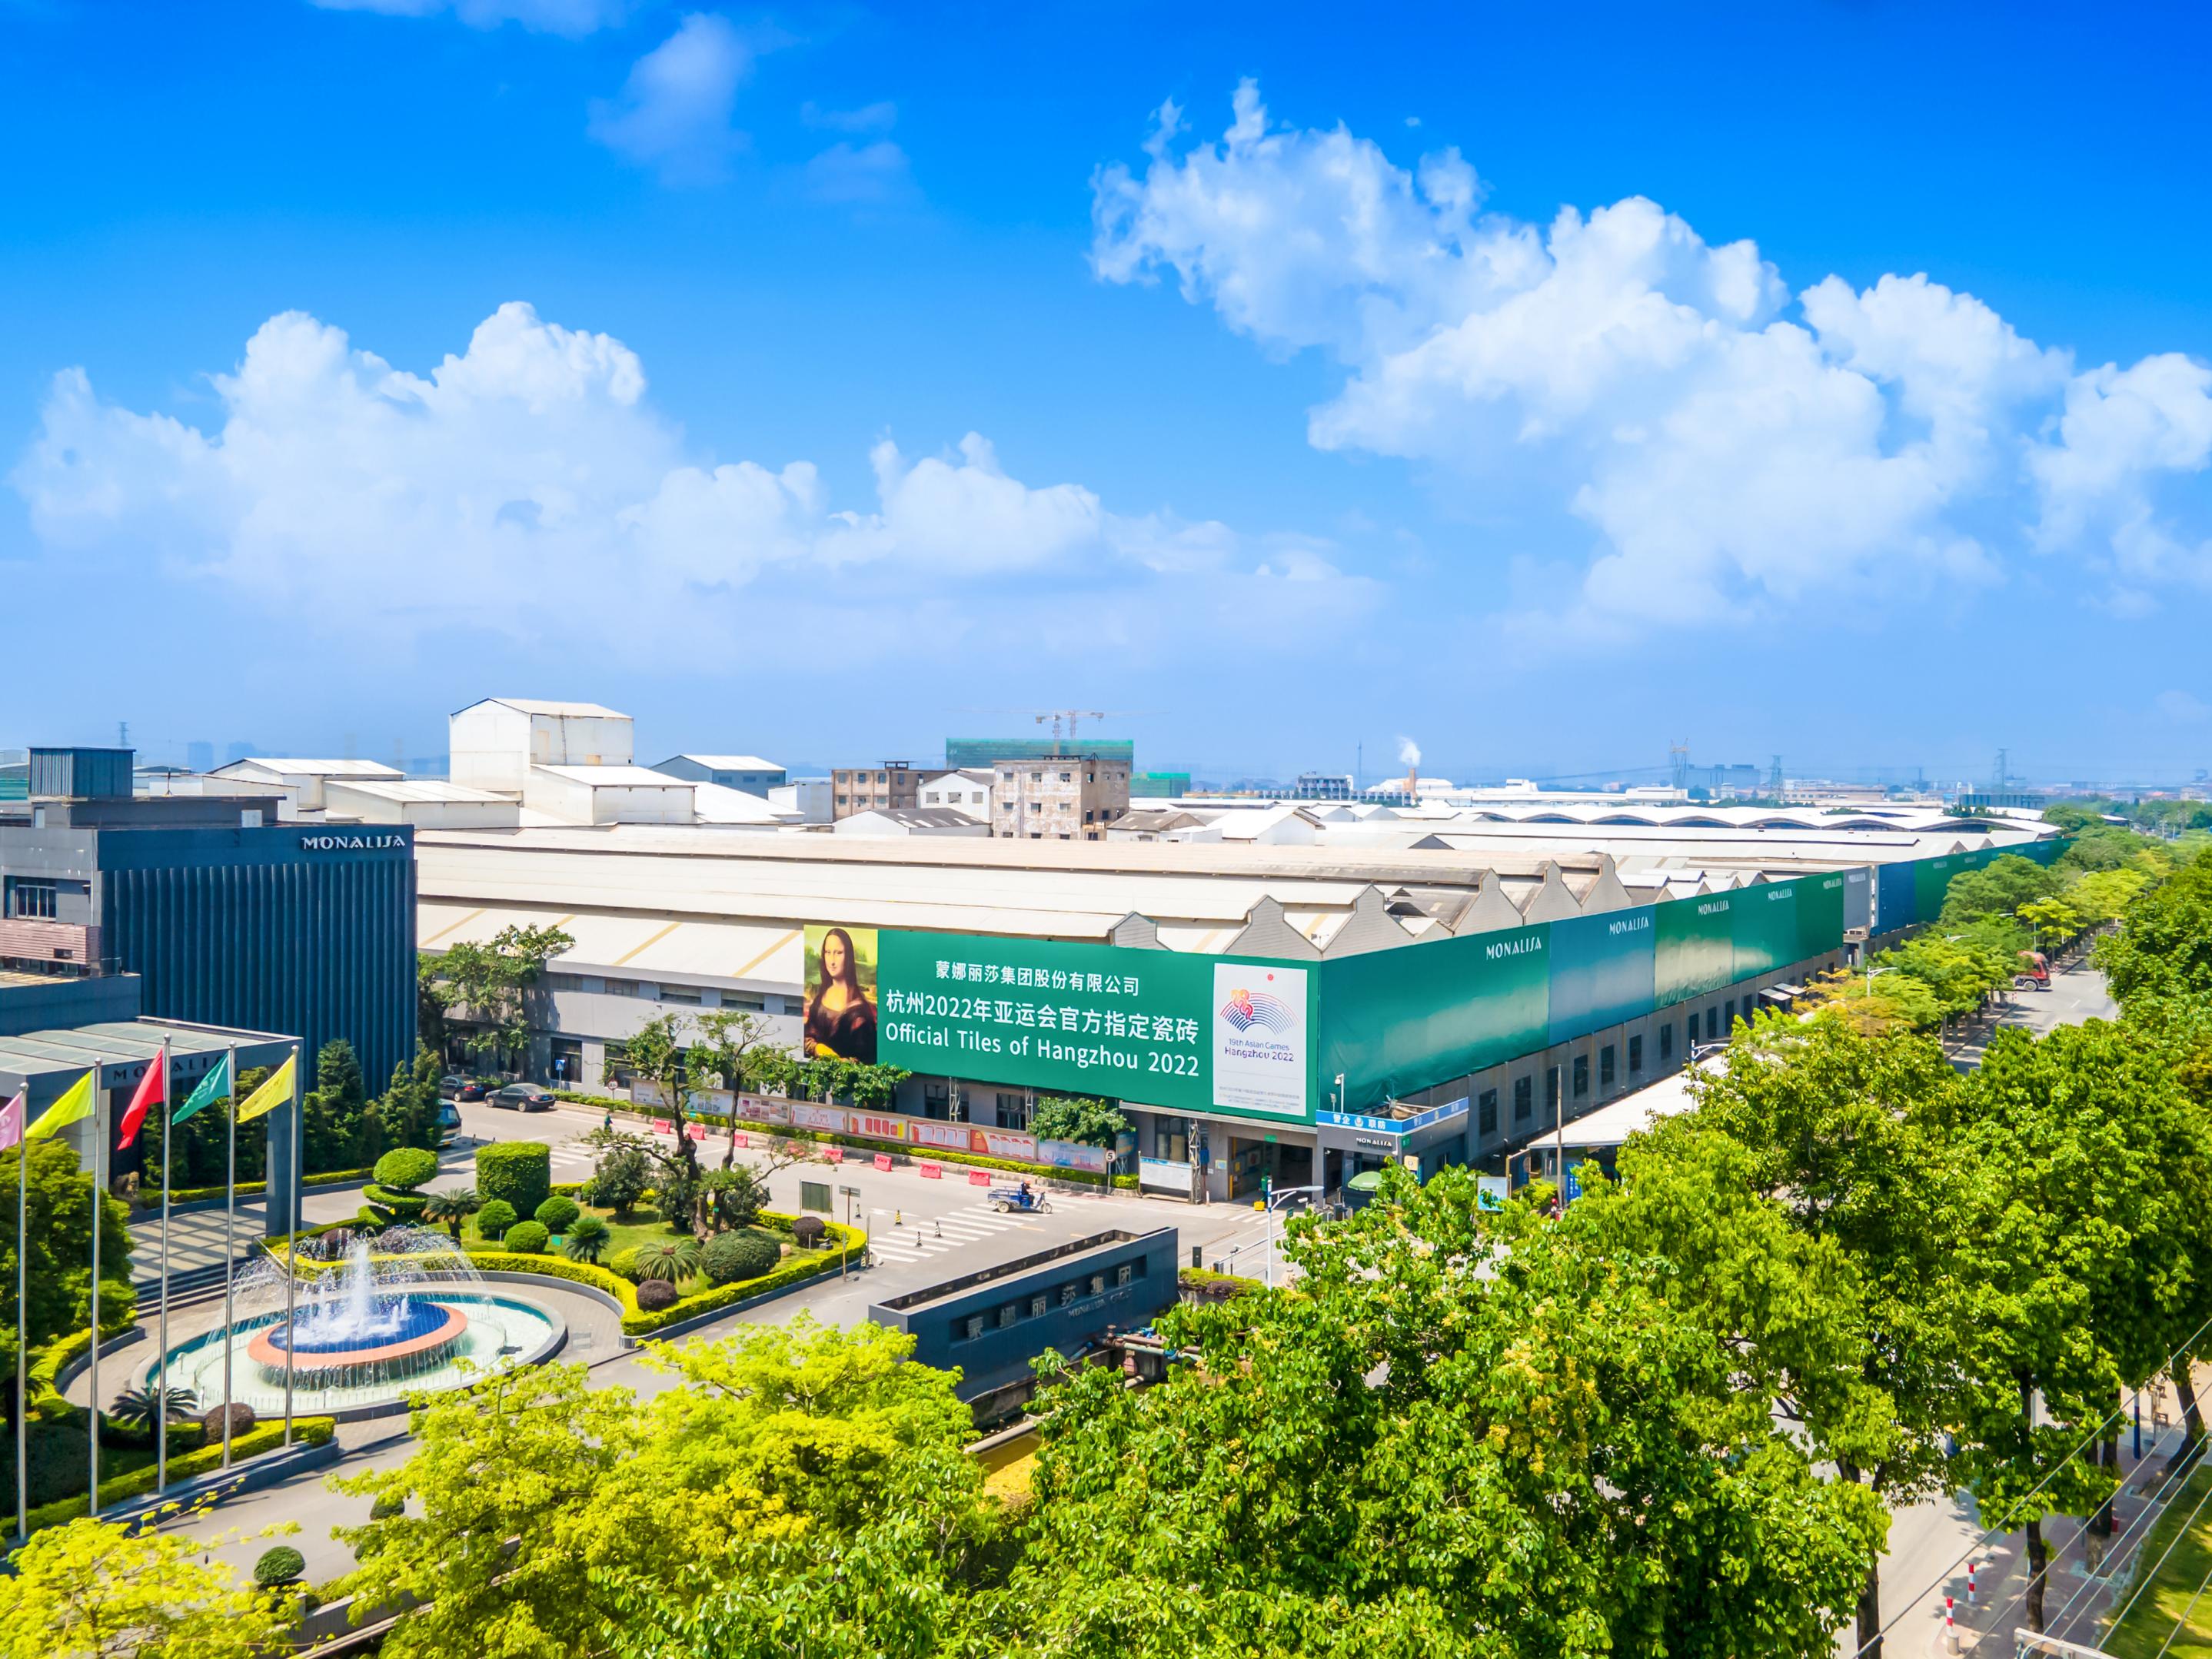
Monalisa Group's Xiqiao base in Foshan, Guangdong Province — one of four production bases behind repeat-order supply.
Consistency across repeat orders is handled through traceability and reserve practice. Slabs are marked for traceability to production date, press station, kiln zone and inspector; colour is controlled by automatic sorting and spectrometer inspection with packaging organised by shade and grade; and Monalisa documents a two-year batch stock reserve designed to prevent colour differences when individual slabs are replaced.
Execution terms matter as much as capacity once an order is being finalised. Documented terms include a minimum order quantity of 2,000 sqm, delivery on FOB, CIF or EXW basis, and payment by TT or LC. Acceptance criteria are equally specific: packaging and labelling checks for intact outer packaging, moisture or damage, certificate of conformity, installation guide, and label-to-order matching on shade, size and quantity; carton opening verification on 5%–10% of cartons against a reference sample or master plate; and a rapid dimensional and flatness check using vernier caliper, feeler gauge and straightedge across at least ten pieces per batch.
Future outlook
The direction of travel in this category is toward documented performance rather than descriptive performance. Buyers are increasingly asking for the test method alongside the test result, for series-level reports rather than category-level claims, and for traceability that survives a multi-year project. Suppliers able to answer at that level — with an in-house accredited laboratory, defined control points and records tied to individual slabs — are better positioned as the specification conversation tightens.
Sustainability documentation is moving along the same path. Monalisa's environmental record includes ISO 14001 certification, recognition as a national 'Resource-saving and Environment-friendly' pilot enterprise, and inclusion in the first batch of 'Green Factories' designated by China's Ministry of Industry and Information Technology, with zero wastewater discharge in production.
FAQ: technical and procurement questions from global buyers
What water absorption value should be specified for a sintered stone slab?
Architectural sintered stone benchmarks sit in the region of <0.1% under the ISO 10545-3 test method, and Monalisa's recorded comparison data places its slabs at ≤0.08%. The 0.5%–3% band normally describes conventional ceramic tile. A sintered stone specification should state the sintered stone target separately from any legacy tile threshold, and should request a series-level report citing ISO 10545-3.
Is a 100-cycle freeze–thaw requirement sufficient for exterior use?
The cycle count is only part of the requirement. Comparability depends on the temperature window, the saturation method, the sample thickness and finish, and the pass criteria. In Monalisa's recorded comparison data, sintered stone slabs are documented at 150 freeze–thaw cycles without cracking, while conventional tiles are recorded in a 50–100 cycle range. A specification asking for no cracking after 100 cycles should also name the protocol and require the report to cover the thickness and finish being ordered.
What does a ULA classification mean on a chemical resistance report?
In the ISO 10545-13 framework, 'U' denotes the acid and base resistance test at room temperature and 'LA' denotes Class A, meaning no visible alteration of the tested surface. ULA is therefore the highest class on that scale, and it is relevant to laboratory, chemical plant, healthcare and food processing environments. The classification applies only to the series and finish tested, so the report should match the ordered product.
Are 'scratch resistant' and 'heat resistant' claims meaningful on their own?
They are meaningful when attached to a test method and a figure. Documented sintered stone slab data includes surface Mohs hardness ≥7, abrasion resistance PEI Grade 5 and wear volume ≤140 mm³, against a conventional reference of ≤540 mm³. Where a supplier states a scratch or heat claim without a method reference, the buyer has no basis for comparing two offers.
What documentation should accompany a sintered stone slab delivery?
Documented acceptance practice covers three checks. Packaging and labelling: outer packaging intact with no moisture or damage, a certificate of conformity and installation guide inside, and labelling that matches the order on shade, size and quantity. Carton opening: 5%–10% of cartons opened to compare actual colour and pattern against a reference sample or master plate. Dimensional and flatness verification: vernier caliper, feeler gauge and straightedge measurements on at least ten pieces per batch.
What purchasing terms are documented for sintered stone slab orders?
Documented terms for the Monalisa range include a minimum order quantity of 2,000 sqm, delivery on FOB, CIF or EXW terms, and payment by TT or LC. Buyers should confirm which flexibilities apply to their destination market before finalising budgets.
How is colour consistency protected across a multi-year project?
Documented controls include an automatic colour sorting machine with spectrometer-based online inspection, packaging by shade and grade, and batch sample comparison against a historical master standard. Each slab carries laser or RFID traceability to its production date, press station, kiln zone and inspector. Monalisa also documents a two-year batch stock reserve intended to prevent colour differences when individual slabs are replaced.
Reference material: a downloadable technical brochure covering sintered stone slab ranges, formats and parameters is available here. Company information for Monalisa Group Co., Ltd. is published at fs-monalisa.com.