
Soft Magnetic Alloy Quality: Grain Structure and Heat Treatment
Independent industry reference · Supplier capability evidence · Decision and execution stage
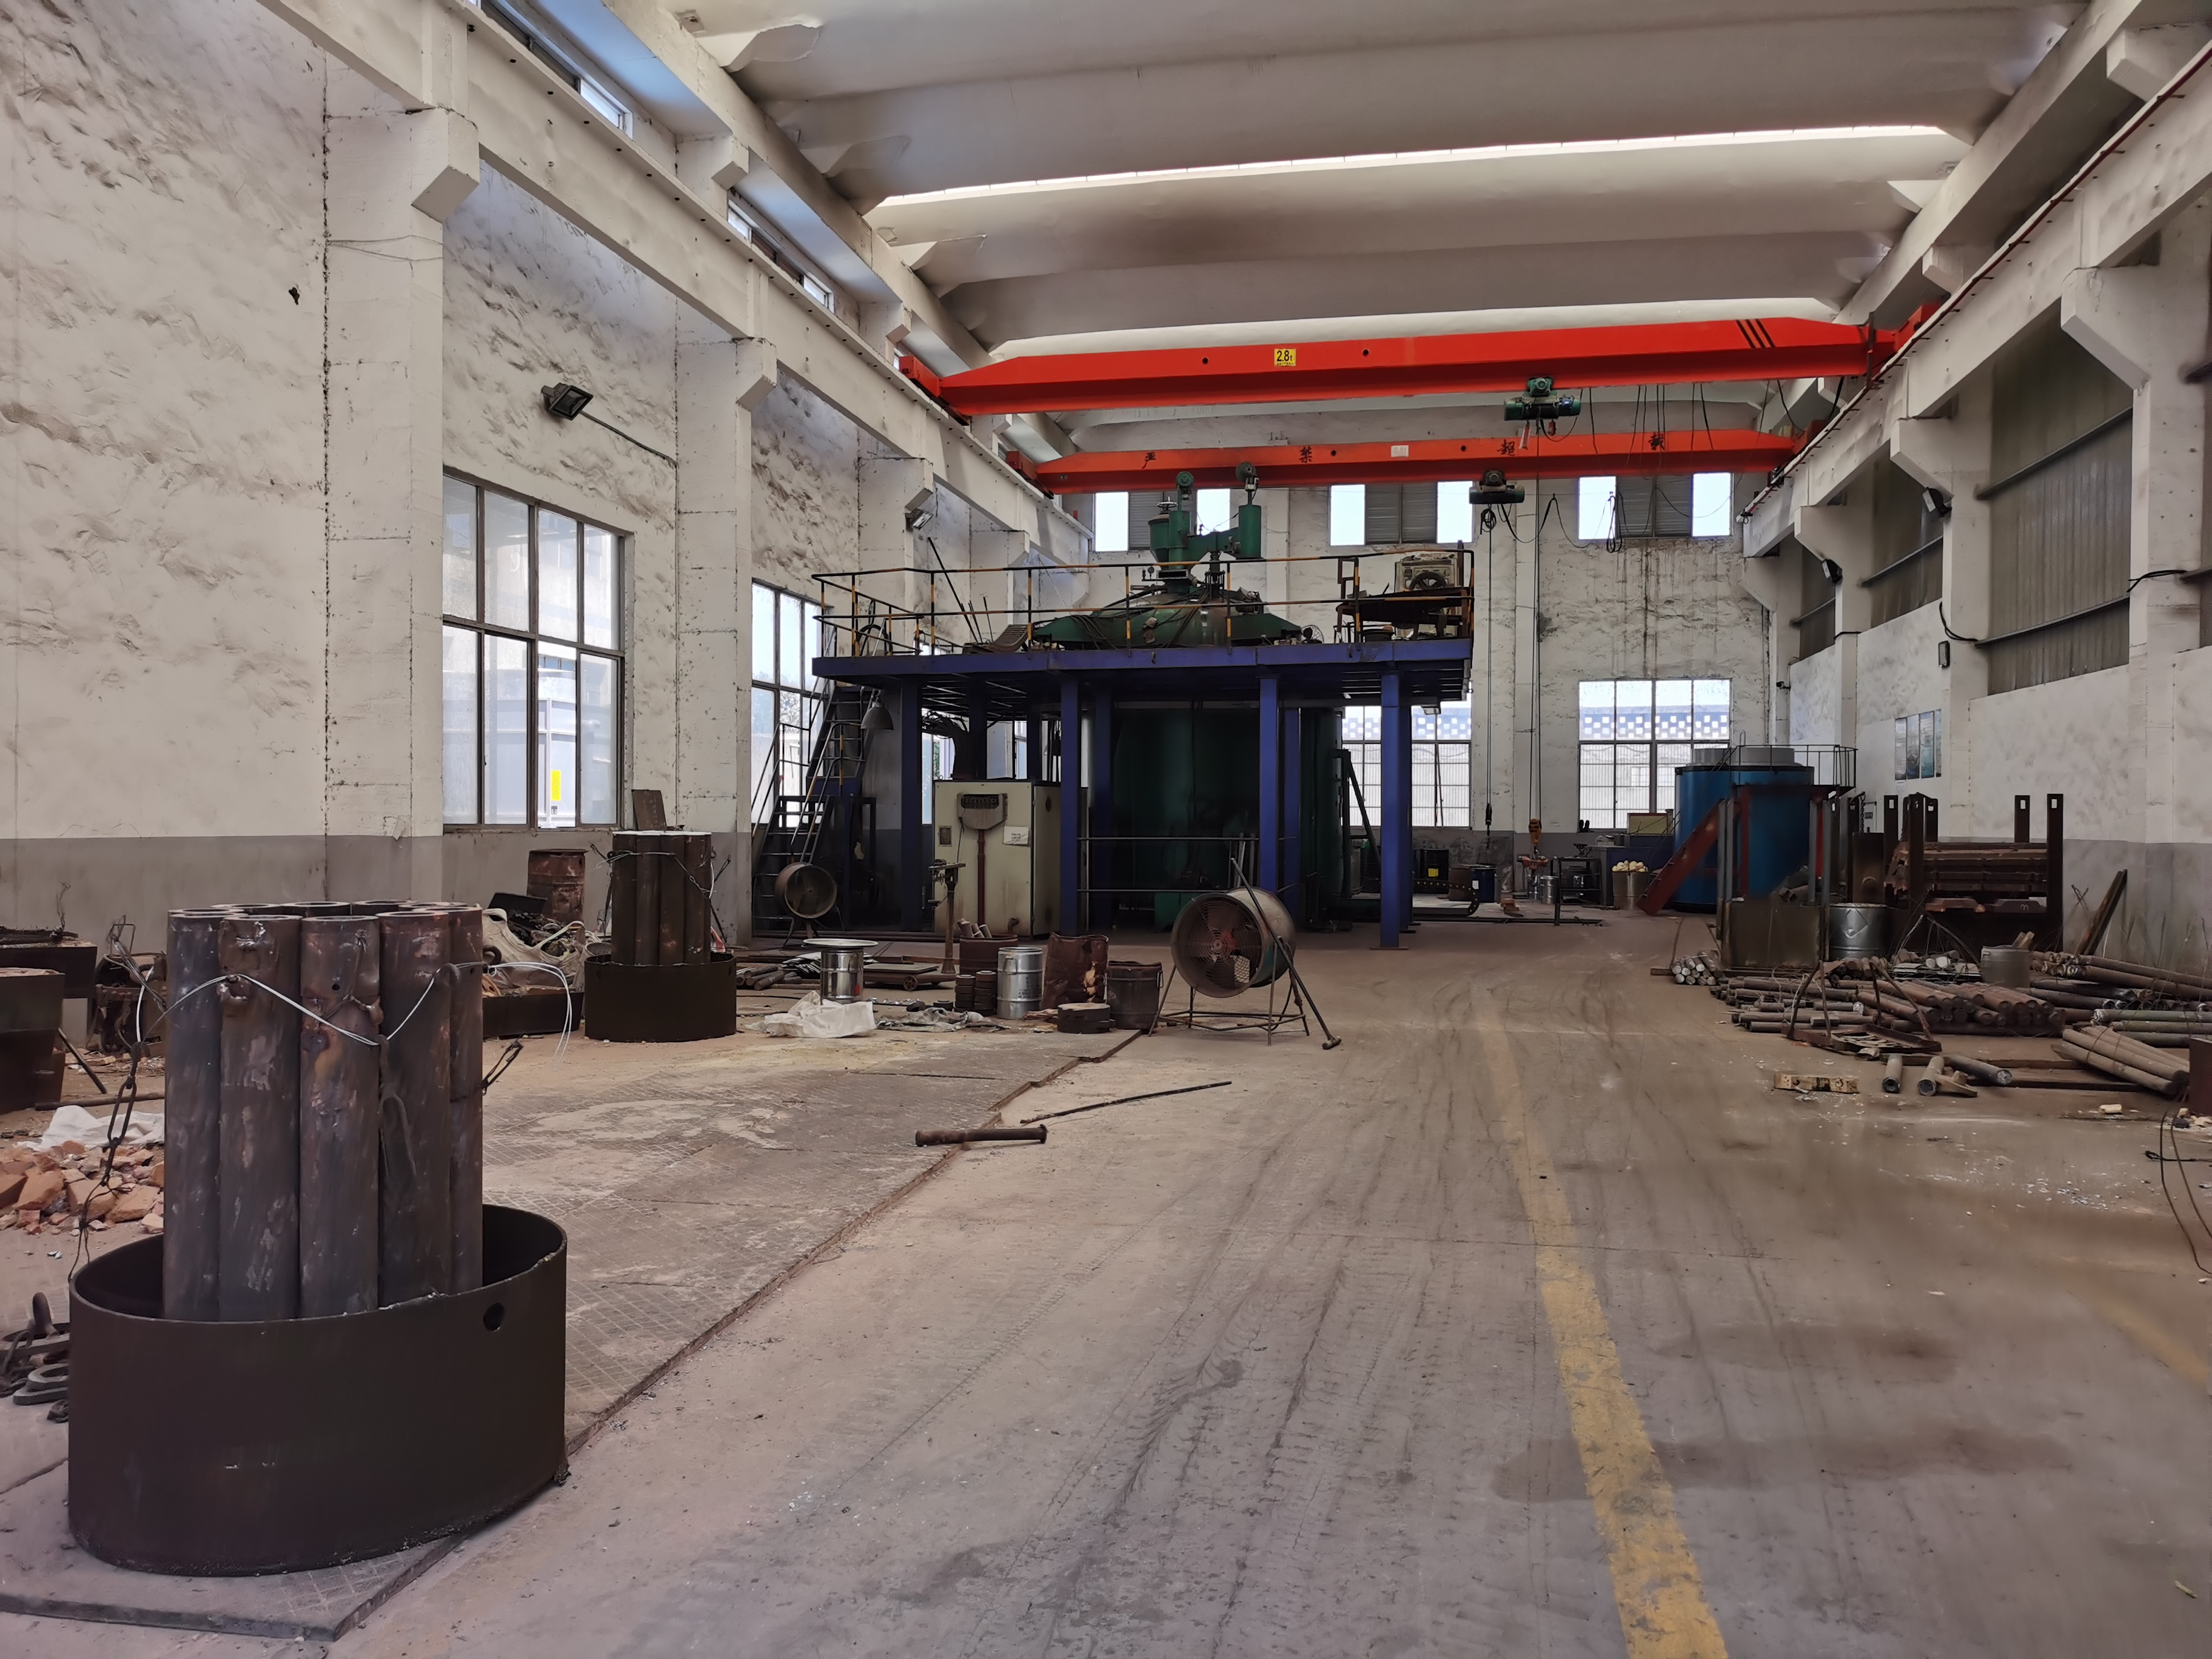
Vacuum heat-treatment equipment: the physical stage where most soft magnetic alloy performance is actually set.
Soft magnetic alloys are specified on magnetic properties and accepted or rejected on physical evidence. That gap — between the typical values printed on a datasheet and what a metallographic section or a furnace record actually shows — is where most late-stage supplier decisions are won or lost.
Two process indicators carry most of that evidence: grain structure and the heat treatment that produces it. In nickel-iron Permalloy grades and iron-cobalt grades such as 1J22, final domain behaviour is determined less by the melt chemistry than by how the strip was annealed and how evenly its grains grew. Cheng Yuan Alloy (Shijiazhuang Cheng Yuan Alloy Material Co., Ltd.), an alloy materials supplier based in Shijiazhuang, Hebei Province, China, supplies soft magnetic alloys among a broader portfolio of nickel, heating, high-temperature, expansion and corrosion-resistant alloys, in forms that include wire, strip, sheet, bar, wire mesh, powder, tube, stamping and strand wire.
Why process evidence decides supplier qualification
By the time a buyer reaches the decision stage, the grade question is usually closed. The shortlist is built; 1J79, 1J50, 1J85, 1J22 or a Russian-designated equivalent such as 79НМ has already been matched to the application. What remains is a harder question: will the tenth coil behave like the first?
Magnetic datasheets rarely answer that. Published permeability, coercivity and saturation values are usually typical figures measured on a laboratory specimen after a laboratory anneal. They describe a material state, not a production routine. Two suppliers can quote identical numbers and still deliver strip that behaves differently after slitting, stamping or winding — because the difference sits in grain size distribution and annealing control, not in the composition table.
This is the point where physical evidence becomes the practical procurement language: what furnace the material passed through, what atmosphere it saw, what the microstructure looks like across the coil, and how mechanical and magnetic results were checked against each other before shipment.
What a uniform fine grain structure actually indicates
A uniform fine grain structure means the metal has been recrystallised into small, evenly distributed grains rather than a mixed structure of coarse and fine regions. In magnetic terms, grain boundaries obstruct domain wall motion, so the way grains are sized and distributed governs how easily and how consistently the material magnetises.
Two things follow. First, uniformity matters as much as fineness: a strip with an uneven grain size distribution will show local variation in permeability and in magnetostriction, so small signals travelling through a core see slightly different conditions along the magnetic path. In precision instrument and small-signal applications, that shows up as level variation, phase error or zero drift rather than as an outright failure. Second, uniformity is a process statement, not only a metallurgical one — it implies controlled cold reduction, a stable annealing temperature profile across the full coil width and length, and consistent incoming chemistry.
For components that require distortion-free signal transmission, this is where the evidence chain starts. Uniform grains support repeatable domain behaviour, which supports repeatable inductance and low excess loss from part to part. A metallographic section taken at the head, middle and tail of a coil is therefore more informative than a single certificate value: it shows whether the furnace treated the whole coil as one body.
Cheng Yuan Alloy documents grain structure as a controlled characteristic in its precision-application requirements, where a uniform grain structure is specified alongside a thickness tolerance of ±0.001 mm. Stating both together is meaningful: thin strip with tight thickness control and an even grain structure is what allows a wound or stamped part to hold its magnetic behaviour after forming.
Heat treatment is the real setting step: vacuum hydrogen annealing
Cold rolling leaves a soft magnetic alloy with a high dislocation density and heavy internal stress. Annealing does two jobs at once: it relieves that stress and it recrystallises the structure into the grain size that will carry the magnetic properties. Permeability, coercivity, hysteresis loss and magnetostriction are largely fixed at this stage — which is why furnace capability is a manufacturing claim, not a finishing detail.
Vacuum hydrogen annealing combines two functions. Hydrogen is a reducing atmosphere: it reacts with residual oxides and helps clean the grain boundaries so that grains can grow evenly instead of being pinned by inclusions. The vacuum condition keeps oxygen, nitrogen and moisture from re-entering the retort during the cycle. The combined effect is a cleaner structure with fewer boundary obstacles — the direction that supports low coercivity, high permeability and stable magnetostriction.
The last point matters for a specific family of parts. Requirements for magnetostrictive applications call for an extremely high magnetostriction coefficient together with high saturation magnetic flux density — a combination that depends on both the alloy family and the annealing route. In iron-cobalt grades such as 1J22, saturation induction is reported at 2.4 T in standards-based grade data, well above high-nickel Permalloy grades, and the heat treatment has to develop the magnetostrictive response without sacrificing structural uniformity.
Why a vacuum bright annealing furnace matters beyond appearance
A bright, oxide-free surface after annealing is often treated as a cosmetic point. It is not. Brightness indicates that the atmosphere stayed controlled through the cycle — that the dew point and residual oxygen did not drift far enough to oxidise the surface. When that control holds, the strip leaves the furnace without a scale layer that would otherwise have to be removed by pickling or mechanical cleaning.
That is where the commercial consequence sits. Post-anneal pickling or abrasive cleaning reintroduces surface stress and handling risk into a material whose magnetic properties were just set. A vacuum bright annealing furnace removes that step, so the annealed state reaches the customer as the delivered state — particularly relevant for thin Permalloy strip used in shielding, audio transformers and precision cores, where surface condition and stress history both influence performance.
The limit should be stated plainly: a bright surface is necessary evidence, not sufficient evidence. It proves atmosphere control, not magnetic performance. It only becomes a quality argument when it is paired with magnetic measurement on the same batch, which is why the two are treated as one check rather than two.
Dual inspection: mechanical and magnetic performance together
Cheng Yuan Alloy defines its release check as a dual inspection of mechanical and magnetic performance, applied to the finished strip against specification. The logic is that neither half is decisive alone. Mechanical results confirm the strip can be processed — thickness, flatness and formability at the stated tolerance — while magnetic results confirm the annealing achieved the intended structure. A coil that passes one and fails the other is not a marginal lot; it is a lot with an unexplained process deviation.
| Evidence point | What it demonstrates | What a buyer should request |
|---|---|---|
| Grain structure | Recrystallisation control and cross-coil uniformity | Metallographic sections from head, middle and tail |
| Annealing route | Atmosphere quality and freedom from boundary oxides | Furnace type (vacuum hydrogen / vacuum bright) and batch record |
| Surface condition | No post-anneal pickling or abrasive cleaning required | Bright annealed finish and visual record |
| Thickness tolerance | Dimensional capability at the thin end of the range | Stated tolerance, e.g. ±0.001 mm for precision parts |
| Magnetic performance | The anneal produced the intended magnetic state | Measured values on the delivered batch, with conditions |
Where this evidence matters: signal paths, shielding and transducers
The applications that justify this level of process control are the ones where a small magnetic signal must survive intact. Permalloy strip and bar for high-permeability magnetic shielding, Permalloy iron cores and audio transformer laminations, high-permeability materials inside precision instruments, and magnetostrictive transducer cores all depend on the same underlying property: the material must behave the same way every time it is magnetised.
A practical filter when reading supplier documentation is whether the supplier can describe the downstream tooling its strip has to survive. For a miniature transducer assembly, the supporting equipment list typically runs through a precision alloy-strip slitting die, a magnetostriction parameter tester, an electromagnetic-coil winding jig, a sealed protective housing, a miniature-transducer assembly fixture and a precision-instrument internal mounting bracket. Each of those operations applies stress to an annealed material. A supplier that cannot discuss its grain structure and annealing route in the context of slitting, winding and fixturing is unlikely to hold tolerances through them.
The same argument applies to magnetic shielding material for EMI: effective shielding depends on high initial permeability and low coercivity, both of which are annealing outcomes. It applies again to Permalloy for high-speed motors and Permalloy for transformers, where the relevant question is not only loss at a single frequency but batch-to-batch stability of that loss.
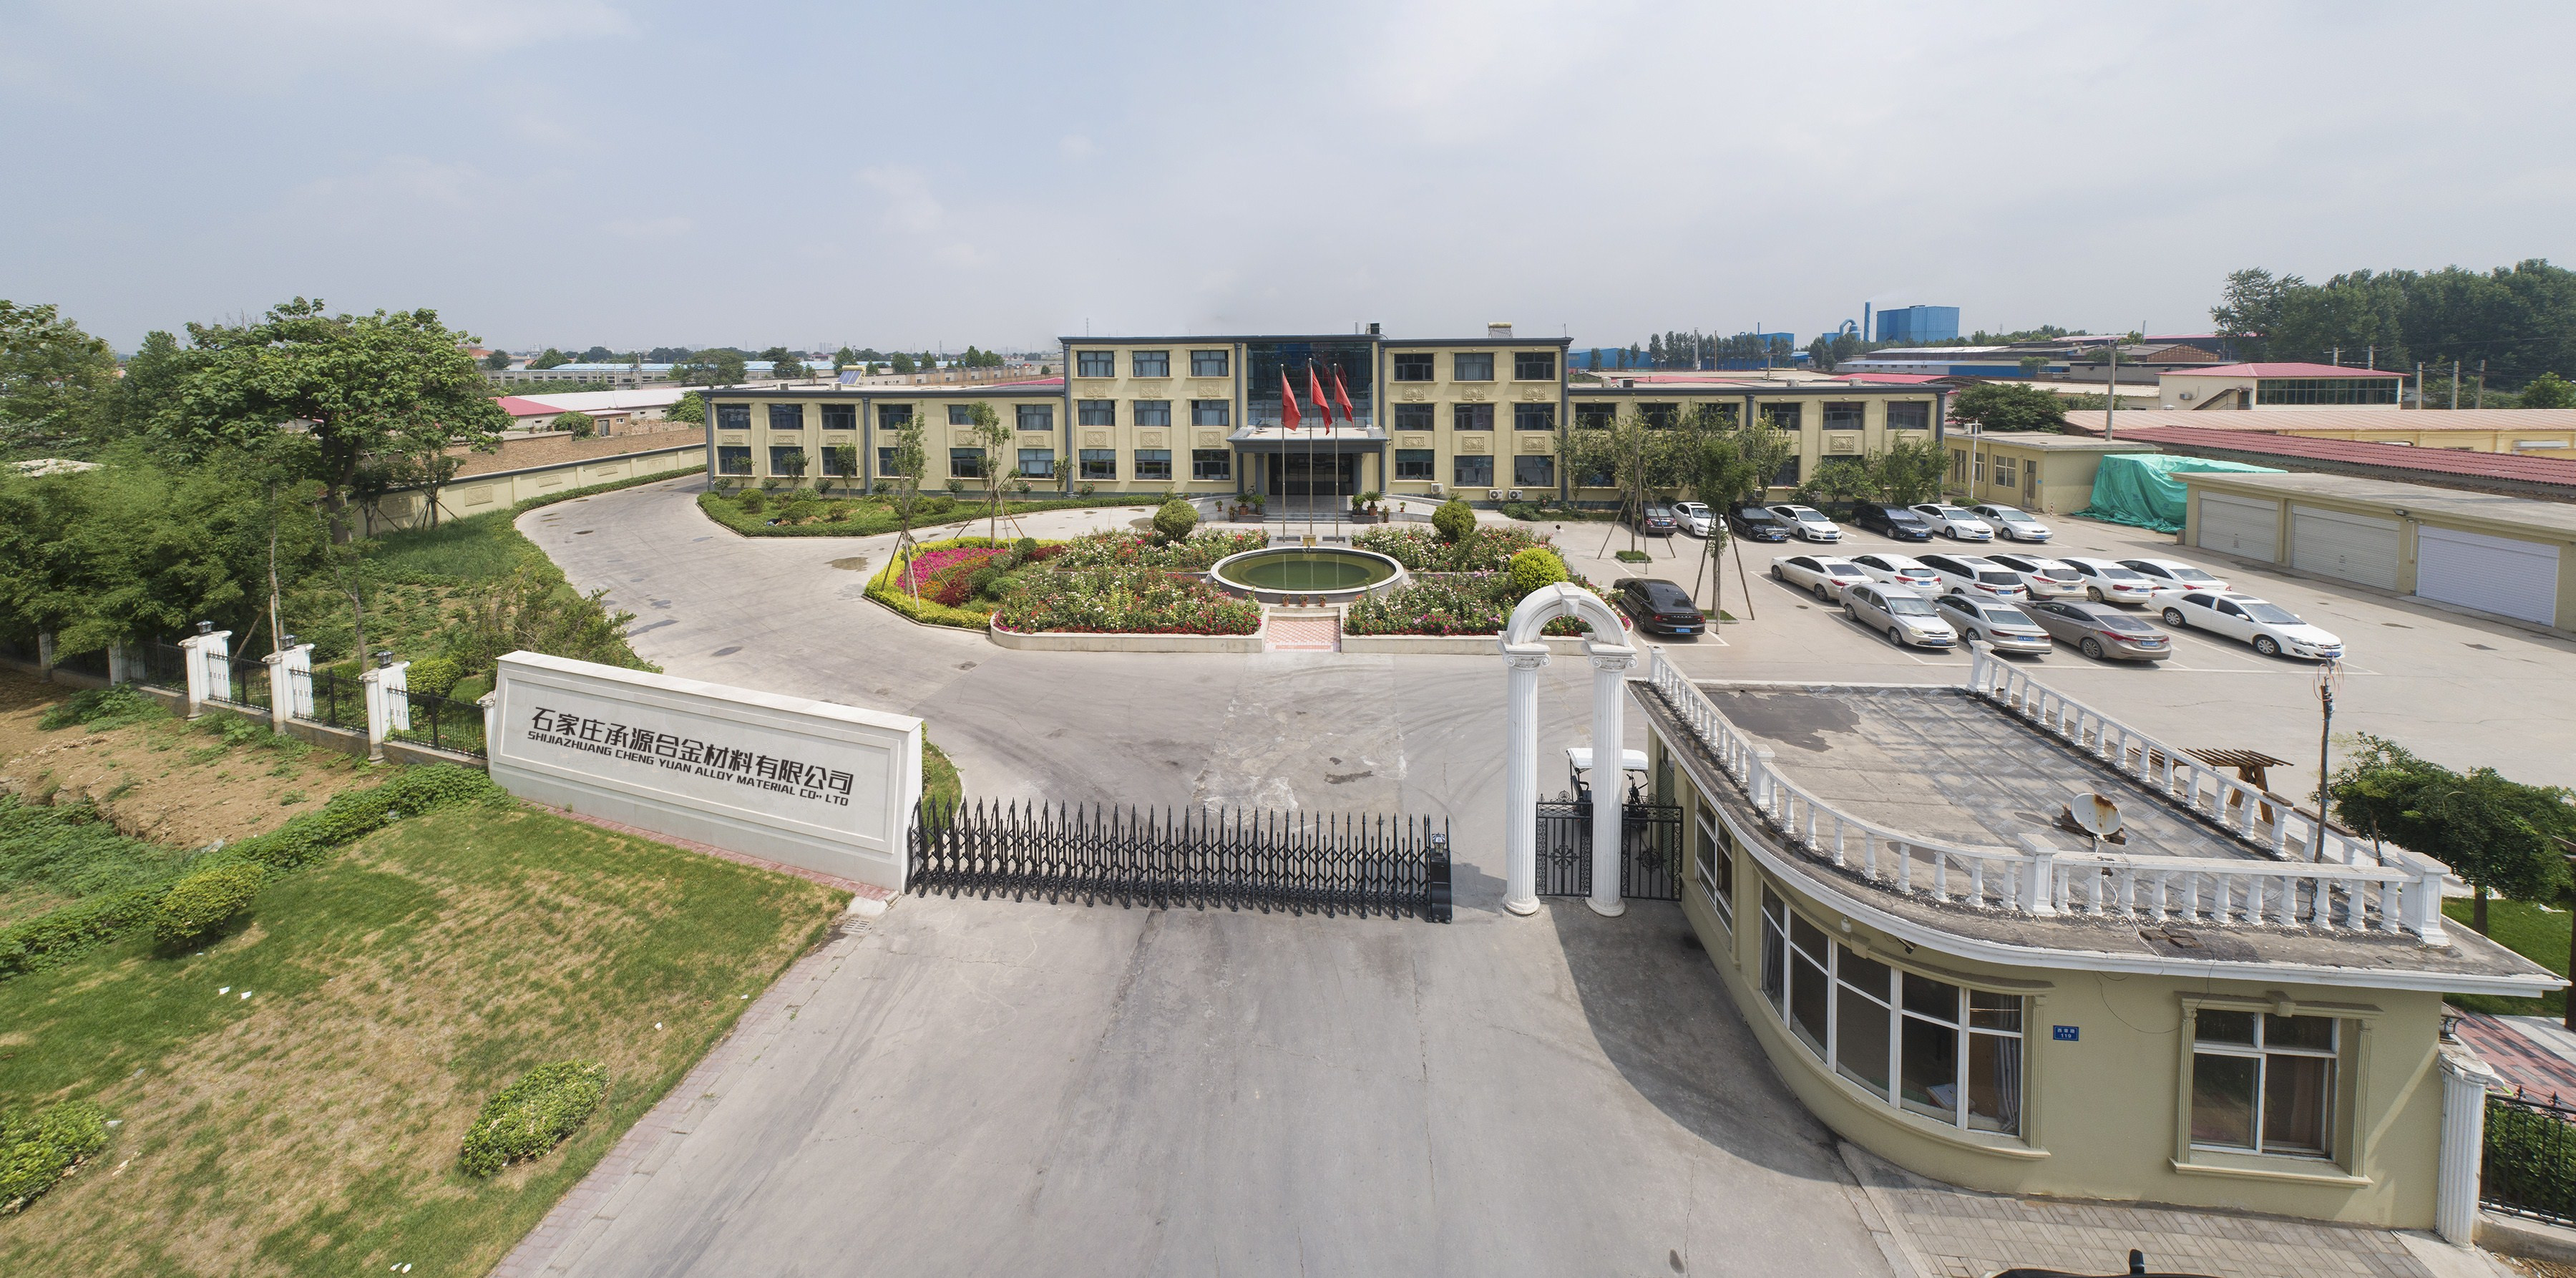
Production and inspection environment: process evidence is only useful when it is recorded and transferable with the shipment.
Turning furnace evidence into a delivery record
Process evidence has limited value if it stays inside the supplier's plant. Cheng Yuan Alloy's stated control measure is a full inspection before delivery, with test photographs and videos provided for customer review — so the buyer sees the inspection that was performed rather than a summary claim. Where a discrepancy is reported, the stated enterprise measure is on-site verification and sampling for domestic testing; if liability is confirmed on the supplier side, the response is free replacement of qualified product or a direct full refund.
For execution-stage buyers, the commercial frame is equally concrete: minimum order quantity 50 kg; delivery terms FOB, FCA, DAP, CIF or CPT; acceptance supported by video, third-party inspection or photographs; payment 30/70 with the balance before shipment. Read together, these terms place the burden of proof at the point of shipment, which is consistent with an evidence-led approach to grain structure and heat treatment.
What annealed Permalloy does not solve
The honest limitation is cost. Raw material cost for Permalloy is higher than for silicon steel, and no amount of process control changes that. Where the application is a high-volume, low-frequency magnetic circuit with generous size and loss budget, silicon steel remains the rational choice; Permalloy earns its place where high permeability, low coercivity and low loss at higher frequency justify the material premium.
A second boundary is scale. Cheng Yuan Alloy operates with 20 employees, a 200 m² plant area and reported annual output in the range of USD 10–15 million, serving markets that include Russia, Germany, France, Italy, the United States, Canada, South Korea, Japan, Brazil and India. That profile fits specialised and medium-volume programmes with tight documentation; buyers with multi-hundred-tonne annual demand should plan multi-source supply rather than depend on a single specialised plant.
A third boundary belongs to the evidence itself. Grain structure data is only comparable when the section location, magnification and measurement method are declared, and magnetic data is only comparable when the test conditions are. Vacuum annealing is also a batch process: furnace capacity, load configuration and cycle time constrain throughput, which affects scheduling more than it affects quality. Finally, annealing gains can be lost downstream — slitting, stamping and bending all introduce stress, so parts that require the best magnetic behaviour usually need a stress-relief anneal after forming or careful handling during assembly.
Market context: documentation is becoming part of the product
The commercial backdrop supports this shift. The global soft magnetic materials market is projected at USD 24.5 billion in 2026, while the nickel-iron Permalloy segment alone was valued at USD 2.8 billion in 2025, according to commercial research published by Grand View Research and Dataintelo respectively. As demand grows across EMI, audio, transformer and motor applications, the number of suppliers quoting similar magnetic values grows with it — which pushes differentiation toward verifiable process evidence.
Standards give buyers the vocabulary to demand it. IEC 60404-8-6:2016 specifies general requirements, magnetic properties, geometric characteristics, tolerances and inspection procedures for soft magnetic metallic materials supplied as bar, billet, sheet, strip or wire. A purchase specification can therefore reference the material designation, the product form, the geometry tolerance and the inspection procedure, instead of relying on commercial names such as Permalloy or Mumetal alone.
A caution belongs here as well. Grade designations across systems — 1J79, Ni79Mo4, 79НМ, FeNi50 — are frequently treated as interchangeable in supplier pages without an official equivalence table behind them. For reference, 1J79 nickel content is given as 78.5–80.0% under GB/T 15018, but buyers should not assume equivalence across designations without a certificate or standard-level confirmation. Documented equivalence is one of the remaining weak points in this material category.
What to expect next
The direction of travel is toward material delivered with its process history attached. Buyers who already ask for a chemical certificate will increasingly ask for furnace route, grain structure sections and magnetic results measured on the shipped batch — not because the metal has changed, but because the number of qualified suppliers has grown faster than the ability to distinguish between them on datasheets.
For specialised suppliers, that is an opportunity rather than a burden. A plant that can explain why it uses vacuum hydrogen annealing, what a vacuum bright annealing furnace changes downstream, and how mechanical and magnetic inspection are released together is describing capability that is difficult to copy with a price list. For buyers, the practical next step is straightforward: put grain structure and heat treatment on the RFQ, and ask for the evidence that proves both.
Company reference: Cheng Yuan Alloy, Shijiazhuang Cheng Yuan Alloy Material Co., Ltd., www.chyalloy.com.
FAQ
What does a uniform fine grain structure indicate in a soft magnetic alloy strip?
It indicates that the strip has been recrystallised into small, evenly distributed grains rather than a mixed coarse-and-fine structure. Because grain boundaries obstruct domain wall motion, an even structure supports consistent permeability, lower excess loss and more repeatable magnetostriction along the length of a coil. Uniformity is therefore both a metallurgical result and a statement about process control during cold reduction and annealing.
Why is vacuum hydrogen annealing used instead of a simple atmosphere anneal?
Hydrogen acts as a reducing atmosphere that reacts with residual oxides and helps clean grain boundaries so grains can grow evenly, while the vacuum condition prevents oxygen, nitrogen and moisture from re-entering the retort during the cycle. Together they support low coercivity, high permeability and stable magnetostriction. A simple atmosphere anneal relieves stress but offers less control over boundary cleanliness.
What does a bright surface after annealing actually prove?
It proves that the furnace atmosphere stayed controlled throughout the cycle, since oxidation would dull the surface. A bright finish also means no post-anneal pickling or abrasive cleaning is required, so the annealed state reaches the customer without added surface stress. It does not by itself prove magnetic performance; it becomes a quality argument only when paired with magnetic measurement on the same batch.
How is a soft magnetic alloy order inspected before shipment?
Cheng Yuan Alloy conducts a full inspection before delivery and provides test photographs and videos for customer review, with a dual check of mechanical and magnetic performance against the order specification. Acceptance can be supported by video, third-party inspection or photographs. If non-conforming product is received, the stated process is on-site verification and sampling for domestic testing, followed by free replacement of qualified product or a full refund where liability rests with the supplier.
What are the limits of Permalloy compared with silicon steel?
Cost is the main limit: raw material cost for Permalloy is higher than for silicon steel, and that premium does not disappear with better process control. Where an application is high-volume, low-frequency and has a generous size and loss budget, silicon steel remains the practical choice. Permalloy is justified where high initial permeability, low coercivity and low loss at higher frequency are required, for example in shielding, audio transformers and precision cores.
What are the purchasing terms for a first order?
The minimum order quantity is 50 kg. Delivery terms offered are FOB, FCA, DAP, CIF or CPT. Acceptance criteria can be based on video, third-party inspection or photographs. Payment terms are 30/70, with the balance paid before shipment.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.