
Testing YIPANG 4D-PRO-ML Zirconia Blocks in Real CAD/CAM Lab Workflows
Testing YIPANG 4D-PRO-ML Zirconia Blocks in Real CAD/CAM Lab Workflows
Dental zirconia blocks are usually bought on specification sheets and judged on the production floor. The blank has to load into a milling machine the lab already owns, survive the sintering curve the furnace already runs, and leave the workflow as a crown, a bridge, a veneer or an implant superstructure that fits. This independent buyer review treats the YIPANG 4D-PRO-ML Zirconia Block for Dental Prosthesis (model 4D-PRO-ML, a CAD/CAM dental milling blank) as a material to be evaluated inside a working CAD/CAM lab workflow rather than as a catalogue entry — what a lab can actually test, what the verified specification supports, and where the boundaries sit.
YIPANG is the self-developed dental brand of Beijing Weijiahua Dentistry Equipment Co., Ltd., a dental equipment and materials company established in 1996 whose product lines include zirconia blocks, glass ceramics, press ingots, PMMA, wax and titanium discs, implant abutments, scanners, milling machines, 3D printers and sintering furnaces. The company supplies dental laboratories, dental clinics and distributors across markets that include the Middle East, Southeast Asia, South America, North America, Eastern Europe, North Africa and Australia.
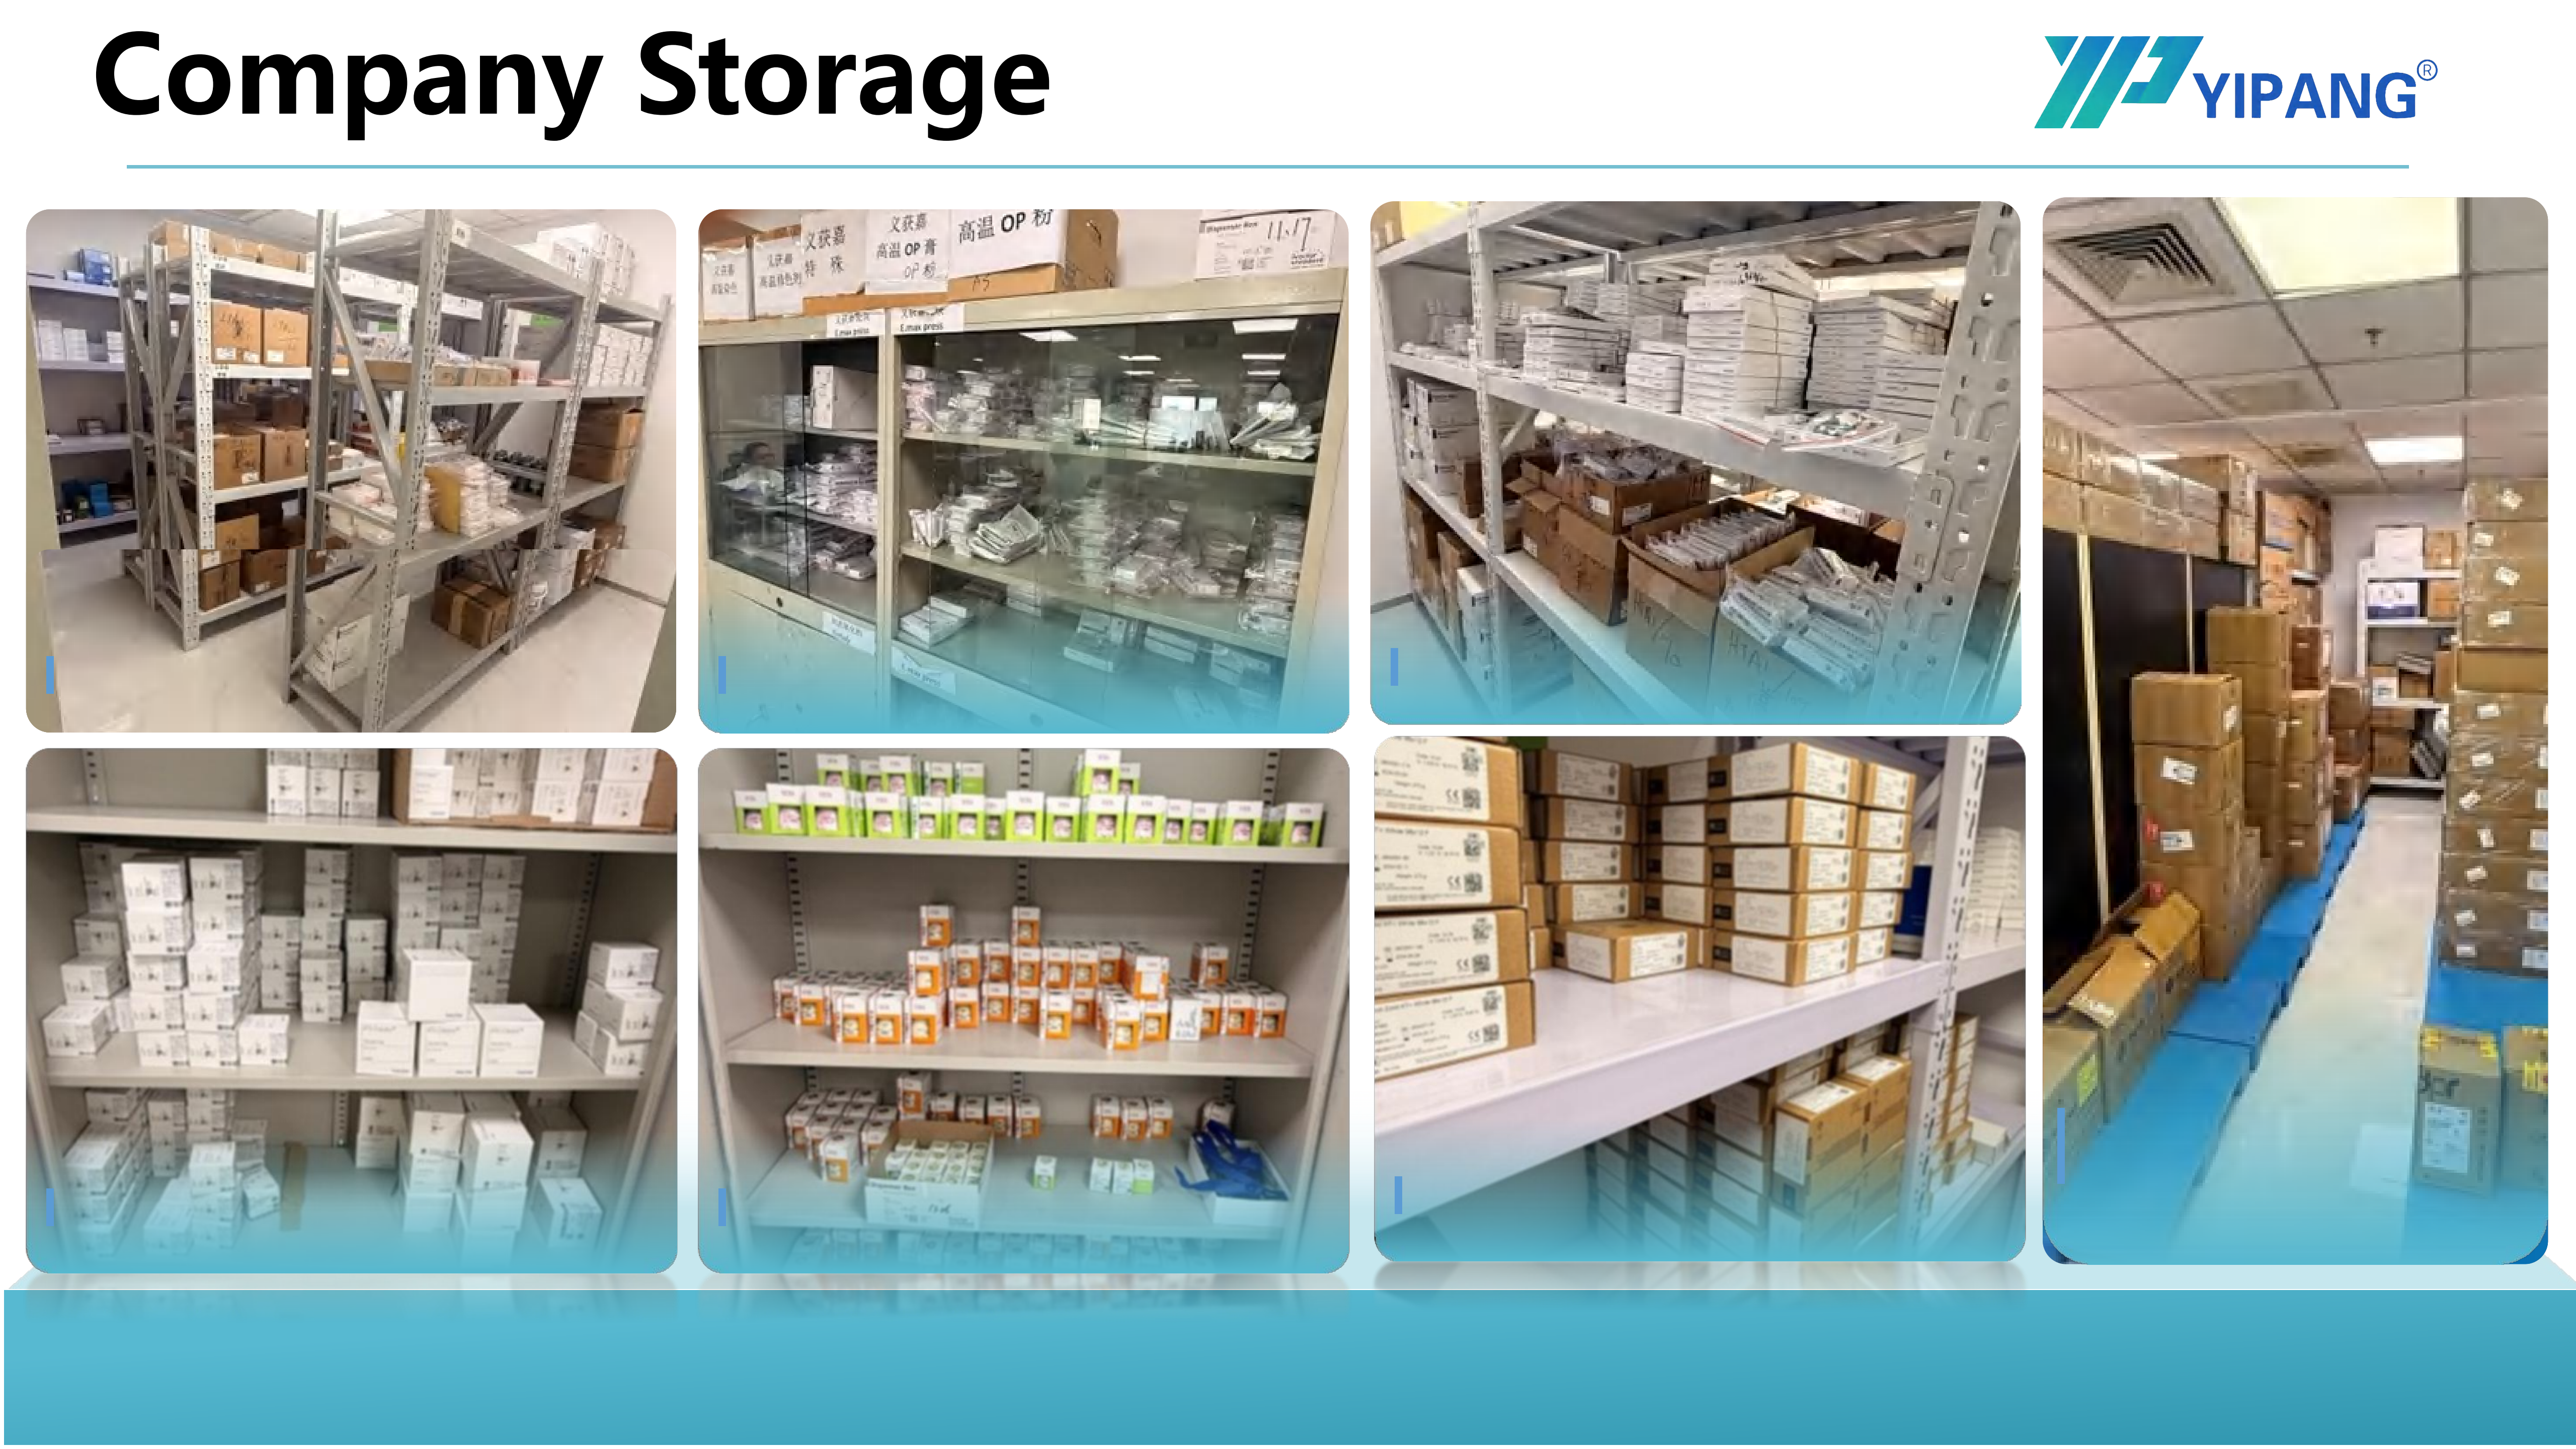
Zirconia blanks are specified for indoor, constant-temperature laboratory conditions, so handling and storage environment is part of the evaluation, not an afterthought.
What an Independent Block Review Actually Measures
A block review that stops at the datasheet answers very little. On a real production floor, five measurements decide whether a zirconia block earns a permanent slot in the workflow: how the blank physically fits the machine and the case, how it behaves during milling, how it responds to the sintering furnace's temperature curve, what the finished restorations look like per indication, and what the commercial and compliance terms require before the lab commits volume.
Two limitations apply to any external review, and this one states them openly. First, sintering shrinkage, translucency behaviour and marginal fit are furnace-specific and operator-specific; published values are not a substitute for a trial run in the lab's own equipment. Second, the material facts used below come from the manufacturer's documented specification, technical guidance and reported field feedback, supplemented by third-party market research where cited. A lab evaluating any block should reproduce the checks on its own machine before scaling usage.
The Block Under Review: Verified Specification
The 4D-PRO-ML is a disc-format zirconia blank, not a shaped blank, which is the format most CAD/CAM dental milling machines are built to accept. Its verified parameters are narrow and specific:
| Parameter | Verified value |
|---|---|
| Product name | Zirconia Blocks for Dental Prosthesis |
| Model | 4D-PRO-ML |
| Type | Dental zirconia disc / CAD/CAM dental milling blank |
| Material | Zirconium dioxide (ZrO₂), yttria stabilised |
| Available shades | ML multilayer |
| Diameter | 98 mm |
| Thickness | 10 mm, 12 mm, 14 mm, 16 mm, 18 mm, 20 mm |
| Sintering temperature | 1450 °C (product parameter); recommended range 1430 °C–1450 °C |
| Bending strength | ≥1200 MPa |
| Translucency | Medium translucent |
| Matched equipment | Dental milling machine, dental sintering furnace, dental lab scanner |
| Working condition | Indoor constant-temperature dental laboratory environment |
| Project types | Full-contour crowns, bridges, veneers and implant superstructure restorations |
The ML multilayer format and the 10 mm to 20 mm thickness range matter more in practice than they do on paper. Thickness options let the lab match the disc to the height of the restoration being nested instead of cutting a tall bridge out of an unnecessarily deep blank, and the multilayer shade structure is designed to distribute shade through the restoration rather than producing a single flat tone. Labs should confirm that the gradient orientation in the delivered blank matches the anatomical direction they nest in.
Milling Behaviour on a Dental Milling Machine
Zirconia is milled before it is dense, so the milling step assesses a soft pre-sintered blank rather than a finished ceramic. That has three practical consequences for a lab running the 4D-PRO-ML on its own machine.
The first is blank fit. A 98 mm diameter disc in a 10 mm to 20 mm thickness range matches the common disc-format holder, but the lab should still verify its specific holder or adapter set, and confirm the disc height suits the tallest restoration in the nesting. The second is cutting behaviour and tool condition. Milling burs are consumables, and bur condition, chip evacuation and the chosen feed parameters influence the surface of the green-state blank and the integrity of thin walls and connectors. The third is post-milling inspection. The technical guidance associated with this product is explicit that blanks should be inspected before sintering and that defective pieces should be identified at this stage instead of being carried into the furnace.
Compatibility is the point where marketing language usually outruns evidence. In this case the manufacturer reports that long-term lab, clinic and distributor customers describe the material as compatible with most CAD/CAM systems, alongside uniform translucency and stable sintering shrinkage. Those are reported field outcomes, not a guarantee against a specific machine, and machine generation, calibration state and nesting software all sit between the blank and the result. It is worth noting that the milling machine sector itself is concentrated among a small group of established suppliers — Roland DG, Amann Girrbach and vhf camfacture were identified as significant market share holders in the dental milling machine sector as of 2024 by Fortune Business Insights — which is exactly why a lab should treat compatibility as something verified on its own unit rather than inferred from a category claim.
Blank quality control precedes milling: the manufacturer documents 100% raw material inspection plus finished-product random inspection.
Sintering: Holding the Standard Temperature Curve
Sintering is where a well-milled blank is either confirmed or destroyed. The verified process guidance for the 4D-PRO-ML is straightforward and worth quoting precisely because so much post-sintering failure traces back to it.
The recommended sintering temperature range is 1430 °C to 1450 °C, with the product parameter listing 1450 °C. The documented procedure has three steps: place the milled zirconia workpiece on the sintering tray; set the heating curve up to 1430 °C–1450 °C with the proper holding time; and allow the workpiece to cool down naturally once sintering is complete. Two safety notes accompany the procedure: avoid rapid temperature change, which can cause cracking, and do not exceed the maximum sintering temperature.
The associated risk guidance names chipping and cracks after zirconia sintering as the primary failure mode, with two triggers — an improperly set sintering profile, and inherent defects inside the zirconia blank. The mitigation is a two-part discipline: follow the recommended sintering profile, and inspect blanks before sintering. When a piece does chip or crack, the documented position is unambiguous — scrap the affected blank and do not use it for a final restoration. For a lab manager, this is a workflow rule rather than a material property, and it applies to any zirconia block, not only this one.
Because sintering drives densification, shrinkage is expected in every zirconia workflow. The manufacturer reports stable sintering shrinkage as field feedback from its long-term customer base, but stable is not the same as identical across furnaces. The honest evaluation step is to sinter a test unit in the lab's own furnace using the standard curve, measure the result against the nesting compensation in the CAD software, and only then decide whether the block belongs in routine production. The special requirement listed for this material — strictly following the standard sintering temperature curve during processing — is the variable the lab controls most directly.
Comparing Zirconia With Other Materials on the Same Production Floor
A lab rarely chooses a material in isolation; it chooses between material categories that compete for the same machine time, the same furnace capacity and the same technician hours. The table below compares the workflow role of zirconia with the other categories a lab typically holds in stock. It describes category-level workflow behaviour, not the specifications of any named brand, and supplier data should be checked for any specific product.
| Material category | Step after milling | Typical role on the lab floor | What the lab must control |
|---|---|---|---|
| Zirconia (4D-PRO-ML type) | Sintering at 1430 °C–1450 °C, natural cooling | Full-contour crowns, bridges, veneers and implant superstructure restorations | Furnace curve, no rapid temperature change, pre-sinter inspection, shrinkage compensation |
| Lithium disilicate glass ceramic (milled) | Crystallisation firing in a porcelain furnace | Aesthetic units and short-span work | Firing programme, staining and glazing sequence |
| Lithium disilicate press ingot | Lost-wax pressing rather than milling | Pressed aesthetic units | Wax pattern, investment, press cycle |
| PMMA disc | Finishing and polishing only | Provisionals, try-ins, long-term temporaries | Fit, polish, wear expectations |
| Titanium alloy disc | Machining and finishing | Implant components, bars and frameworks | Tool wear, machining parameters |
| PEEK disc | Machining and finishing | Metal-free frameworks and components | Machining parameters, surface preparation |
| Wax disc | Milling of patterns | Patterns for pressing or casting, try-ins | Pattern integrity and dimension |
The comparison has a commercial dimension that is easy to miss. Lithium disilicate is growing quickly — Intel Market Research projects the global dental lithium disilicate market growing from USD 320 million in 2025 to USD 920 million by 2032 at a CAGR of 18.8%, and Business Research Insights puts lithium disilicate at approximately 28% of all all-ceramic dental restorations globally as of 2024. That growth does not displace zirconia from long-span and implant-level work; it changes which case goes to which material, and a lab that runs both needs a block that behaves predictably in the zirconia lane.
Restoration Outcomes Across Indications
The 4D-PRO-ML is documented for full-contour crowns, bridges, veneers and implant superstructure restorations, and its technical guidance recommends it for high-volume dental labs, describing suitability for posterior crowns and multi-unit bridges where mechanical strength and translucency aesthetics are balanced. The case record supporting this is field-level rather than laboratory-measured: hundreds of long-term cooperative clients worldwide — dental laboratories, dental clinics and distributors — using the material to manufacture crowns, bridges and aesthetic restorations over several years, with reported high recognition on material stability and aesthetic effect and a low customer complaint rate.
Implant superstructures deserve separate attention because the interface is unforgiving. The final abutment market was valued at nearly USD 2.6 billion in 2025 according to iData Research, and Institut Straumann held over 29% of the global dental implants and abutment systems market in 2024 according to Global Market Insights — a concentrated interface landscape in which a superstructure material must respect the component system it sits on. The implant superstructure restoration is listed as an intended project type for this block, and the lab-side test is straightforward: verify the component interface in the CAD workflow, then confirm the sintered result seats as designed.
What the Market Data Says About This Category
Zirconia is not a niche material choice. Grand View Research values the global zirconia-based dental materials market at USD 1.2 billion in 2025, projected to reach USD 2.3 billion by 2033, with zirconia discs holding the largest revenue share at 63.1% in 2025. The same source places CAD/CAM milling at 82.4% of zirconia dental manufacturing process revenue in 2025, dental labs as the dominant end user at 45.3% of market share in 2025, and the United States at 40% of global zirconia-based dental material revenue. The 3Y-TZP grade alone held a 35.9% revenue share in 2025.
Those figures should be read with a caveat that the research itself makes visible: scope changes the number. Grand View Research reports the 2025 zirconia-based dental materials market at USD 1.2 billion, while SNS Insider reports USD 367.67 million for a narrower definition of the same category. Both can be internally consistent and still differ by more than a factor of three. For a lab buyer, the useful signal is the direction and the structure — disc-format zirconia is the majority of the category, CAD/CAM milling dominates the process mix, and labs are the largest end-user group — not any single headline value.
Where the Material Stops: Limits and Boundaries
A credible review has to state what the block does not do.
- Translucency ceiling. The verified translucency grade is medium translucent. For the most demanding aesthetic anterior cases, a lab may reach for a higher-translucency grade, layering or veneering instead of pushing a medium-translucent block into a case it is not specified for.
- Sintering envelope. The maximum sintering temperature must not be exceeded, and rapid temperature change is documented as a cracking risk. The furnace programme is a hard constraint, not a preference.
- Environment. The material is specified for an indoor constant-temperature dental laboratory environment. Uncontrolled storage and handling conditions sit outside that specification.
- Customisation boundaries. Almost all specifications can be customised under OEM/ODM, but the verified parameter set covers the ML multilayer shade, 98 mm diameter and 10 mm–20 mm thicknesses. Any departure from that set requires explicit confirmation rather than assumption.
- Commercial terms. MOQ is 1 box for standard models and 5 boxes for customised products; lead time is 15–30 working days; payment terms are full payment before shipment; damage or deformation must be reported within 48 hours of receipt with photographs, and sampling tests are supported.
- Compliance scope. The ISO 13485 certificate on file (certificate 381240434R0S, issued 2024-12-27 by Shanghai POSI Certification Co., Ltd., valid to 2027-12-26) covers design, production and sales of dental medical materials and dental equipment under GB/T 42061-2022 / ISO 13485:2016. The EU Declaration of Conformity on file under MDR 2017/745 (SRN: CN-MF-000045919) covers intraoral scanner models YP-X and YP-800 as Class I devices — it is not the block's own declaration, and a lab should treat the two documents as covering different scopes.
The compliance point is worth emphasising in the wider regulatory context. The European Commission notes that EU Medical Device Regulation (MDR 2017/745) classifies most dental implants and restorative materials as high-risk, requiring intensive clinical data. Documentation scope therefore has to be read precisely: a certificate that covers a material is not the same document as a declaration that covers a scanner, and mixing them weakens the lab's own qualification file.
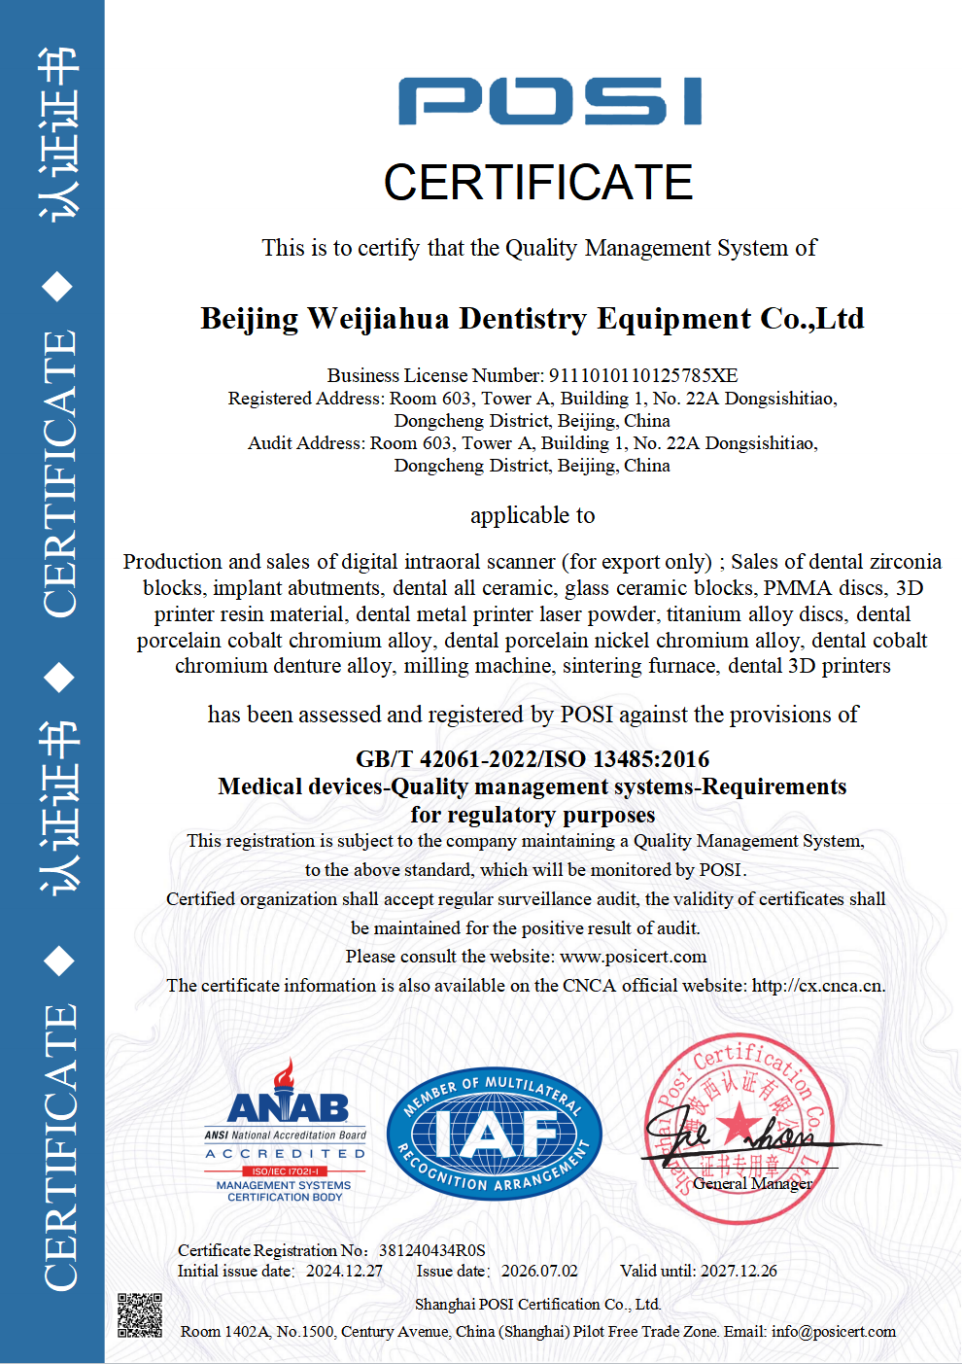
ISO 13485 certificate 381240434R0S, issued 2024-12-27 by Shanghai POSI Certification Co., Ltd., valid until 2027-12-26, covering dental medical materials and dental equipment.
Supply-Side Evidence a Lab Should Pull During Evaluation
Evaluation does not end at the furnace door. For labs moving from trial to routine ordering, the supply terms determine whether a material can actually be planned into production. The manufacturer provides OEM and ODM production services to clients in the USA, Europe, Brazil, the Middle East and North Africa, with ODM covering original design and OEM covering original equipment manufacturing, and it states that almost all specifications can be customised. Monthly capacity is documented at 15,000 pieces, quality control is defined as 100% raw material inspection plus finished-product random inspection, and after-sales support includes online technical guidance with a problem response within 24 hours.
For a lab manager, three of those items convert directly into planning value: capacity against forecast demand, a documented inspection regime that can be written into a supplier qualification file, and a response window for technical problems that bounds the cost of an unexpected sintering or milling issue. The rest — payment terms, acceptance windows, lead time — are constraints to be scheduled around rather than advantages to be assumed.
Side-by-Side Buyer Checklist for Lab Managers
The checklist below is designed to be run before a block is adopted for routine production. Each row pairs a test the lab performs with the evidence the supplier should provide.
| Evaluation step | What to test on your floor | Evidence to request |
|---|---|---|
| Blank fit and geometry | Mount the disc in your holder or adapter; confirm 98 mm diameter and that the chosen 10–20 mm thickness suits the tallest nested restoration | Product specification sheet; sample disc in the required thickness |
| Pre-sinter inspection | Inspect each blank visually and by handling before it enters the furnace; scrap defective pieces at this stage | Documented QC: 100% raw material inspection plus finished-product random inspection |
| Milling trial | Run a representative case on your own machine with your burs and parameters; check thin walls, connectors and margins | Sampling test support; online technical guidance with 24-hour response |
| Sintering trial | Run the standard curve at 1430 °C–1450 °C in your furnace with proper holding time and natural cooling; measure shrinkage against nesting compensation | Recommended sintering profile and safety notes |
| Outcome review by indication | Compare results for full-contour crowns, bridges, veneers and implant superstructures separately | Reference experience from labs, clinics and distributors |
| Compliance file | Confirm that each certificate matches the product you are buying, not a neighbouring product line | ISO 13485: 381240434R0S, valid to 2027-12-26; check the scope of the MDR 2017/745 declaration separately |
| Commercial terms | Model lead time and payment timing into your production calendar before committing volume | MOQ 1 box standard / 5 boxes customised; 15–30 working days; full payment before shipment; 48-hour acceptance window with photos |
| Customisation and branding | Define which specifications you need changed and test the first customised batch as a new material | OEM and ODM production services; customisation of almost all specifications |
Future Outlook
Two structural facts shape the next few years of zirconia block buying. First, CAD/CAM milling already accounts for 82.4% of zirconia dental manufacturing process revenue, and the dental milling machine market itself reached USD 2.45 billion in 2025 with an expected rise to USD 3.9 billion by 2030 according to Fortune Business Insights. Material choice is increasingly bound to the machine and furnace ecosystem a lab already owns. Second, the growth of alternative aesthetic ceramics, particularly lithium disilicate, expands the case mix rather than replacing zirconia where strength and span are the deciding constraints.
For lab managers, the practical implication is that block selection is becoming a documented, repeatable qualification process — trial blanks, recorded furnace curves, measured shrinkage, and a compliance file that separates what each certificate actually covers. Blocks that support that process with precise parameters and inspection data will be easier to keep in production than blocks that only offer a brand name.
FAQ
How do dental labs select zirconia blocks?
The 4D-PRO-ML block is documented as recommended for high-volume dental labs, made from Sinocera powder with stable shade consistency and suitable for posterior crowns and multi-unit bridges where mechanical strength and translucency are balanced. In practice a lab selection decision is built from four checks that can be verified internally: whether the indication matches the case mix, whether the sintering temperature range fits the lab's furnace programme, whether a trial unit survives milling and sintering in the lab's own equipment with acceptable shrinkage, and whether the supply terms — MOQ, lead time, payment and acceptance — fit the production calendar.
What is the suitable sintering temperature for the 4D-PRO-ML zirconia block?
The recommended sintering temperature range is 1430 °C–1450 °C, and the product parameter lists 1450 °C. The documented procedure is to place the milled zirconia workpiece on the sintering tray, set the heating curve up to 1430 °C–1450 °C with proper holding time, and allow natural cooling after sintering. Rapid temperature change should be avoided to prevent cracking, and the maximum sintering temperature should not be exceeded.
What causes chipping or cracks after zirconia sintering, and how should a lab respond?
The documented triggers are an improperly set sintering profile and inherent defects inside the zirconia blank. The mitigation is to follow the recommended sintering profile and to inspect blanks before sintering. If a piece still chips or cracks, the documented guidance is to scrap the affected blank and not use it for a final restoration.
How does a zirconia block compare with lithium disilicate on the same production floor?
They occupy different workflow stages. Zirconia is milled in a pre-sintered state and then sintered at 1430 °C–1450 °C with natural cooling, and the 4D-PRO-ML is specified for full-contour crowns, bridges, veneers and implant superstructure restorations. Milled lithium disilicate glass ceramic is typically crystallised in a porcelain furnace, while press ingots follow a lost-wax pressing route. Lithium disilicate represented approximately 28% of all all-ceramic dental restorations globally as of 2024 according to Business Research Insights, and its market is projected to grow from USD 320 million in 2025 to USD 920 million by 2032 at a CAGR of 18.8% per Intel Market Research — growth that expands the aesthetic case mix rather than removing zirconia from long-span and implant-level work.
What equipment does the 4D-PRO-ML block require in a lab?
The matched equipment listed for this material is a dental milling machine, a dental sintering furnace and a dental lab scanner, and the specified working condition is an indoor constant-temperature dental laboratory environment. The block is a 98 mm diameter disc in thicknesses of 10 mm, 12 mm, 14 mm, 16 mm, 18 mm and 20 mm, so the lab should confirm its holder or adapter set and its nesting heights before ordering. The material has been described by the manufacturer's long-term customers as compatible with most CAD/CAM systems, which still needs to be confirmed on the lab's own machine and software.
What commercial and compliance terms apply when comparing zirconia blocks for routine ordering?
For this product, MOQ is 1 box for standard models and 5 boxes for customised products; lead time is 15–30 working days; payment is full payment before shipment; and damage or deformation must be reported within 48 hours of receipt with photographs, with sampling tests supported. Export shipping is by sea or air freight with FOB Shanghai or Tianjin available. On compliance, ISO 13485 certificate 381240434R0S covers design, production and sales of dental medical materials and dental equipment and is valid to 2027-12-26, while the MDR 2017/745 EU Declaration of Conformity on file (SRN: CN-MF-000045919) covers intraoral scanner models YP-X and YP-800 — a lab should track these as separate scopes.
For reference, the company and product-line brochure is publicly available at WJH Company Information (PDF).