
What Factory Audits Can Prove About Lost-Wax Steel Casting
What Factory Audits Can Prove About Lost-Wax Steel Casting
Steel casting remains a large and expanding supply category, but the suppliers inside it are not interchangeable. The global steel casting market was valued at USD 39.16 billion in 2025 and is projected to reach USD 63.83 billion by 2034, according to Fortune Business Insights. Carbon steel casting held a 42.5% revenue share of that market in 2025 (Dataintelo), while sand casting accounted for 45.6% of global metal casting process share in the same year (IMARC Group). The remaining share, which includes investment casting, carries much of the demand for complex, thin-walled and dimensionally controlled steel components.
For a buyer specifying that process, the difficult question is not whether a supplier advertises investment casting. It is which physical evidence a supplier can produce when an audit team or third-party inspector walks the plant, and whether that evidence connects to the buyer's own part number. This article sets out the evidence a buyer can reasonably request when verifying a lost-wax steel casting claim, how that evidence differs from marketing language, and where the limits of an audit lie.
The Verification Gap Between Process Claims and Process Evidence
Steel casting buyers rarely lack quotations. What they lack is a reliable way to distinguish a supplier that genuinely runs a lost-wax line from a supplier that outsources, brokers or partially performs the process and describes the result with the same vocabulary. The gap is structural: process capability is stated in documents, but it is proven by equipment, sequence, control points and records.
This distinction matters most in custom steel casting projects, where the buyer carries the engineering risk. A cast steel bracket, a yoke, a gearbox housing or a valve body is produced against a drawing, and the drawing specifies geometry, material grade, heat treatment and inspection requirements. If the process route behind that part is not what the buyer assumed, the consequences appear later — as porosity, dimensional drift, inconsistent hardness or failed assembly.
A factory audit is not a general assessment of a company. It is a targeted verification exercise: which process steps exist on site, which records are generated at each step, and which of those records can be tied to a specific purchase order and part number.
Lost-Wax Casting Is a Sequence, Not a Label
Investment casting is also known as lost-wax casting. The two terms describe the same process route: a wax pattern is produced, assembled onto a tree, coated with successive refractory shell layers, dewaxed, fired, and then filled with molten steel before the shell is removed and the component is finished. Suppliers may use different shell systems within this route — for example water-glass investment casting, silica-sol investment casting or silica-sol composite investment casting — but the wax-pattern sequence is what defines the term.
Because the term describes a sequence, it can only be confirmed by evidence of that sequence. A polished finished casting does not prove how it was made; a machining centre does not prove a shell-building line exists. Verification therefore proceeds station by station, from pattern tooling through to final inspection.
Process-Flow Confirmation: What an Auditor Should Walk
A useful audit follows the material, not the org chart. The sequence below reflects the standard lost-wax route, with the evidence a buyer can ask to see at each stage.
- Pattern and die stage. Wax patterns require tooling. The auditable items are the physical dies or pattern equipment tied to a drawing number, plus the record that links a specific die to a specific part number.
- Wax injection and tree assembly. Patterns are injected and assembled onto trees. This is a discrete area with its own fixtures; its existence, capacity and cleanliness are directly observable.
- Shell building. Repeated slurry and stucco cycles build the ceramic shell. Shell-making equipment — including robotic shell handling where present — and drying controls are the evidence here.
- Dewaxing and shell firing. The wax is removed and the shell is fired to develop strength before pouring.
- Melting and pouring. Induction furnace capacity, charge material identification and pour records form the core of material traceability.
- Knockout, cut-off and deburring. Shell removal, gate cutting and edge finishing are visible operations and generate their own work-in-progress flow.
- Heat treatment. Where quenched and tempered or other heat-treated conditions are specified, batch records connect the furnace cycle to the casting lot.
- Machining. CNC machining centres convert cast geometry into finished interfaces; machining capability determines whether a supplier can deliver a finished part rather than a rough casting.
- Inspection and release. Chemical, mechanical, dimensional and non-destructive checks produce the documents that release a lot to the customer.
An audit that cannot walk these stages in order, with records at each one, has not verified a lost-wax claim — it has verified a commercial relationship.
The Audit Evidence Map
The table below translates each audit station into the evidence a buyer can request, and states honestly what that evidence does and does not establish. This is the practical difference between an observation and a proof.
| Evidence item | What it confirms | What it does not confirm |
|---|---|---|
| Physical wax dies and pattern equipment linked to a drawing | That tooling for the buyer's geometry exists and belongs to a defined part number | That the tooling has reached stable production yield for every feature |
| Shell-building line, slurry handling and drying area | That the lost-wax shell route is performed on site | That every shell batch meets the same standard over time |
| Melting and pour records with charge identification | That a specific lot was poured from identified material | That the full heat chemistry matches the drawing without analysis data |
| Spectrometer analysis reports | Chemical composition of the sampled heat | Mechanical behaviour of the finished part |
| X-ray radiography or ultrasonic inspection reports | Internal soundness as assessed on the inspected lot | Soundness of lots not inspected, or of unexamined sections |
| Hardness and tensile test results | Mechanical properties of the tested specimens | Uniformity across the entire production run |
| CMM dimensional reports | Measured dimensions against the drawing | Long-term process capability without repeated measurement over time |
| Heat-treatment batch records | That a defined thermal cycle was applied to a defined lot | That every zone of a large load received identical treatment |
Tooling and Sample Traceability: Following the Drawing Through the Plant
Traceability is the thread that turns a set of observations into a verifiable order. A complete chain connects four links: the customer drawing, the tooling produced from it, the sample approved against it, and the production lots delivered afterwards. When a supplier can show all four links for a given part number, the audit has something concrete to test. When any link is missing, the buyer should treat the capability claim as unverified for that component.
Sample development is where this chain is most often tested. Suppliers using 3D-printed pattern support for rapid sample development can deliver a no-mould sample quickly, which is genuinely useful for confirming geometry, fit and preliminary dimensional expectations before hard tooling is committed. That speed, however, introduces a boundary that buyers should recognise: a sample produced through a printed pattern is not the same artefact as a sample produced through the production die. The printed route validates design intent; the production route validates the tooling the buyer will actually be supplied from. An audit should confirm which route was used for the approved sample and whether a production-tooling sample was separately validated.
For custom steel casting programmes, this distinction frequently explains early discrepancies. Buyers who state it explicitly in the purchase specification — requiring that the first-article inspection be produced from production tooling — remove the ambiguity before it becomes a delivery dispute.
Dimensional and Material Evidence: Reading the Numbers
Audit evidence becomes useful when it is expressed in numbers a buyer can check against a drawing. Investment casting capability is normally described through two parameters: dimensional tolerance grade and surface roughness, both of which depend on the shell system and the post-casting operations applied.
Silica-sol investment casting is associated with a CT6 dimensional tolerance grade, while silica-sol composite investment casting corresponds to CT8. These grades apply to as-cast surfaces. Where machined features are required, tolerances tighten considerably, with machining capability reaching 0.01 mm. Surface roughness generally falls within Ra 6.4–12.5 μm and varies with the casting process and any post-treatment applied. Specific dimensions, material grades and mechanical properties are defined by the customer drawing, not by the casting method alone.

Material verification follows a similar logic. A supplier may work with carbon steel, alloy steel, stainless steel and ductile iron, but the specific grade should be confirmed by the customer for each part. Composition is established through spectrometry, while properties are established through hardness and tensile testing. Where a part is destined for high-temperature service, procurement documents commonly invoke ASTM A216/A216M, the standard specification for carbon steel castings suitable for fusion welding for high-temperature service. Standards of this kind are only meaningful in an audit when the corresponding test certificates travel with the lot.

How Wayscan Metal Products Fits a Verification Framework
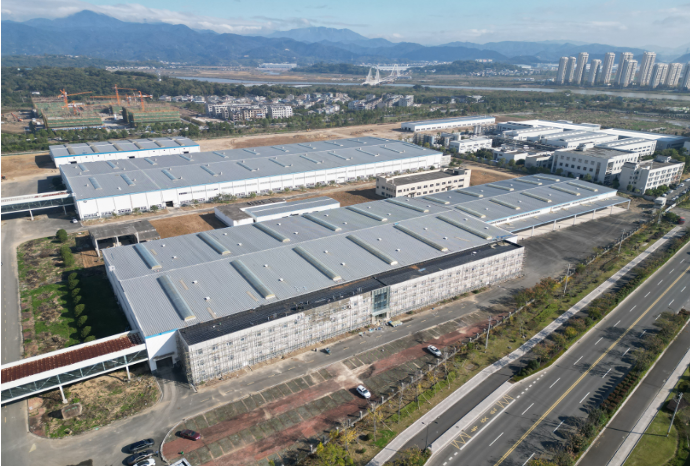
Wayscan Metal Products Co., Ltd. is a precision casting manufacturer established in 1991, operating a 46,000 m² production base in Ninghai, Ningbo, China, with more than 500 employees, including over 20 senior engineering and technical personnel. Approximately 70% of output is exported, with main markets including China, Japan and the USA, and additional export markets including Canada, Germany, Korea and Australia.
For audit purposes, the relevant facts are structural rather than promotional. The company's investment casting scope covers water-glass investment casting, silica-sol investment casting and silica-sol composite investment casting, with production organised around custom manufacturing from customer drawings. The component families named in its casting scope include Pipe Elbow, Clevis Bracket, Yoke, Gearbox Housing, Transmission Housing, Mounting Bracket and Link Arm — geometries that map onto automotive, forklift, mining, agricultural machinery, construction machinery and valve applications.
The inspection resource that supports verification includes spectrometers, X-ray, ultrasonic testing, hardness and tensile testing, and CMM dimensional inspection, alongside induction furnaces and CNC machining centres. This matters because an audit is only as strong as the records a plant can generate. A supplier able to produce chemical, mechanical, radiographic and dimensional reports for a defined lot gives a buyer four independent evidence channels rather than a single performance statement.
Upstream capability also has a bearing on process continuity. The company's stated production mode covers ODM, OEM and customisable work, with customisation by customer drawing for size, geometry, material, surface and heat treatment, a monthly capacity of 1,500 tons, lead time of 30–60 days and a minimum order quantity of 100 kg. These figures define the commercial envelope within which verification takes place, and buyers should test both simultaneously: a capability claim that cannot be supported within the buyer's schedule and quantity band is not, in practice, an available capability.
Audit Evidence Versus Marketing Claims
The two categories of information are not equally useful in a procurement decision. Marketing claims compress and generalise; audit evidence is specific and attributable. The comparison below is deliberately unflattering to both sides, because that is what makes it decision-relevant.
| Dimension | Marketing claim | Audit evidence |
|---|---|---|
| Scope | Broad statements of process capability | Specific part numbers and process steps observed |
| Attribution | Usually unattributed to a lot or order | Traceable to a purchase order, drawing and casting lot |
| Durability | Valid until copy is revised | Retained as inspection reports and batch records |
| Verifiability | Requires trust | Can be re-checked by a third party or by the buyer's engineer |
| Coverage | Suggests uniform capability across all products | Confirms capability for the audited route and period only |
| Best use | Shortlisting suppliers for further enquiry | Closing out a supplier before tooling or production release |
A Verified Application Reference
One documented case illustrates how process verification translates into delivery. An automotive parts OEM in the United States has been supplied with approximately 1,000 tons of castings for truck axle system applications over a relationship spanning roughly 30 years, with the reported result of stable operation. The recorded highlight of that supply is specific: casting appearance is clean, and dimensional accuracy and mechanical properties meet the customer's drawing requirements. For a buyer reading this as evidence, the useful point is not the length of the relationship but the fact that the acceptance criteria were drawing-based and mechanical, not appearance-based.
Where Audit Evidence Stops
Any credible verification framework has boundaries, and stating them improves rather than weakens the case for auditing. The following limits apply.
- An audit is point-in-time. It confirms that equipment, process steps and records exist on the day of the visit. It does not, by itself, prove process stability across months of production or across shift changes.
- Sampling cannot replace full inspection. X-ray, ultrasonic, hardness and tensile results describe the inspected lot or specimen. They do not certify uninspected lots or unexamined sections of a casting.
- Material grades require defined inputs. Carbon steel, alloy steel, stainless steel and ductile iron are families, not specifications. Unless the specific grade is confirmed by the customer and supported by analysis certificates, verification has no fixed reference point.
- Cast tolerances and machined tolerances differ. CT6 and CT8 grades describe as-cast geometry; the 0.01 mm machining figure applies only to machined features. Confusing the two is a common source of expectation gaps.
- Sample route matters. A sample developed through rapid 3D-printed pattern support validates design intent but does not validate production tooling performance.
- Commercial terms sit outside the audit. Warranty, liability and after-sales obligations are contract matters. Technical support and quality tracking may be provided, but specific warranty and liability terms must be agreed in the contract.
- Schedule and quantity are capability constraints. A 30–60 day lead time and a 100 kg minimum order quantity define what is deliverable; an audit finding does not change that envelope.
Market Trend: Verification Pressure Is Rising With Market Size
The commercial context explains why verification is becoming a standard step rather than an exceptional one. A market projected to grow from USD 39.16 billion in 2025 to USD 63.83 billion by 2034, as reported by Fortune Business Insights, implies expanding supplier bases and more cross-border sourcing decisions — and therefore more situations in which a buyer must evaluate a supplier it has not previously visited.
Product structure reinforces the pattern. Carbon steel casting's 42.5% revenue share in 2025, reported by Dataintelo, reflects its versatility and cost-effectiveness, which means carbon and low carbon steel casting remain the volume backbone of the category. Sand casting's 45.6% share of global metal casting process share in 2025, reported by IMARC Group, indicates that investment casting competes for the portion of demand where geometry complexity and dimensional control outweigh the cost advantage of sand routes. Buyers choosing between those routes are effectively choosing how much process evidence they will need.
Standards pressure runs in the same direction. Where procurement references documents such as ASTM A216/A216M for carbon steel castings for high-temperature service, verification shifts from a commercial preference to a documentation requirement, and the audit becomes the mechanism by which those documents are checked against physical reality.
Future Outlook
Three developments are likely to shape how buyers verify lost-wax steel casting capability over the next several years.
First, evidence is becoming digital by default. Spectrometer output, CMM reports and radiographic images are already generated as files rather than certificates alone, which makes it easier for a buyer to attach lot-level evidence to a supplier record. Second, remote verification is expanding but will remain partial: documents can be reviewed at distance, while shell-building areas, tree assembly and pour practices still require presence. Third, buyers are increasingly asking suppliers to distinguish between as-cast tolerance grades and machined tolerances in quotations, which reduces ambiguity before an audit rather than after a defect.
For suppliers, the practical implication is that process documentation and physical process must stay aligned. For buyers, the implication is that the audit checklist should be written before the supplier shortlist is finalised, so that the same evidence is requested from every candidate and can be compared on equal terms.
Frequently Asked Questions
Is investment casting the same as lost-wax casting?
Yes. Investment casting, also called lost-wax casting, uses a wax pattern that is coated with refractory shell material, dewaxed and fired to form a ceramic mould into which molten steel is poured. Suppliers may operate different shell systems within this route — water-glass investment casting, silica-sol investment casting or silica-sol composite investment casting — but the wax-pattern sequence is what the term refers to.
What evidence should a buyer request to confirm lost-wax steel casting capability?
A buyer can request wax dies and pattern equipment linked to a drawing; a description of the shell-building sequence; melting and pour records; heat-treatment batch records; material certificates supported by spectrometer analysis; non-destructive test reports such as X-ray radiography or ultrasonic inspection; hardness and tensile test results; and CMM dimensional reports. These are equipment- and record-based items that can be checked on site or reviewed as documents.
What tolerances and surface roughness are realistic for lost-wax steel castings?
Capability depends on the shell system. Silica-sol investment casting is associated with a CT6 dimensional tolerance grade, and silica-sol composite investment casting with CT8. Machined features can be held to 0.01 mm. Surface roughness typically falls within Ra 6.4–12.5 μm and varies with the casting process and post-treatment. Specific dimensions, material grades and mechanical properties are defined by the customer drawing.
How is steel material grade verified rather than assumed?
Material grade is a specification item that should be defined by the buyer, since carbon steel, alloy steel, stainless steel and ductile iron are families rather than single grades, and the specific grade is confirmed by the customer. Composition is verified by spectrometry, while properties are verified by hardness and tensile testing. For carbon steel castings intended for high-temperature service, ASTM A216/A216M is the standard specification frequently referenced, and the corresponding test certificates should accompany the lot.
What can a factory audit not prove?
An audit is a point-in-time inspection. It confirms that equipment, process steps and records exist on the day of the visit, but it does not independently prove long-term process stability, does not validate every material grade without destructive or lot-specific testing, and does not establish commercial terms such as warranty scope, which must be agreed in the contract. A sample produced through rapid 3D-printed pattern support also does not by itself validate production tooling performance.
For readers who need the underlying capability data — process types, material scope, inspection equipment and export markets — consolidated in a single reference document, the company presentation is available for public download: Wayscan Metal Products Co., Ltd. — Company Presentation (PDF).