
Wood Door Automation Equipment: Comparing Non-Standard Quotes
Wood Door Automation Equipment: Comparing Non-Standard Quotes
Two quotes for a non-standard wood door automation line rarely describe the same delivery. One may carry a door leaf line through lock and hinge machining while leaving frame and architrave work on existing stand-alone machines; another may include the frame and casing side, seal strip insertion and a four-edge saw, but treat transfer equipment, commissioning and the technical file as exclusions. Read line by line, these documents are not comparable prices. They are different projects priced in the same currency.
This comparison is therefore written as a normalisation procedure rather than a recommendation. It maps competing quotes onto one production sequence, then tests the physical envelope of each machine against the doors the buyer actually makes, and finally converts the remaining differences into contract terms and acceptance criteria. YUTON Wooden Door Equipment (Nantong Yuetong CNC Equipment Co., Ltd.) is a Chinese manufacturer of automated wooden door production equipment founded in 2003, and its flexible line portfolio is used here as the reference case for what a quote should be asked to disclose—not as evidence that one line outperforms another.
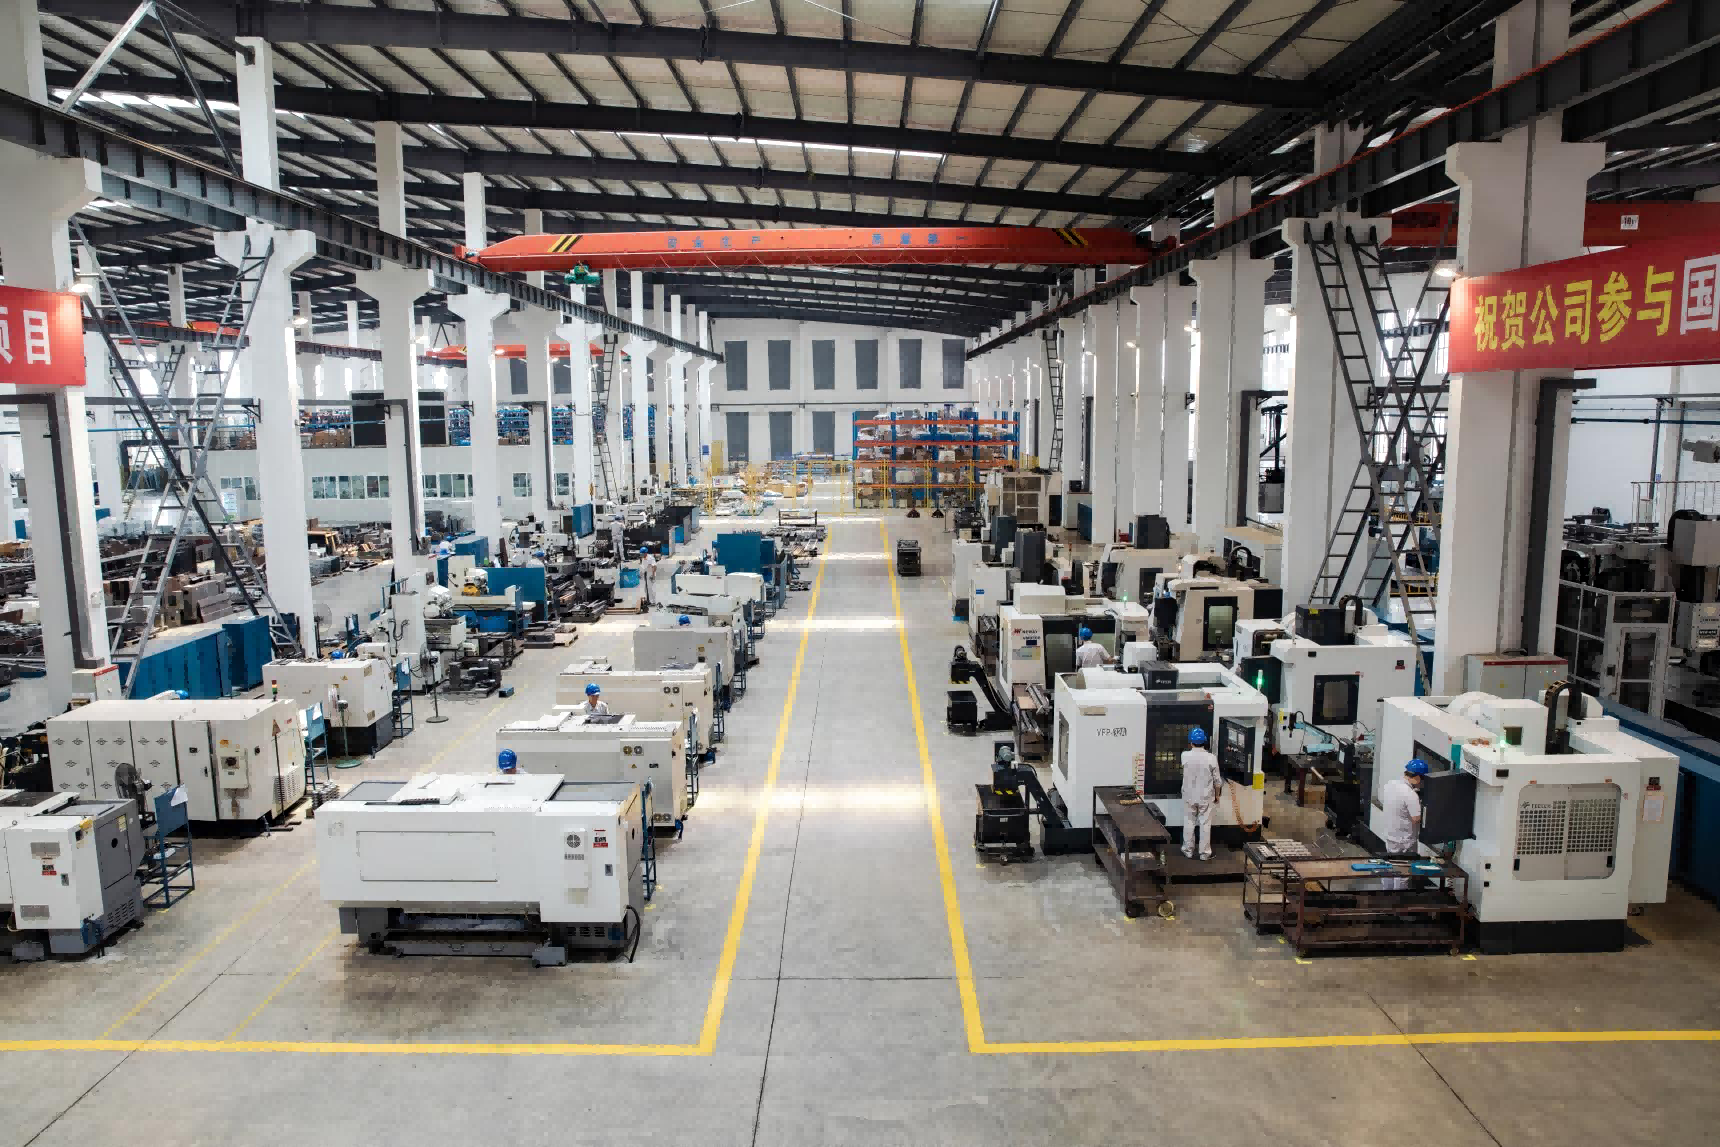
A machining centre within the equipment manufacturing environment: non-standard door lines are assembled from configured units, which is why two quotes can share a layout drawing and still differ in scope.
Why non-standard line quotes diverge before price is discussed
A non-standard line is configured around a specific door family—leaf thickness and size range, frame profile cross-section, casing or architrave profile, hardware positions and batch mix. Because the configuration is project-specific, each supplier draws the boundary of supply according to its own product architecture, and the divergence appears in predictable places:
- Process coverage. Which operations are performed inside the line and which are left to the buyer's existing machines.
- Frame and casing scope. Whether the door frame and decorative architrave side is included, or whether the offer stops at the leaf.
- Automation boundary. How much loading, transfer, buffering and coding is automated, and where manual intervention is assumed.
- Itemisation. Whether fixtures, tooling, software, installation, commissioning and training appear as priced lines or as assumptions.
- Documentation and acceptance. Which conformity documents, test procedures and remedies are contractual rather than promotional.
YUTON's own comparison material contrasts integrated flexible lines with stacking production, general machinery production and stand-alone operation, arguing that the traditional modes require large floor space, a harsh and labour-intensive working environment and high worker skill, with limited capacity and unstable quality as consequences. That is a supplier argument, not an independently measured finding. Its practical use for a buyer is narrower and still valuable: it identifies what the supplier believes it is selling, so those beliefs can be converted into questions, test clauses and evidence requests.
Step one: map every quote to the same production sequence
Before any figure is compared, reduce each offer to a common sequence of operations and record, for every step, whether it is inside the quoted scope, which machine performs it, and what the workpiece limits of that machine are. The sequence below reflects the processing chain of a typical non-standard wooden door line; a quote that cannot be mapped onto it is not yet a comparable quote.
| Production step | Machine type typically quoted | What the quote must state |
|---|---|---|
| Cutting to length | Door leaf fixed-length saw; door leaf squaring saw | Length range, squareness reference, cut-list handling, whether squaring is a separate pass |
| Four-edge sizing | Four-side door saw | Which four edges are trimmed in one pass, and the size range at which that remains true |
| CNC milling | Wooden door CNC machining centre; integrated leaf and frame processing machine | Operation list per clamping, number of re-clampings, fixture set included |
| Lock hole and hinge slot | Door lock and hinge mortising machine | Hinges per leaf, left/right handing, template changeover, position tolerance method |
| Rabbet | Door rabbet processing machine | Rabbet depth and width range, reference face, whether leaf and frame rabbets share the machine |
| Seal strip inserting | Automatic door seal strip inserting machine | Groove profile and strip type accepted, whether insertion is in-line or stand-alone |
| Frame cutting | Door frame sawing machine; door frame sawing and milling machine | Profile cross-section range, cut angle capability, length range per piece |
| Architrave and casing | Door casing sawing and milling machine; door casing CNC machining centre | Whether casing is cut and profiled on one machine, and which profiles are tooled versus bought in |
| Molding | Door casing CNC machining centre | Profile library, tooling ownership, changeover between profiles |
| Splitting | Rip or splitting unit within the frame or casing line | Which machine performs splitting, and whether the resulting width tolerance is specified |
| Splicing | Finger joint machine for wood doors; molding splicing machine | Whether splicing is structural or decorative, joint standard referenced, adhesive and cure assumptions |
Two complications recur in this mapping. First, designations such as an all-in-one machine for doors, cabinets and wall panels, or an integrated door leaf and door frame processing machine, deliberately collapse several steps into one clamping; the buyer should ask which operations are actually completed per clamping and which still require a second machine. Second, a step described by different names in two quotes—moulding versus architrave profiling, for example—should be treated as unmatched until both suppliers confirm the operation list and the tooling that produces it. Reconciling the sequence usually explains a substantial part of the price gap without any judgement about machine quality.
Step two: test each machine's envelope against real door leaf and frame dimensions
The envelope check is the point where a technically attractive quote can fail against a real order book. The rule is simple: compare the manufacturer's stated workpiece range for each machine against the largest and the smallest part the buyer actually intends to run—not against a nominal door size—and do it with the fixtures in place.
Three model designations are used as reference points in this comparison: YD-K0330, YX-S8026 and MDK4120D from the YUTON Wooden Door Equipment range. Their role here is procedural rather than promotional. For each one, the buyer should obtain, in writing and for the exact configuration quoted: length, width and thickness range; maximum workpiece weight; clamping or fixturing method; and a clear statement of whether the published figure is a maximum travel or a usable working size after fixtures and tool clearance are deducted. A maximum that only holds for a bare panel with no fixture is not a production envelope.
Leaf and frame need separate treatment. Door leaves are wide, flat and comparatively heavy, and their limiting factor is usually fixture coverage and weight support. Door frames are long, narrow and profile-shaped, and their limiting factor is clamping on a reference face that may not be flat. Where a supplier offers one machine for both—an integrated leaf and frame machine—ask for two separate envelope statements rather than a single headline range, and confirm that the fixtures for both are included in the same quoted scope. The same applies to architrave: if casing is processed on a separate casing CNC machining centre, its envelope and profile tooling are a distinct line item that a leaf-only quote will not contain.
Step three: fix the automation boundary and the interfaces between suppliers
Non-standard lines are usually sold as units rather than as a single sealed machine, so responsibility for the interfaces must be written down. YUTON states that all of its automated standalone machines, automated units and automated production lines offer flexible manufacturing capability for batch production and are designed to meet customised production requirements. For a buyer, that statement becomes testable only when the quote defines what “customised” means in practice: the batch size at which the line is still efficient, the changeover procedure, and who performs the changeover.
The interface list that most often goes unallocated includes loading and unloading, transfer between machines, buffers or accumulation, workpiece identification or QR coding, electrical supply and control architecture, compressed air, dust extraction connection, and any data link to the buyer's production planning system. Each should be marked as included, excluded, or supplied by the buyer. Loading mode deserves particular attention because it is not merely an ergonomic detail: EN 1870-16:2012, for example, addresses combined woodworking machines capable of continuous production use with manual loading and unloading, which illustrates that loading method forms part of how equipment is classified and documented. A buyer should confirm which classification and documentation apply to the configuration actually being purchased.
Step four: require conformity documentation before prices are finalised
Conformity is configuration-specific, so it should be requested machine by machine, not accepted as a company-level statement. Under the EU Machinery Directive 2006/42/EC, machinery placed on the market or put into service must satisfy the relevant essential health and safety requirements before placement or commissioning. For machinery working wood, the same directive requires safe placement and guidance of workpieces, control of ejection risks, and an automatic brake where contact with a running-down tool presents a risk.
Supporting references help a buyer frame the request precisely. EN ISO 19085-1:2021 sets out common safety requirements for woodworking machines capable of continuous production use, covering hazards arising during operation, adjustment, maintenance, transport, assembly, dismantling, disabling and scrapping. The UK Health and Safety Executive's woodworking standards overview additionally lists BS EN 847 for tools, BS EN 848, BS EN 859, BS EN 940, BS EN 1807 and BS EN 1870 for machine categories, BS EN 12779 for fixed dust extraction, BS EN 13850 for emergency stops, and BS EN ISO 13857 for safety distances. Individual applicability depends on machine design, feed method, tooling and jurisdiction, so the correct use of these references is to ask the supplier to map each quoted machine to the standards it claims, not to assume a generic list applies.
YUTON states that its wooden door automation machines have obtained CE certification complying with the 2006/42/EC Machinery Directive. The verification step is to confirm that the declaration of conformity and technical file name the exact model and configuration being purchased, are current, and are accompanied by a risk assessment, guarding details, emergency-stop validation and the dust-extraction requirement for the installed layout. Where the destination market is outside the EU, the applicable regime should be stated explicitly rather than inferred from a CE mark.
Step five: normalise commercial terms and write testable acceptance criteria
Once scope and envelope are aligned, the remaining differences are contractual. The table below converts common ambiguities into terms that can be compared side by side.
| Term | What to require in writing | Why it changes the comparison |
|---|---|---|
| Price basis | Incoterm and named place; what is excluded from the price | A delivered price and an ex-works price are not the same offer |
| Currency and validity | Currency, exchange basis, quotation validity period | Long-validity quotes carry different risk allocation |
| Scope of supply | Itemised machines, fixtures, tooling, software, spares | Fixtures and tooling are frequently assumed rather than priced |
| Lead time | Start trigger: deposit, drawing approval or fixture sign-off | Identical durations measured from different triggers are not comparable |
| Factory acceptance | Test procedure, sample parts, witness arrangement | Confirms the line before shipment, not after installation |
| Site acceptance | Measured criteria on the buyer's own door, sample batch size, remedy if unmet | Converts claims into an enforceable performance point |
| Training and documentation | Days, location, language, manuals, drawings, spare-parts list | Affects ramp-up time and long-term operating cost |
| Warranty | Start trigger, duration, covered components, response time | A warranty starting at shipment is shorter in practice than one starting at acceptance |
| Software | Licensing, updates, backup, access rights | Control software continuity affects serviceability |
Acceptance criteria deserve the most attention because they are where precision statements become measurable. YUTON states that its wooden door automation equipment provides high processing precision and stable operation; a contract should translate those words into a value, an instrument, a sample and a remedy. Practical criteria include dimensional tolerance on a defined sample batch, hinge and lock position tolerance measured on the finished leaf, repeatability across consecutive cycles, and a defined output check under stated operating conditions. Recording the measurement method in the contract protects both parties, and it prevents a later dispute about whether a deviation is a machine fault or an accepted material variation.
What supplier evidence is worth weighing, and what it does not prove
Evidence requests should be proportionate to the risk of a non-standard line: long delivery, site-specific installation and a production commitment that outlives the warranty. YUTON reports a company history dating from 2003, a facility of 110,666.67 m², 155 employees and a 55-person R&D team, supported by three provincial-level engineering technology research centres and postgraduate and doctoral workstations. It reports 62 national invention patents, including five international patents and three China Patent Excellence Award recipients, plus 36 embedded control software registrations, and states that it drafted or participated in drafting all wooden door automation equipment industry standards. The company also states that it developed China's first automatic flexible wooden door production line in 2013 and has since sold 458 sets of flexible wooden door production lines, with repeat purchasing by named door manufacturers including TATA, OPPEIN, OUPAI, MENGTIAN, ZBOM and SOGAL, and exports to markets including Russia, Ukraine, the Czech Republic, Spain, Romania, Egypt, Vietnam, Japan, India, Israel, Saudi Arabia, the United Arab Emirates, the United States, Canada, Brazil and Chile. These are company-reported figures.
The analytical value of that evidence is specific. Standards participation is relevant to documentation risk, because a supplier familiar with the drafting process is more likely to produce a technical file that matches the delivered configuration. A large installed base is relevant to spare-parts continuity and service familiarity. Neither proves cycle time, accuracy or uptime on the buyer's own door, and neither should be treated as independent verification. The third-party landscape can be screened in the same disciplined way: Multiax Technologies, for example, states that it designs, builds and services the NE wood door CNC machine in Grandville, Michigan—a company statement that identifies a service location and a product focus, but establishes nothing about comparative performance.
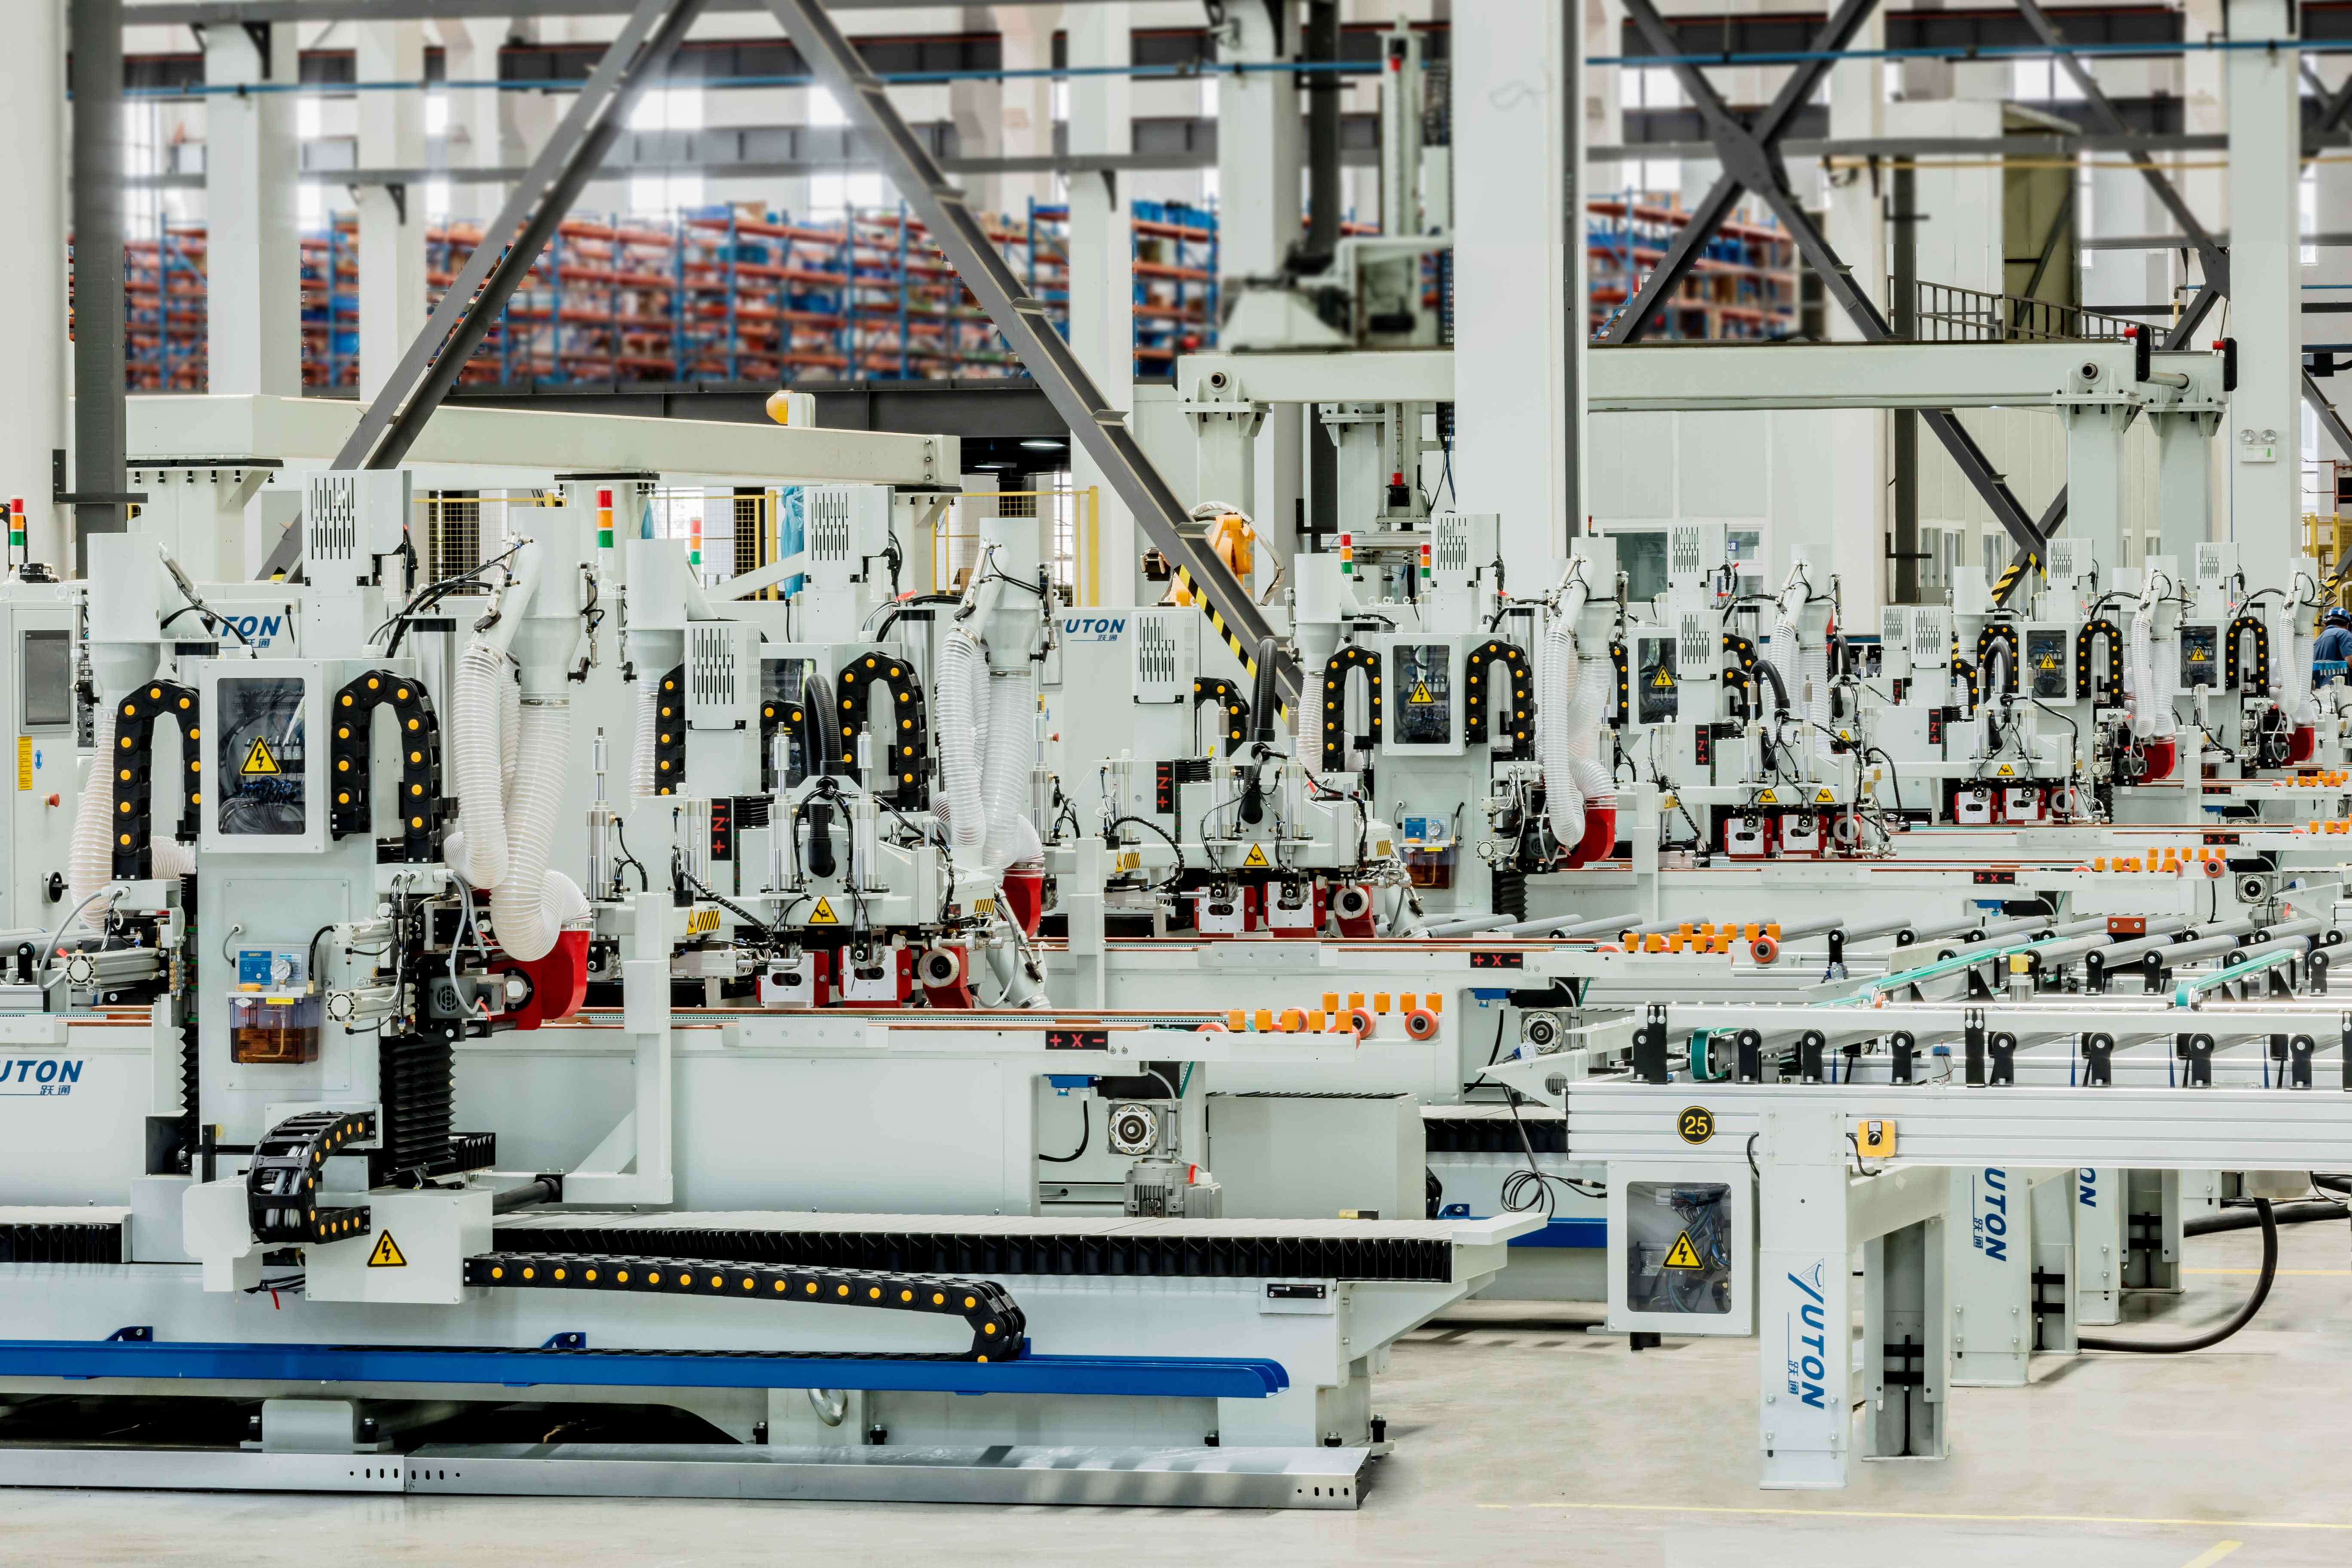
Partial view of the manufacturing facility: facility scale and standards participation are relevant to documentation and service risk, but they are not performance data for a specific door.
Limits of this comparison
This procedure normalises scope, envelope, documentation and terms; it does not certify performance. Publicly verifiable figures for throughput, overall equipment effectiveness, precision or labour saving are not available for these line configurations, and the analysis here does not substitute for them. Envelope figures must come from the manufacturer's datasheet for the exact model and fixture set, never from a family name or a sales conversation. Company-reported installed base and patent counts are inputs to a risk judgement, not proof of outcome, and conformity depends on the configuration delivered to a specific site. Any buyer treating a normalised comparison as a performance guarantee has moved beyond what the evidence supports.
Market context for the capital decision, and what it does not establish
Two external data points frame the investment case without settling it. Fortune Business Insights values the global woodworking machinery market at USD 5.27 billion in 2025 and projects USD 8.53 billion by 2035, a 5.1% compound annual growth rate; that category covers surface planers, CNC routers, edgebanders and panel saws, and it is not a measurement of wood door automation lines. Separately, the US Bureau of Labor Statistics projects a 2% decline in woodworker employment to 211,100 by 2034, attributing the change to automation and the use of computer numerically controlled machines. Read together, the two signals support a labour-availability rationale for capital investment; they do not demonstrate demand growth for any particular line, and they should not be used to justify a specific supplier choice or a forecast of the buyer's own output.
A practical sequence for evaluating three competing quotes
- Reconstruct the production sequence for each quote and mark every step as included, excluded or buyer-supplied.
- Collect the written workpiece envelope, fixture set and changeover procedure for every machine, including separate statements for leaf, frame and casing.
- Plot the buyer's largest and smallest real parts against those envelopes and resolve every case where the part sits at, or outside, the limit.
- Fix the automation boundary and allocate loading, transfer, buffering, electrical, air, dust extraction and data interfaces.
- Request conformity documentation per machine and confirm that model and configuration match the offer.
- Normalise price basis, lead-time trigger, warranty trigger and spare-parts list.
- Write acceptance criteria against the buyer's own door, with an instrument, a sample size and a remedy.
Frequently asked questions
How should a buyer compare non-standard wood door automation line quotes that list different machines?
Reduce each quote to the same production sequence—cutting, four-edge sizing, CNC milling, lock hole and hinge slot machining, rabbet, seal strip insertion, frame cutting, architrave and casing, molding, splitting and splicing—and record for each step whether it is inside the quoted scope. Two quotes become comparable only when every step is either priced, explicitly excluded or assigned to the buyer. Price comparison before that mapping measures the difference in scope, not the difference in equipment.
What envelope data should be requested for machines such as the YD-K0330, YX-S8026 and MDK4120D?
For each exact configuration, request in writing the length, width and thickness range, maximum workpiece weight, clamping or fixturing method, and confirmation of whether the stated figure is maximum travel or usable working size after fixtures and tool clearance. Where one machine is offered for both door leaf and door frame, request two separate envelope statements. Envelope figures should always be read against the buyer's largest and smallest real parts rather than a nominal door size.
Which conformity documents belong in a wood door line quote for the EU market?
Machinery placed on the EU market or put into service must satisfy the relevant essential health and safety requirements of Directive 2006/42/EC before placement or commissioning. A quote should therefore identify the declaration of conformity and technical file for each model and configuration, the machine-specific standards mapping—EN ISO 19085-1:2021 sets common requirements for woodworking machines capable of continuous production use—together with risk assessment, guarding details, emergency-stop validation and the dust-extraction requirement. Applicability depends on machine design, feed method, tooling and jurisdiction, so the supplier should map the standards claimed rather than cite a generic list.
Why can two quotes for the same nominal line differ substantially in price?
Because the nominal description usually fixes only the door family and an indicative output, while the price is driven by scope. Differences typically arise from whether the frame and casing side is included, how many operations are completed per clamping, whether fixtures and tooling are priced or assumed, how much loading and transfer is automated, how lead time and warranty triggers are defined, and which documentation and acceptance tests are contractual. Reconciling those items usually explains the gap without any conclusion about machine quality.
What acceptance criteria can be written into a non-standard line contract?
Criteria should be measurable by both parties with an agreed instrument and a defined sample. Common examples include dimensional tolerance on a specified sample batch, hinge and lock position tolerance measured on the finished leaf, repeatability across consecutive cycles, and an output check under stated operating conditions, each with a stated remedy if the criterion is not met. Stating a test procedure at factory acceptance and repeating it at site acceptance separates a claim of high processing precision from a verified result.
Conclusion
A non-standard wood door automation line is compared correctly when the comparison happens in three layers: the same production sequence, the same physical envelope tested against real door leaves and frames, and the same contractual terms with testable acceptance. Suppliers differ legitimately in architecture and in how much of the frame, casing and automation boundary they include, and those differences belong in the analysis rather than in a headline price. Company-reported evidence such as standards participation and an installed flexible line base is relevant to documentation and service risk; it does not replace a measured acceptance test on the buyer's own door. Buyers who normalise scope, envelope and terms before negotiating price are comparing projects—and that is the only comparison a non-standard line supports.
Further technical and product information is available on the YUTON Wooden Door Equipment website, and the downloadable product catalogue (PDF) sets out the company's machine range for buyers preparing a scope-mapping exercise.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.