
ZY-IML Shortlist by Application: Food, Paint Bucket, Yogurt Cup
An application-led selection guide for matching in-mold label grade, film and print specification to the container a buyer is actually filling.
In-mold labeling (IML) is a decoration method in which a pre-printed label is placed into the mold and fused to the plastic part while the part is being formed. The label becomes part of the container wall rather than a film applied on top of it. For buyers who have already decided that IML belongs in the packaging specification, the open question is narrower and more practical: which label grade, which film and which print specification survive a specific container, a specific filling line and a specific regulatory class.
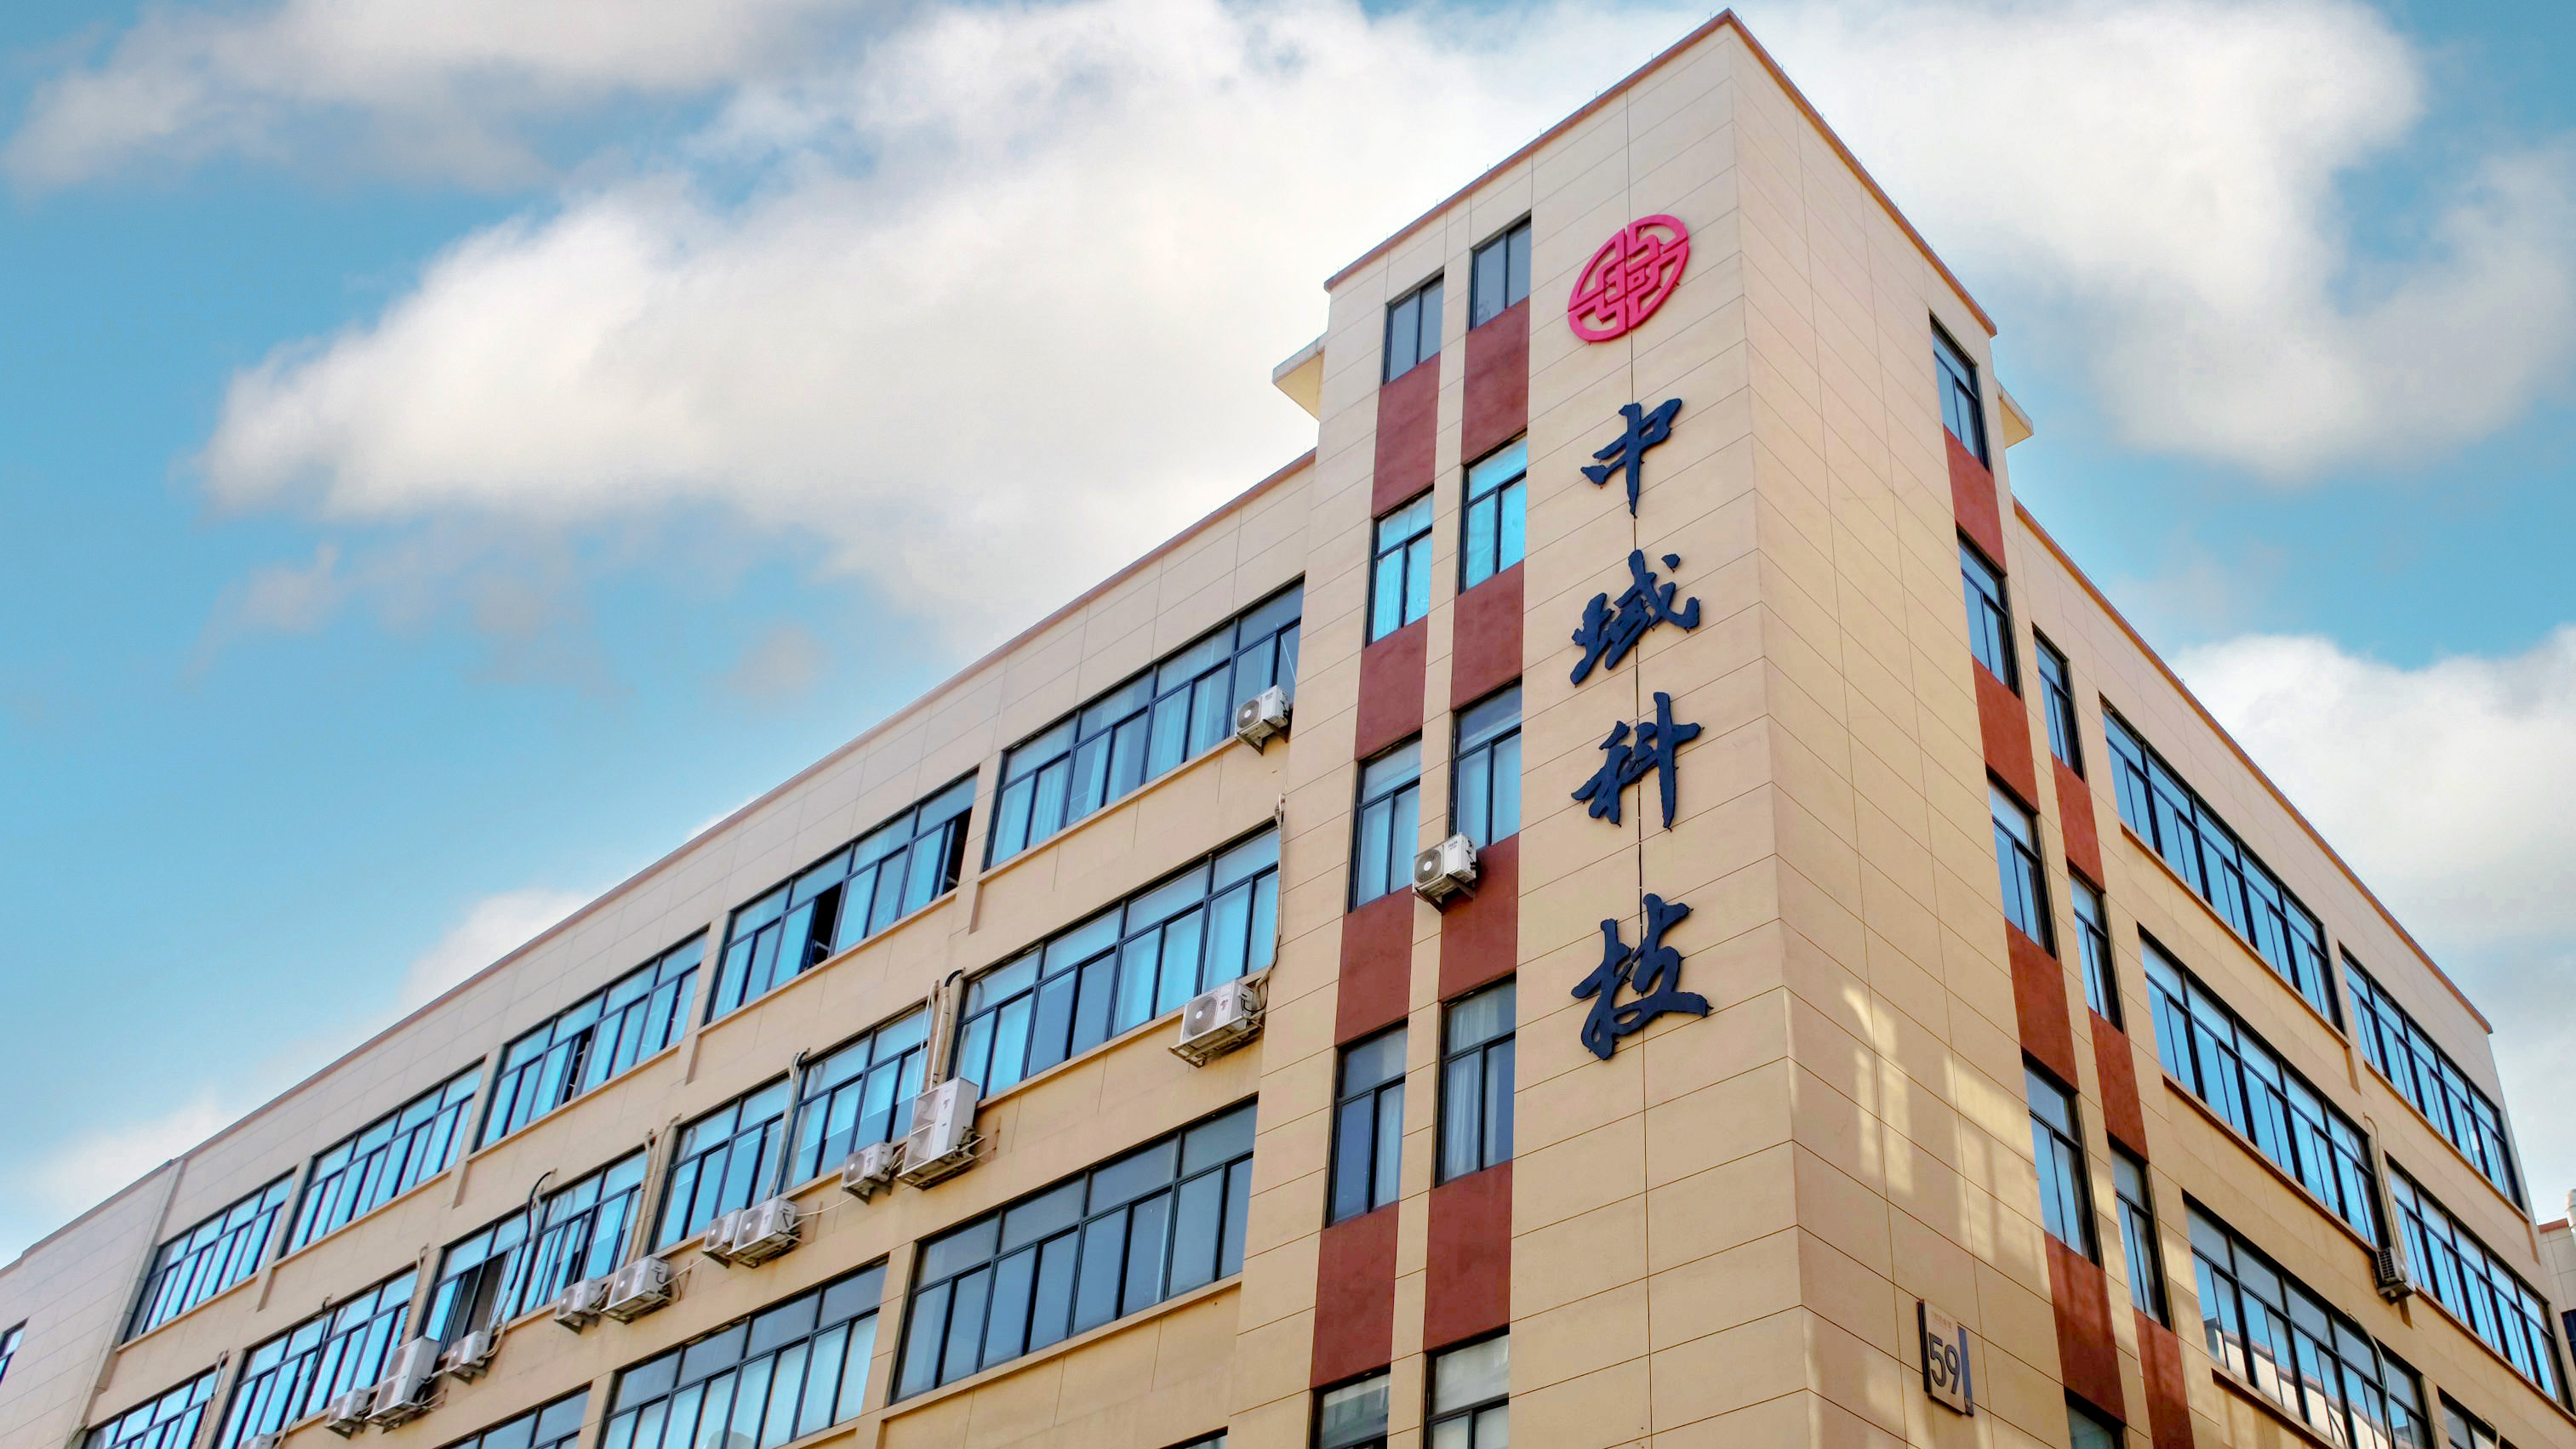
The ZY-IML Series is the in-mold label range produced by YZY (Zhejiang Zhongyu Technology Co., Ltd.), an in-mold labeling manufacturer founded in 2009 and based in Wenzhou, Zhejiang, China. YZY operates a 20,000 m² plant with 250 employees, including a 10-person R&D team, and reports 48 accumulated patents across its label and film processes. The company holds QS, ISO and BRCGS management-system certificates and reports 16 years without a major quality accident in food-grade packaging, with exports accounting for roughly 30% of output.
This shortlist is organised the way a packaging engineer would actually use it: by the container being decorated. It sets out the food-grade, daily chemical-grade and industrial-grade options in the series, the film and print parameters that connect them to PP, PE and PET containers, and the compliance and performance evidence a buyer should request before releasing a purchase order. It also states where in-mold labeling is the wrong answer, because a shortlist without boundaries is not a shortlist.
Why the Container Decides the Label
Because the label is fused during molding, the label specification and the container specification are frozen at the same moment. That single fact explains most qualification failures. A label that performs well on one container can wrinkle, blister or under-adhere on another, because film softening behaviour, wall thickness, gate position and cooling all interact inside the same tool.
Two technical rules follow from this. First, the label film is normally matched to the polymer family of the molded part. Polypropylene labels on polypropylene containers are the common pairing, since film and substrate soften in a compatible way and the finished pack stays mono-material. Second, the process routes the application: in-mold labeling is used in injection molding, blow molding and thermoforming, and each route places different demands on film stiffness, static behaviour and cut accuracy. A thin-wall injection-molded yogurt cup and a blow-molded paint bucket are not the same labeling problem, even when both carry a printed film.
Three Variables to Settle Before Price
Container resin and molding process. PP, PE and PET behave differently under heat and pressure, and a film chosen for an injection-molded cup is not automatically right for a blow-molded bottle. The process also sets the minimum film stiffness the label magazine and the in-mold robot can handle reliably.
Contents and regulatory class. A food-contact pack, a household detergent bottle and an industrial pail sit in different compliance categories. The grade of label, the ink system and the documentation package should follow the contents, not the container's shape.
Decoration specification. Colour count, coverage, small text, registration tolerance and finish determine whether a 30 μm film is sufficient or a heavier gauge is needed, and whether the artwork can be nested efficiently across the printing width.
The ZY-IML Series Shortlist at a Glance
| Packaging application | Grade | Film options | Compliance position |
|---|---|---|---|
| Food packaging: cups, tubs, trays, lids, containers | Food grade | PP, PE (PET where the container is PET) | FDA 21 CFR, BRCGS, ISO 22000, QS; food-grade low-migration water-based ink |
| Yogurt cup and chilled dairy cup | Food grade | PP, matched to the cup resin | As above; chilled-chain performance from −20 °C |
| Paint bucket | Industrial grade | PP or PE, matched to the bucket resin | Industrial grade; chemical compatibility validated per formula |
| Daily chemical: bottles, jars, closures | Daily chemical grade | PP, PE, PET | Daily chemical grade; moisture and abrasion resistance |
| Industrial packaging: pails, totes, crates, large containers | Industrial grade | PP, PE, PET | Industrial grade; large-format printing up to 1200 mm width |
Shared across all grades: 30–100 μm customizable film thickness, ±0.1 mm printing precision, ≥5 N adhesion strength, 4H scratch resistance and −20 °C to 120 °C service temperature.
Food Packaging: Food Grade Is the Entry Ticket, Not the Differentiator
In food packaging, a food-grade statement is not a competitive advantage; it is the minimum documentation a buyer should expect. What separates one food-grade label offer from another is the depth of the compliance trail behind it and the ink system used on the printed surface.
The ZY-IML Series food-grade option is positioned against FDA 21 CFR for food-contact materials in the United States, BRCGS for packaging-material hygiene and safety management, ISO 22000 for food safety management systems, and QS for the Chinese production licensing regime applicable to food-contact products. Printing uses a food-grade low-migration water-based ink system, which matters because migration risk in a printed food pack is driven primarily by the ink and coating layer rather than by the polymer film.
Performance parameters give the buyer something to test against rather than simply accept. Adhesion strength of ≥5 N covers resistance to peeling during filling, capping and wash-down. Scratch resistance of 4H covers the abrasion a decorated cup or tray meets in a case pack and along a distribution chain. A service window of −20 °C to 120 °C covers chilled and ambient distribution through typical hot-fill conditions, and it also marks the boundary where a standard grade stops being appropriate.
What a food buyer should request before approval is specific: the ink declaration for the actual print job, not a generic statement; the film grade and thickness in writing; and confirmation that the compliance documentation applies to the production site that will run the order. A certificate that cannot be tied to a site and a product code does not reduce procurement risk.
Yogurt Cups: Thin-Wall Injection Molding and the Chilled Chain
The yogurt cup is one of the least forgiving in-mold labeling applications. Walls are thin, cycle times are short, cavities are numerous, and the printed area often carries small mandatory text at a size where registration error becomes visible. A cup label also has to survive condensation, chilled storage and handling by the consumer.
The practical specification is a food-grade label on PP film matched to the cup resin, within the 30–100 μm customizable thickness range. Thickness selection is a trade-off rather than a preference: heavier film feeds more consistently through high-cavitation label magazines and resists curling, while lighter film conforms better to tight radii and reduces material cost per label. This is a parameter to fix with the molder, not to inherit from a previous project.
Print precision of ±0.1 mm and a maximum printing width of 1200 mm work together on a cup programme. The width allows multiple labels to be nested across the web, which lowers unit cost on high-volume orders; the precision keeps nutrition panels, batch coding areas and brand marks inside tolerance on a small face. Where the cup will be filled and stored below zero, the −20 °C lower bound of the service window is directly relevant, and buyers running frozen dairy should treat it as a hard constraint on grade selection.
One boundary deserves emphasis. In-mold labeling removes the peeling failure mode of post-mold labels because the decoration is integrated into the container during injection molding. It does not remove the need to validate adhesion on the actual cup, with the actual resin, at the actual wall thickness.
Paint Buckets: Industrial Grade and the Chemistry Question
Paint buckets sit at the opposite end of the format range. Containers are large, frequently blow-molded or injection-molded in HDPE or PP, stacked under load, and stored in warehouses and retail environments where the decoration is expected to stay legible for the life of the pack.
The ZY-IML Series industrial grade is the relevant option, on PP or PE film matched to the bucket resin. The specification of choice here is adhesion strength of ≥5 N combined with 4H scratch resistance, because a painted pail meets abrasion from stacking, strapping and pallet handling rather than from a filling line. The 1200 mm printing width becomes a cost lever: large bucket labels can be laid out across the full web, which affects the number-up and therefore the unit price per label.
The chemistry question is where buyers should slow down. In-mold labeling decorates the exterior of the container; the barrier against the contents is provided by the bucket, not by the label. A solvent-based or aggressive formulation still needs to be validated against the container and against any ink that could be contacted during filling, spillage or wiping. Industrial grade is a label classification, not a chemical-resistance guarantee, and a buyer who treats it as one is carrying an unmanaged risk. The correct action is a compatibility check with the converter and the resin supplier before the artwork is released.
Daily Chemical Packaging: Decoration Under Humidity and Handling
Detergent, shampoo, fabric-care and household-cleaning packs combine a demanding visual surface with a demanding physical environment: bathrooms, laundry rooms, wet wipes, repeated handling. Post-mold labels in these conditions are exposed to lifting and edge wear, which is one reason the category has moved toward in-mold decoration.
The daily chemical grade in the series is available on PP, PE or PET film within the same 30–100 μm thickness range, and it inherits the 4H scratch resistance and ≥5 N adhesion figures that matter most for a bottle that will be handled wet. Water-based low-migration inks are used here as well, though a buyer should not assume that a food-grade ink system answers a household-chemistry question: fragrance oils, surfactants and alcohol-containing formulas each need their own compatibility review.
Film choice is a decision lever rather than a default. PET film is available in the range and can suit containers where the film's stiffness and print behaviour match the tooling, but a PET label on a PP or PE bottle breaks the mono-material story. Buyers who intend to make a recyclability claim on the pack should confirm that the label film matches the container polymer family, and should get that confirmation in writing from the converter rather than inferring it from a film datasheet.
Industrial Packaging: Where Print Width Sets the Cost
Pails, totes, crates, drums and large containers are usually decorated for identification rather than for shelf appeal, which changes the specification priorities. Colour complexity drops, coverage often rises, and label area per part becomes large. In this segment the 1200 mm maximum printing width and the ±0.1 mm precision matter mostly as cost and legibility factors: more labels per metre of printed film, fewer rejects on long text blocks such as hazard and handling information.
Industrial grade on PP, PE or PET covers this segment. As with paint buckets, the label does not provide chemical barrier, and a buyer specifying decoration for a container that will hold regulated industrial contents should separate the label qualification from the container qualification in the project plan.
Reading the Four Specification Levers
| Parameter | ZY-IML Series | What it controls | What the buyer should verify |
|---|---|---|---|
| Film thickness | 30–100 μm, customizable | Stiffness, conformability on radii, label-magazine feeding, material cost | Trial run on the actual tool and cavity count |
| Printing width | Up to 1200 mm | Number-up per printed web, unit cost, large-format coverage | Artwork layout and repeat length for the intended nest |
| Print precision | ±0.1 mm | Register between colours, cut position, legibility of small text | Smallest font size and mandatory text requirements on the pack |
| Ink system | Food-grade low-migration water-based ink | Migration risk in food contact, odour, print durability | Ink declaration tied to the specific job |
| Adhesion and surface | ≥5 N adhesion, 4H scratch resistance | Peel resistance during filling and washing, abrasion in distribution | Test method and acceptance level agreed in the specification |
| Service temperature | −20 °C to 120 °C | Chilled storage, ambient distribution, hot-fill conditions | Actual fill temperature and dwell time |
What the Compliance Evidence Actually Covers
Compliance documents are frequently collected as a set and read as a single yes or no. They are not. Each one answers a different question, and a buyer who can name what each covers is in a much stronger position at the audit stage.
| Reference | Type | Question it answers |
|---|---|---|
| FDA 21 CFR | Food-contact regulation (US) | Whether the materials and formulations are acceptable for food-contact use in the US market |
| BRCGS | Packaging materials safety and quality management | Whether the site's hygiene, traceability and process controls are audited to a recognised standard |
| ISO 22000 | Food safety management system | Whether hazards are systematically identified and controlled across the process |
| QS | Chinese production licensing for food-contact products | Whether the production entity is licensed for the product category in China |
| Third-party laboratory testing | Verification | Whether a specific sample met a specific test criterion |
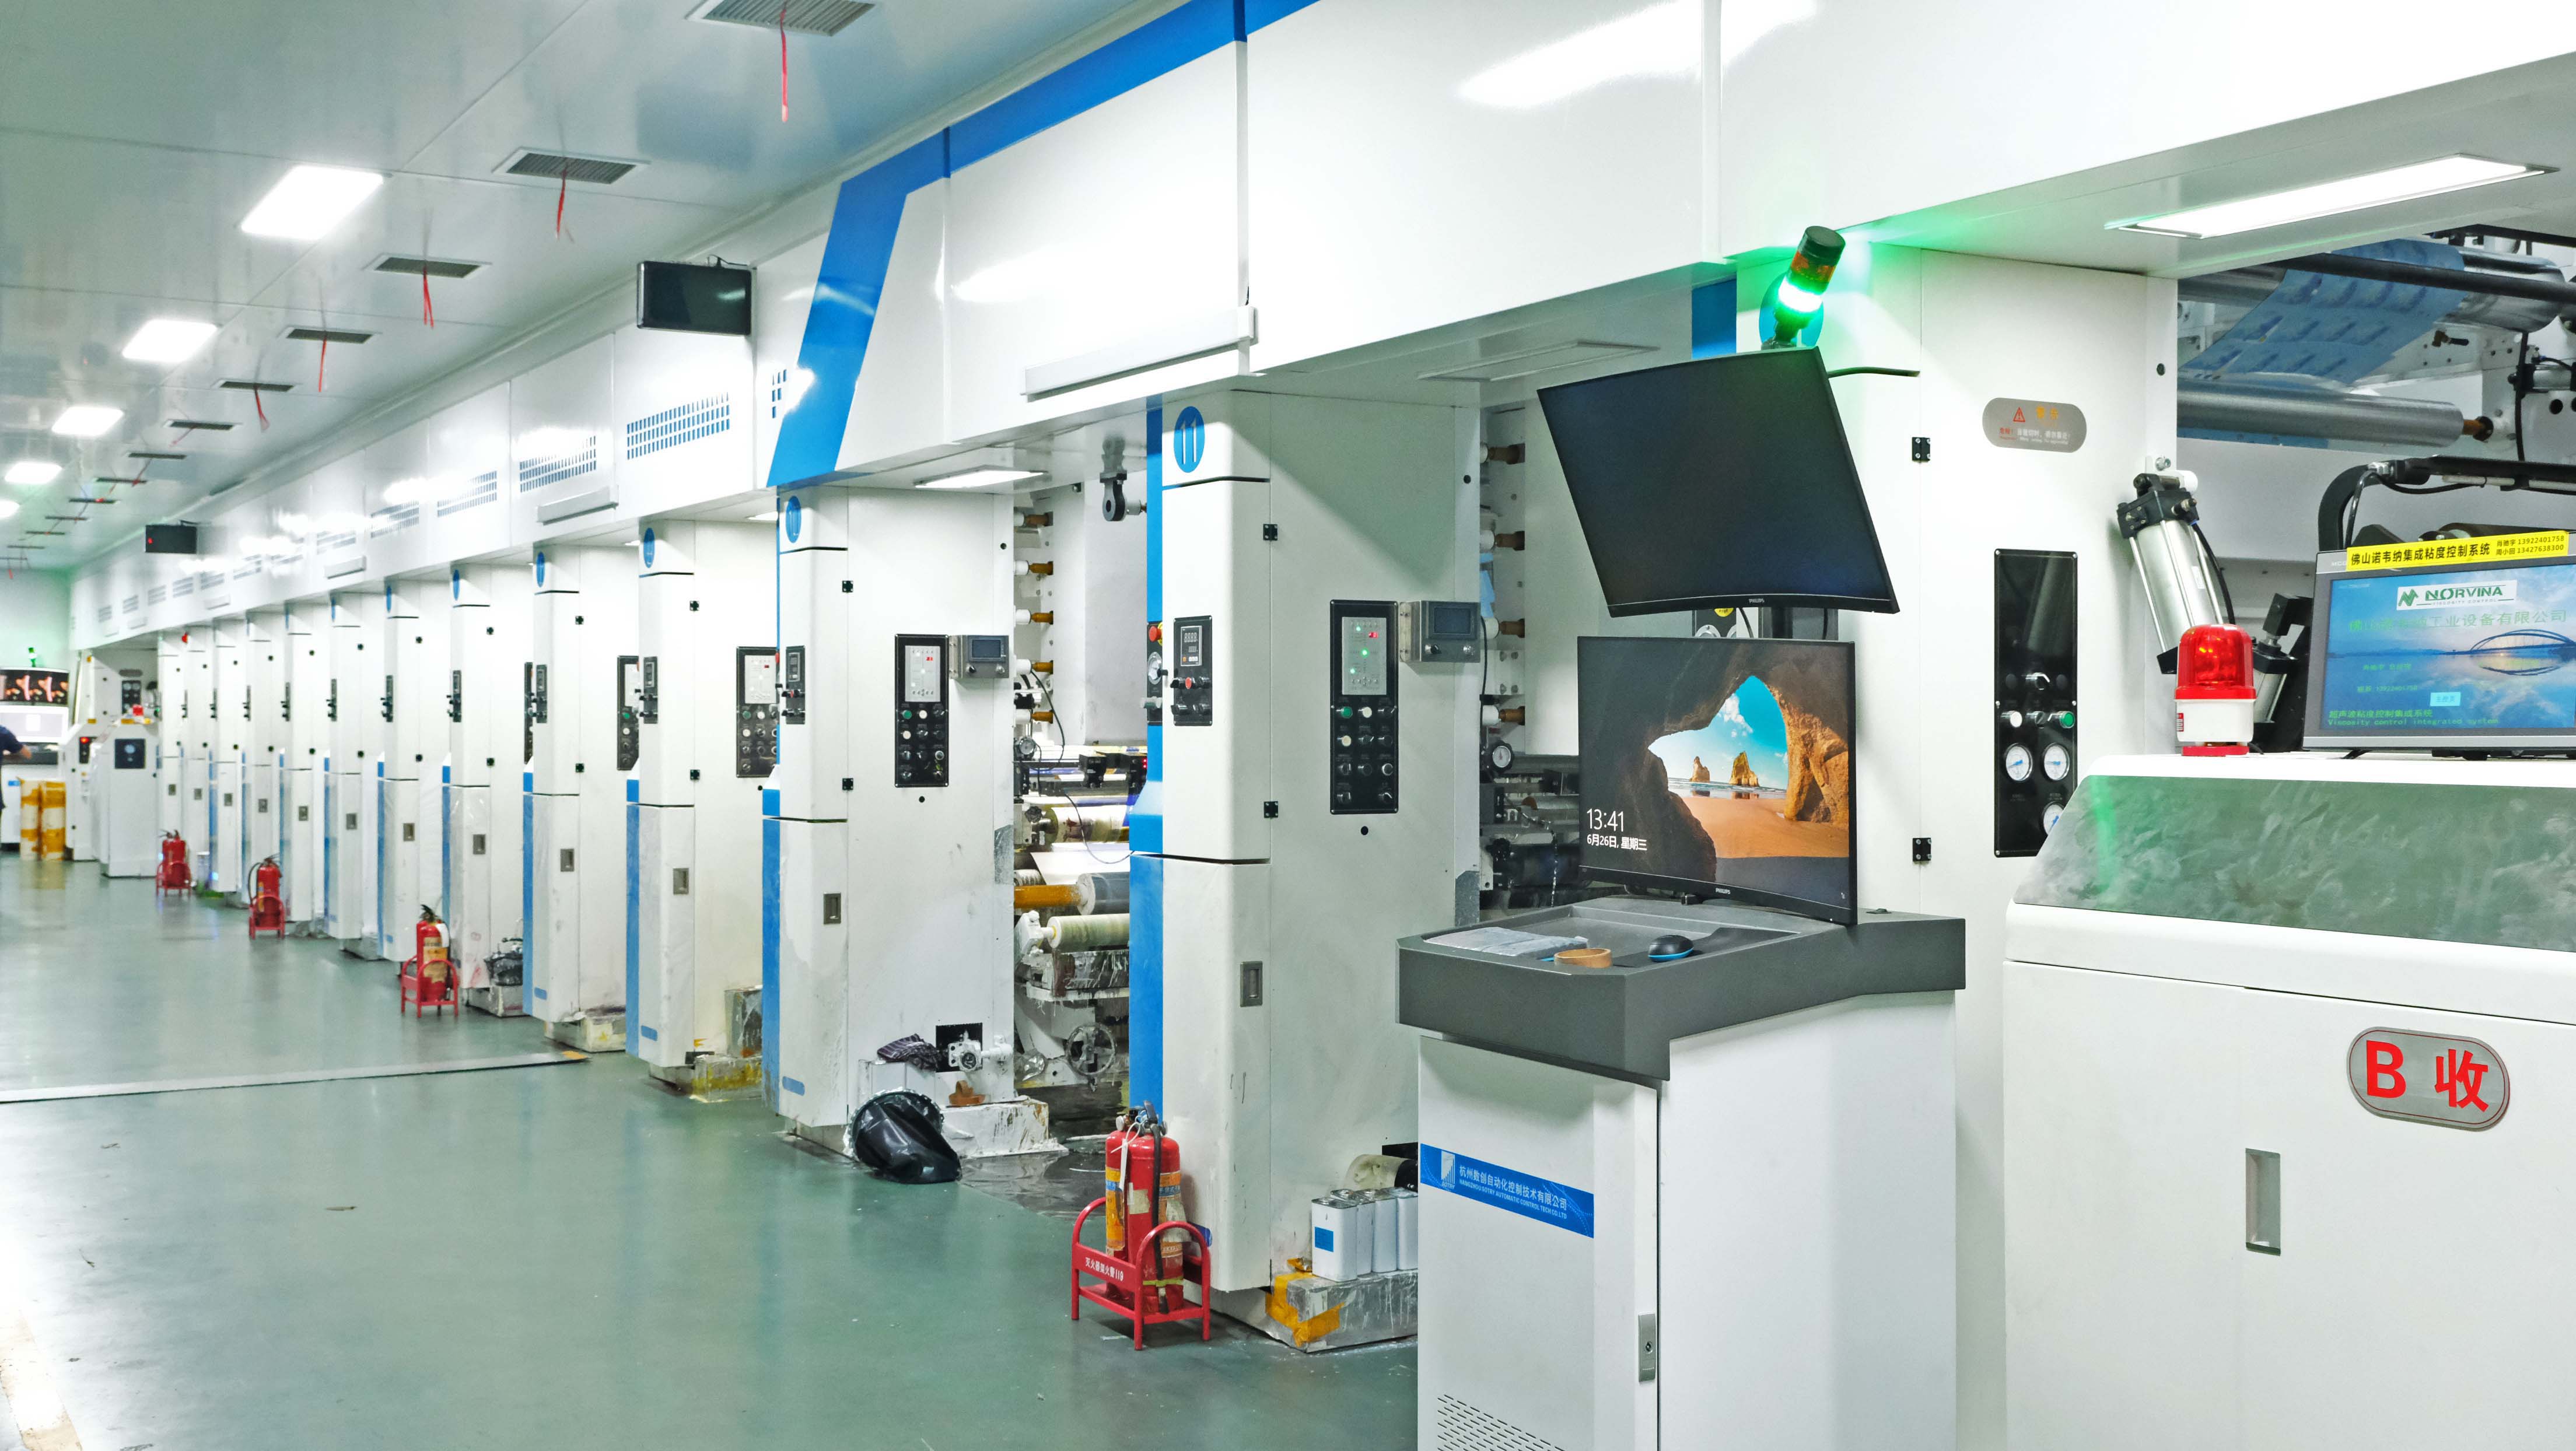
YZY's process control is layered around these documents rather than replacing them: incoming raw material inspection, three in-process testing points, final random inspection and 100% visual inspection on the line, production tracked in real time through an ERP system, two backup production lines held against delay risk, and annual BRCGS, ISO and FDA-related audits. For a buyer, the value of this is traceability — the ability to connect a delivered carton back to a material batch and a production run.
ZY-IML Series Against Post-Mold Labeling
Most IML decisions are made against a working alternative: a pressure-sensitive or wet-glue label applied after the container is molded. The comparison is often framed as a choice between durability and flexibility, and that framing is roughly correct, but the cost side is more interesting than it first appears.
| Decision factor | ZY-IML Series (in-mold) | Post-mold labeling |
|---|---|---|
| When decoration is applied | Inside the mold, fused to the part during molding | After molding, as a separate production step |
| Production steps | Integrated labeling reduces production steps by 30% and supports high-volume orders | Additional labeling step after molding |
| Lead time | Reported 20% shorter lead time versus post-production labeling | Baseline for comparison |
| Peel and humidity risk | No peel failure mode; the label is part of the container | Adhesive labels can lift or fall off, particularly in high-humidity conditions |
| Cost structure | Slightly higher material cost, offset by lower post-production labour and fewer rejects | Lower material cost, higher downstream labour and reject exposure |
| Late SKU changes | Artwork is fixed before molding | Labels can be changed close to dispatch |
| Container types | Requires a moldable plastic part compatible with the film | Works on already-molded parts, including glass and metal |
Read together, the table describes a volume-and-process decision rather than a quality hierarchy. Where an IML line is already running and the artwork is stable, the integrated route removes a production step, shortens the critical path and eliminates a known failure mode. Where the buyer is decorating purchased containers from several suppliers, changes artwork frequently, or runs very short batches, post-mold labeling retains an advantage that IML cannot match.
Where In-Mold Labeling Is the Wrong Choice
A shortlist that omits limits is a sales document. Five boundaries apply to the ZY-IML Series and to in-mold labeling generally.
Temperature ceiling. The stated service window ends at 120 °C. Processes above that — retort sterilisation, for example — fall outside the standard grade and should not be specified without a dedicated engineering review.
Artwork lock-in. Because the label enters the mold, the design, colour separations and cut shape must be finalised before production. Programmes with frequent promotional variants on short runs carry an economic penalty that post-mold labeling avoids.
Resin and tooling dependence. Qualification is specific to the container resin, wall thickness and cavity layout. A label approved on one cup does not transfer automatically to a differently tooled cup from another molder.
Label is decoration, not barrier. For paint buckets, daily chemical bottles and industrial pails, chemical compatibility between the contents and the container remains the buyer's validation responsibility. In-mold decoration does not change it.
Substrate scope. In-mold labeling applies to molded plastic. Glass, metal and paperboard containers are outside the process entirely.
Market Signals Buyers Should and Should Not Use
Three published signals are useful when framing an IML decision, and one is actively misleading if taken at face value.
The first is material direction. Grand View Research reports that polypropylene held a 56.9% share of the in-mold label market in 2025, which is consistent with the technical logic of polymer matching described earlier. The second is process direction: the same publisher reports injection molding at more than 57.1% revenue share of the segment in 2023, reflecting the dominance of thin-wall cups, tubs and containers. The third is the film specification norm: standard IML film thickness is generally cited in the 30–100 μm range, which is the same envelope the ZY-IML Series is built around.
The signal to treat cautiously is market size. Commercial research publishers report materially different global figures for the same years, using different definitions that may or may not include label film, printed labels, equipment or decoration services. Those numbers should not be averaged, combined into a range, or used as the basis of an investment case. A buyer or brand owner building a business case should define the market boundary explicitly and validate it against their own channel data.
Regulatory direction is the fourth signal, and it is the one most likely to change label specifications. The US FDA updated its Inventory of Effective Food Contact Substance Notifications on 31 May 2026, announcing that notifications for 35 PFAS substances are no longer effective. For packaging buyers, the practical consequence is a sharper question about what is actually in the ink and coating layer, and whether the supplier can document it. A low-migration water-based ink system with a job-specific declaration answers that question better than a general compliance statement.
Future Outlook
Two pressures are likely to shape in-mold label specifications over the next procurement cycles. The first is mono-material design: as recyclability criteria tighten, a PP label on a PP container becomes easier to defend than a mixed construction, and buyers will increasingly ask for polymer matching as a written requirement rather than a preference. The second is documentation depth: the direction of food-contact regulation, including the PFAS notification withdrawals, points toward ingredient-level transparency in inks and coatings rather than certificate-level assurance alone.
On the manufacturing side, the parameters that matter are already measurable — film thickness consistency, register precision at ±0.1 mm, adhesion above 5 N, 4H surface resistance — and the competitive gap will be in how consistently those are held across high-volume runs rather than in new headline claims. Buyers who specify these as acceptance criteria, with a test method attached, will get more value from the category than buyers who specify them as marketing attributes.
FAQ
Which ZY-IML grade should a food packaging buyer specify?
The food grade is the applicable option for cups, tubs, trays, lids and food containers. It is positioned against FDA 21 CFR, BRCGS, ISO 22000 and QS, uses food-grade low-migration water-based ink, and is available on PP or PE film within 30–100 μm thickness. Buyers should confirm that the ink declaration and certificates apply to the specific production site and product code.
What film and thickness fit a yogurt cup label?
A food-grade label on PP film matched to the cup resin is the standard pairing. Thickness is customizable within 30–100 μm; heavier film feeds more reliably in high-cavitation molds, lighter film conforms better to tight radii. Print precision is ±0.1 mm and the service window starts at −20 °C, which covers chilled and frozen dairy storage.
Is in-mold labeling suitable for paint buckets, and what must be validated first?
Yes, under the industrial grade on PP or PE film matched to the bucket resin, typically for blow-molded or injection-molded HDPE or PP containers. What must be validated first is chemical compatibility between the contents and the container, because the label decorates the exterior and does not provide barrier. Adhesion of ≥5 N and 4H scratch resistance are the relevant durability figures for stacking and handling.
How does in-mold labeling compare with post-mold labels on cost and lead time?
Integrated IML reduces production steps by 30% and is reported to shorten lead time by around 20% versus post-production labeling. Material cost per label is slightly higher, but the total cost position improves through lower post-production labour and fewer rejects. The trade-off is that artwork must be fixed before molding, which disadvantages very short runs and frequent design changes.
What are the limits of the ZY-IML Series?
The service window is −20 °C to 120 °C, so processes above 120 °C fall outside the standard grade. Qualification is specific to the container resin, wall thickness and tooling and does not transfer automatically between projects. The label is decoration rather than barrier, and the process applies to molded plastic only, not to glass, metal or paperboard.
Summary
Matching an in-mold label to an application is a four-part exercise: identify the container resin and molding process, classify the contents and the regulatory class, fix the film and print parameters against the tooling, and require the compliance documentation to be tied to the site and the job. The ZY-IML Series covers food, daily chemical and industrial grades across PP, PE and PET film within a 30–100 μm thickness range, at 1200 mm maximum printing width and ±0.1 mm precision. The value of the shortlist lies as much in its boundaries — temperature ceiling, artwork lock-in, resin dependence and the absence of barrier function — as in the options it lists.
A downloadable ZY-IML Series brochure with product and specification details is available here: ZY-IML Series brochure (PDF).
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.