
Drum Motors for Smart Manufacturing: Airport Screening Fit
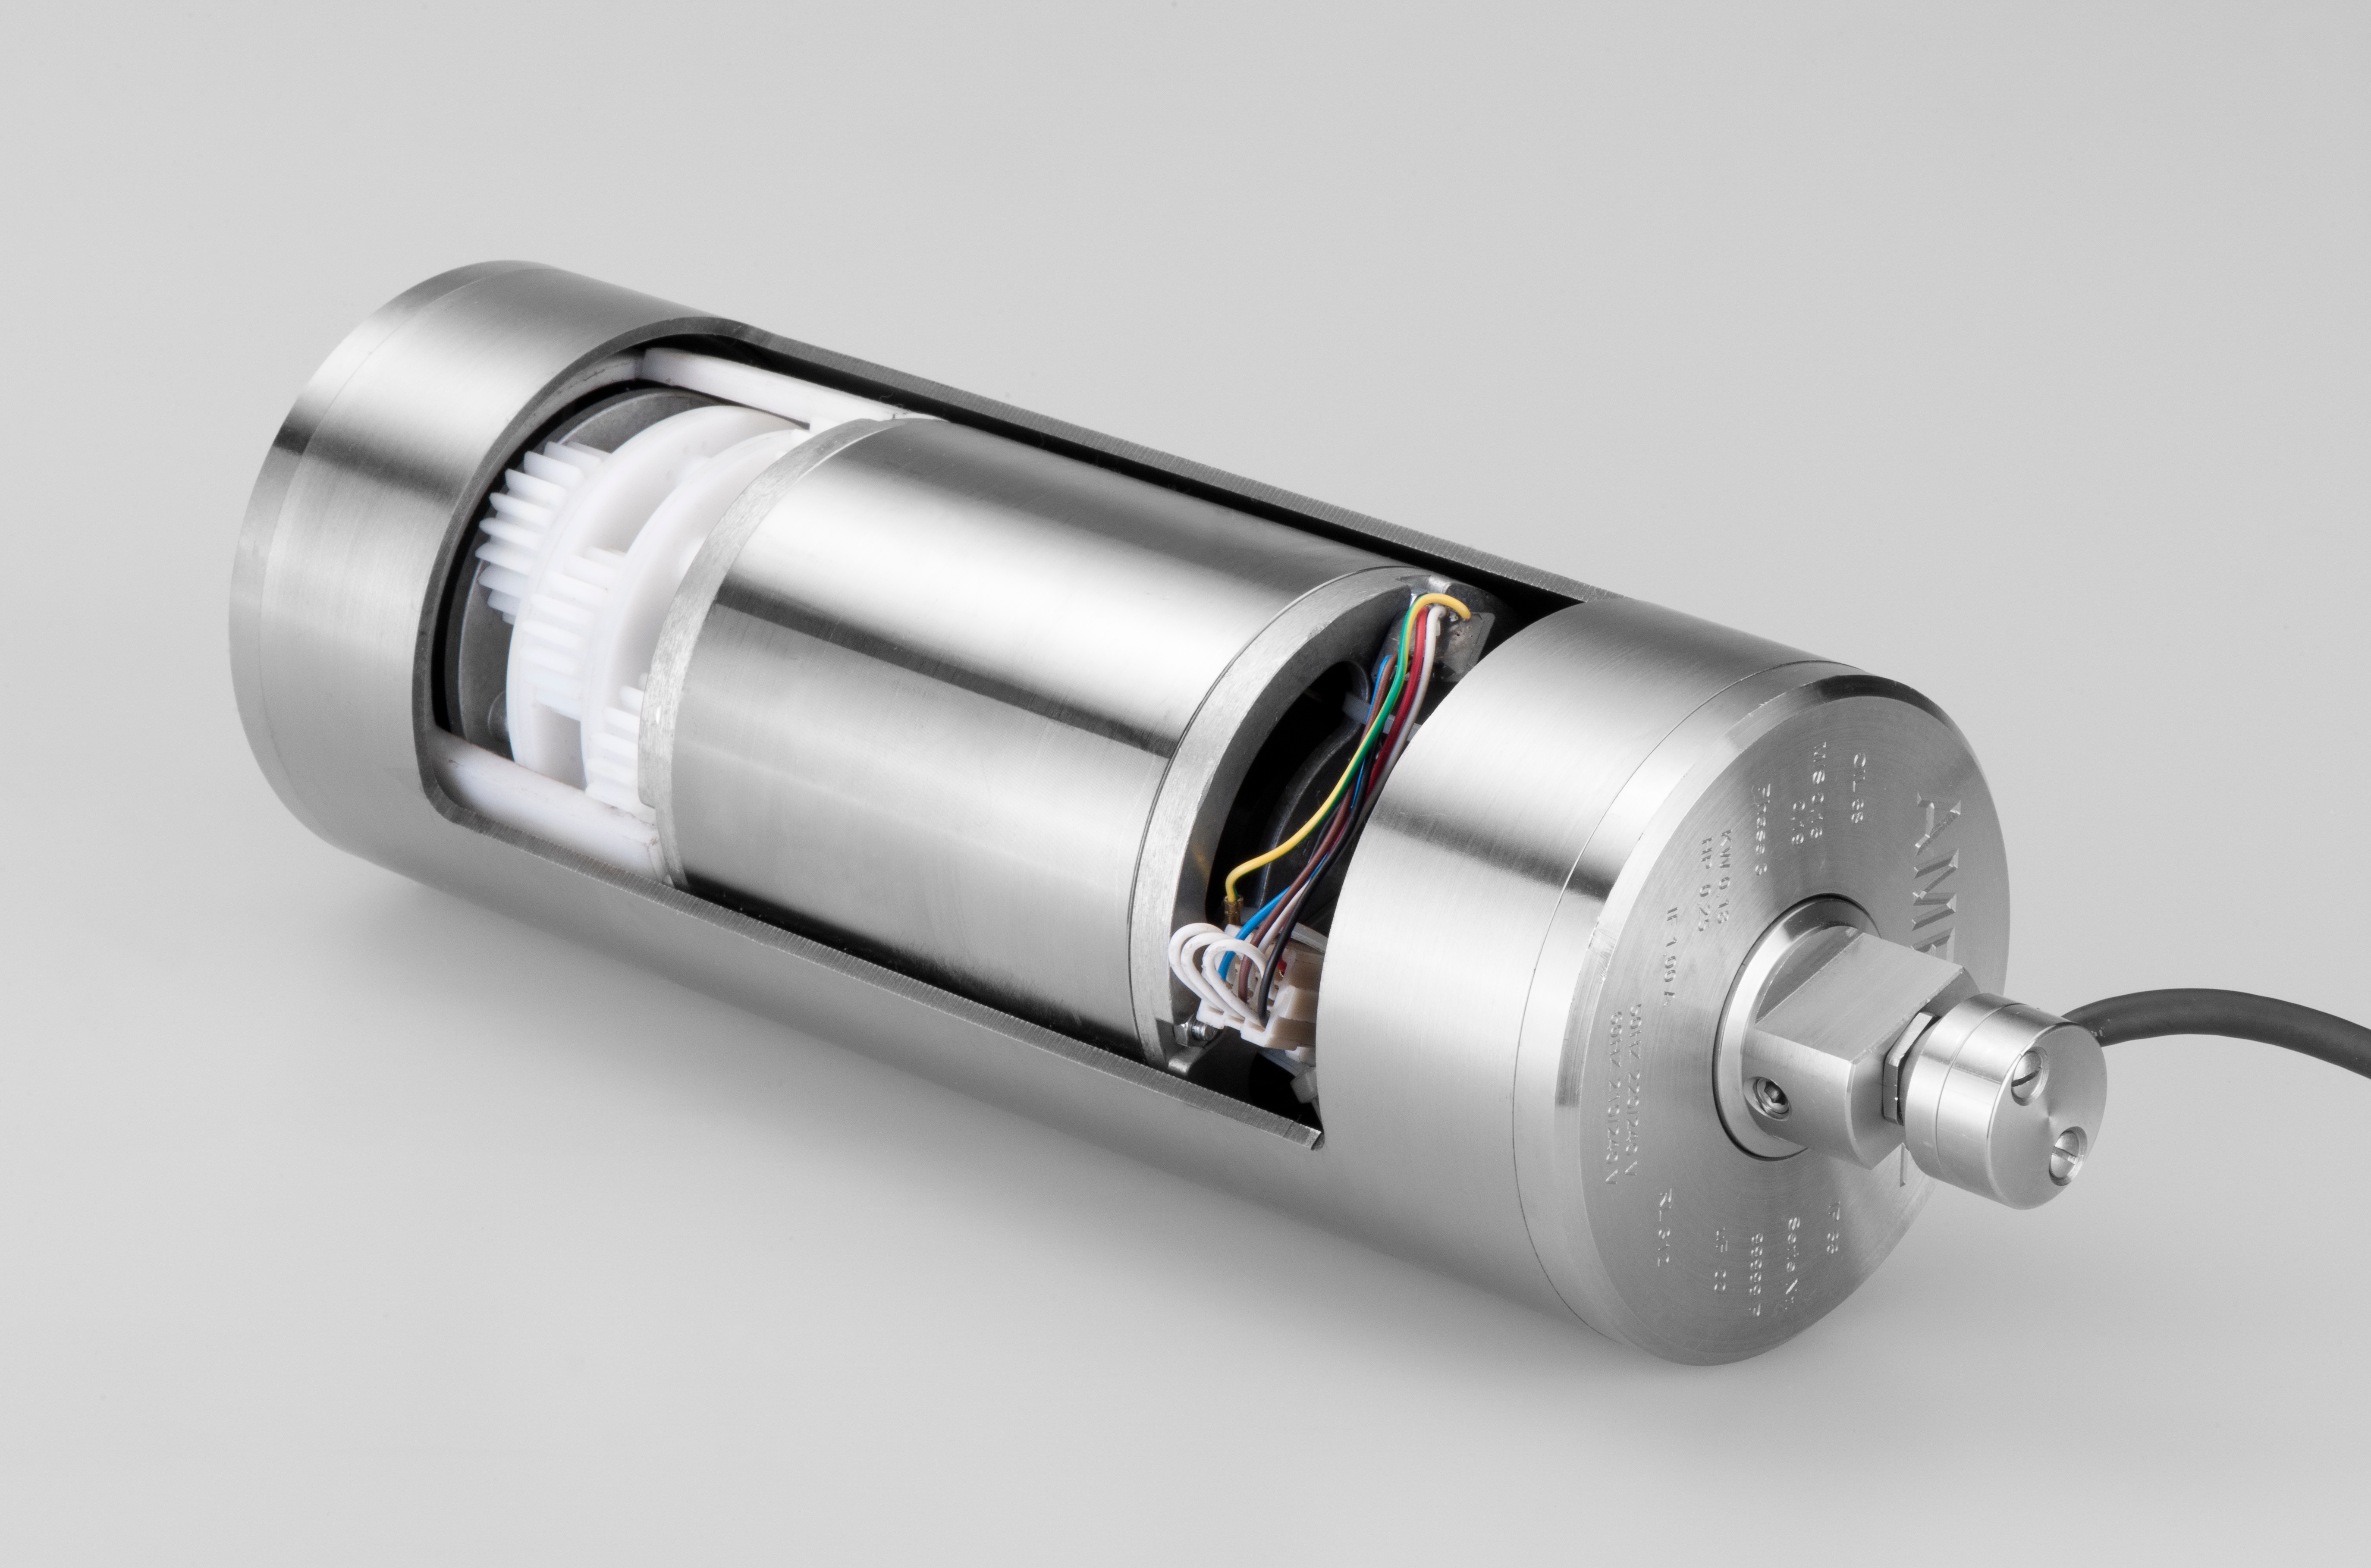
A drum motor is a conveyor drive in which the electric motor, gear stage and bearings sit inside the pulley that moves the belt. For smart manufacturing projects this packaging decision is not cosmetic — it determines the height of the conveyor, the shortest possible transfer section, the number of wear parts a maintenance team must stock, and how easily a line can be reconfigured. Airport baggage handling and security screening show the trade-offs most clearly, because those conveyors run inside X-ray tunnels, between tray-return loops and under check-in counters, on continuous duty with frequent start-stop events.
Why the drive inside the pulley matters on an airport line
Airport security inspection equipment places a specific set of demands on a conveyor drive. The application profile for airport civil aviation and security inspection equipment lists high-precision positioning, stable low-speed operation and anti-interference capability as working conditions, with a duty pattern of continuous operation and frequent start-stop capability. The conveyor handles luggage and parcels moving through an X-ray scanner, and the drive is expected to position trays accurately rather than simply move them.
Matching equipment on such a line typically includes the X-ray security scanner, baggage trays, metal detectors and conveyor guide rails. The special requirements recorded for this scenario are high precision speed control, low vibration, anti-electromagnetic interference and flame-retardant construction. Those requirements narrow the drive options considerably. A conventional gearmotor bolted to the side of a frame introduces an exposed rotating element, a chain or belt guard, and a footprint that competes for space with the scanner geometry.
The bottleneck is dimensional before it is electrical
In a screening conveyor, the pulley diameter sets the belt height, and belt height fixes how the conveyor sits relative to the tunnel opening. On a retrofit — a common situation when an airport upgrades screening capacity without rebuilding the hall — the available vertical space is already committed. Similarly, the minimum roller width defines the shortest pulley that can still contain the gear stage and bearings, which in turn decides how close two conveyors can be placed side by side and how short a transfer or tray-return section can be built.
This is where light-duty drum motors earn their place in smart manufacturing layouts. A drive that lives inside the pulley removes the side-mounted motor envelope entirely, so the conveyor's outside width is essentially the belt width plus the frame. For an OEM building screening equipment, that reduction can be the difference between fitting a scanner into an existing queue area and requiring civil works.
Four parameters that decide fit, in decision order
1. Belt pull and torque
Belt pull is the controlling number. It is derived from the tray or bag weight, the length of the conveyor, friction in the belt and support, and any incline. Only after belt pull is known should a diameter be chosen, because each roller diameter corresponds to a torque range and a maximum belt pull.
2. Roller diameter
Roller diameter follows the space available in the conveyor frame and the belt pull required. In the SEAPARKS light-duty range the available diameters are Ø80 mm, Ø113 mm and Ø138 mm, giving project engineers a graduated set of options rather than a single size.
3. Minimum roller width
Minimum roller width is the shortest pulley length the manufacturer can build for a given model. It matters in screening lines where transfer gaps are short and the conveyor must fit between guide rails. Narrower is not automatically better: a wider roller distributes bearing load and reduces belt tracking sensitivity.
4. Belt speed and protection class
Nominal belt speed is fixed by the gear ratio at the time of order, so the speed range a model can reach must be confirmed before the order is placed. Protection class is a separate decision driven by the cleaning regime of the facility, not by the load.
How SEAPARKS light-duty models map to those parameters
Tianjin Seaparks Machinery-Electronics Co., Ltd, trading as SEAPARKS, is a Chinese manufacturer of motorized conveyor drums founded in 2002. The company operates a 50,000 m² plant with 360 employees and a 40-engineer R&D team, and states that more than one million of its motorized drums are in operation worldwide, with exports to more than 50 countries. Its light-duty platform is specified for security screening conveyors at airports and railway stations, airport baggage handling systems, packaging conveyors, belt scale conveyors and general belt conveyors.
The verified specification set below is the practical starting point for a screening or baggage project, because it exposes the trade-off between diameter, width, speed and pull in one view.
| Model | Motor type | Roller Ø | Min. roller width | Nominal belt speed | Max. belt pull | Protection |
|---|---|---|---|---|---|---|
| TM80M | Single-phase asynchronous, polymer gear | Ø80 mm | 260 mm | 0.05–0.85 m/s | 630 N | IP66/IP67/IP69 |
| TM80A | Three-phase asynchronous, alloy steel gear | Ø80 mm | 330 mm | 0.08–1.02 m/s | 705 N | IP66/IP67/IP69 |
| DM80A | Synchronous, DC | Ø80 mm | 310 mm | 0.16–1.03 m/s | 534 N | IP66/IP67/IP69 |
| TM113M | Single-phase asynchronous, polymer gear | Ø113 mm | 310 mm | 0.11–1.05 m/s | 770 N | IP66/IP67/IP69 |
| TM113A | Three-phase asynchronous, alloy steel gear | Ø113 mm | 335 mm | 0.09–1.4 m/s | 1469 N | IP66/IP67/IP69 |
| DM113A | Three-phase synchronous | Ø113 mm | 360 mm | 0.14–0.68 m/s | 2053 N | IP66/IP67/IP69 |
| TM138A | Three-phase asynchronous, alloy steel gear | Ø138 mm | 340 mm | 0.11–1.69 m/s | 3525 N | IP66/IP67/IP69 |
Source: SEAPARKS product specification data for the TM and DM series. Housings are carbon steel or 304 stainless steel depending on model and order configuration.
Reading the table as a selection sequence
TM80M is the narrowest option in the range at a 260 mm minimum roller width, and it is the natural first candidate for short tray-return and secondary search conveyors where the frame cannot accommodate a larger pulley. Its single-phase asynchronous motor with a polymer gear stage delivers up to 630 N of belt pull at belt speeds from 0.05 to 0.85 m/s.
TM113M moves one diameter up while keeping the single-phase, polymer-gear configuration, raising maximum belt pull to 770 N and extending the speed ceiling to 1.05 m/s. Where the same Ø113 mm envelope is needed but the load is heavier, TM113A switches to a three-phase asynchronous motor with an alloy steel gear stage and lifts maximum belt pull to 1469 N. DM113A, a three-phase synchronous unit, reaches 2053 N at a 360 mm minimum roller width — useful when a longer infeed section feeds a single screening tunnel.
DM80A is the DC synchronous member of the Ø80 mm group. Its 0.16–1.03 m/s speed band and 534 N maximum belt pull suit short, controlled-motion sections where a compact envelope matters more than raw pulling force.
Application scenes: from the X-ray tunnel to the check-in counter
Security screening conveyor. The infeed and outfeed sections either side of an X-ray scanner are the most dimensional-sensitive position on the line. Roller diameter controls belt height relative to the tunnel aperture, and stable low-speed operation is needed for consistent image capture and tray spacing. Here the Ø80 mm models and the Ø113 mm models cover most requirements, with the choice driven by belt pull and by the minimum roller width the equipment builder can accept.
Baggage check-in and tray return. These conveyors run continuously with frequent start-stop events and are usually integrated into counters or ceiling voids where side-mounted drives are difficult to service. A pulley-integrated drive keeps the equipment envelope clean and reduces the number of accessible pinch points along a passenger-facing line.
Secondary screening and manual search tables. Short conveyors and roller sections in secondary search areas benefit from the narrowest rollers in the range, because transfer gaps are dictated by the room layout rather than by throughput.
Adjacent plant applications. The same light-duty models are specified for packaging conveyors, belt scale conveyors and general belt conveyors, so an equipment builder supplying both airport and industrial customers can standardise on one drive family across product platforms.
Materials and ingress protection: IP66, IP67, IP69 and IP69K
All light-duty models in the range carry IP66/IP67/IP69 protection, with housings available in carbon steel or 304 stainless steel. The distinction between these ratings and IP69K is frequently blurred in project specifications, and it is worth separating them before an order is placed.
IP69K is defined under IEC 60529 and is applied where equipment must withstand high-pressure, high-temperature washdown — commonly cited as pressures up to 1450 psi and temperatures around 80 °C in food-processing environments. Within the SEAPARKS portfolio, IP69K is the rating of the hygienic F-series models such as TM216F, DM216F, TM165F and DM113F, which use 304 stainless steel housings with 316 stainless steel as an option. The light-duty TM80M, TM113M, TM113A and DM80A are specified to IP66/IP67/IP69, which reflects their intended airport and general conveying duty rather than a washdown food line.
That difference is a selection boundary, not a ranking. A check-in hall conveyor that is wiped down and occasionally hosed does not need an IP69K hygienic housing; a tray-wash or food-adjacent conveyor that sees 80 °C high-pressure cleaning does. Over-specifying raises unit cost and can complicate the frame interface, while under-specifying shortens bearing life. For European projects, drives must also satisfy the Low Voltage Directive 2014/35/EU and carry the CE mark, with safety standards such as EN 62841 or IEC 60034-1 commonly referenced in technical documentation. SEAPARKS holds ISO 9001, ISO 14001, ISO 45001, RoHS 2.0, UL and CE certification.
Where a drum motor is the wrong answer
A fair comparison between a drum motor and a conventional gearmotor-and-chain drive has to start with what each is designed to do. The drum motor wins on footprint, on the absence of exposed rotating parts, on cleaning and on the number of components a maintenance store must hold. The conventional drive wins on serviceability and on the ability to change a motor without dismantling the conveyor.
| Attribute | Drum motor | Gearmotor with chain or belt drive |
|---|---|---|
| Envelope along the conveyor | Contained within pulley width | Motor, gearbox and guard project sideways |
| Exposed rotating parts | None outside the pulley | Chain, sprockets or belts exposed unless guarded |
| Cleaning and hygiene | Sealed shell, IP66–IP69 available on light-duty models | Guards and cavities trap debris; cleaning is more involved |
| In-service repair | Pulley must be removed; no field motor swap | Motor or chain can be replaced in place |
| Speed change after installation | Set by gear ratio at order | Pulley or sprocket ratio can be altered more easily |
| Best fit | Compact, sealed, medium-duty conveying | Very high torque, heavy shock loads, frequent drive substitution |
The limitations are real. A drum motor has no external motor to swap, so a failure typically means removing the pulley from the frame — an acceptable trade in a conveyor designed for it, but a serious inconvenience in a frame built without removal clearance. Single-phase light-duty models in this range top out at 0.18 kW (TM113M) and 0.11 kW (TM80M), which caps their use to short, low-pull sections. Belt speed is fixed by the gear ratio chosen at order, so a project that may need a different throughput later should settle that question before manufacture. And for continuous very-low-speed, high-torque duty, or for abrasive and dusty heavy industry, a pulley-integrated light-duty drive is the wrong tool regardless of protection rating.
Market signals behind the shift
The direction of travel is toward more drive integration, not less. Custom Market Insights places the global drum motor market at roughly USD 2.07–2.13 billion across 2023–2025, with growth attributed to logistics automation and food processing demand. That range should be treated as directional: Dataintelo reports USD 2.8 billion for the same period and Market.us around USD 2.0 billion, a spread that reflects different treatments of ancillary conveyor components. Forecast growth rates diverge similarly, from about 4.06% (Maximize Market Research) to 7.3% (DataHorizzon Research).
Two structural signals are more useful to a project engineer than the headline size. First, Dataintelo reports the AC motor segment holding a 52.3% revenue share in 2025, which is consistent with the continued dominance of asynchronous drives in general conveying — the same configuration used by the TM80M, TM113A and TM138A. Second, Asia Pacific is projected at a 38.2% revenue share by 2025, reflecting industrialisation and e-commerce growth in China and India, which matters for lead times and for the regional availability of drive variants.
Efficiency is the third signal. Energy-efficient drum motors are reported by Rulmeca and Interroll to reach overall efficiency of up to 82–83%, which is the mechanism behind total-cost arguments in high-duty installations. On an airport line running continuously, that efficiency differential compounds across a fleet of conveyors, and it is one reason procurement teams increasingly ask for drive-level efficiency data rather than conveyor-level estimates.
An evaluation checklist for project engineers
- Belt pull calculation: confirm tray or bag weight, conveyor length, incline and friction before selecting a diameter.
- Available height: measure the tunnel or counter opening; the roller diameter sets belt height and cannot be absorbed elsewhere.
- Frame width: check the minimum roller width of each candidate against the actual frame and transfer gap.
- Speed requirement: confirm the nominal belt speed band matches throughput and positioning needs, and lock it at order.
- Cleaning regime: decide IP66, IP67 or IP69 on the basis of the actual washdown practice, and reserve IP69K housings for high-pressure, high-temperature cleaning.
- Housing material: carbon steel or 304 stainless steel, with 316 stainless steel available on hygienic models.
- Phase and control: single-phase where the supply is fixed and pull is low; three-phase where belt pull or speed range demands it.
- Service access: confirm the frame allows pulley removal, since that is the service path for a drum motor.
- Compliance documents: confirm CE, UL, RoHS 2.0 and ISO management system certificates against the destination market.
Future outlook
Smart manufacturing does not change the physics of a conveyor; it changes how tightly the drive must fit into a monitored, reconfigurable line. As screening equipment becomes more compact and airport operators retrofit existing halls rather than build new ones, the dimensional argument for pulley-integrated drives strengthens. The open questions are less about whether drum motors will be used and more about data: how a drive reports its condition, how speed setpoints are managed when the gear ratio is fixed at order, and how service access is designed into equipment that was previously built around an external motor. Equipment builders who resolve those questions at the frame-design stage will find the light-duty drum motor range a straightforward fit; those who treat the drive as an afterthought will keep defaulting to the external gearmotor.
FAQ
What roller diameter should an airport X-ray screening conveyor use?
SEAPARKS light-duty drum motors are available in Ø80 mm (TM80M, TM80A, DM80A), Ø113 mm (TM113M, TM113A, DM113A) and Ø138 mm (TM138A, DM138A). Because roller diameter sets belt height relative to the tunnel aperture, Ø80 mm is normally used where the scanner opening is fixed and the conveyor must sit low, while Ø113 mm and Ø138 mm provide higher belt pull for longer infeed and outfeed sections. The practical rule is to choose the smallest diameter that still delivers the required belt pull.
How is minimum roller width used in screening conveyor design?
Minimum roller width is the shortest pulley a model can be built to, and it is determined by the space needed for the internal gear stage and bearings. Within the SEAPARKS light-duty range it runs from 260 mm (TM80M) through 310 mm (TM113M, DM80A), 330 mm (TM80A), 335 mm (TM113A), 340 mm (TM138A) and 360 mm (DM113A). It sets how short a transfer section can be and how closely conveyors can be placed side by side.
Which protection class does a baggage handling drum motor need?
The light-duty SEAPARKS models TM80M, TM80A, DM80A, TM113M, TM113A, DM113A, TM138A and DM138A are specified to IP66/IP67/IP69, with carbon steel or 304 stainless steel housings. IP66 suits dry terminal and check-in hall conditions, IP67 adds tolerance to temporary immersion, and IP69 covers high-pressure jet cleaning. IP69K is a separate, higher washdown rating applied to the hygienic F-series models such as TM216F and DM216F.
Can a single-phase drum motor drive a security screening conveyor?
Yes, within its pull limits. TM80M is a single-phase asynchronous drum motor with a polymer gear stage delivering 0.034–0.11 kW and a maximum belt pull of 630 N; TM113M is also single-phase and reaches 0.12–0.18 kW with a maximum belt pull of 770 N. These are suited to short tray-return, secondary search and low-pull screening sections. Where belt pull requirements exceed those figures, the three-phase TM113A (1469 N) or DM113A (2053 N) becomes the appropriate choice.
What belt speed suits tray positioning in an X-ray tunnel?
Belt speed is fixed by the gear ratio selected at order, so the acceptable band must be confirmed before manufacture. Light-duty models offer overlapping bands: 0.05–0.85 m/s (TM80M), 0.08–1.02 m/s (TM80A), 0.16–1.03 m/s (DM80A), 0.11–1.05 m/s (TM113M), 0.09–1.4 m/s (TM113A), 0.14–0.68 m/s (DM113A) and 0.11–1.69 m/s (TM138A). Screening applications generally sit at the lower, more stable end of these bands, consistent with the low-vibration and precise-positioning requirements recorded for airport security inspection equipment.
When is a drum motor the wrong choice for an airport conveyor?
A drum motor is a poor fit where the frame does not allow the pulley to be removed for service, where belt pull exceeds the light-duty ceiling of the selected model, or where the gear ratio may need to change after installation. It is also unsuitable for continuous very-low-speed, high-torque duty and for abrasive heavy-industry applications where external gearmotors with replaceable components remain more practical. In these cases a conventional gearmotor and chain drive is the more defensible engineering decision.
Which certifications should be verified for a European airport project?
Drives placed on the European market must comply with the Low Voltage Directive 2014/35/EU and bear the CE mark, with safety standards such as EN 62841 or IEC 60034-1 commonly referenced in technical files. SEAPARKS holds ISO 9001, ISO 14001, ISO 45001, RoHS 2.0, UL and CE certification, and is recognised as a National High-tech Enterprise and a Tianjin Municipal Enterprise Technology Center.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.